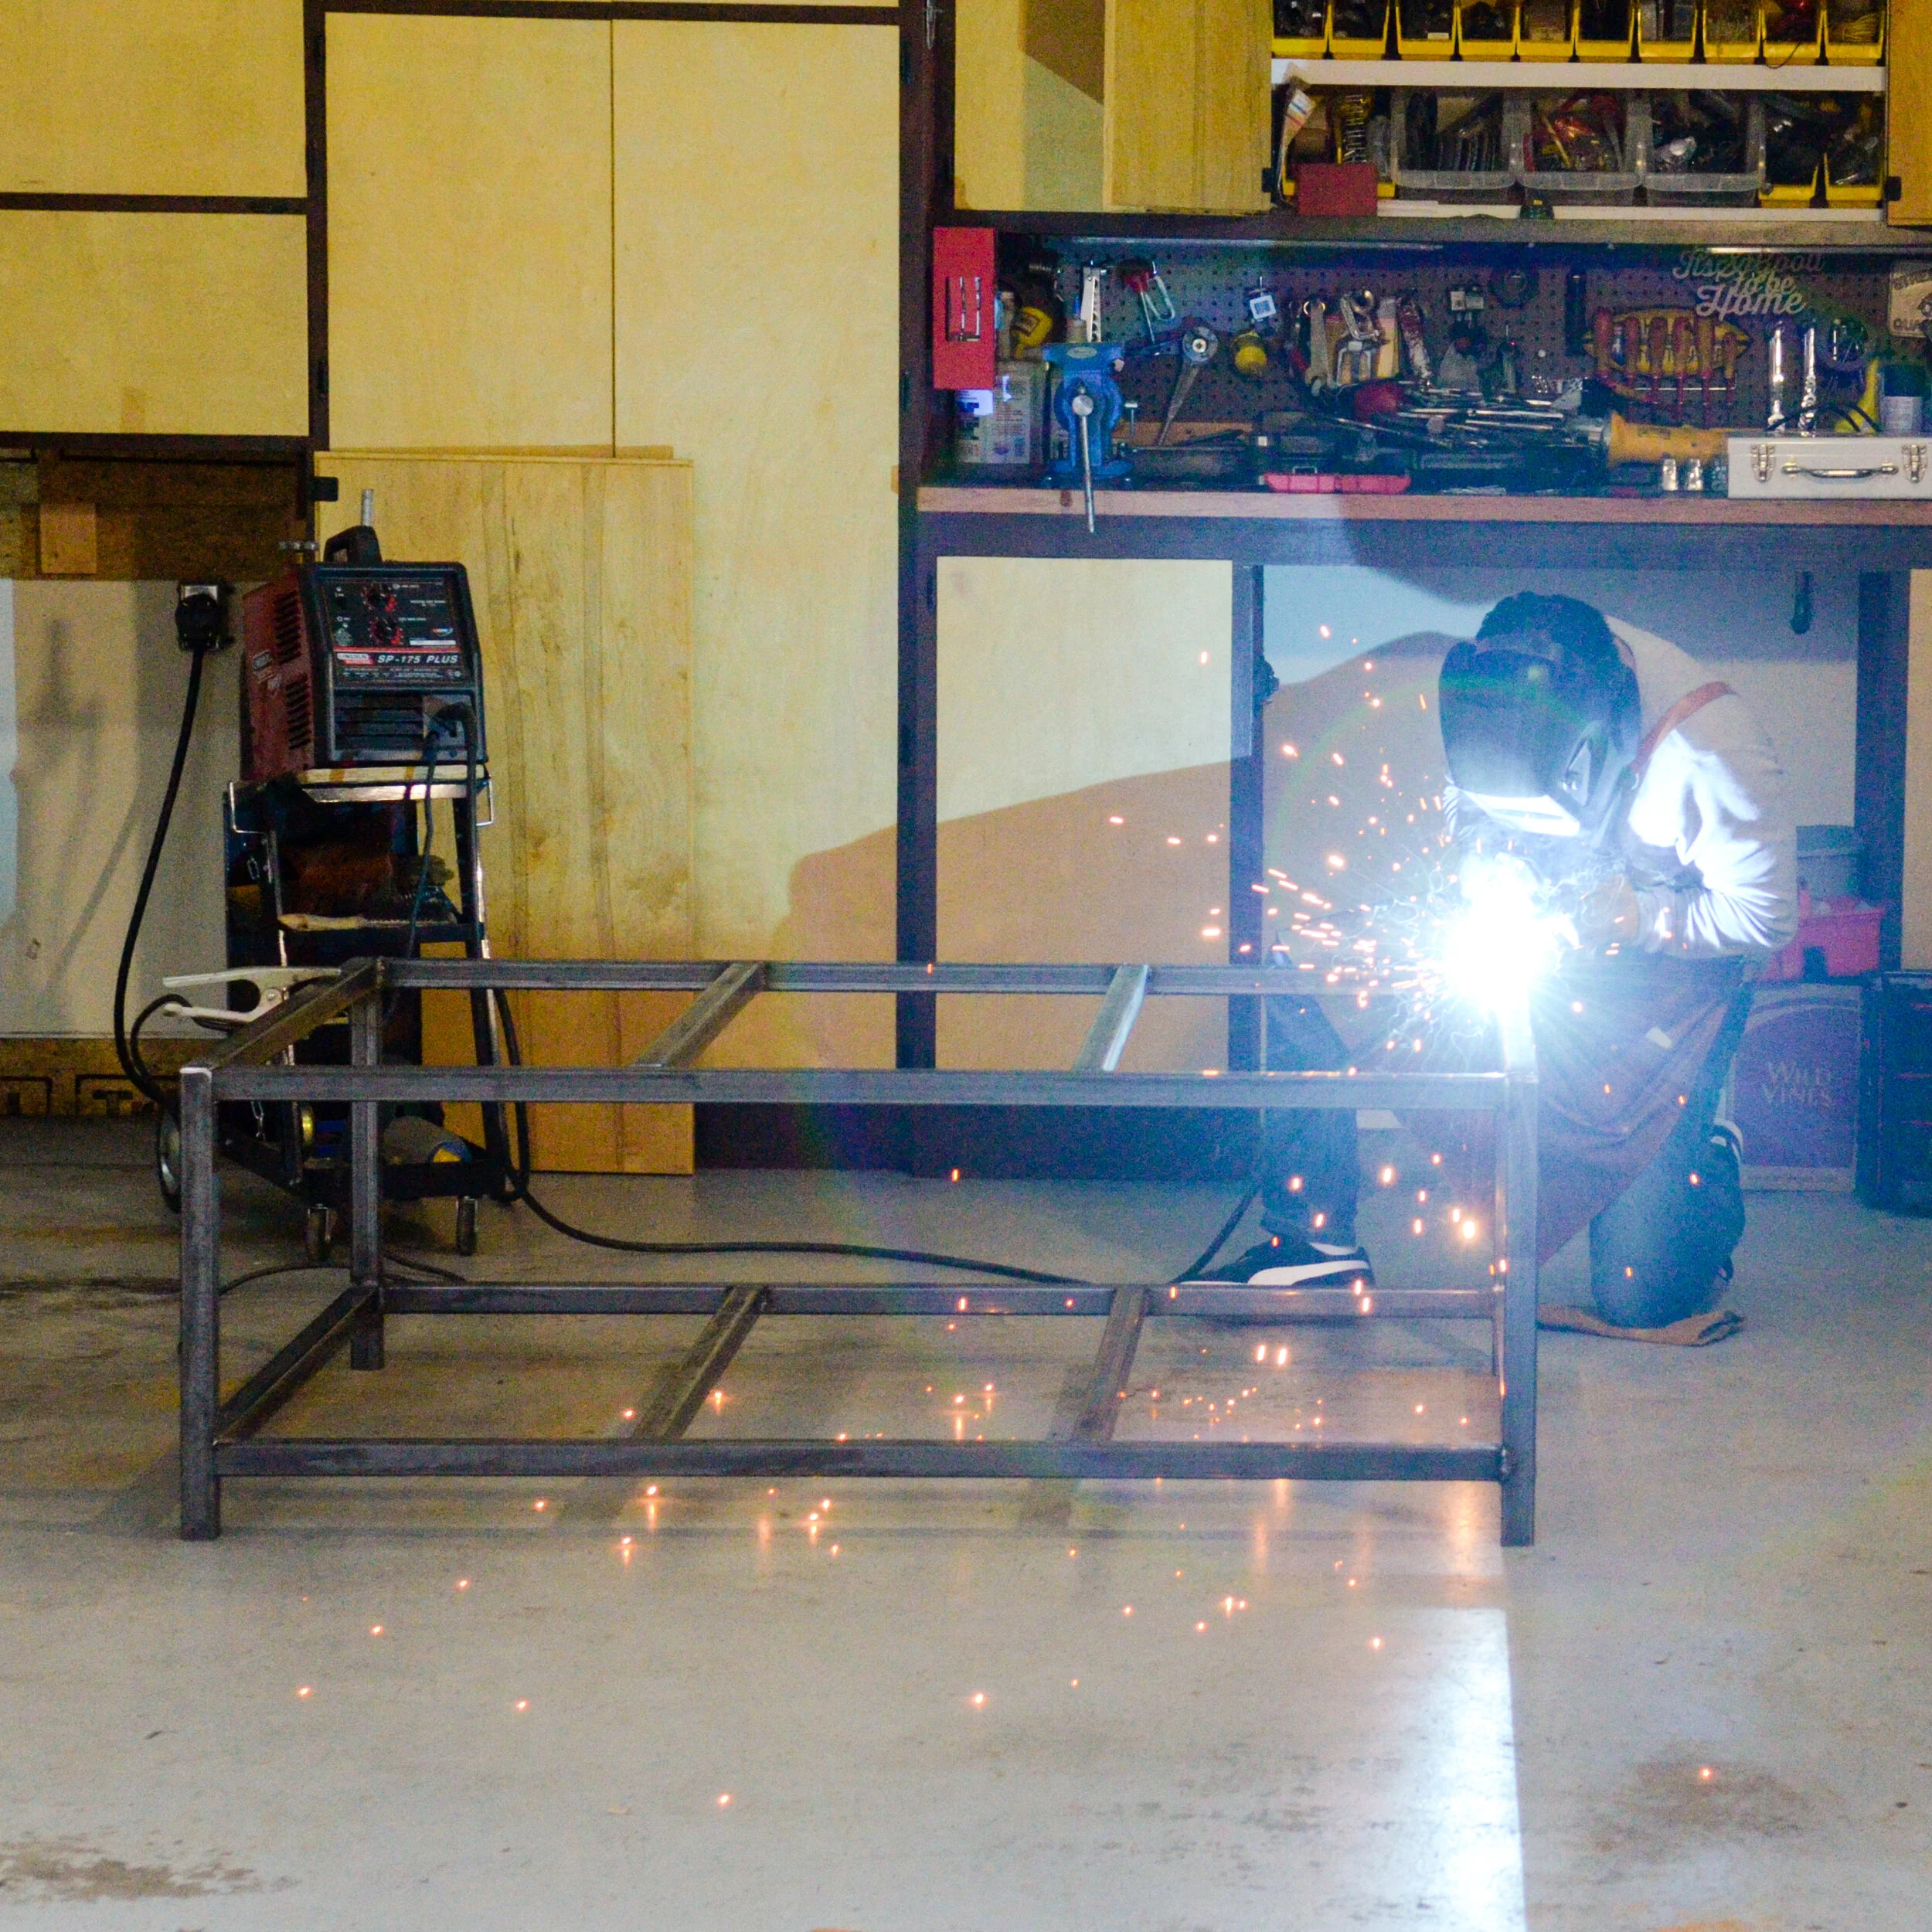
Welded Steel Base for CNC Machine
As I start exploring digital woodworking and automation through the use of a 4’x4’ CNC spindle machine. I made a welded steel base to support the CNC machine that I’ll be receiving in late June of 2020.
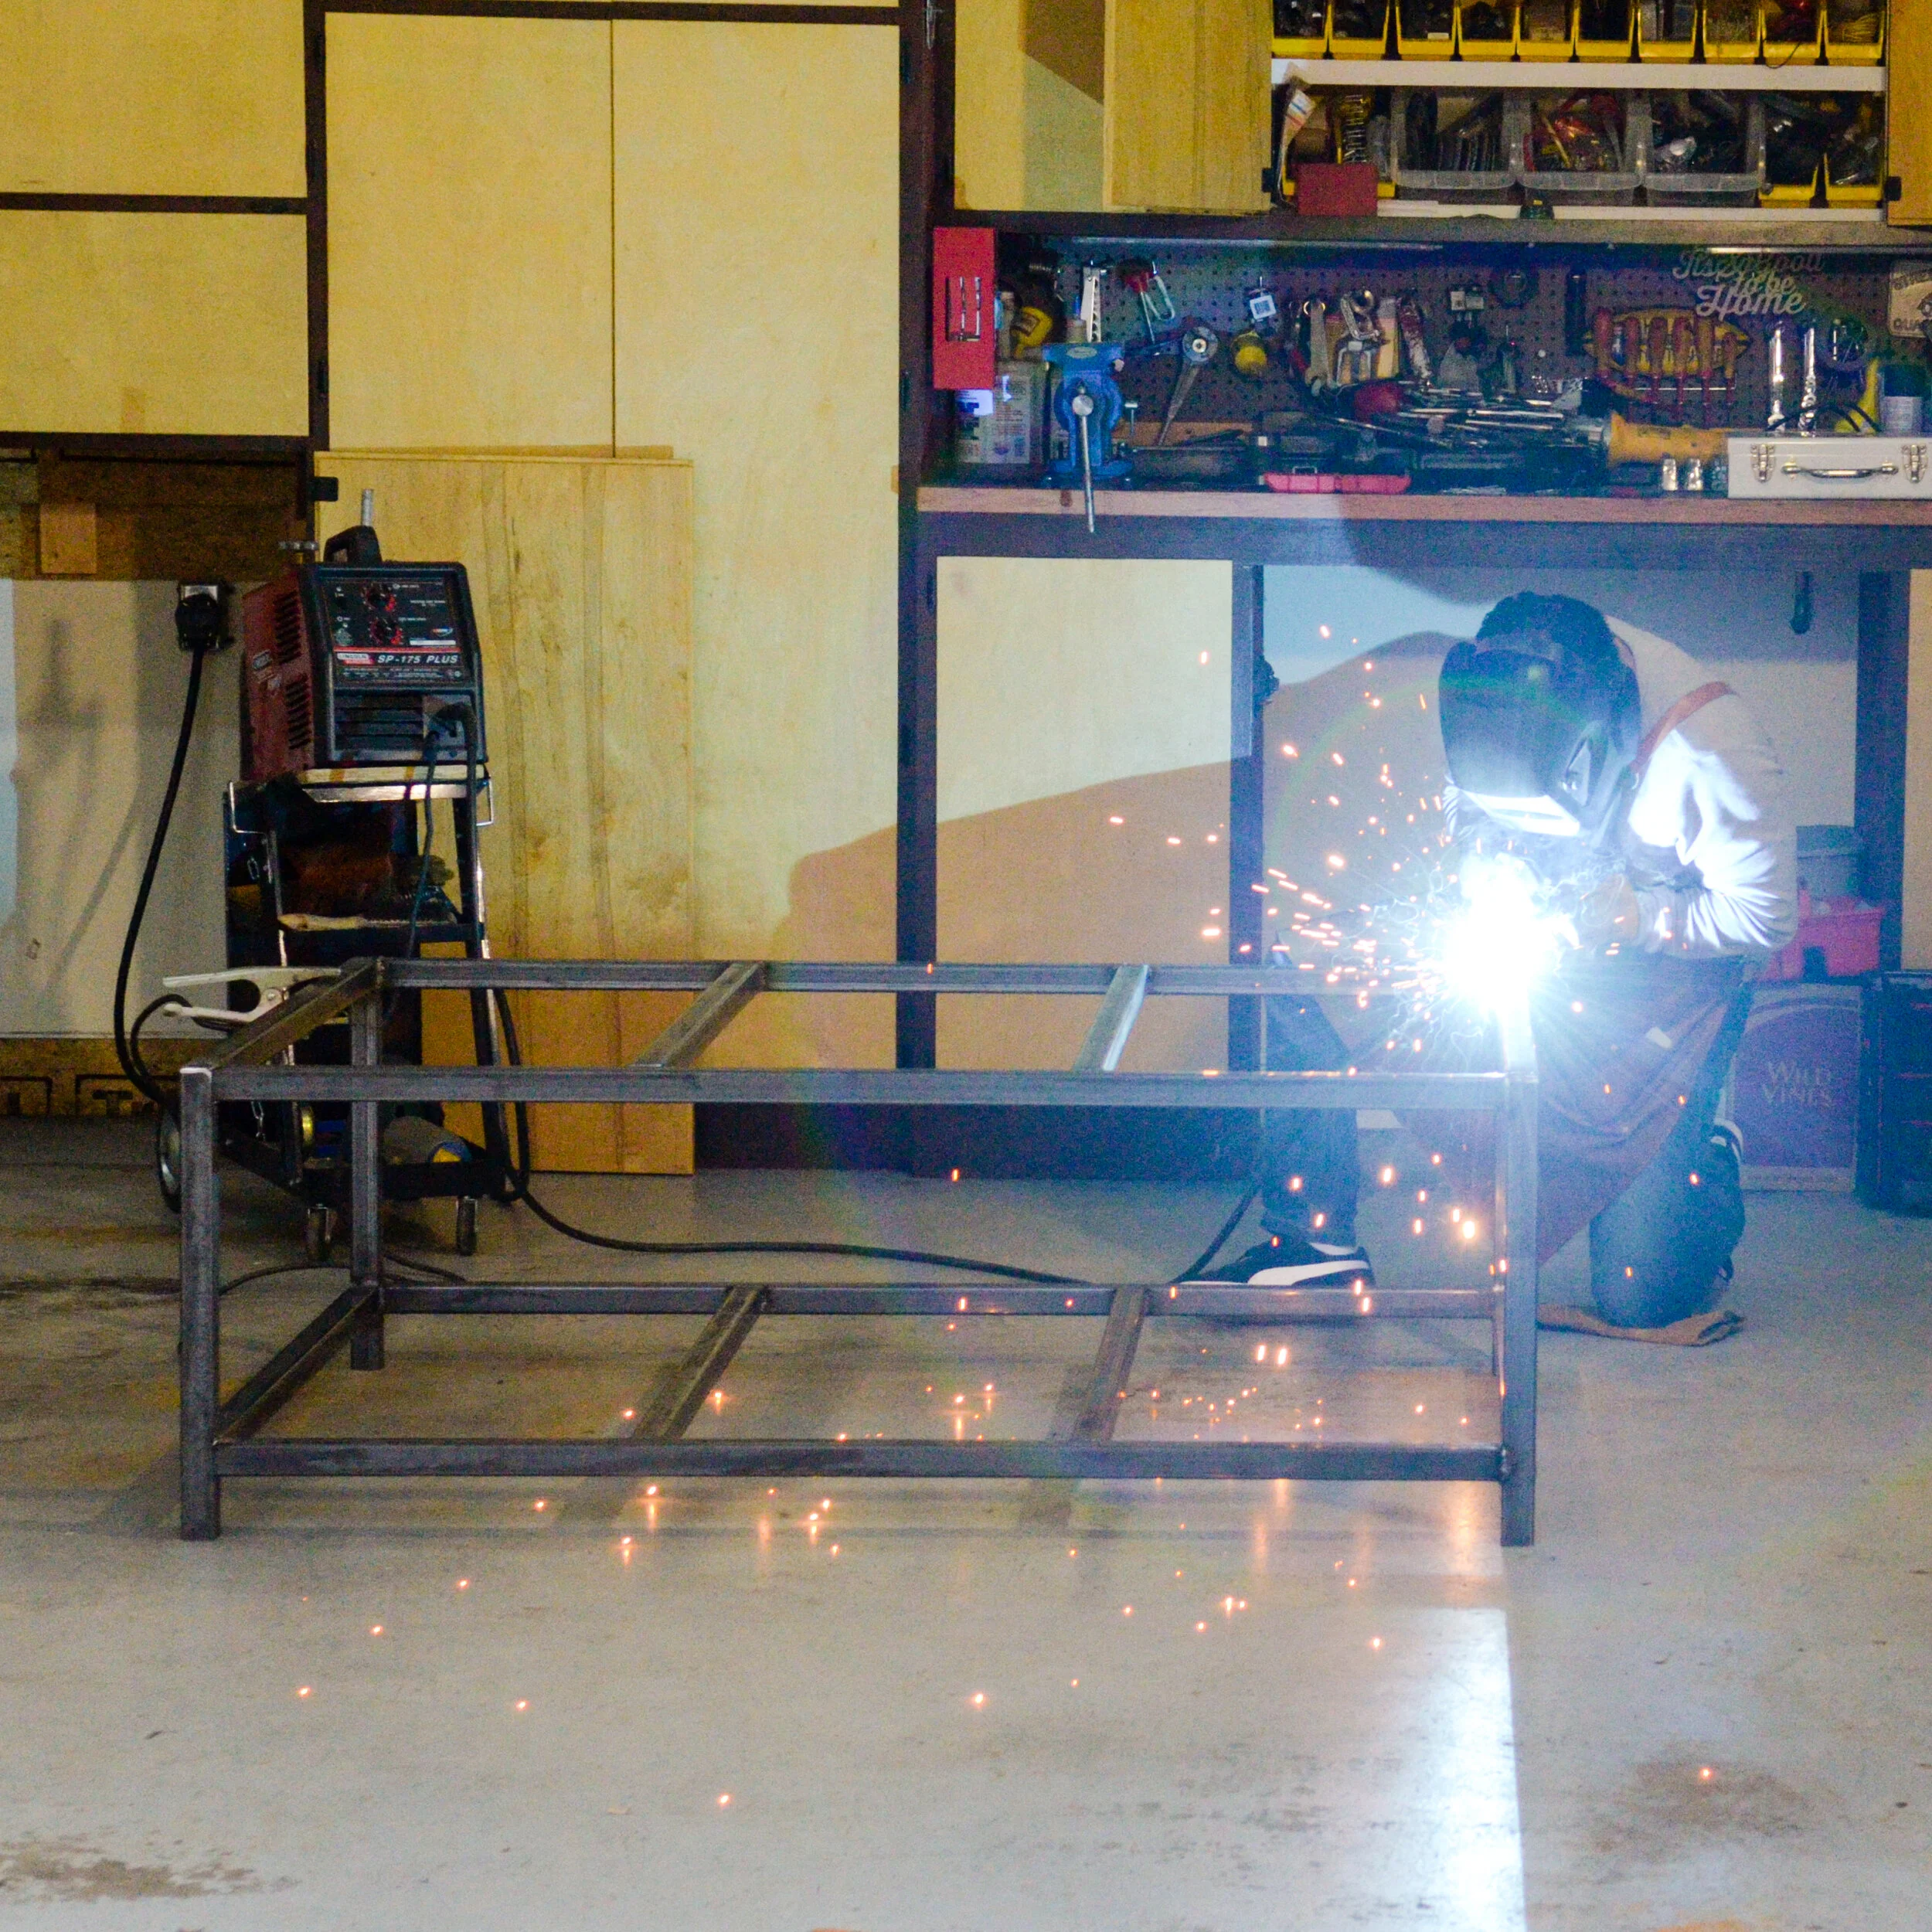
Building a welded steel base for a 4’x4’ CNC spindle machine.
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
In the fall of 2019, I asked a custom CNC builder, Carl Bruce of SpeedLine CNC in Seattle, WA, to build me a budget friendly small shop CNC capable of producing furniture pieces. He advised me to go with a 4’x4’ CNC and for me to build a welded steel table for the CNC machine sit atop. I knew nothing about working with metal or welding, so I contacted my friend, David Moncada @rocketcitywoodshop, to help me with this build.
David has built several steel frames for his woodworking equipment. Under his advice, I built a “welding jig structure” out of OSB to ensure my 1-1/2” steel tubing remains square as I weld them together.
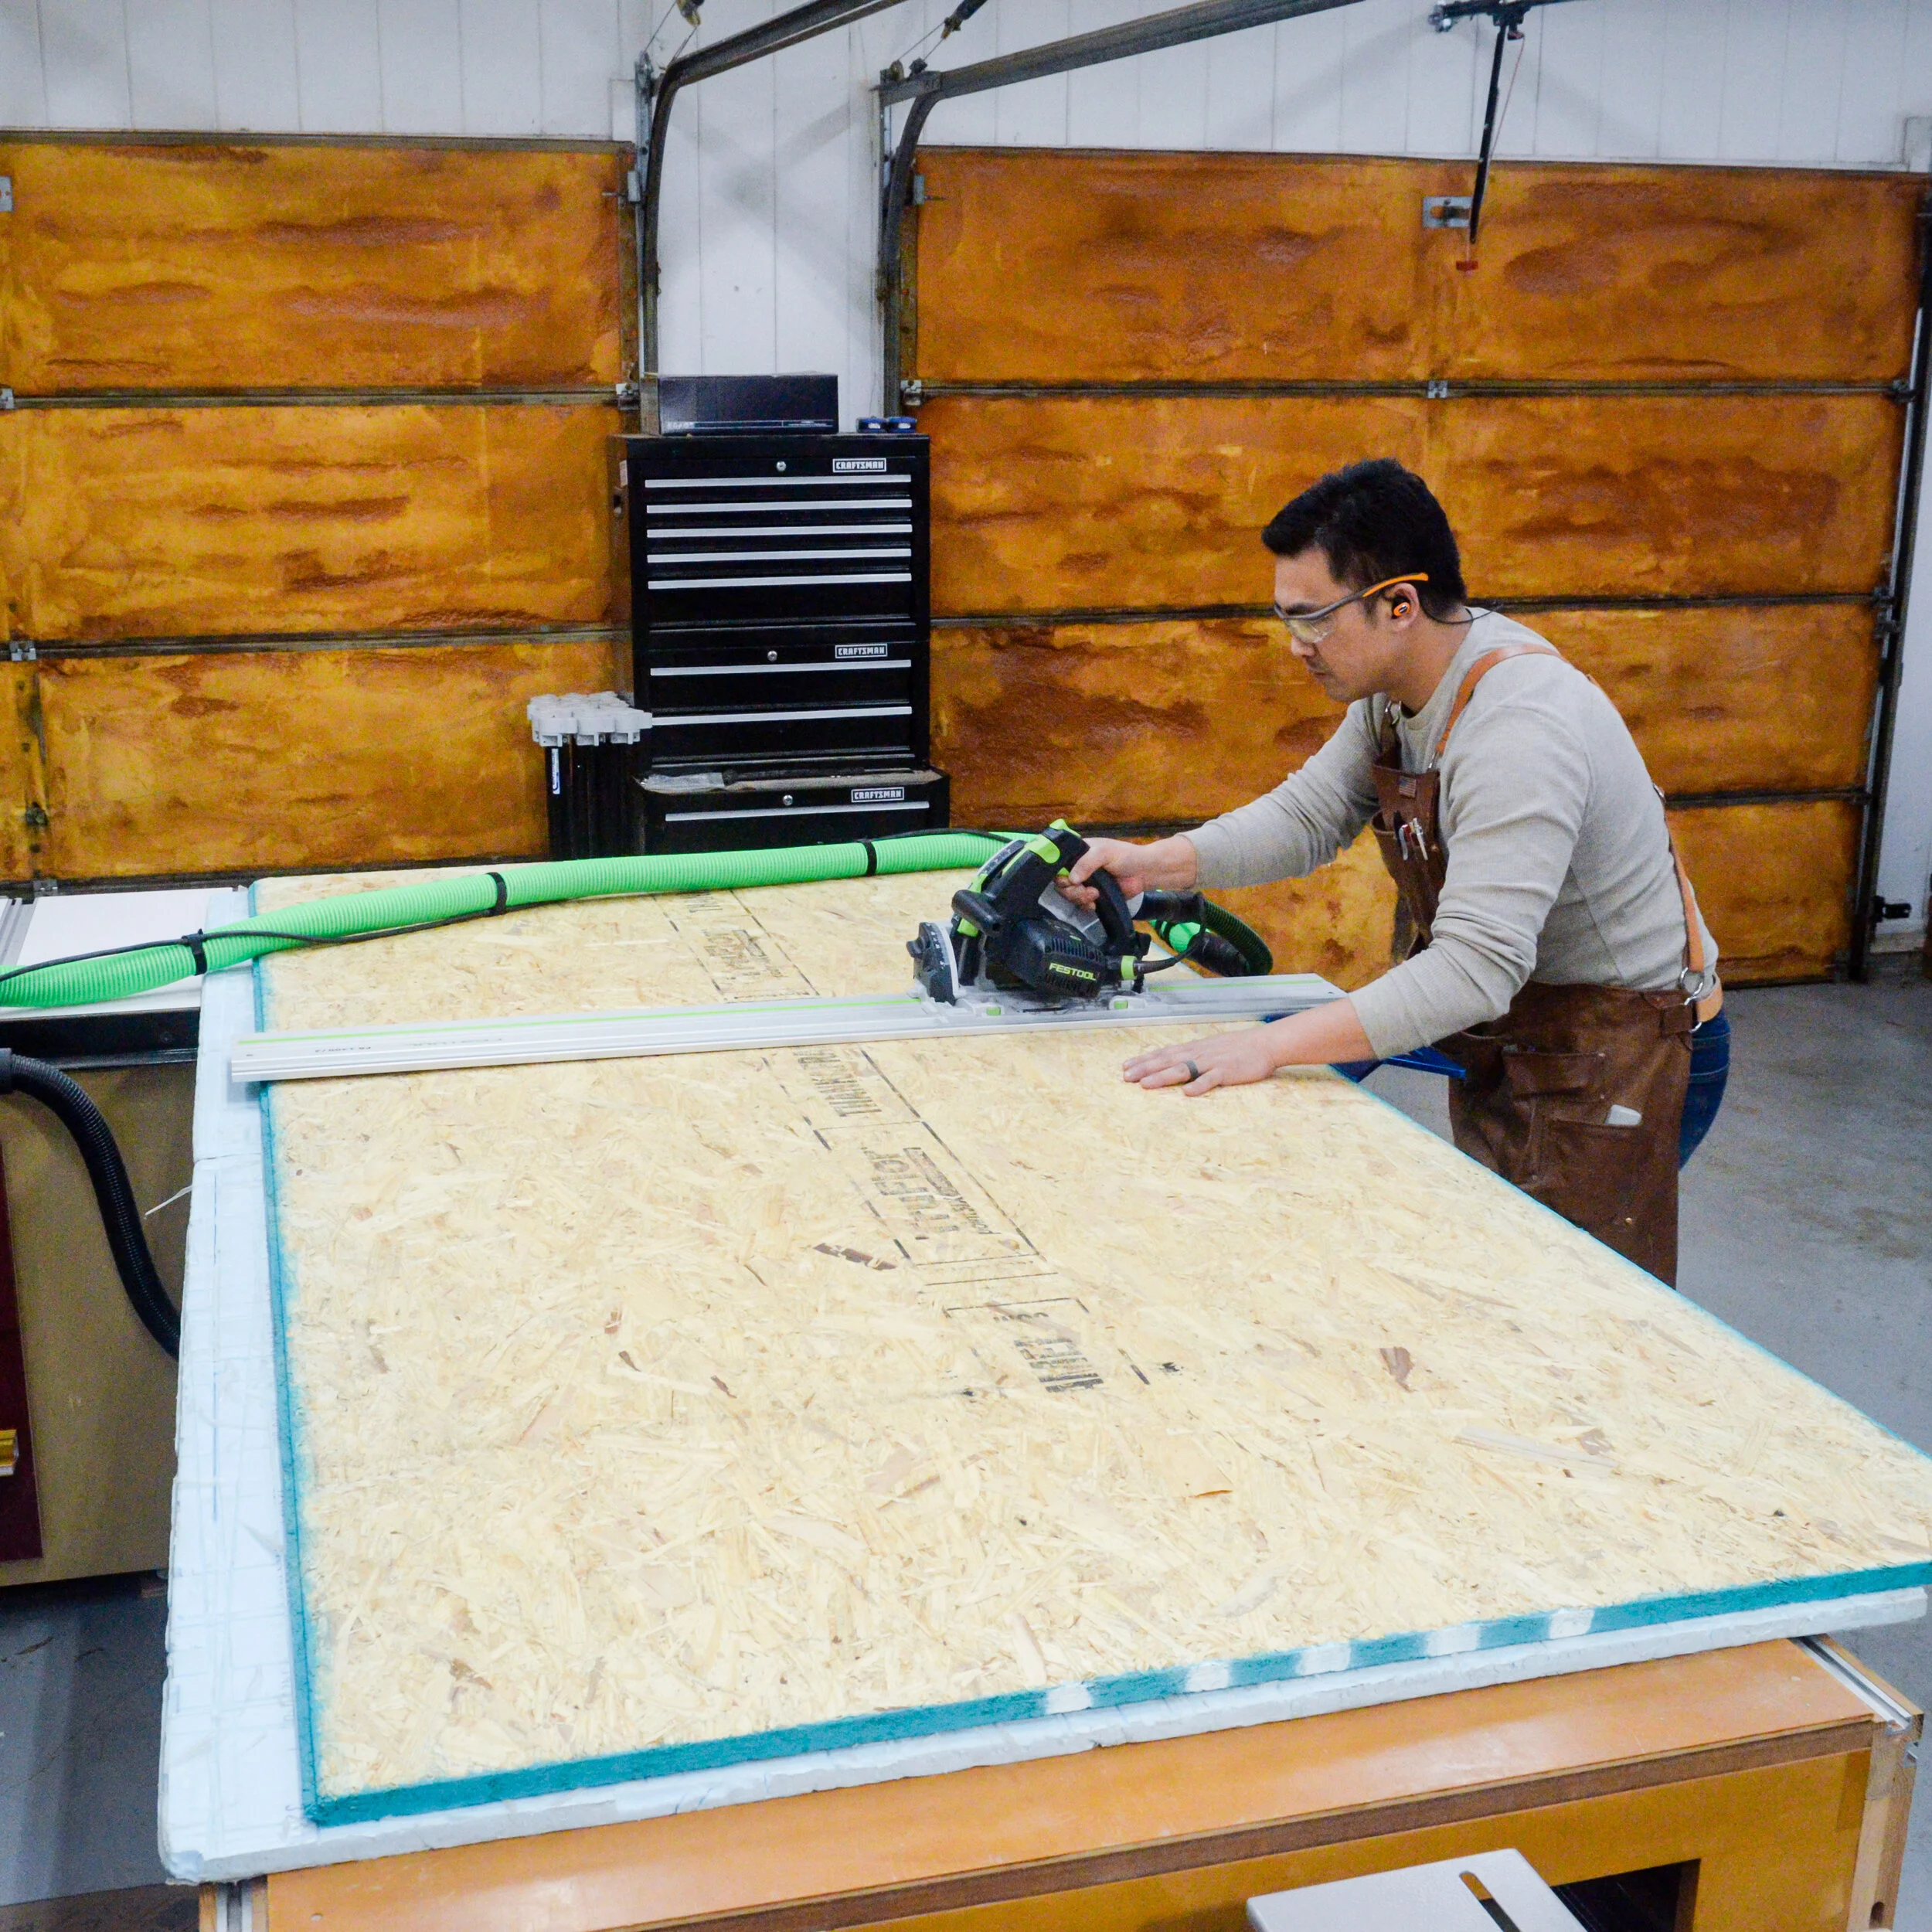
I first broke down a full sheet of OSB with a track saw. This made the OSB more manageable, where I can cut the sheet down more precisely at the table saw.
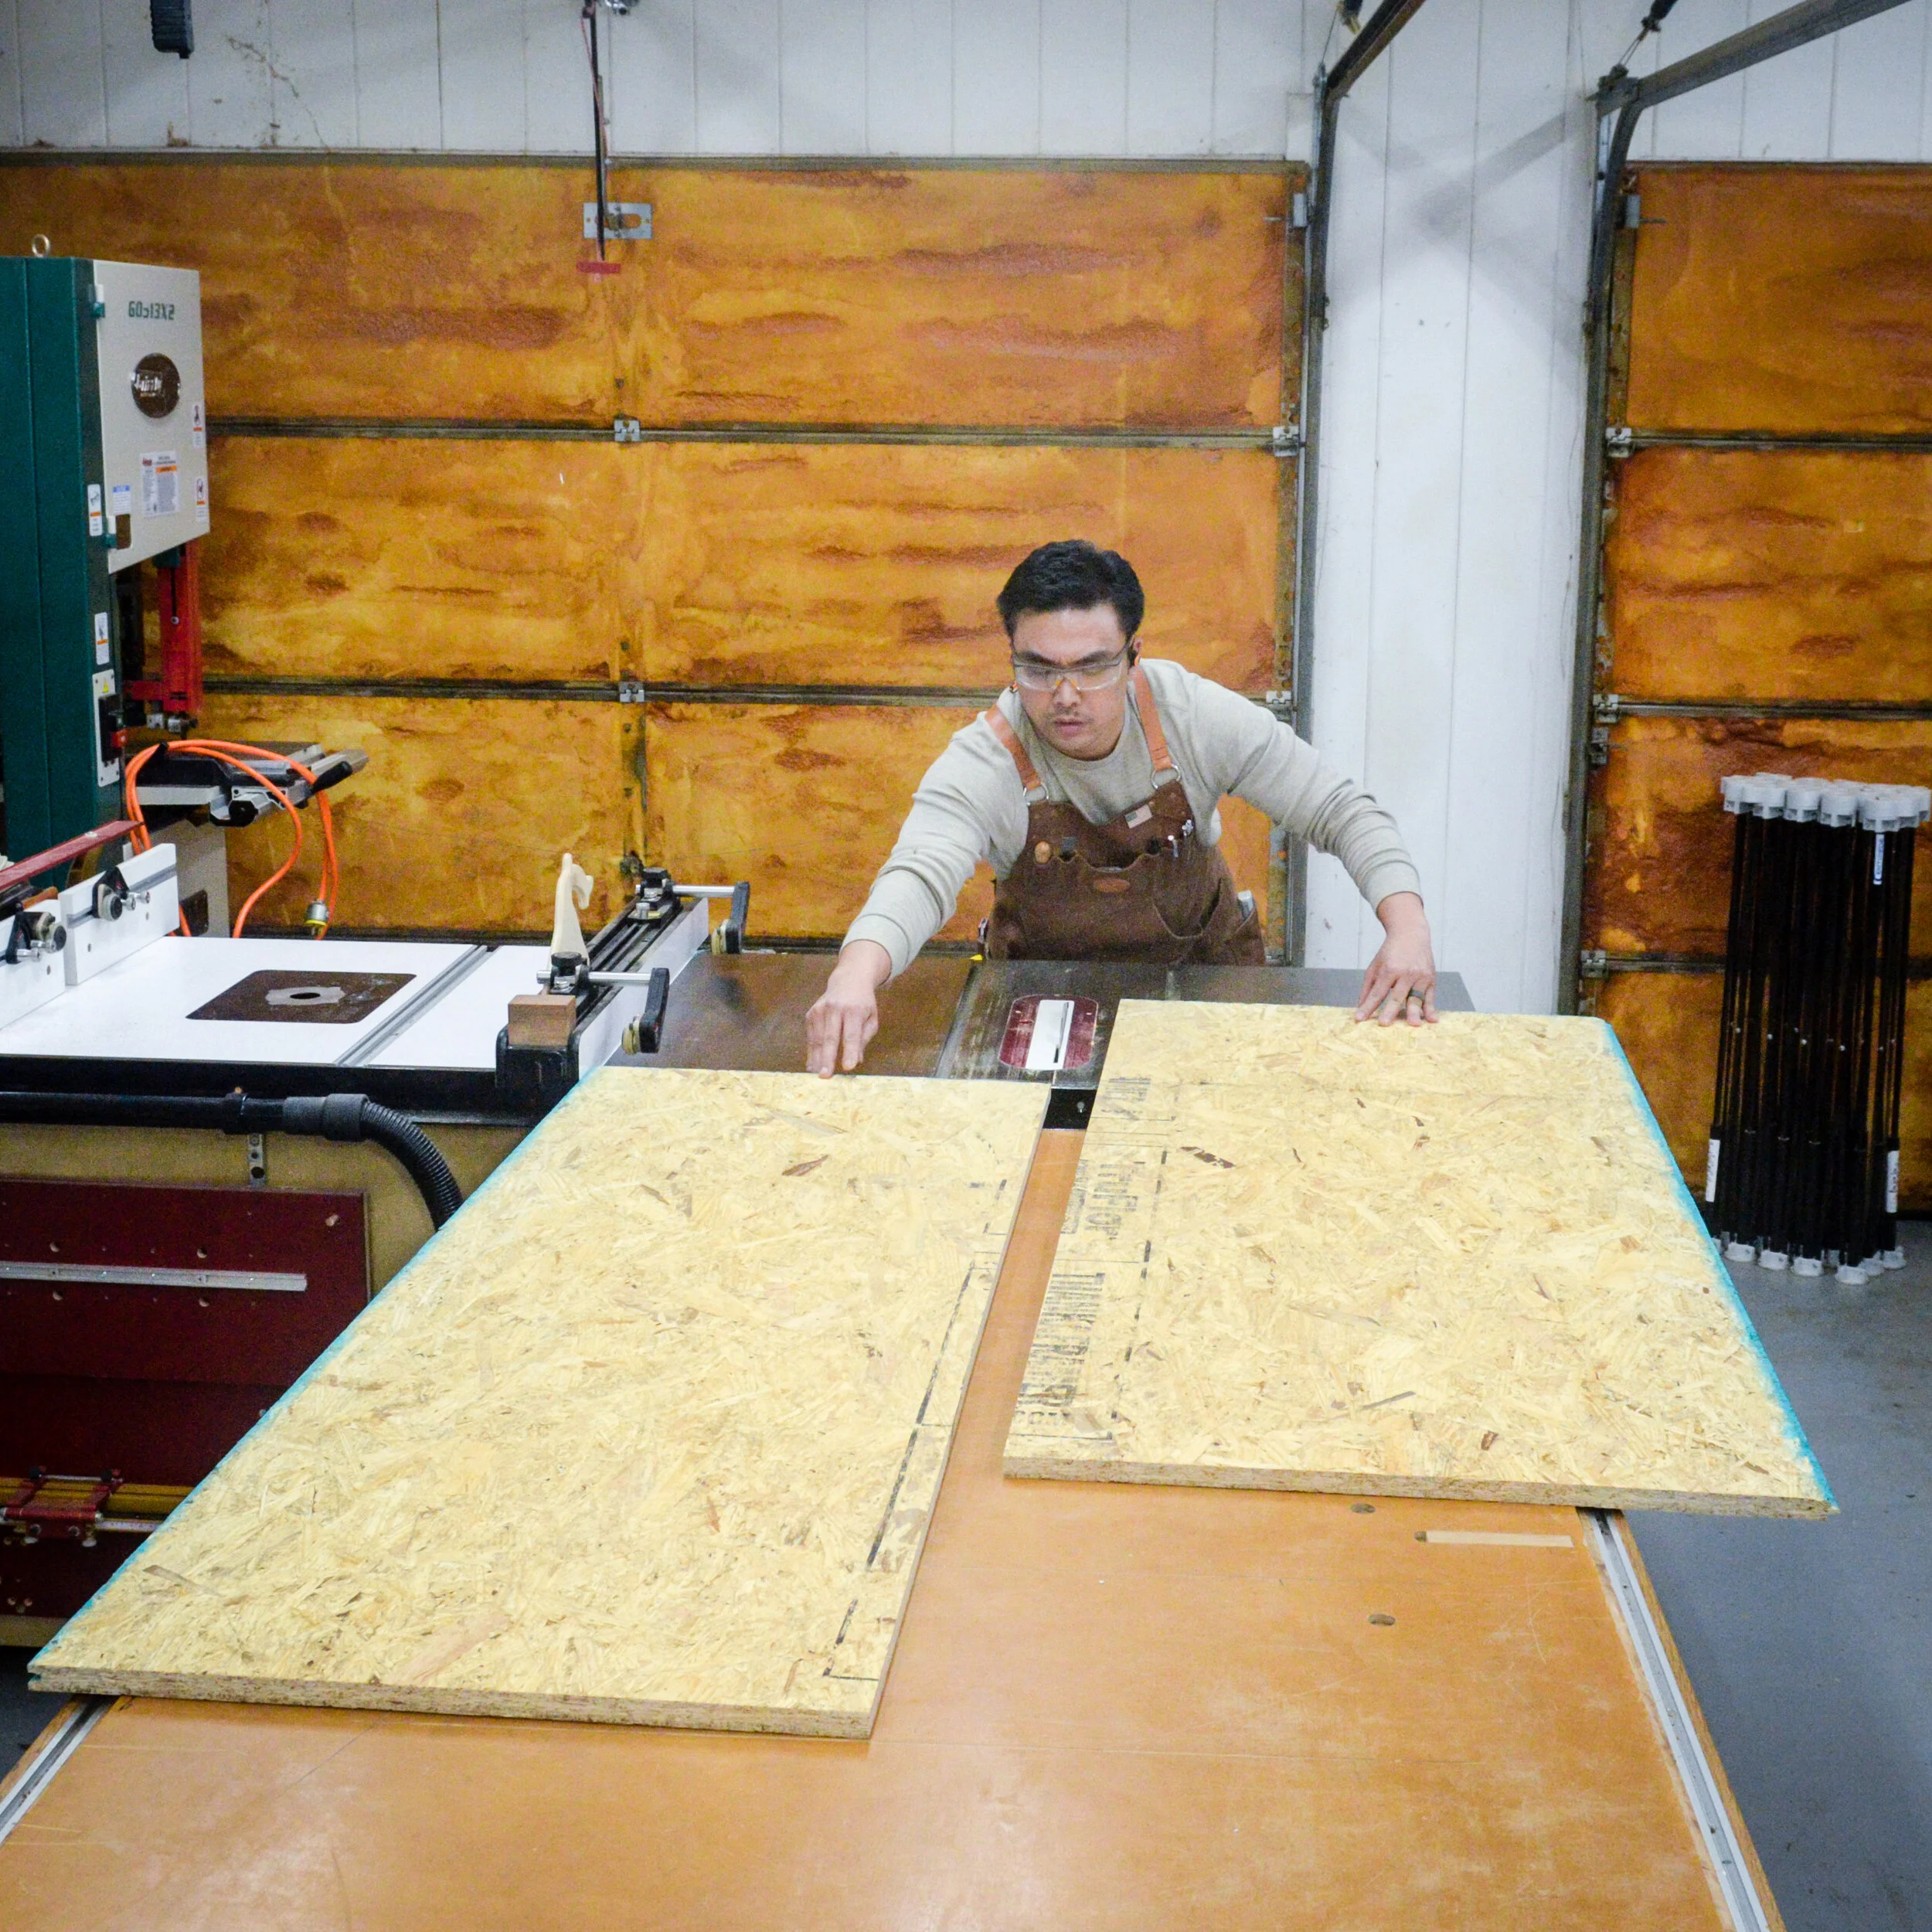
Making final cuts on the table saw.
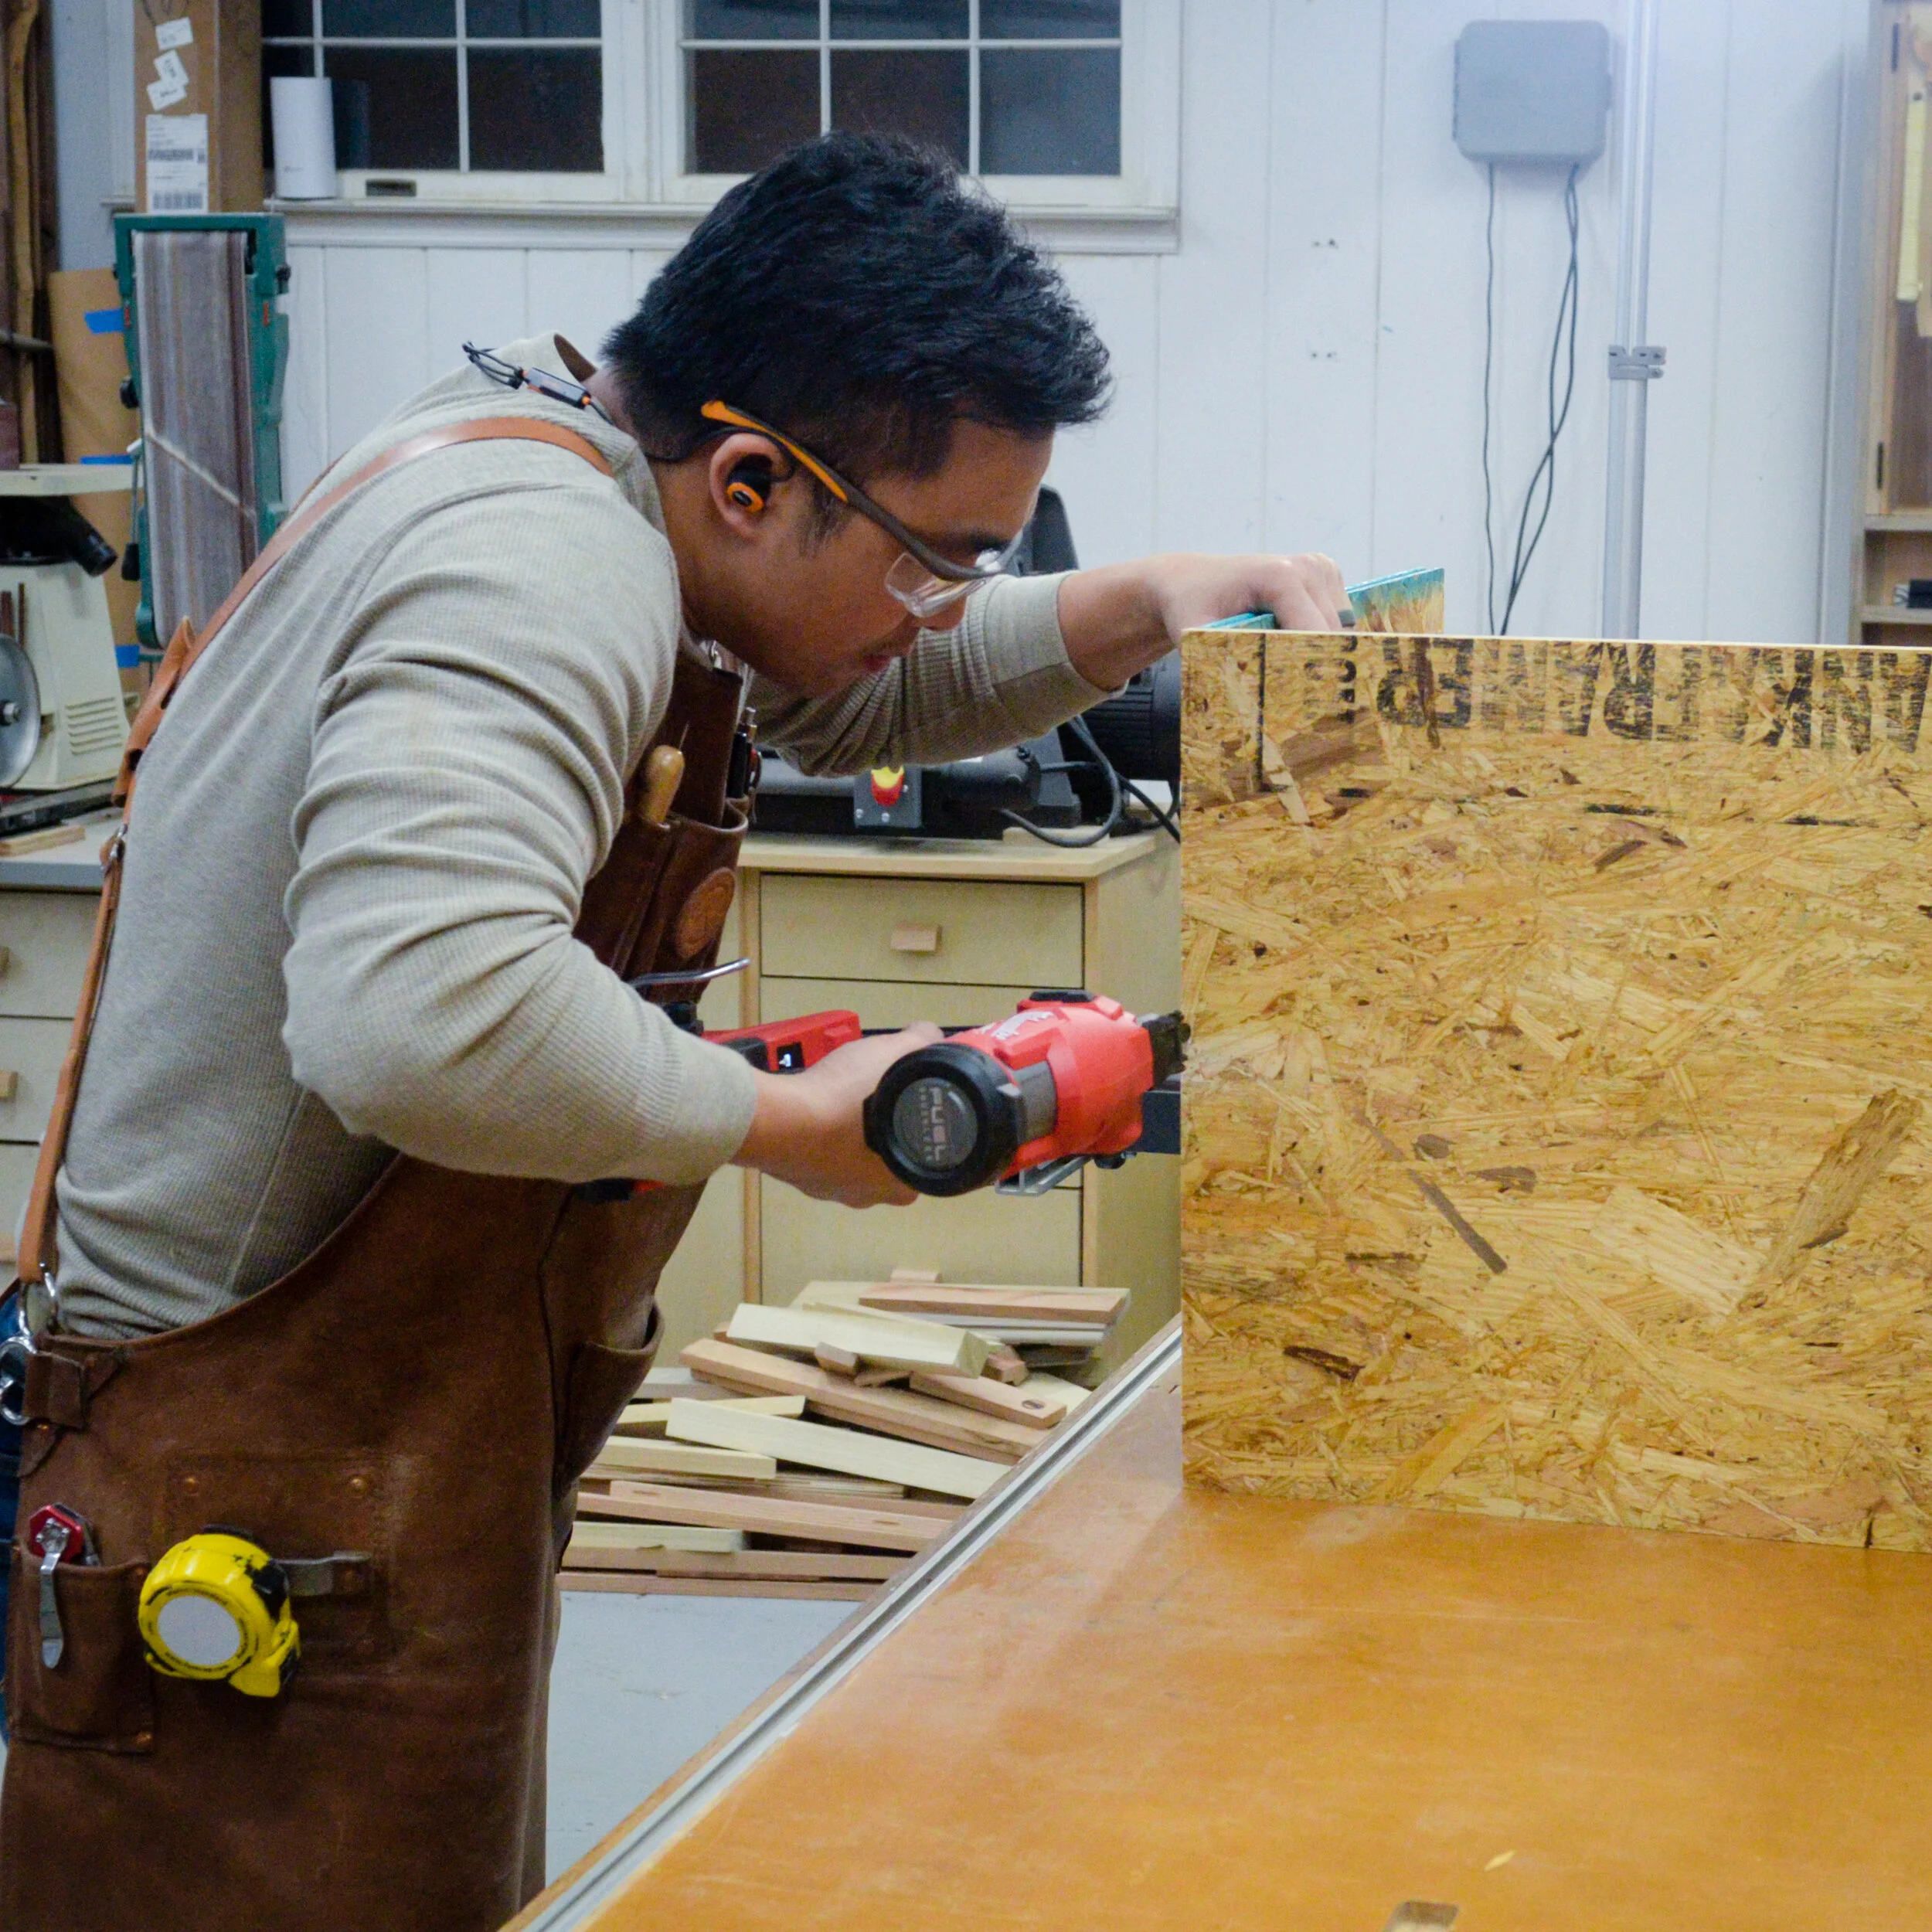
The pieces of the welding jig structure are first glued and brad nailed to tack the pieces together.
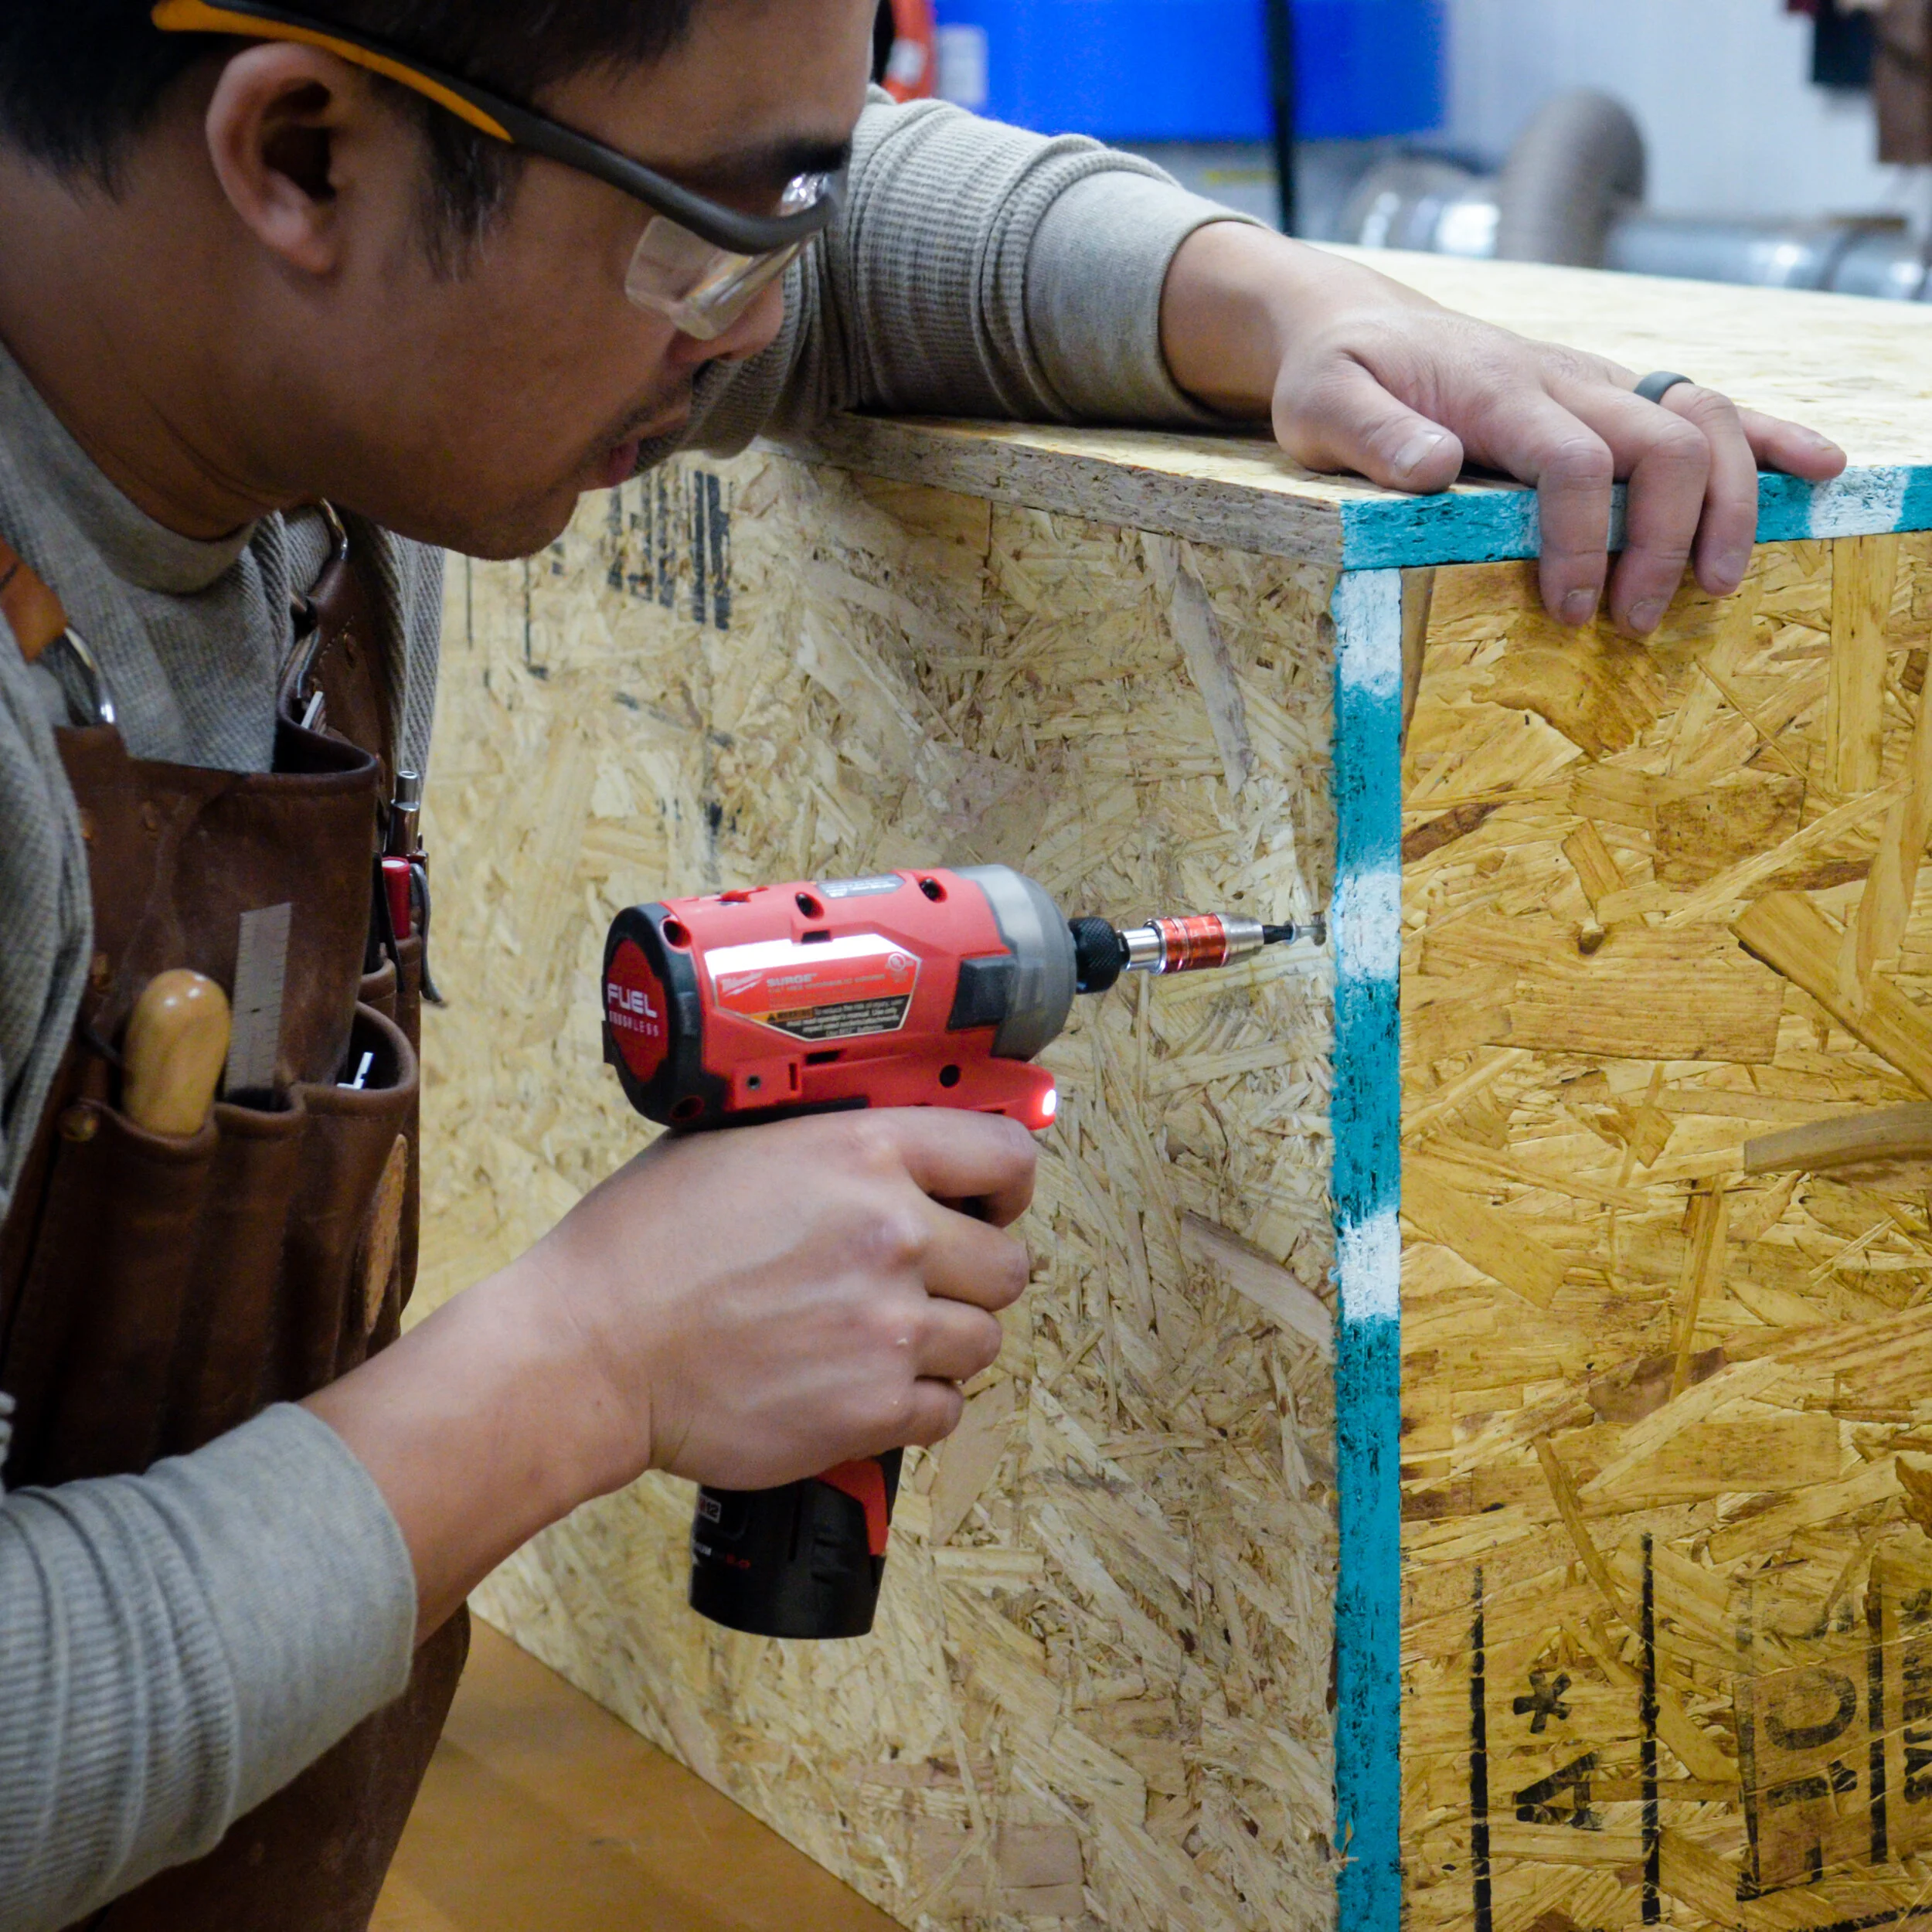
The butt joints are reinforced with torx head construction screws.
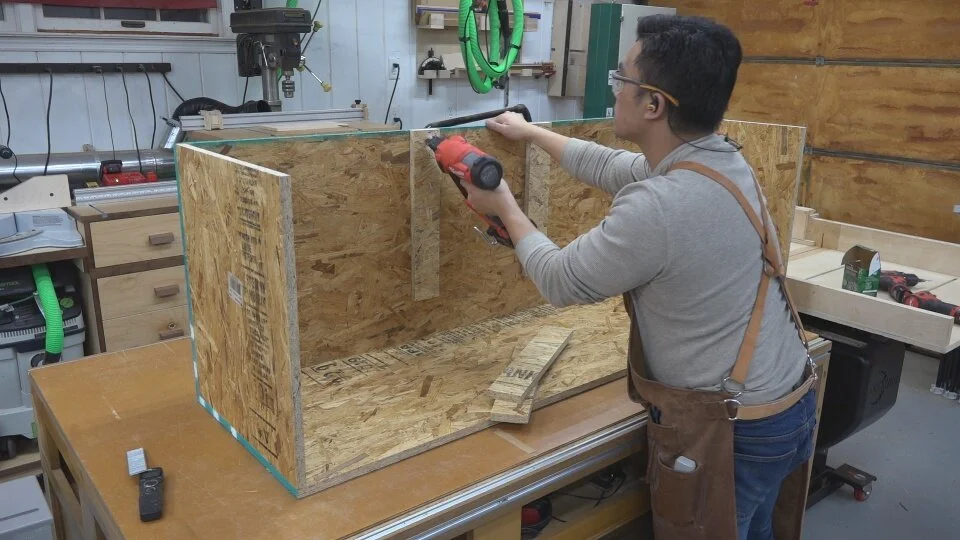
OSB strapping is glued and brad nailed to the inside of the welding jig structure to reference and locate the two middle cross-supports.
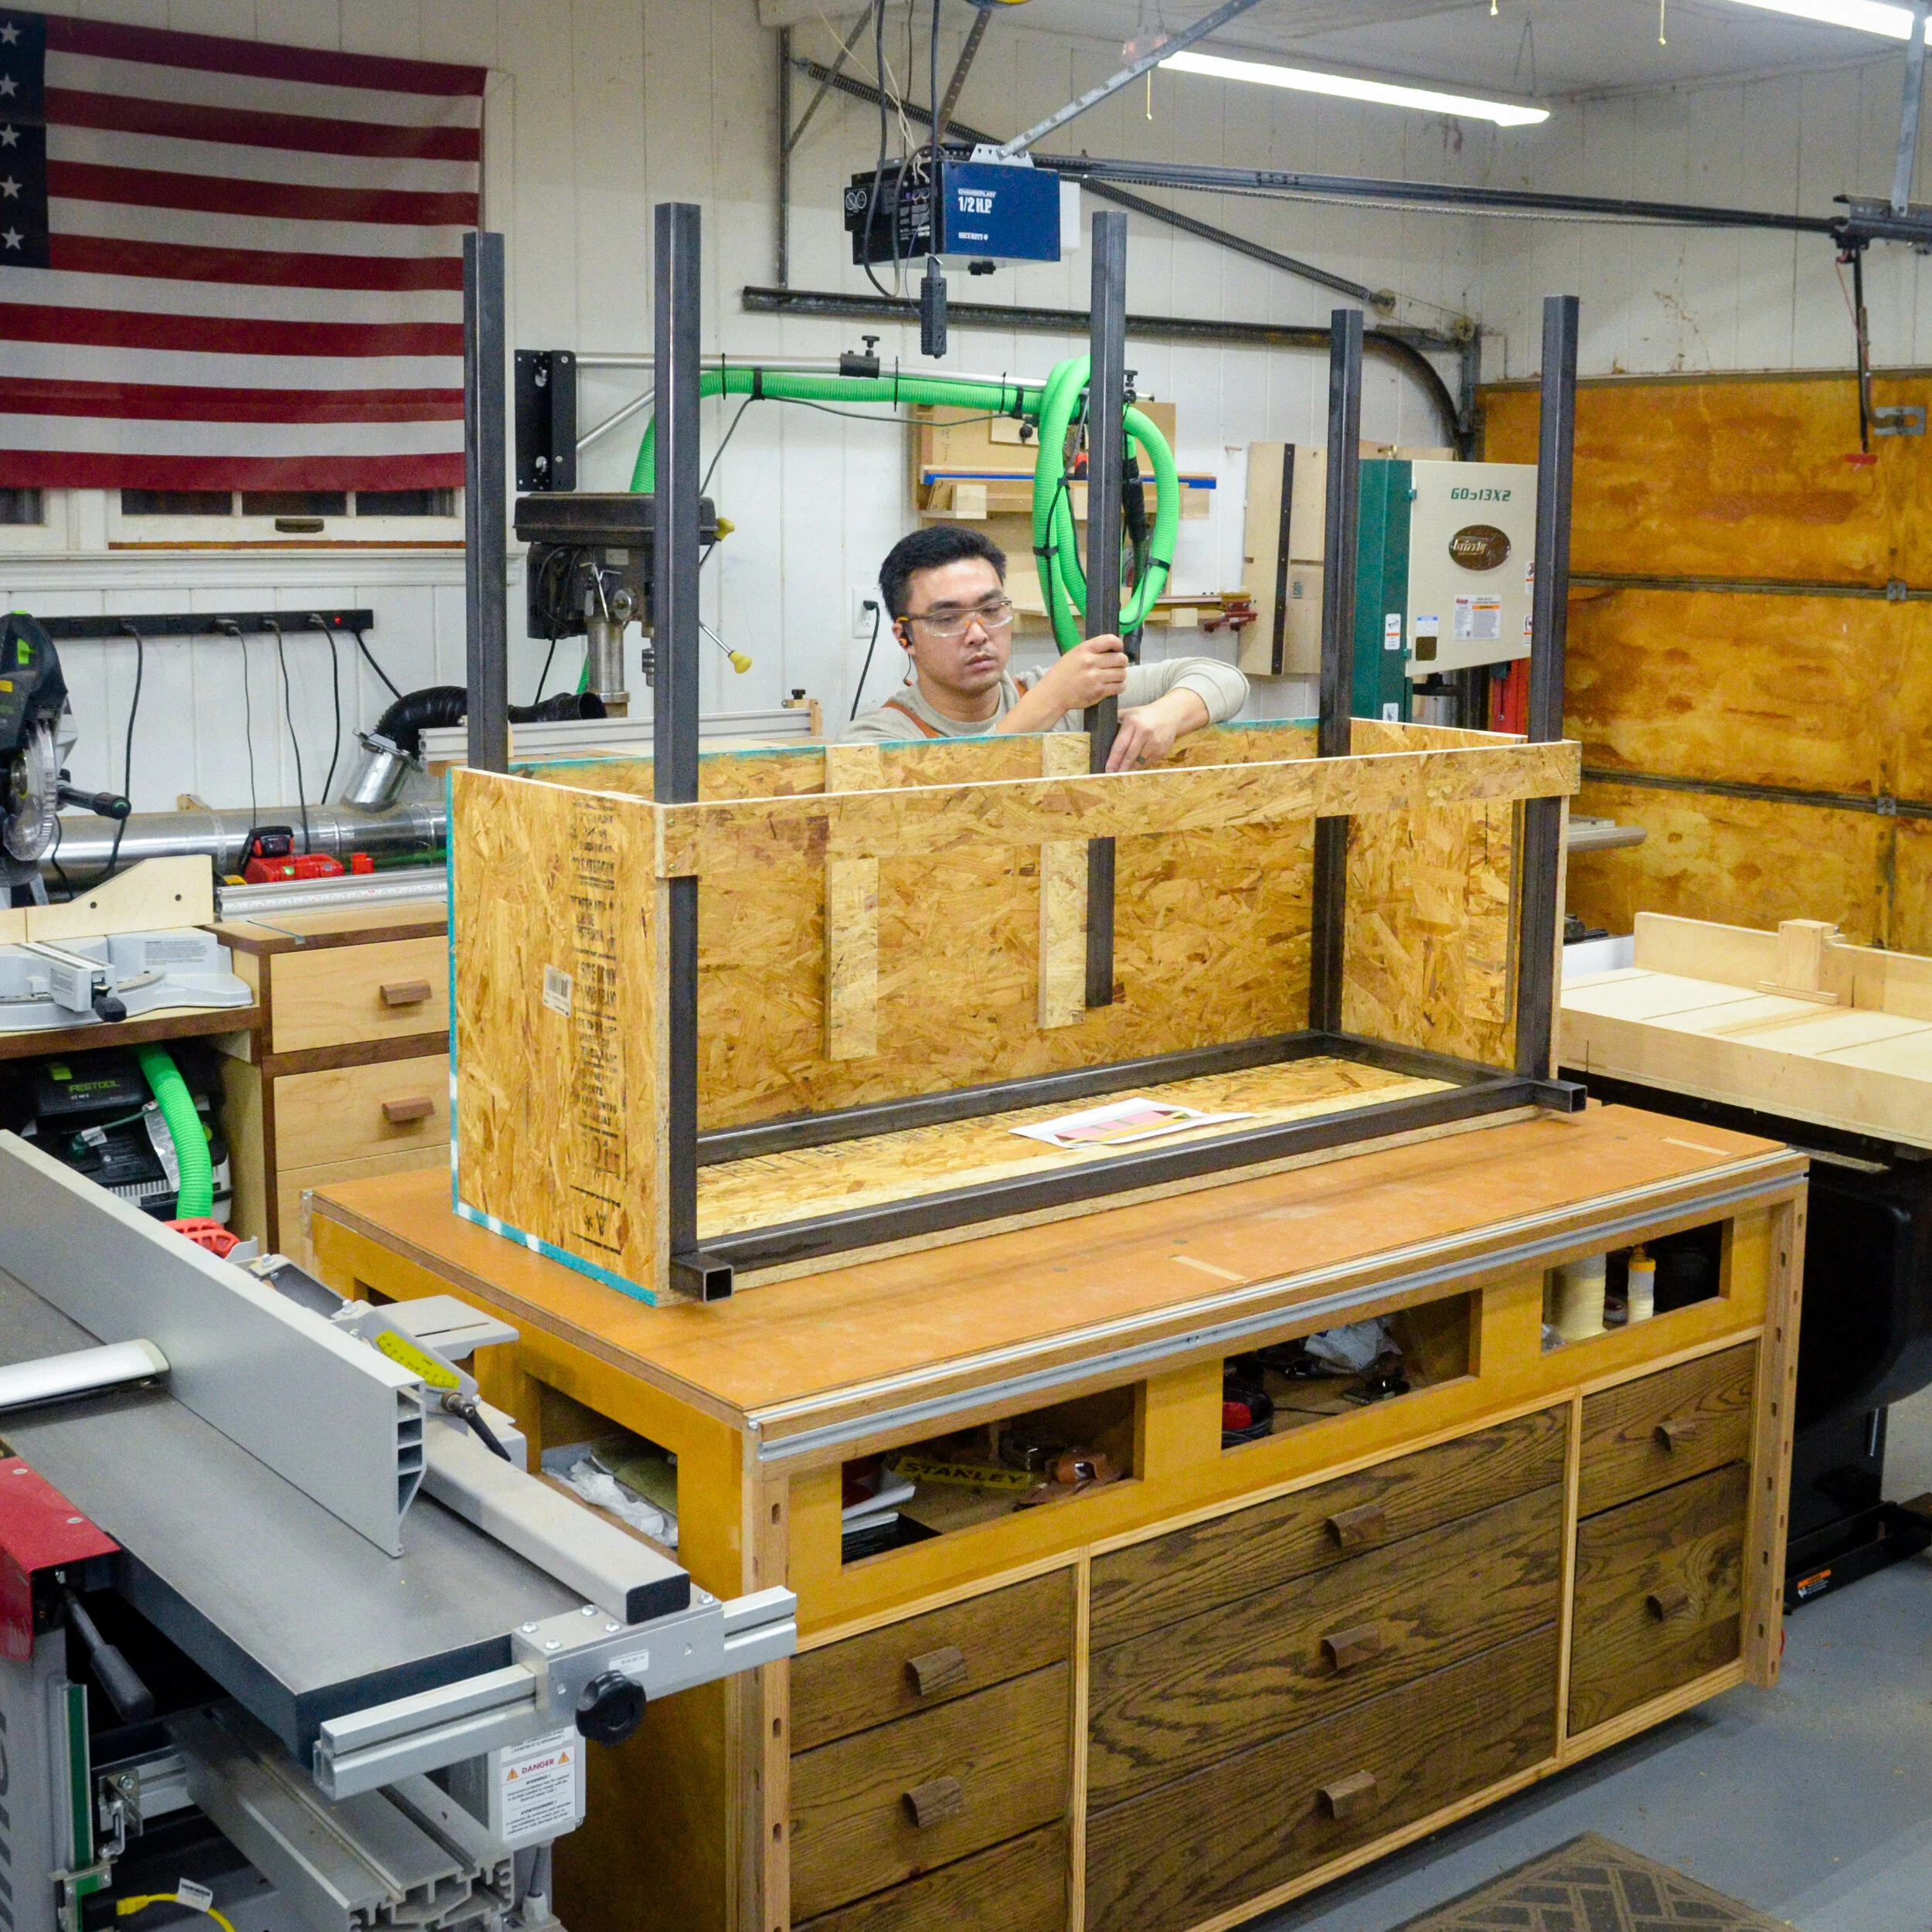
The completed welding jig structure holds the steel tubing in place while it’s being welded.
I used 1-1/2" square steel tubing with a wall thickness of 1/8." I was fortunate enough to have the steel tubing cut to size from the vendor. However, I cut the 1/8" thick steel strapping at my shop. To cut the steel strapping, I used the Diablo 5-1/2 in. x 30-tooth metal cutting saw blade with bushings. This blade is made to cut steel studs, angle iron, channel, flat bar, and threaded rod up to 1/8" wall thickness. The blade includes three bushings allow it to be used on 1/2 in., 5/8 in., 10 and 20 mm saw arbors. Most importantly, the TiCo hi-density carbide is designed for mild steel with 40x longer life. The Diablo metail cutting blade also comes in a 5-3/8 in. x 30-tooth version. To trim pieces once they were welded as end caps to the steel tubing, I used the AvantiPRO 4-1/2 in. carbide metal cutting wheel on my angle grinder.
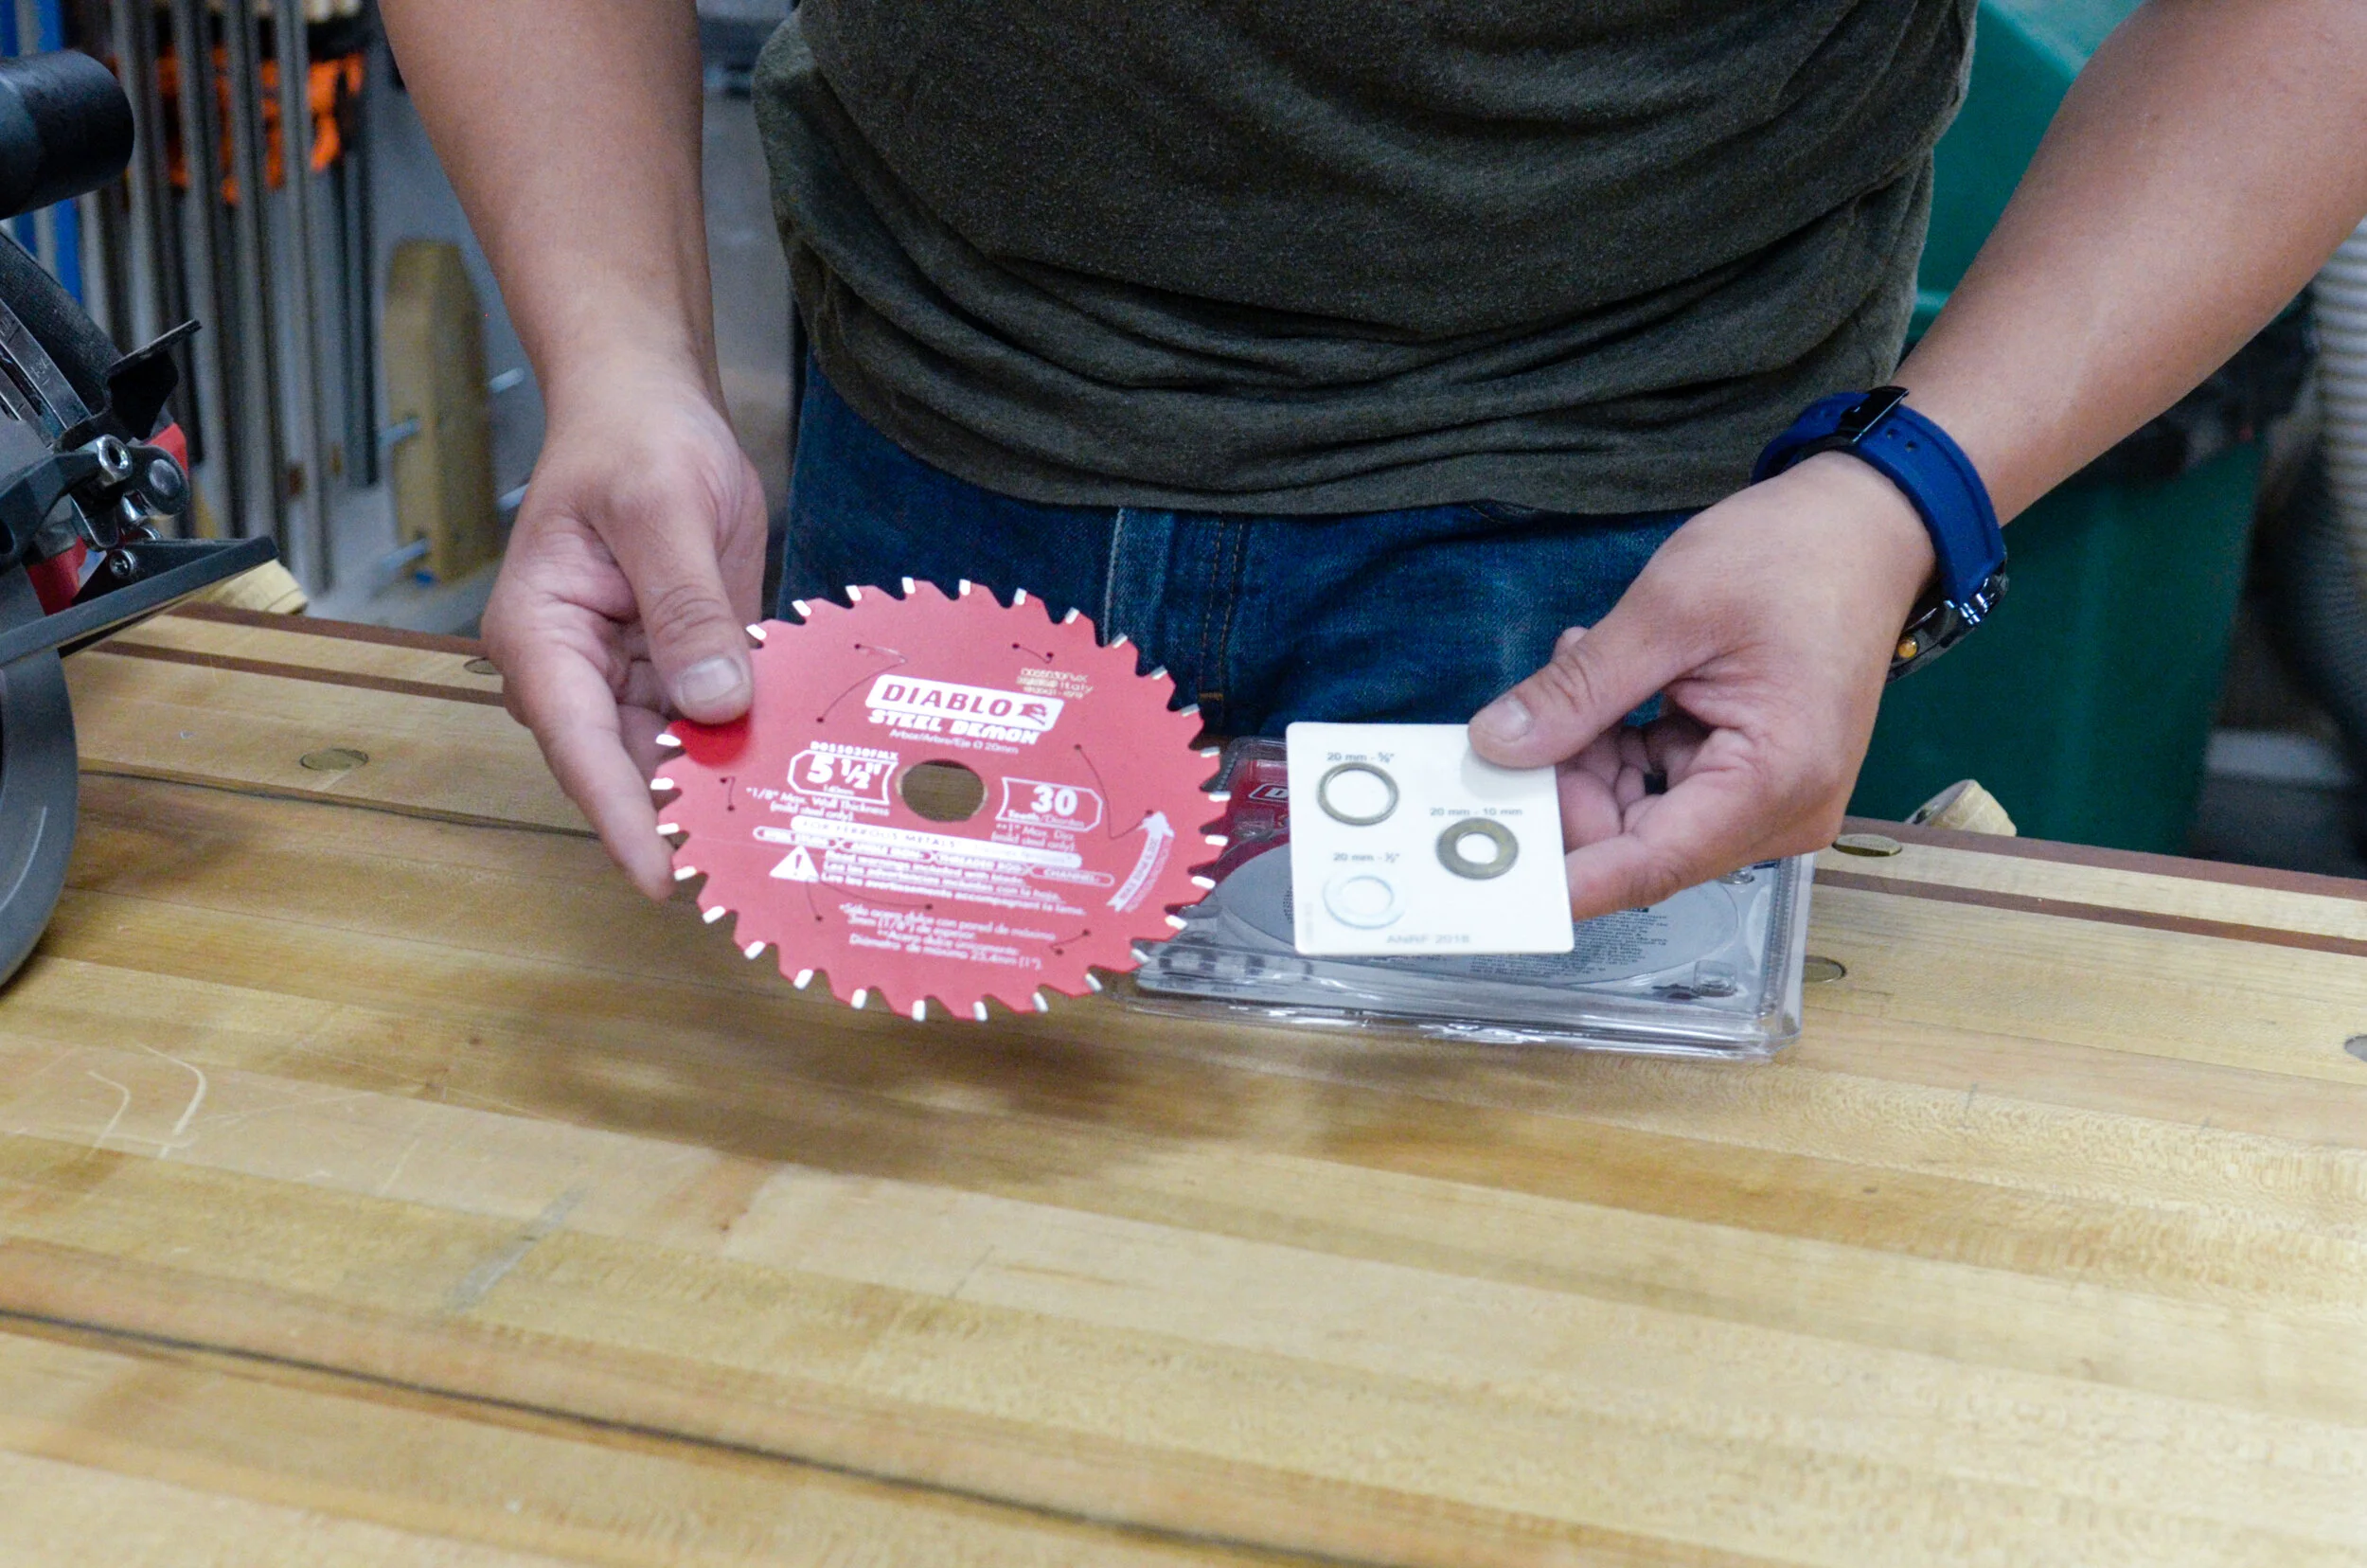
The Diablo metal cutting blade comes with three bushings to fit on a multitude of circular saws.
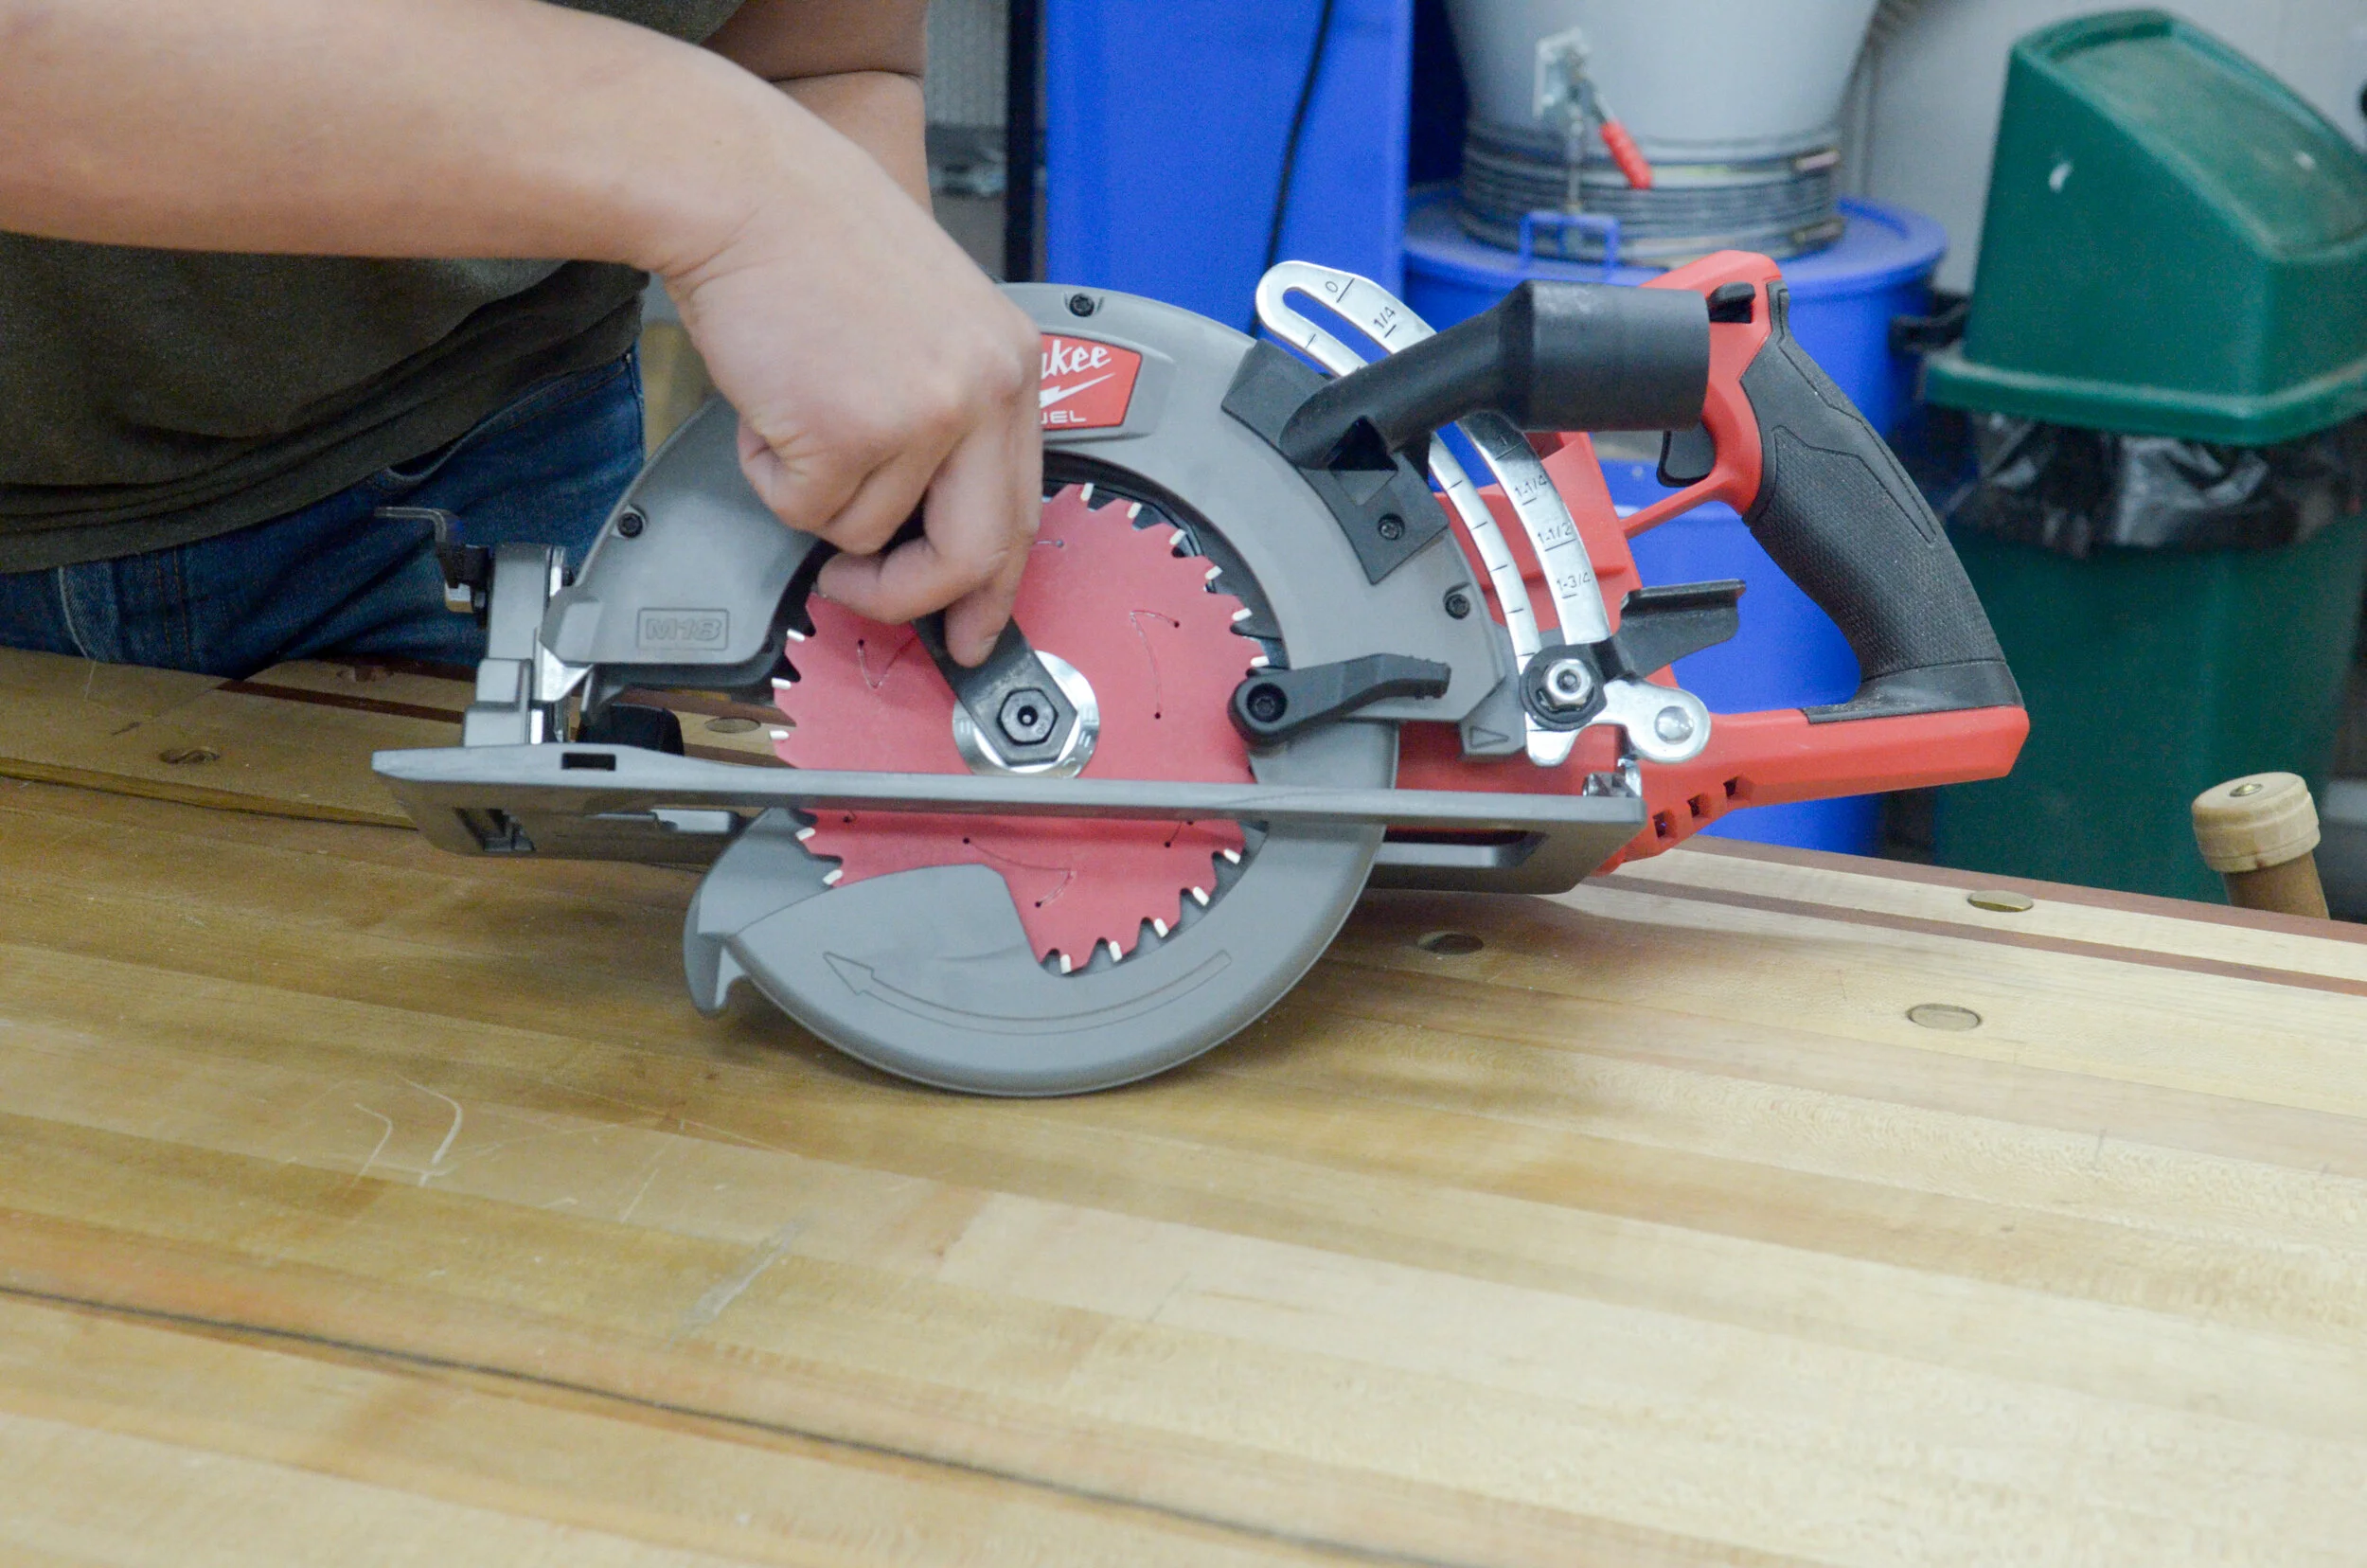
The Diablo metal cutting blade mounted on my Milwaukee circular saw. I used this to cut 1/8” thick flat steel bar.
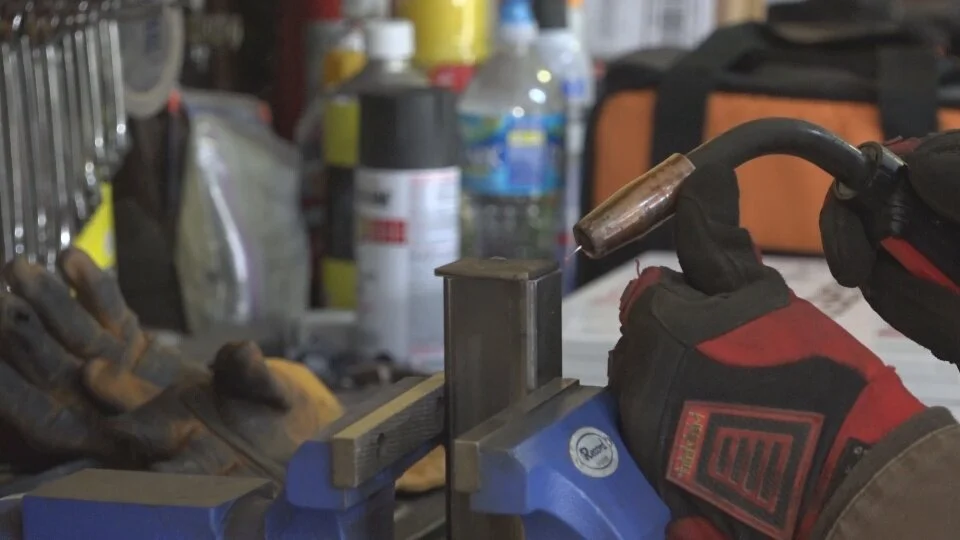
The steel flat bar is welded to the end of the steel tubing.
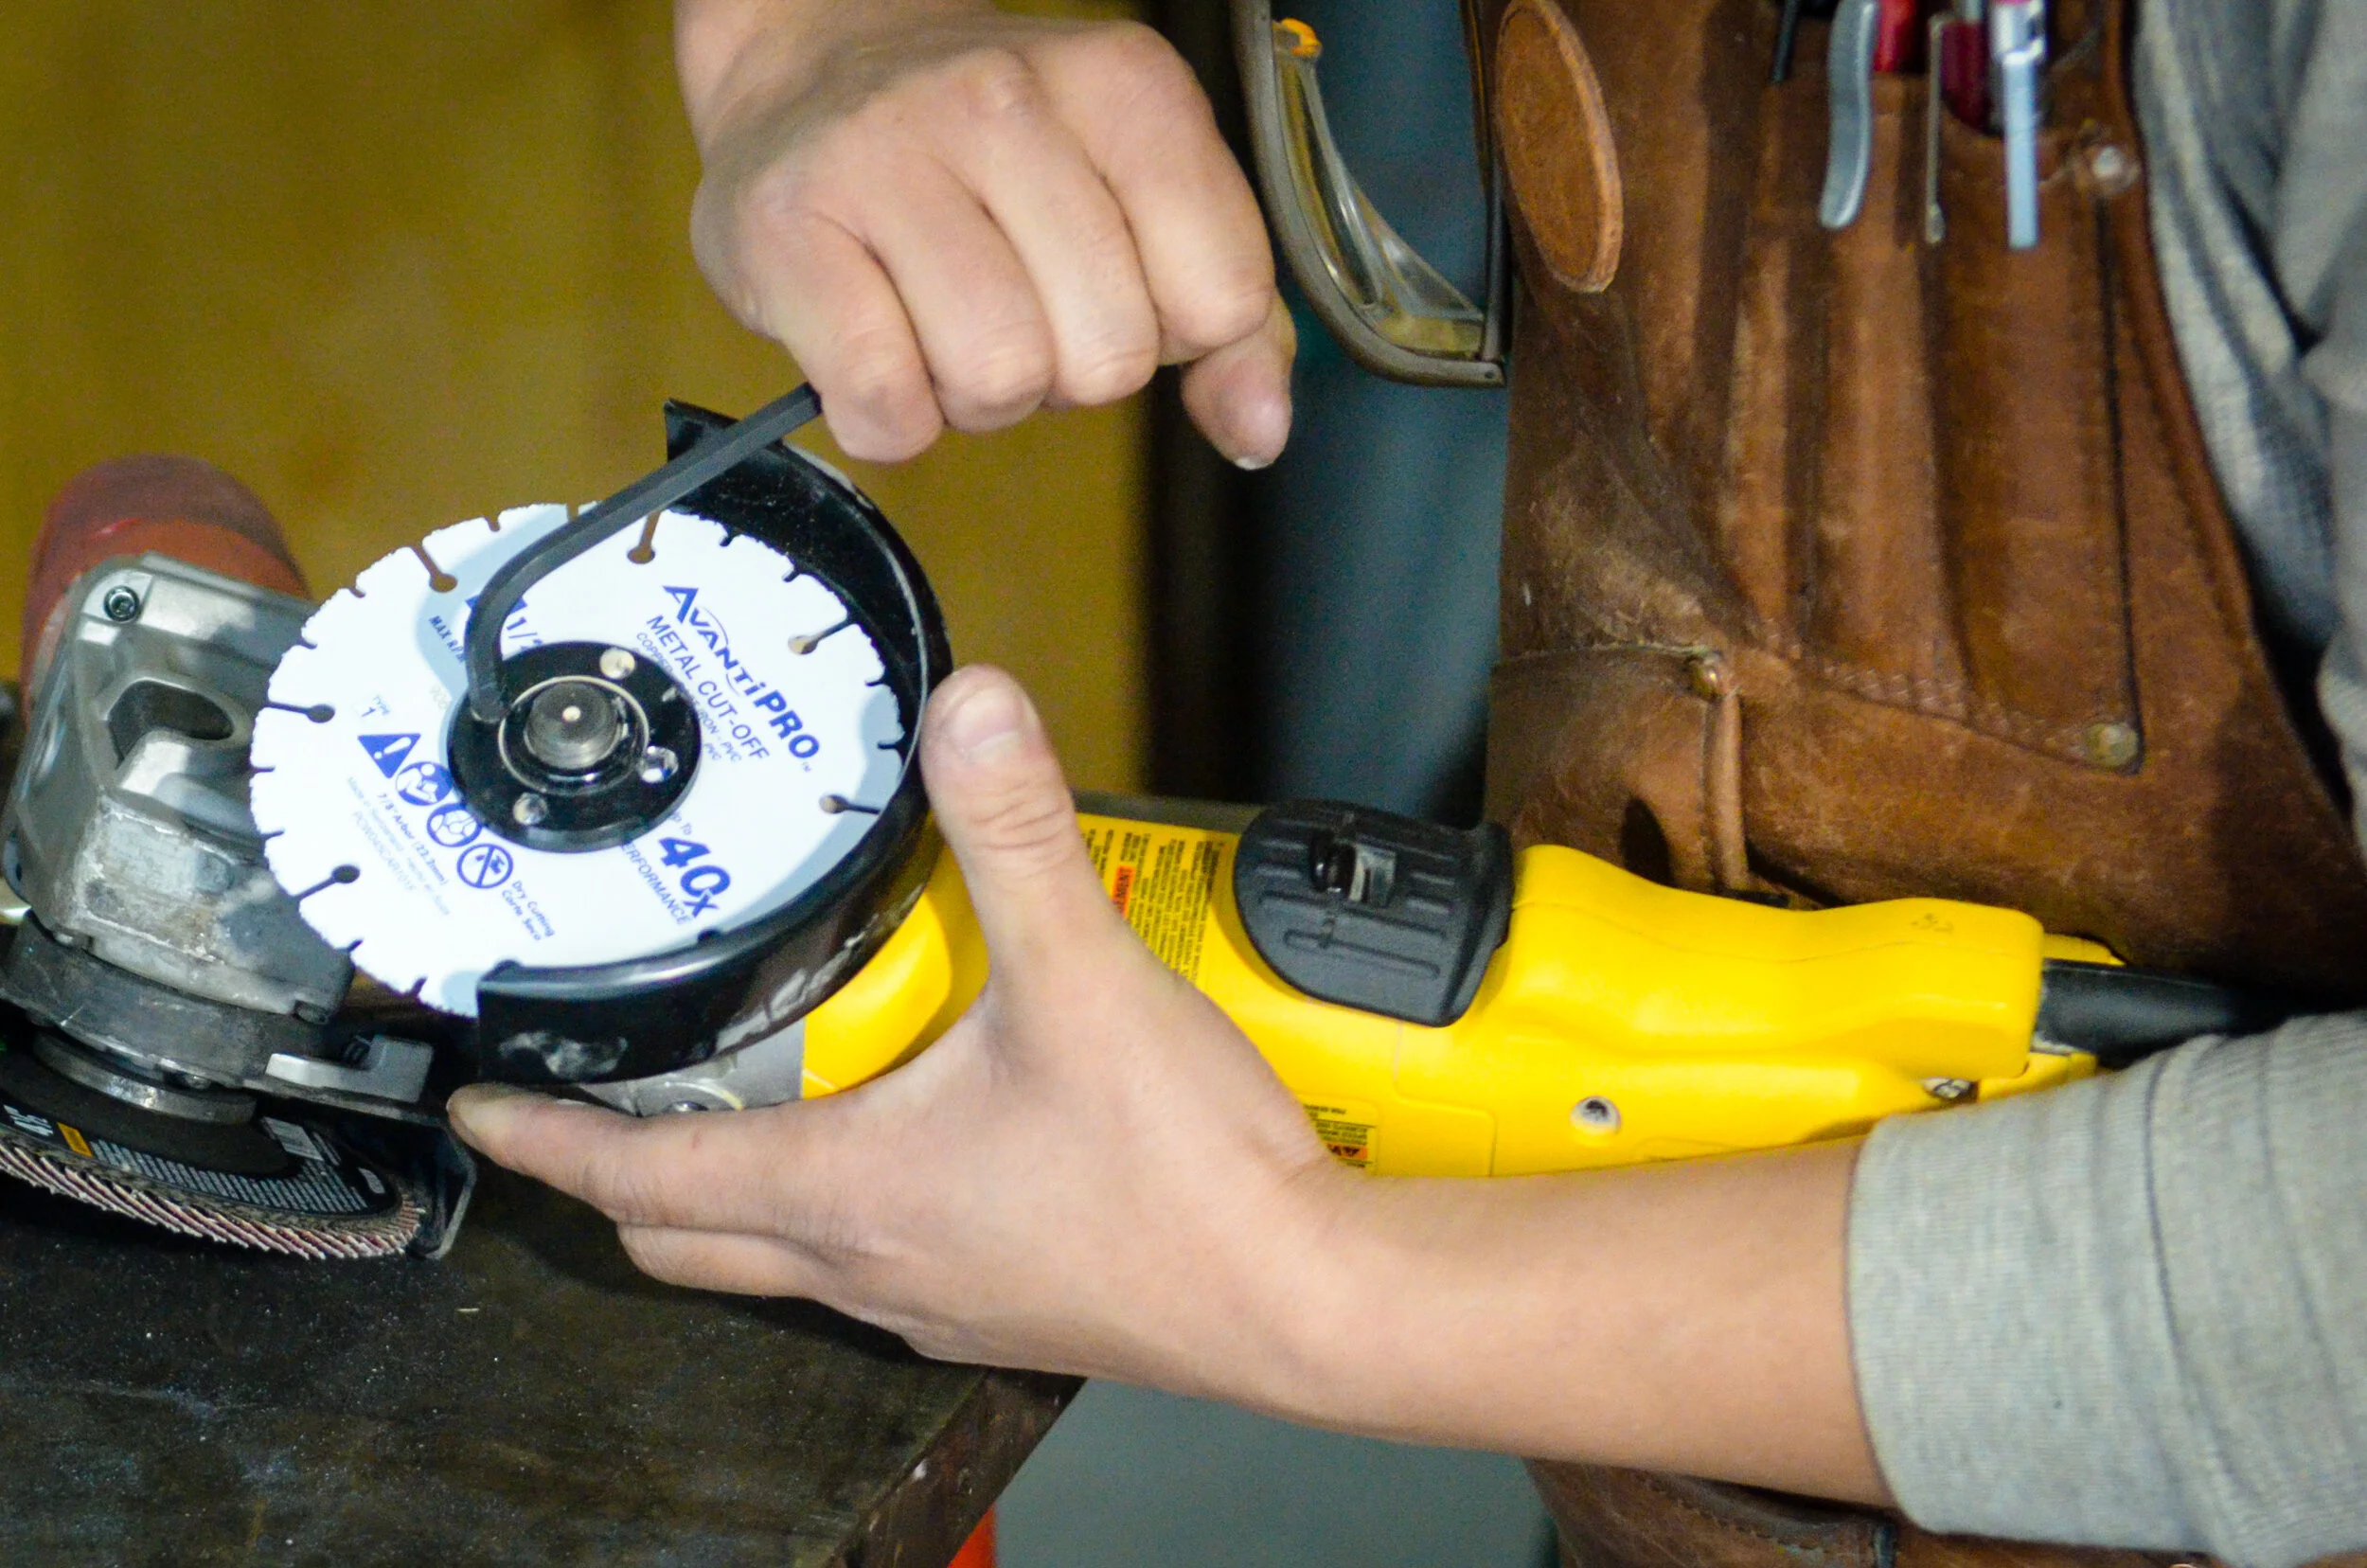
The AvantiPRO metal cutting wheel is compatible with most corded and cordless angle grinders.
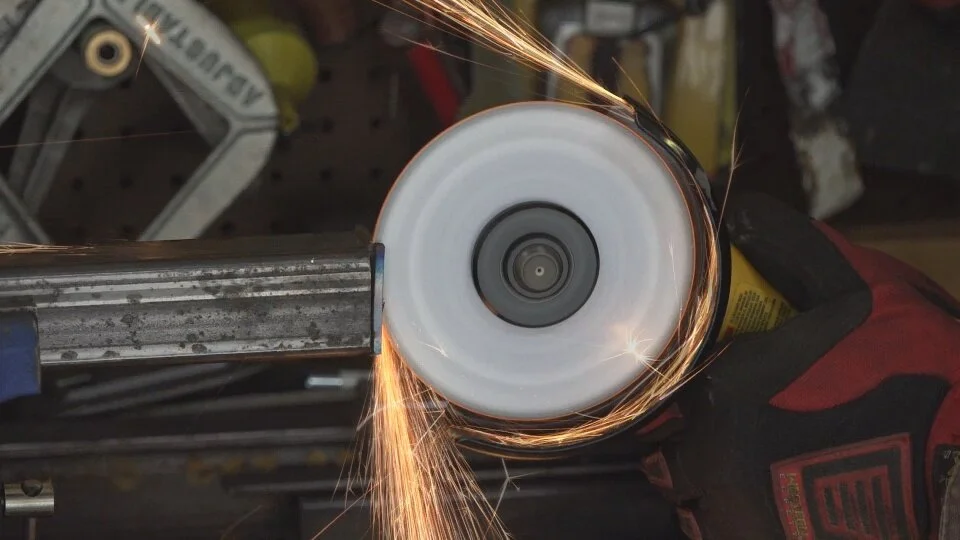
The AvantiPRO metal cutting wheel trims up the end caps to the steel tubing.
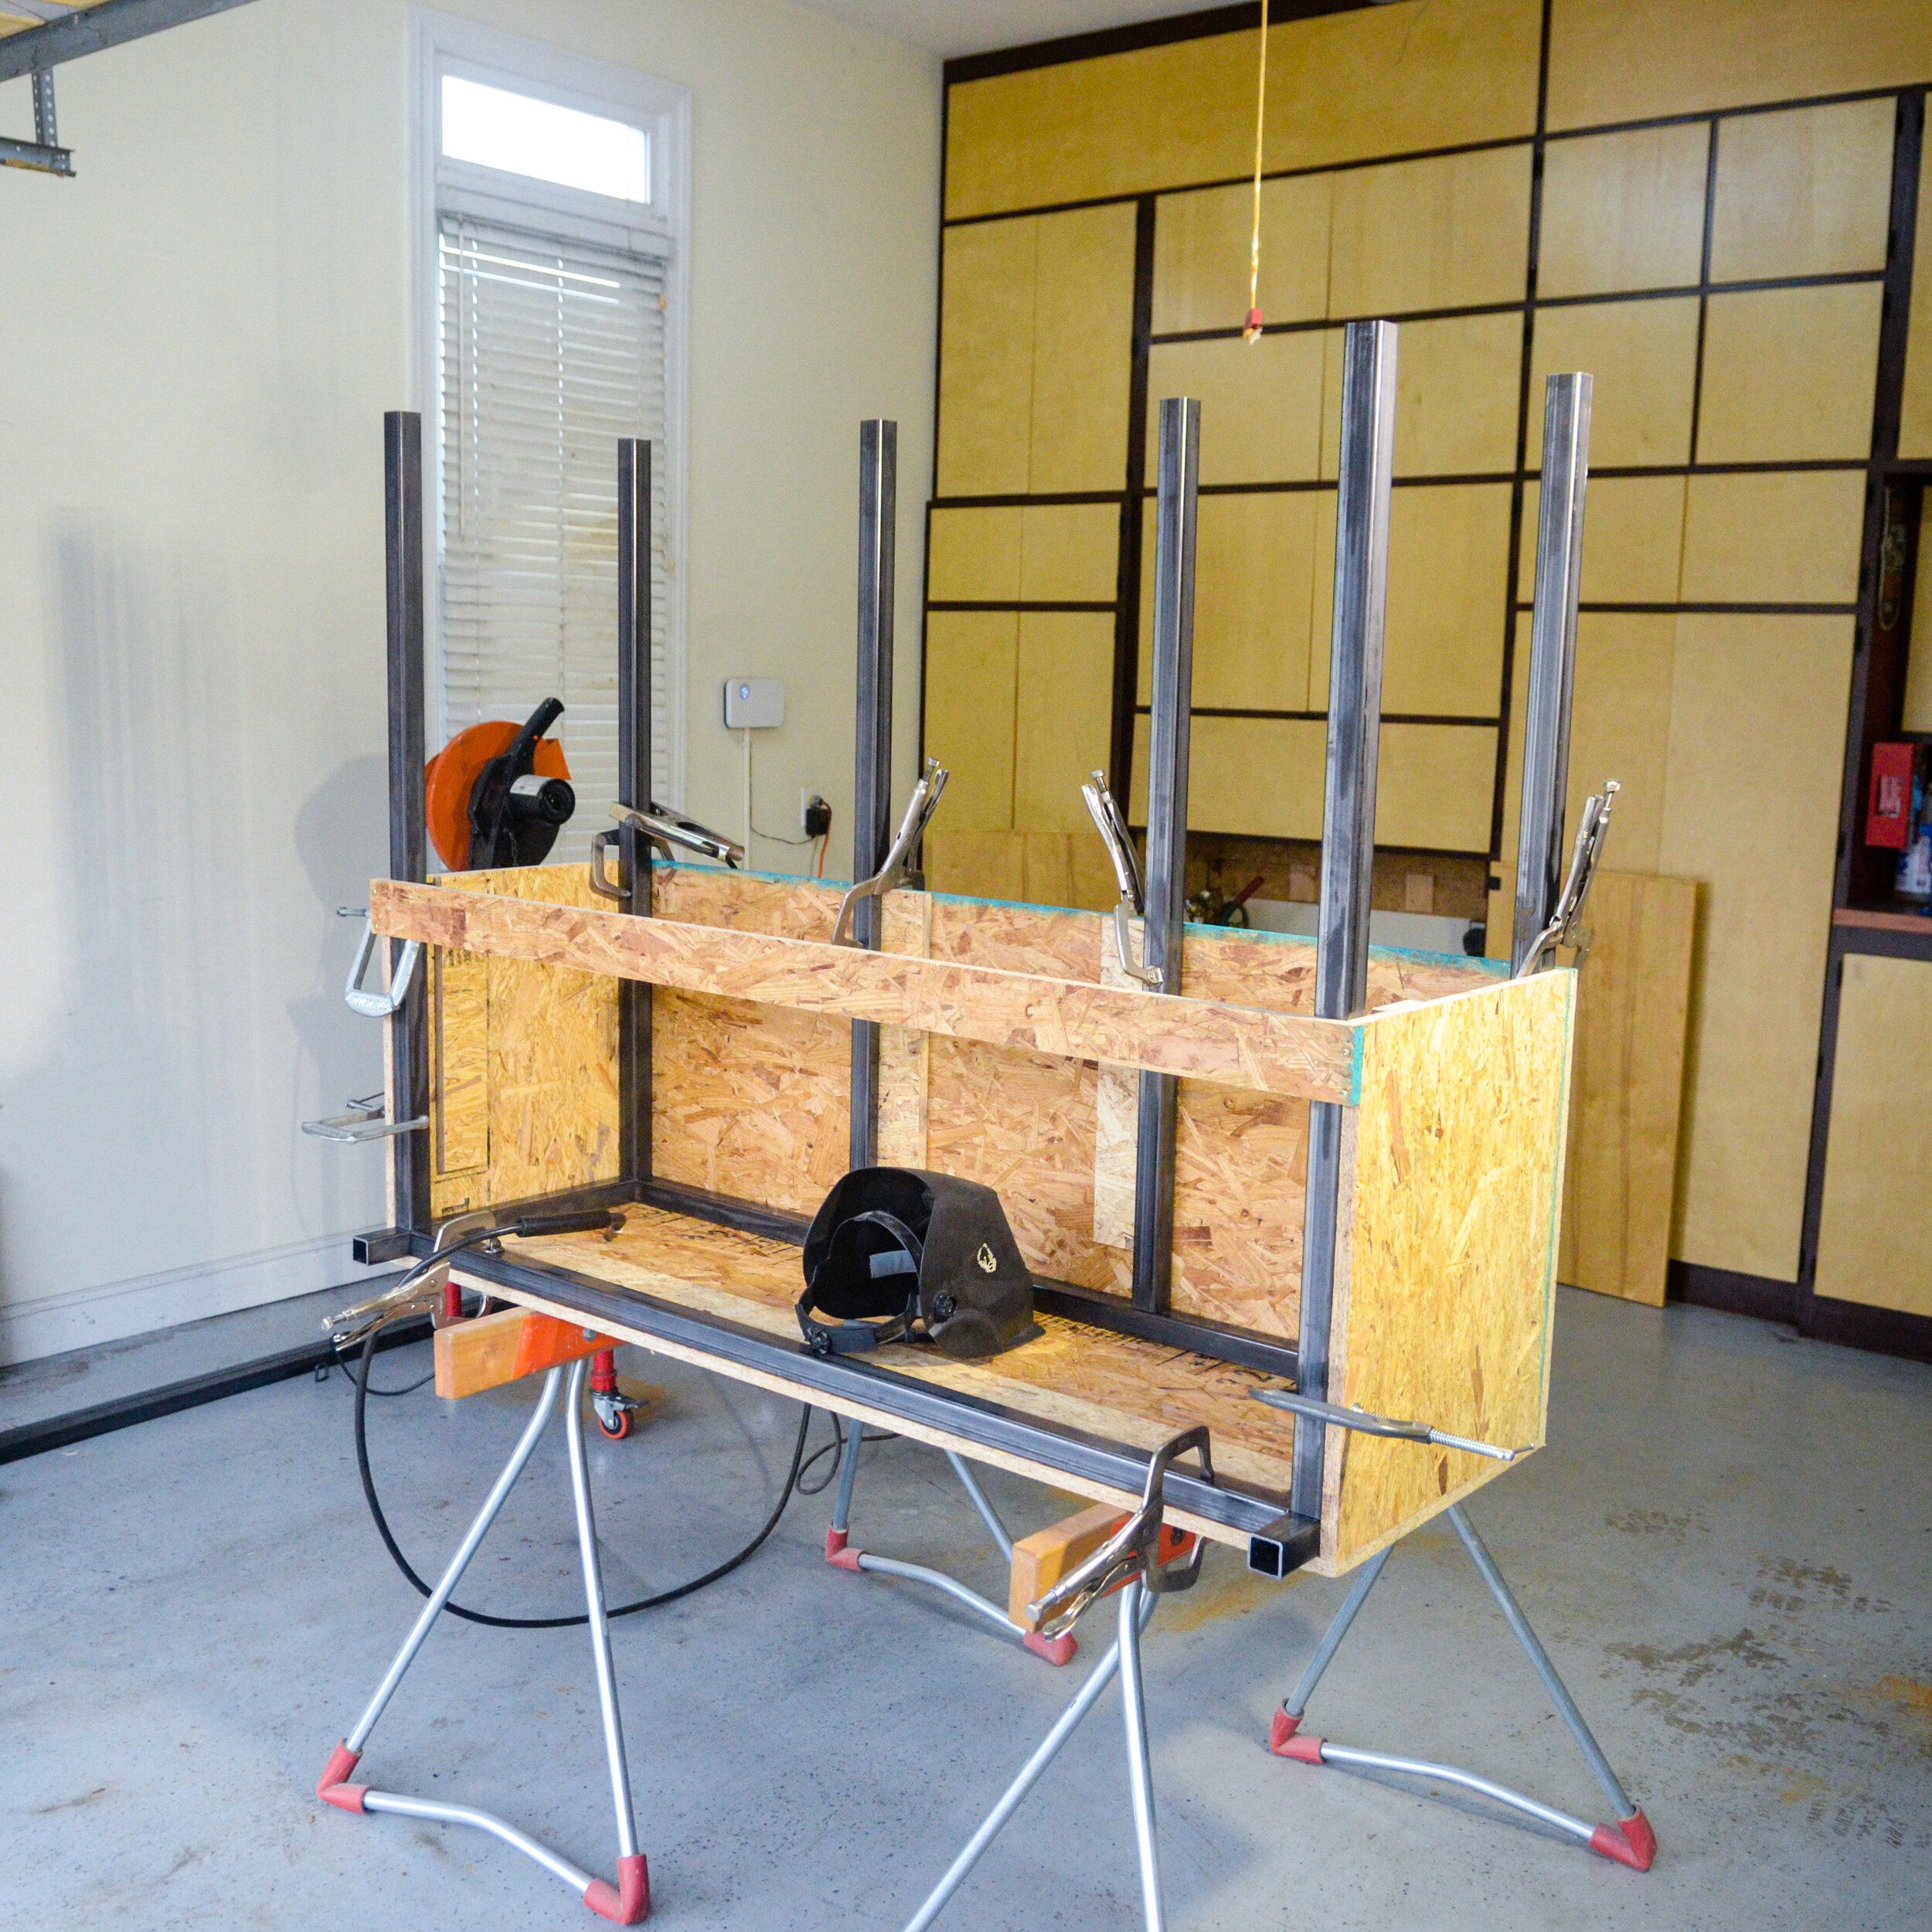
The welding jig structure holds the steel tubing in place as each piece is welding into place.
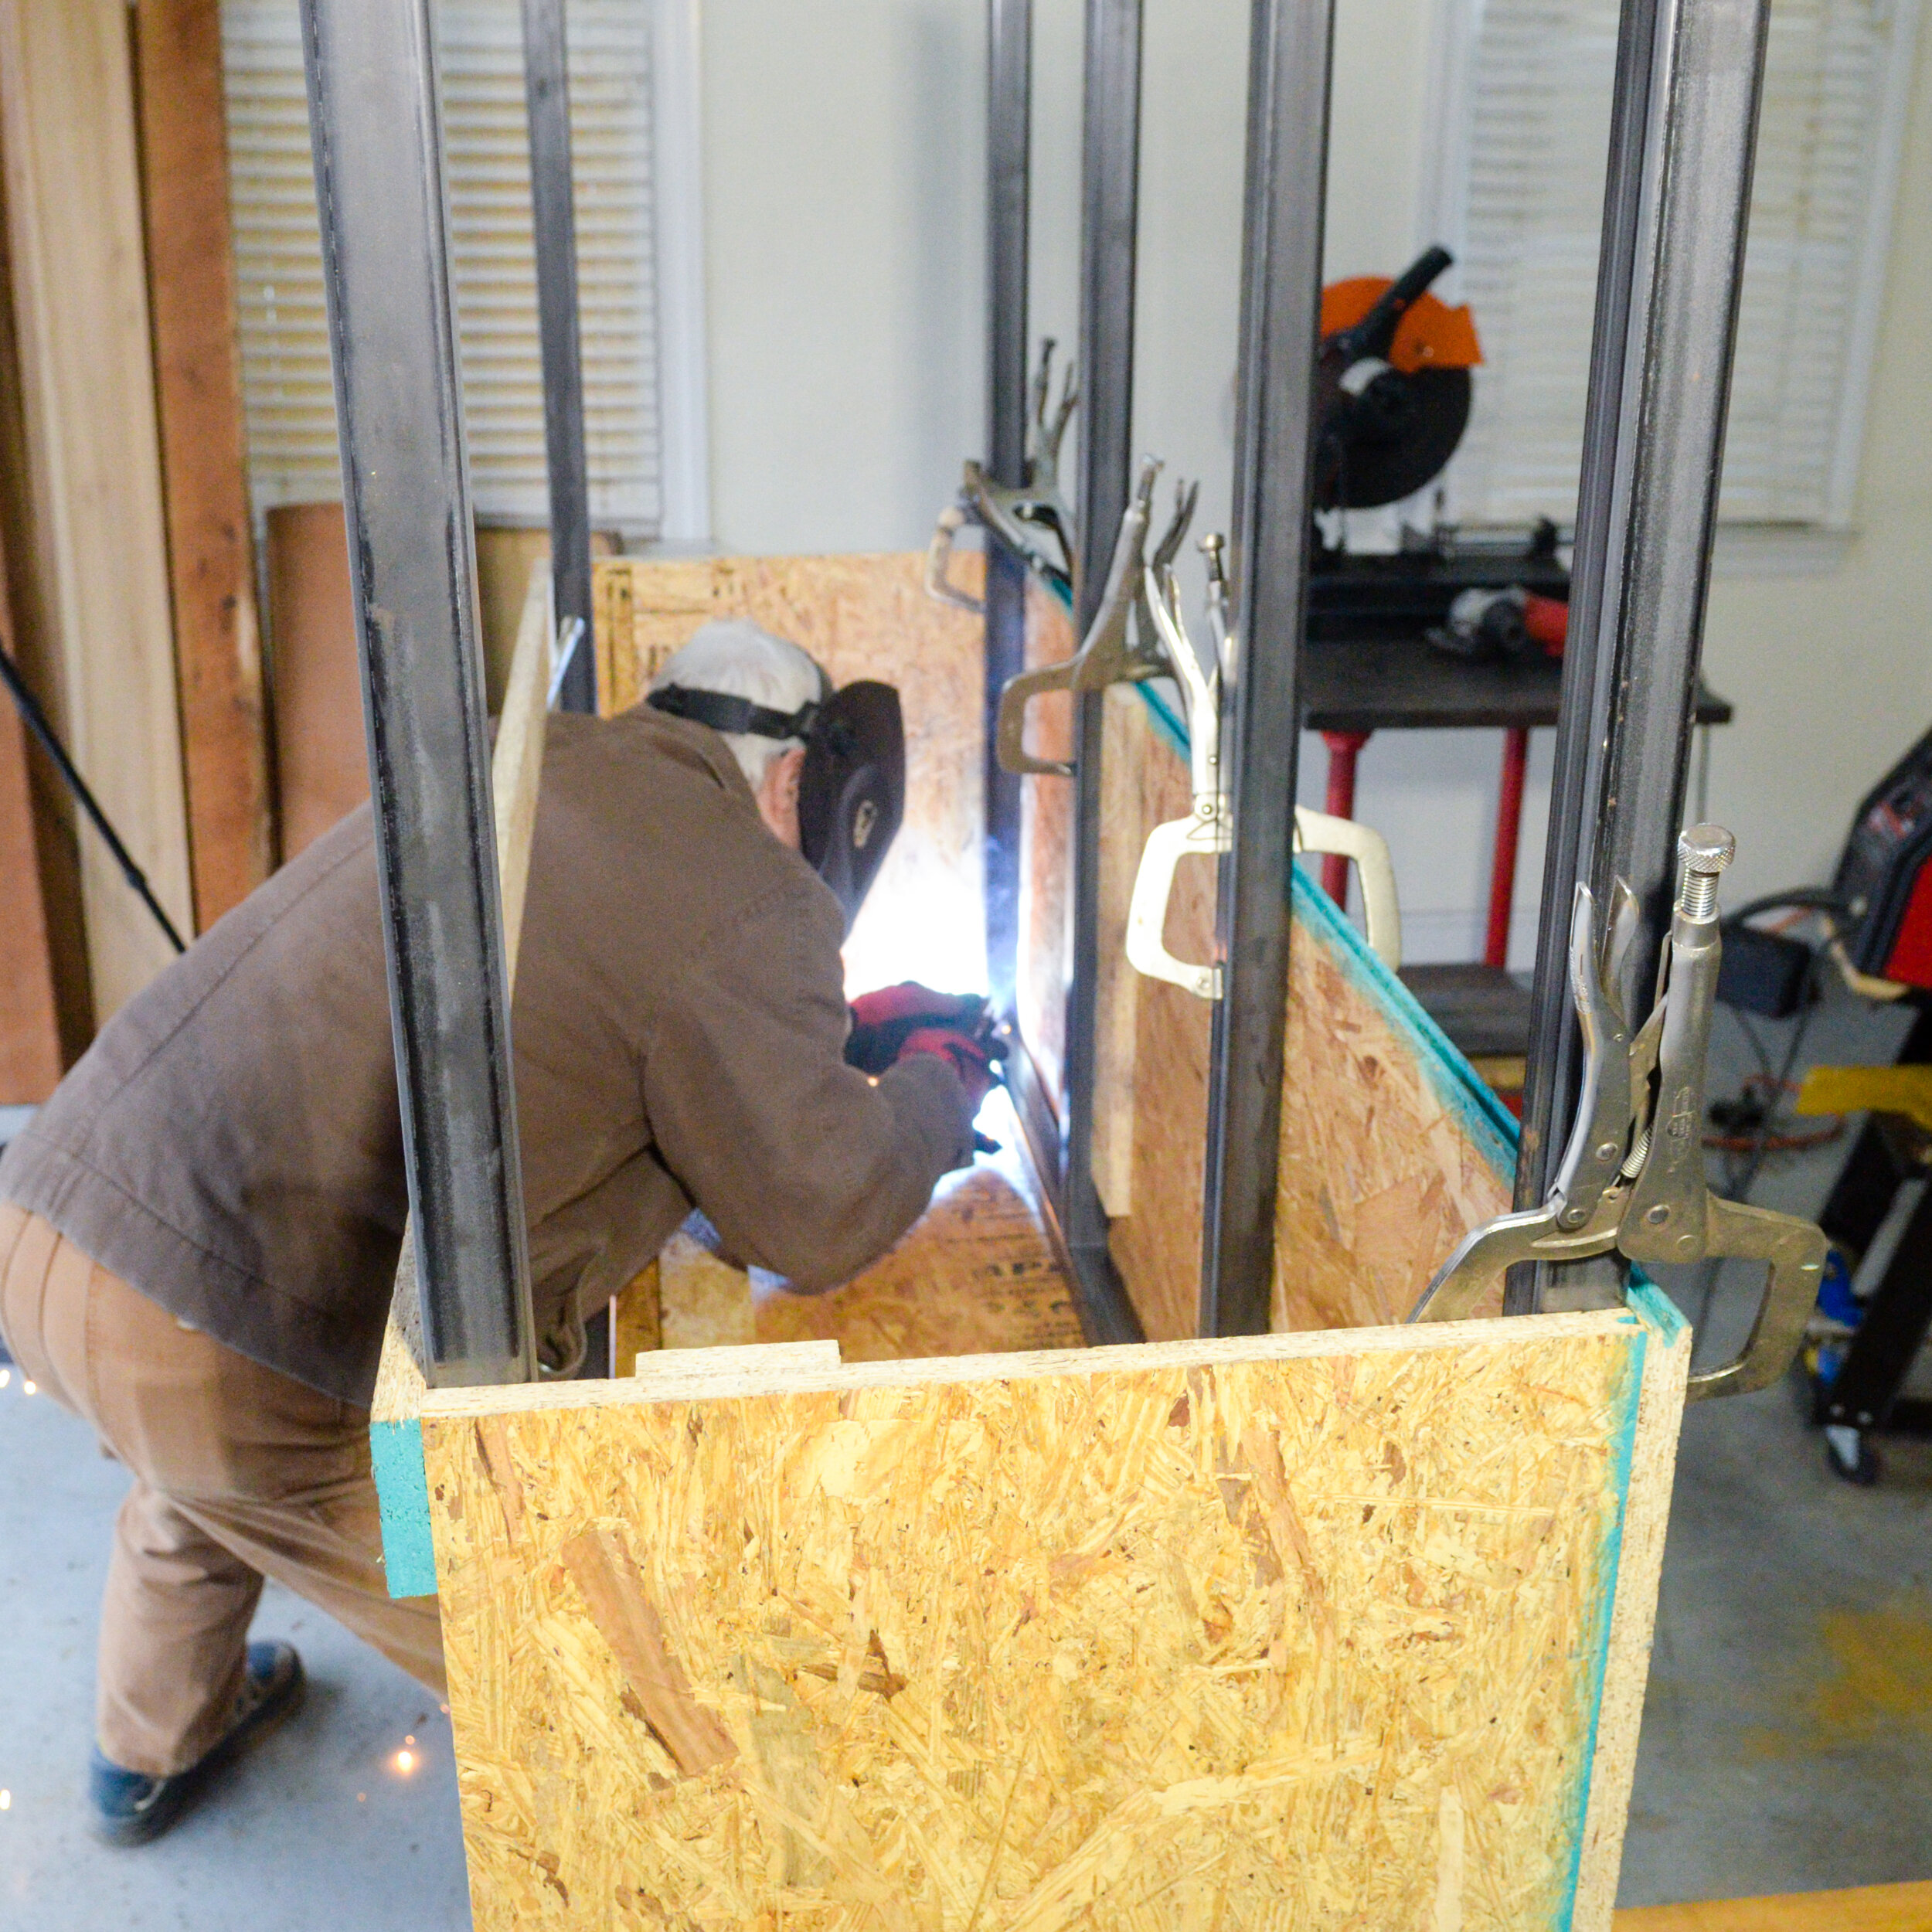
David showed me how to weld with Lincoln model SP-175 Plus MIG welder.
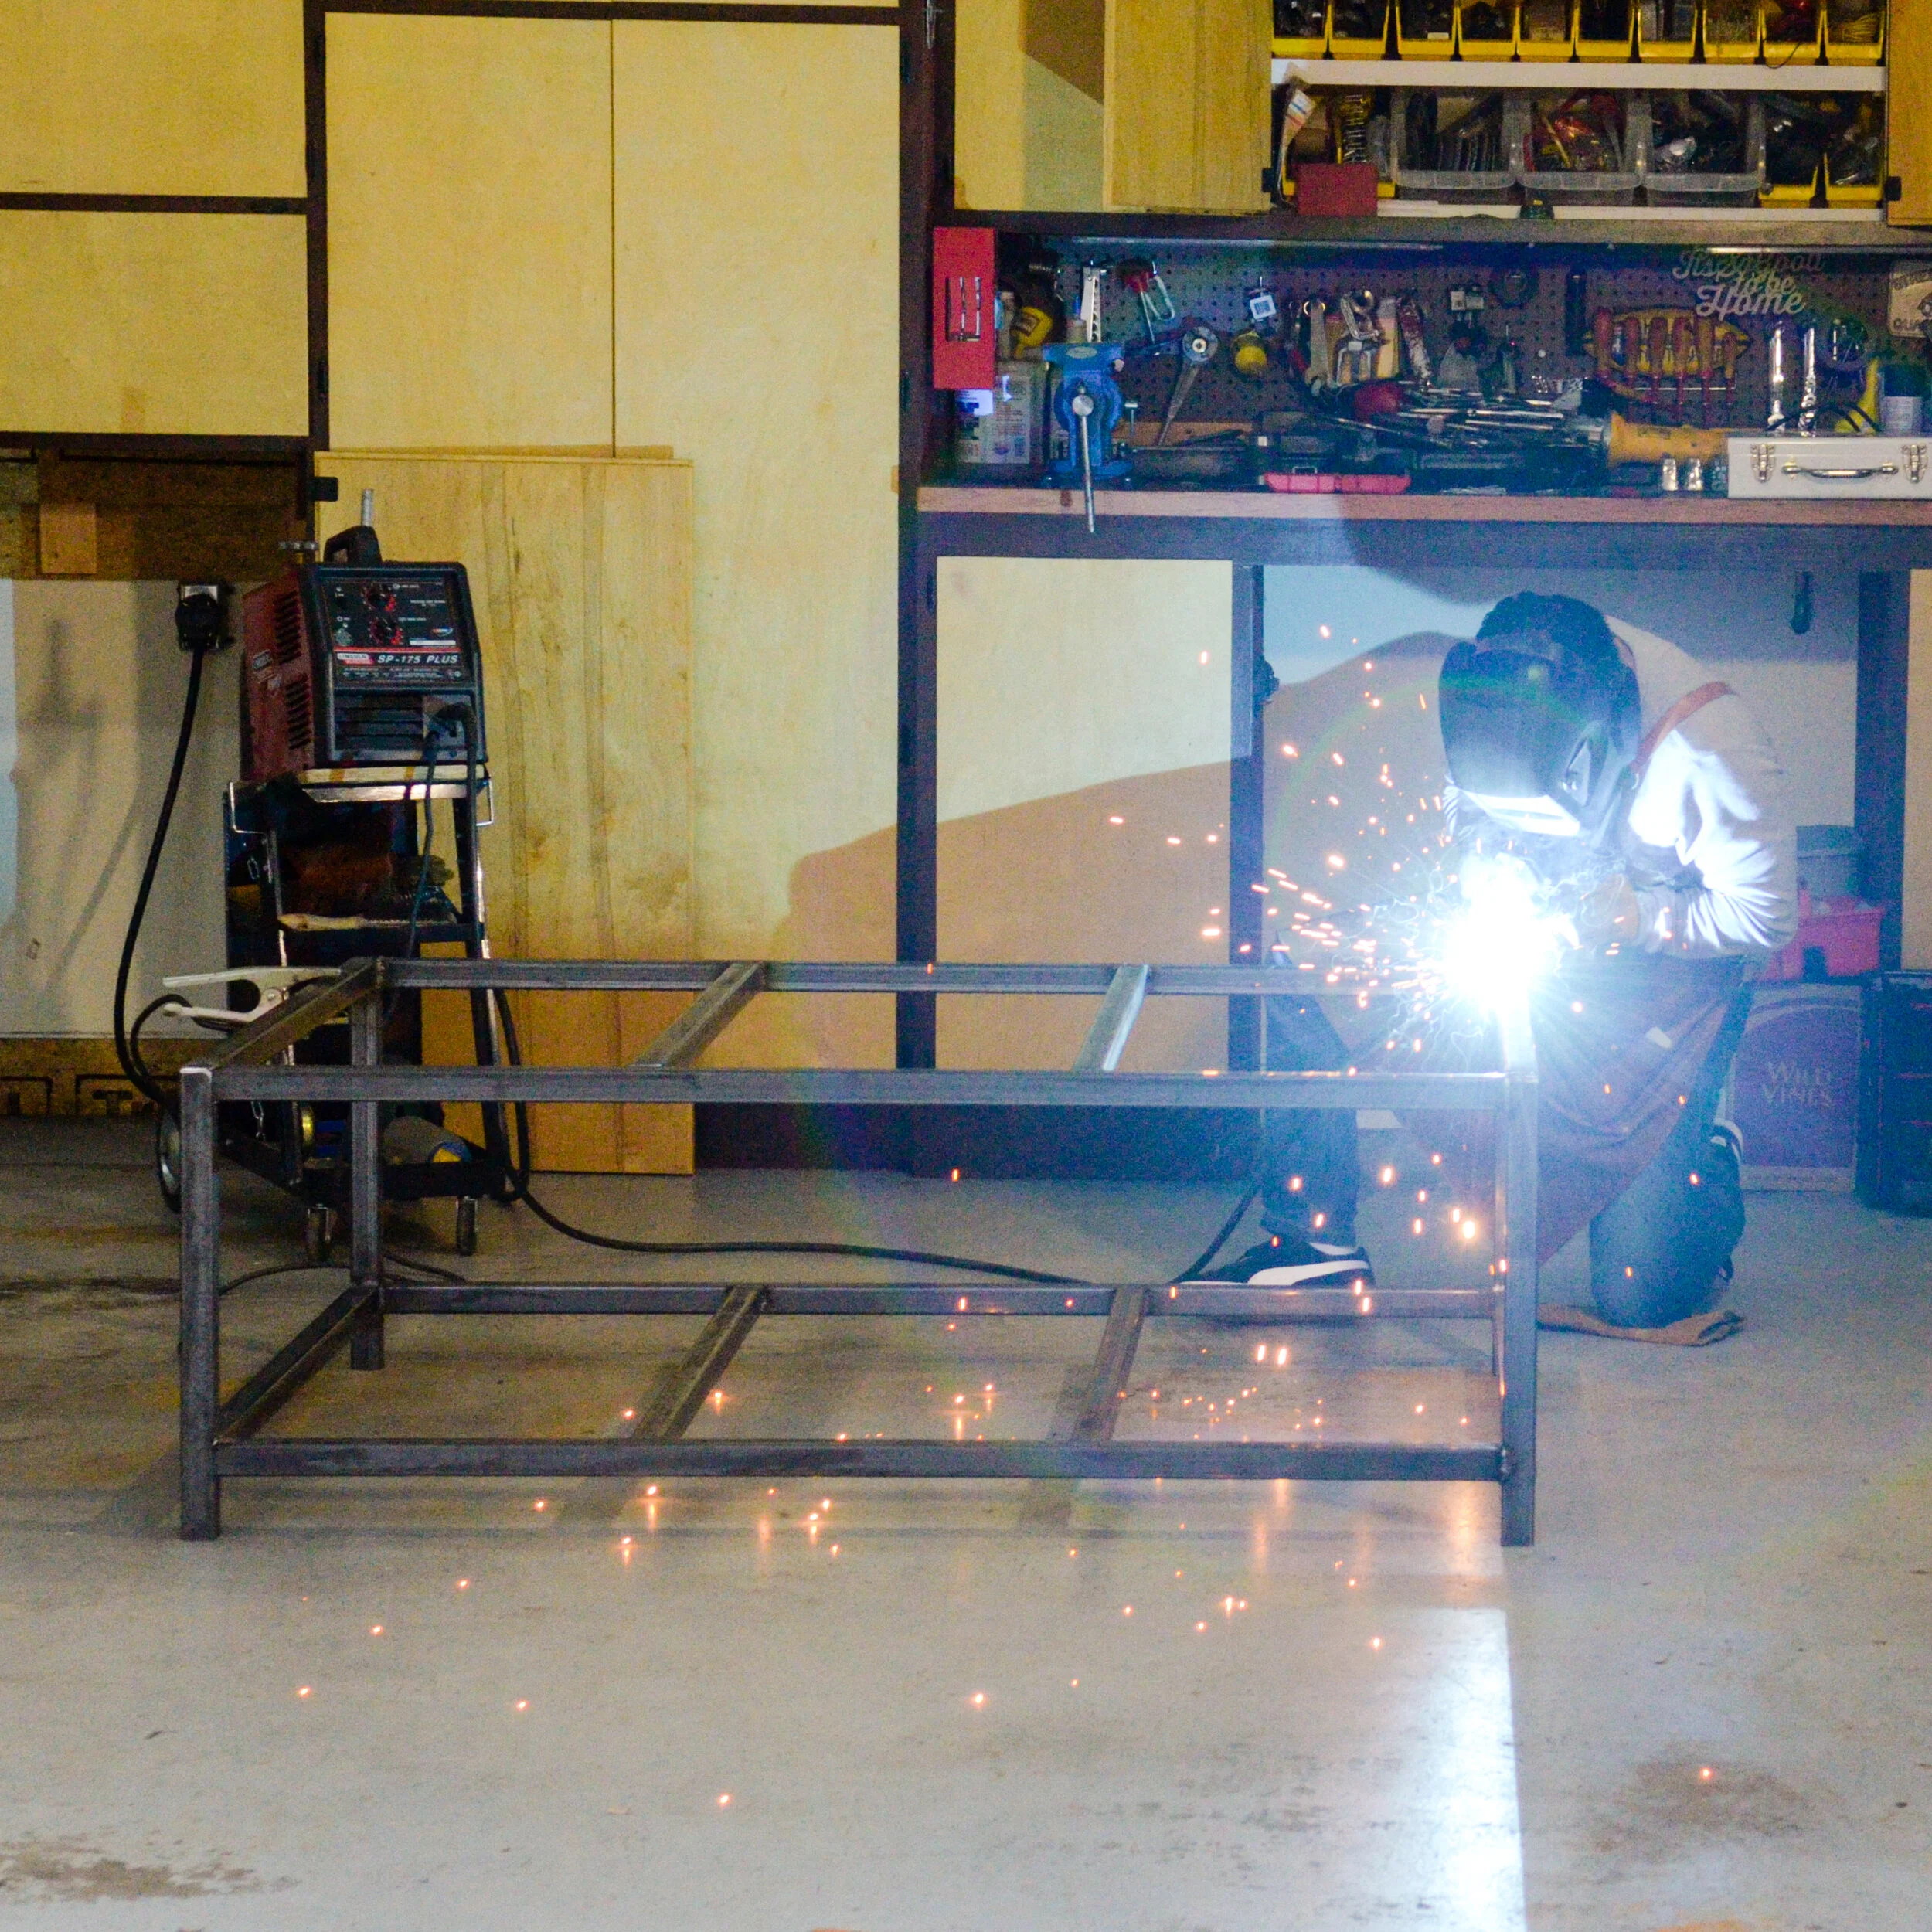
I tried my hand at welding.
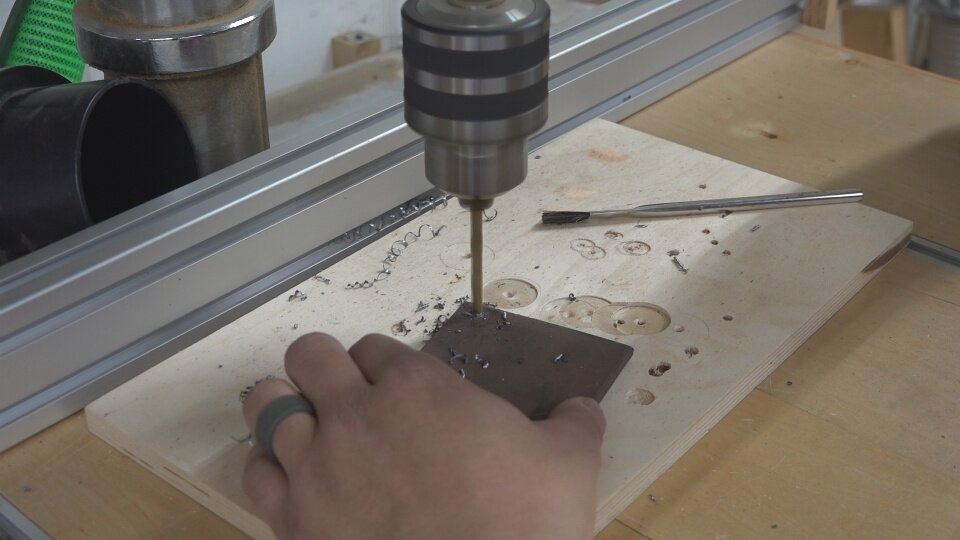
The legs of the steel table were capped with a piece of 3” square flat bar.
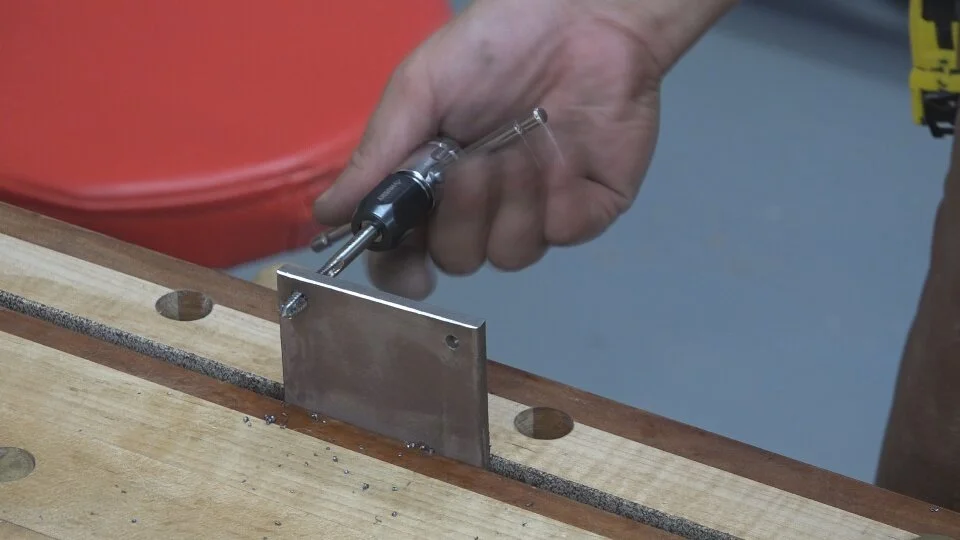
The end caps for the legs were tapped using a 1/4"-20 tpi tap from the Husky 77 PC SAE and MM Tap and Die Set. The end caps were tapped to attach a set of 1-3/4" diameter leveling foot caster sold by Apollo Caster.
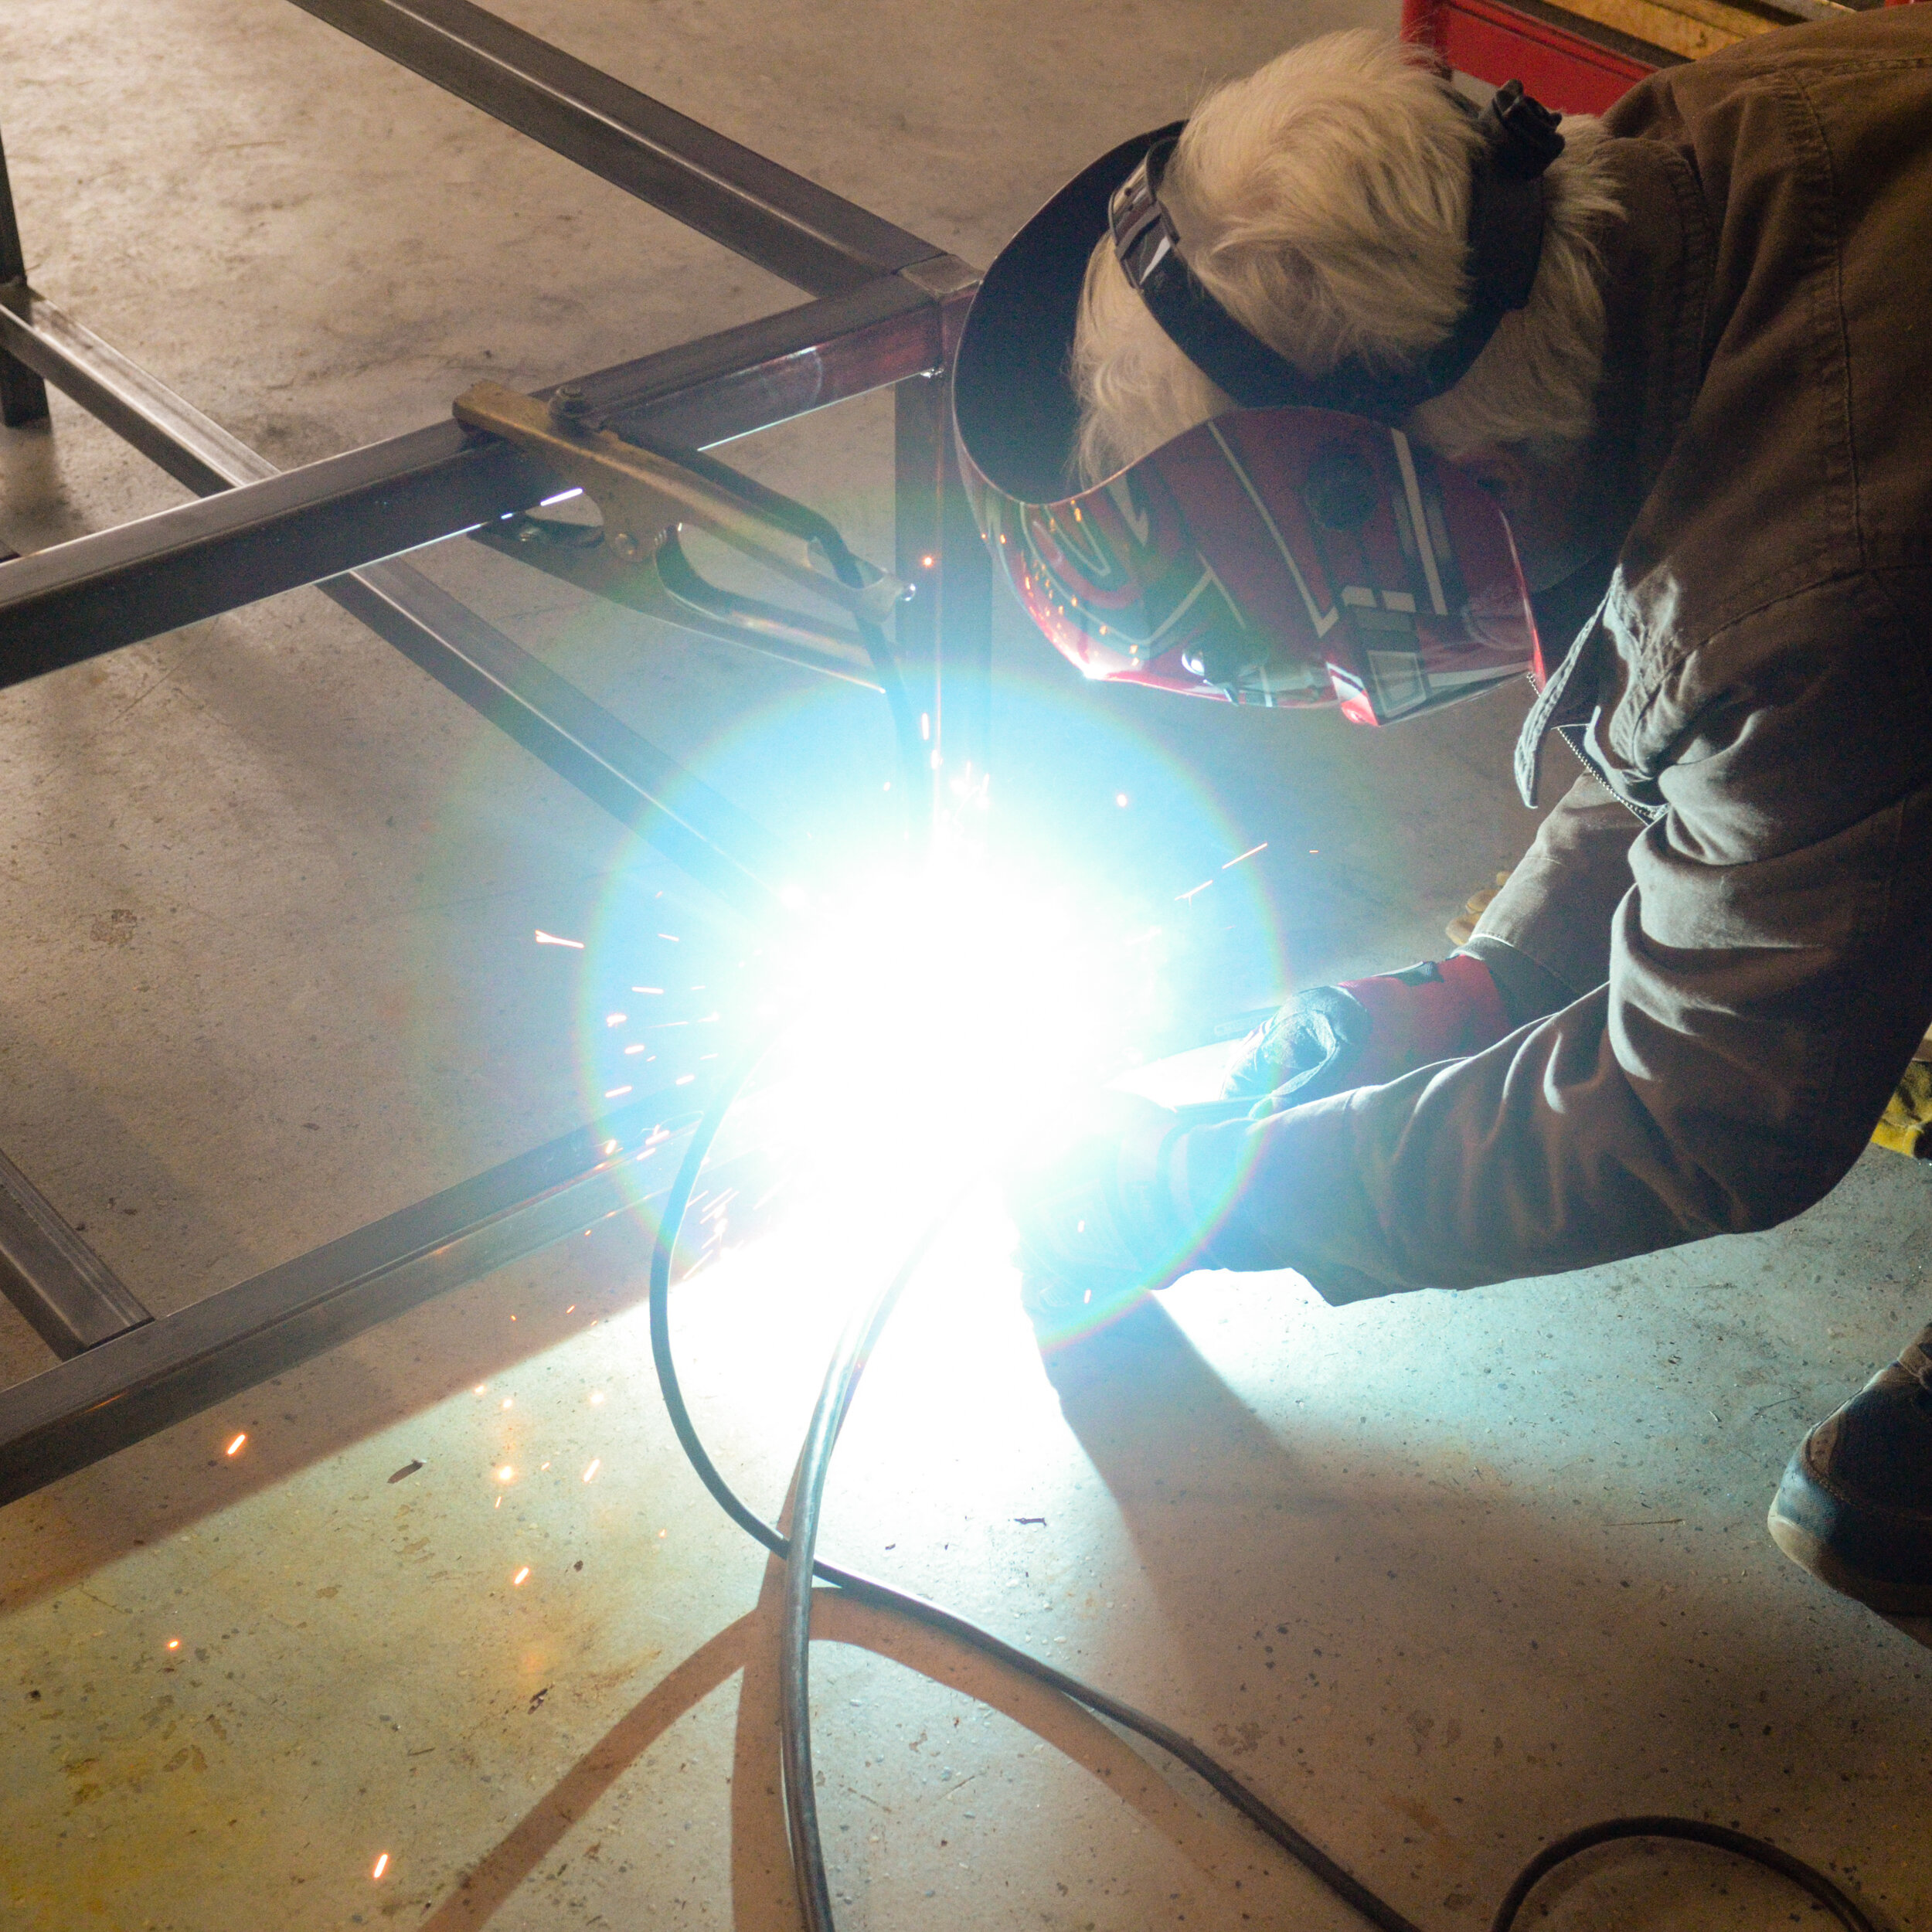
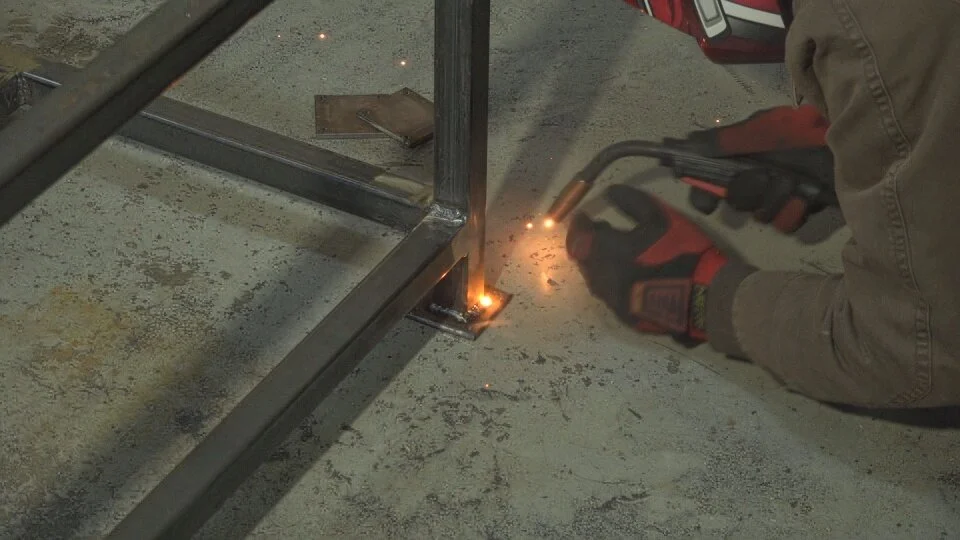
After the end caps are threaded and tapped, they were welded to bottom of the legs.
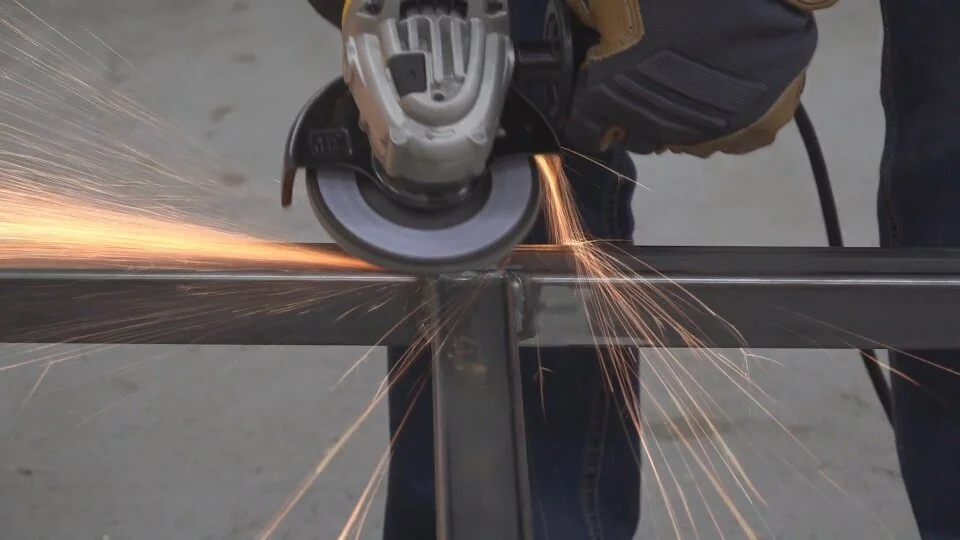
After the welding was complete, I used an 80-grit flap wheel on my angle grinder to clean up the welds.
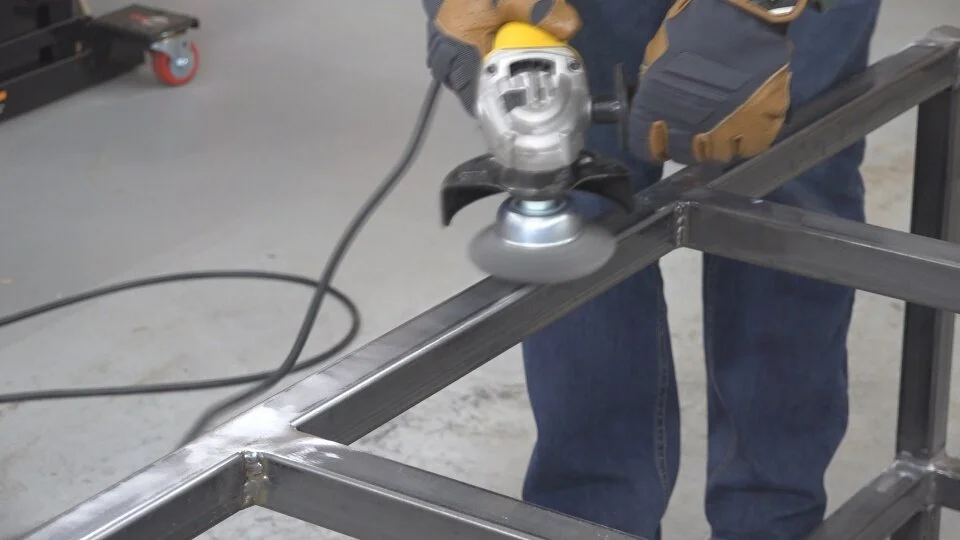
I then cleaned up all the steel before applying a coat black spray paint.
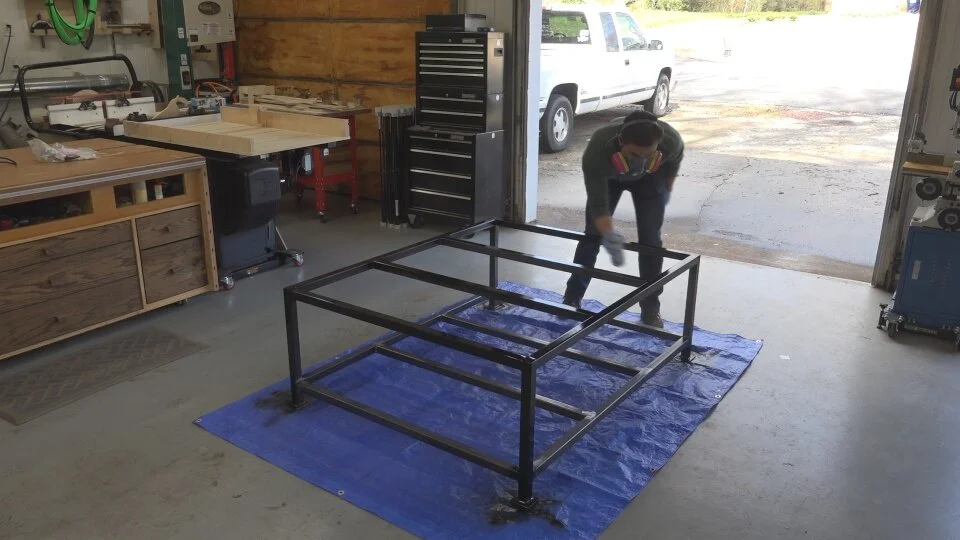
The steel table base received a coat of black spray paint to protect it from rust.
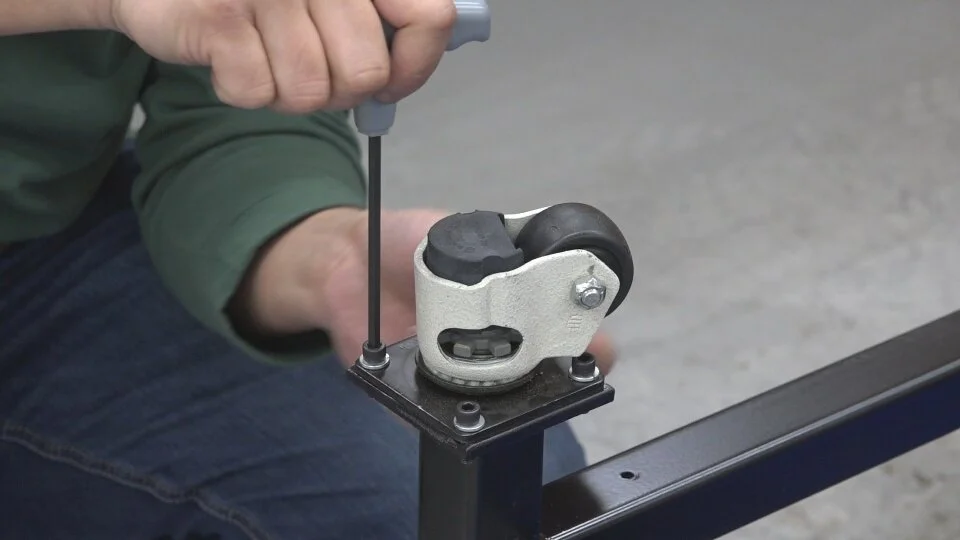
Finally, I attached the level foot caster.
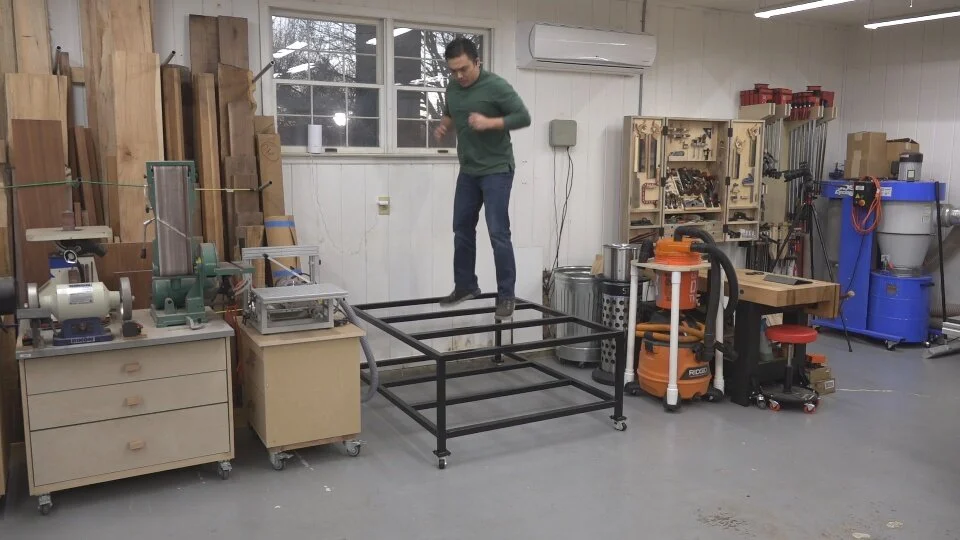
The welded steel table will be a solid, level table to support my new 4’x4’ CNC machine.
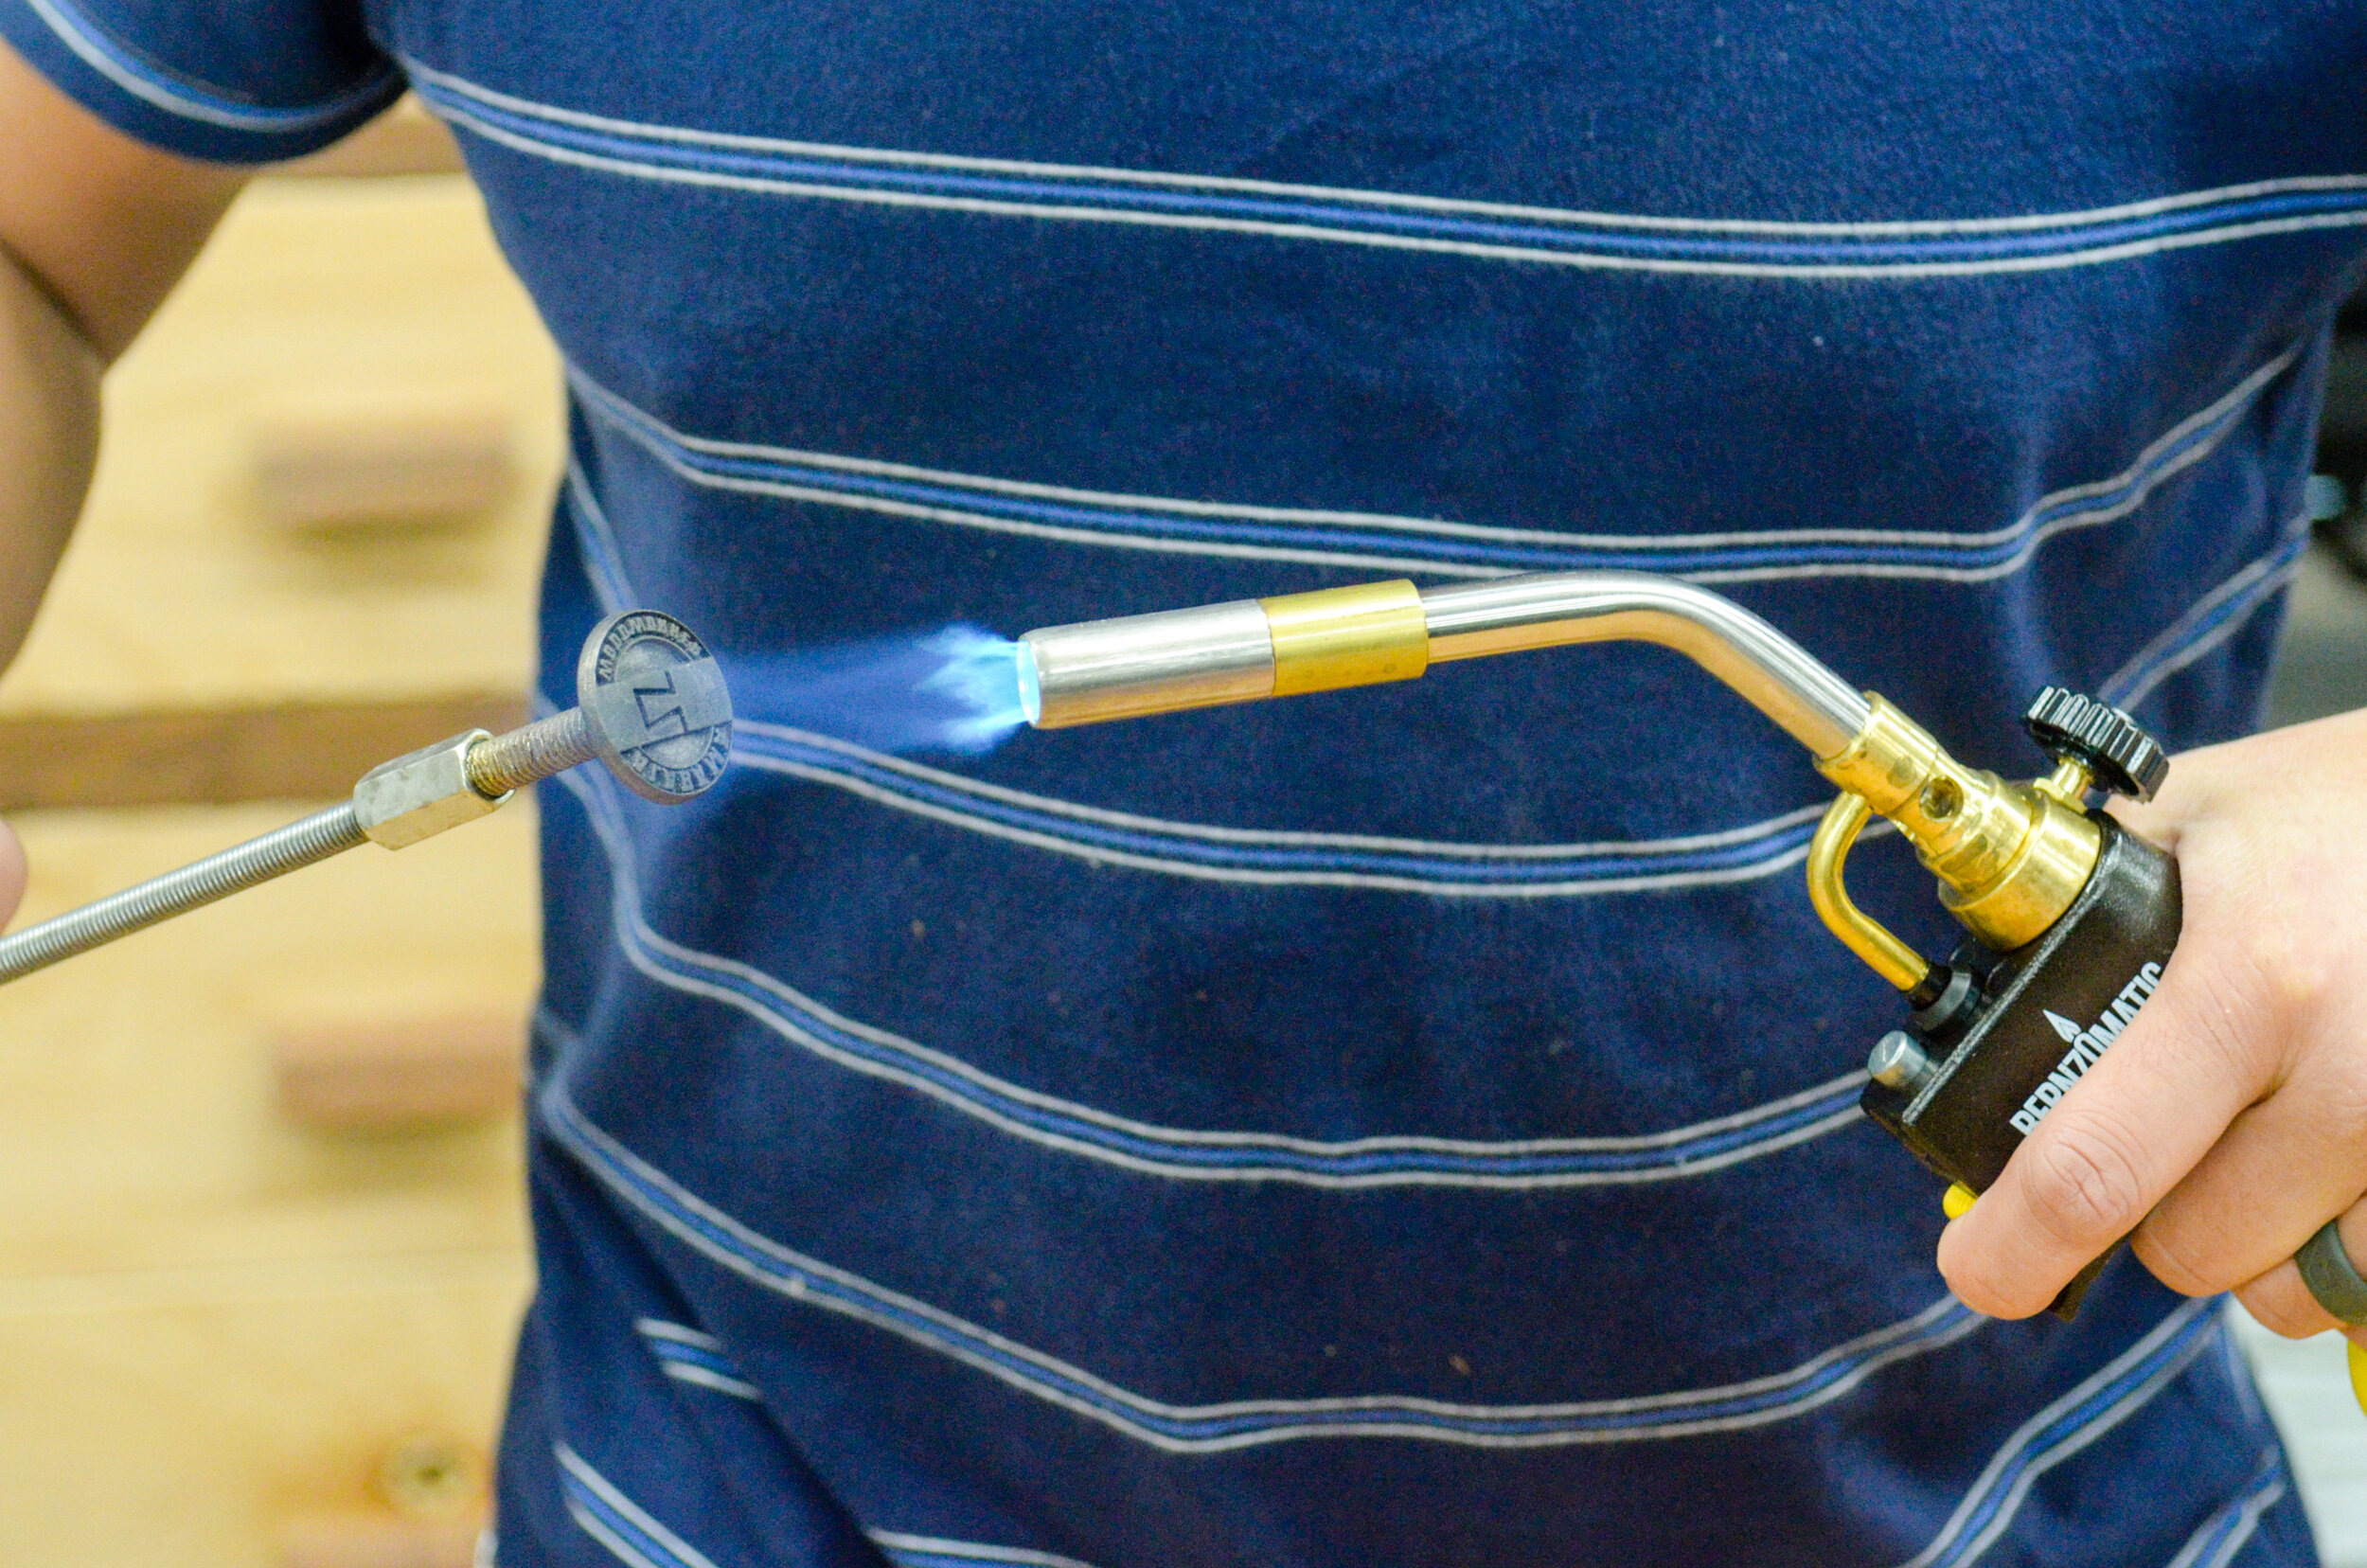
Using a Branding Iron
I’ve started using a branding iron with my logo to identify my work. Here are some things I’ve learning that may help you if you’ve thought about using a branding iron.
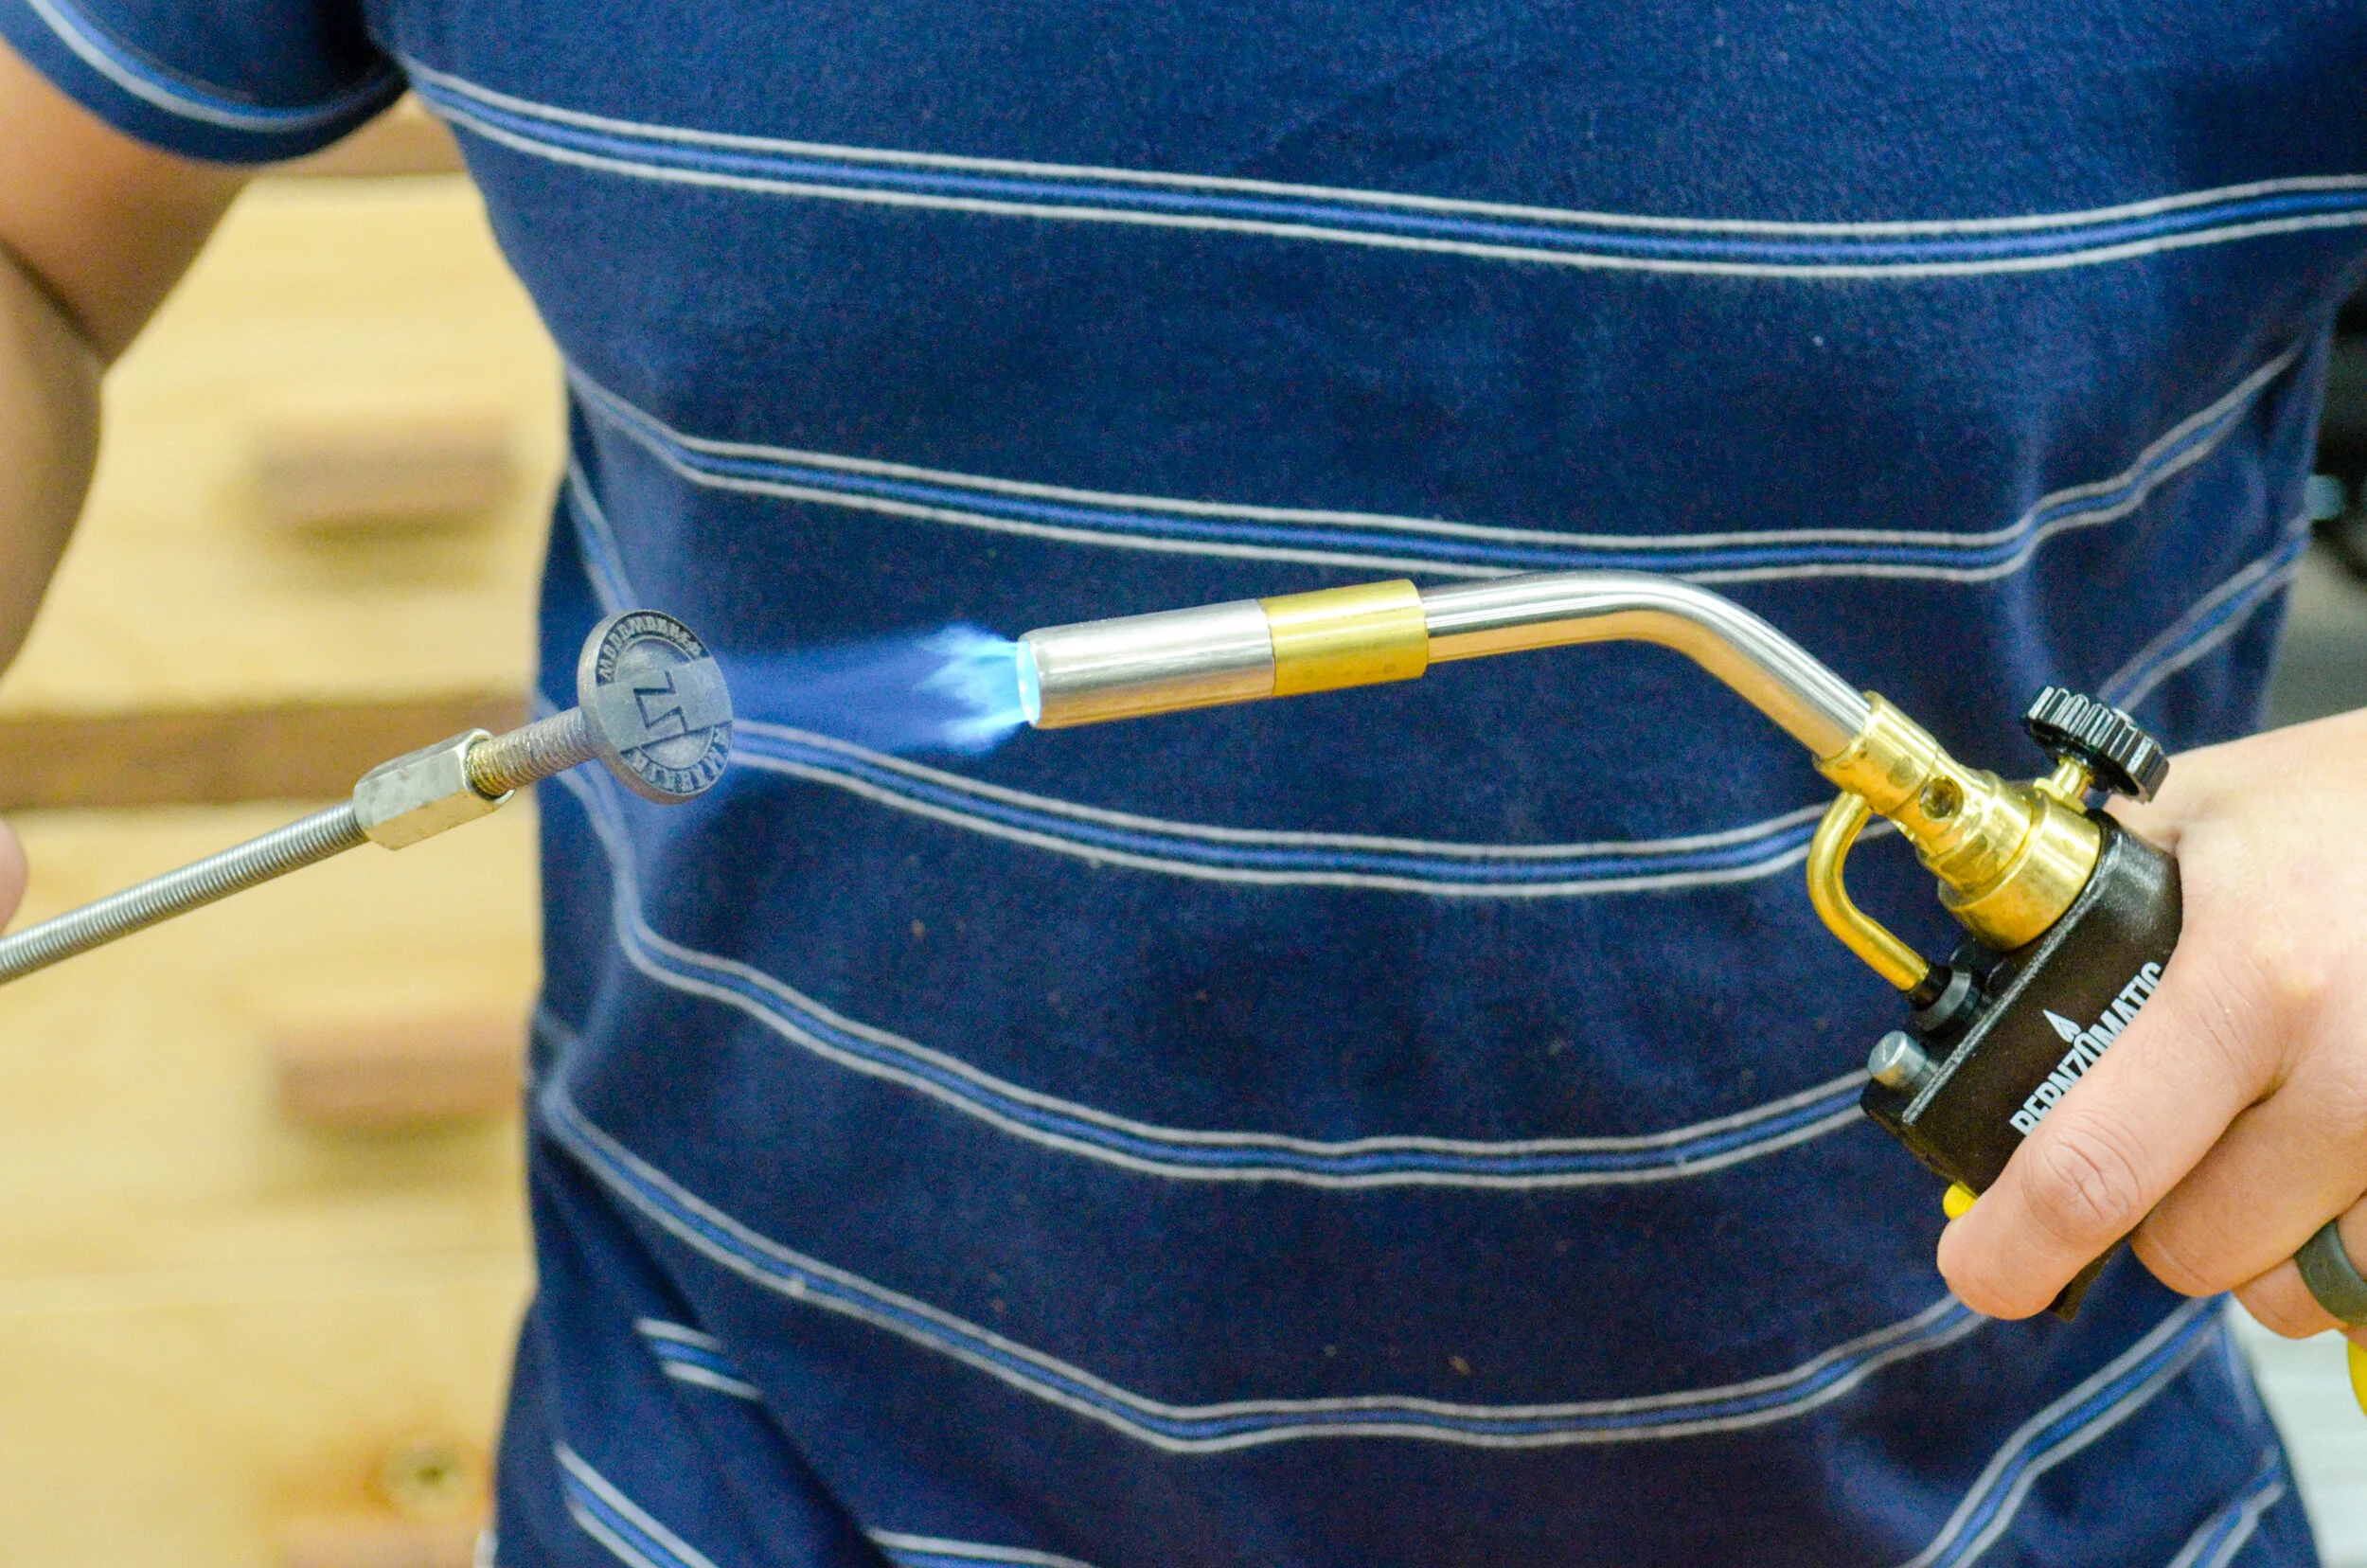
I’ve started using a branding iron with my logo to mark my work. Here are some things I’ve learning that may help you if you’ve thought about using a branding iron.
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
I’ve recently started using a branding iron to mark my woodworking. If you're thinking of using a branding iron, there are a couple of things you’ll need to consider. First, you’ll need a relatively simple logo, or signature. Logos or signatures with too many loops or too tight of a radius between letters and figures can become muddled when branded onto wood. Keep the lettering and shapes simple with easily definable space between objects. You’ll then need the artwork to be converted to a vector graphic so that your branding iron company can produce the iron.
To properly brand your work, you'll need a heat source and a method to apply even pressure across the whole image. I use a Bernzomatic TS8000KC Premium Torch Kit as my heat source. Many branding iron companies will offer an electric heat source. However, I feel as though using propane torch produces a lot of heat in a relatively fast amount of time.
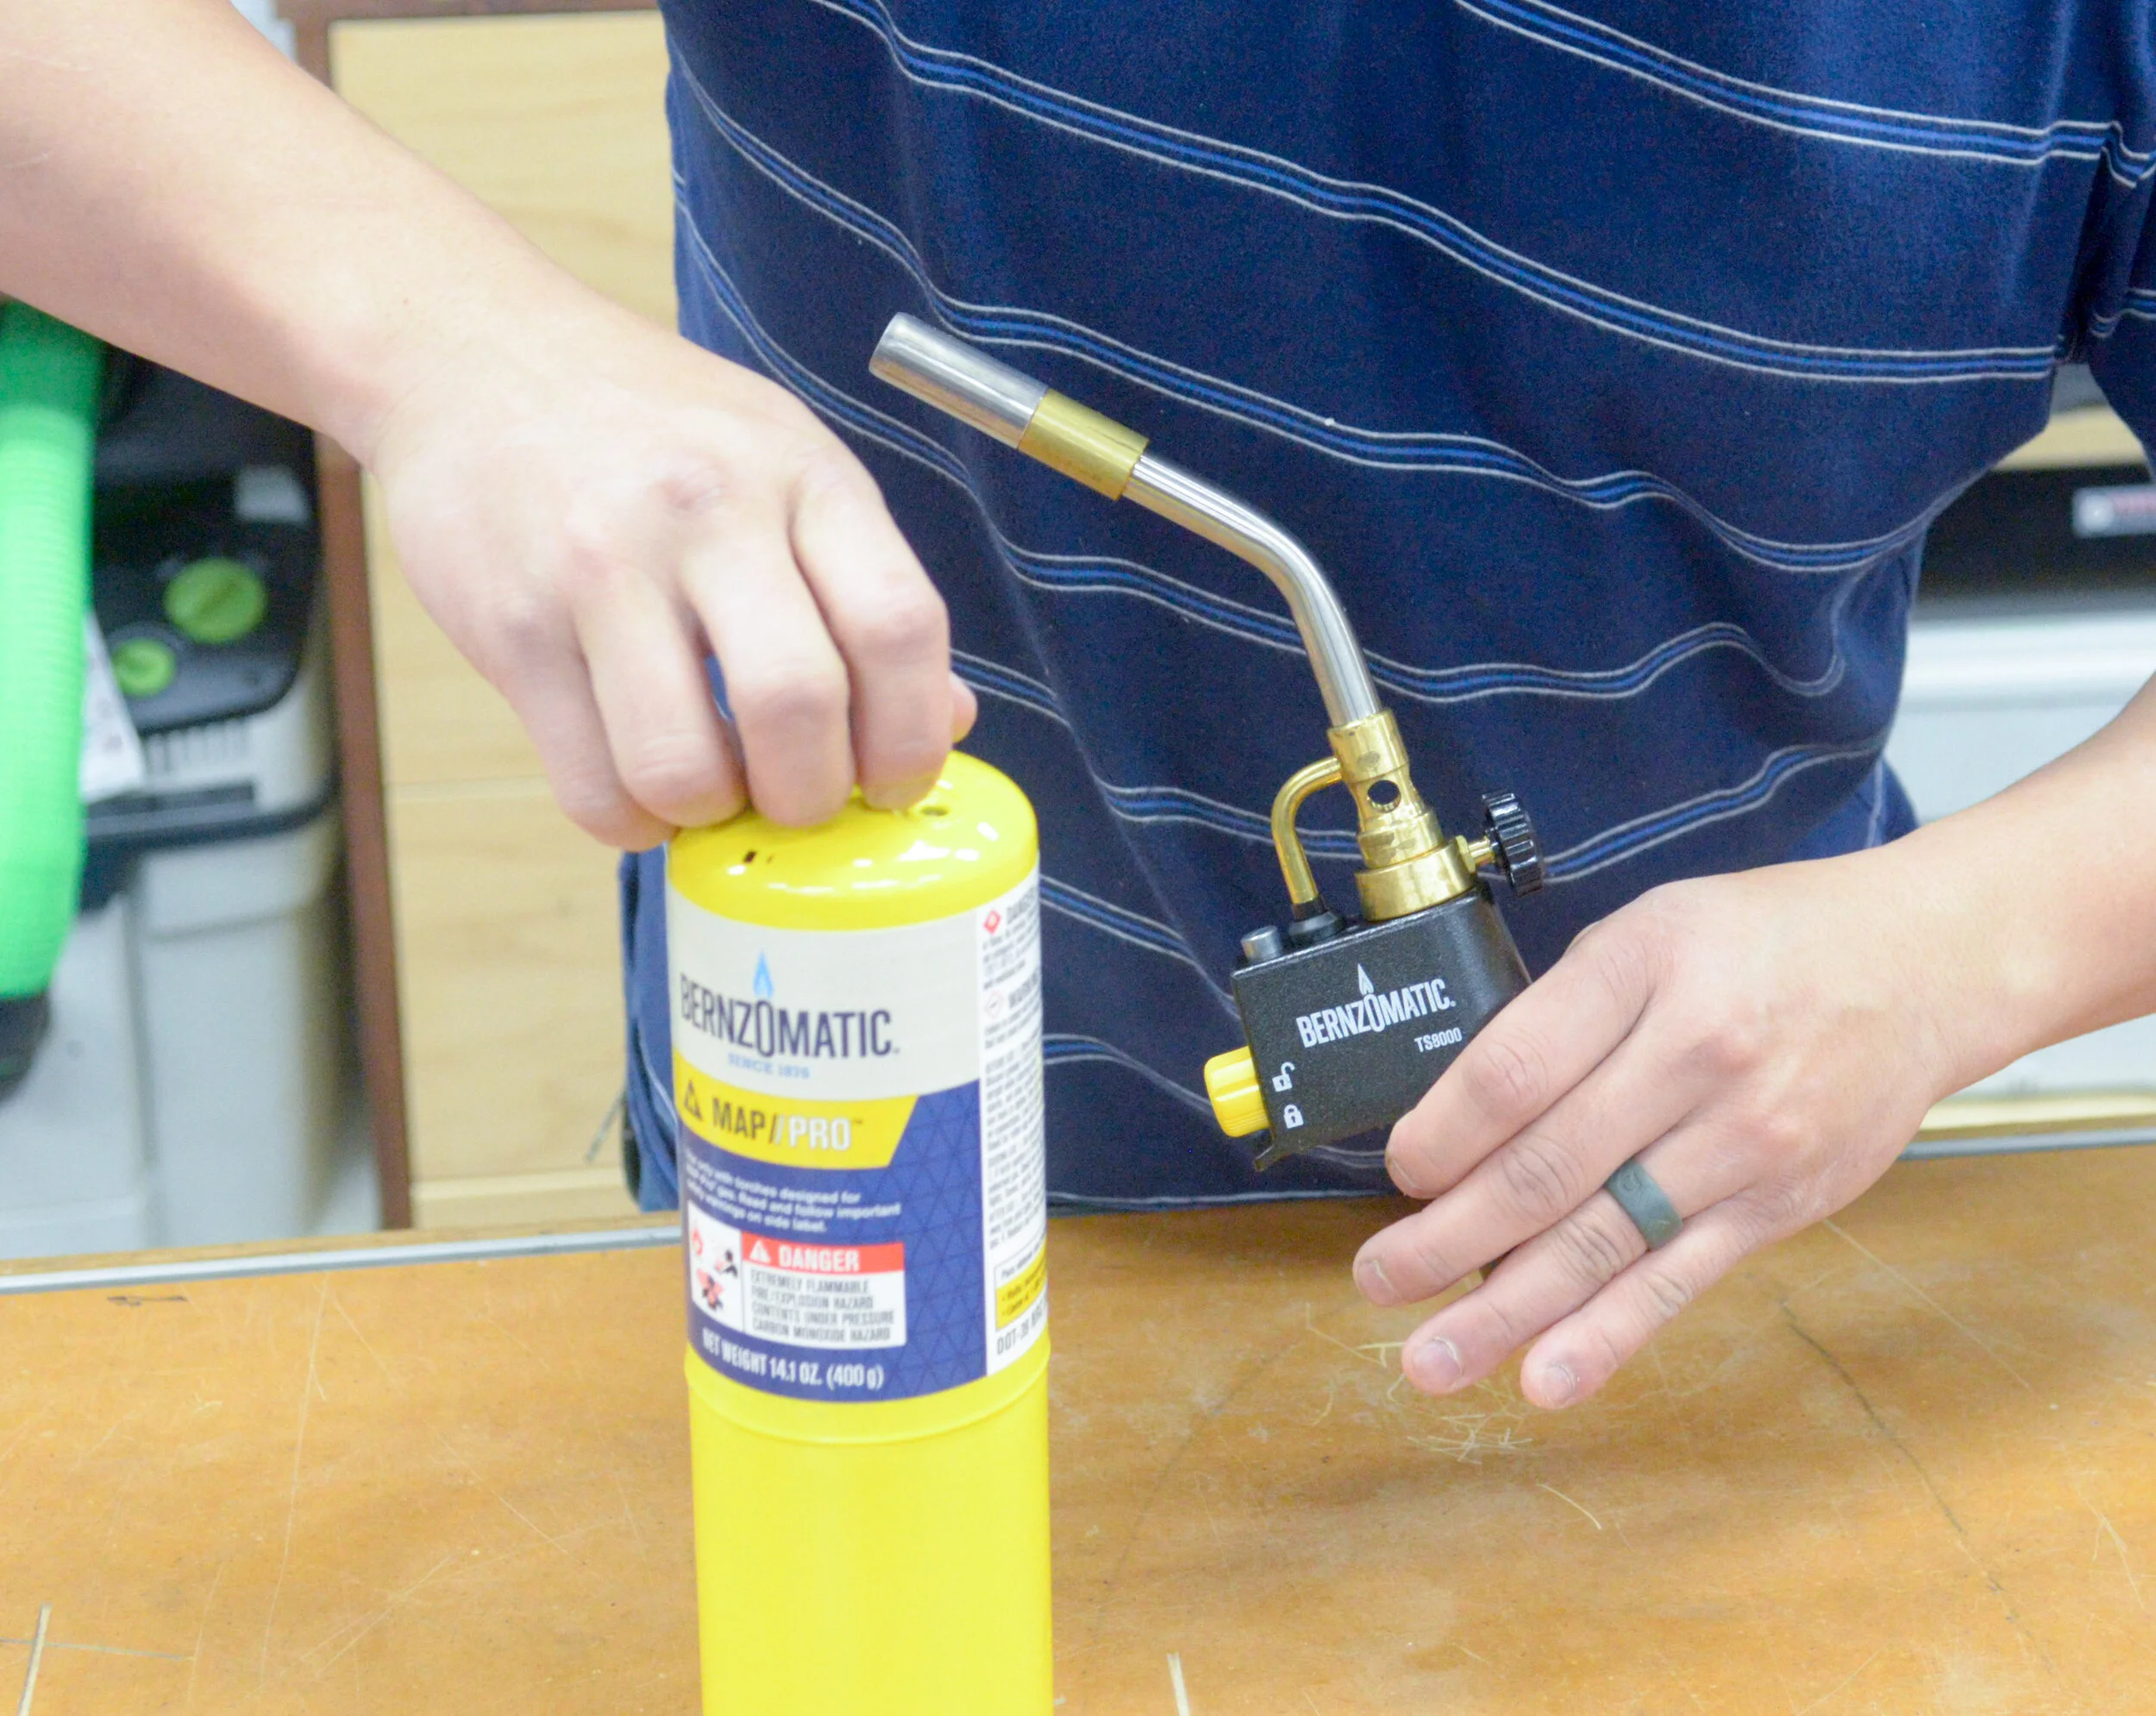
Using a Bernzomatic Torch Kit as a heat source.
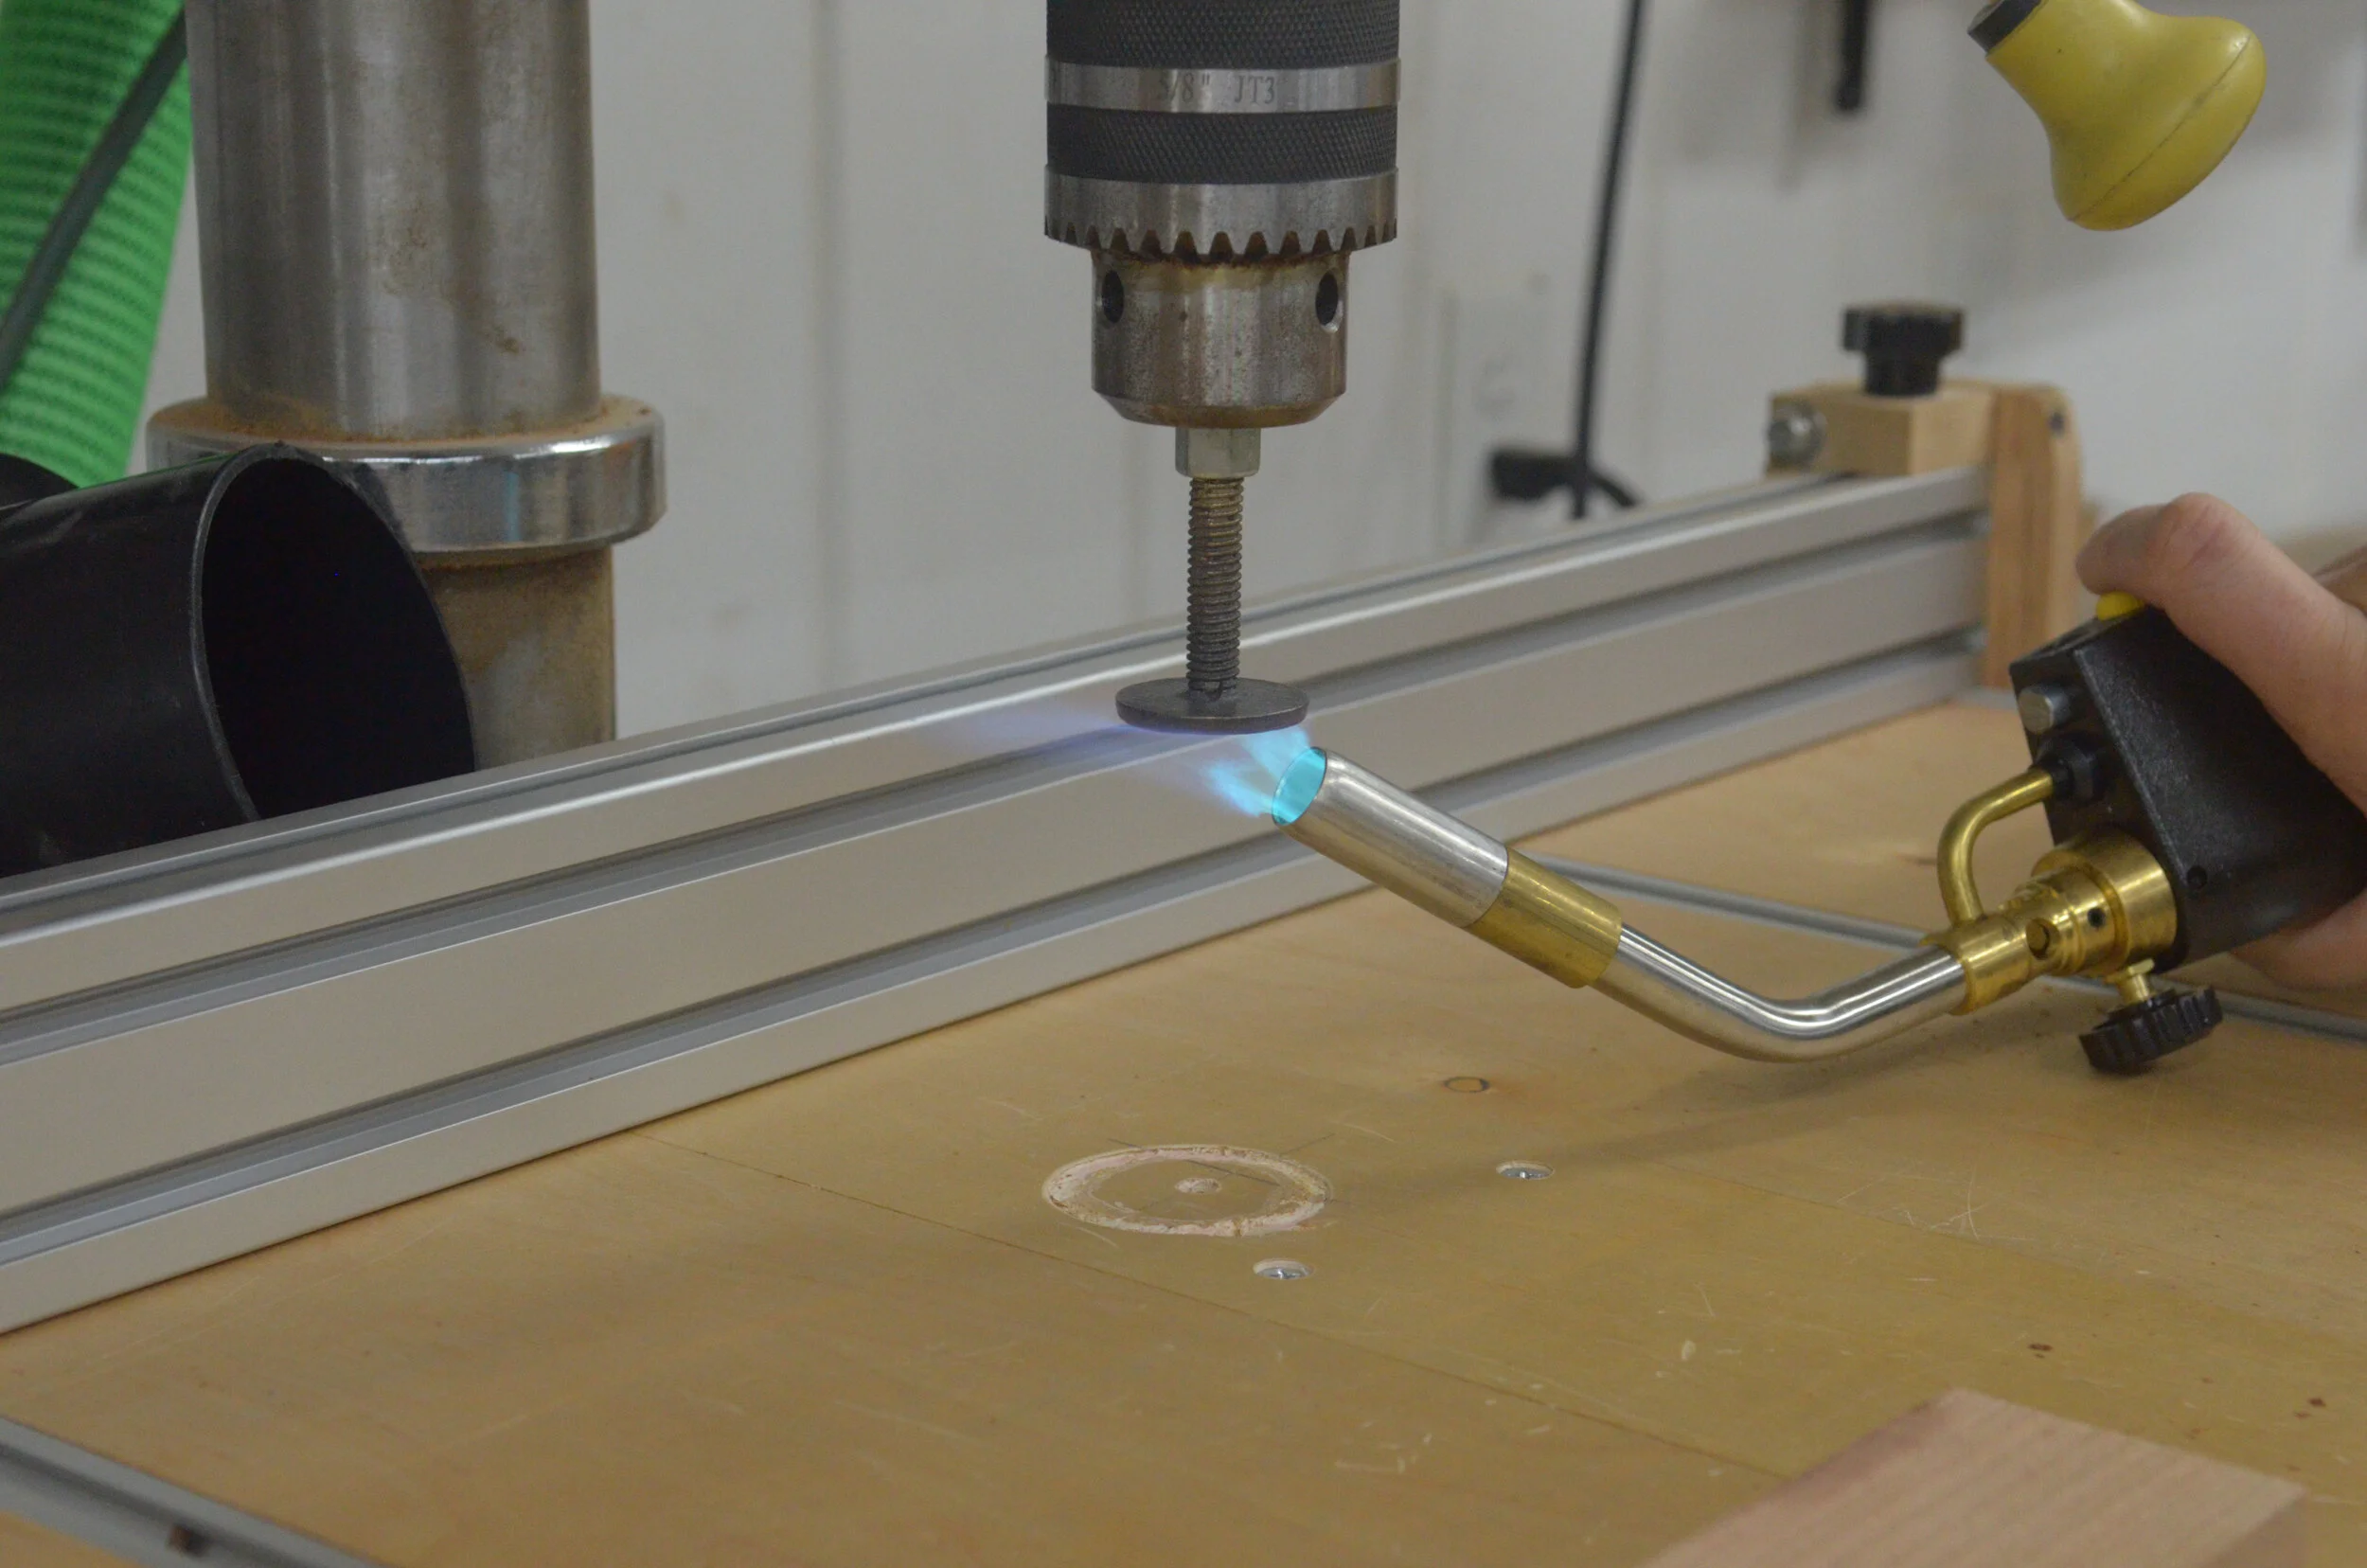
To apply even pressure across the entire logo, I chuck my branding iron into my drill press. My branding iron actually came with a handle but I am unable to apply even pressure using the included handle. Once the iron is chucked into my drill press, I’ll use my torch to heat up the iron.
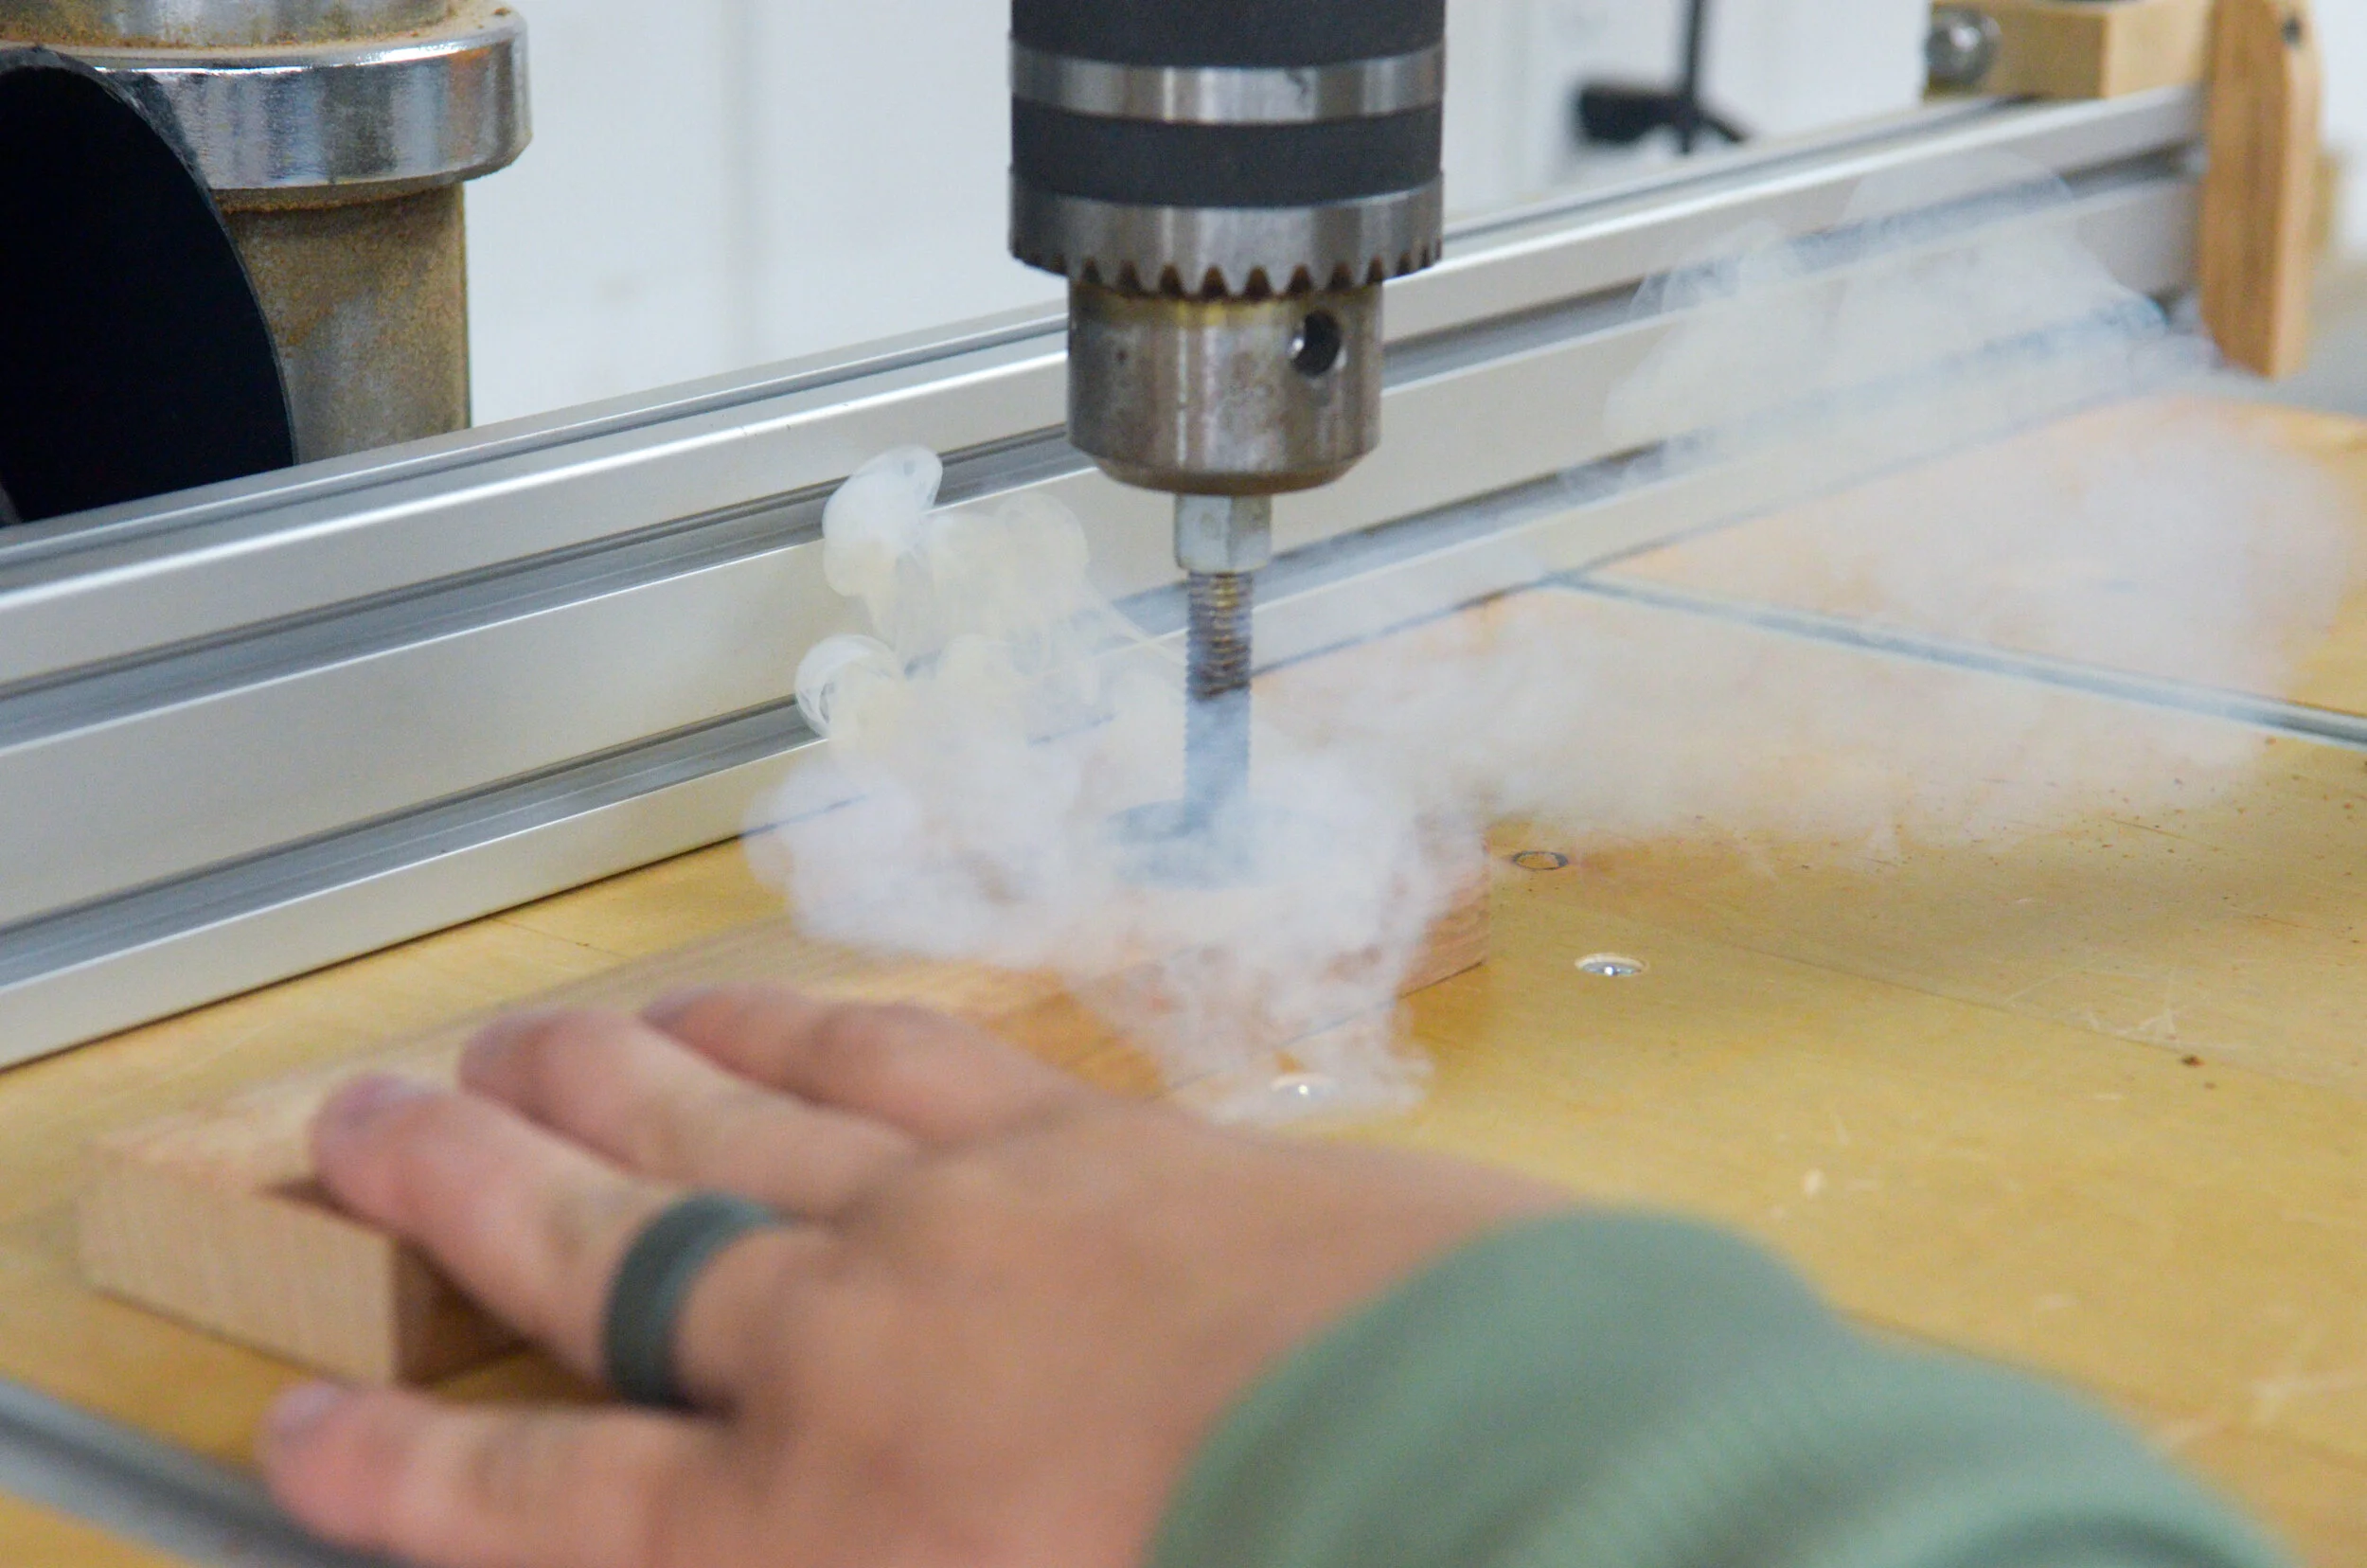
Using the drill gives me great results and ensures that I don’t create an uneven brand.
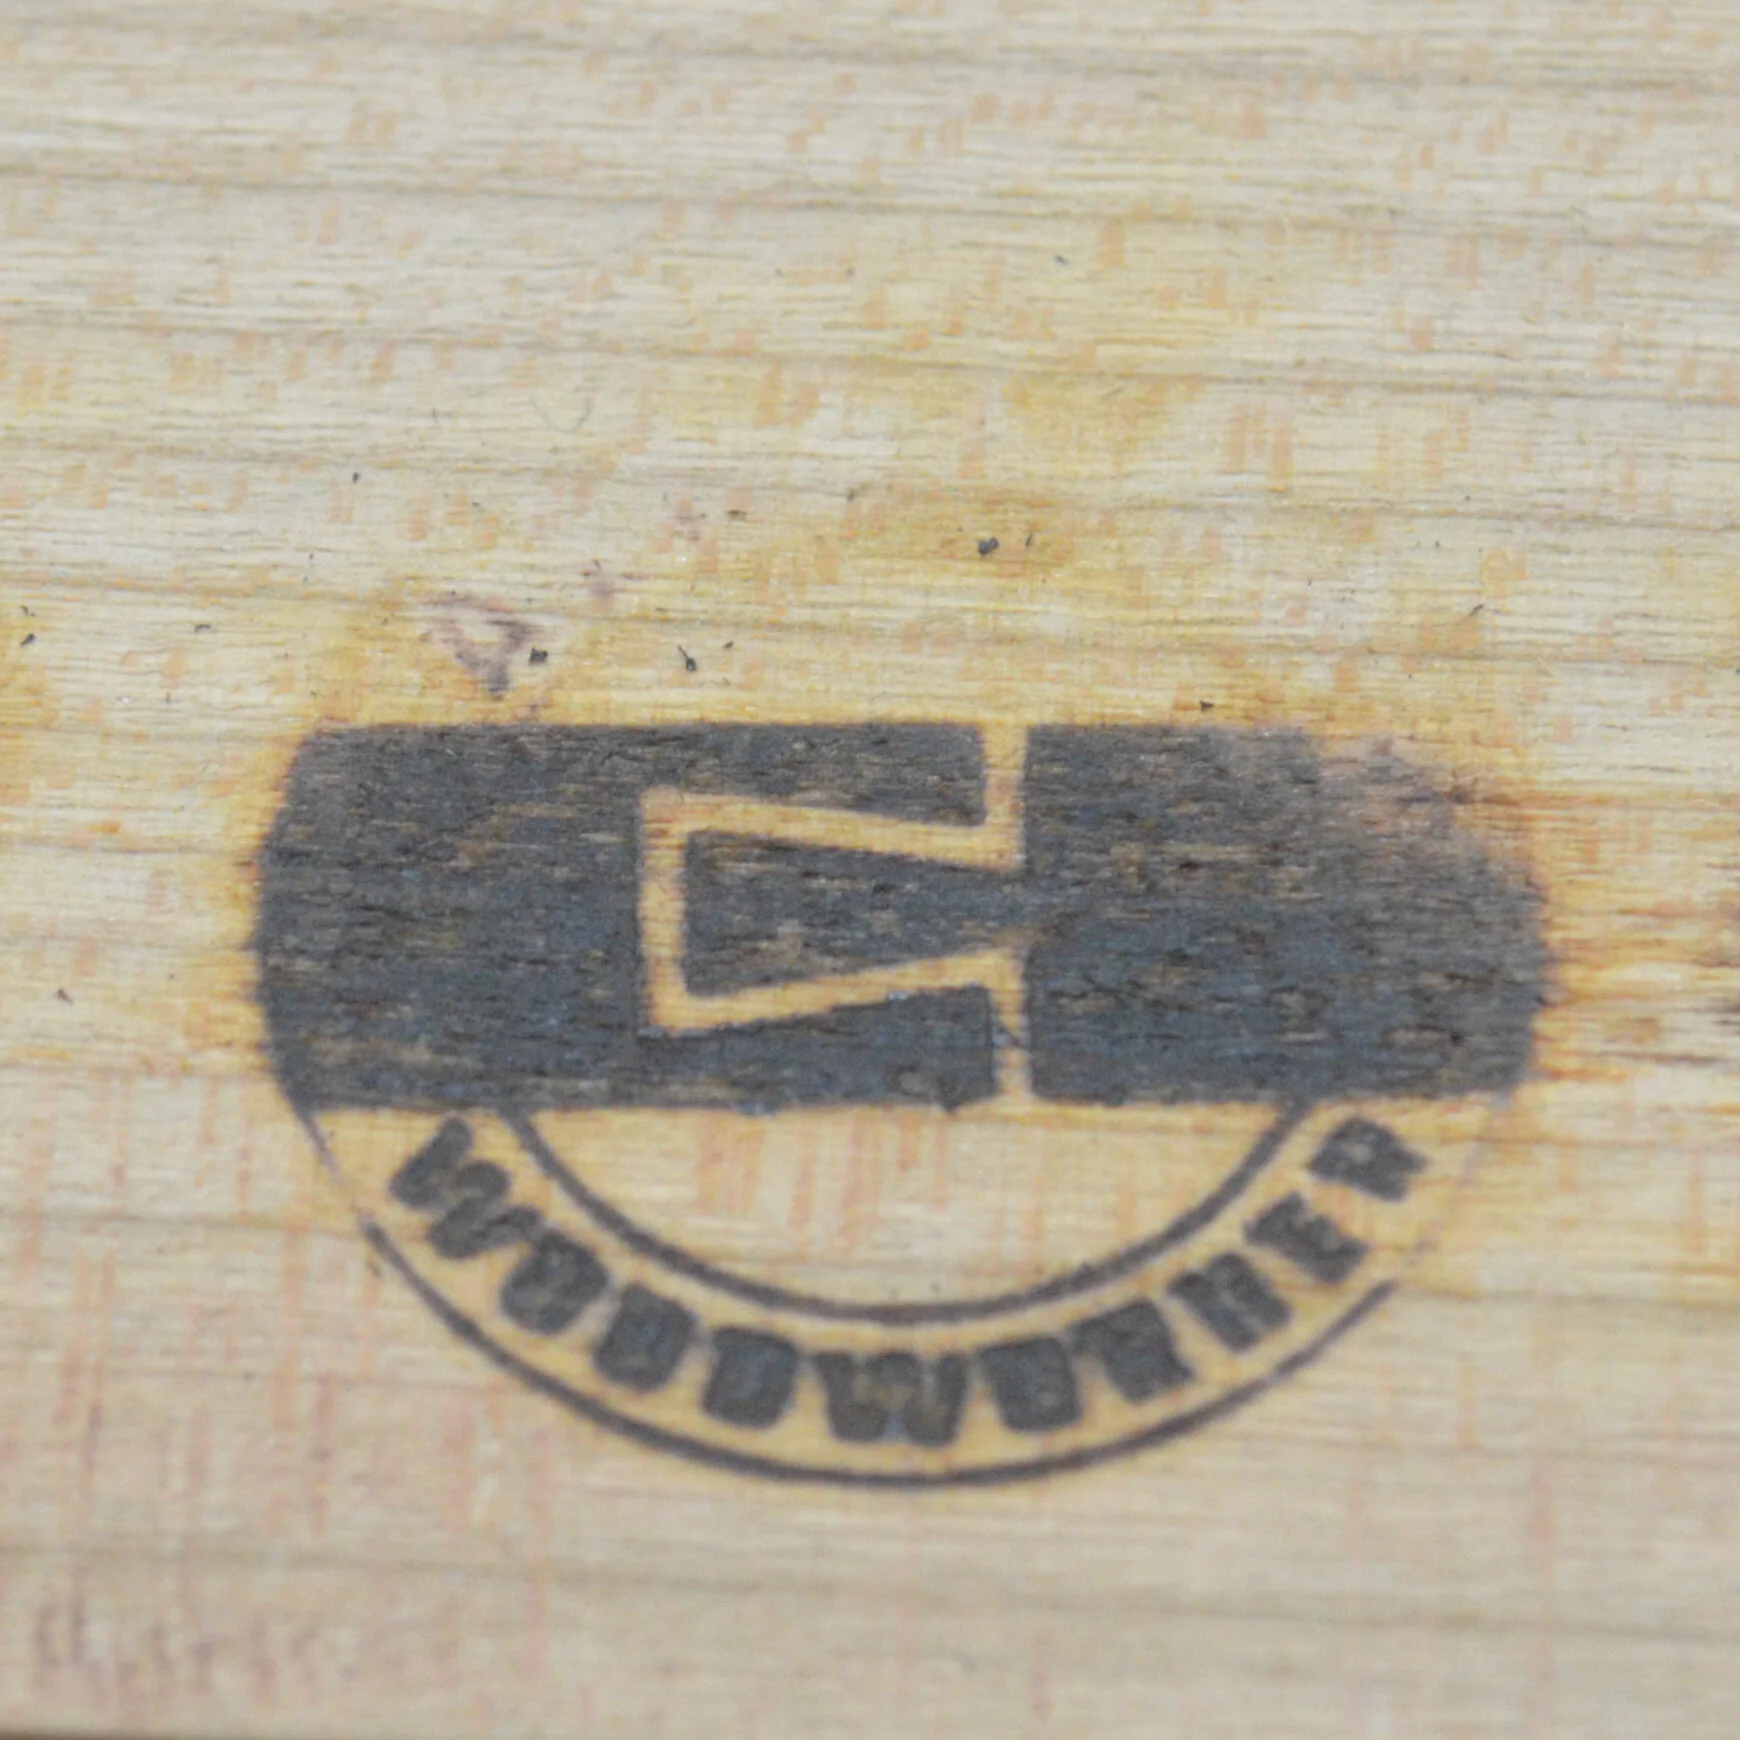
Here’s an example of an uneven brand. I you are using a drill press, you’ll need to adjust your iron, the chuck setup, or your drill press table.
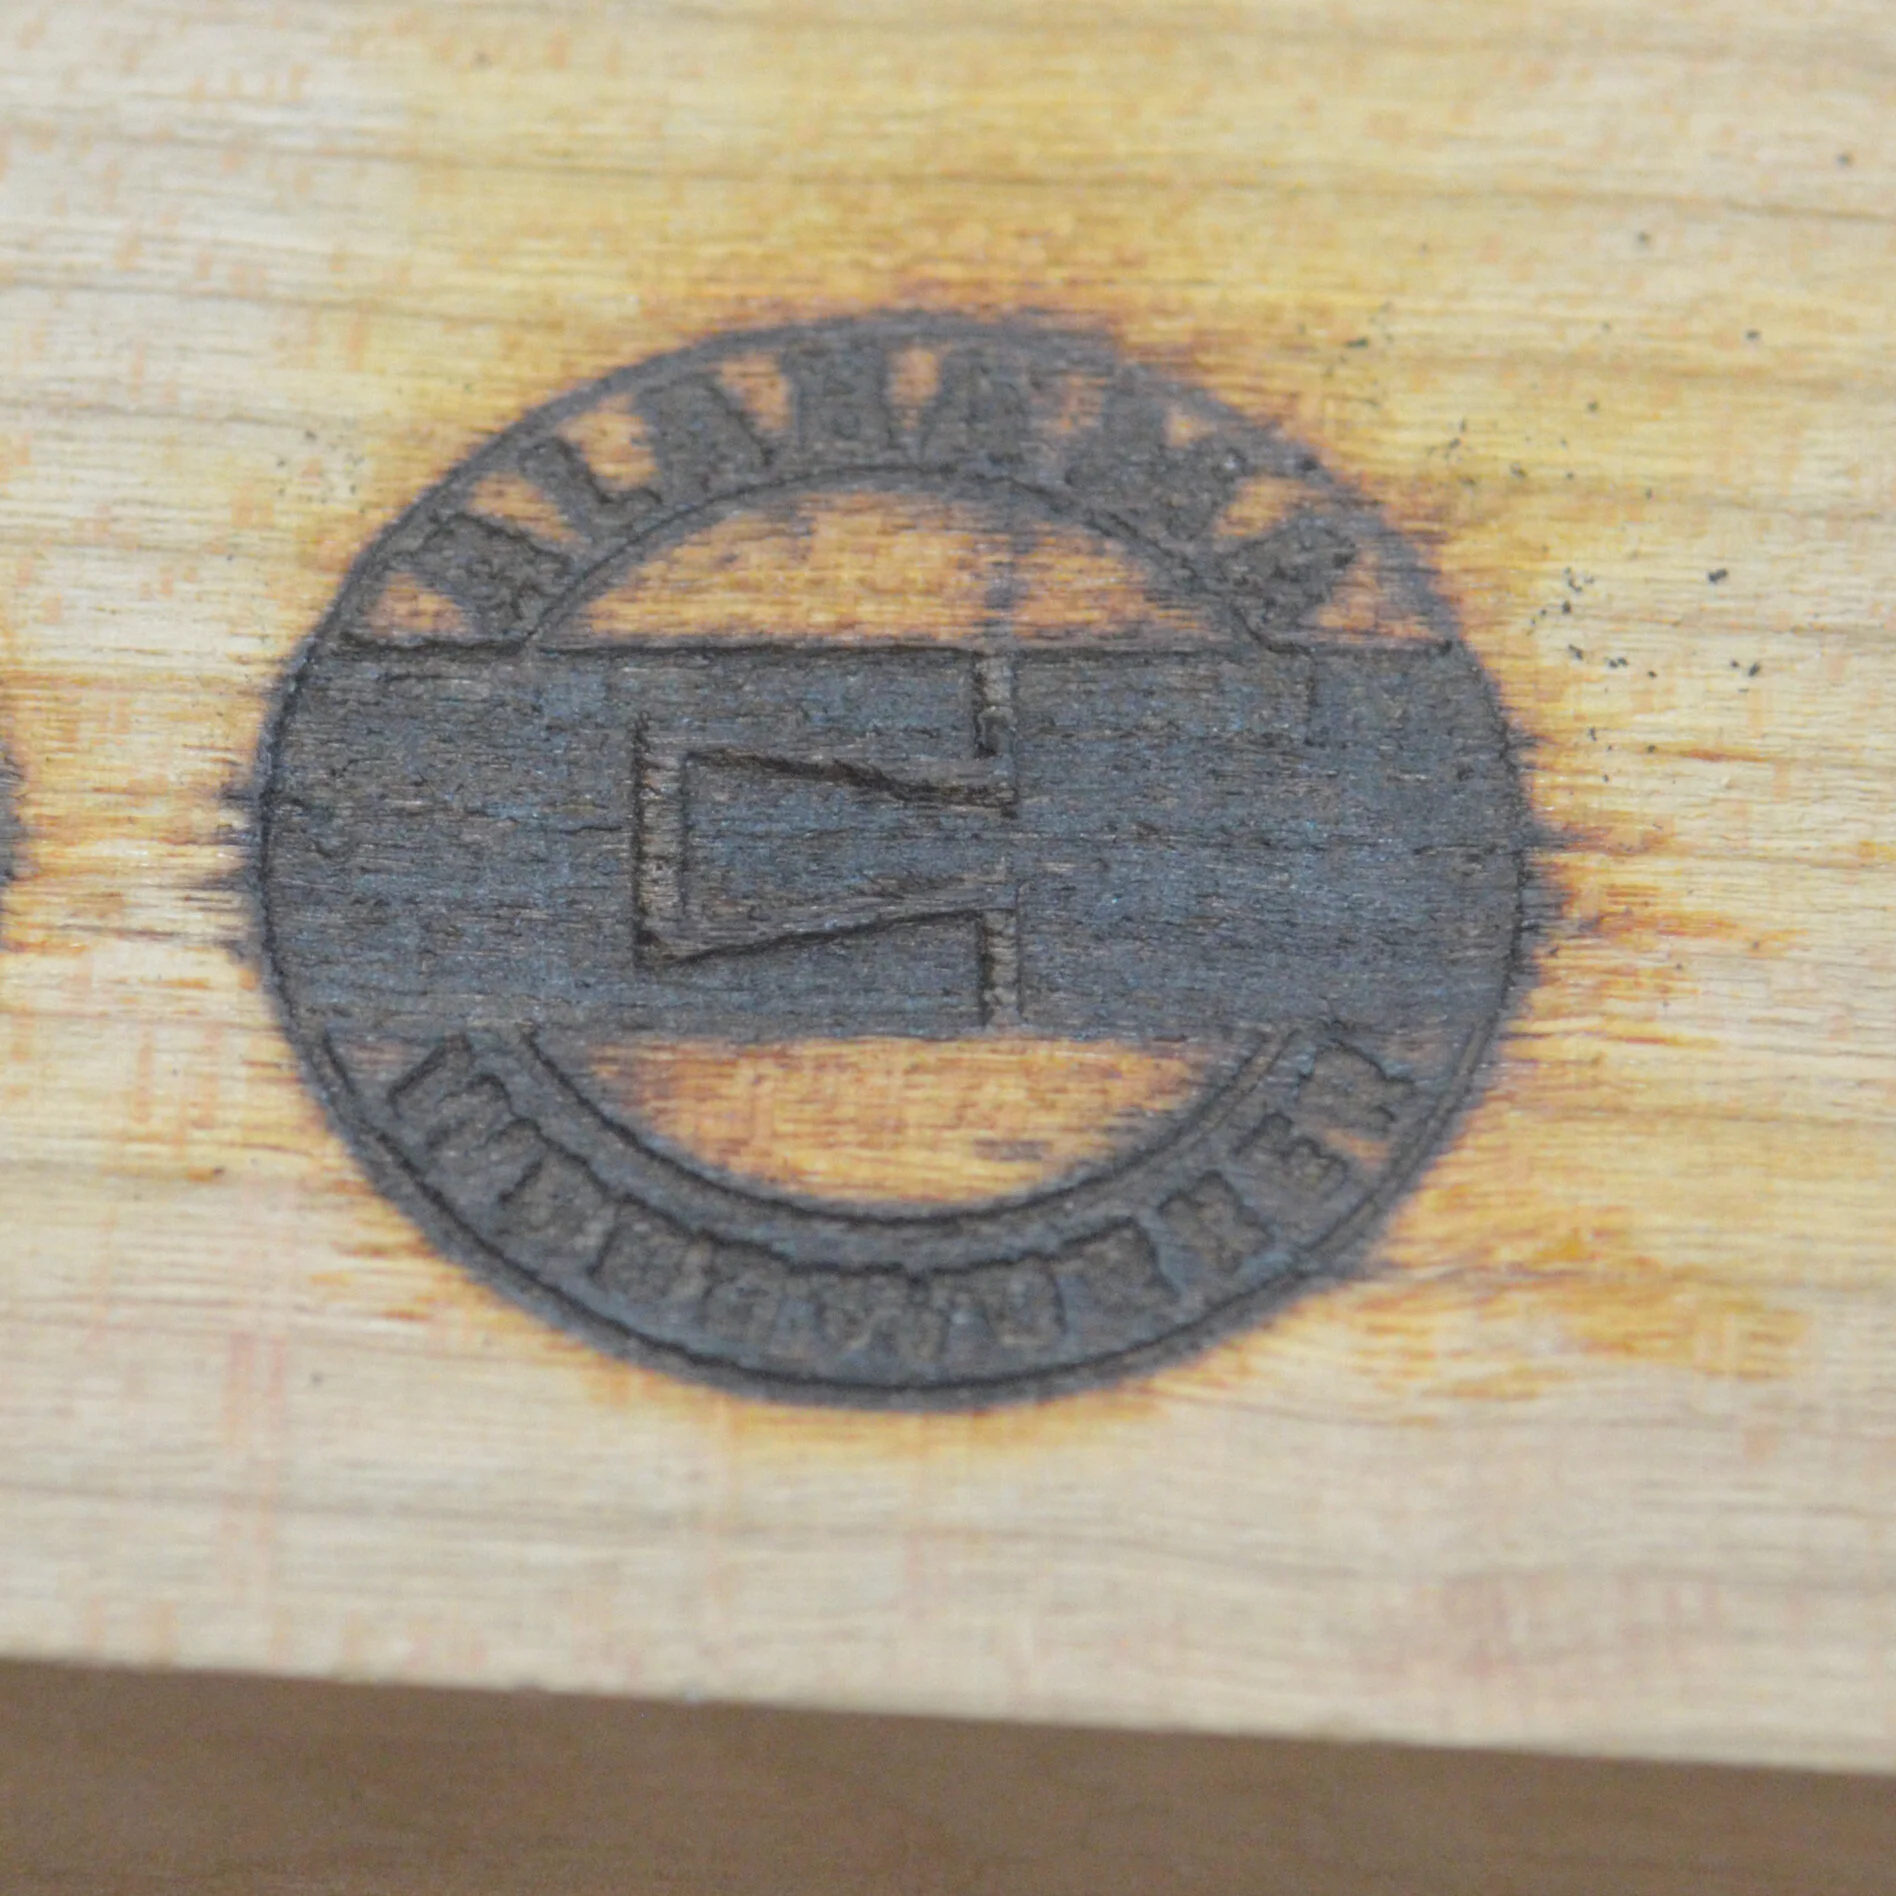
If the iron is too hot, or applied for too long, you’ll get an overburn. You can try to fix this problem by sanding to clean up the excess burning.
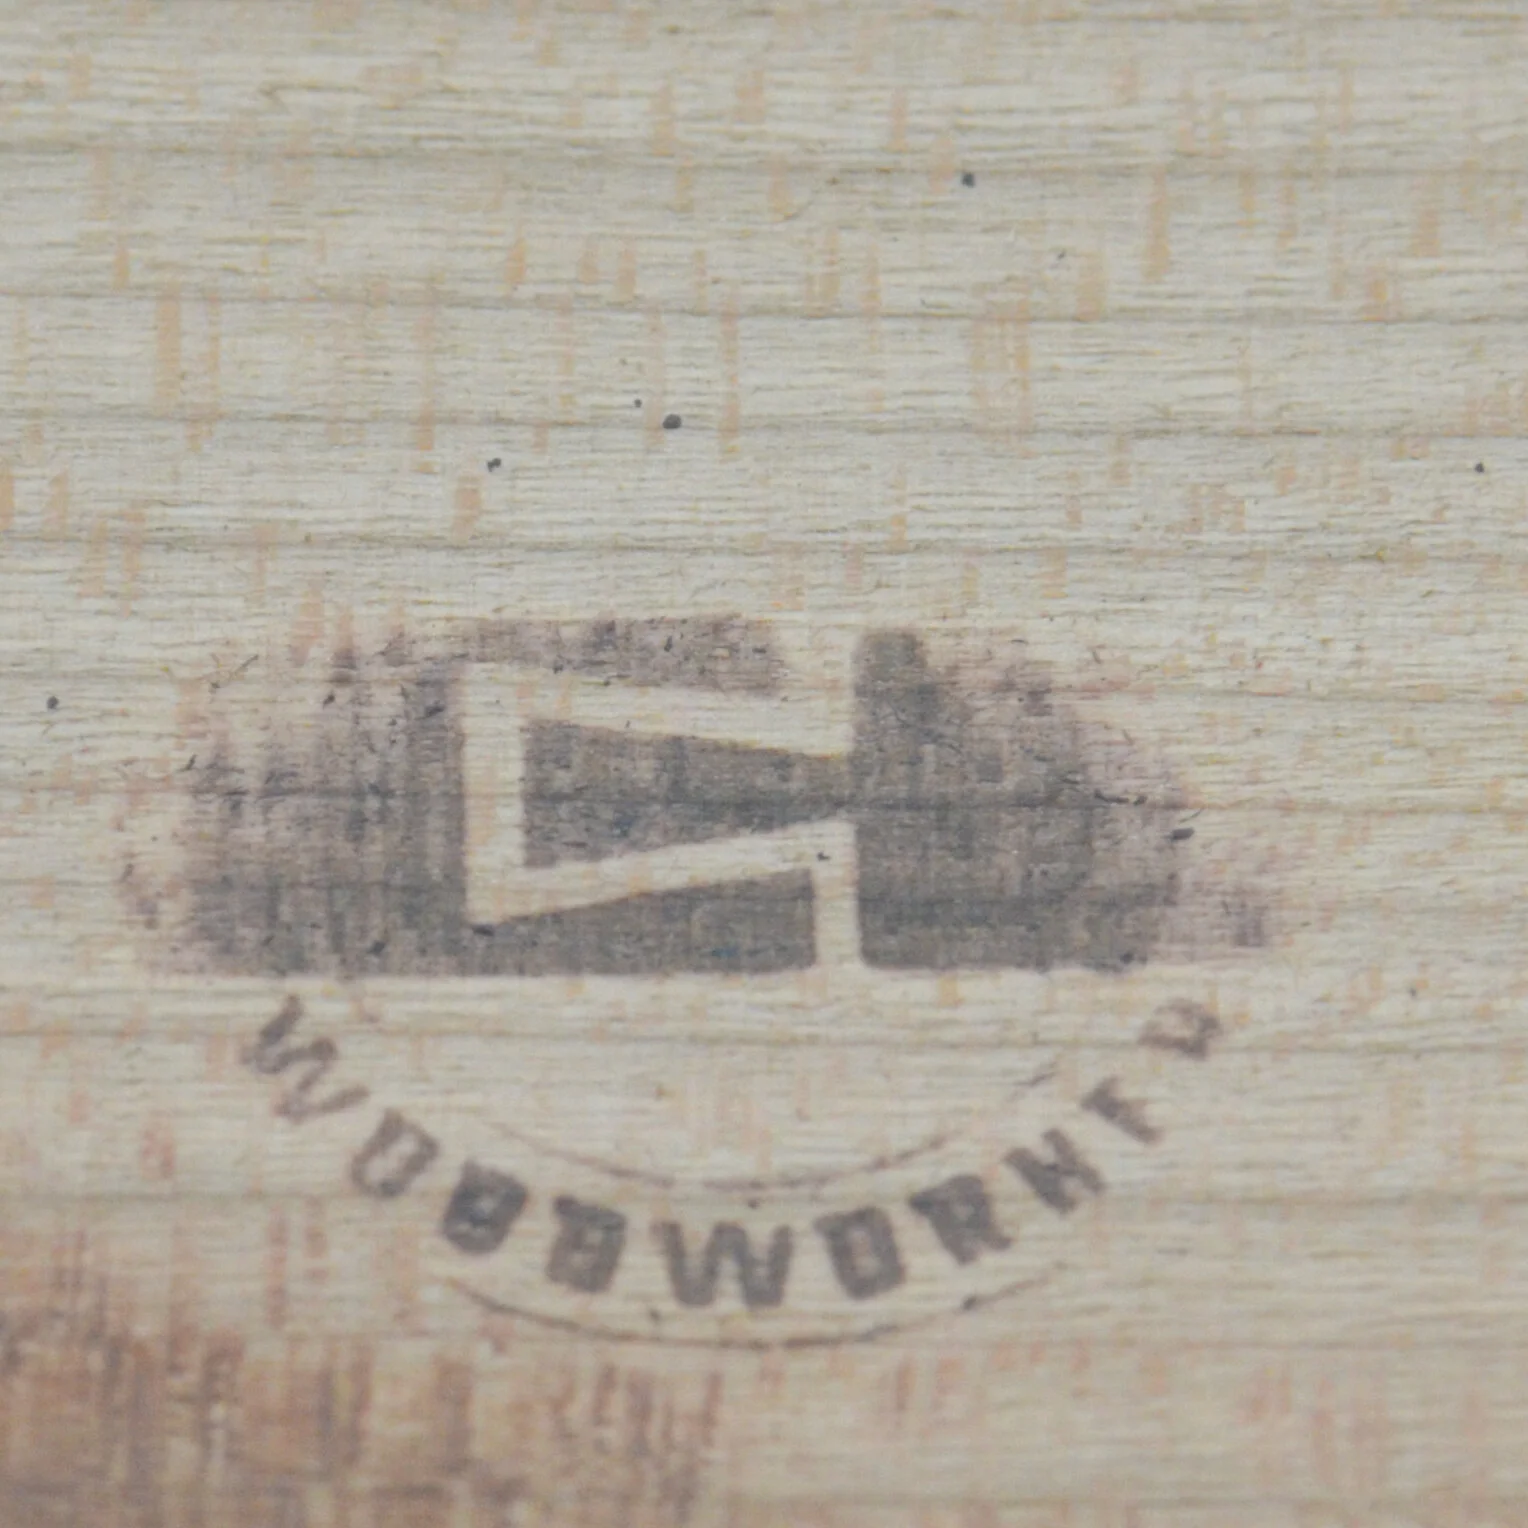
If you get an underburn and using a drill press, you can reapply the iron so long as you haven’t moved your workpiece.
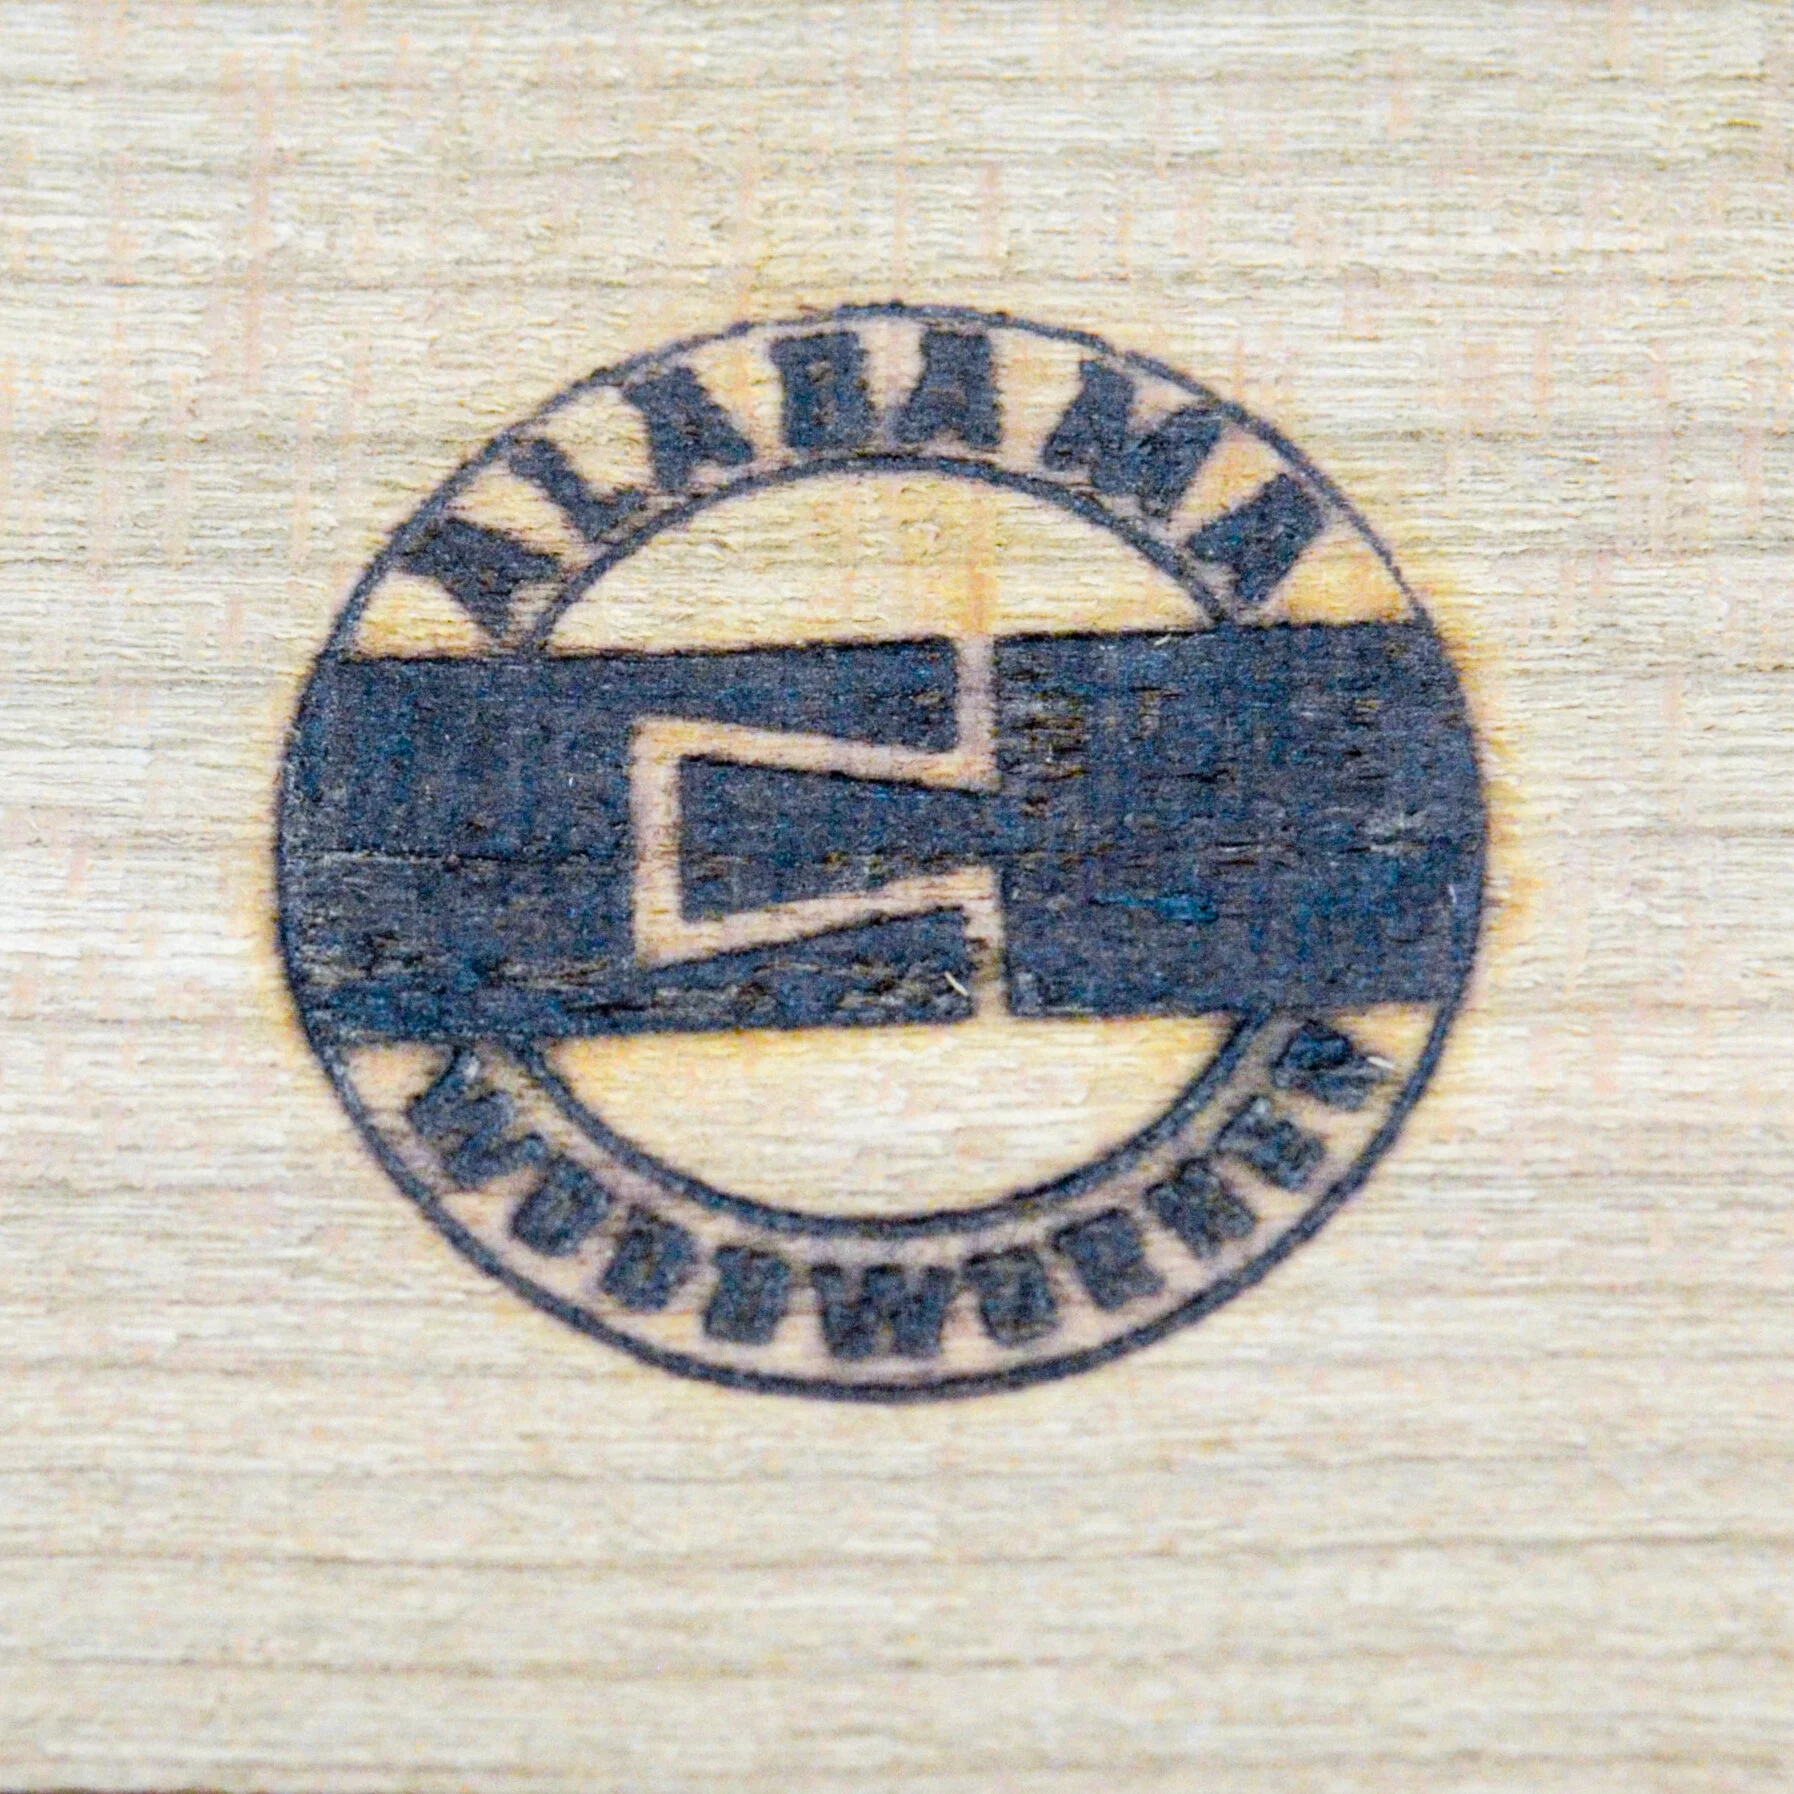
A properly applied brand will give you a clear logo that will remain on your workpiece for life.
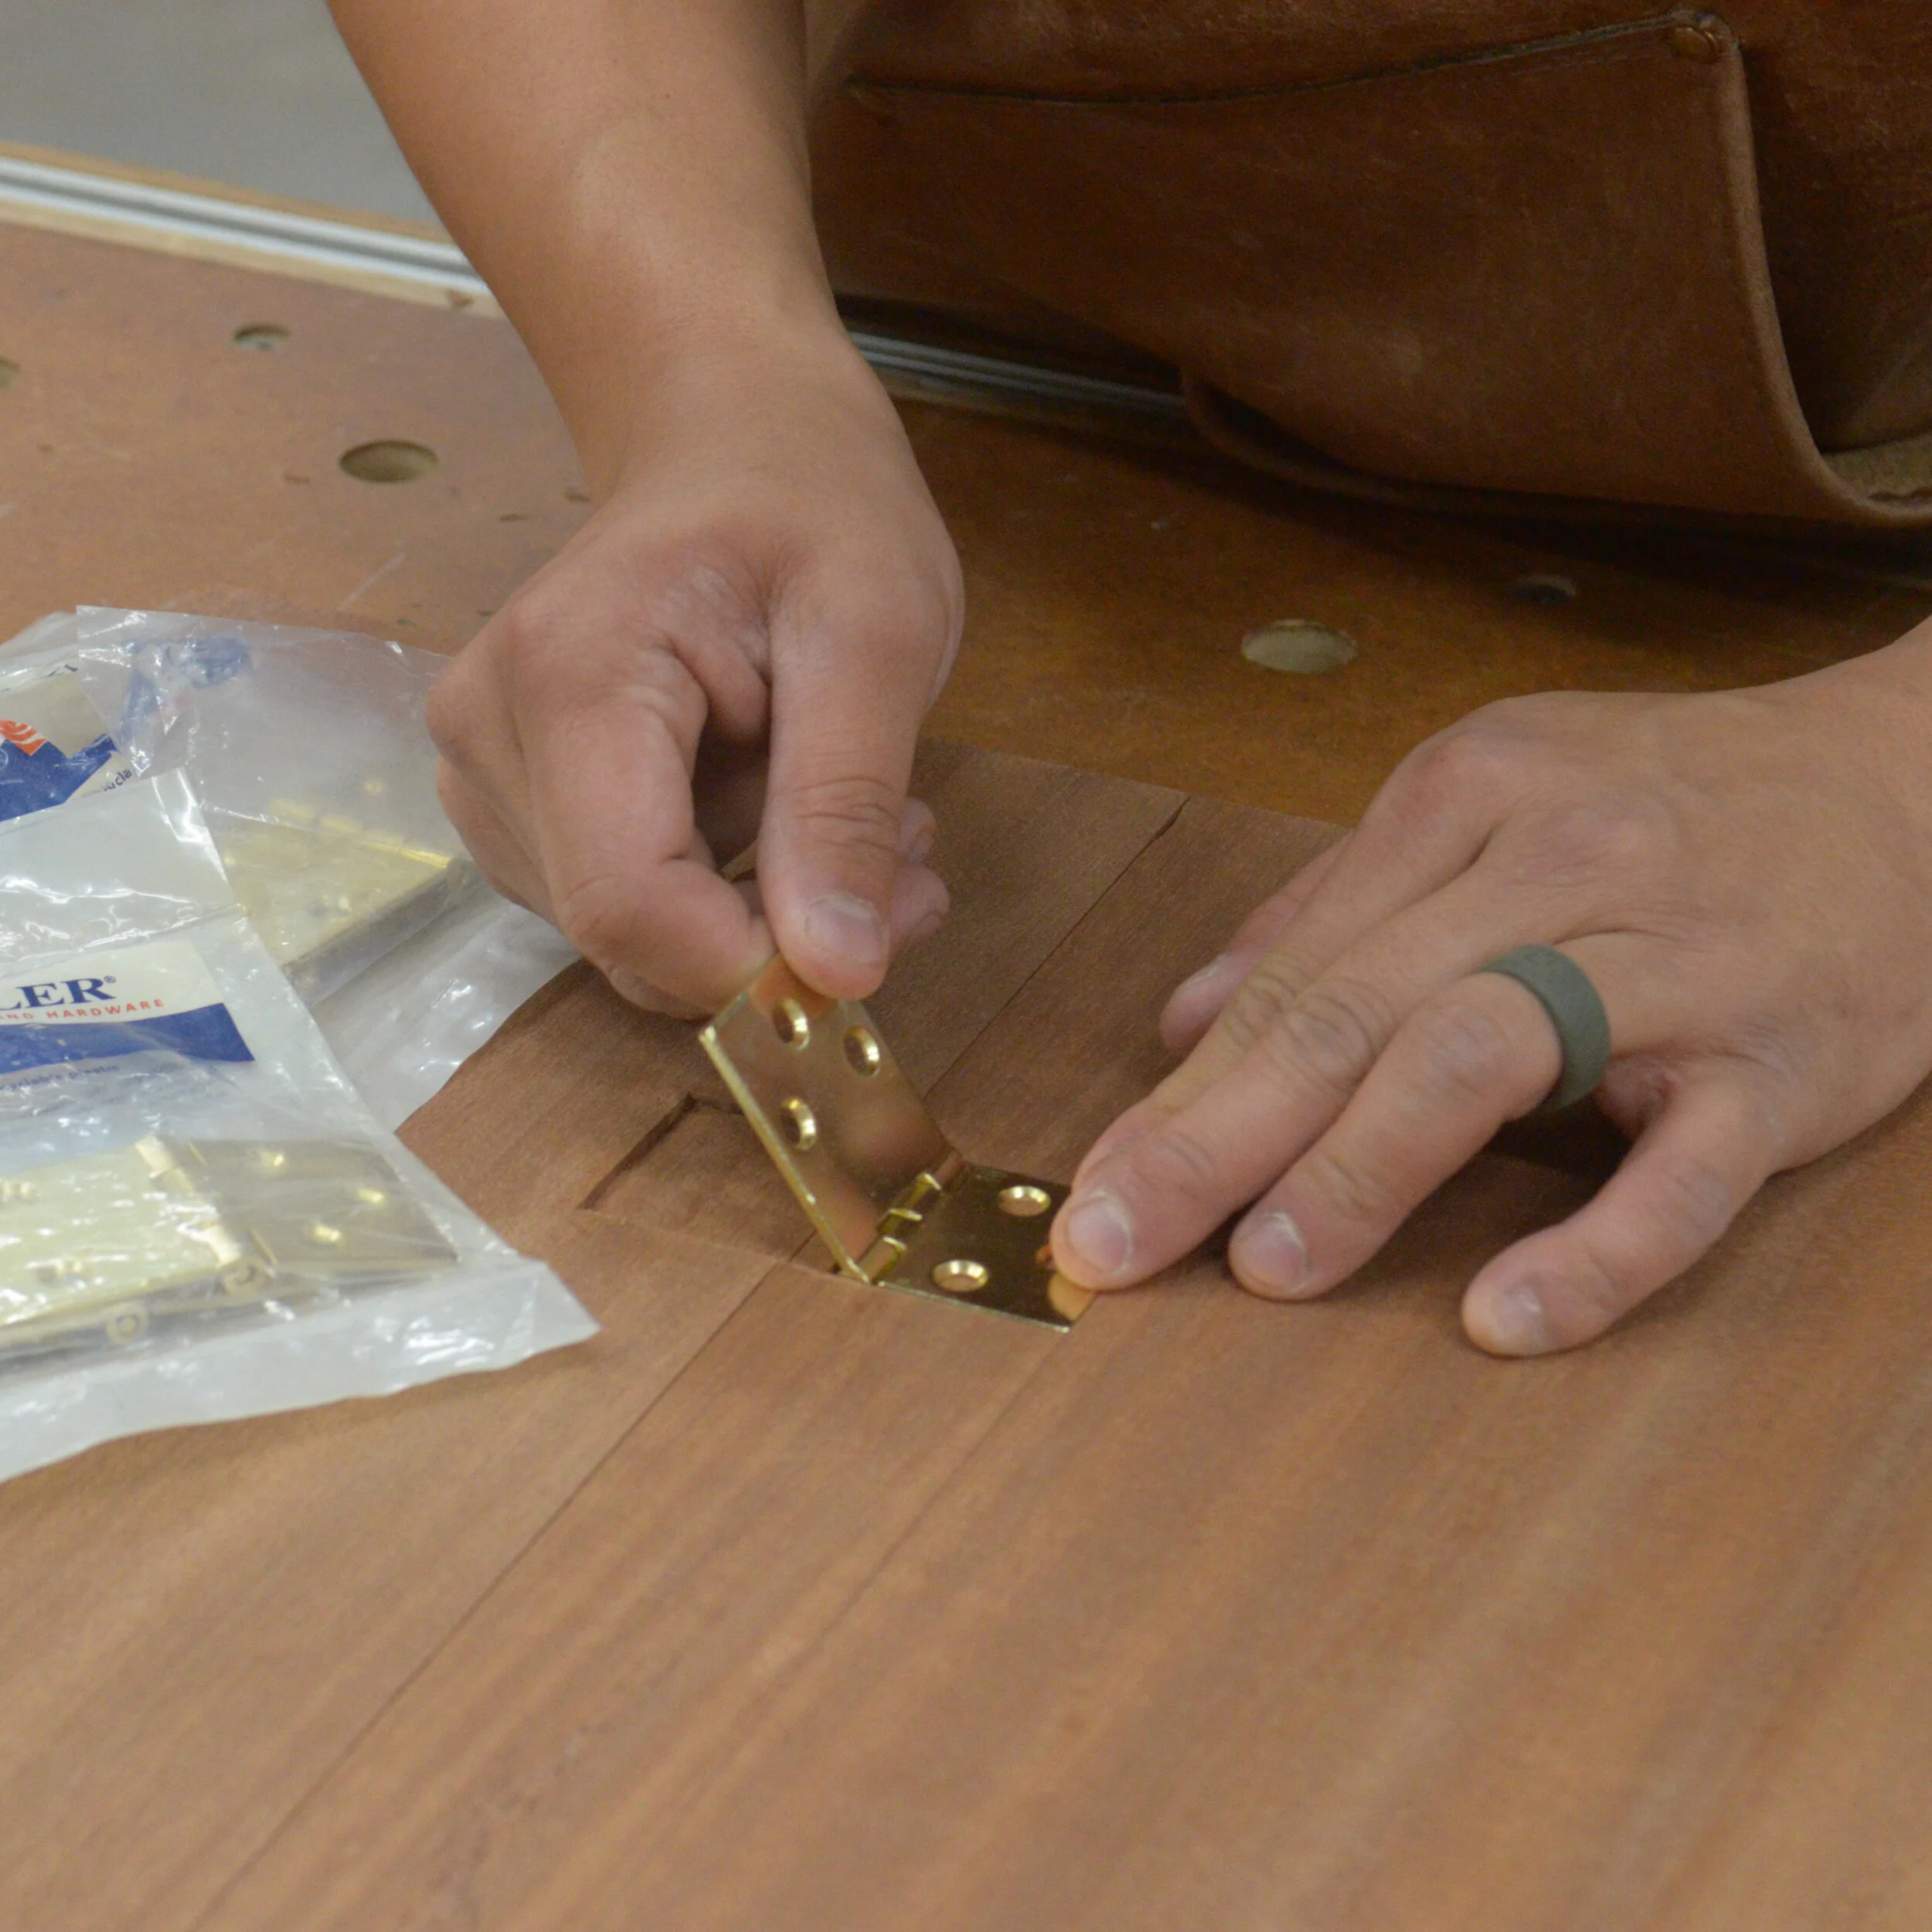
Routing Mortises for Drop Leaf Hinges on a Rule Joint
The mortises for drop leaf hinges requires a single template and spacer for the leaves and barrel of the hinge.
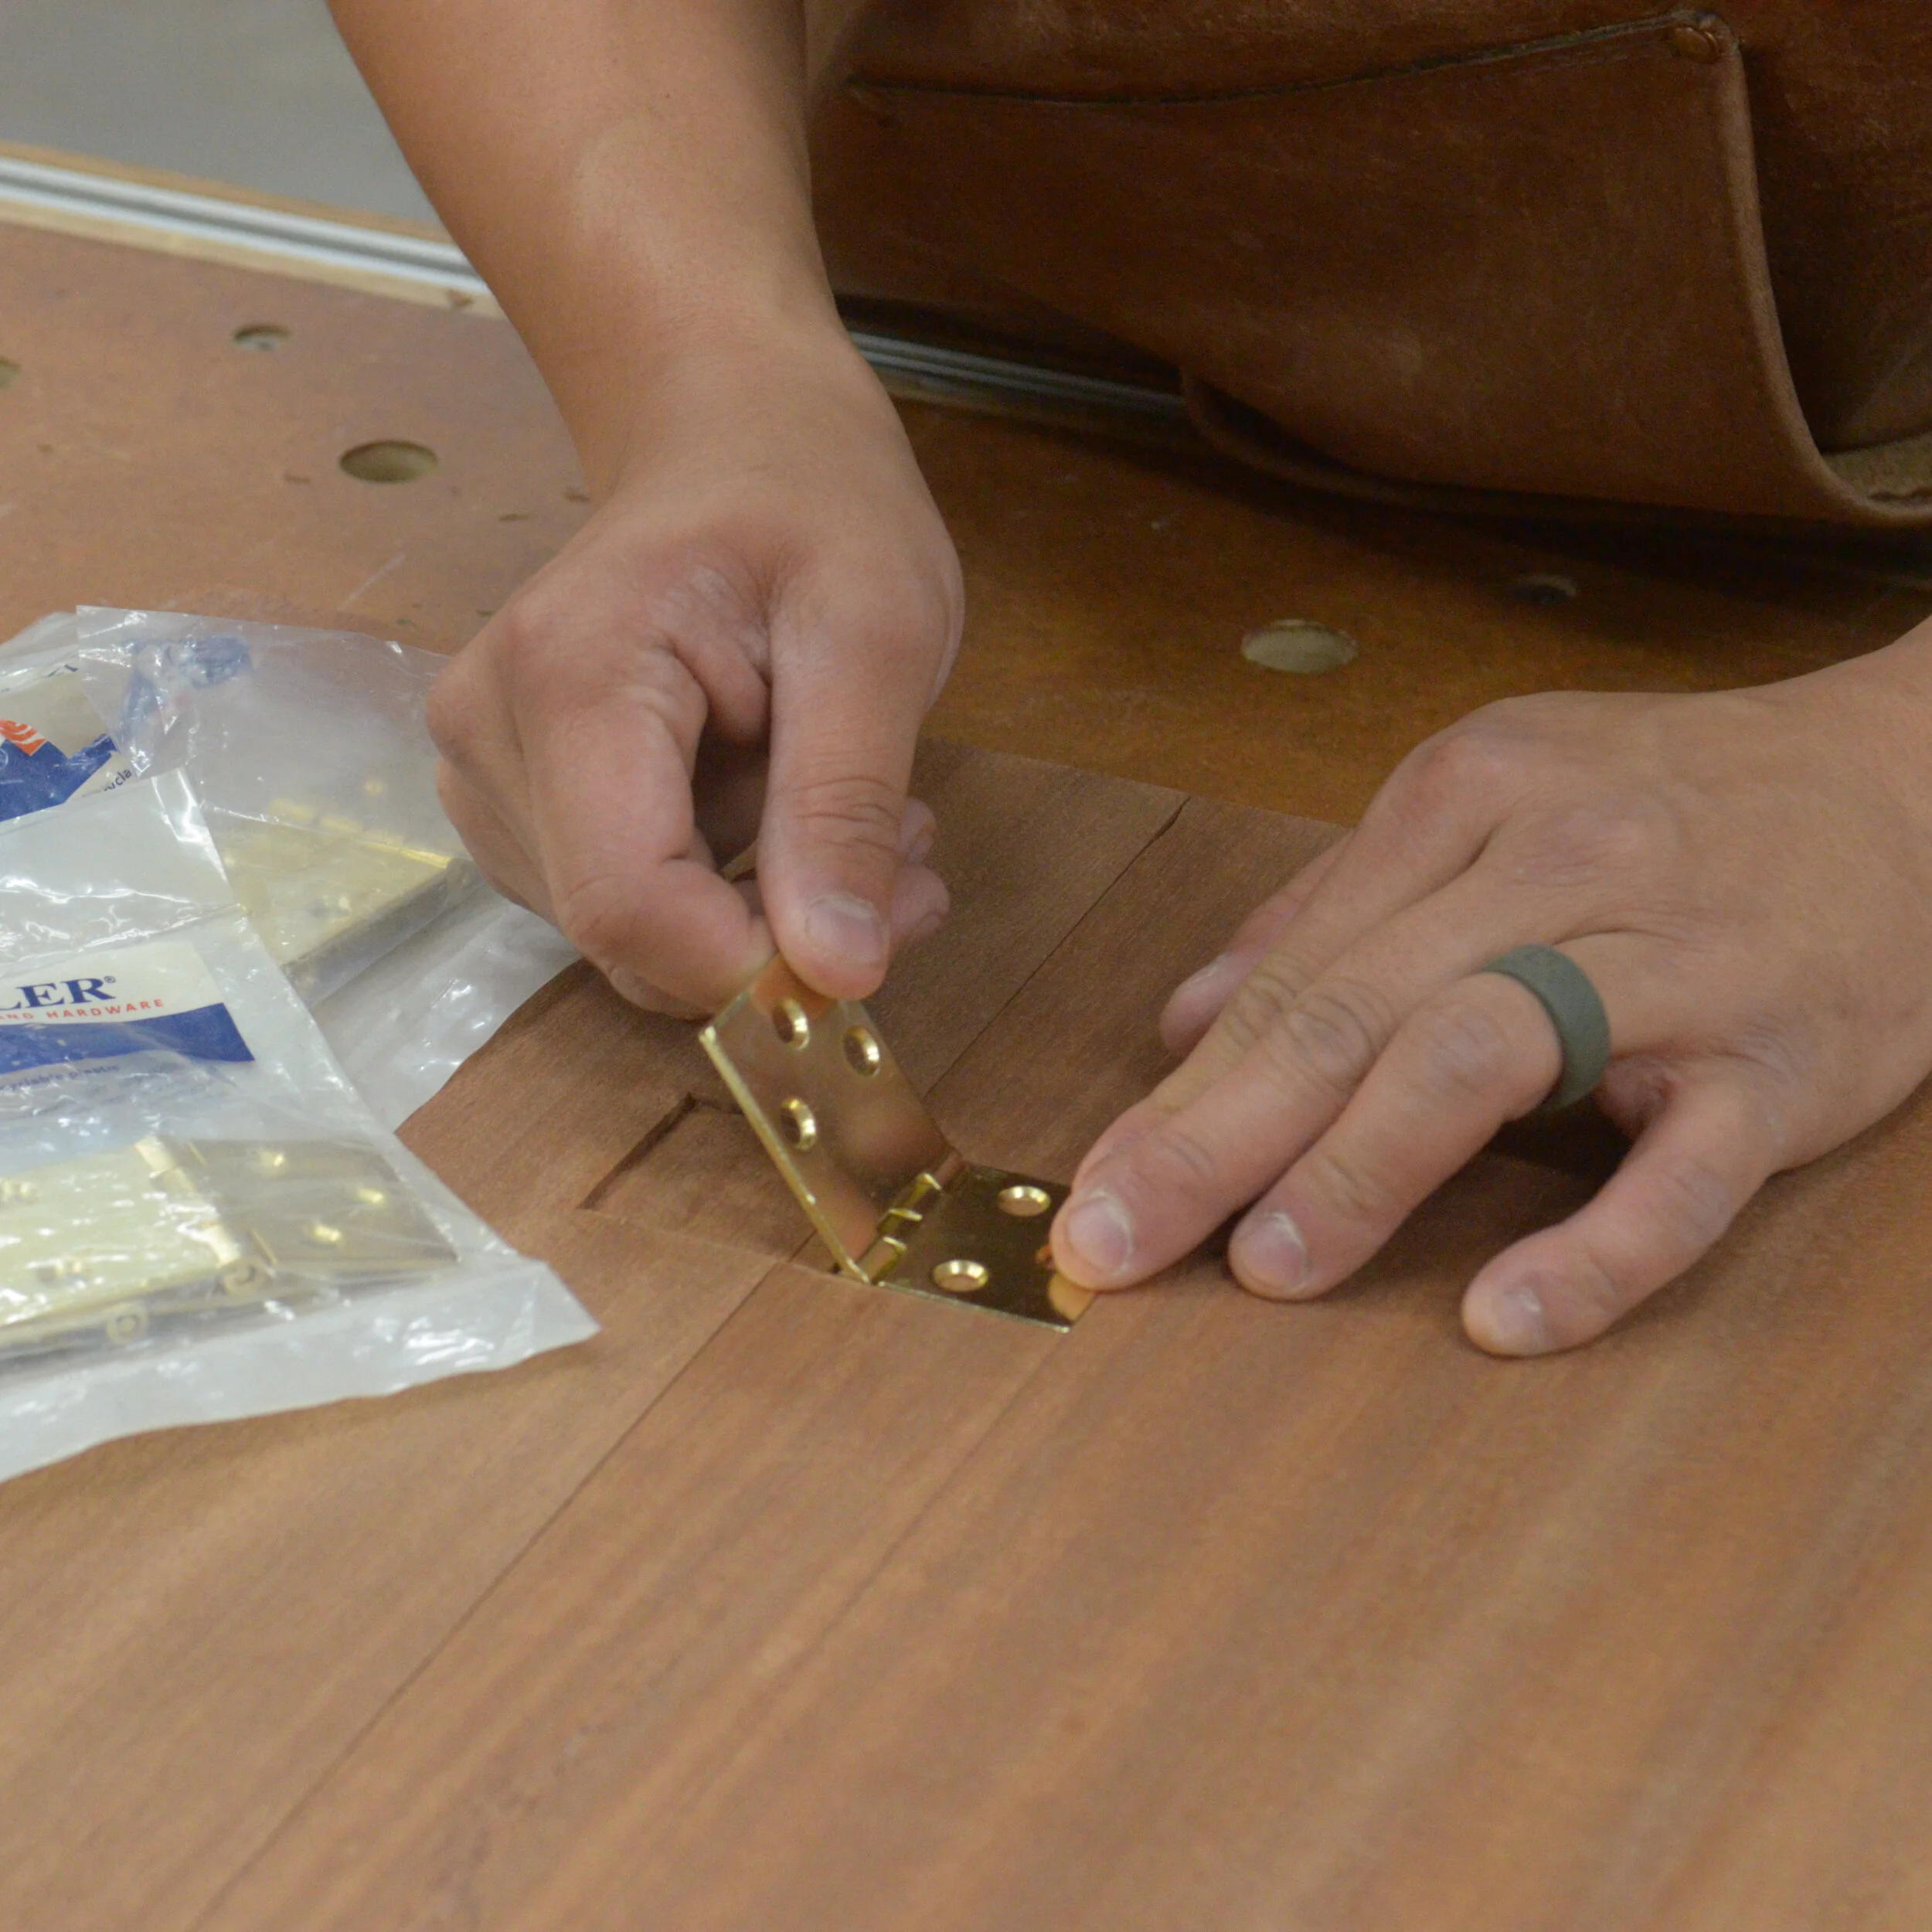
The mortises for drop leaf hinges requires a single template and spacer for the leaves and barrel of the hinge.
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
Drop leaf hinges are different from butt hinges in that the leaves are two different lengths. The shorter leaf attaches to the table top center, whereas the longer leaf attaches to the drop leaf. This configuration allows for the rule joints to rotate past one another. I’m using the Rockler Drop Leaf Hinges for Shaped Edges. Rockler has a downloadable PDF that has some valuable information about the hinges that I used to produce the template that I needed. Installing the hinges is a two step process. I first need to mortise for the hinge leaves and then mortise for the hinge knuckle. This can all be done with a single template and a spacer.
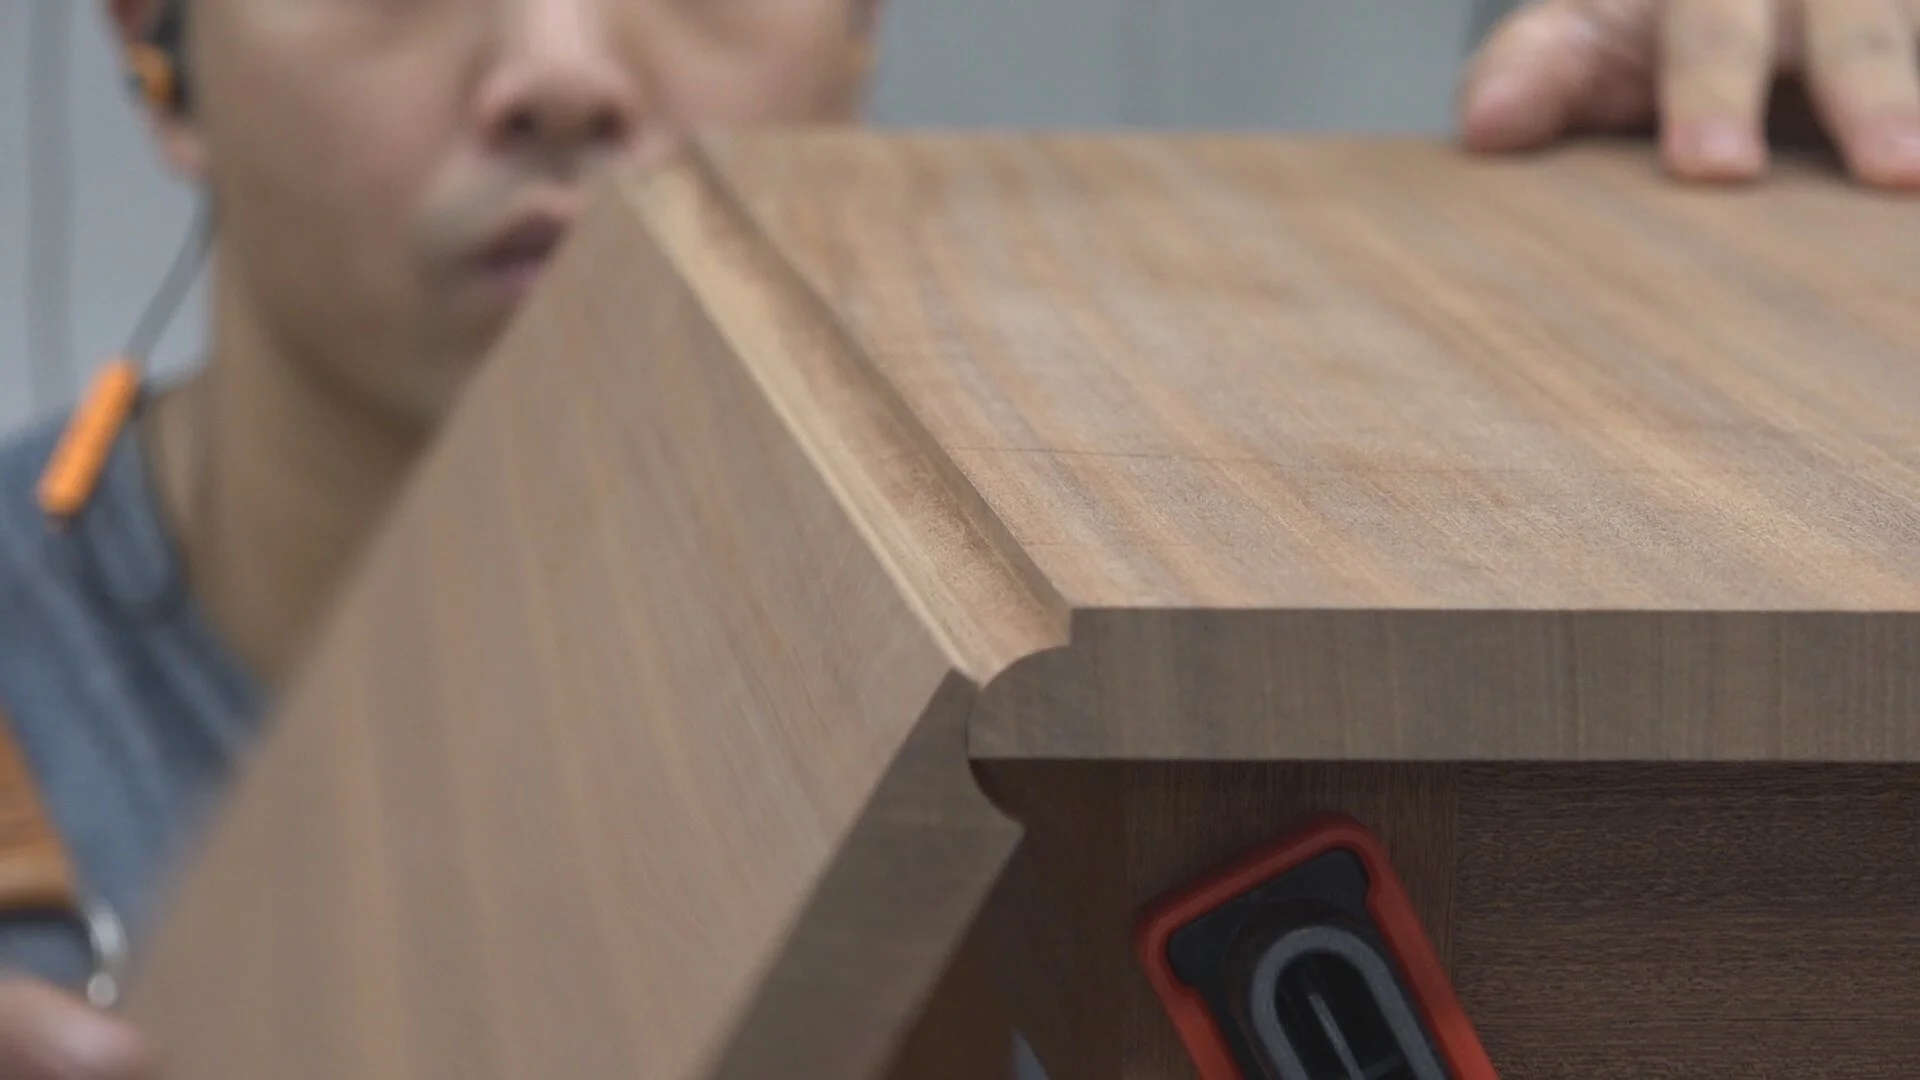
The Rockler Drop Leaf Hinges for Shaped Edges allows for the rule joints to rotate past one another.
The template is quite simple. It is nothing more than a piece of plywood with a pocket cut out to match the exact size of the hinge. This is done by ripping a piece of plywood to the exact of the the hinge. I then sandwich the hinge on all four sides with plywood to create the pocket for the template. I use CA glue to attach these plywood pieces to each other. I also use a thin strip of plywood along the edges of the template for reinforcement.
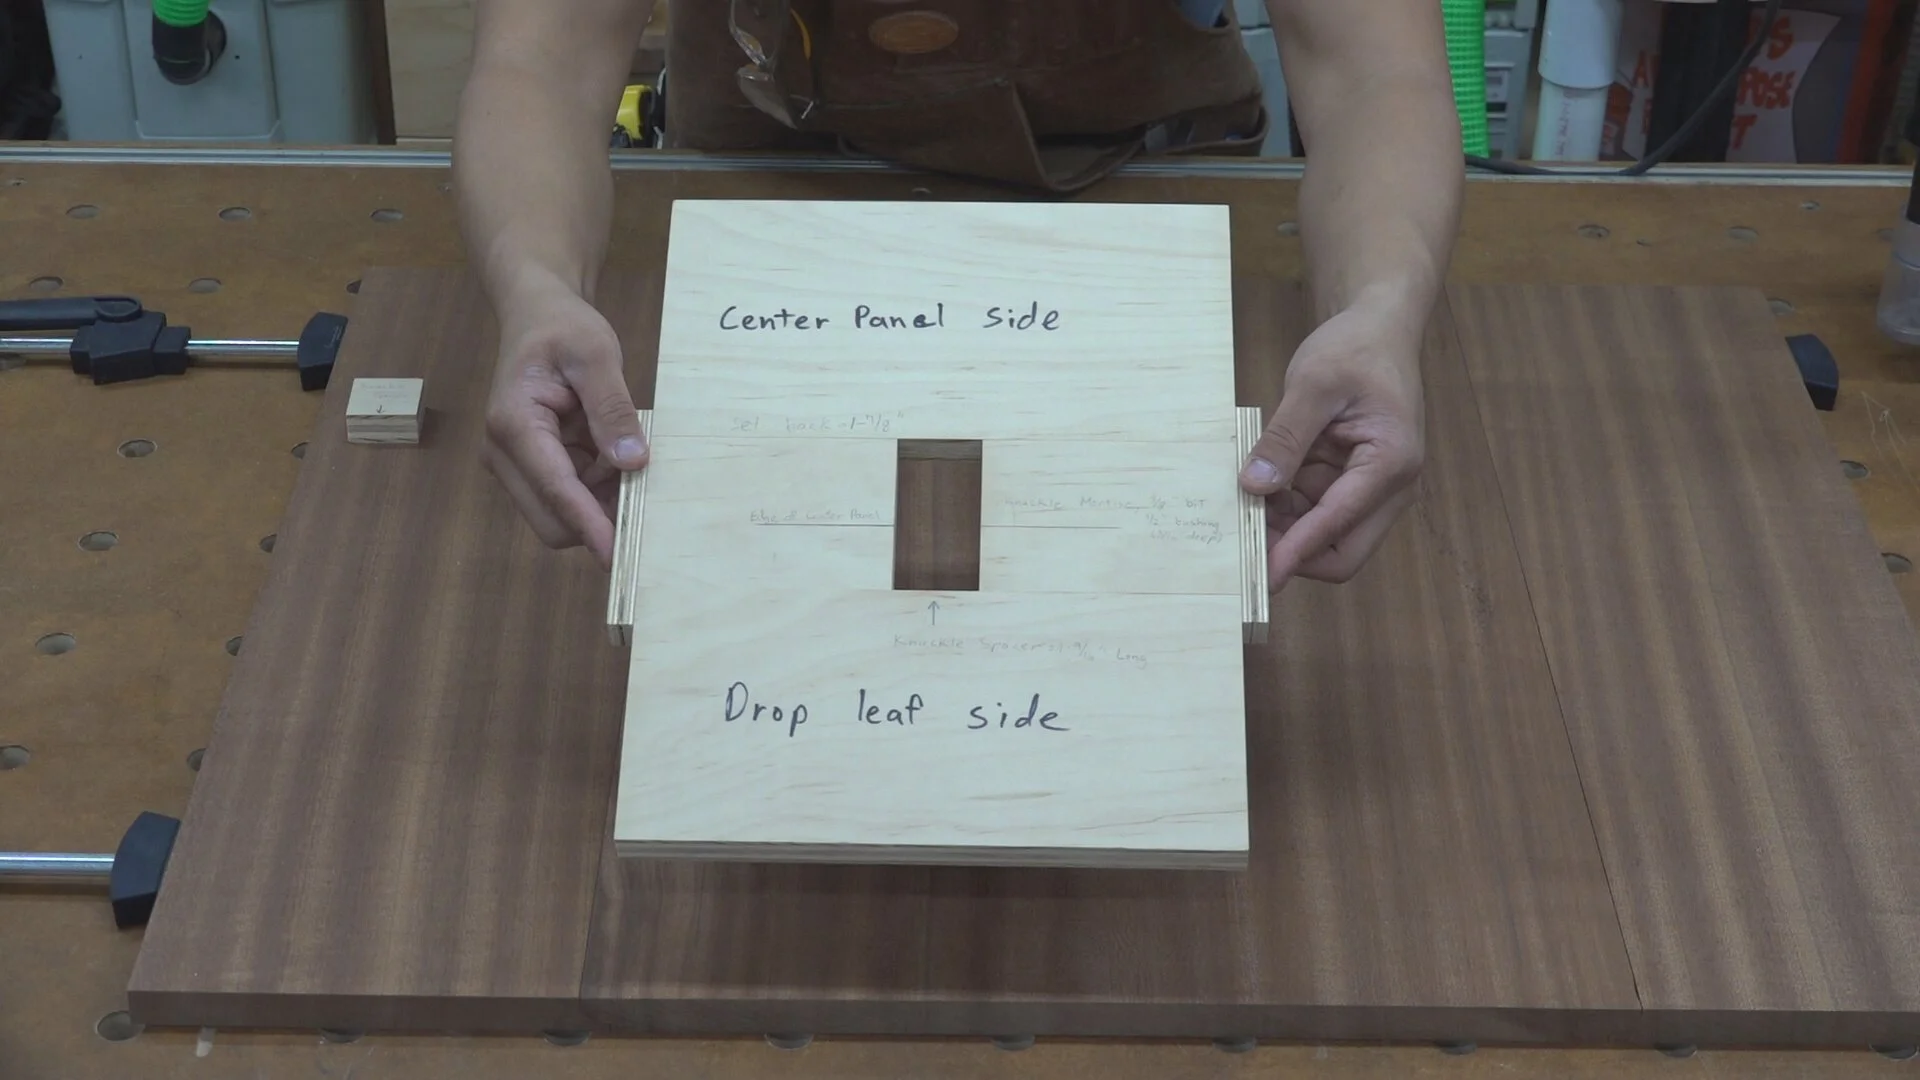
The template is nothing more than pieces of plywood glued together to create a pocket to match the exact size of the hinge.
The tricky part is locating where these hinge mortises need to be located relative to the center panel and drop leaf. Rockler’s spec sheet suggests that back edge of the hinge mortise on the center panel needs to be 1-7/8” from the ruled edge of the center panel. I mark that setback as well as the line for the ruled edge. I write out the orientation the template needs to lay on the table top so that I don’t make any mistakes. I also mark the setback on the center panel to make sure I properly align the template. Next, I clamp the center panel and drop leaves together to prepare for the routing operation.
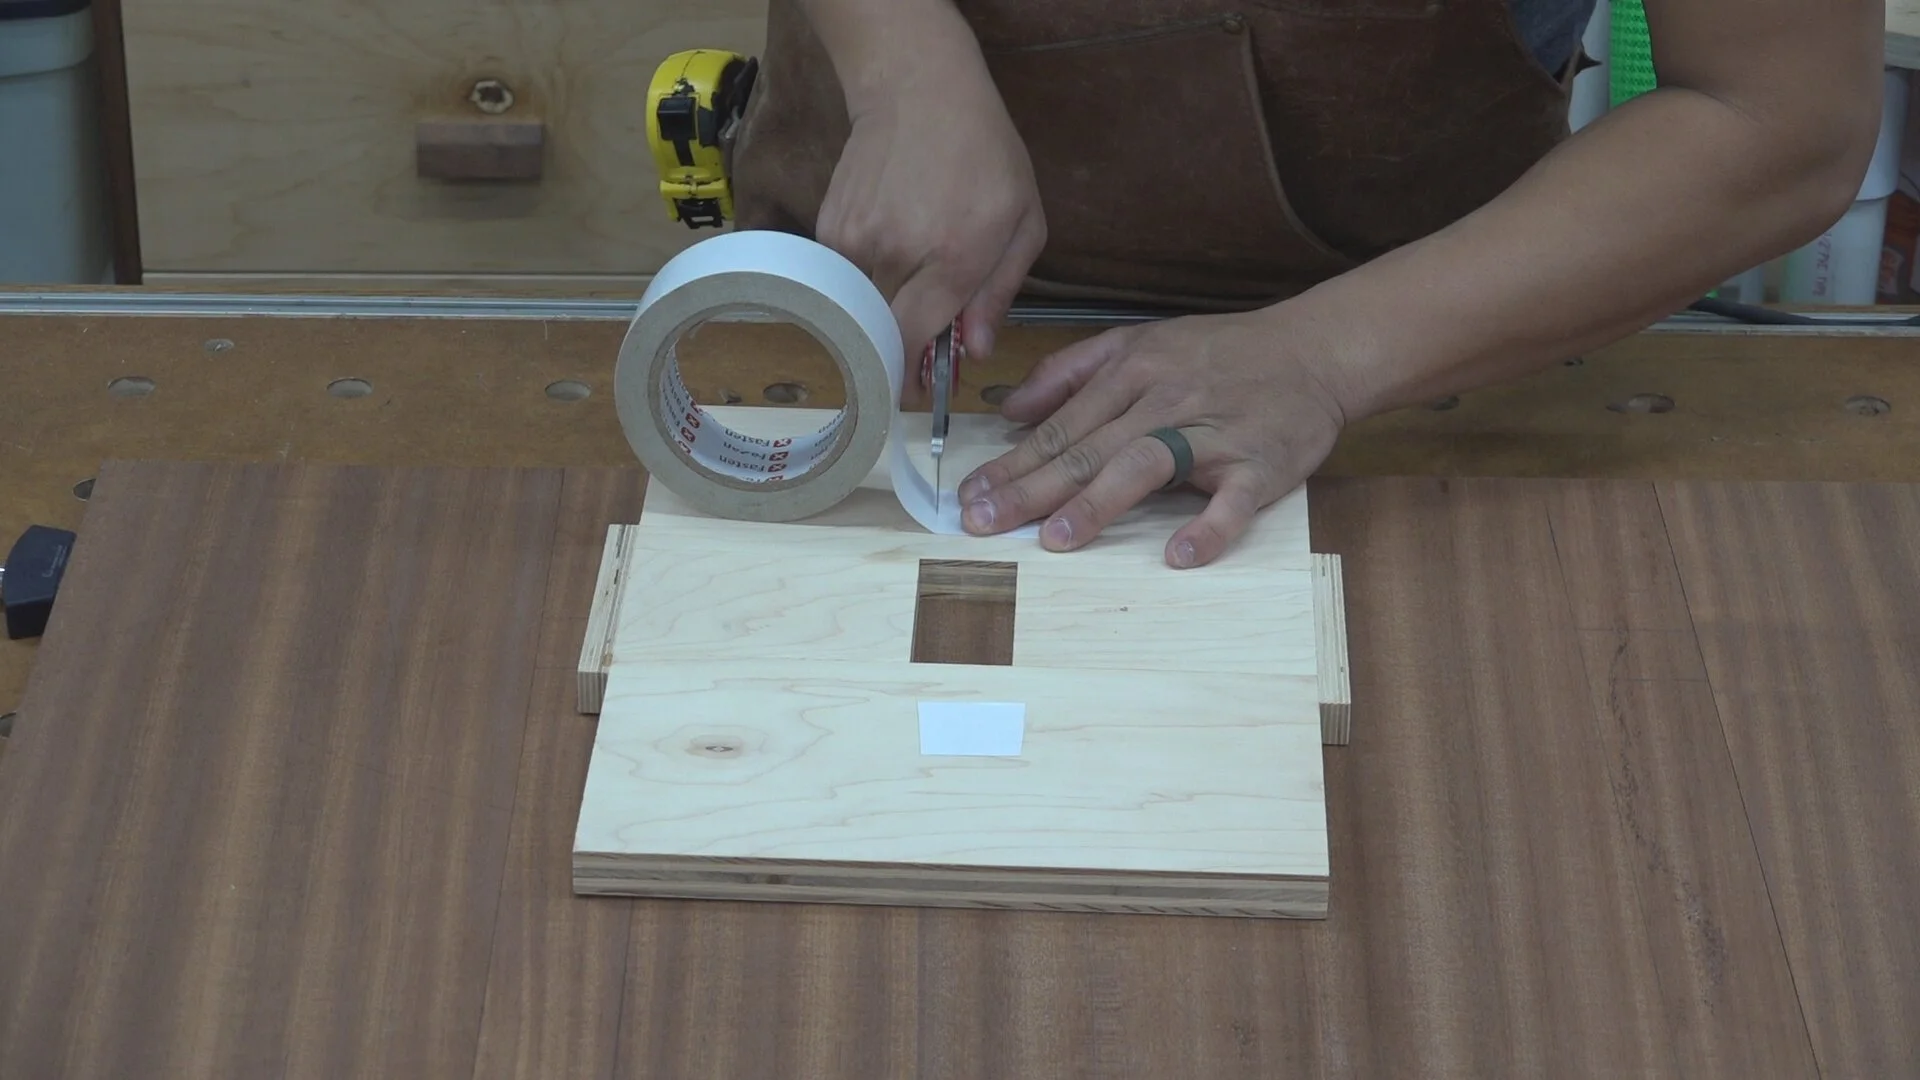
I use double stick take to attach the template to the table top. This offers plenty of temporary holding power.
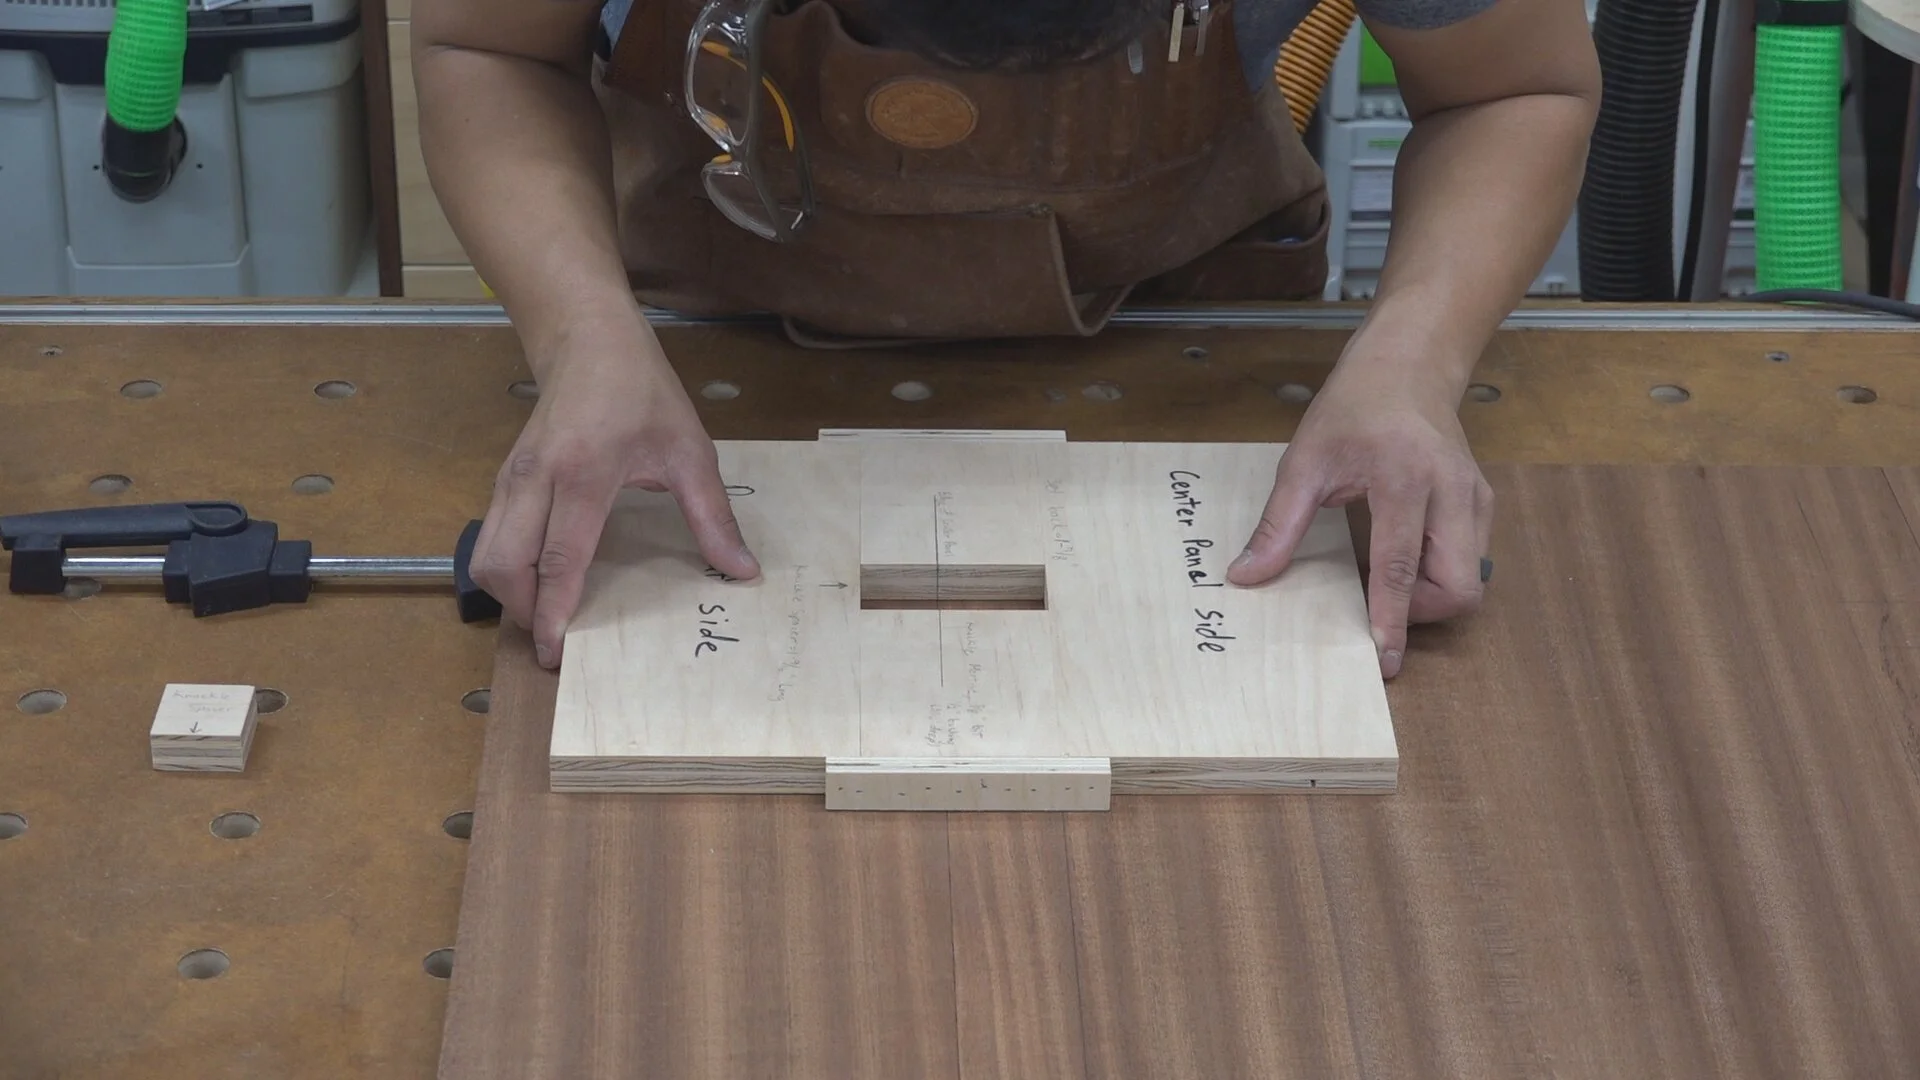
I align the setback edge of the template with the setback line marked on the center panel.
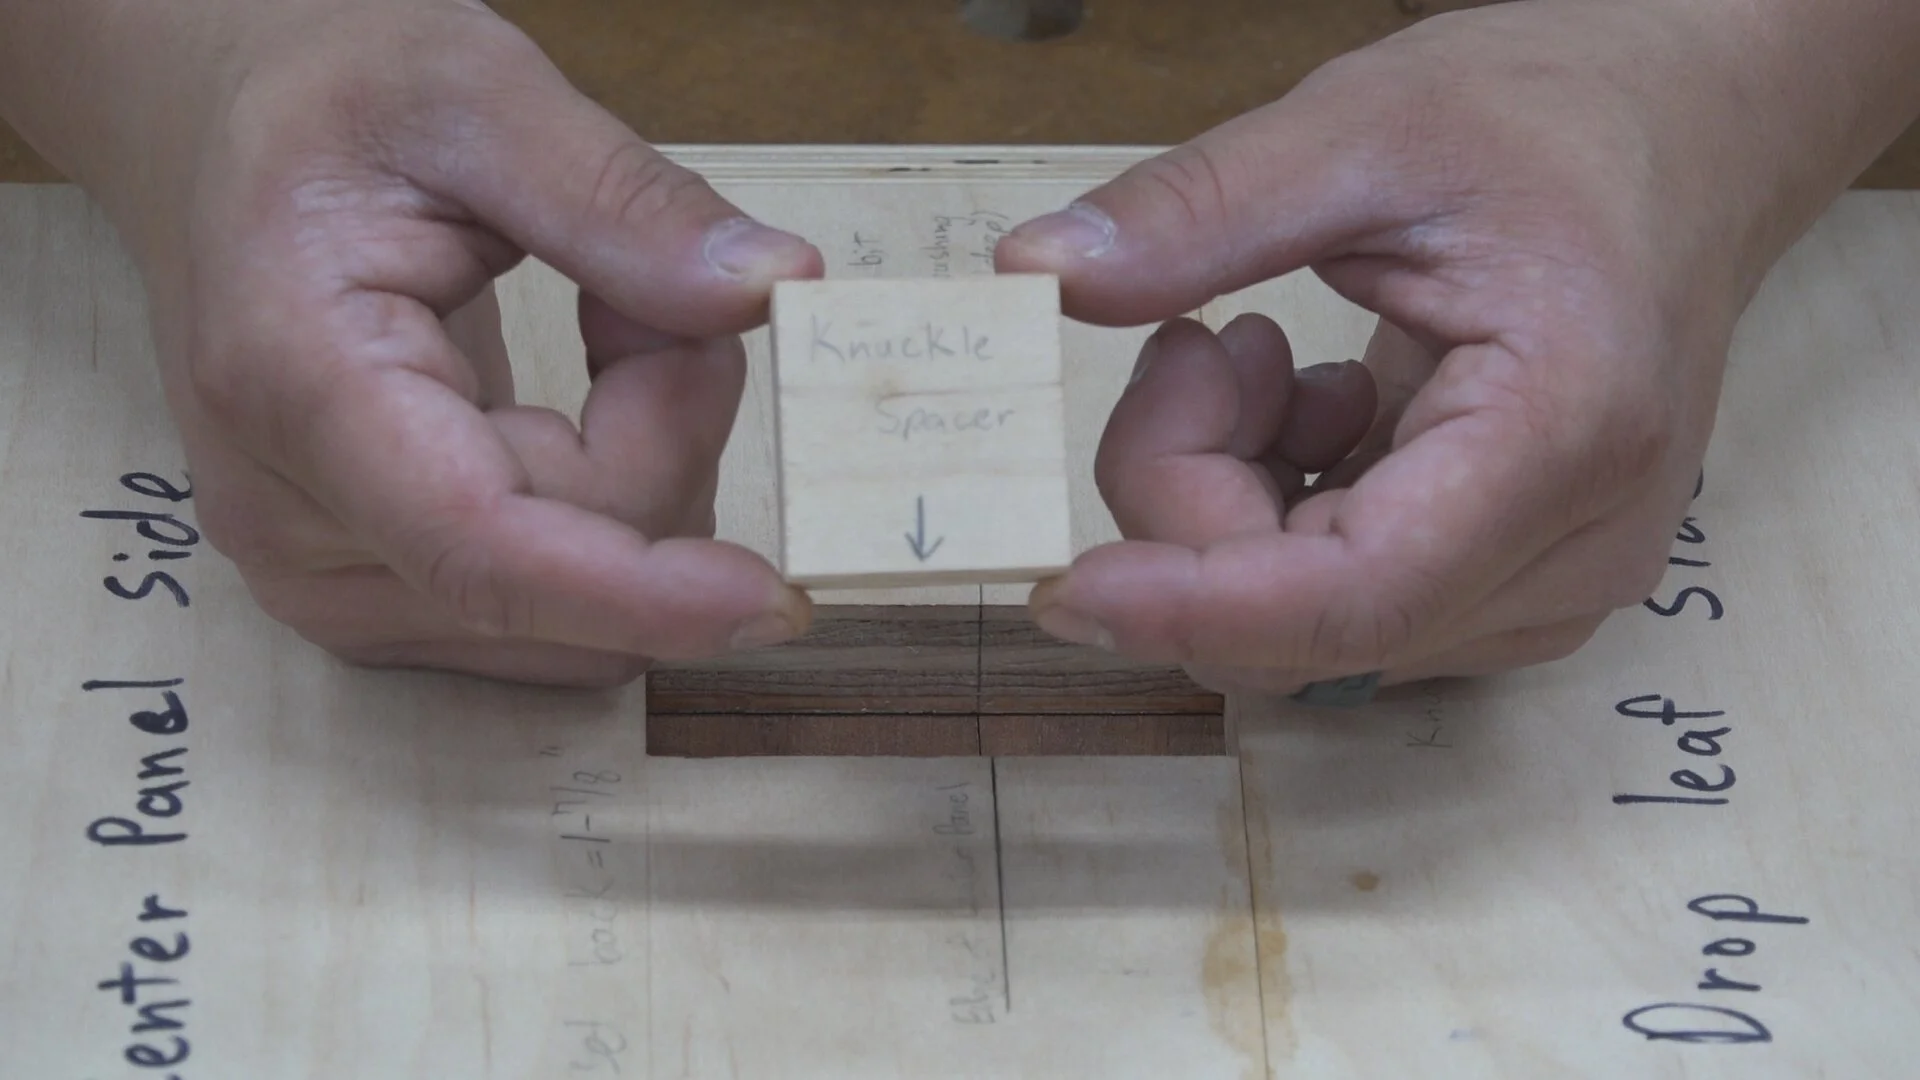
I first need to rout for the knuckle mortise. I use a spacer block that fits into the template to locate the knuckle mortise. The spacer is 1-9/16” long and it goes against the drop leaf side of the hinge template.
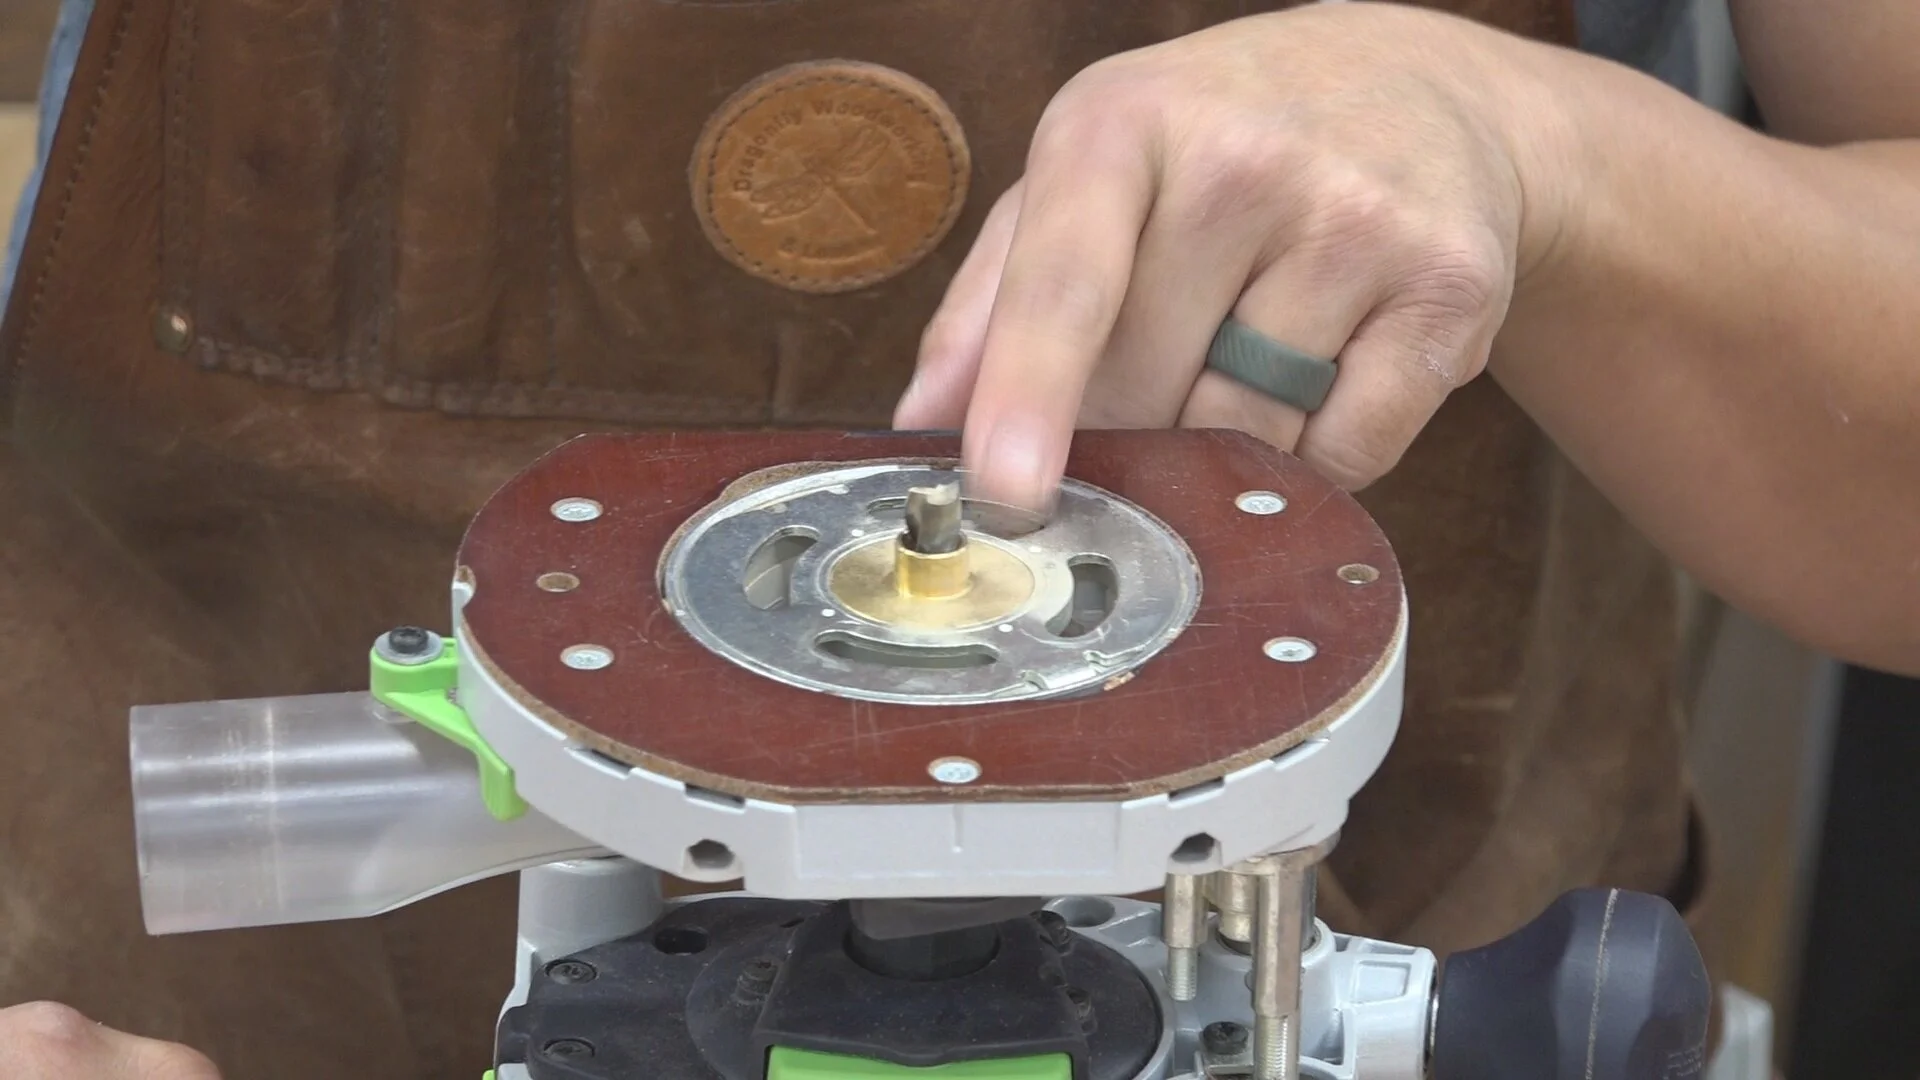
I’m using a 3/8” mortising bit inside of a 1/2” guide bushing to route the knuckle.
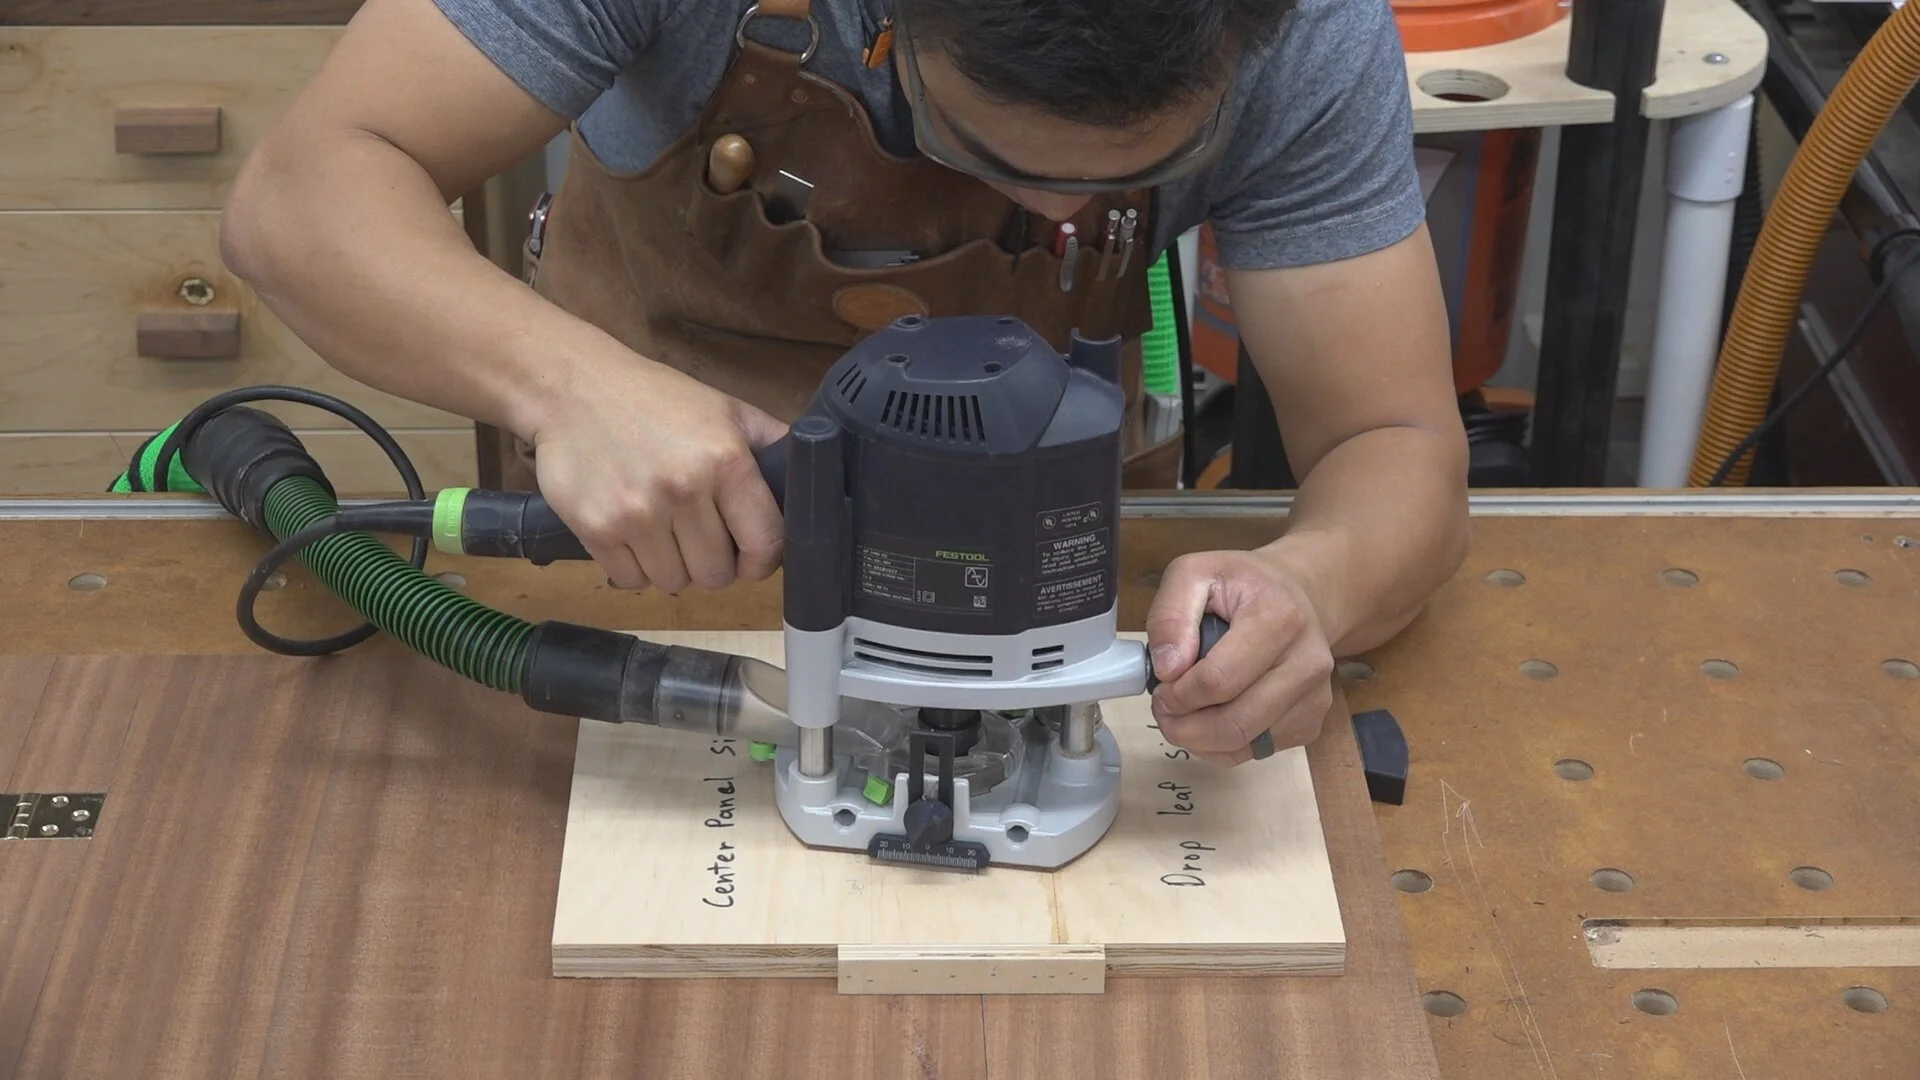
I route the knuckle mortise 3/16” deep making sure to follow the edge of the knuckle spacer.
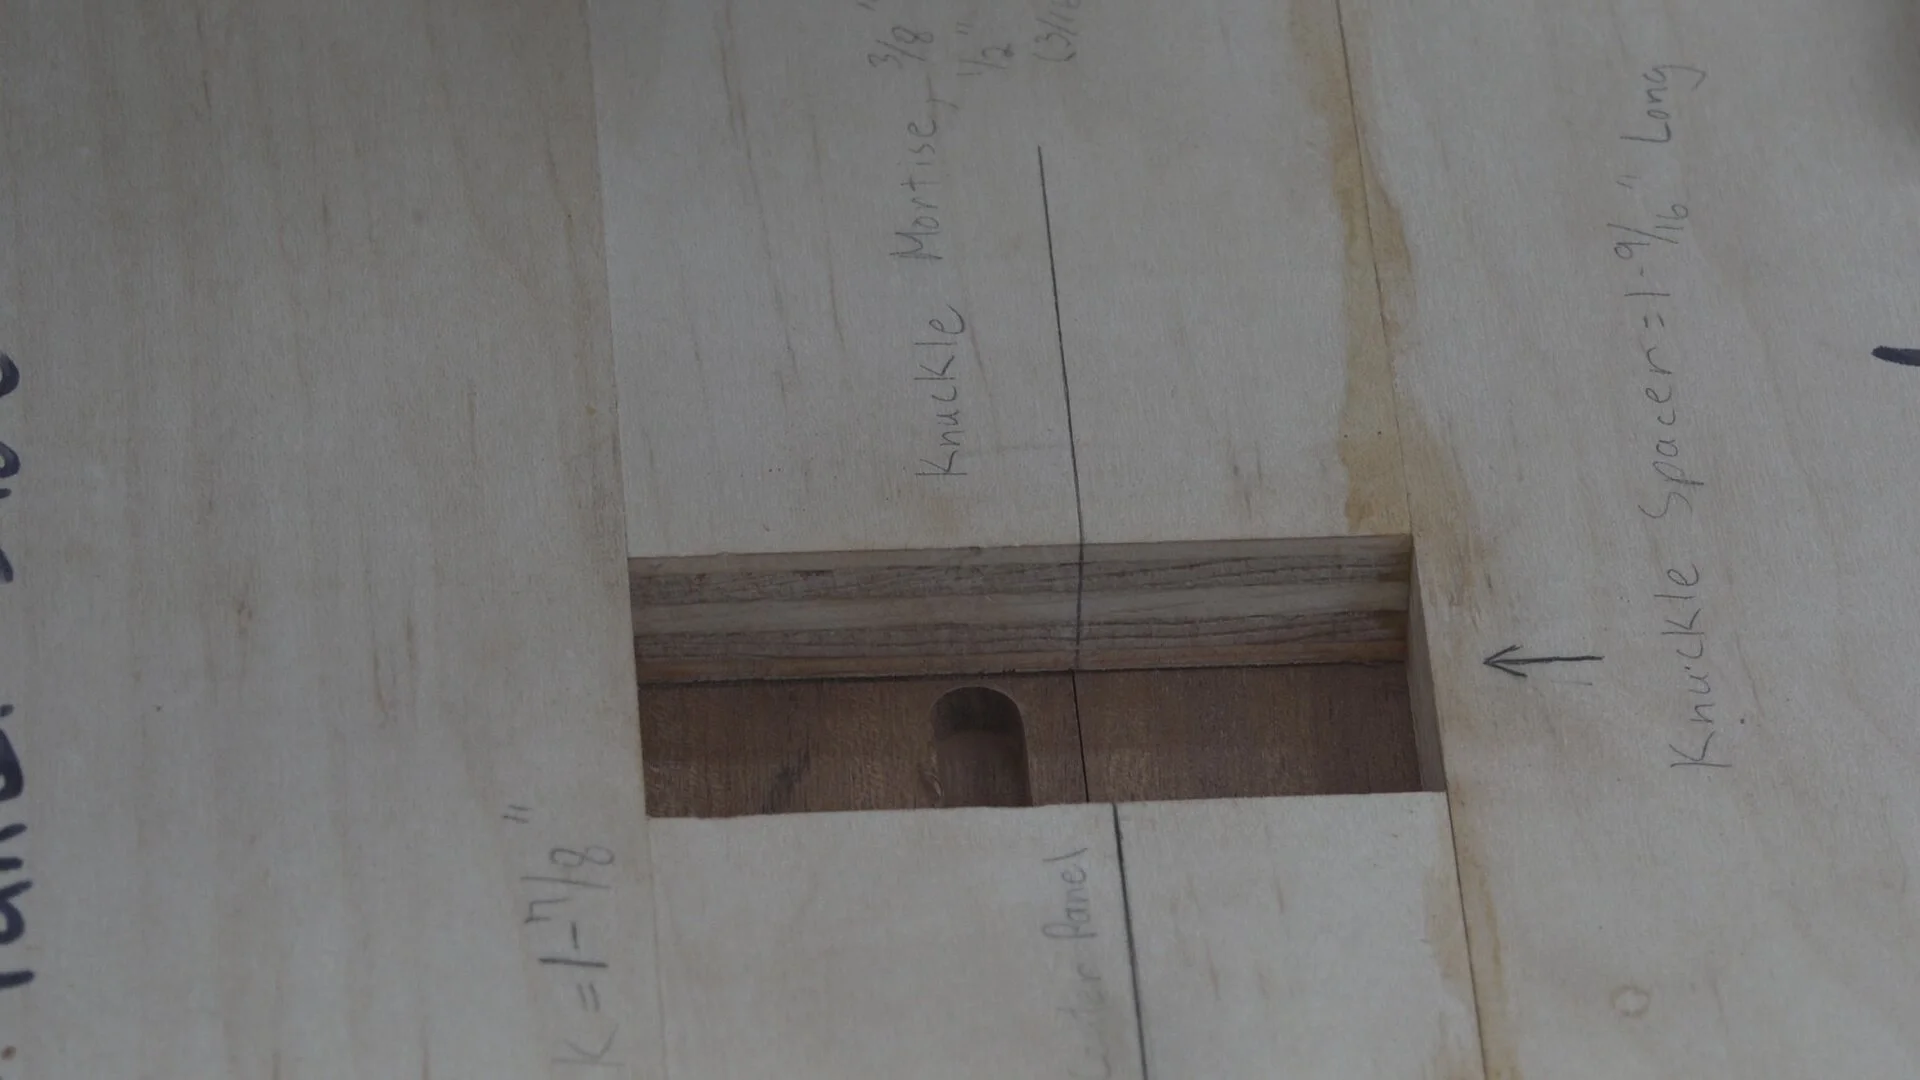
This produces a clean mortise for the knuckle that I’ll square up later with chisels.
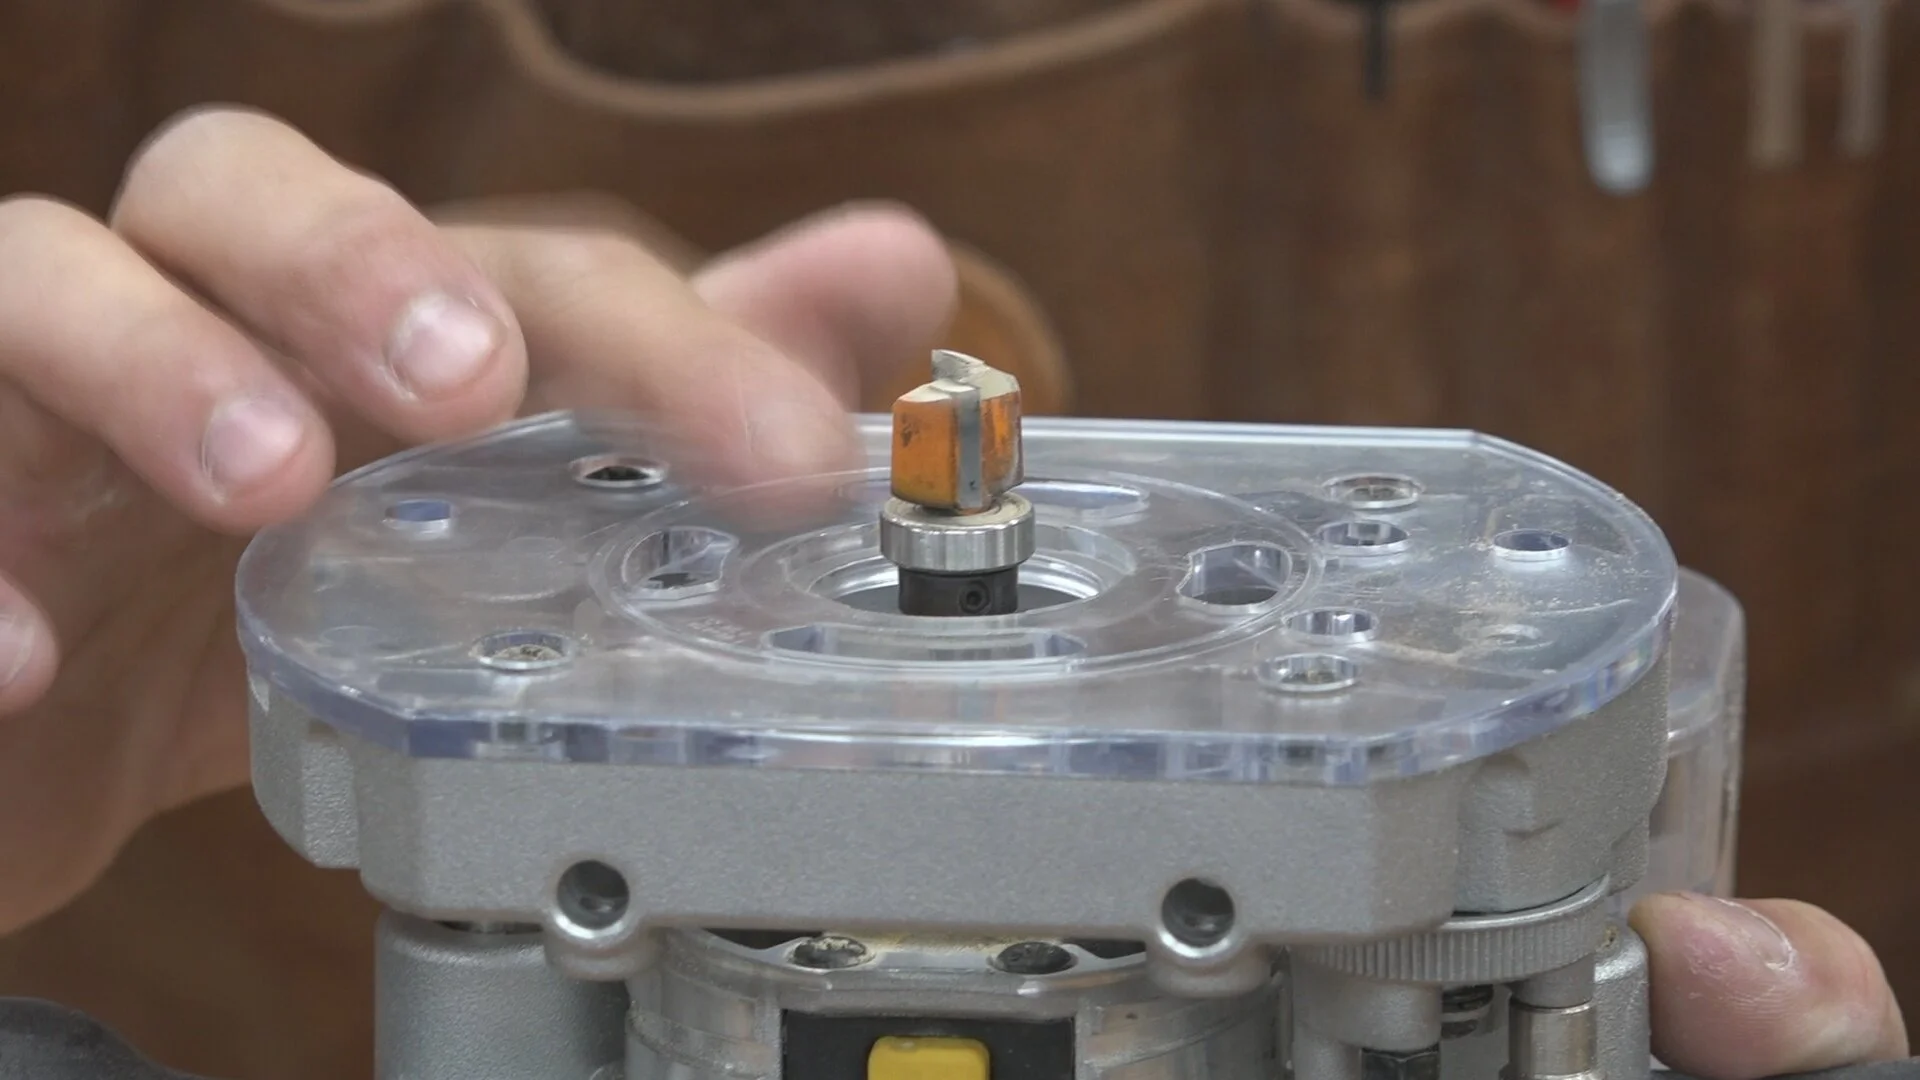
To mortise for the hinge plate leaves, I use a short flush trim bit set to the depth of the template plus the hinge leaf.
I like using the DeWalt 20V Max Compact Router for this operation because it's lightweight and easy to handle for these more refined machining operations.
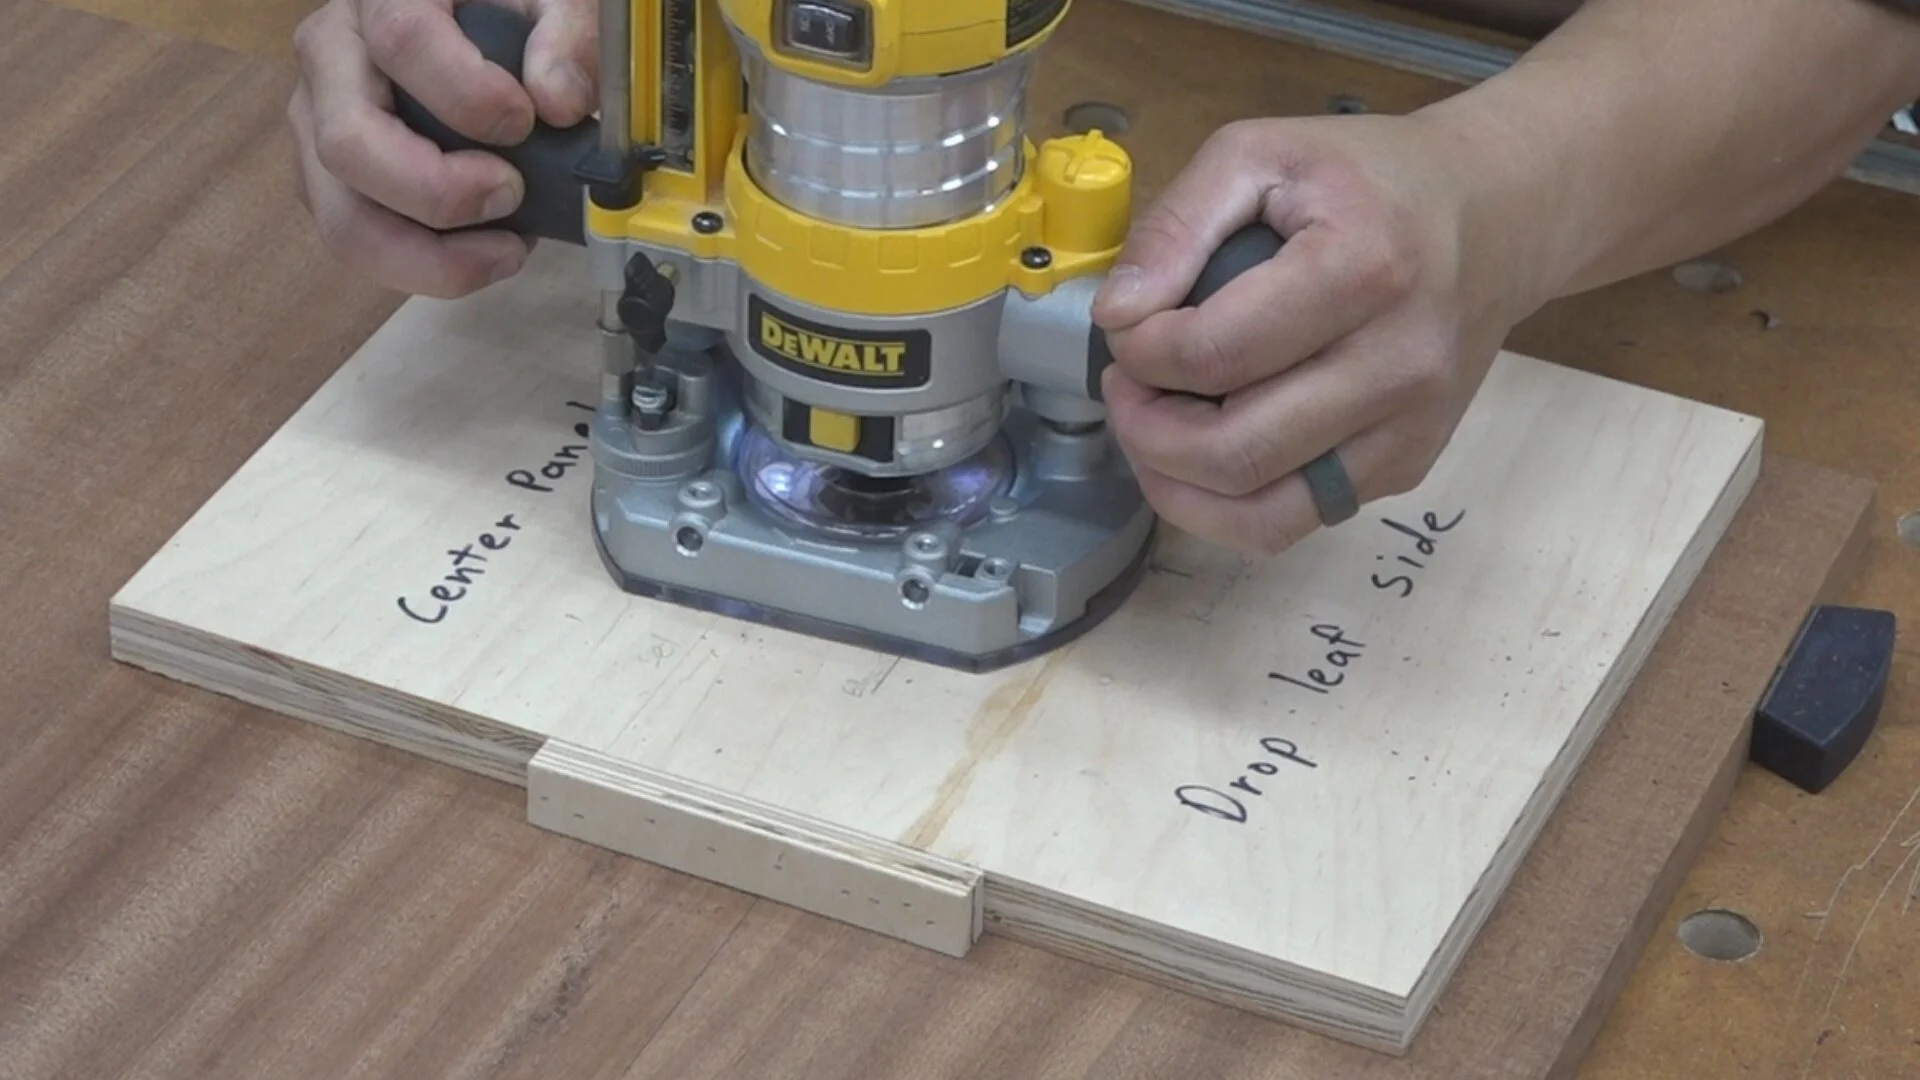
I use a compact router and short flush trim bit to route the hinge mortise leaves.
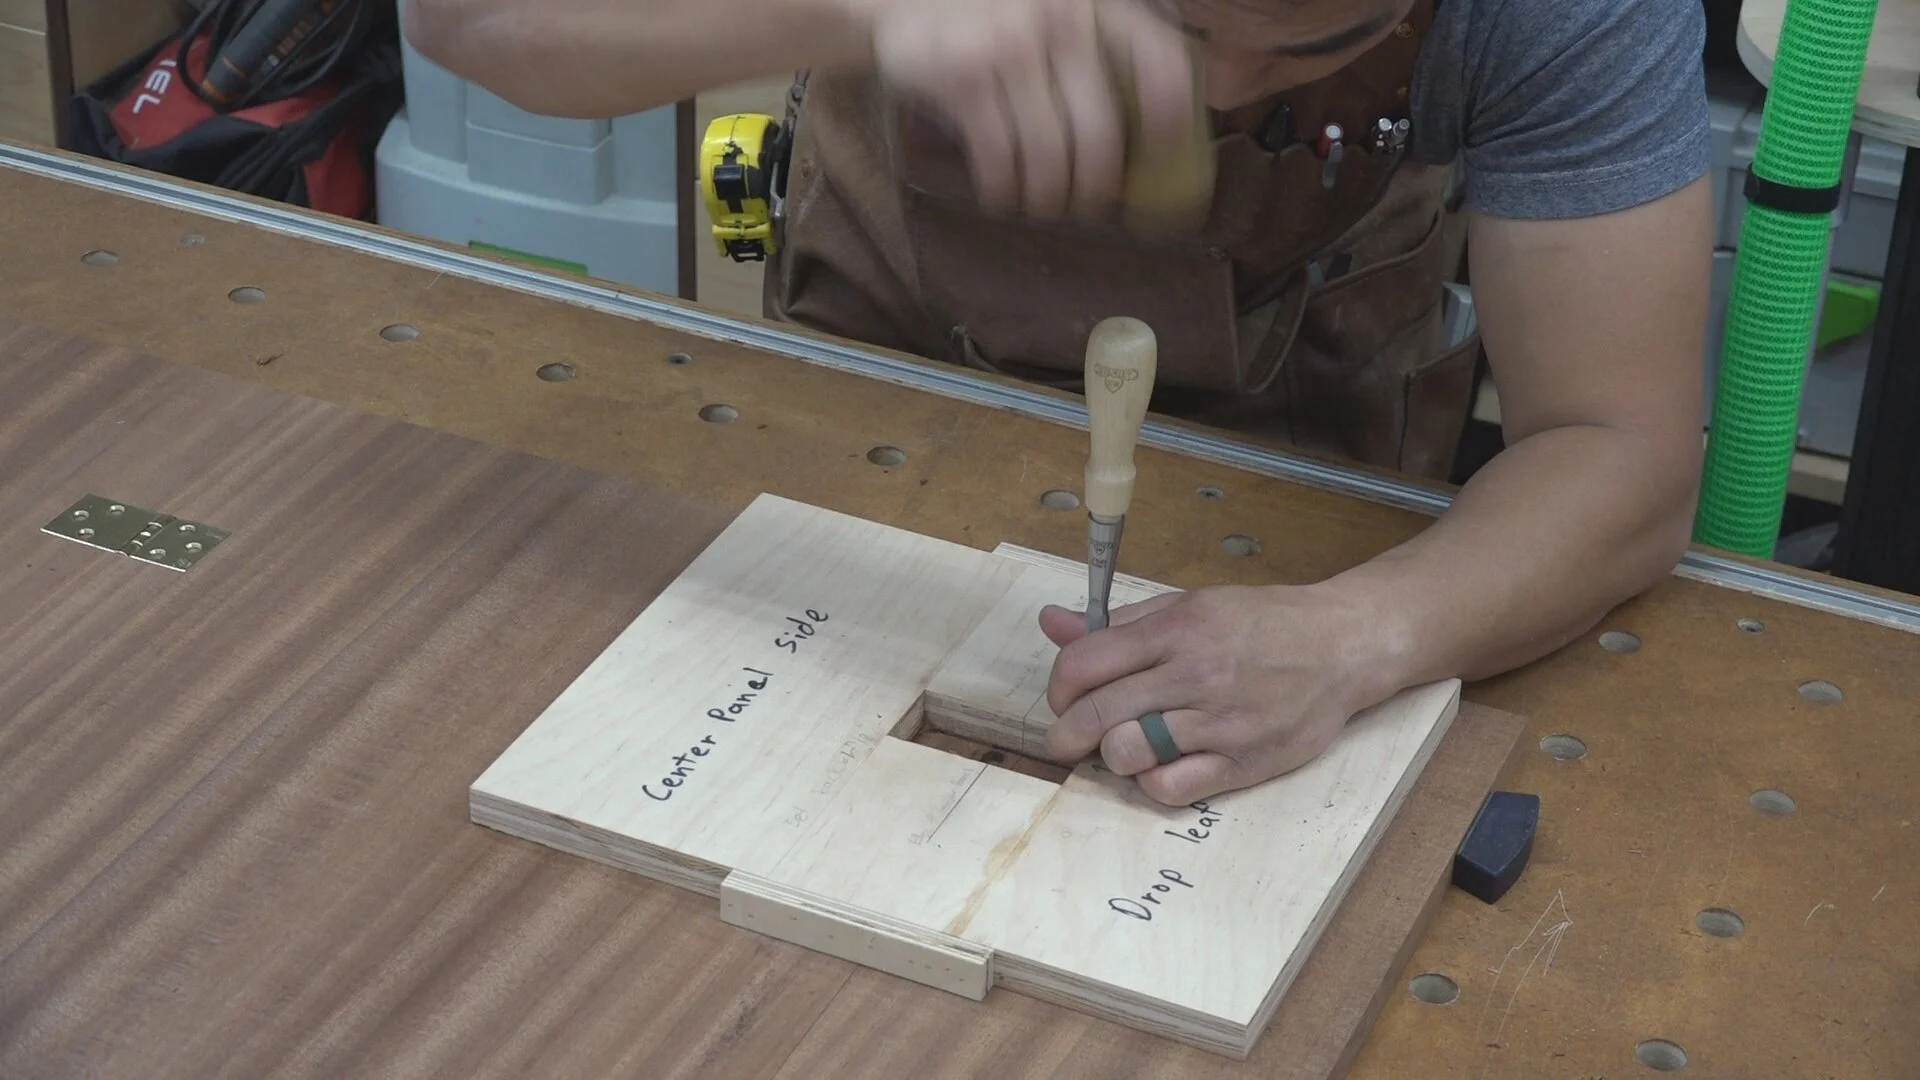
I then use the template as a guide to square up the edges of the hinge mortises with a chisel.
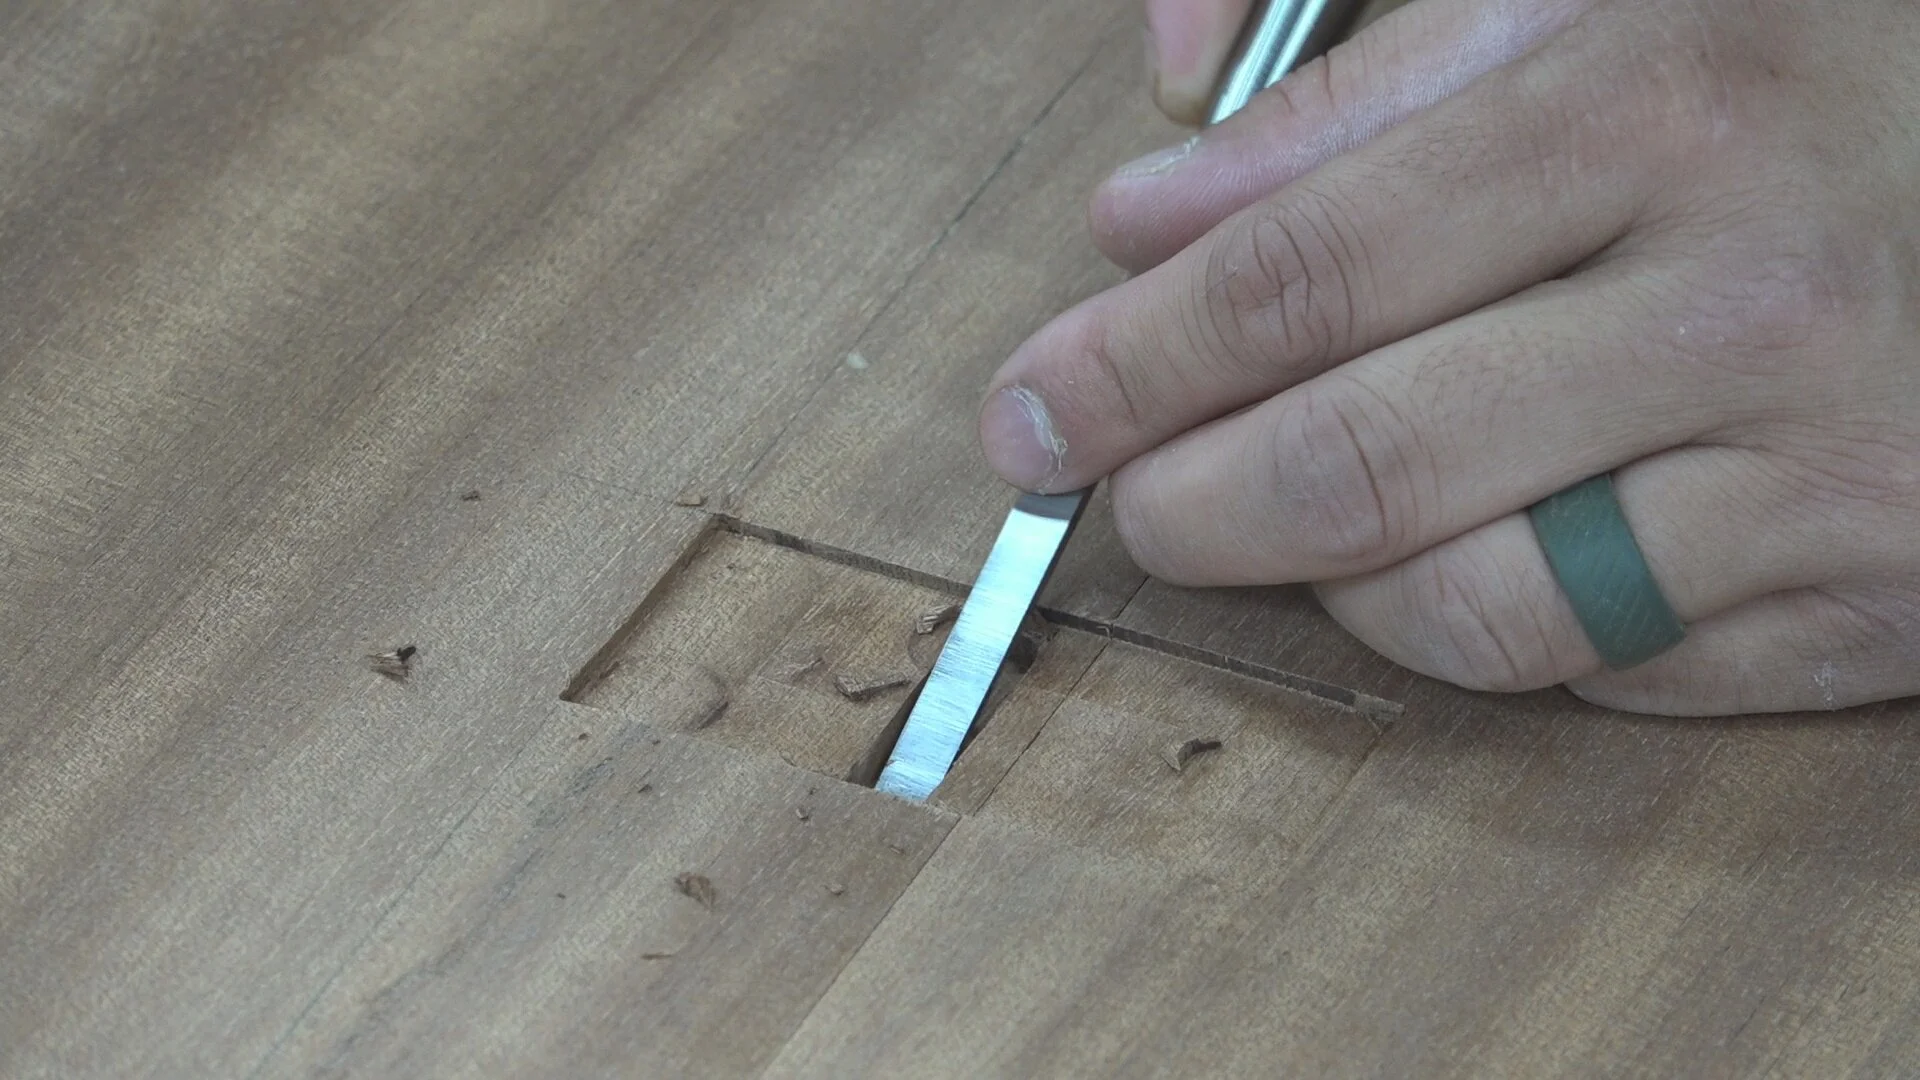
Once I remove the template, I then square up the hinge knuckle mortise with a chisel.
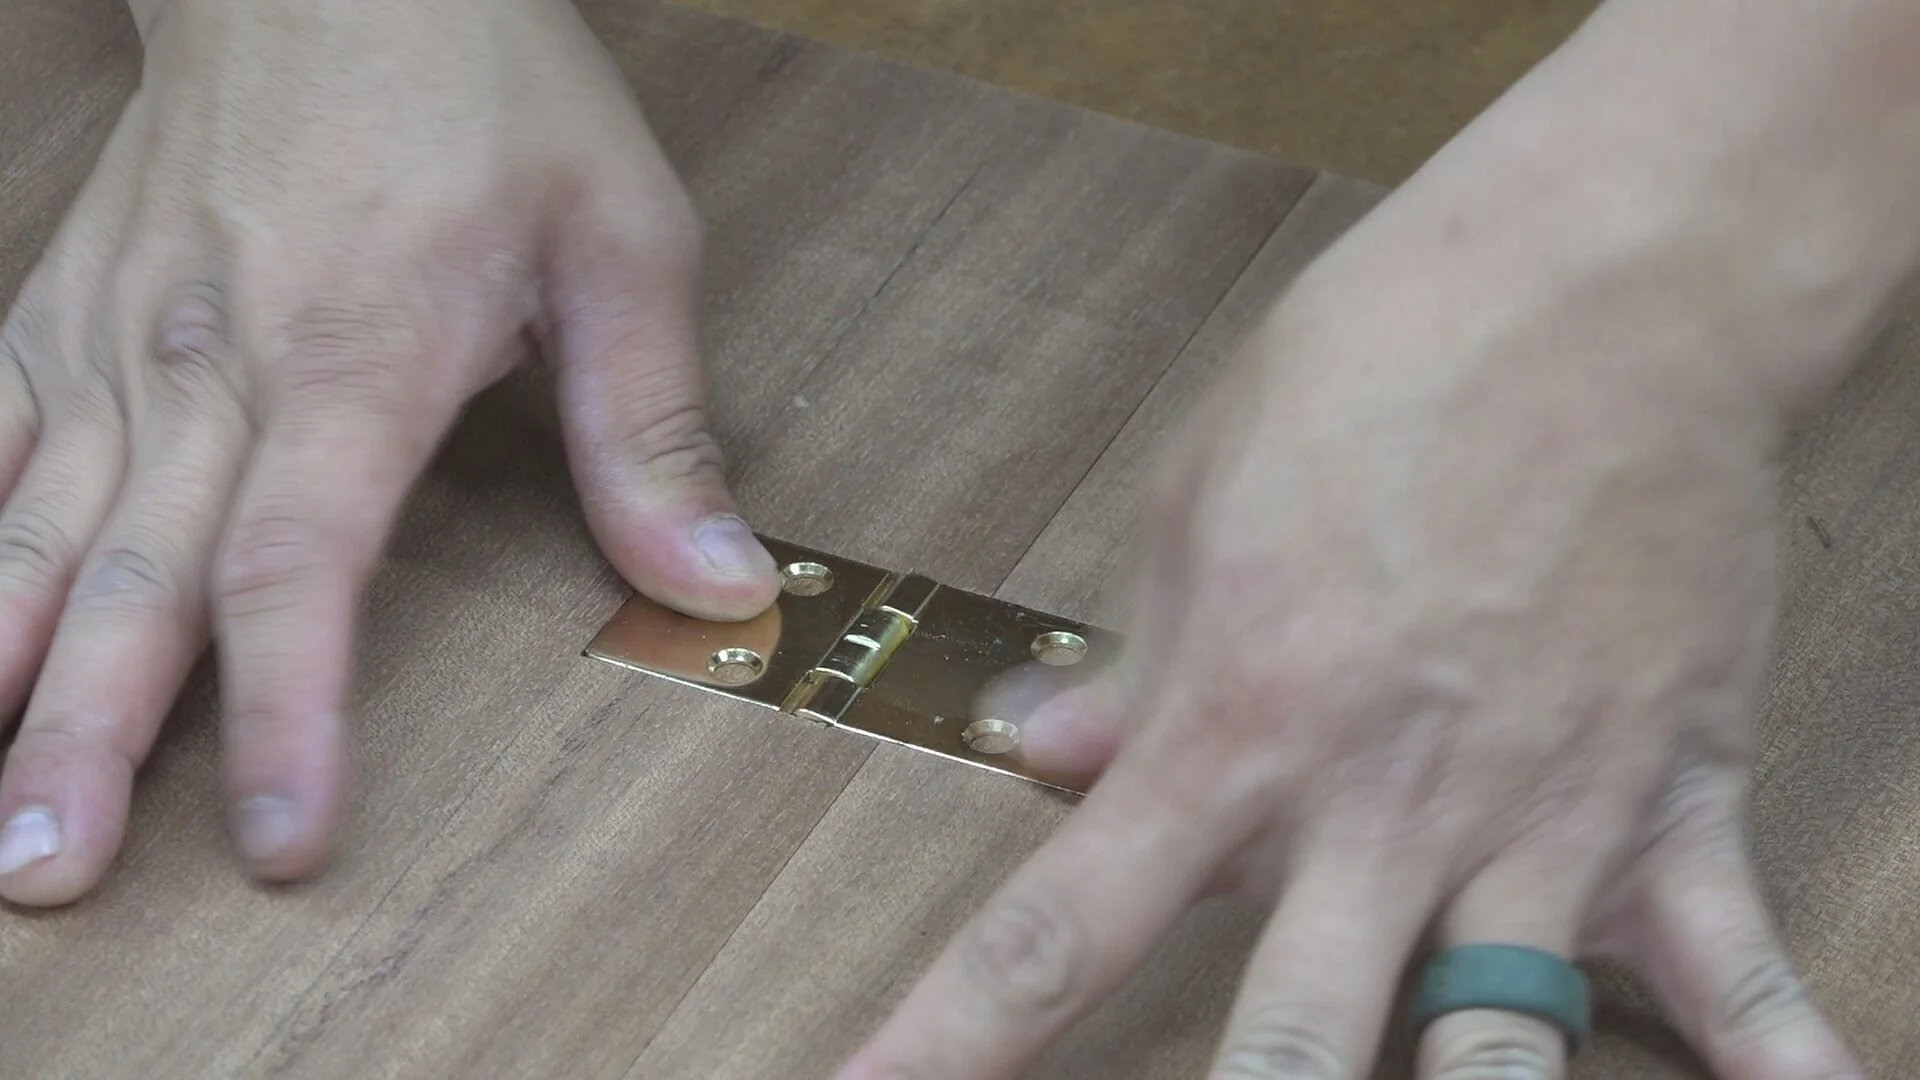
The result is a perfect fitting hinge.
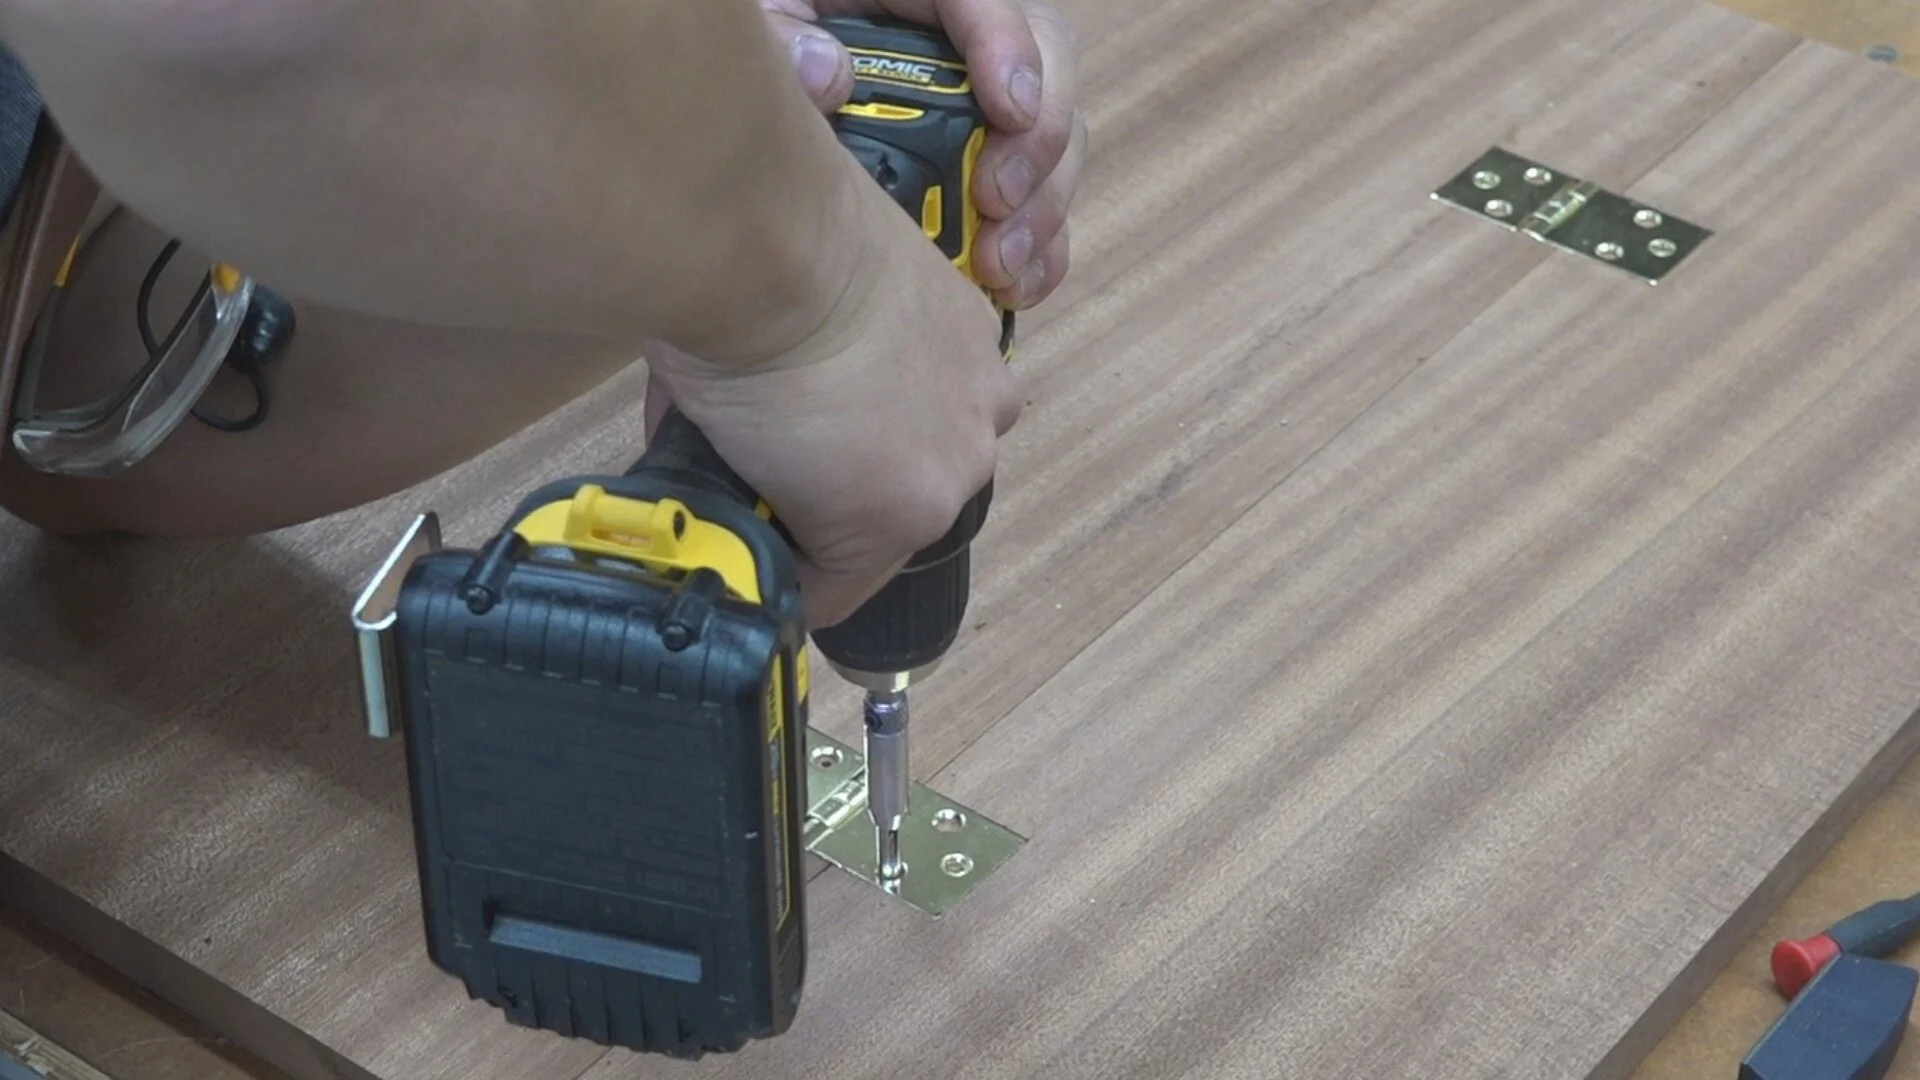
The last thing I need to do is fasten the hinges. I first pre-drill for the screws using a self centering drill bit and the DeWalt ATOMIC 20-Volt MAX Lithium-Ion Cordless Hammer Drill. I then drive the screws using the variable speed function on the DeWalt ATOMIC 20-Volt MAX Lithium-Ion Cordless Impact Driver.
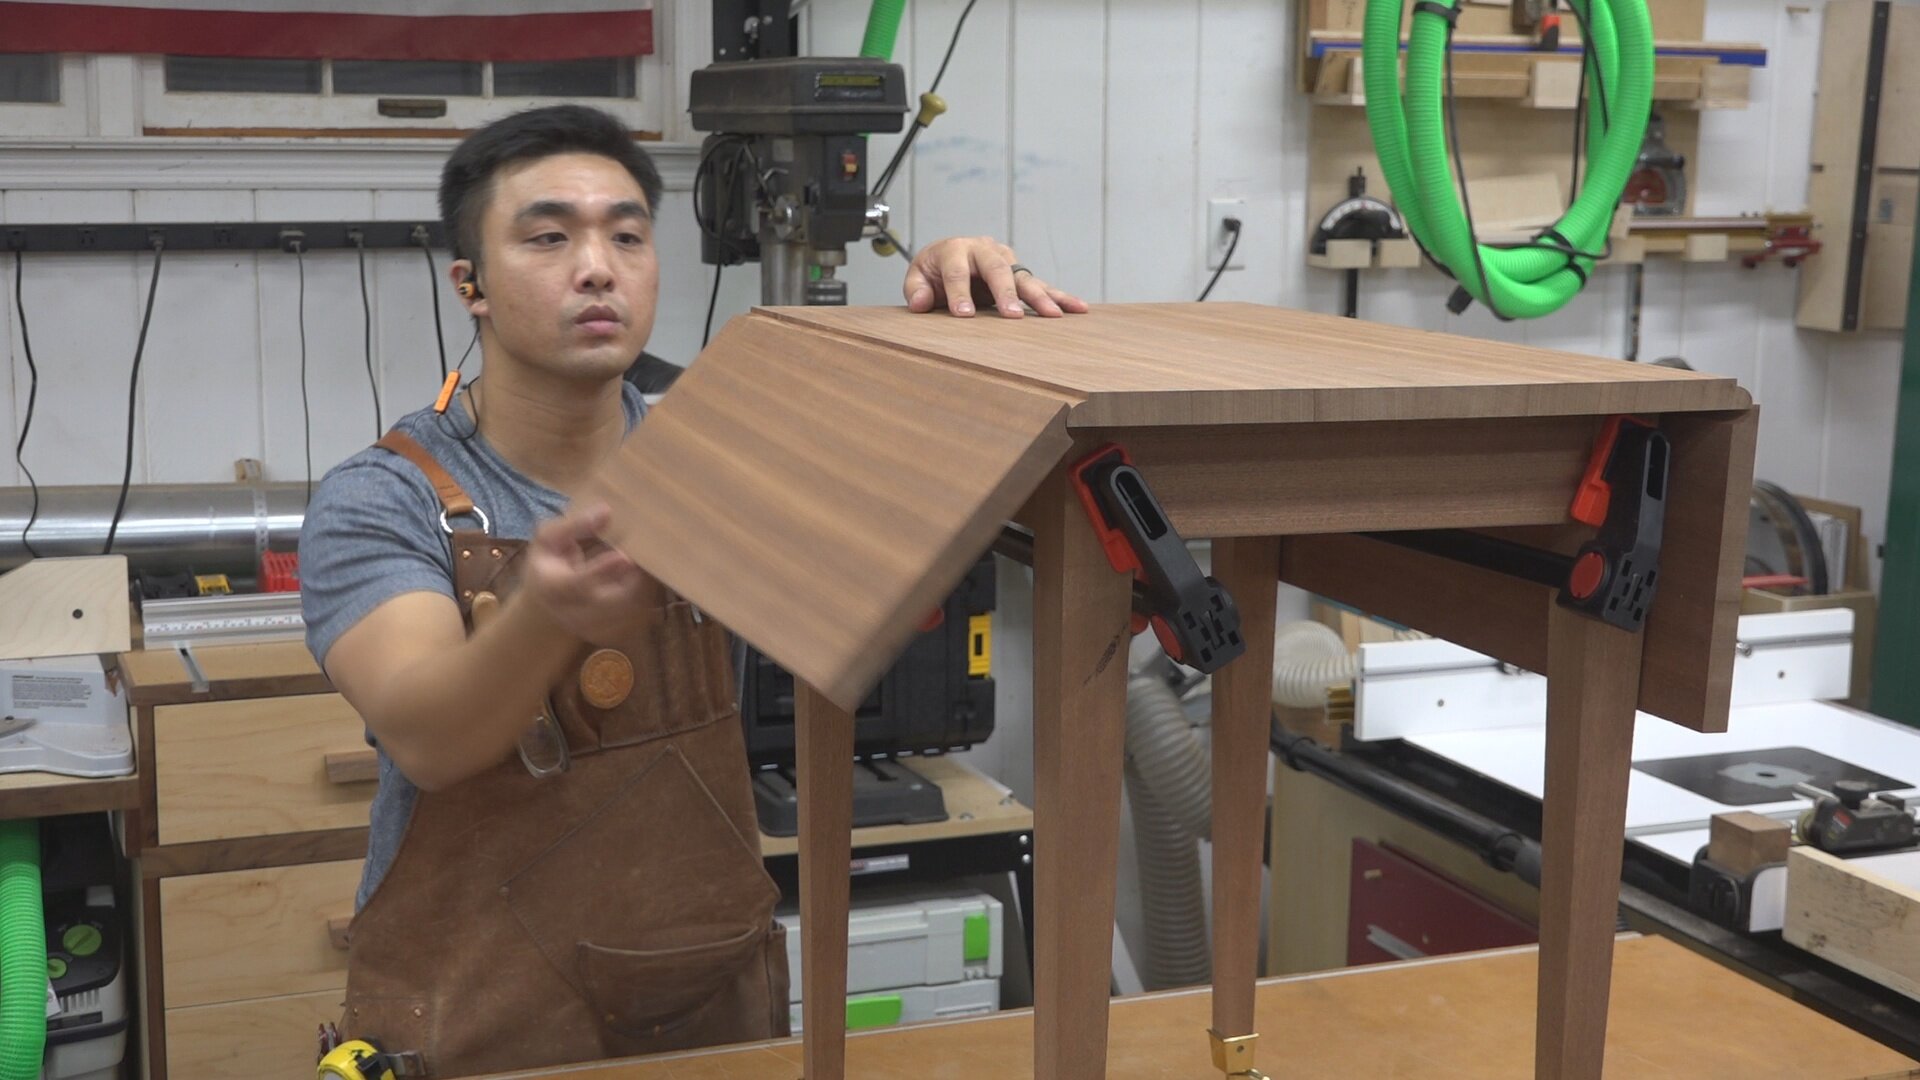
With the use of a single routing template, I was able to produce the mortises for the drop leaf hinges. The result is a properly functioning drop leaf table.
Milling Lumber S4S
Milling lumber S4S (surfaced 4 sides) is the first step to producing great furniture
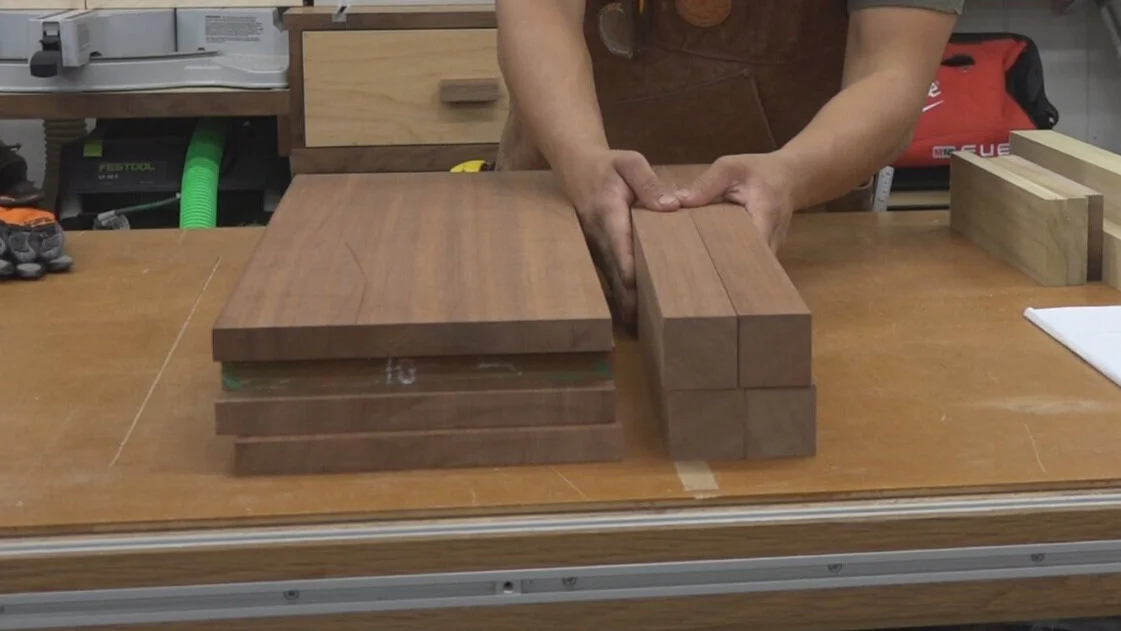
Milling lumber S4S (surfaced 4 sides) is the first step to producing great furniture
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
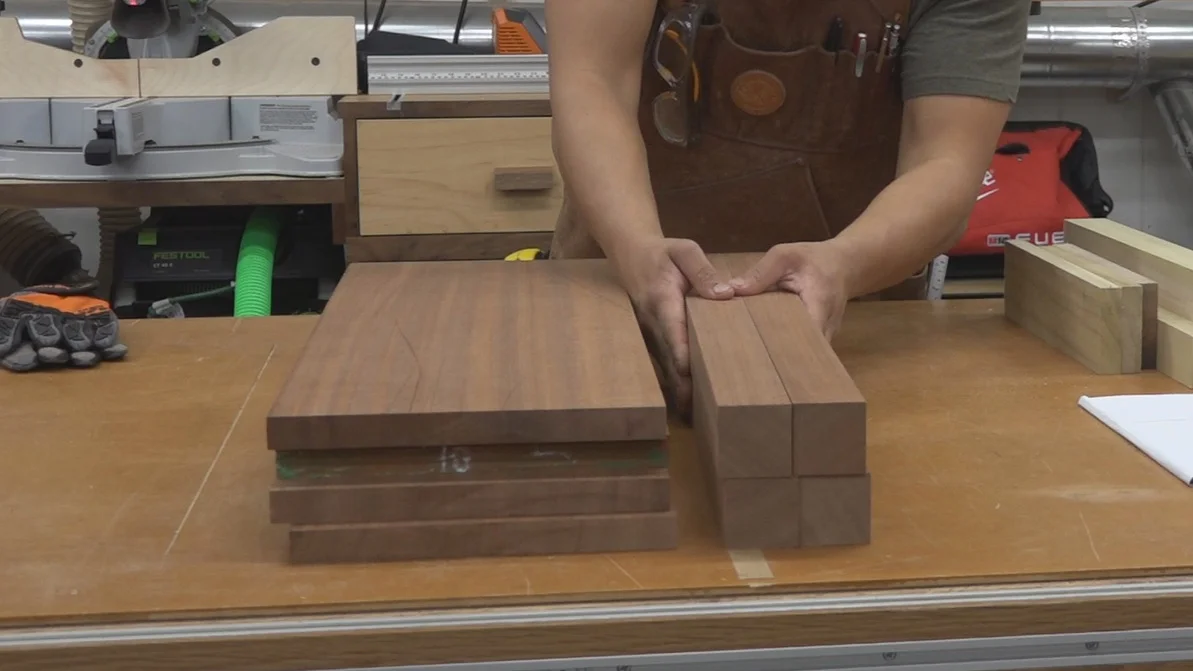
Milling lumber S4S (surfaced 4 sides) is the first step to producing great furniture. Here’s how I go about milling my lumber to get square and parallel.
It’s always important to allow your lumber acclimate to your shop. My shop is climate controlled so there tends to be less humidity in my shop relative to the warehouse these boards were stored in. So I allow at least a week (sometimes 2-3 weeks depending on where they came from and how they were stored and dried). I first come up with a cut list of final dimensions for my furniture parts. My general rule of thumb is to rough cut my material 1/2” greater in length, and 1/4” great in width. I also want to make sure I have enough material in thickness to eliminate any cupping or bowing through the jointing process.
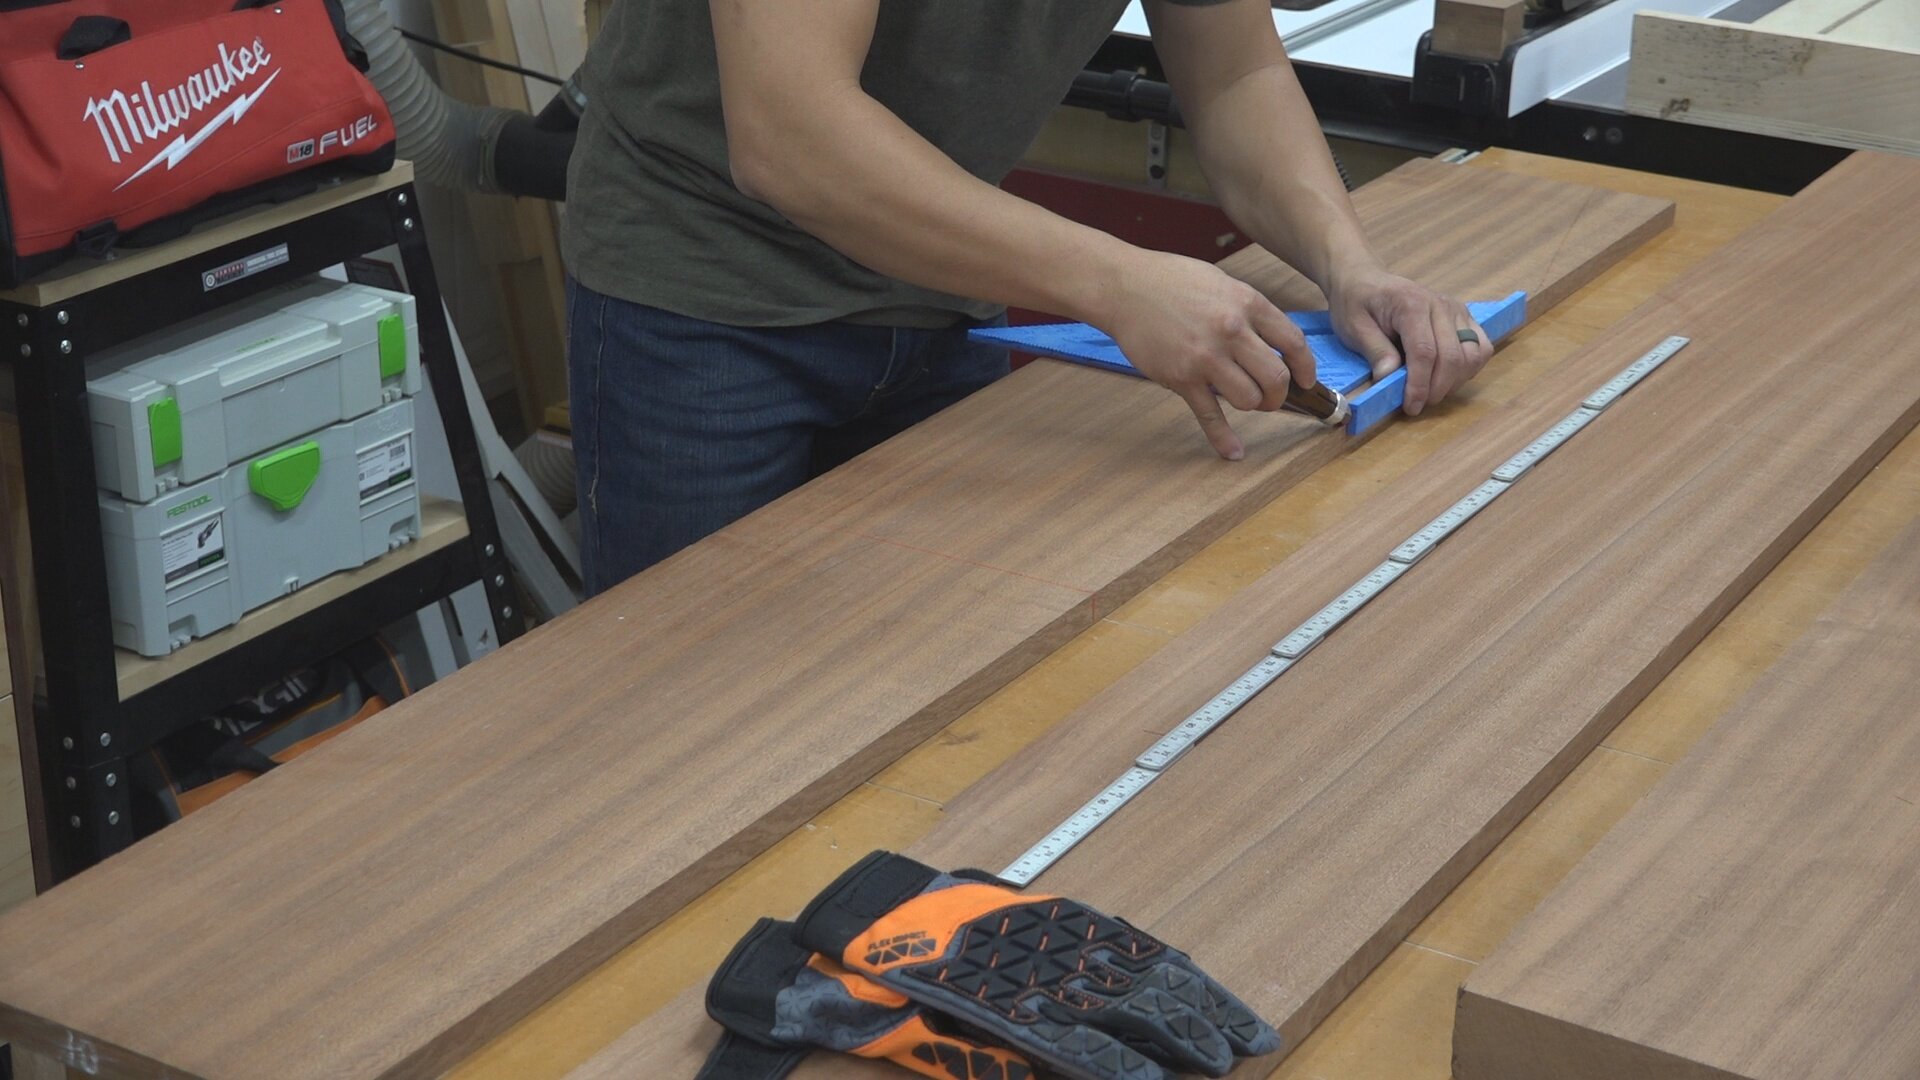
Laying out the rough dimensions of my furniture pieces
Next I crosscut my material to rough length at my Makita 18V X2 (36V) BL MITER SAW. I'm using the Makita Jobsite Miter Saw Stand which is great for processing rough lumber because it's portable and can be moved around to open space for those really long and cumbersome boards. I make sure to use my hold down clamp and take progressively deeper cuts until I'm all the way though my material to ensure I don't get kick-back. When handling rough lumber, I like to use Firm Grip PRO-Fit Flex Impact Gloves. These gloves help protect my hands against splitters, abrasion and impact. They're also extremely comfortable because they flex with my natural hand movement.
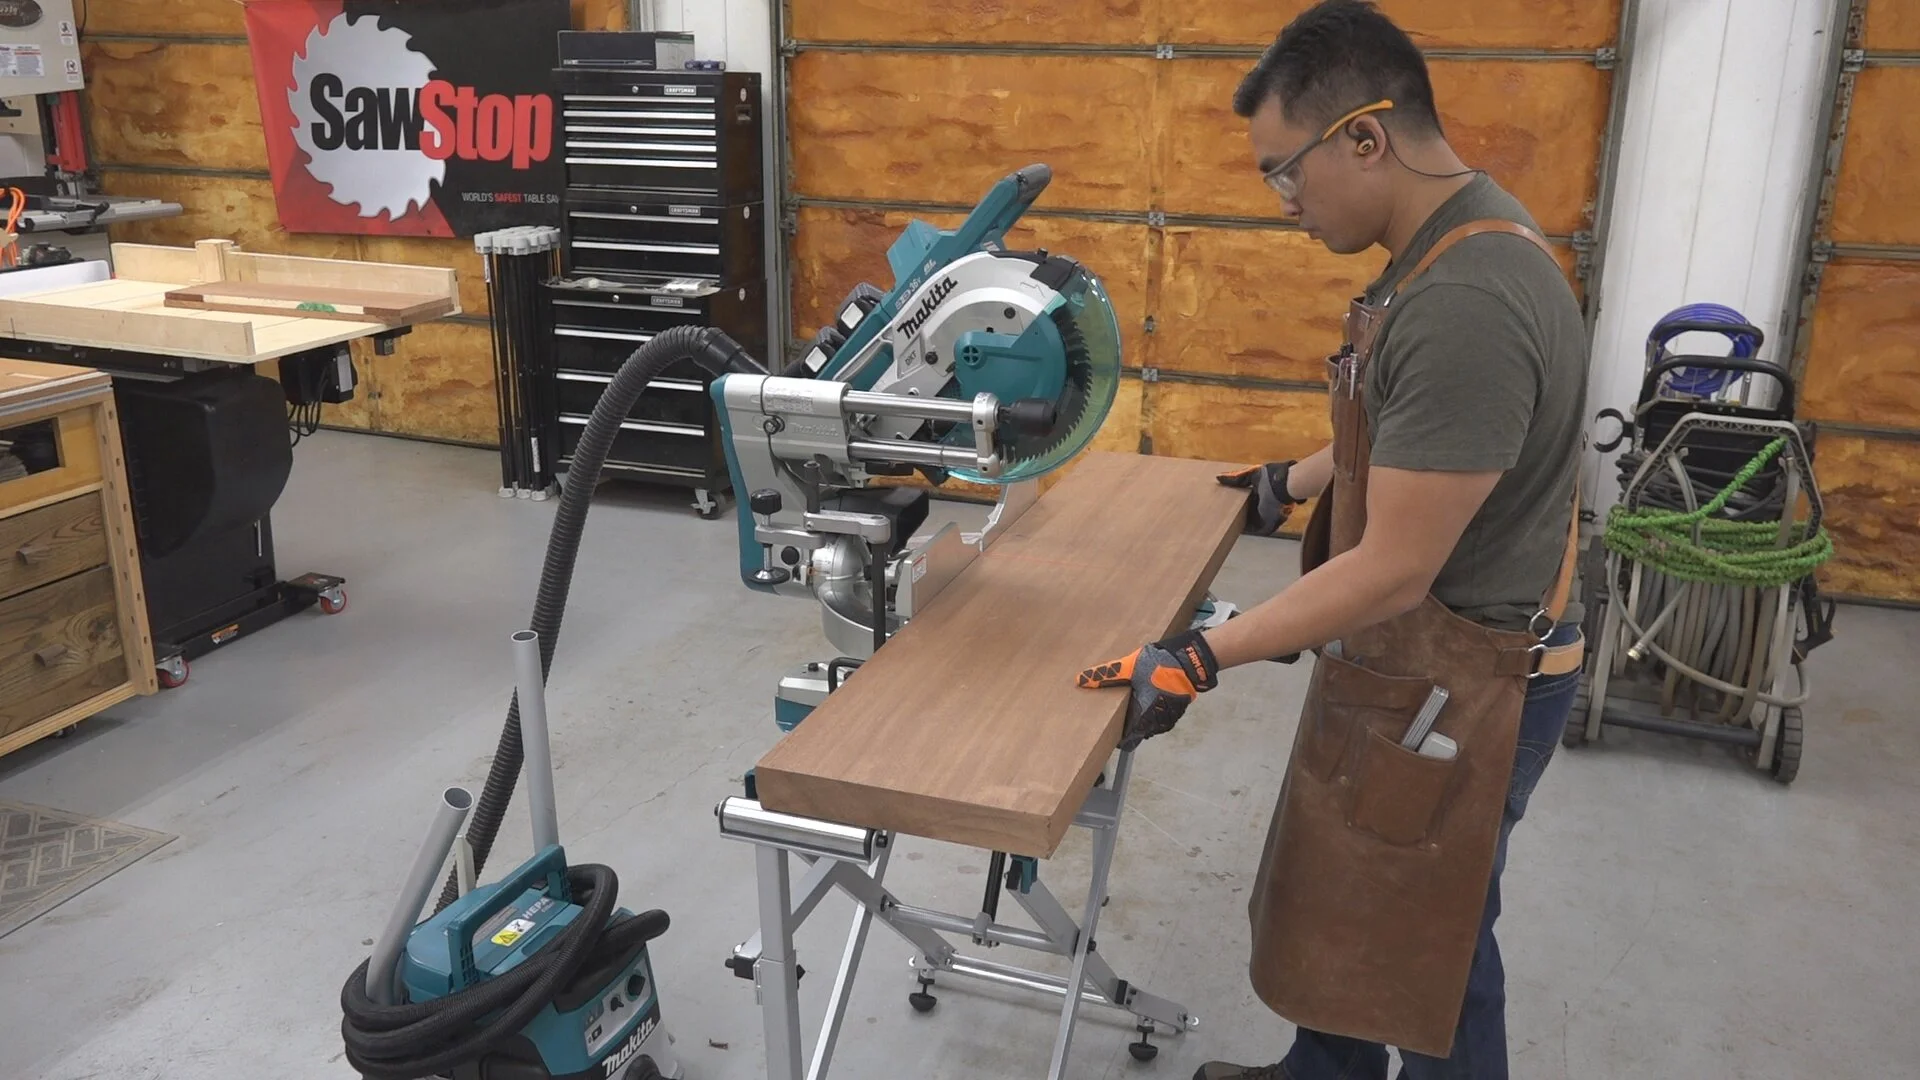
The portable job site miter stand is great to place in an open area for those long and heavy boards
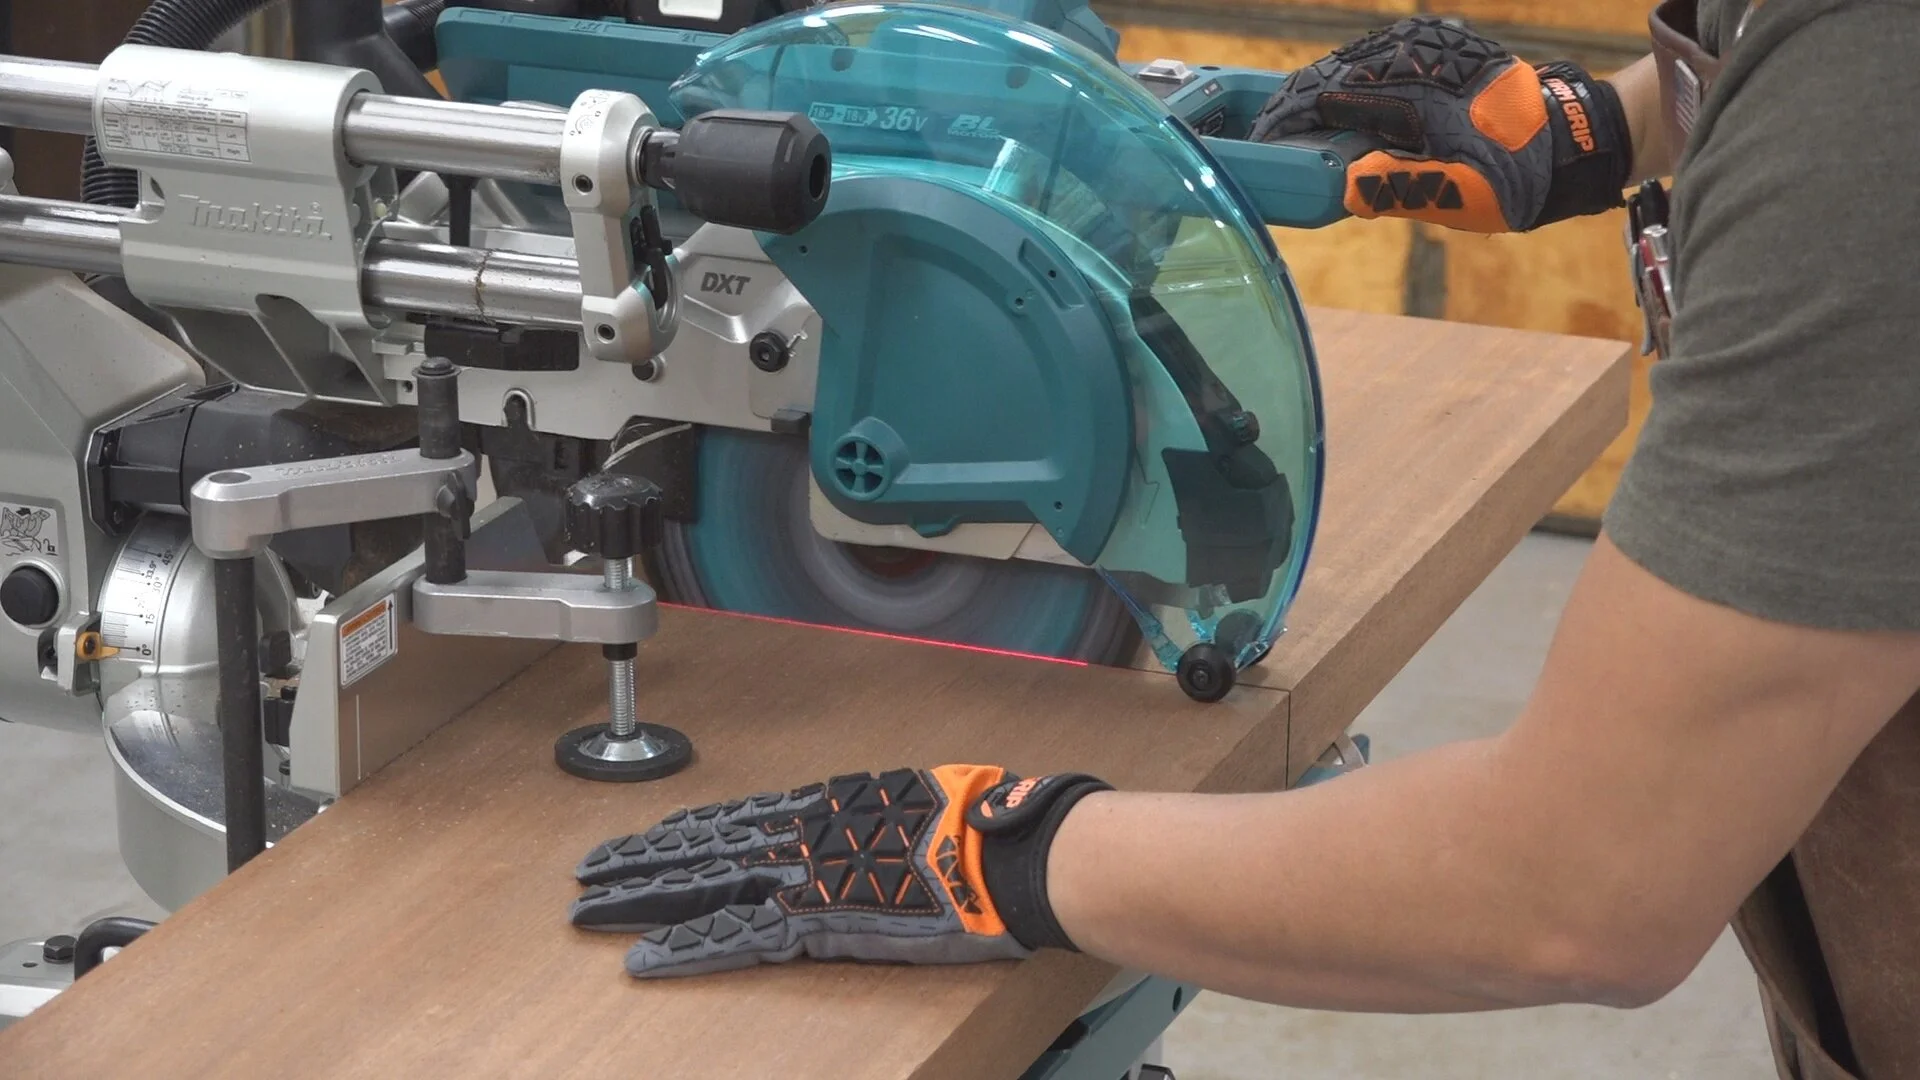
The hold down clamp ensures the board doesn’t move while cross cutting
Next I’ll rip the board down to rough width on the bandsaw. I think the bandsaw is a much safer tool to rip rough lumber. I don’t use the table saw because any slight twist, cup, warp, or internal stresses within the rough lumber can cause the table saw blade to bind. While a bandsaw blade could also bind, there’s less surface area and all of the energy from the blade is being directed down as opposed to towards the user. Just keep that in mind.
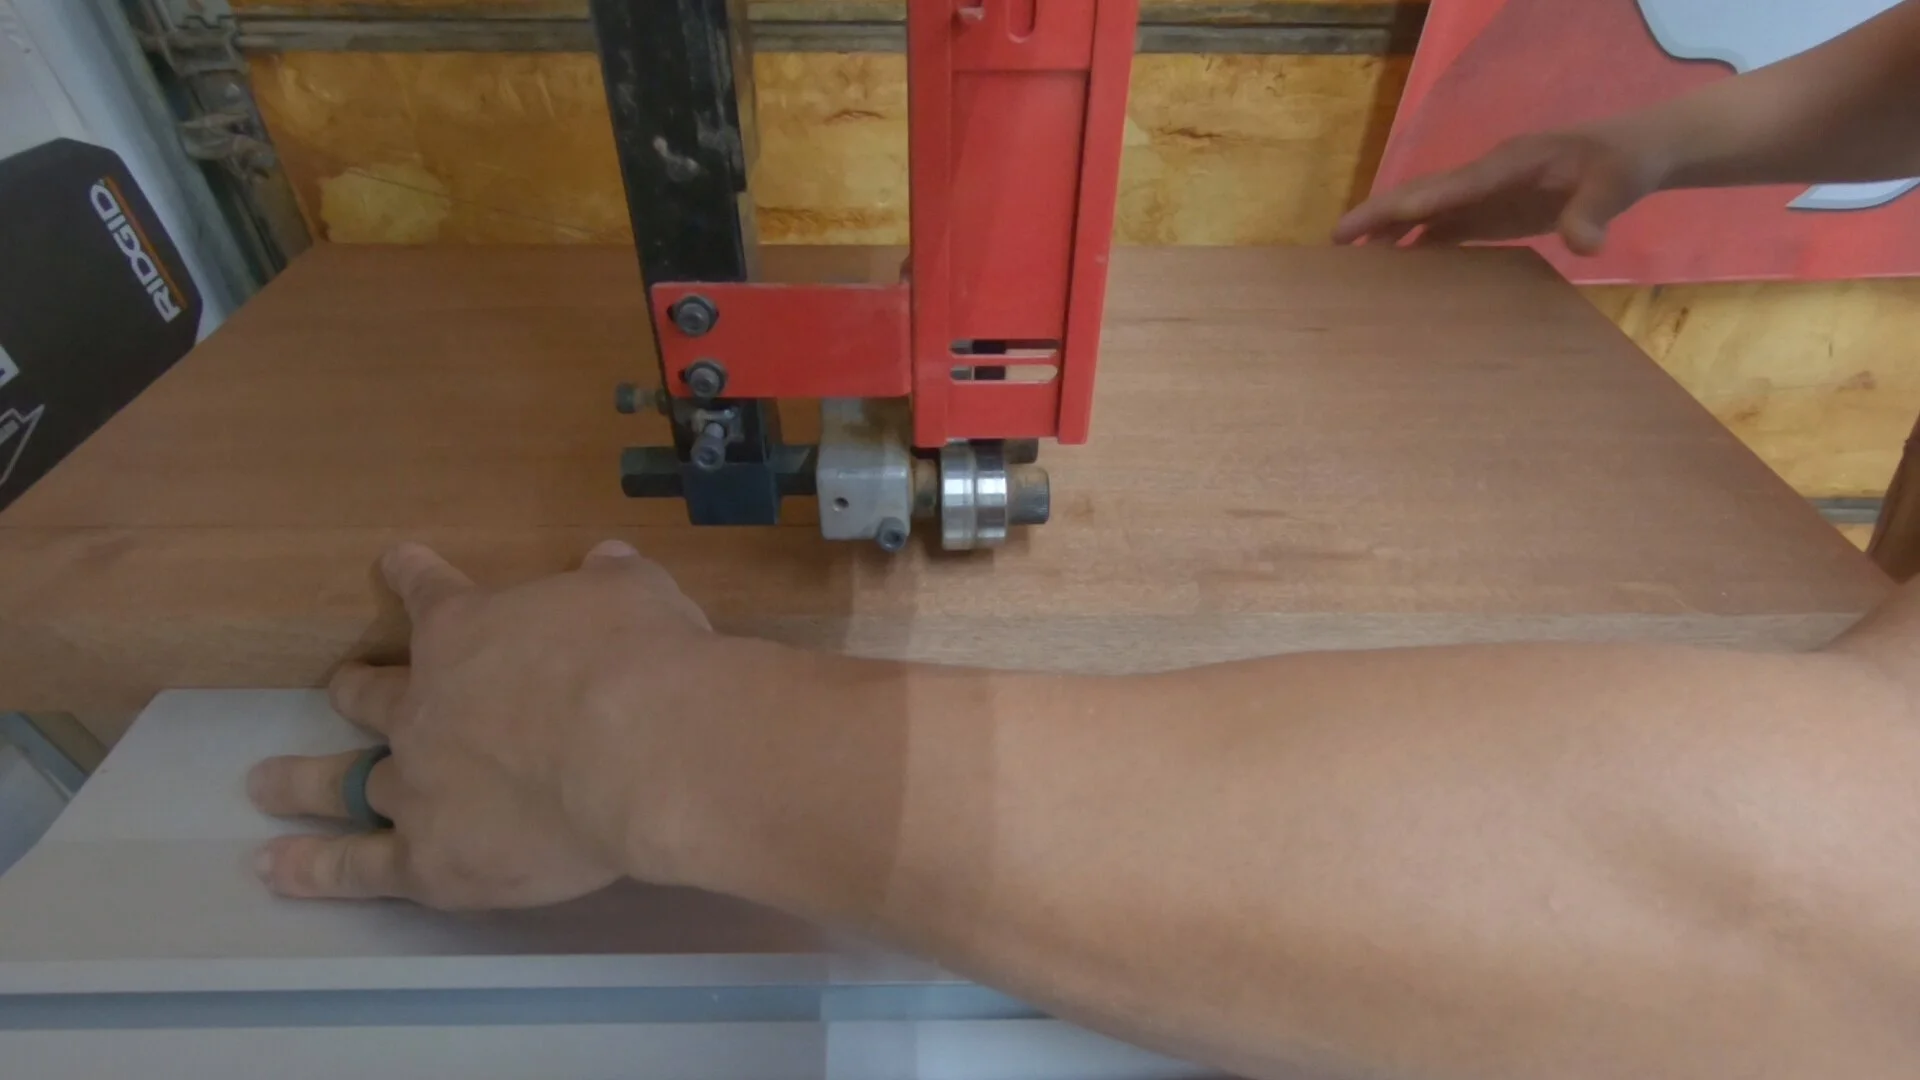
Cutting to rough width on the bandsaw
I like to do my milling in stages. I’ll do an initial face jointing operation to get the face of a board relatively flat and then plane just take off an even surface and get the two face parallel. I’ll then let the boards rest for a couple of days and come back and face joint again and plane to final thickness once I’m ready to start machining the furniture parts. This allows the wood to “move” as it looses moisture through the initial milling process. The final jointing and planing gets the faces flat and parallel right just in case there was any wood movement.
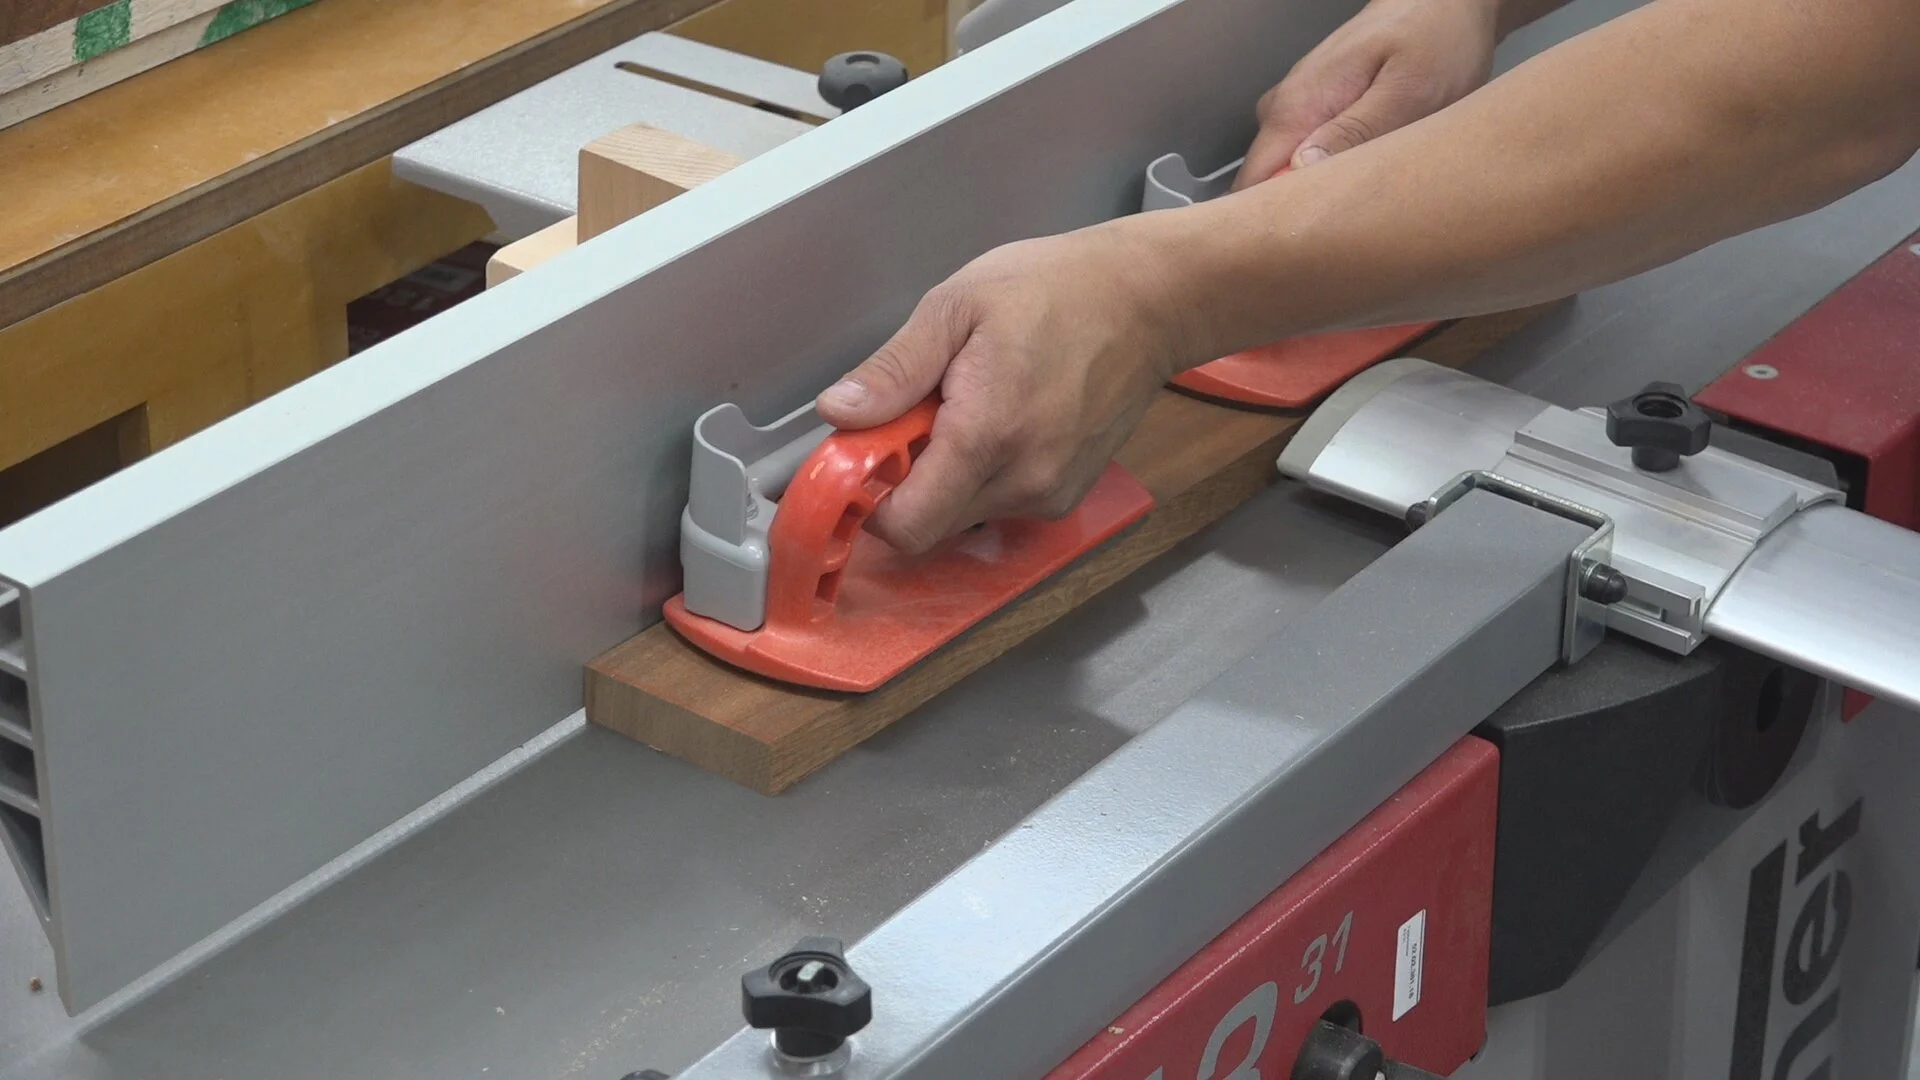
Face jointing get the face of the board flat
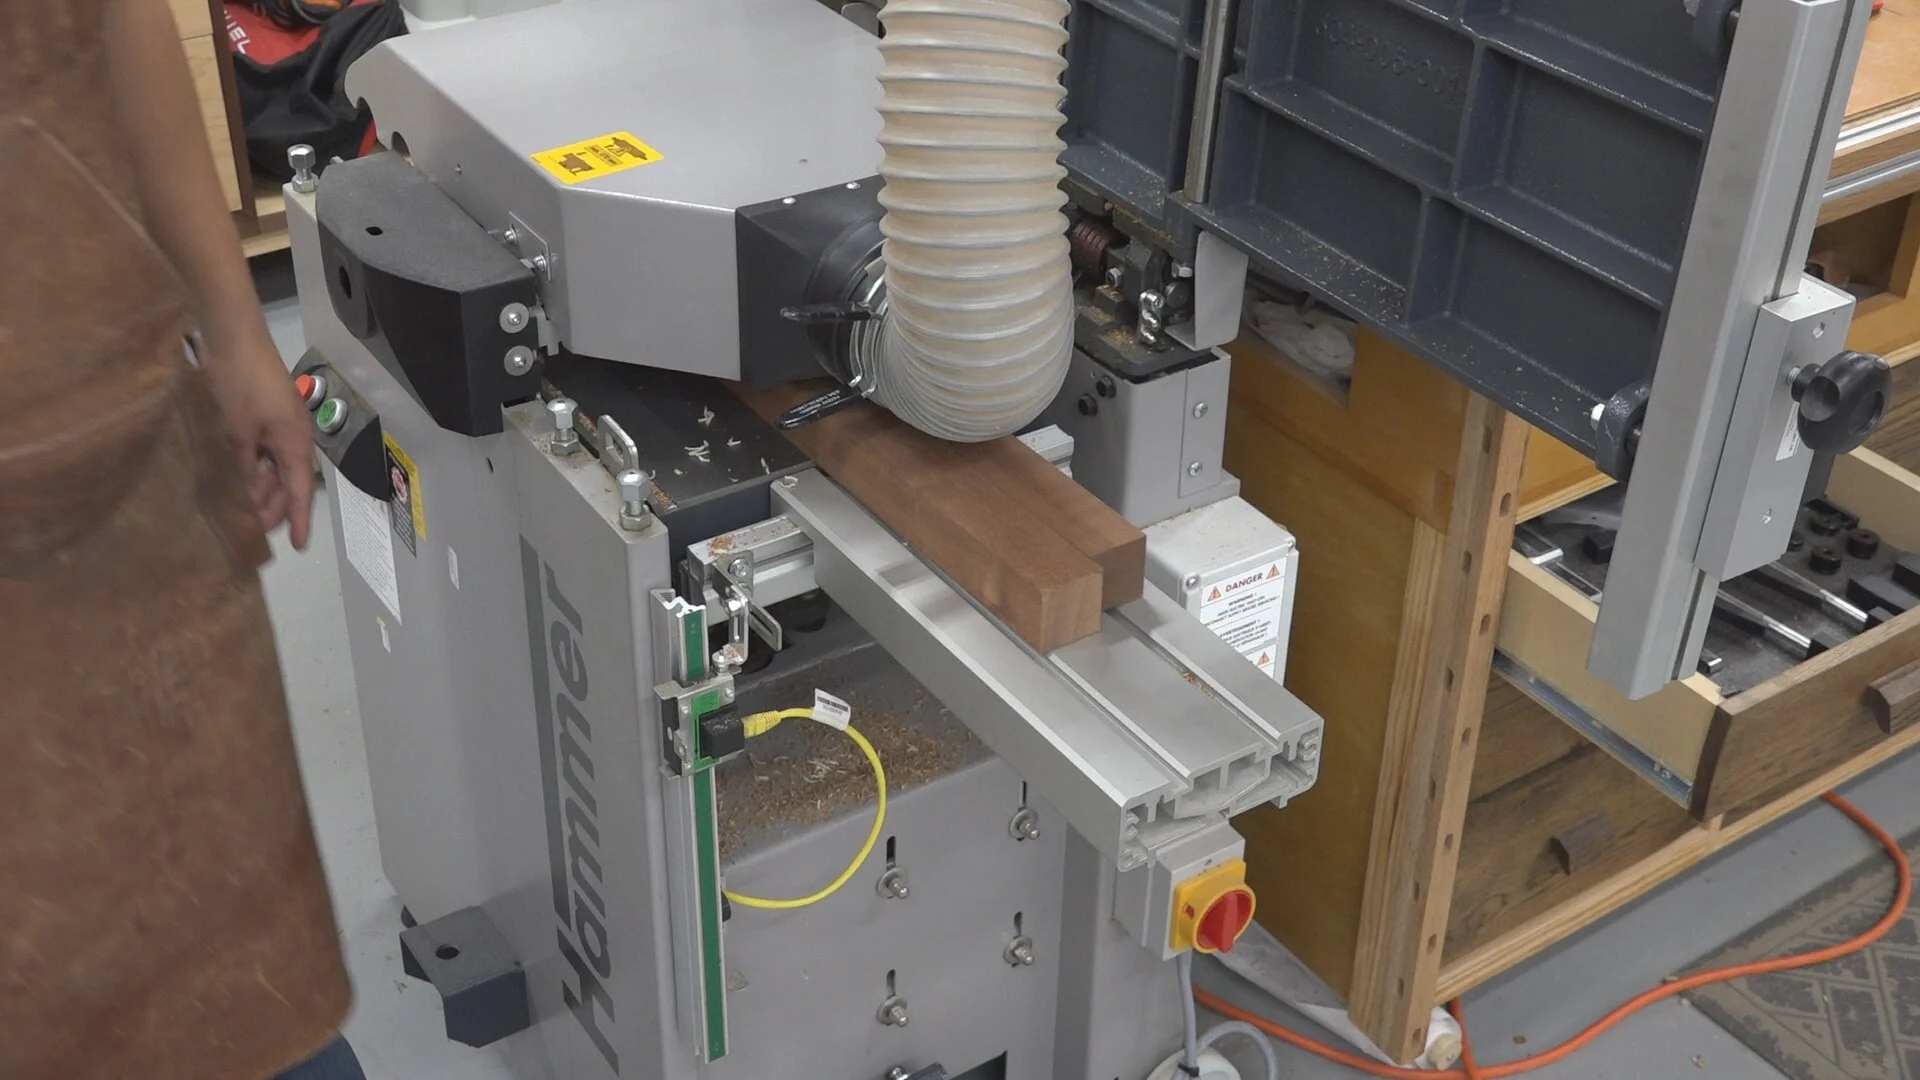
Planing is done after face jointing to get two parallel faces. When planing to final thickness, I try to take an equal amount off of both faces.
When I’m planing to final thickness, I like to take an equal amount on both faces. This way I’m introducing an equal amount of new material to the environment and is less likely to get a cup or a bow post processing. Once I’ve planed down to final thickness, I’ll edge joint. This edge the edges of my material nice and straight. For material wider than 1 inch, I’ll run the jointed edge against my planer bed and use the planer to machine the rough edge down to final width. For stock less than 1 inch, I like to use the table saw. The planer is a much more accurate tool to machine down to final width. However, stock less than 1 inch can be “tippy” on the planer bed.
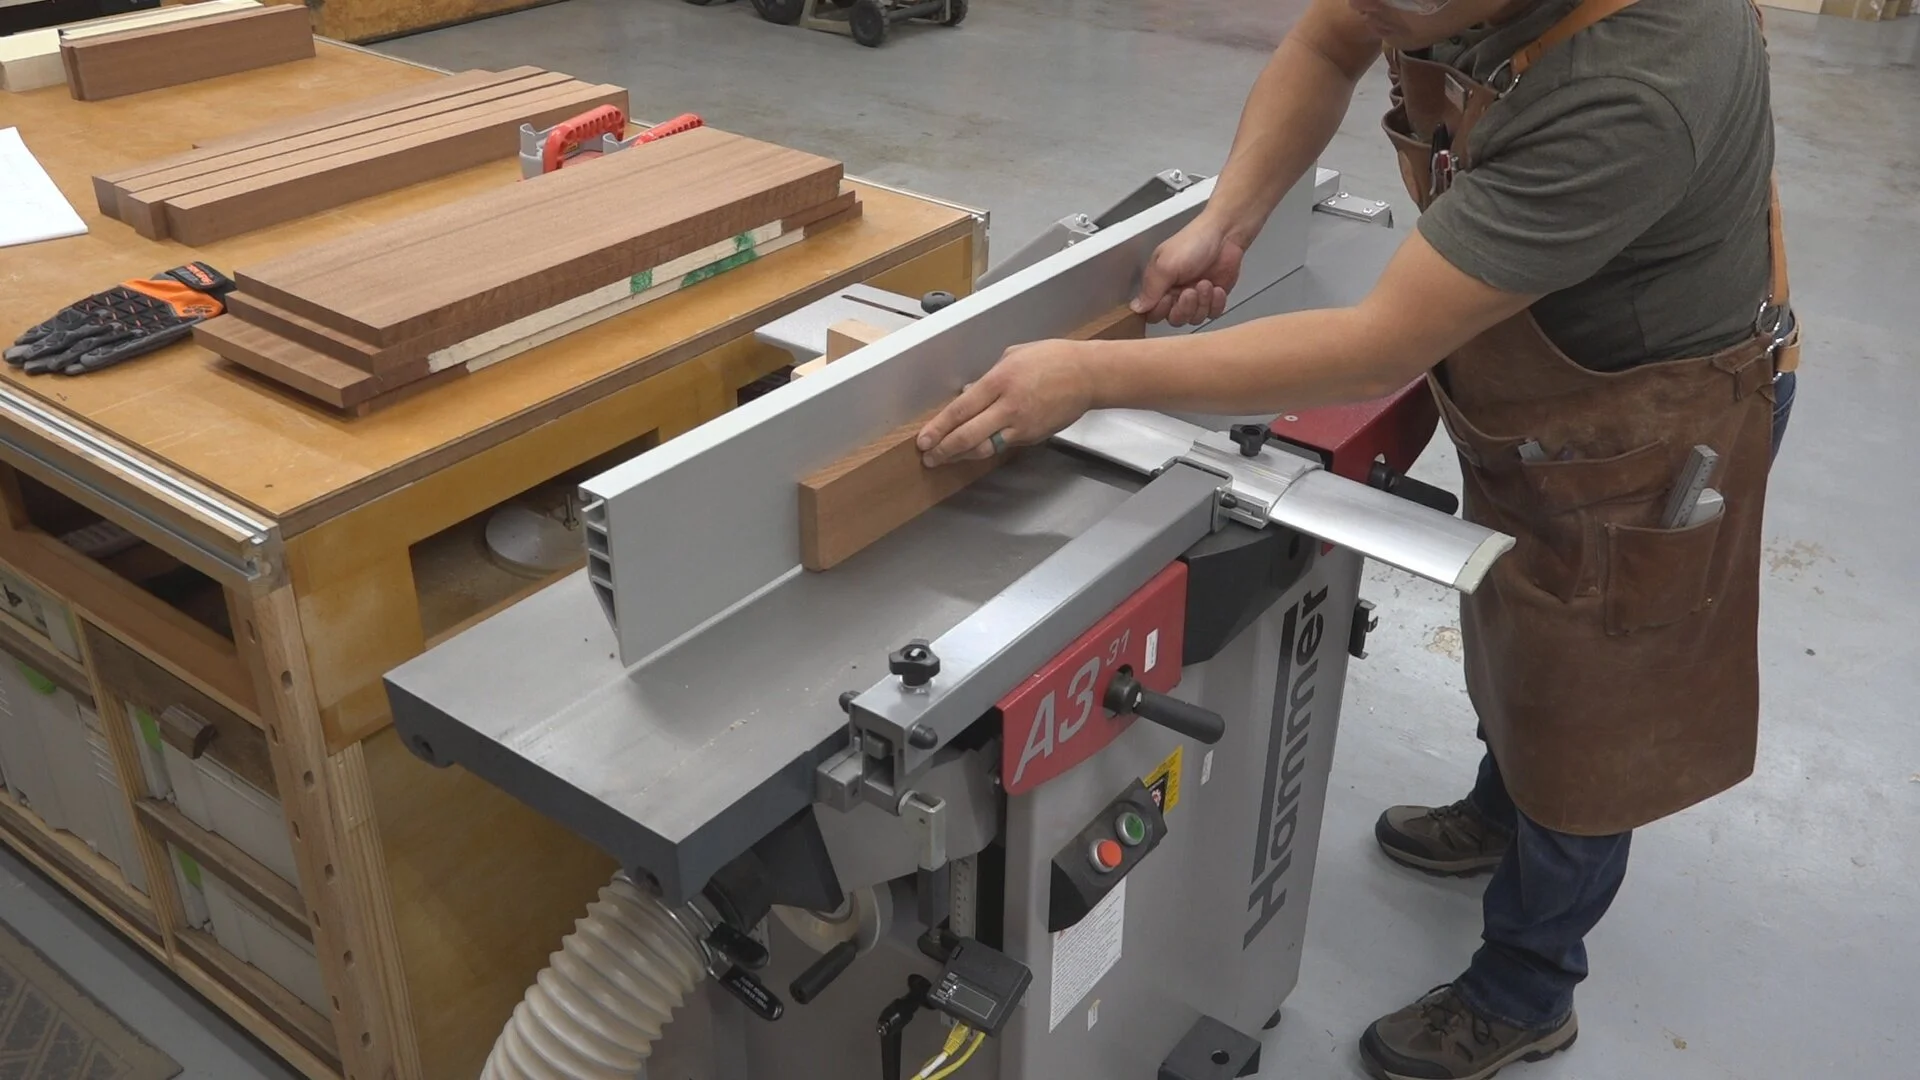
Edge jointing to get a straight and flat reference edge
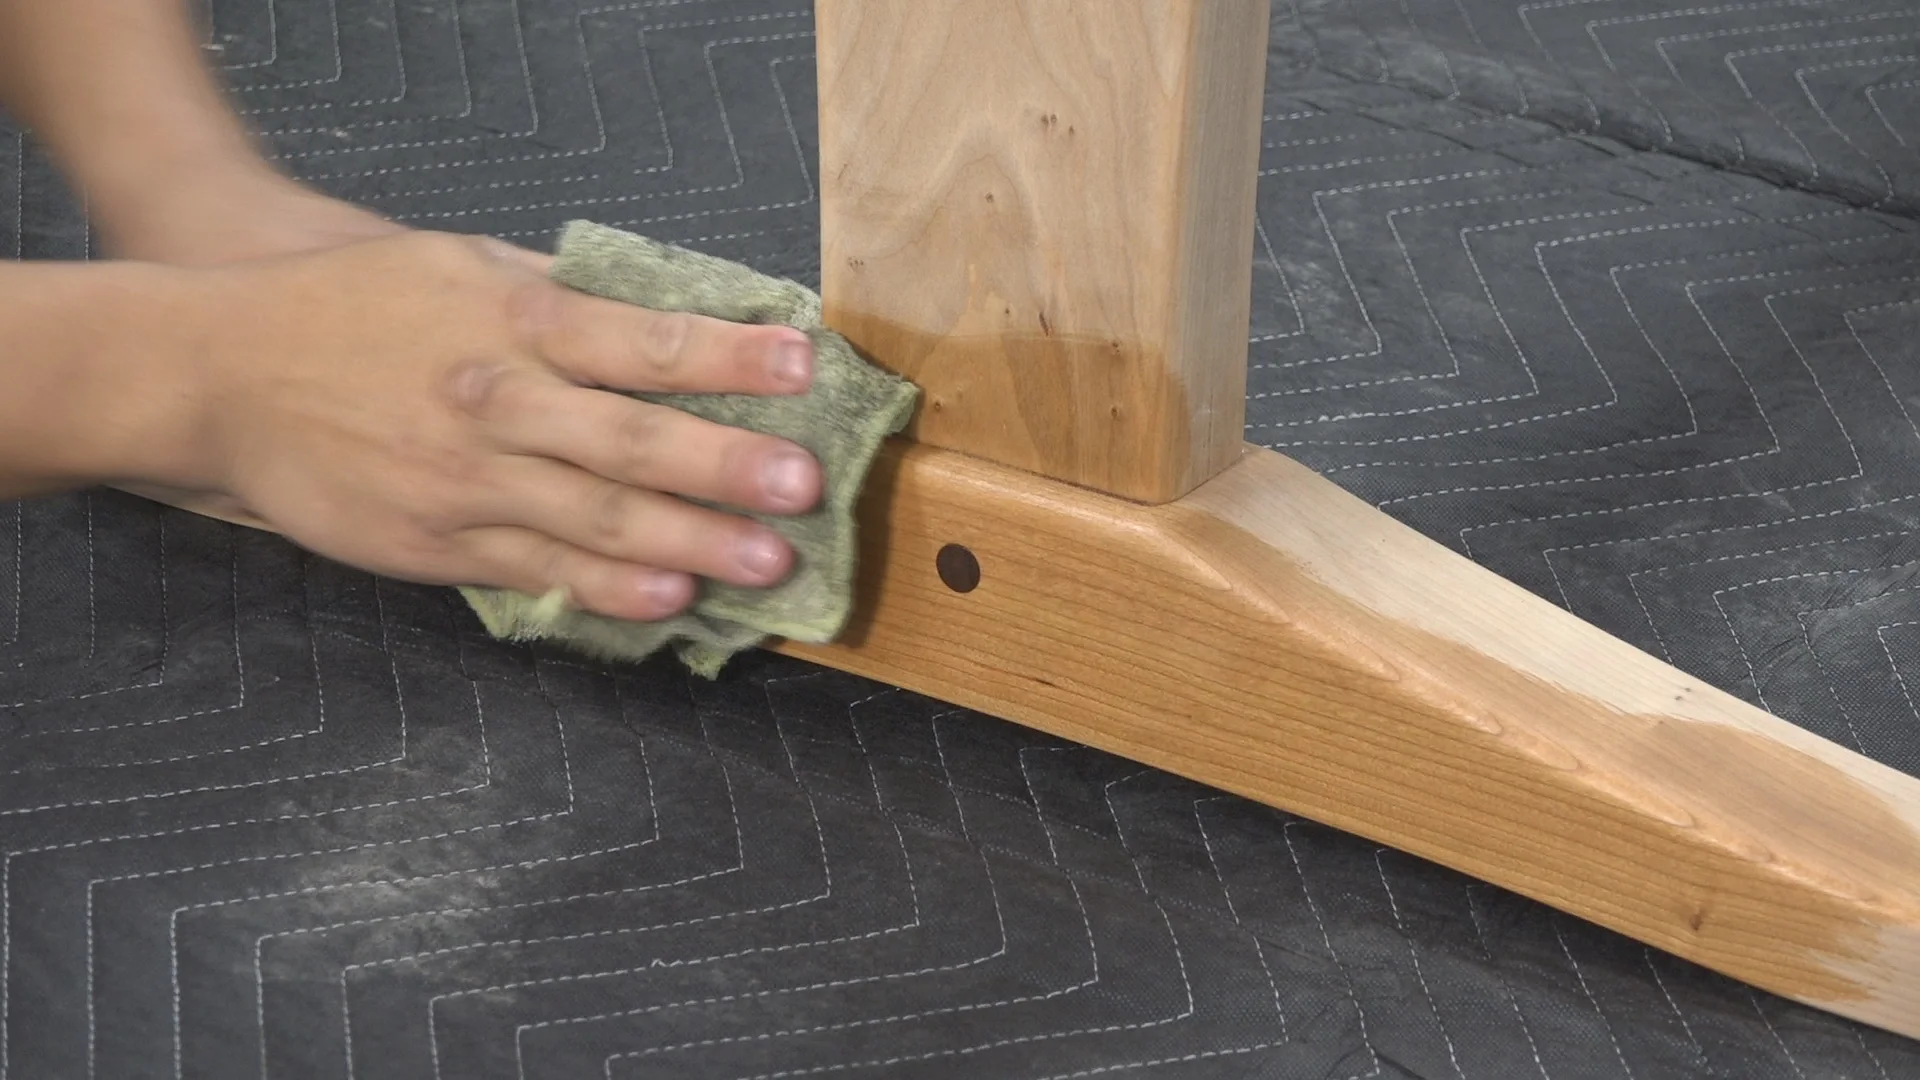
Draw Boring Tenons
Draw boring is an ancient technique of combining the chemical strength of glue with the mechanical strength of an interlocking dowel.
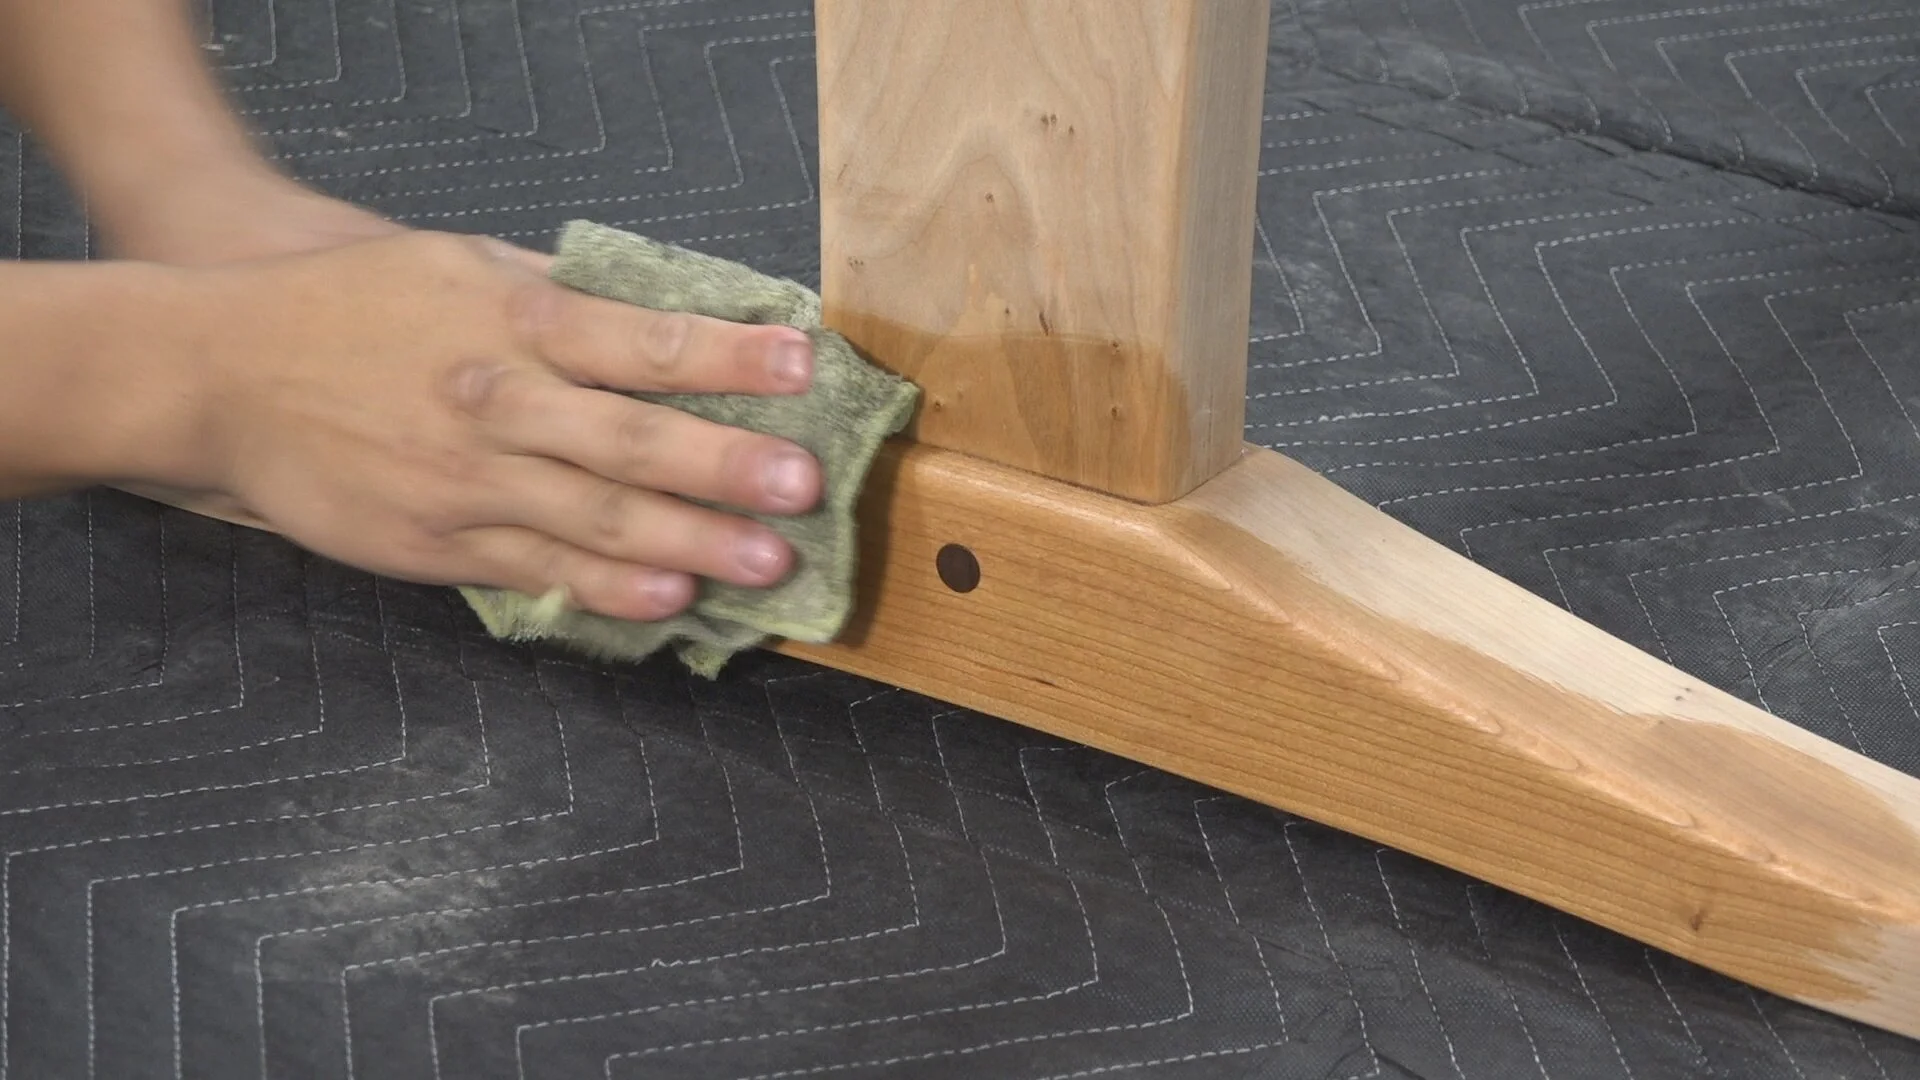
Draw boring is an ancient technique of combining the chemical strength of glue with the mechanical strength of an interlocking dowel
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
Draw boring is a technique that strengthens a mortise and tenon joint by using a dowel and offset holes in the mortise and tenon to draw the joint together. This combines the chemical strength of glue with mechanical strength of an interlocking dowel. Here’s how I draw bored the mortise and tenons on my trestle table leg assembly.
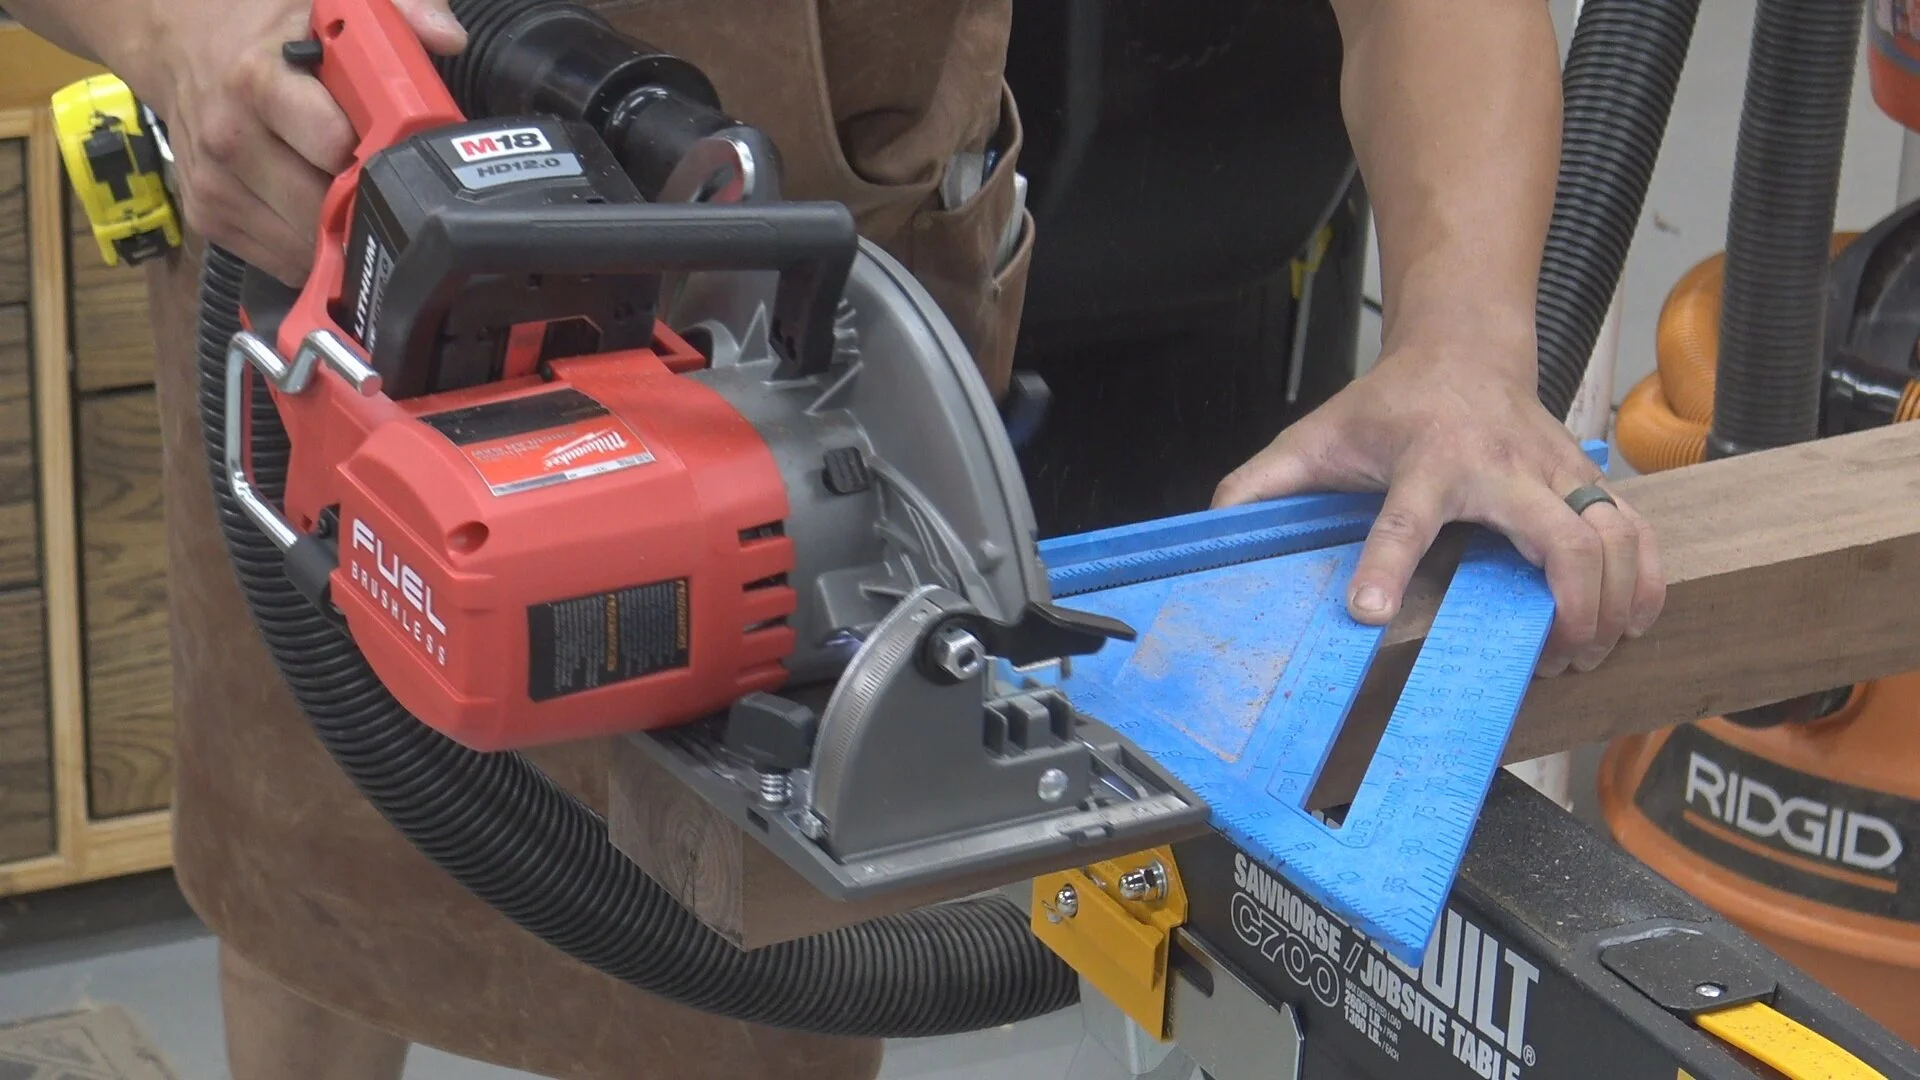
Rough cutting some straight grain Walnut
The first thing I need to do and crosscut some straight grain Walnut with my Milwaukee 18-Volt Lithium-Ion Cordless 7-1/4 in. Rear Handle Circular Saw. This thing is a beast and hogged through this straight grain 12/4 Walnut without issue. The straight grain is important because the dowels that I'll be making out of this material will need to be as strong as possible. Any imperfections within the grain structure would cause the dowel to break as it's being driven through the tenon.
Next I’ll drill out the 2-3/4 inch dowels using the 1/2 inch extra long dowel and plug cutter made by Infinity Cutting Tools at the drill press. I’ll release the dowels by crosscutting at the bandsaw.
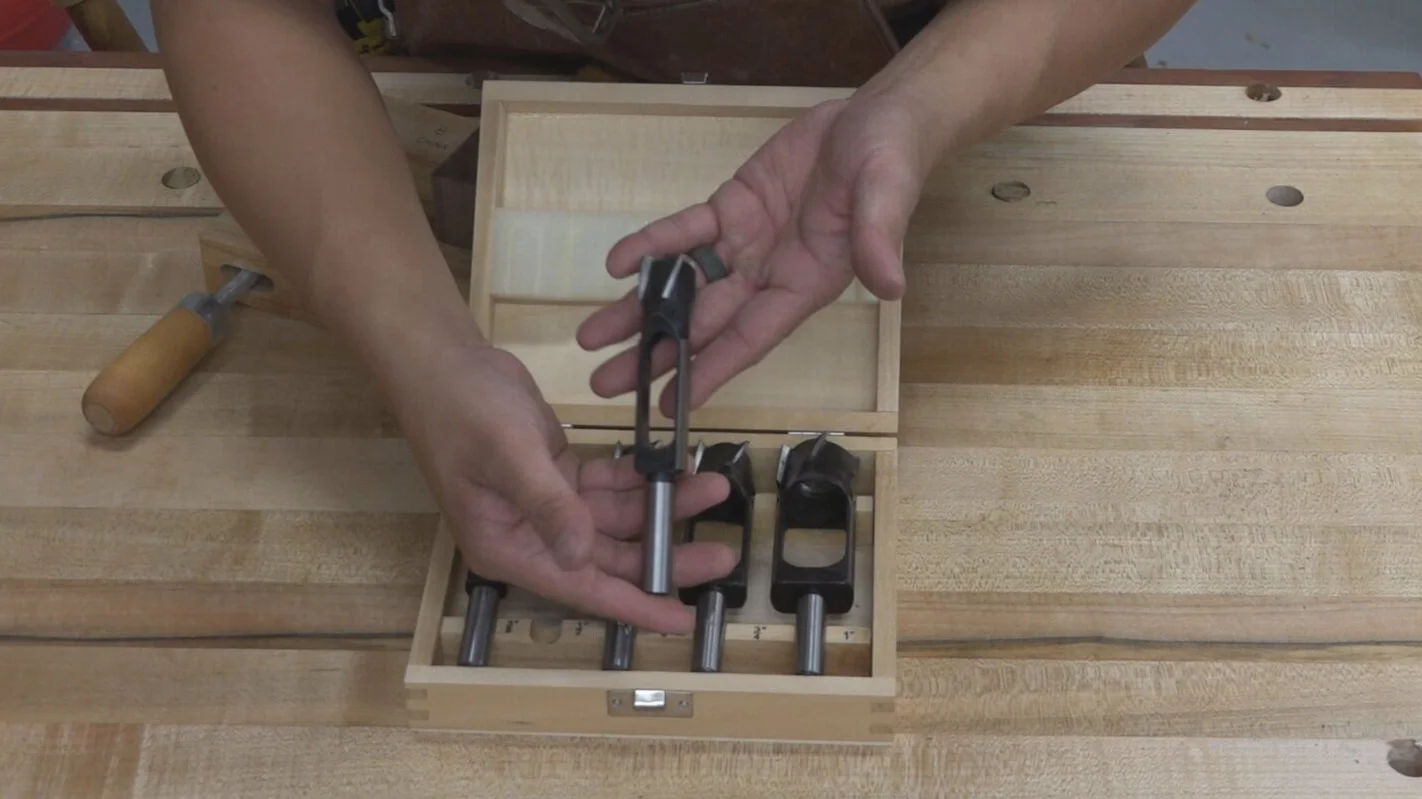
Extra long dowel and plug cutter made by Infinity Cutting Tools
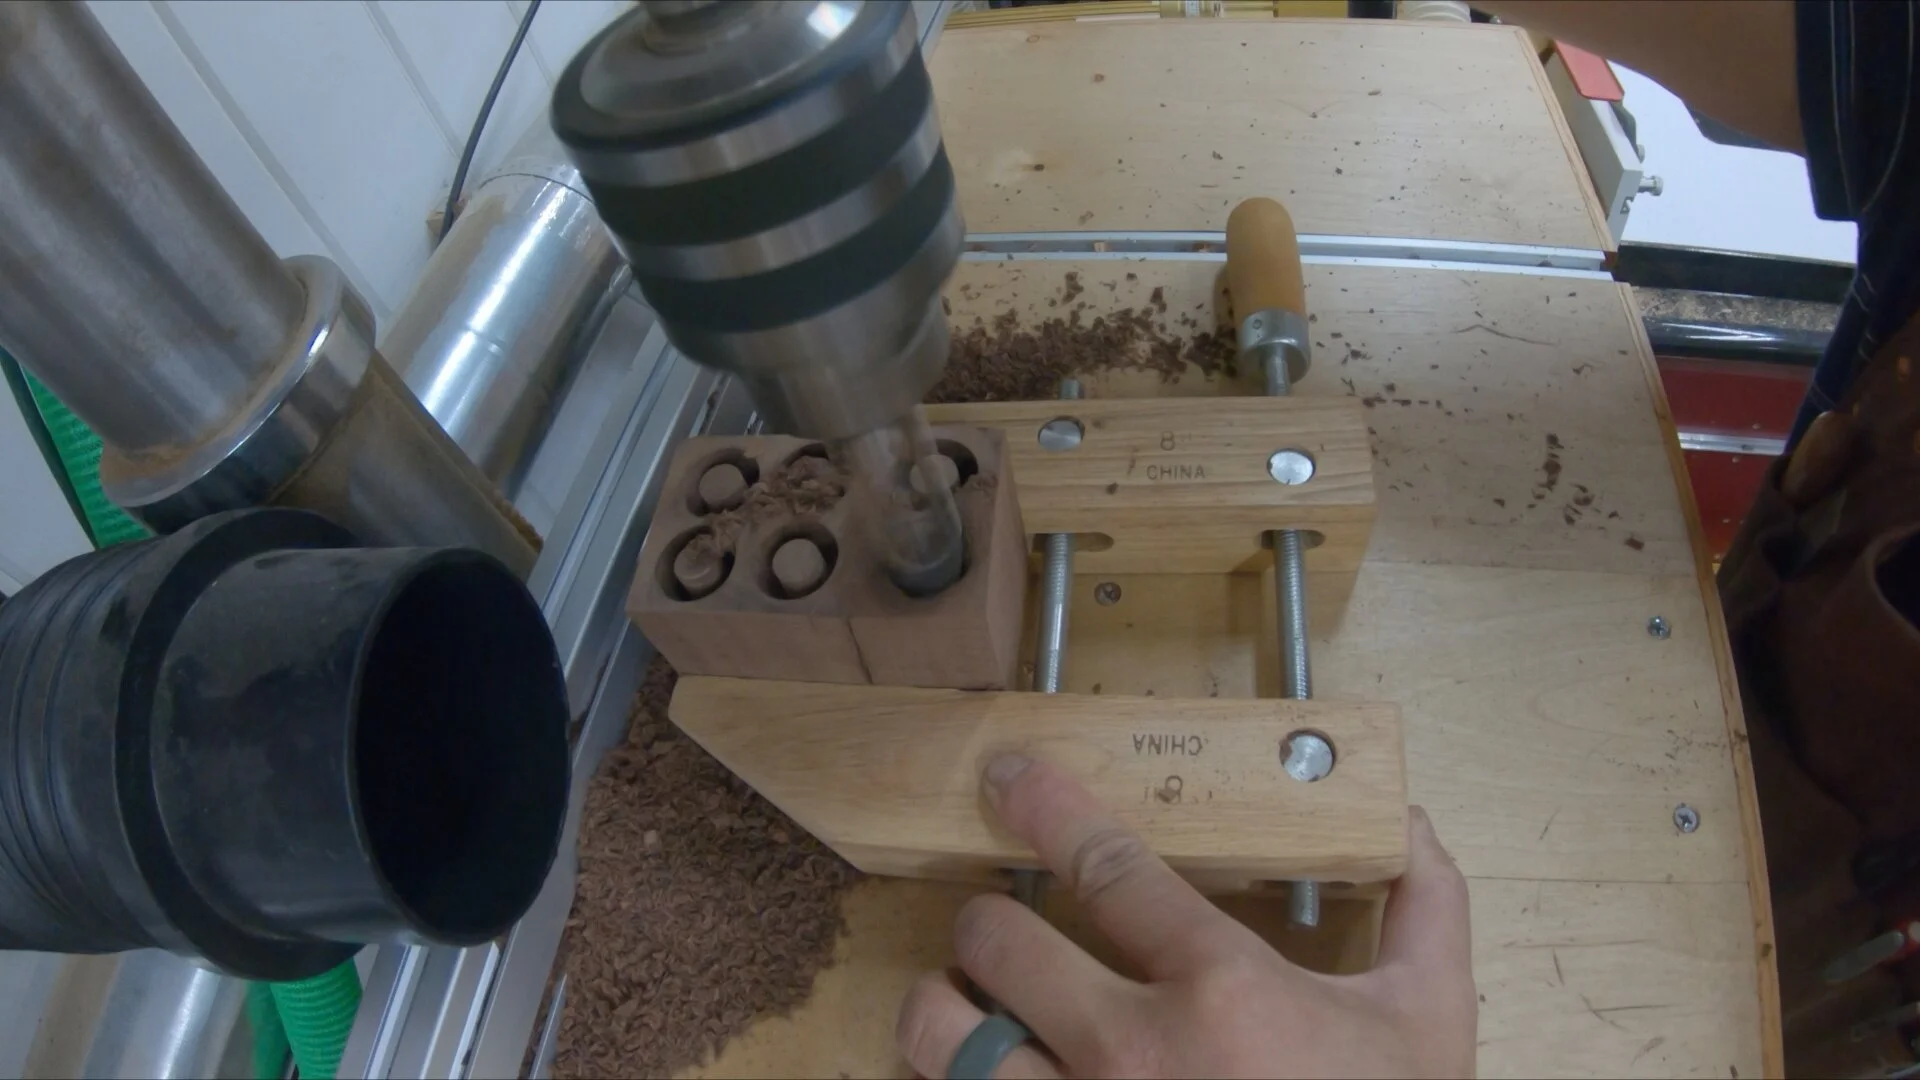
Drilling out the dowels on the drill press
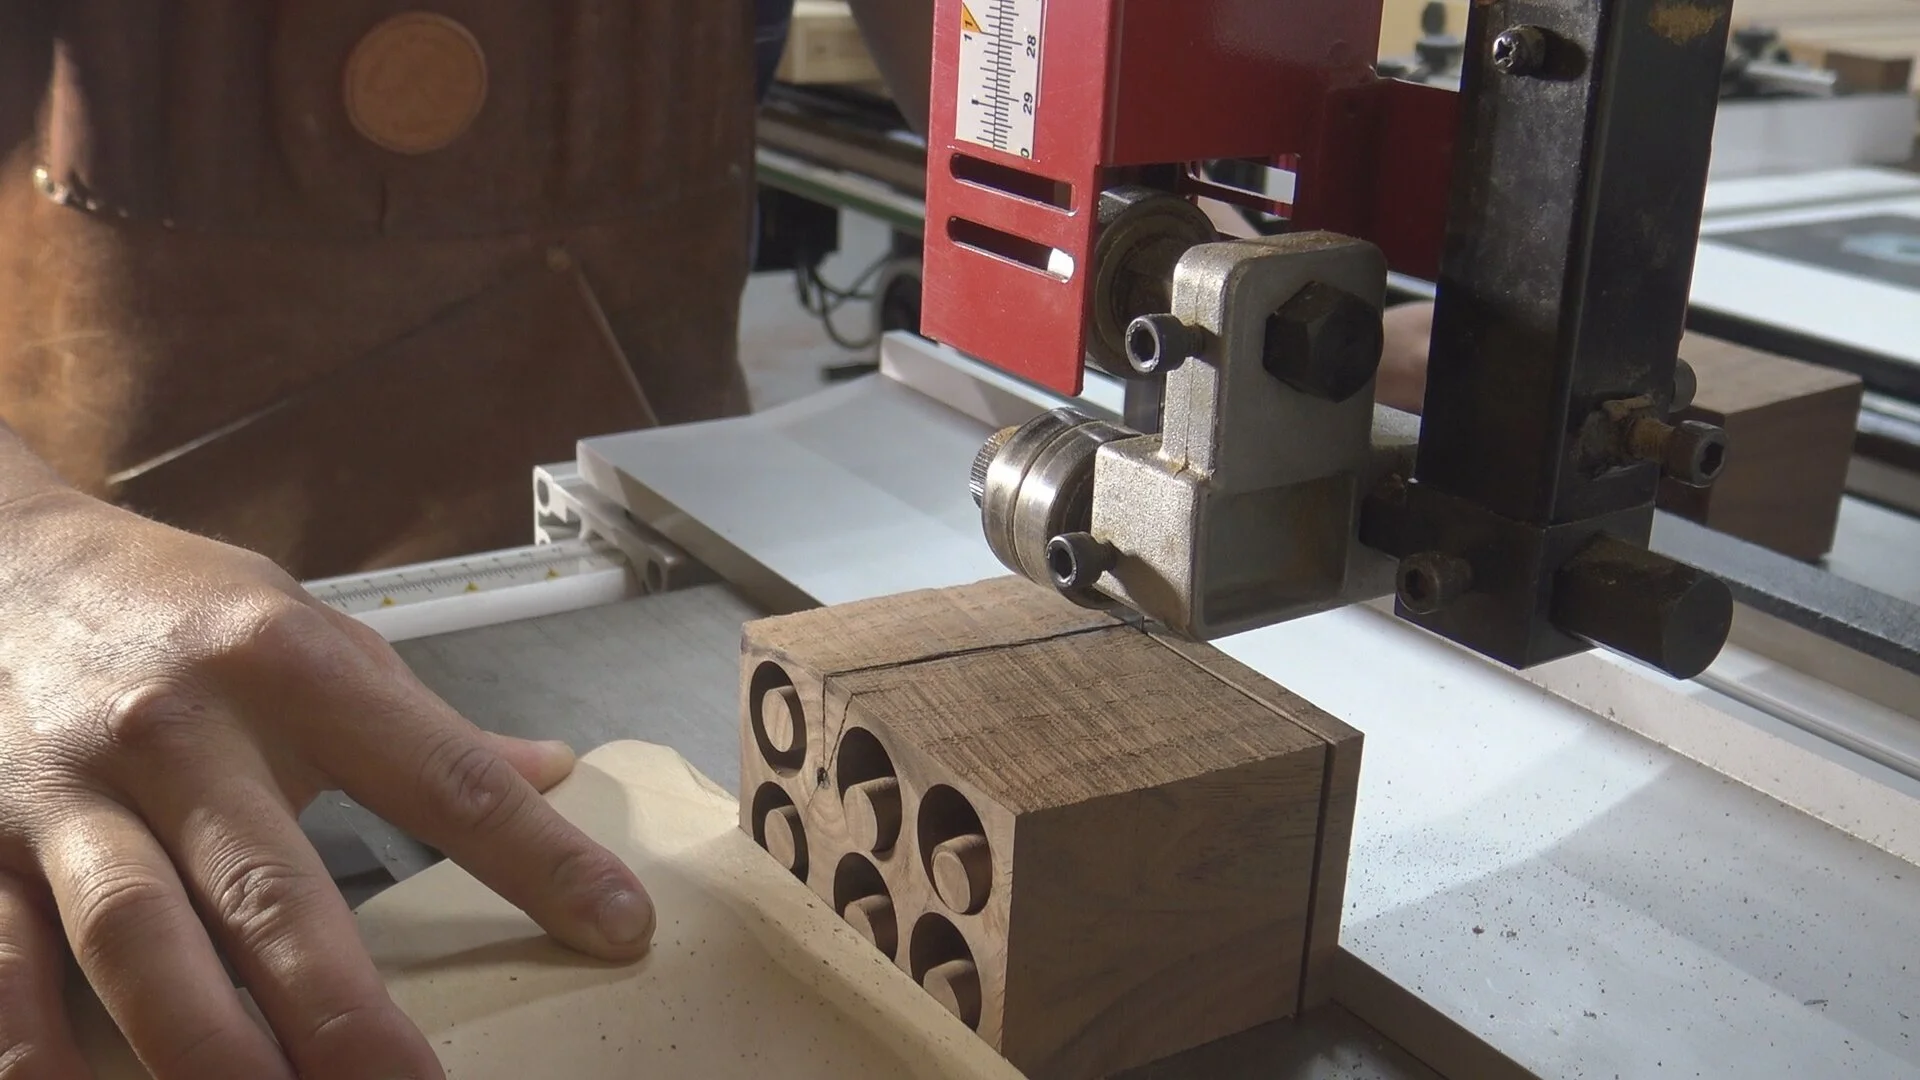
Releasing the dowels by crosscutting at the bandsaw
Now I’ll drill a 1/2” hole into the mortise portion of the leg assembly. I drill all the way through the entrance of the dowel but only dril 1/2” into the back of the leg assembly mortise. The dowel does not need to go all the way through the leg assembly. Doing so could cause the back of the leg assembly to “blow out.”
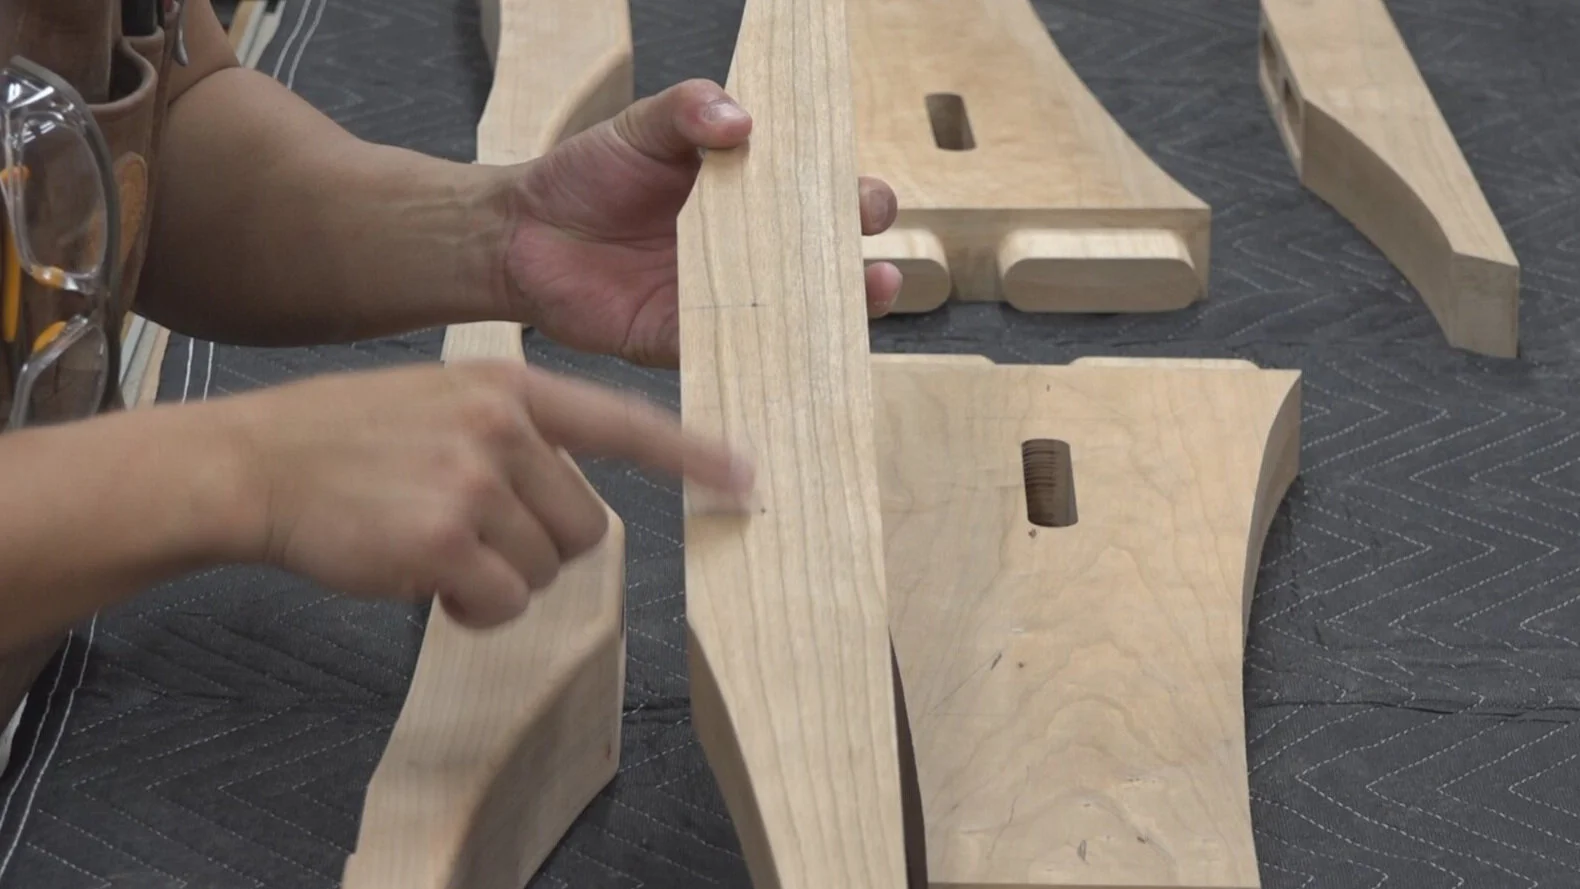
The location of the holes on the mortise portion of the leg assembly
Next, I’ll clamp the mortise and tenon joint together and using a center punch, I’ll locate the center of the hole on the tenon portion of the leg assembly. I’ll then take the mortise and tenon apart and offset the location of the hole I need to drill by 1/16” towards the shoulder of the tenon.
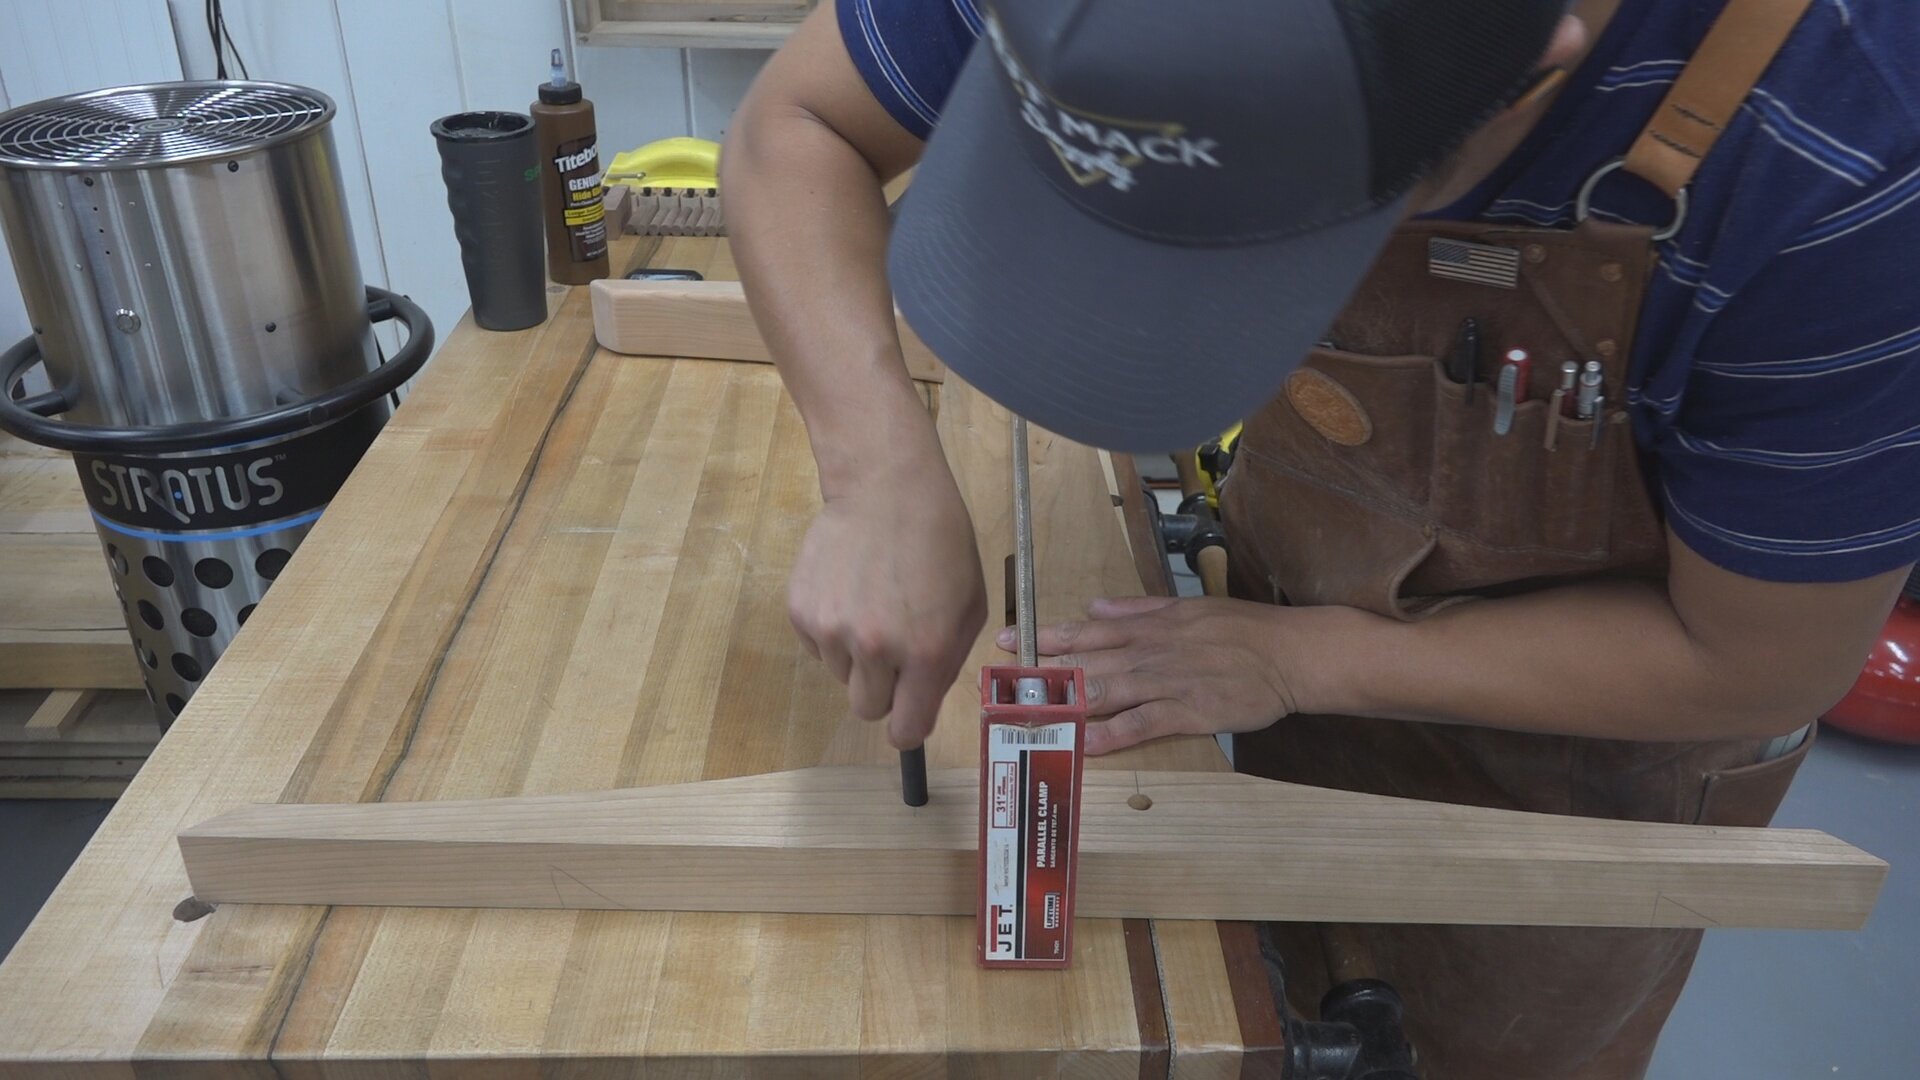
Using a center punch to locate the center of the hole in the mortise
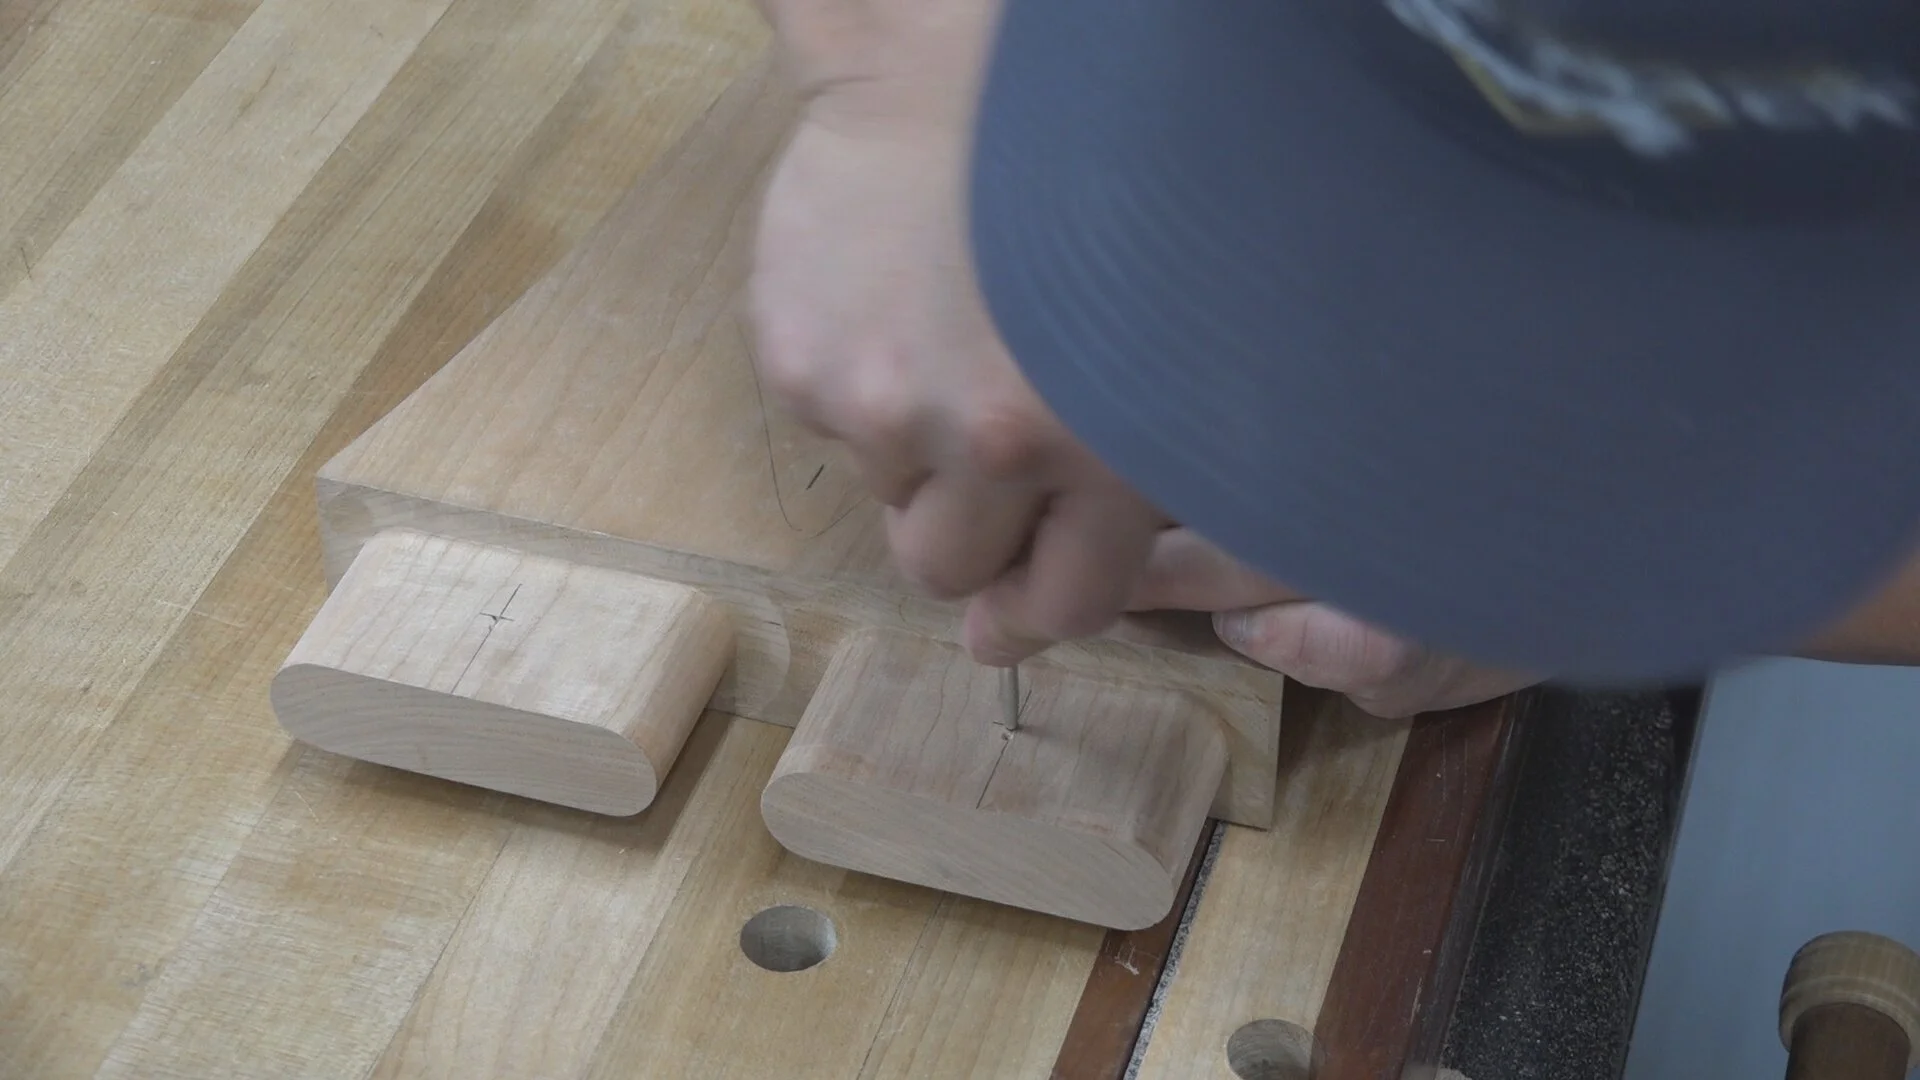
Offsetting the hole 1/16” towards the shoulder of the tenon
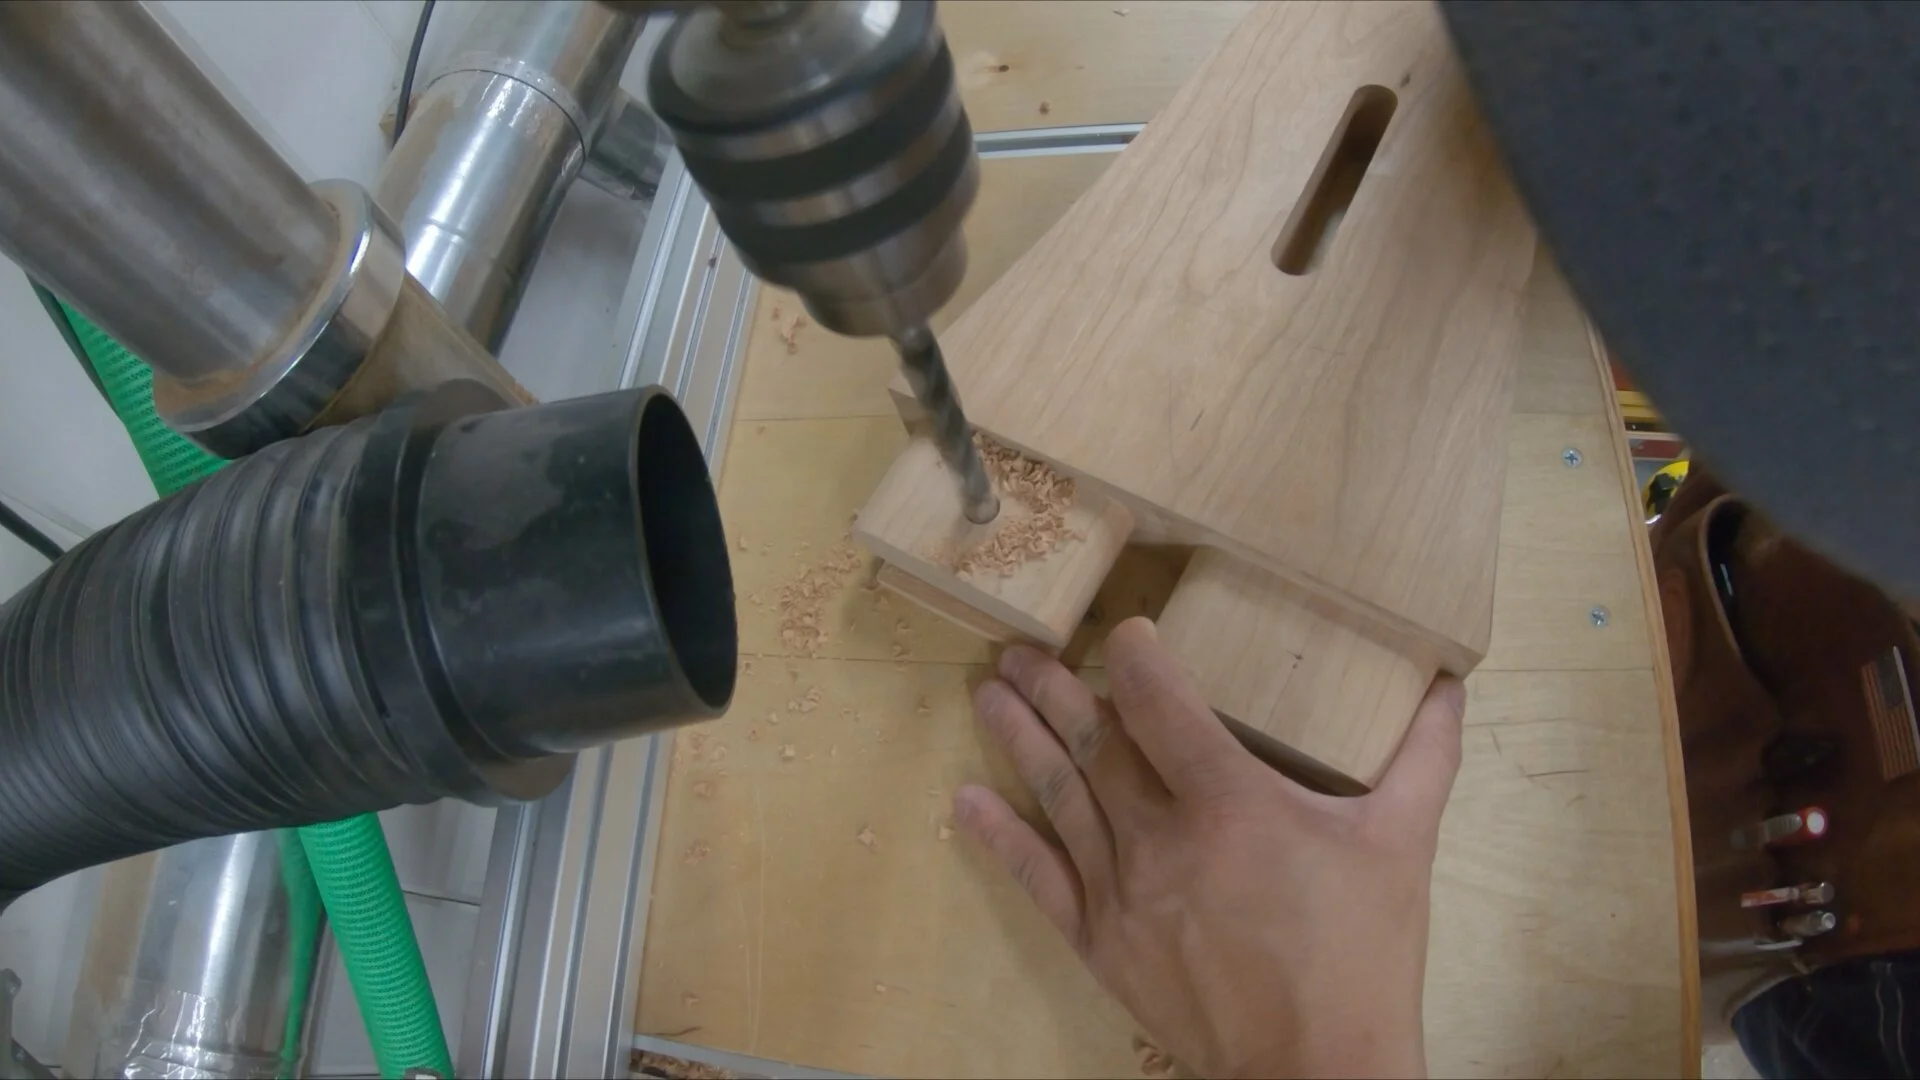
Drilling the offset hole in the tenon
Before I start glue up, I’ll taper the dowels on the disc sander
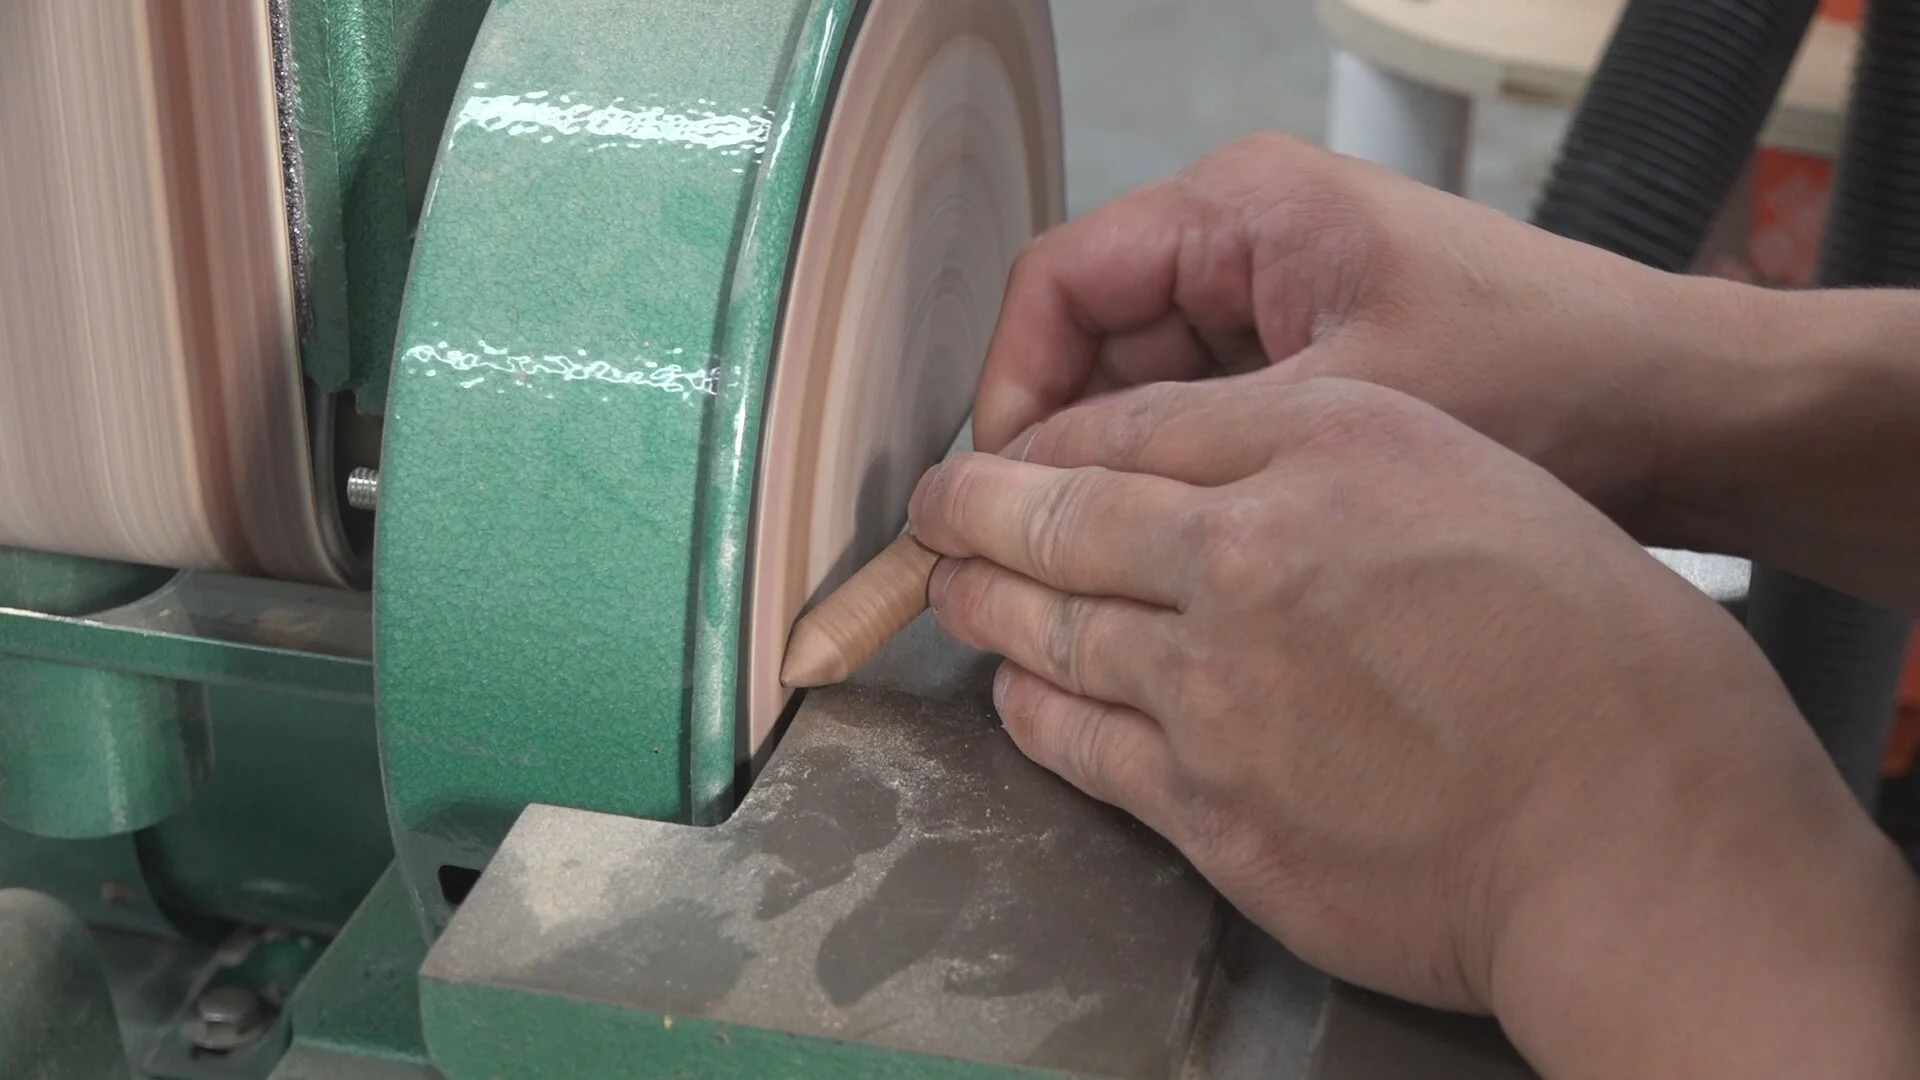
Tapering the dowels
I’ll apply glue to the mortise and tenon and clamp the joint together. I like to use Franklin Liquid Hide Glue because it helps lubricate the joint. I’ll then apply glue to the Walnut dowel and start to drive the dowel through the offset holes. This will draw the shoulder of the tenon tight against the shoulder of the mortise. Once the glue cures, I remove the clamp (honestly, I can remove the clamp before the glue cures because the dowel is holding everything tight together), flush trim the dowel, and plane everything smooth with a smoothing plane.
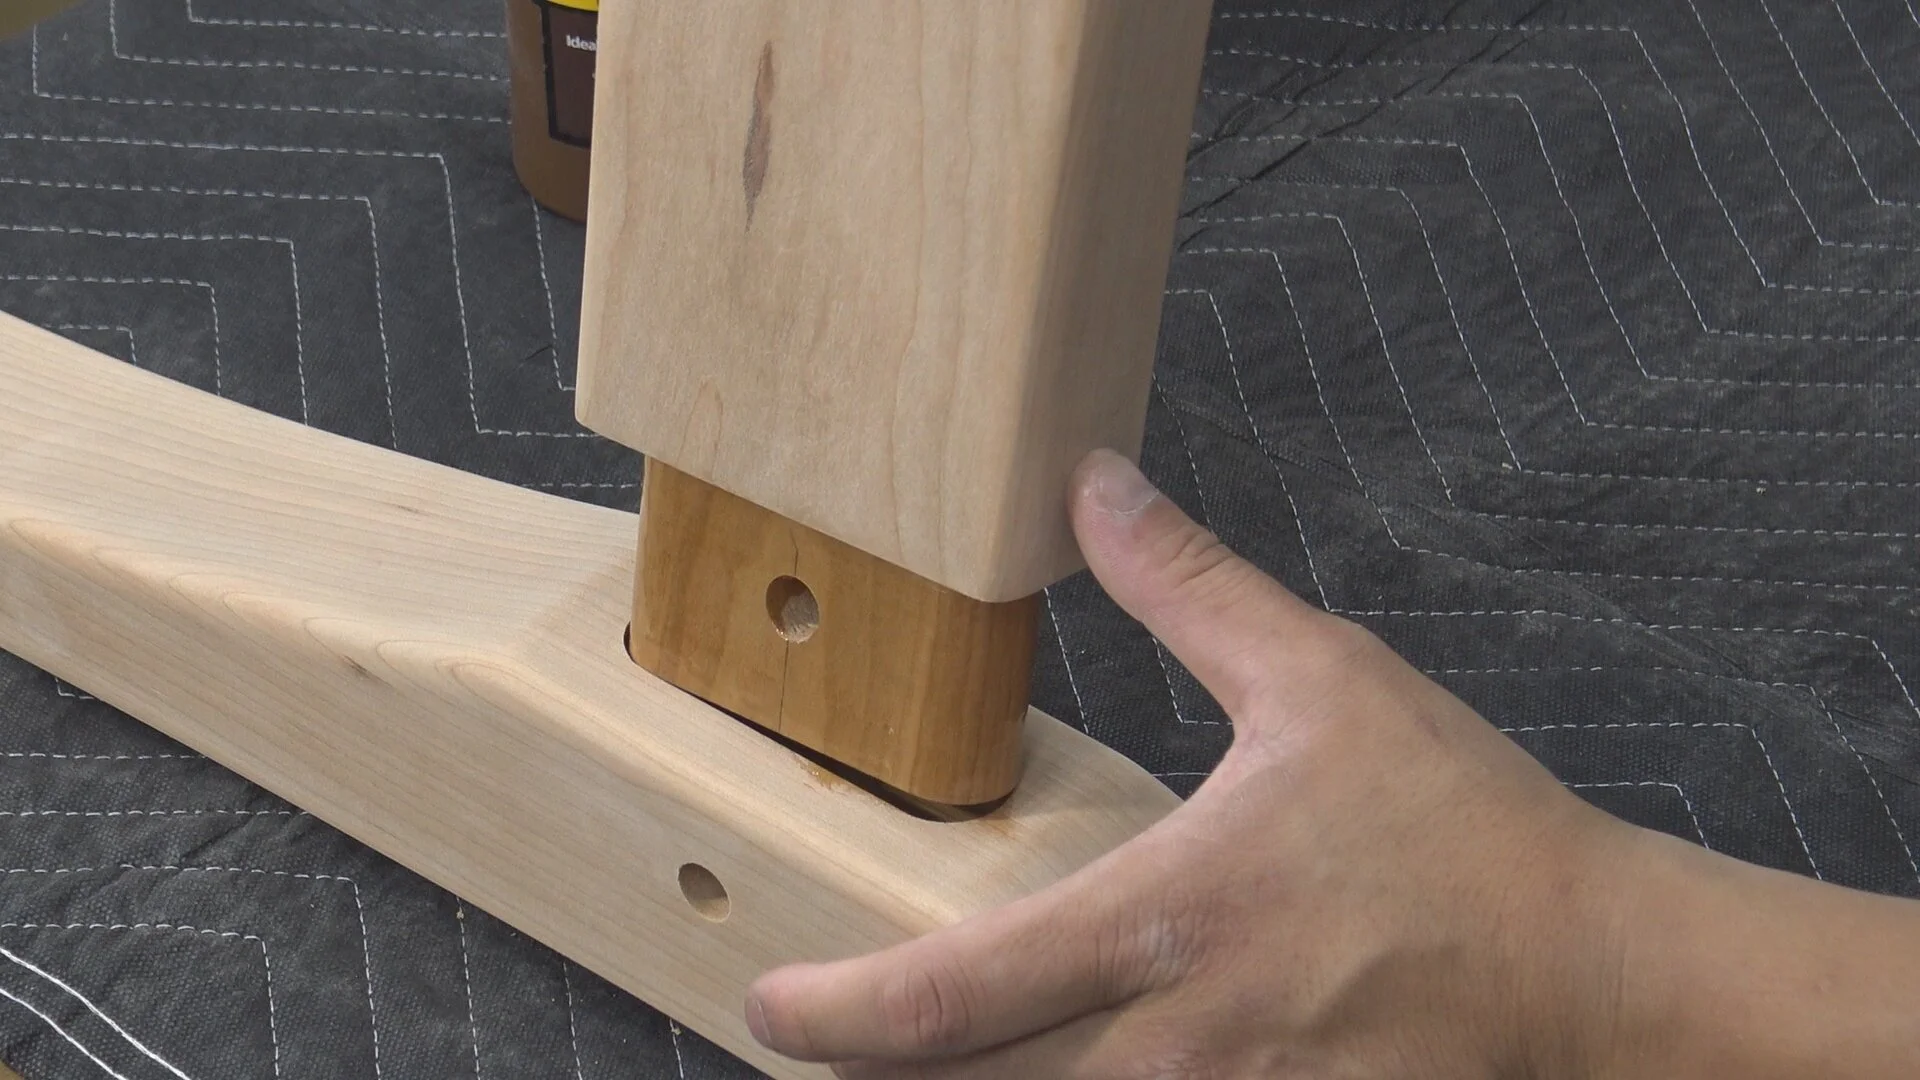
Applying liquid hide glue to the mortise and tenon
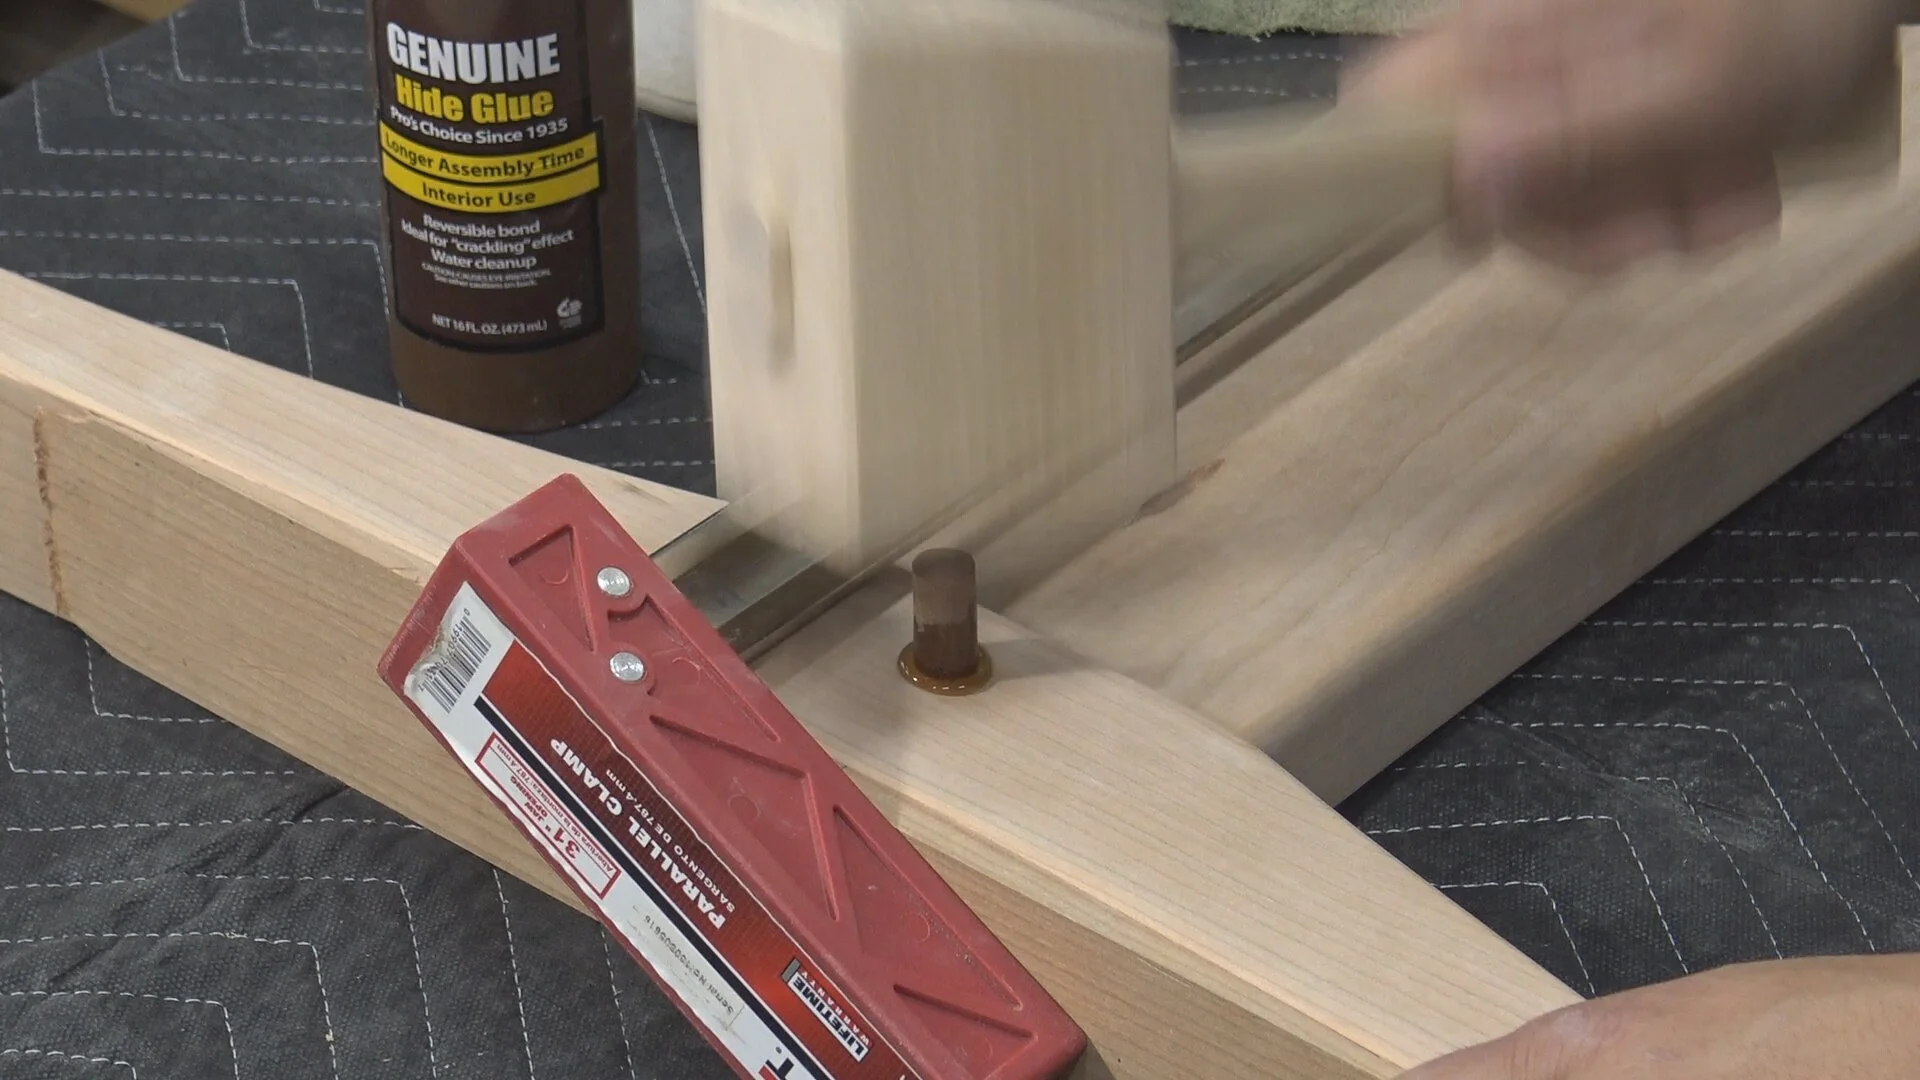
Driving the dowel through the offset holes
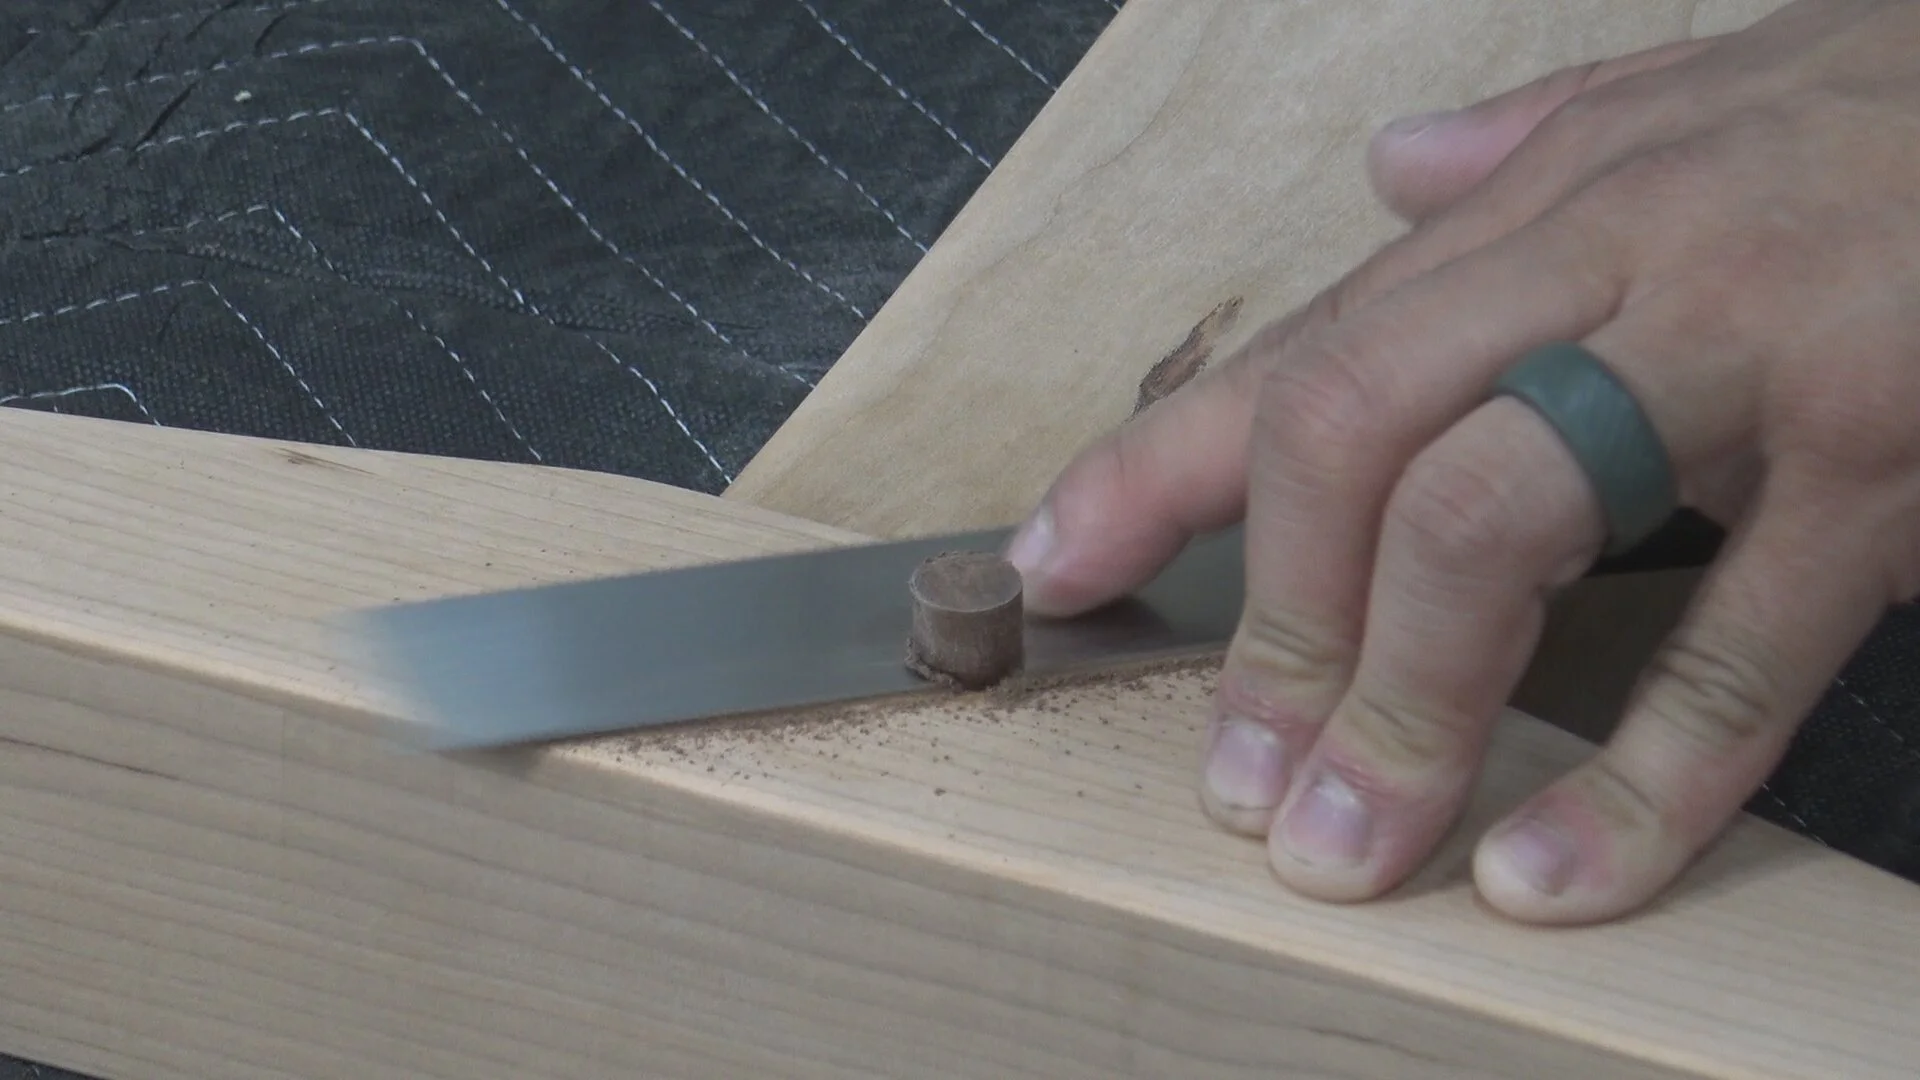
Flush trimming the dowel
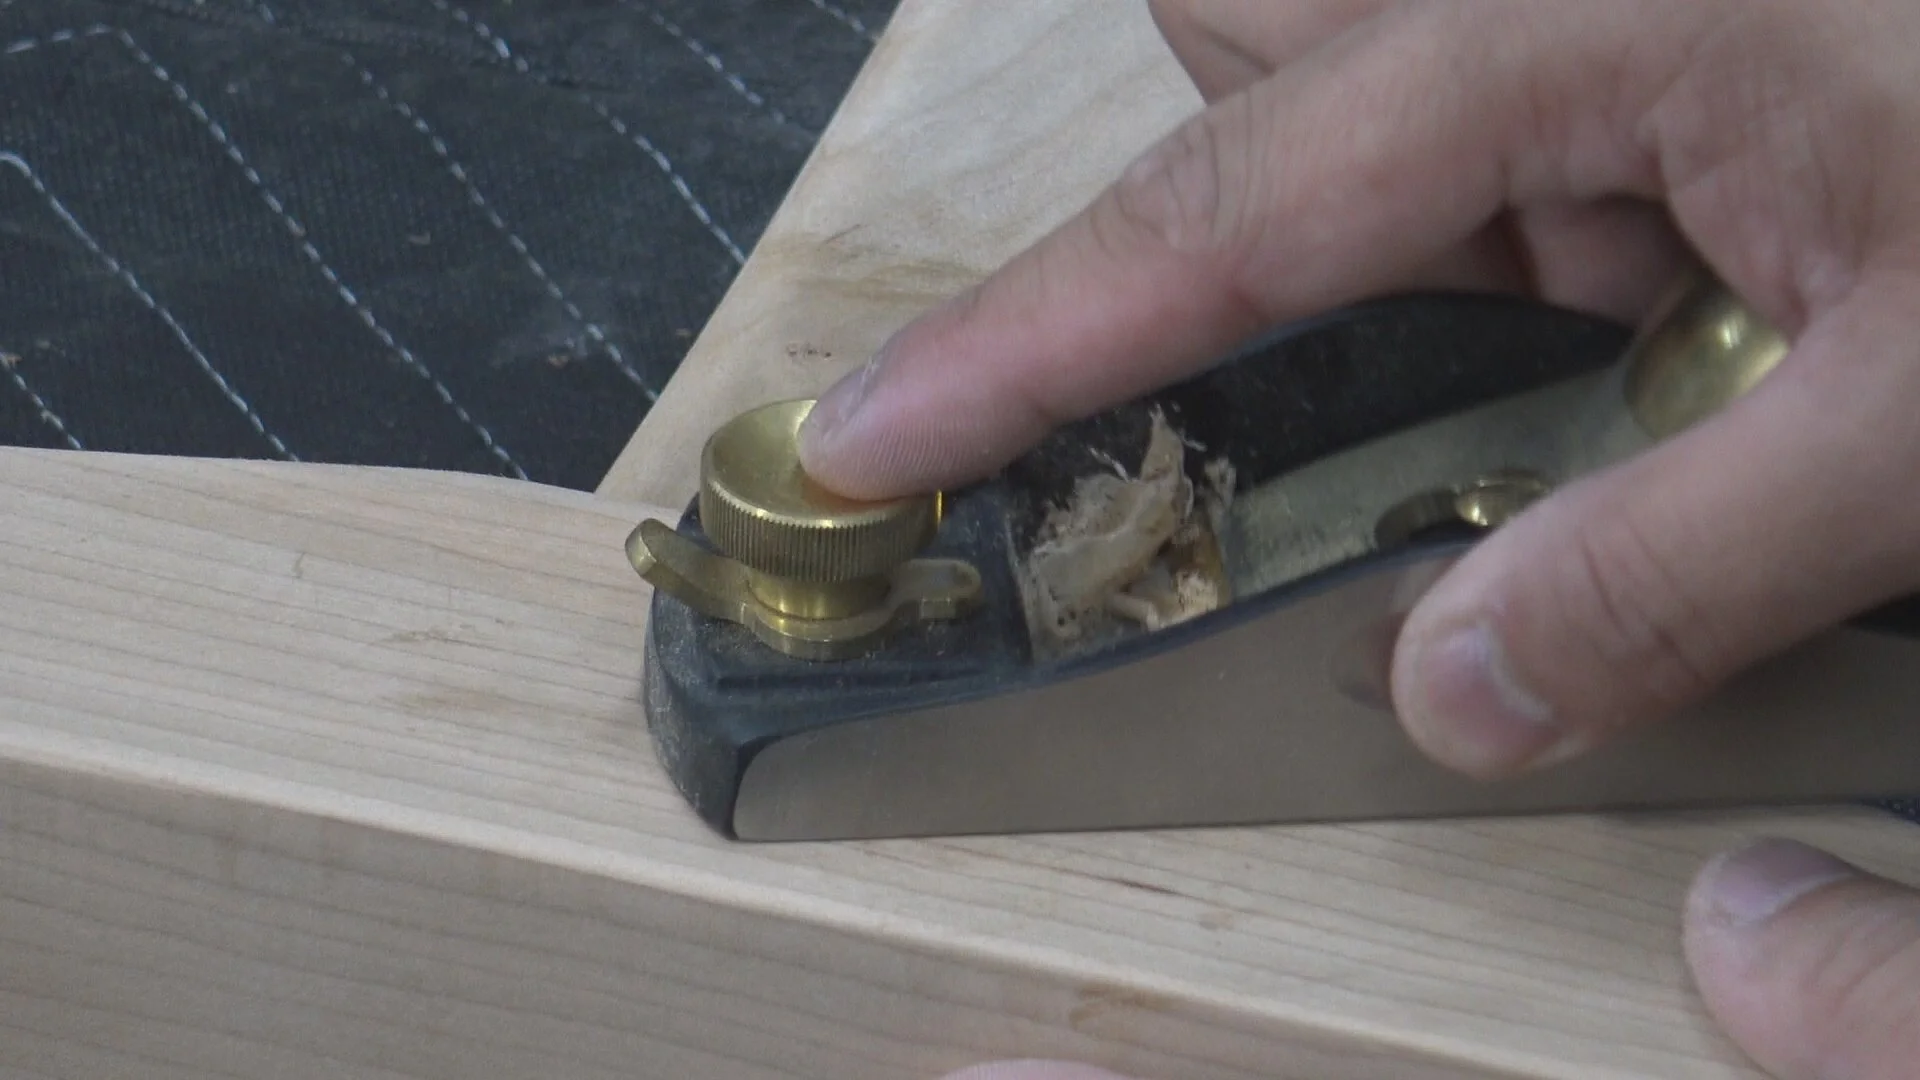
Planing everything smooth
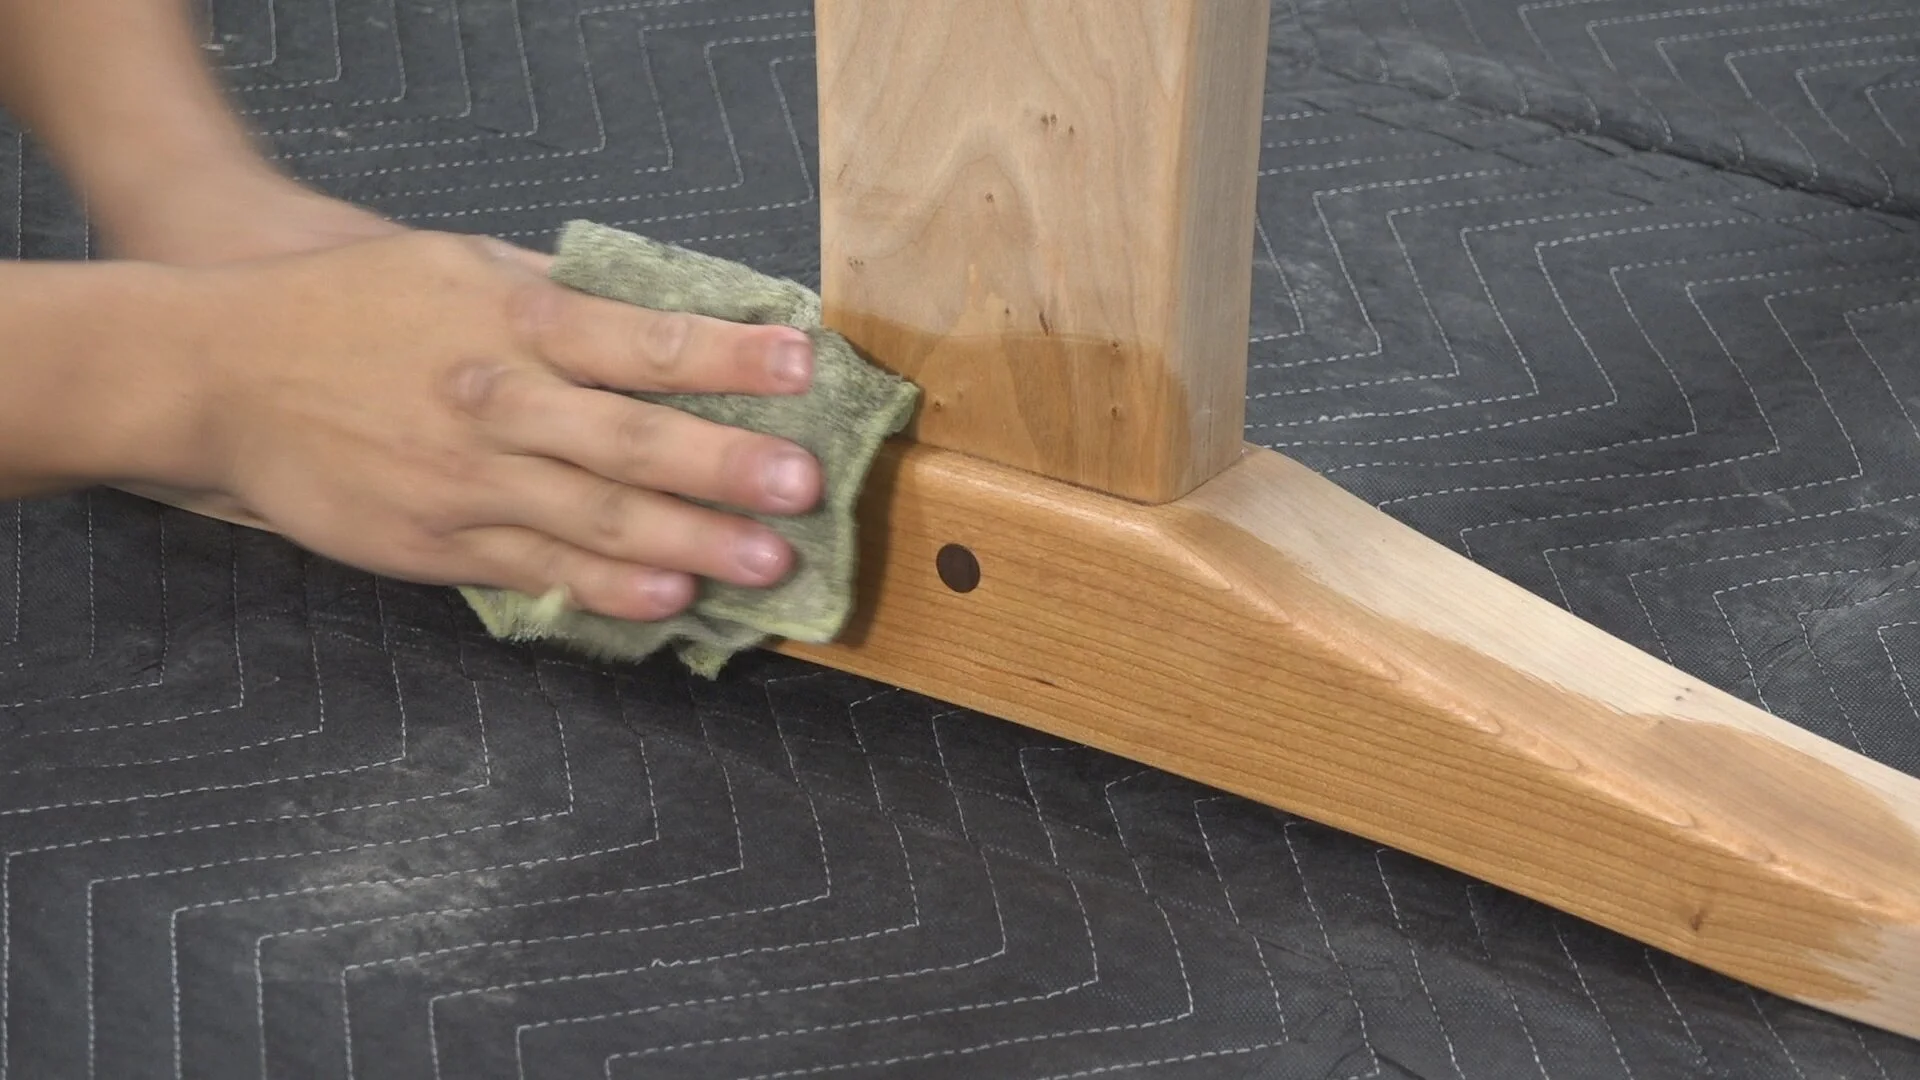
A beautiful contrast between Cherry and Walnut
Multi-Curve Edge Treatment
Using a template to create a subtle curve to the edges and parabolic curve for the edge treatment
Using a template to create a subtle curve to the edges and parabolic curve for the edge treatment
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
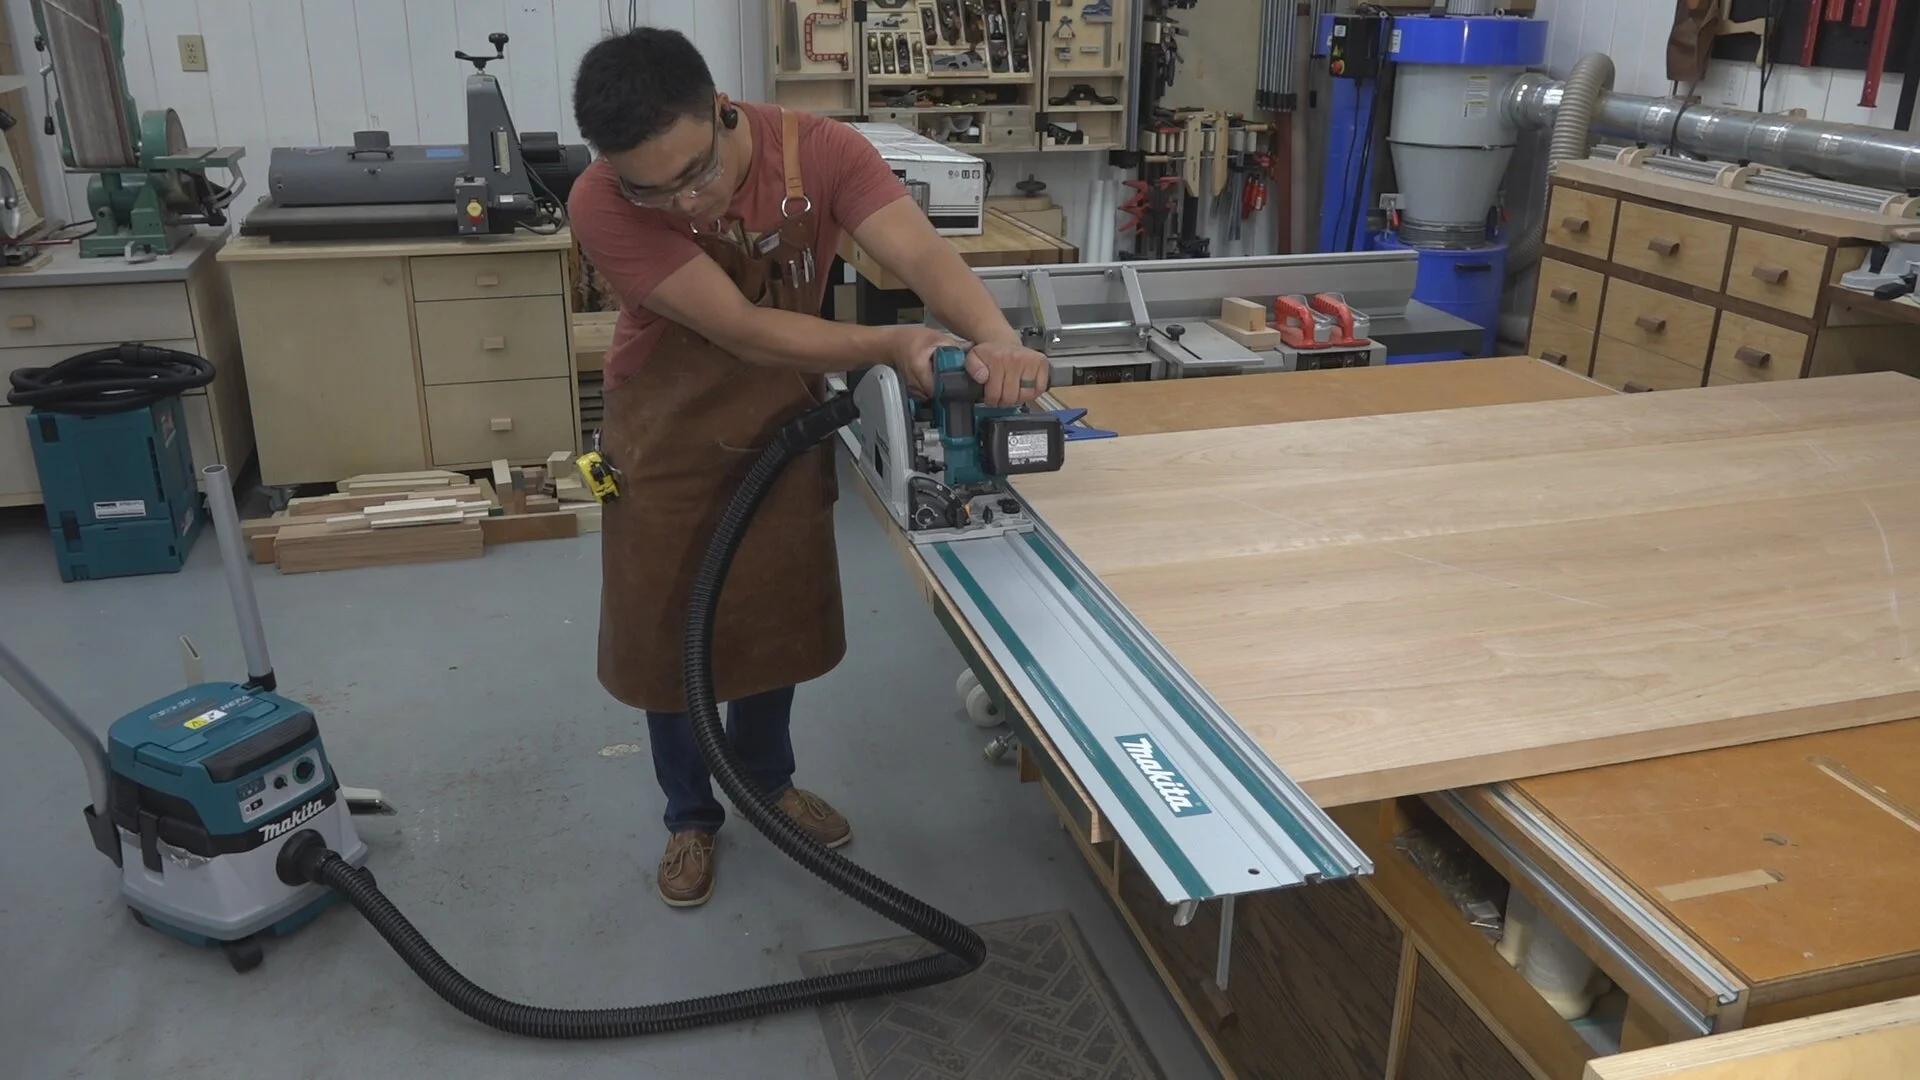
Using the Makita track saw and dust extractor to square up the table top panel
To create the multi-curve edge treatment I first needed to square up my table top panel glue up to have nice reference edges on both long and short sides. To do this I used the Makita 18-Volt X2 LXT (36-Volt) 6-1/2 in. Plunge Circular Saw with 55 in. Plunge Saw Guide Rail. A track saw is a great way to produce clean crisp edges on long panels that would otherwise be cumbersome or dangerous to do on a table saw. I also paired this with the Makita 18V X2 LXT (36V) 2.1 Gal. HEPA Filter Dry Dust Extractor for almost dust free cutting.
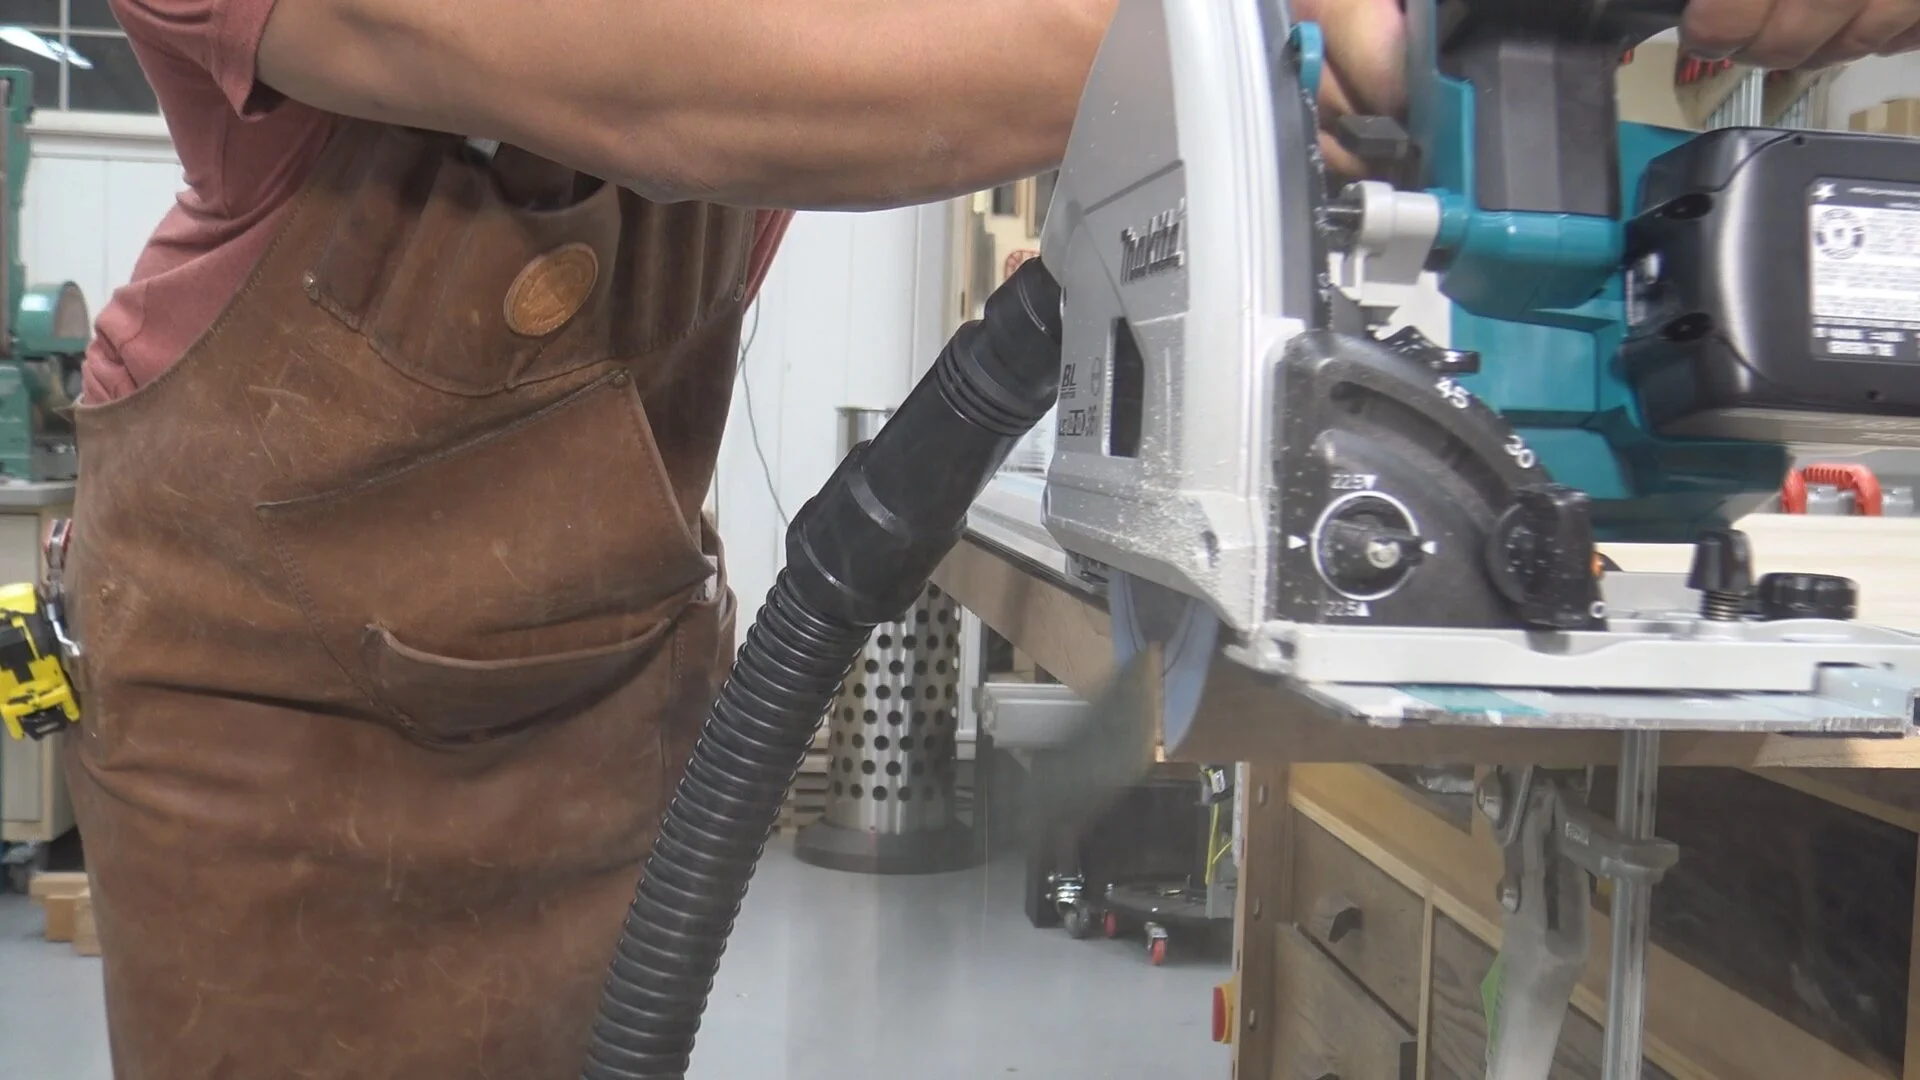
Crisp, clean, tear-out free cut with the Makita track saw
Next, I trace out the template that I made (refer to my previous blog post on how to make templates) to create the subtle curve on the squared up table top. With the template placed to the side, I’ll then rough out this shape using a jigsaw (also known as a saber saw) making sure to leave about 1/8” proud of my pencil line.
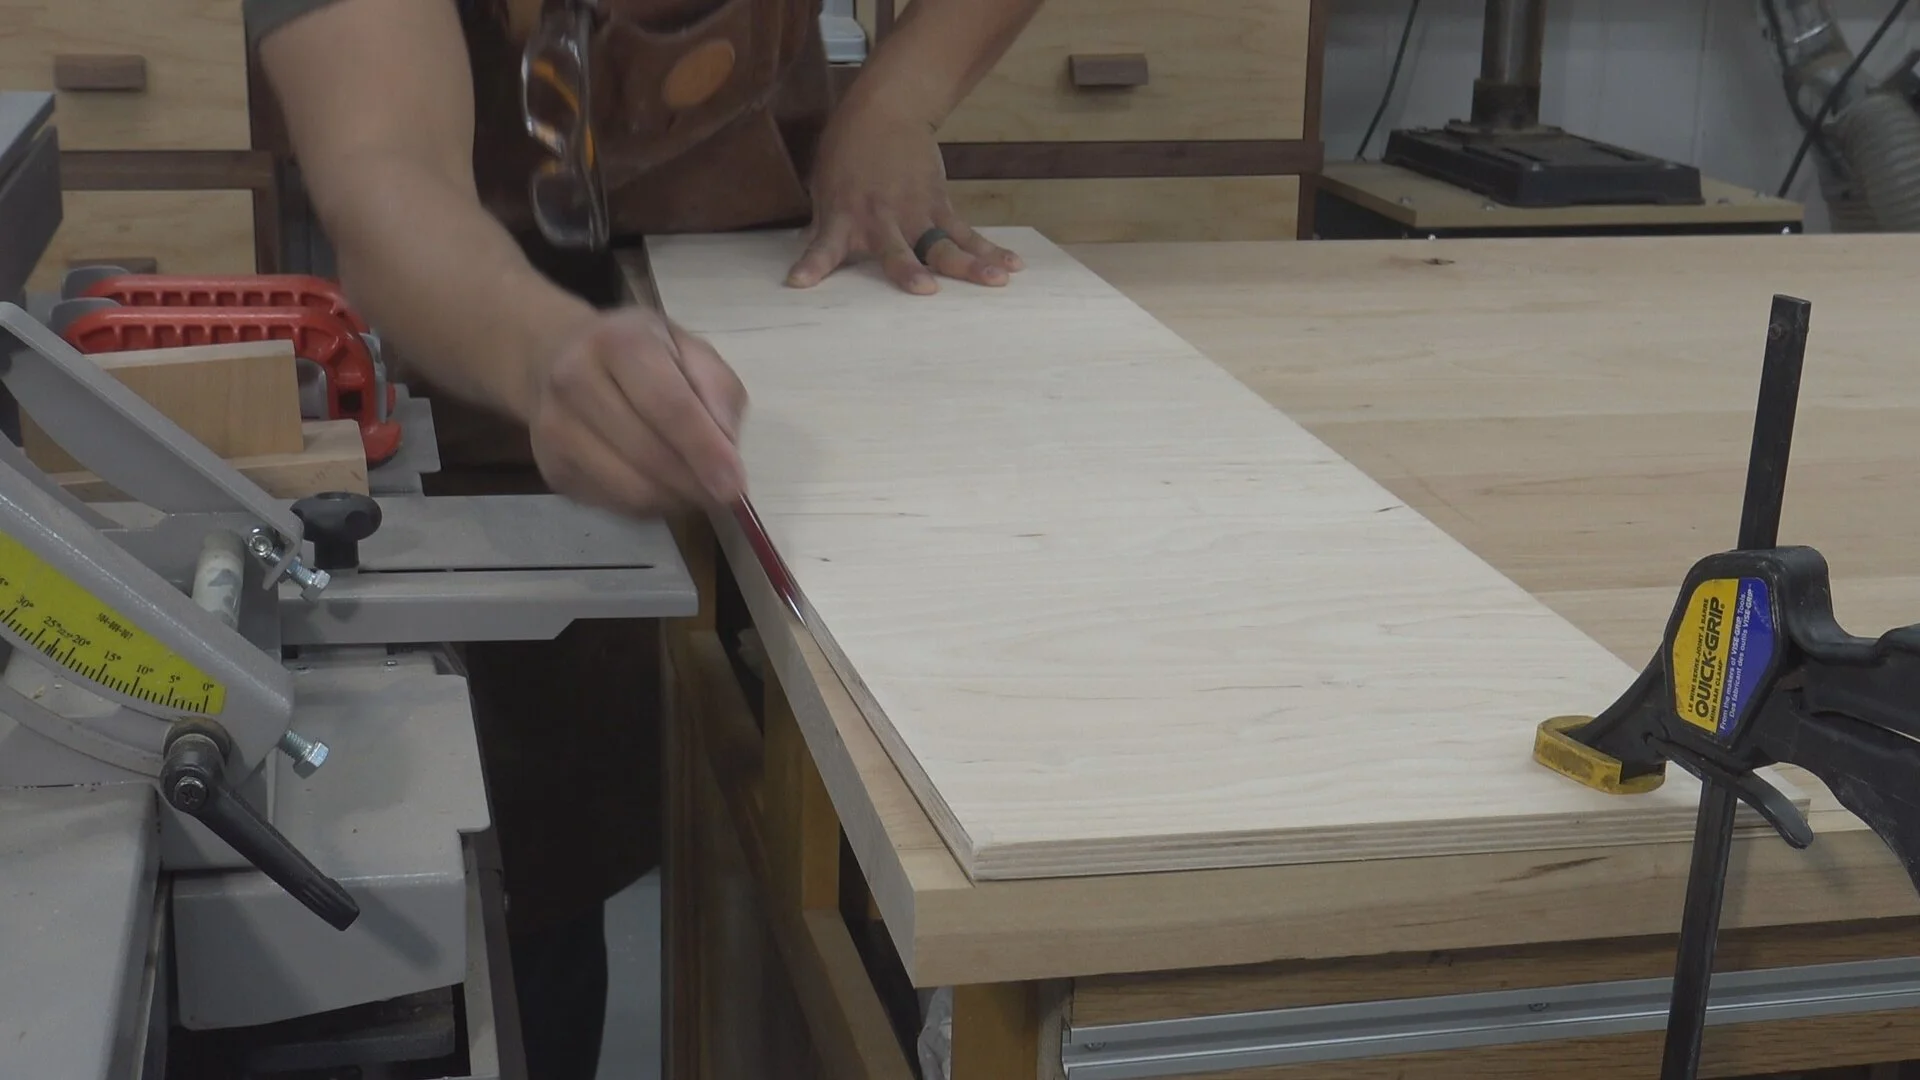
Tracing out the curve of my template onto the table top. Having square edges makes sure the template is perfectly aligned.
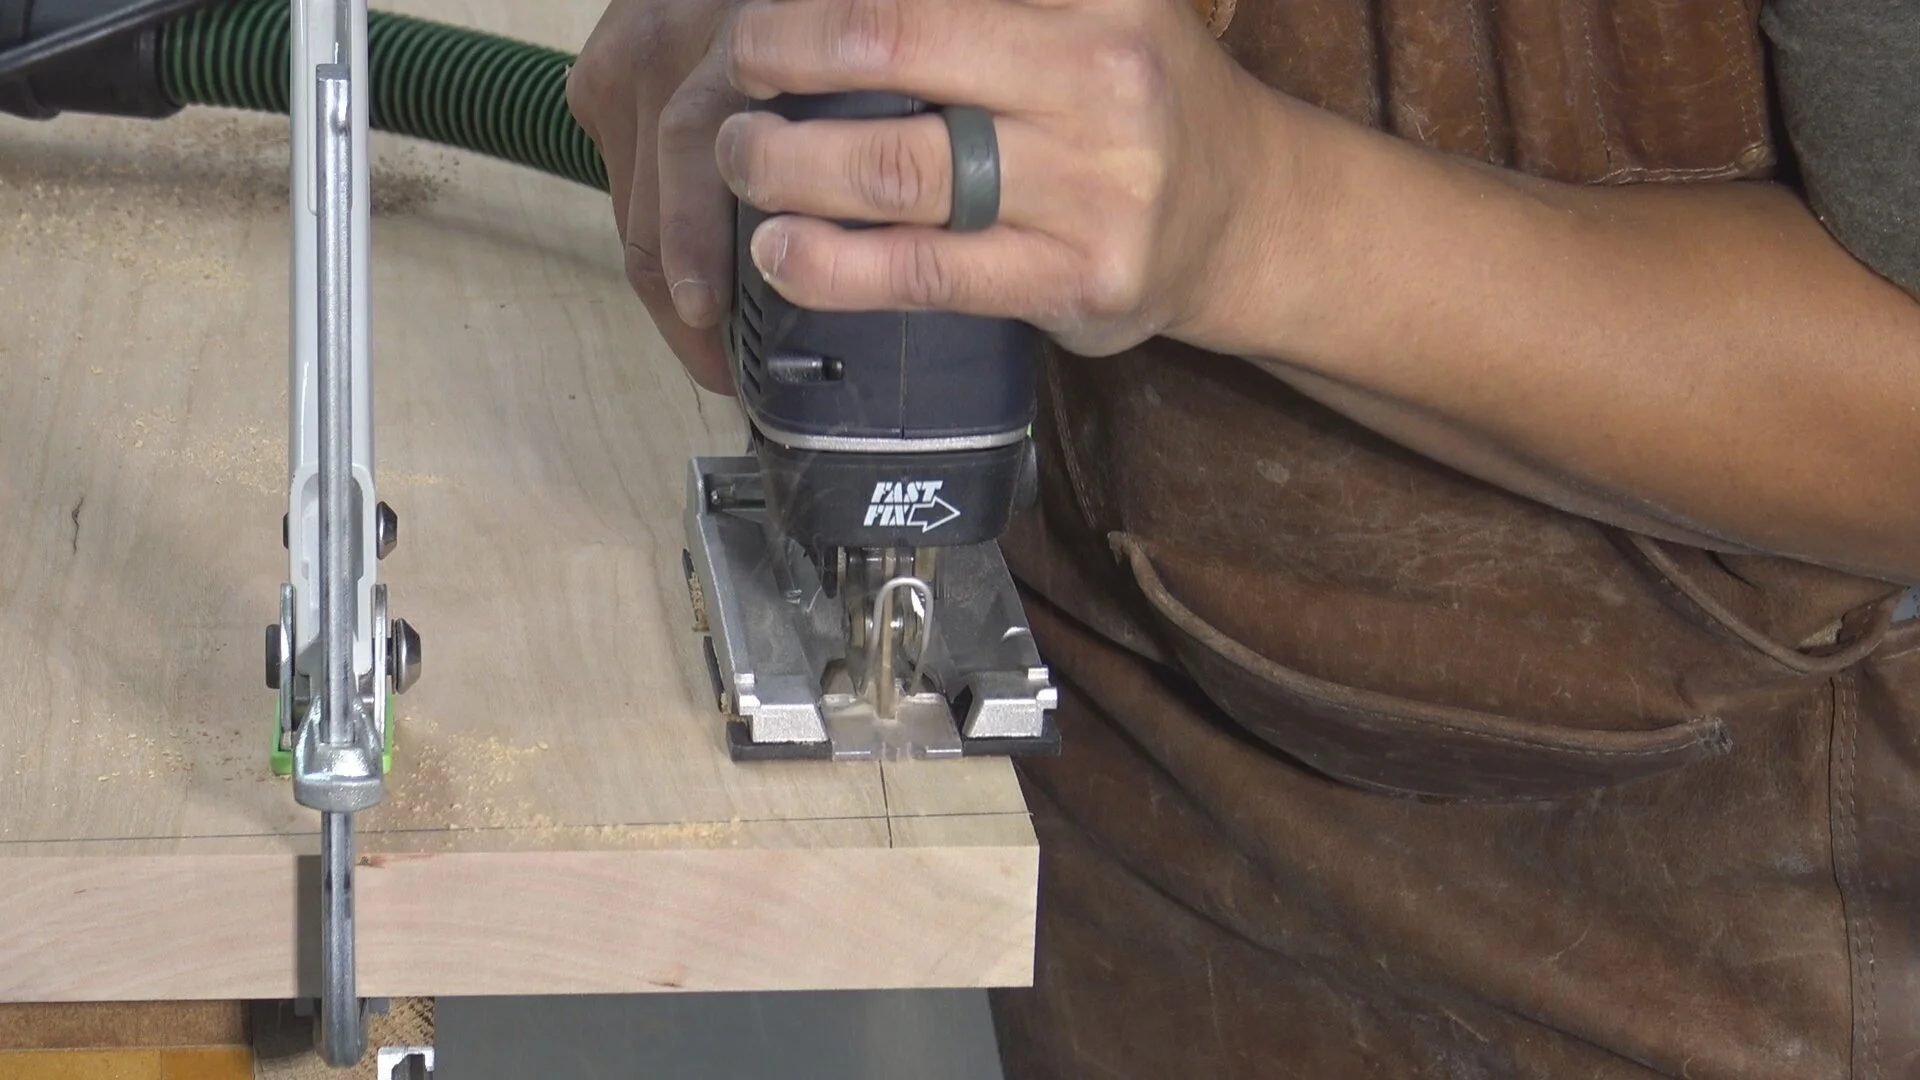
Roughing out the shape of the curve using a jigsaw
I’ll then clamp down the template making sure I’m placing the template back to the original line. To create the parabolic edge I used an oval edge router bit (Whiteside 1480) with a ball bearing (Whiteside B16) and lock collar (Whiteside LC-1/2). The bearing will ride along the template as a guide and the router bit is offset to give the edge a parabolic shape as opposed to an even round-over.
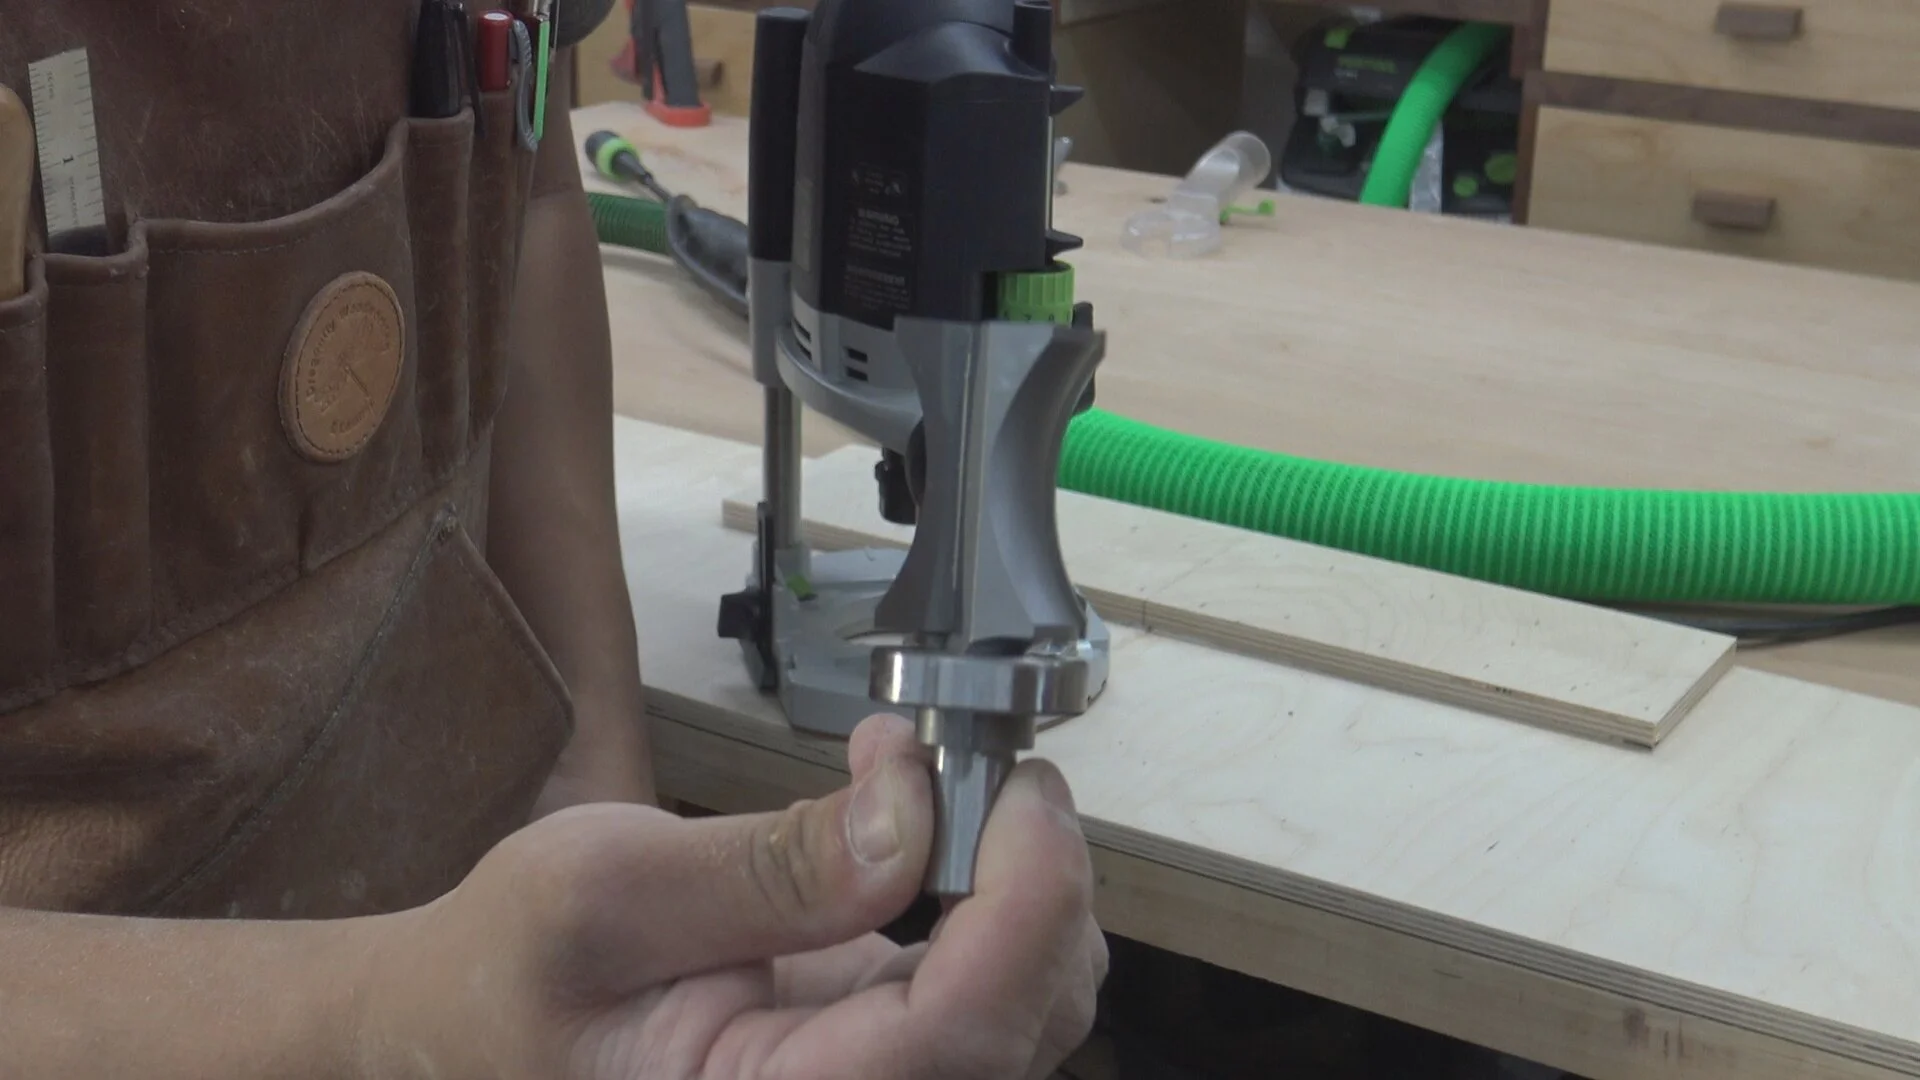
Whiteside 1480 with a B16 ball bearing and LC-1/2 lock collar
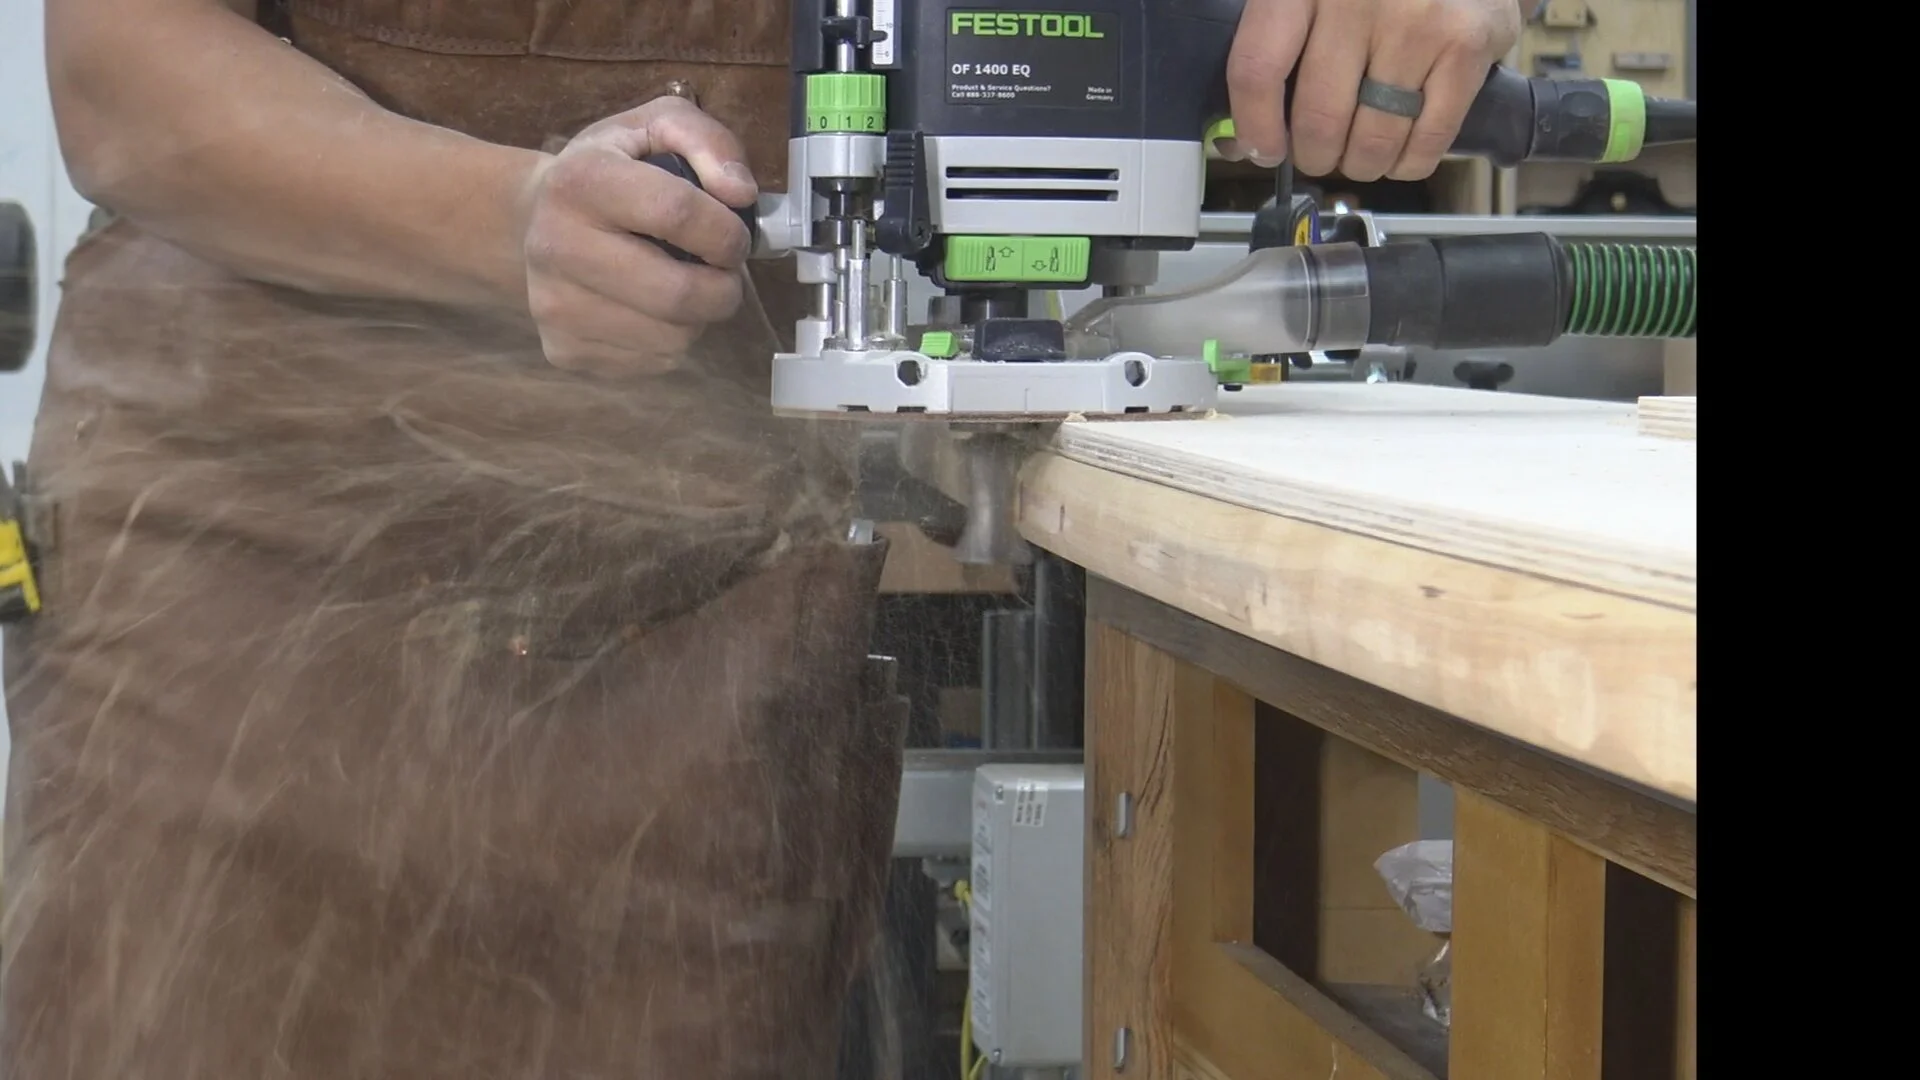
Using the template as a guide for the router bit
Lastly, I use a spokeshave and sandpaper with a flexible backer to ease the sharp edges.
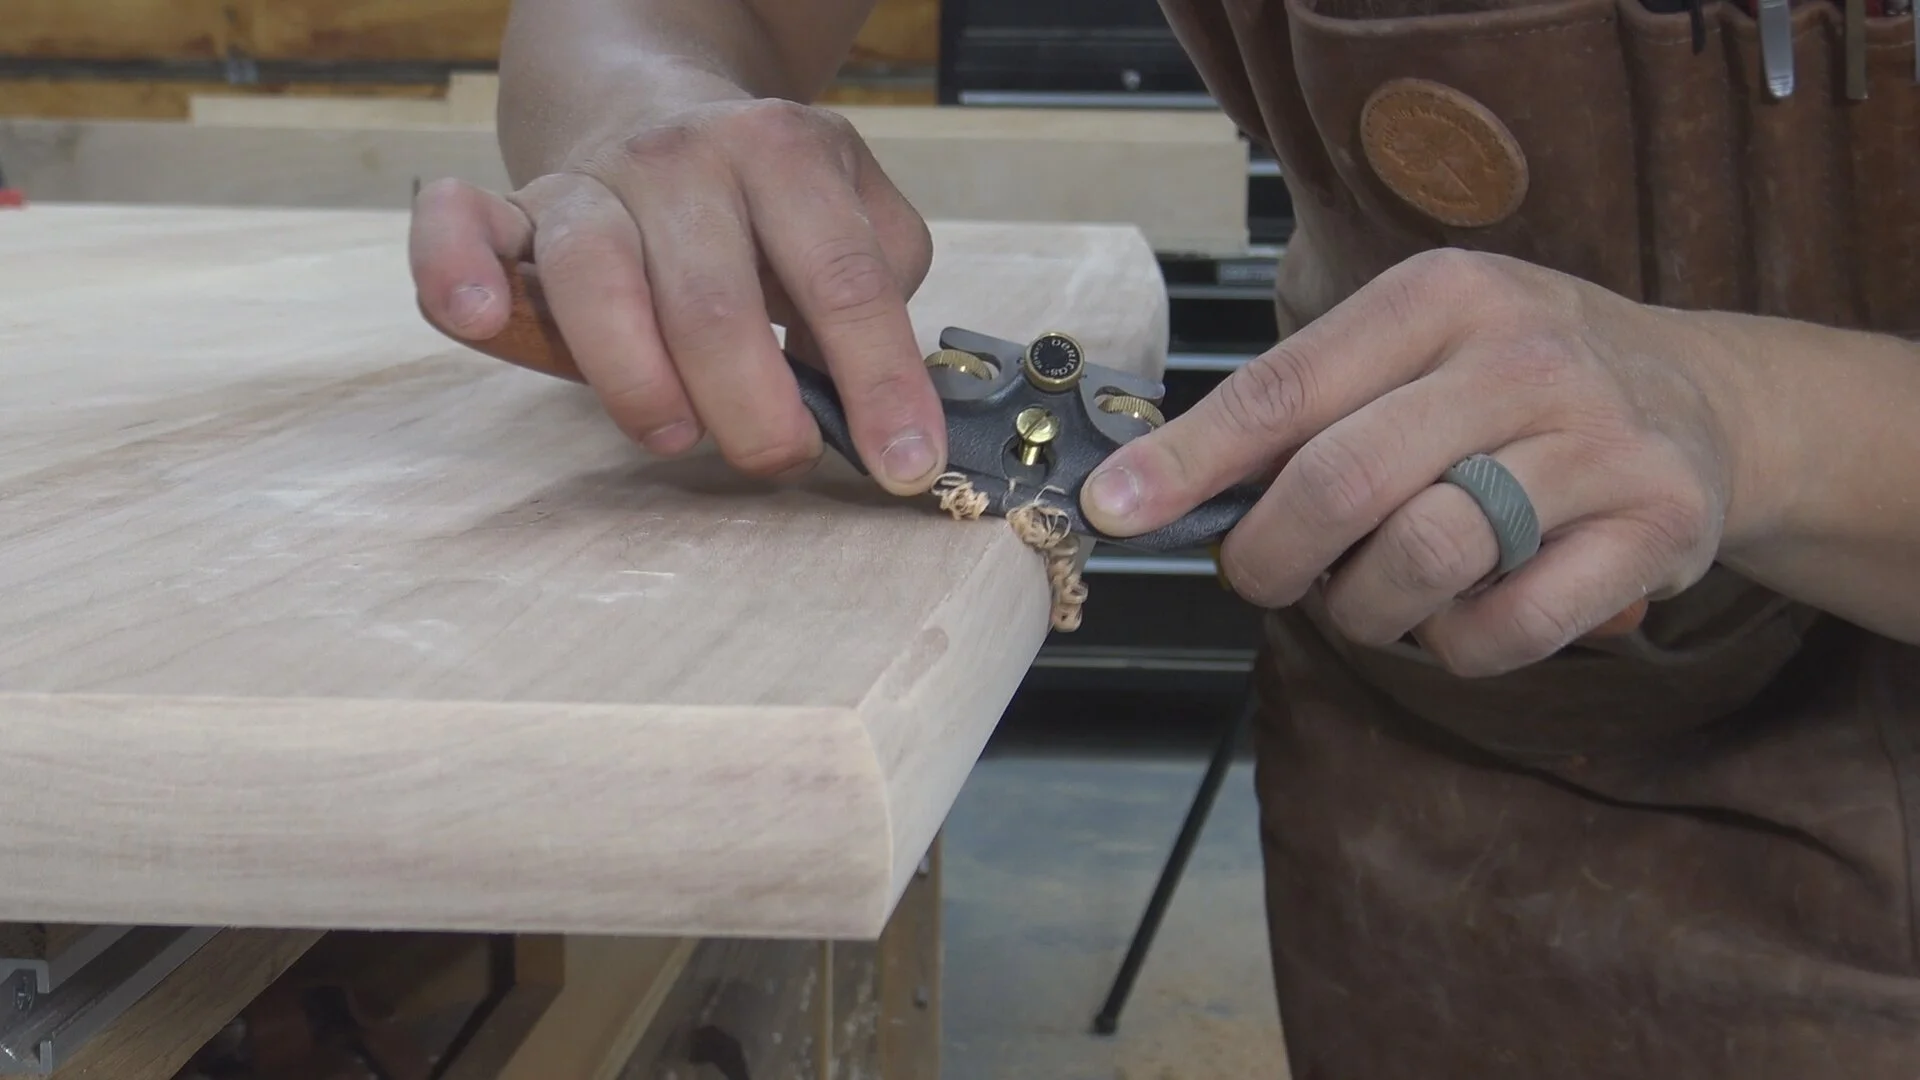
Spokeshave quickly removes the sharp edges
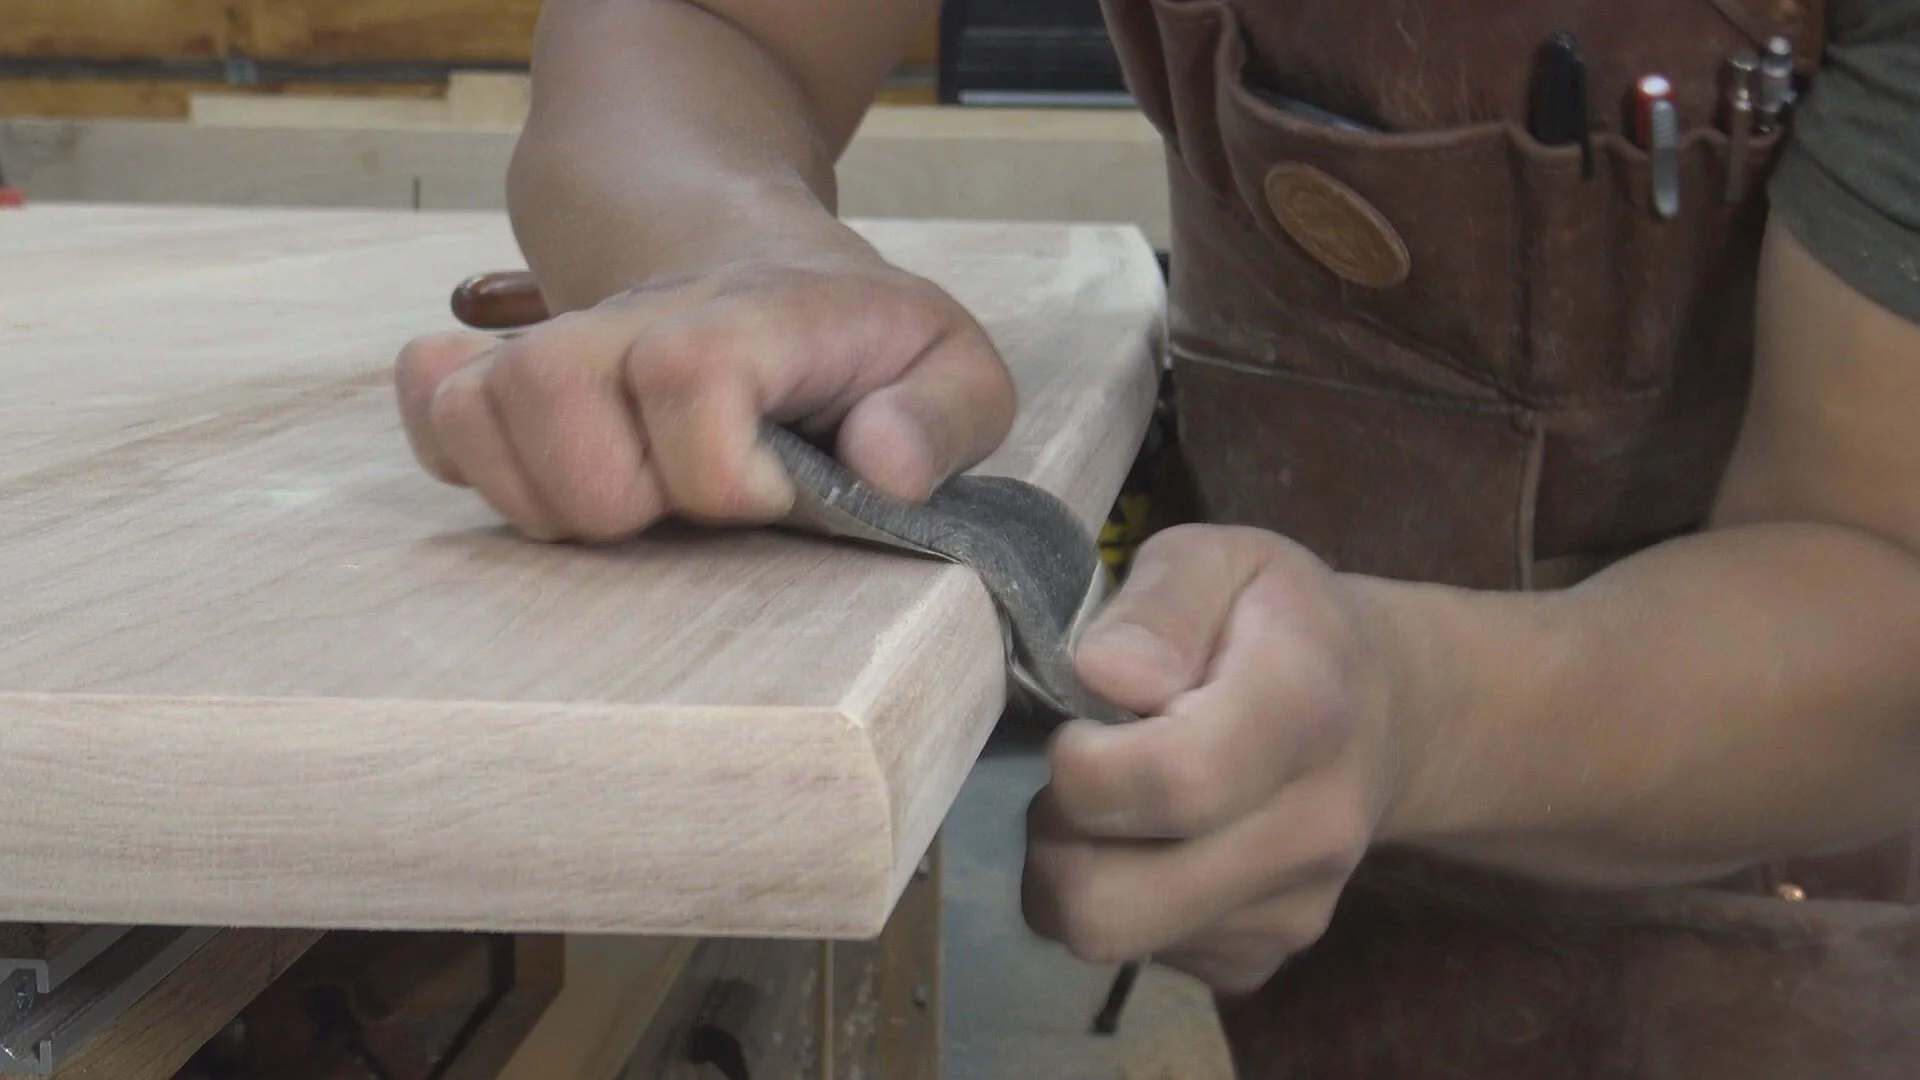
Sandpaper with a flexible backer smooths the edges
Repairing Exposed Tenons
I was at the router table pattern routing the stretcher to a trestle table I was making. I’ve done this type of operation hundreds of times. It simple! Make sure you take off as much material off at the bandsaw as possible and you’ll get a nice smooth surface on the router table with a good sharp pattern routing bit. Then I got over confident and that’s when you make mistakes. Thankfully, I was able to correct that mistake using some clever techniques.
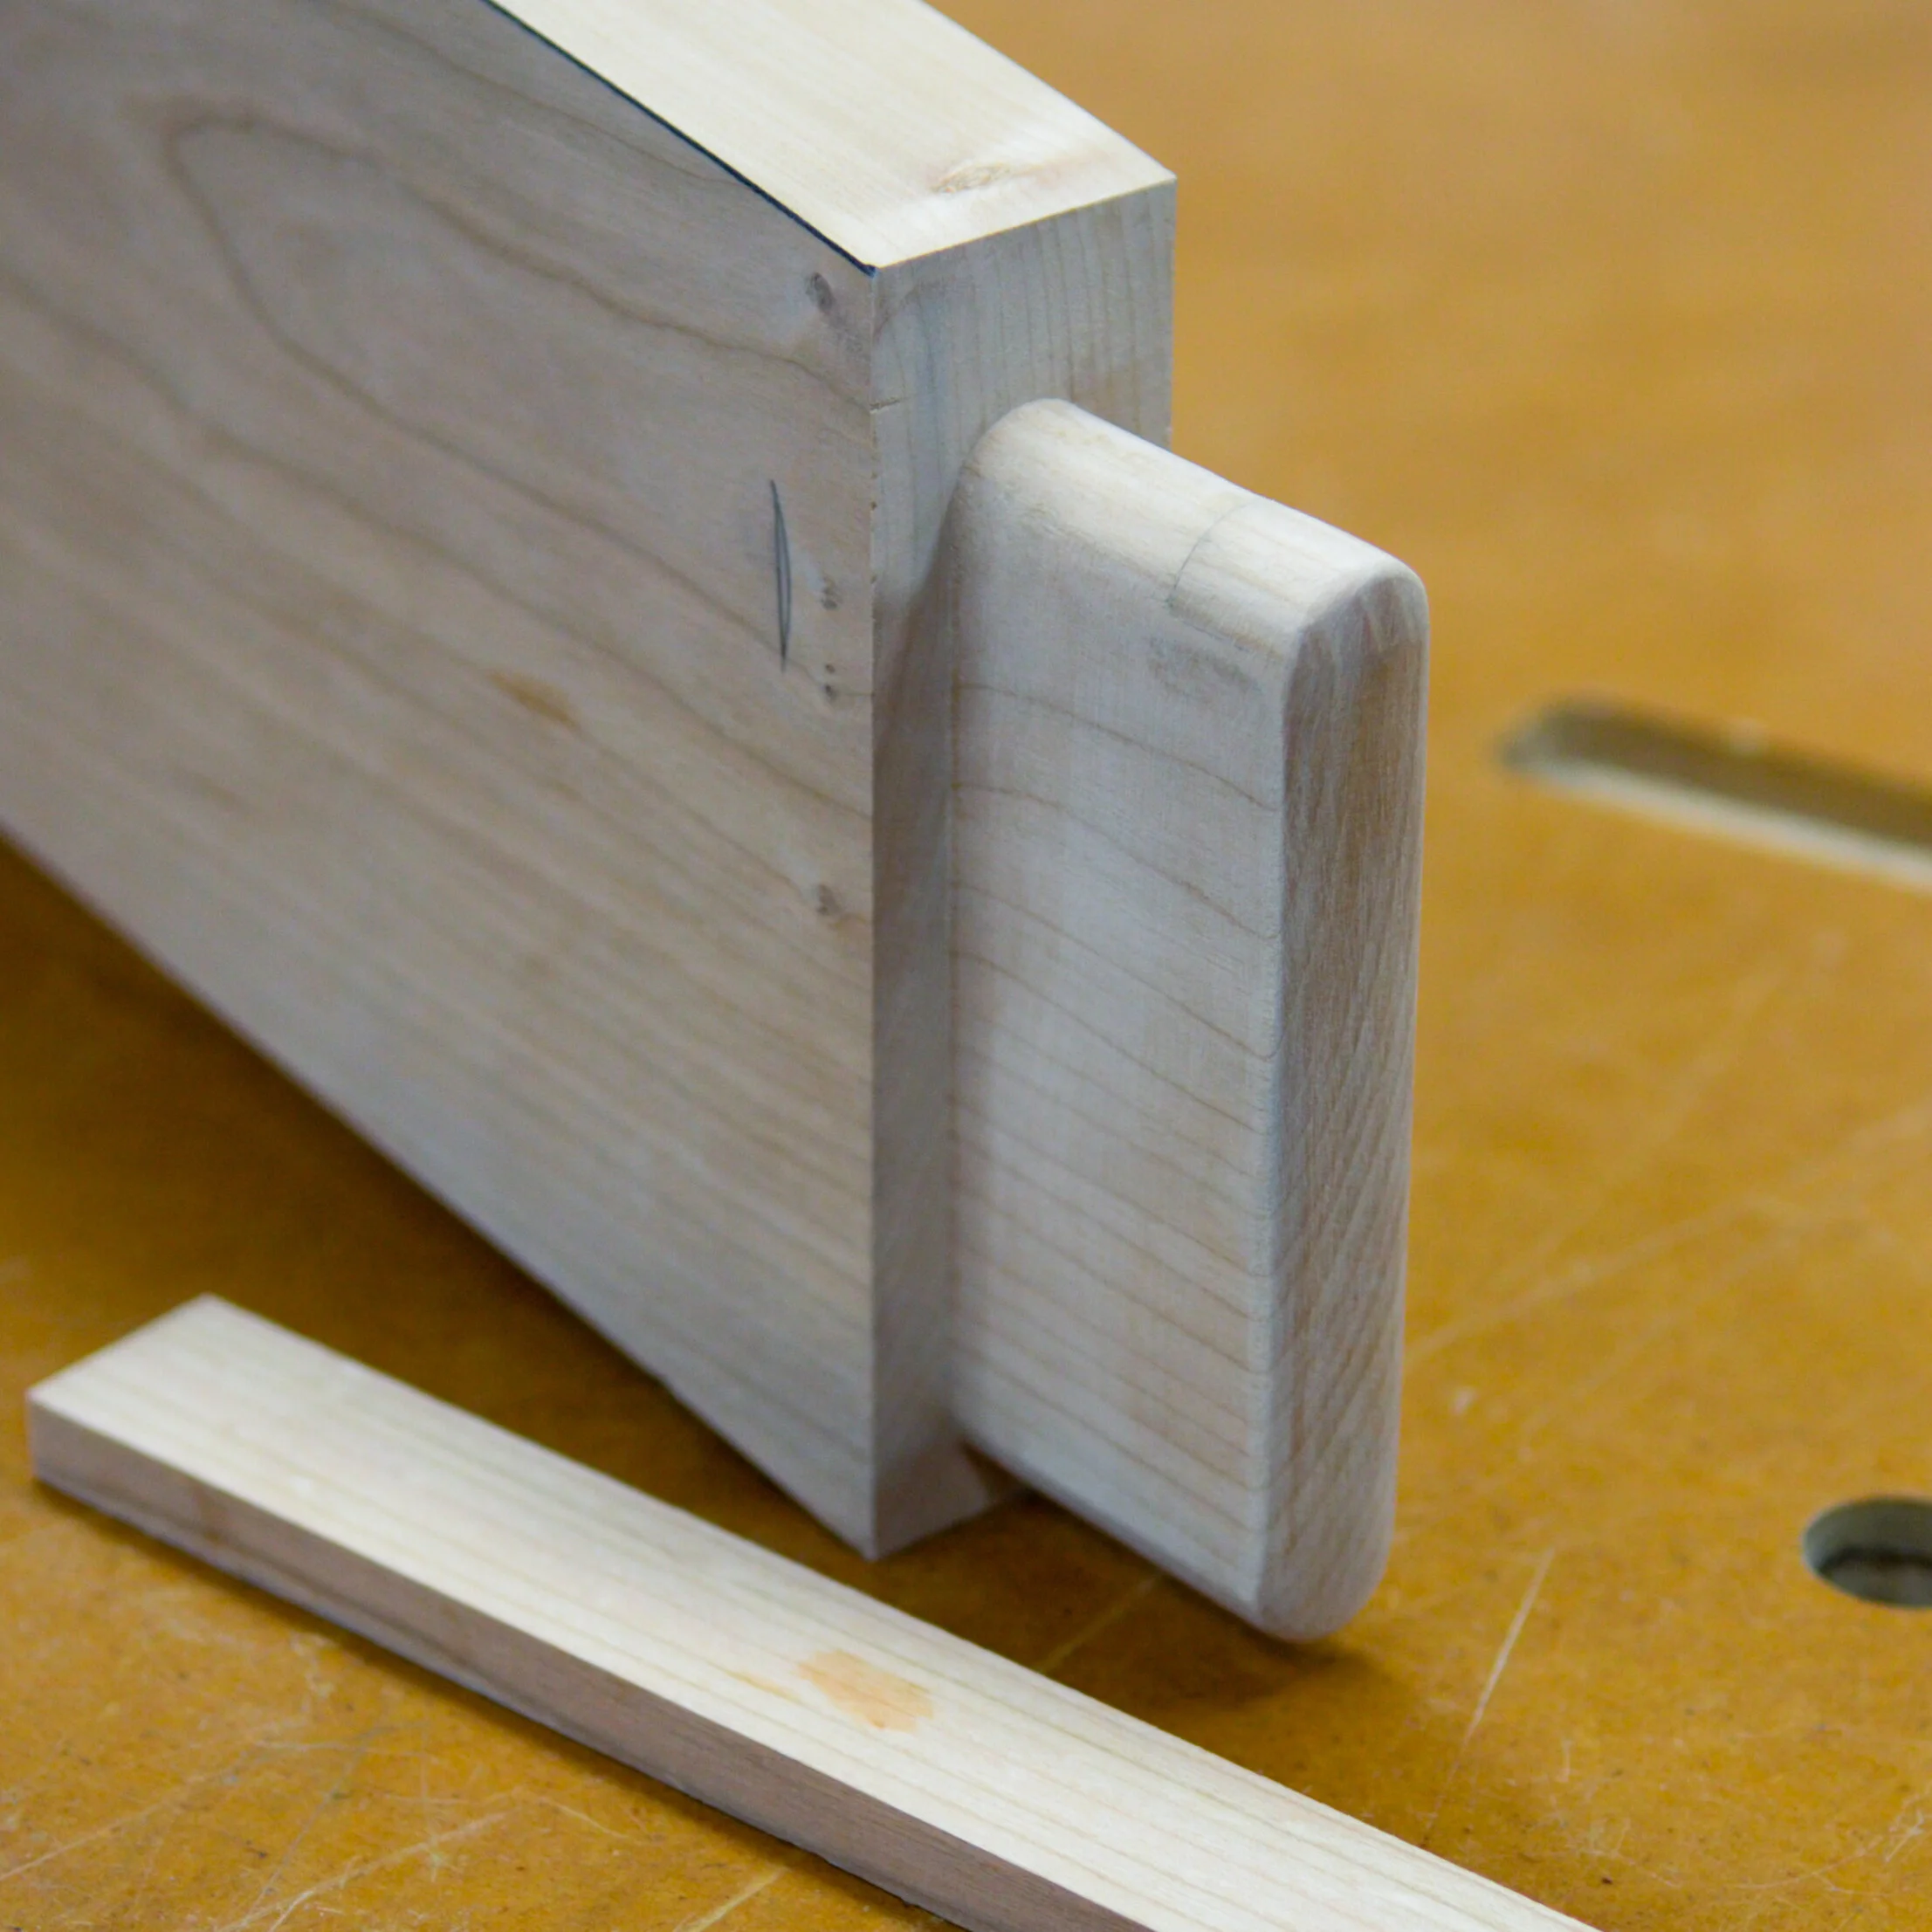
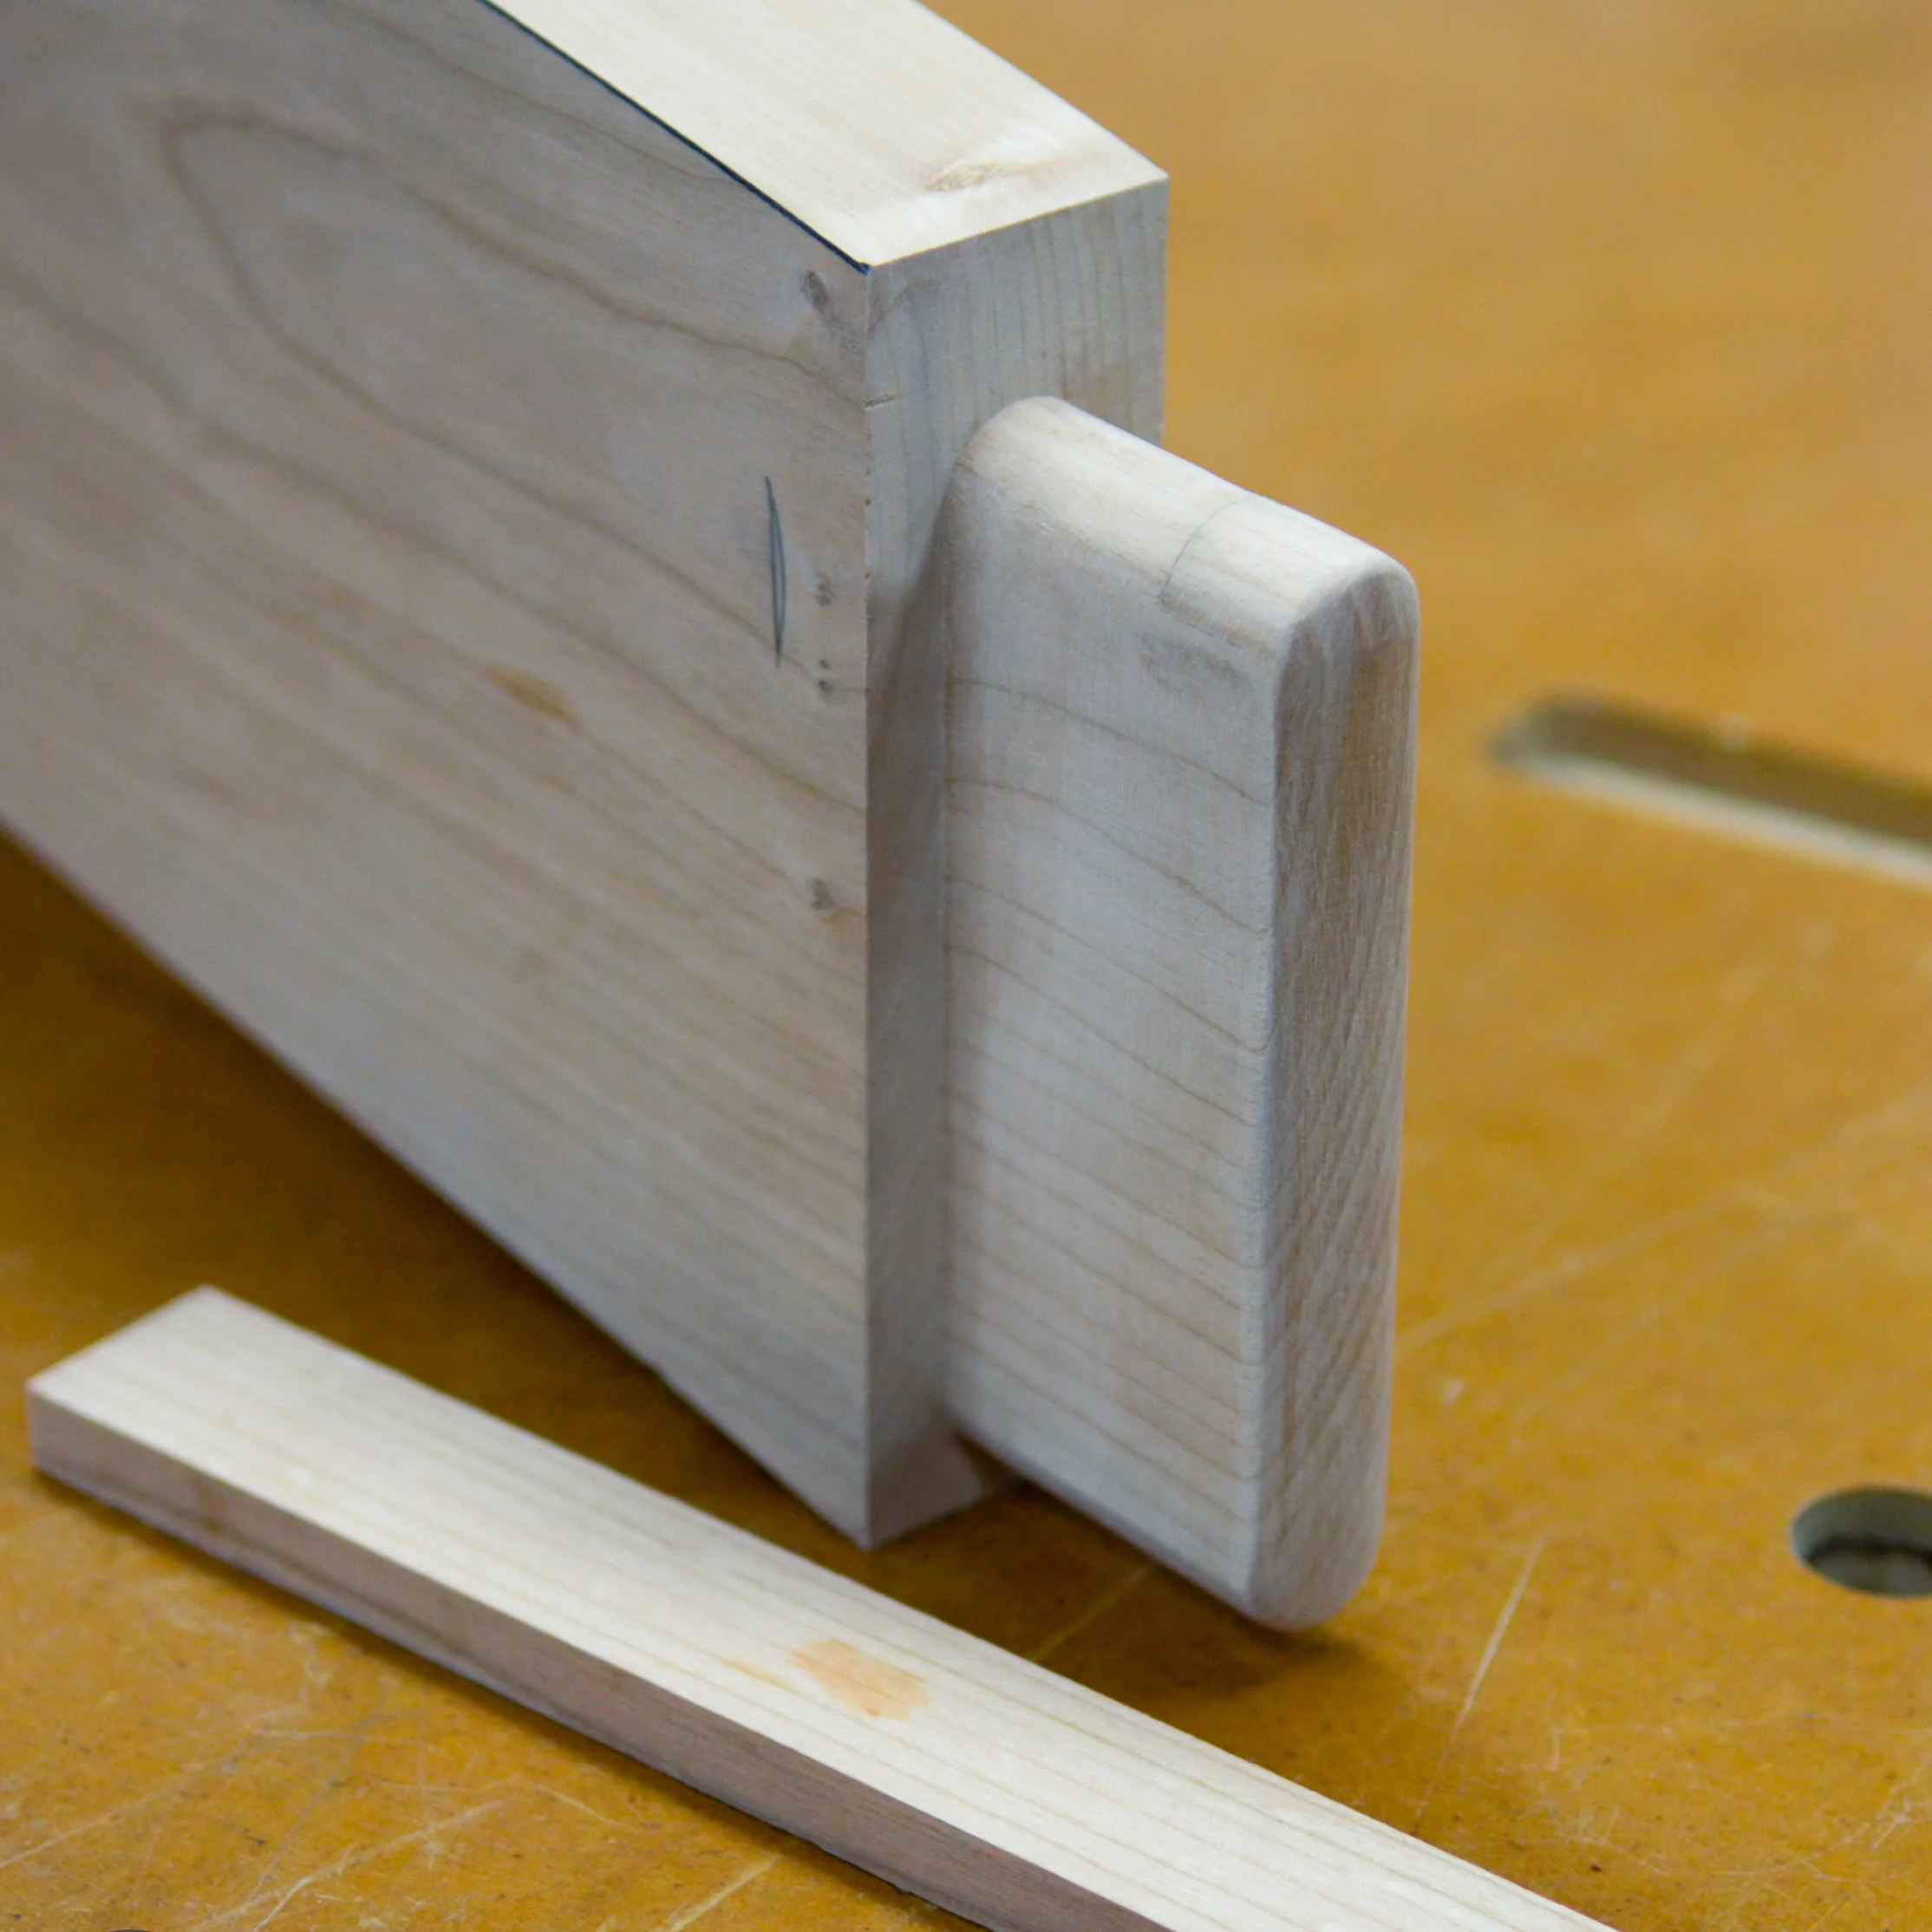
A repair tenon that was gouged by a router bit
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
I was at the router table pattern routing the stretcher to a trestle table I was making. I’ve done this type of operation hundreds of times. It simple! Make sure you take off as much material off at the bandsaw as possible and you’ll get a nice smooth surface on the router table with a good sharp pattern routing bit. Then I got over confident and that’s when you make mistakes. Thankfully, I was able to correct that mistake using some clever techniques.
As I was pattern routing, I forgot to slow down towards the end make sure I did push my exposed tenon on the end of the stretcher into the router bit. Well, I got a little too zealous and BOOM! The tenon nicked the router bit and tenon shards went flying. I was in a panic. Literally sweating and almost sick to my stomach. I’ve already done so much work with the joinery and shaping that I’d literally be adding 3-4 hours to my build.
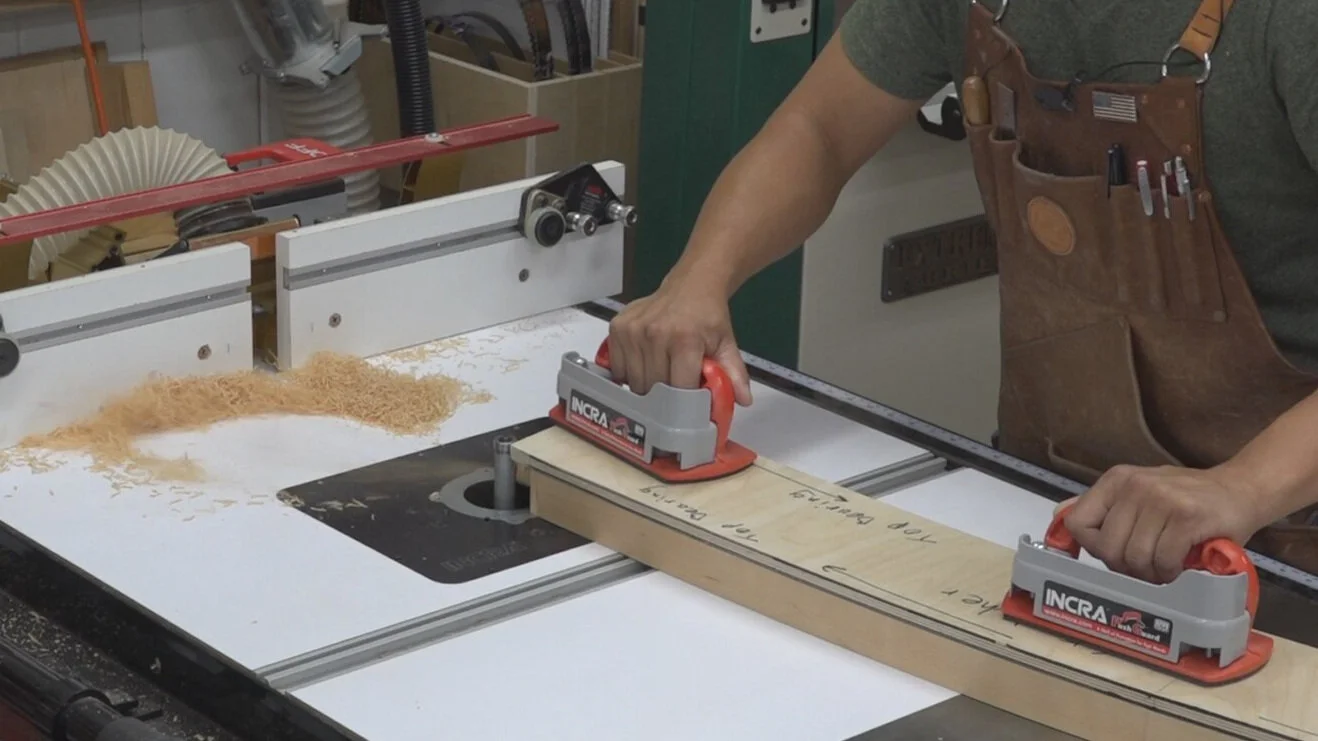
The end of the exposed tenon on the trestle table stretcher hitting the router bit
After I cooled down, I thought about how I could patch up this mistake. In cases where the tenon is concealed, this wouldn’t matter too much. However, the rounded exposed tenons are a design element to this trestle table and required that the tenon look flawless.
The first thing I did was cut the marred portion of the tenon out. That’s right, I cut out even more of the tenon to make sure the defect was perfectly plumb and square. I used a Japanese pull saw to do this. Unfortunately, I was in such a frenzy that I didn’t record myself doing this. I then find matching material. I wanted the end grain to be in the same orientation as the tenon. I cut the wooden strip on the table saw making sure the patch is the same thickness as the tenon.
Next I rough cut the length leaving just a little bit of material overhanging the end of the tenon. I’ll glue the patch in place and wait for the glue to set. Next I’ll use my Dremel 4V ROTARY TOOL to do the rough shaping. This is a delicate enough tool to make sure I don’t remove too much material, but powerful enough so that I’m not spending hours trying to remove material. Finally, I’ll do final shaping with a sanding sponge to get a smooth rounded tenon. Crisis averted!
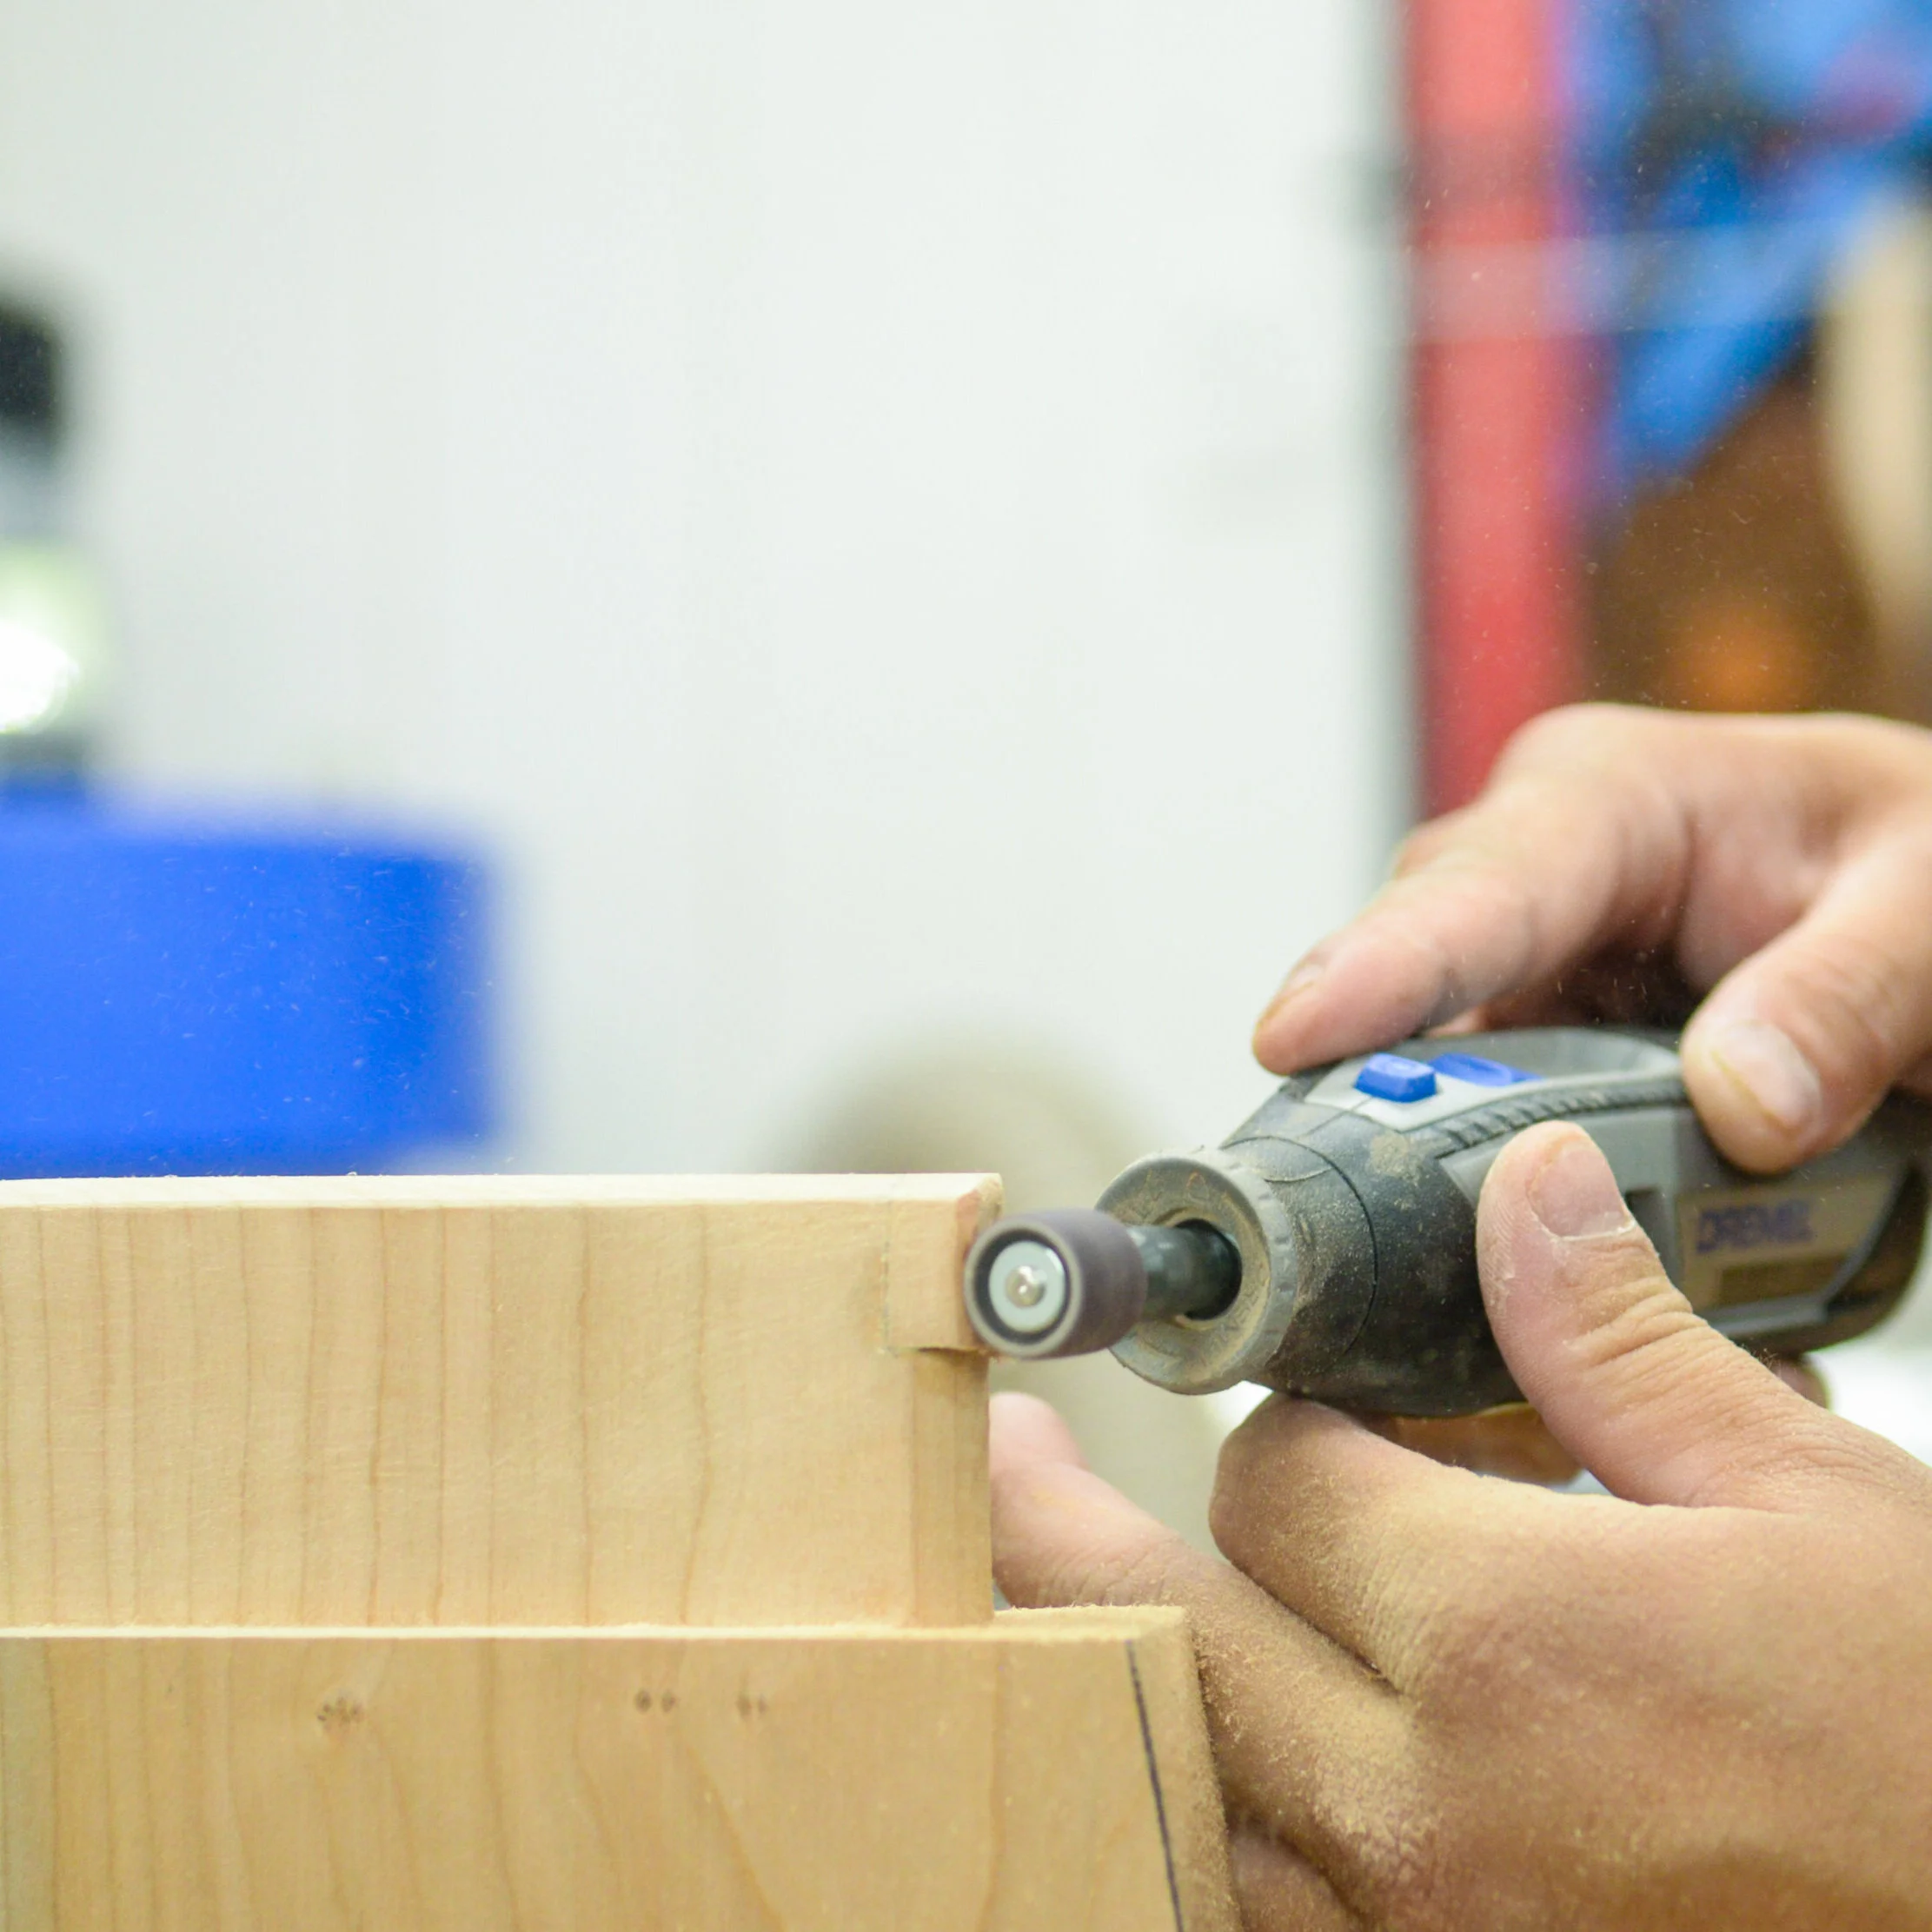
Using my Dremel 4V Rotary Tool to do the rough shaping of the patch
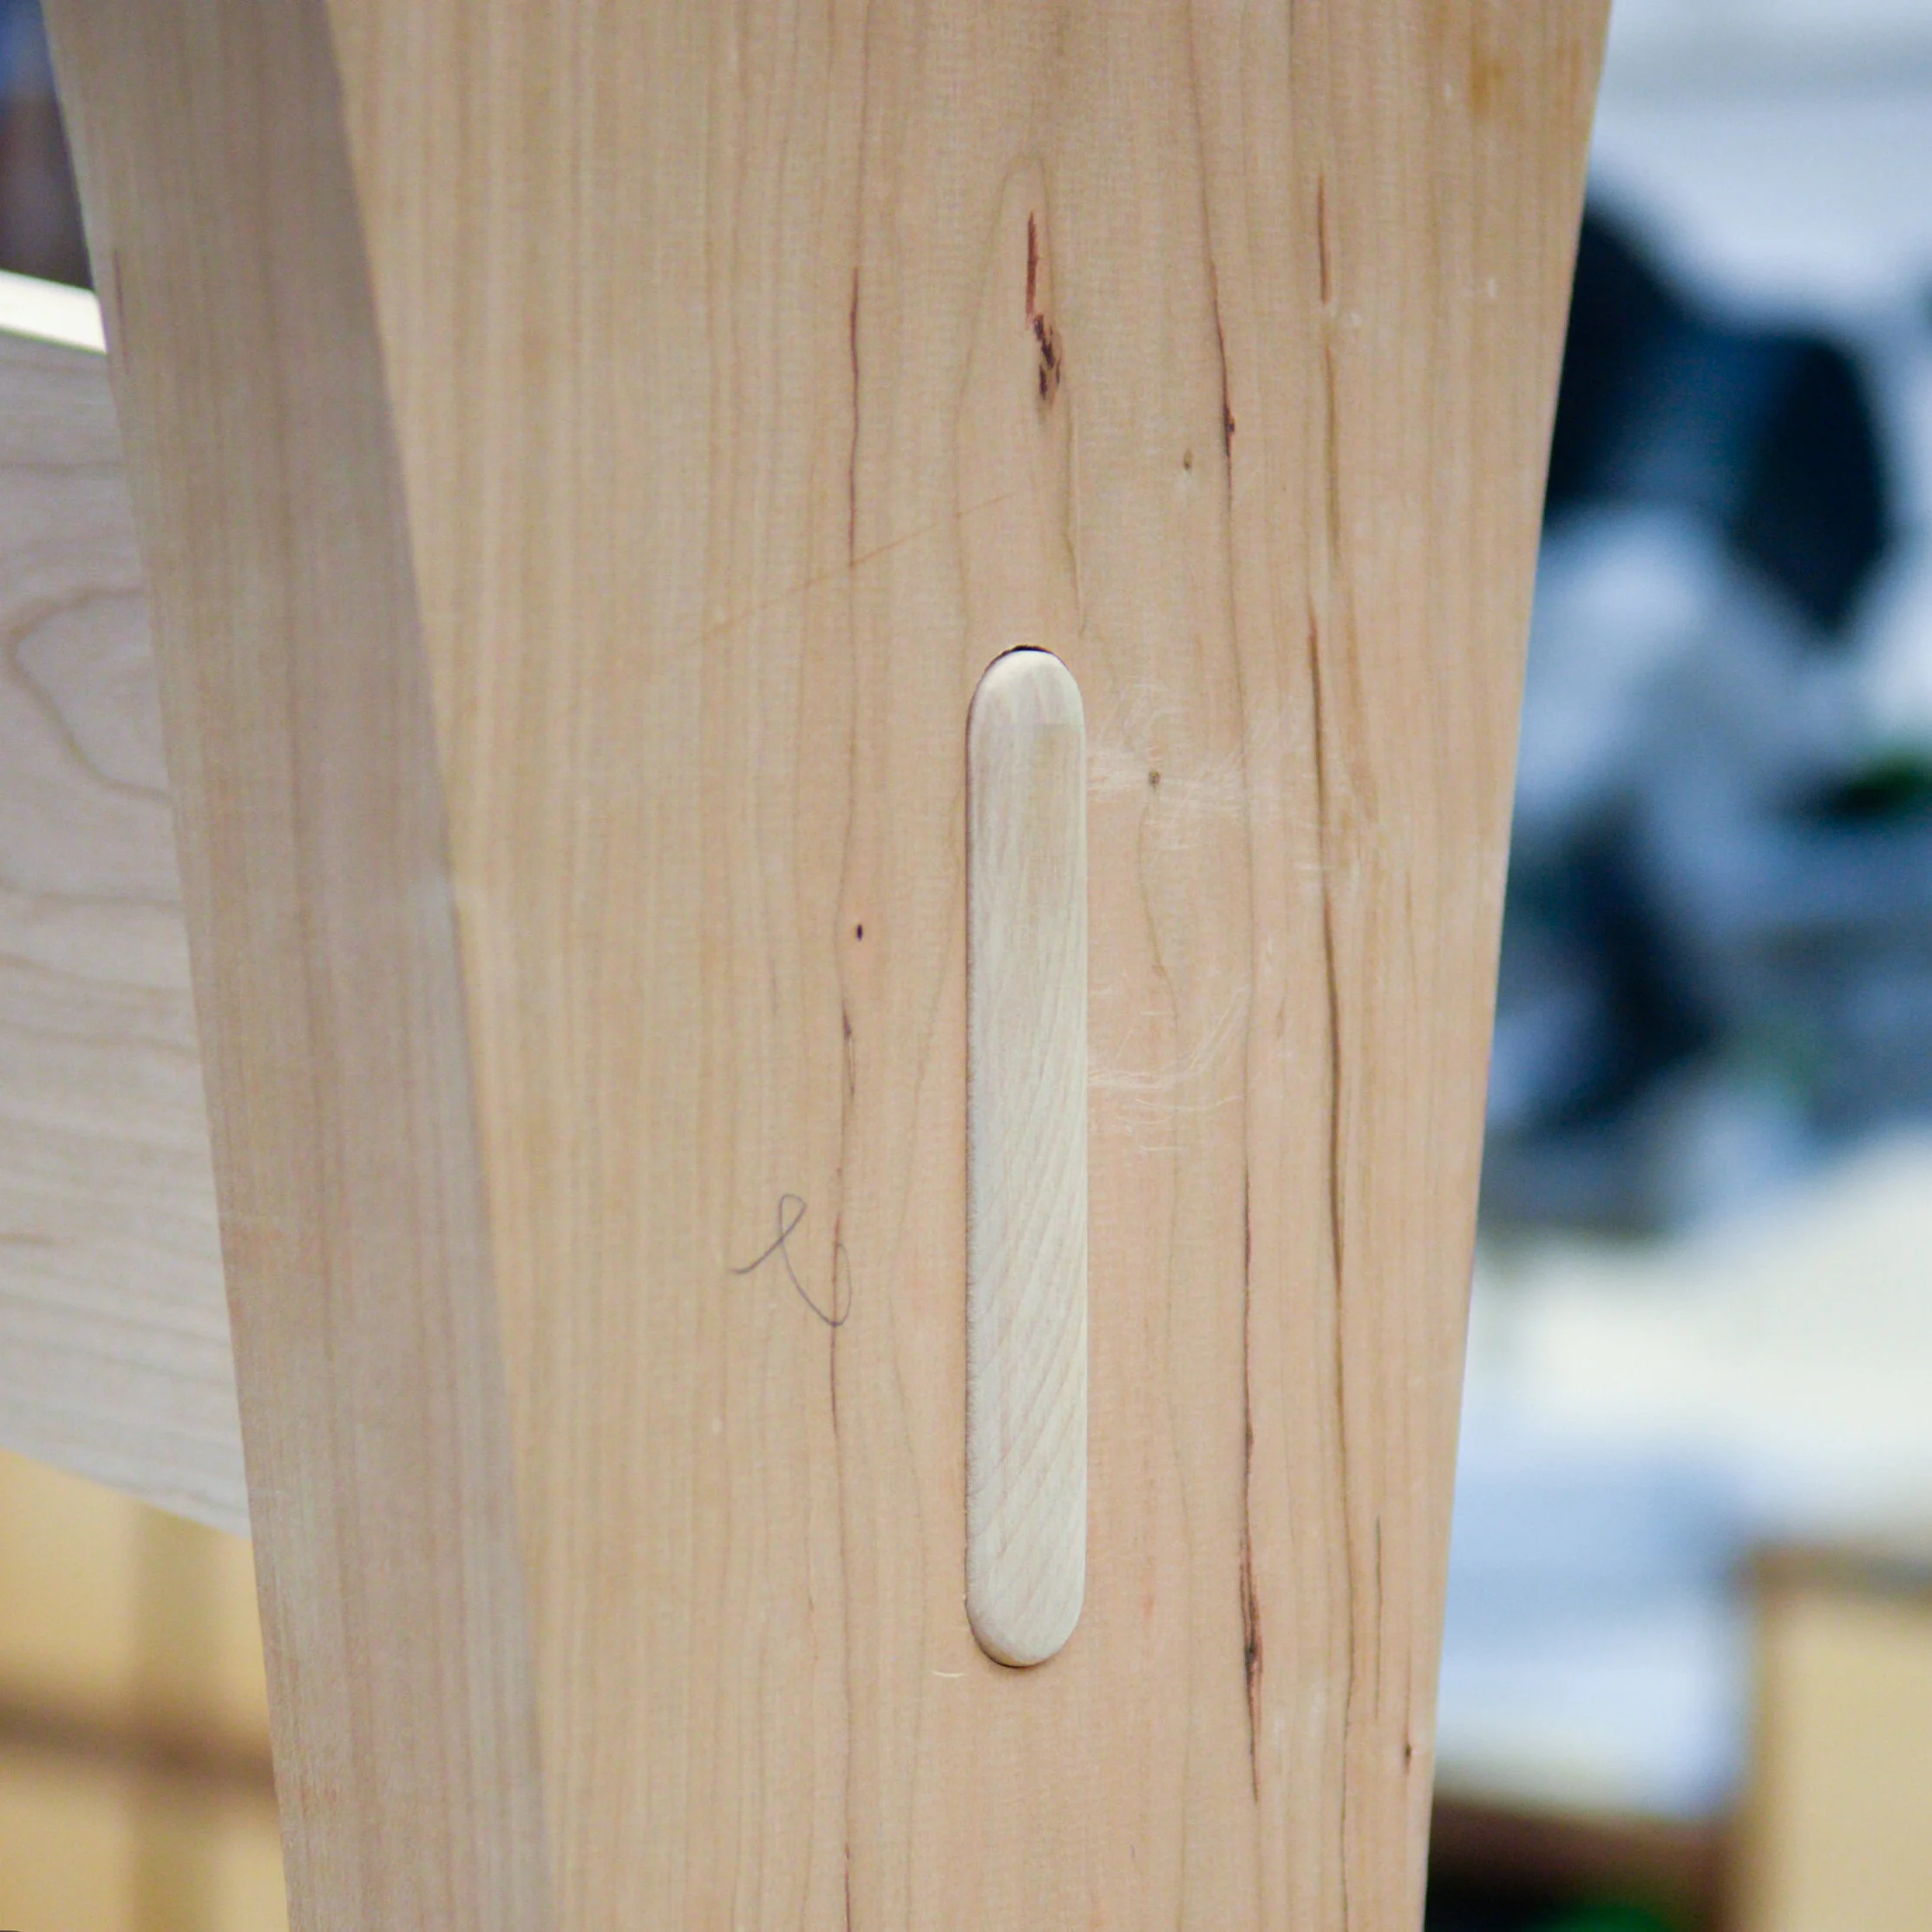
The repair is hardly noticeable
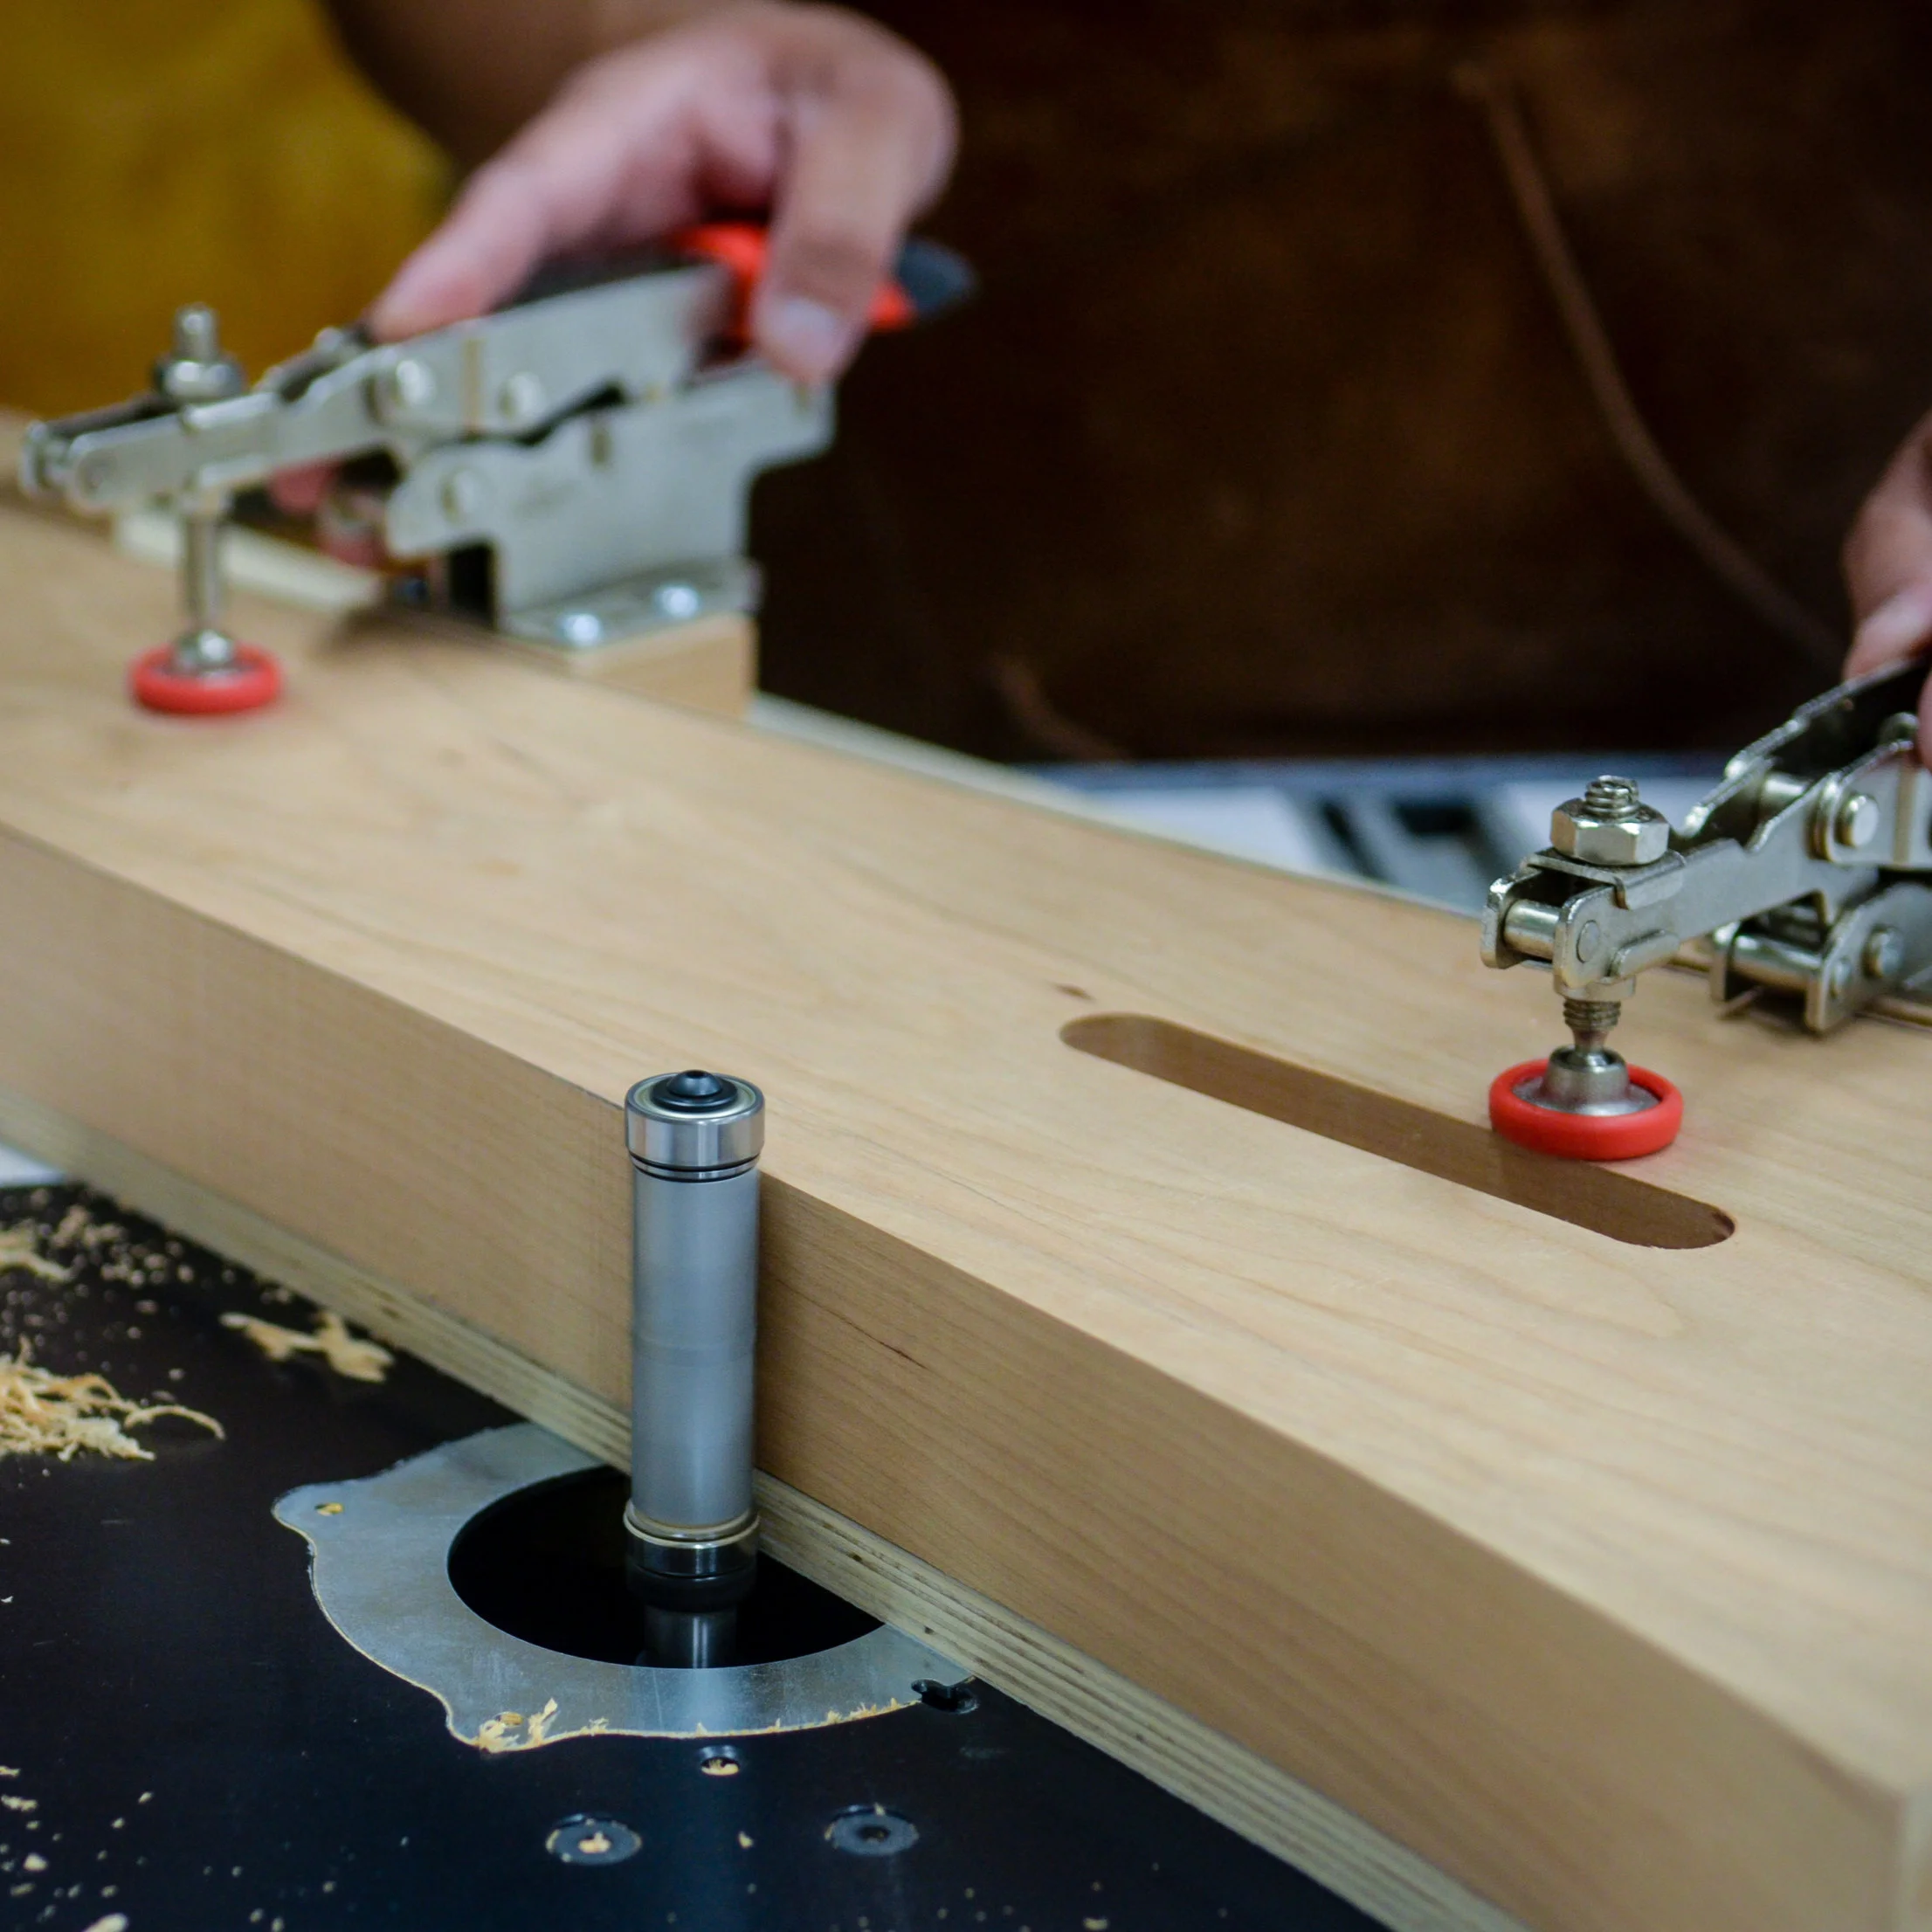
Making Templates and Pattern Routing Jigs
Whenever I’m building furniture with curved pieces, I often produce a template. This helps in the layout of the work piece with respect to grain direction/selection and offers me a life size visualization of the finished piece. This also gives me the ability to reproduce that piece in the future without having to “reinvent the wheel.”
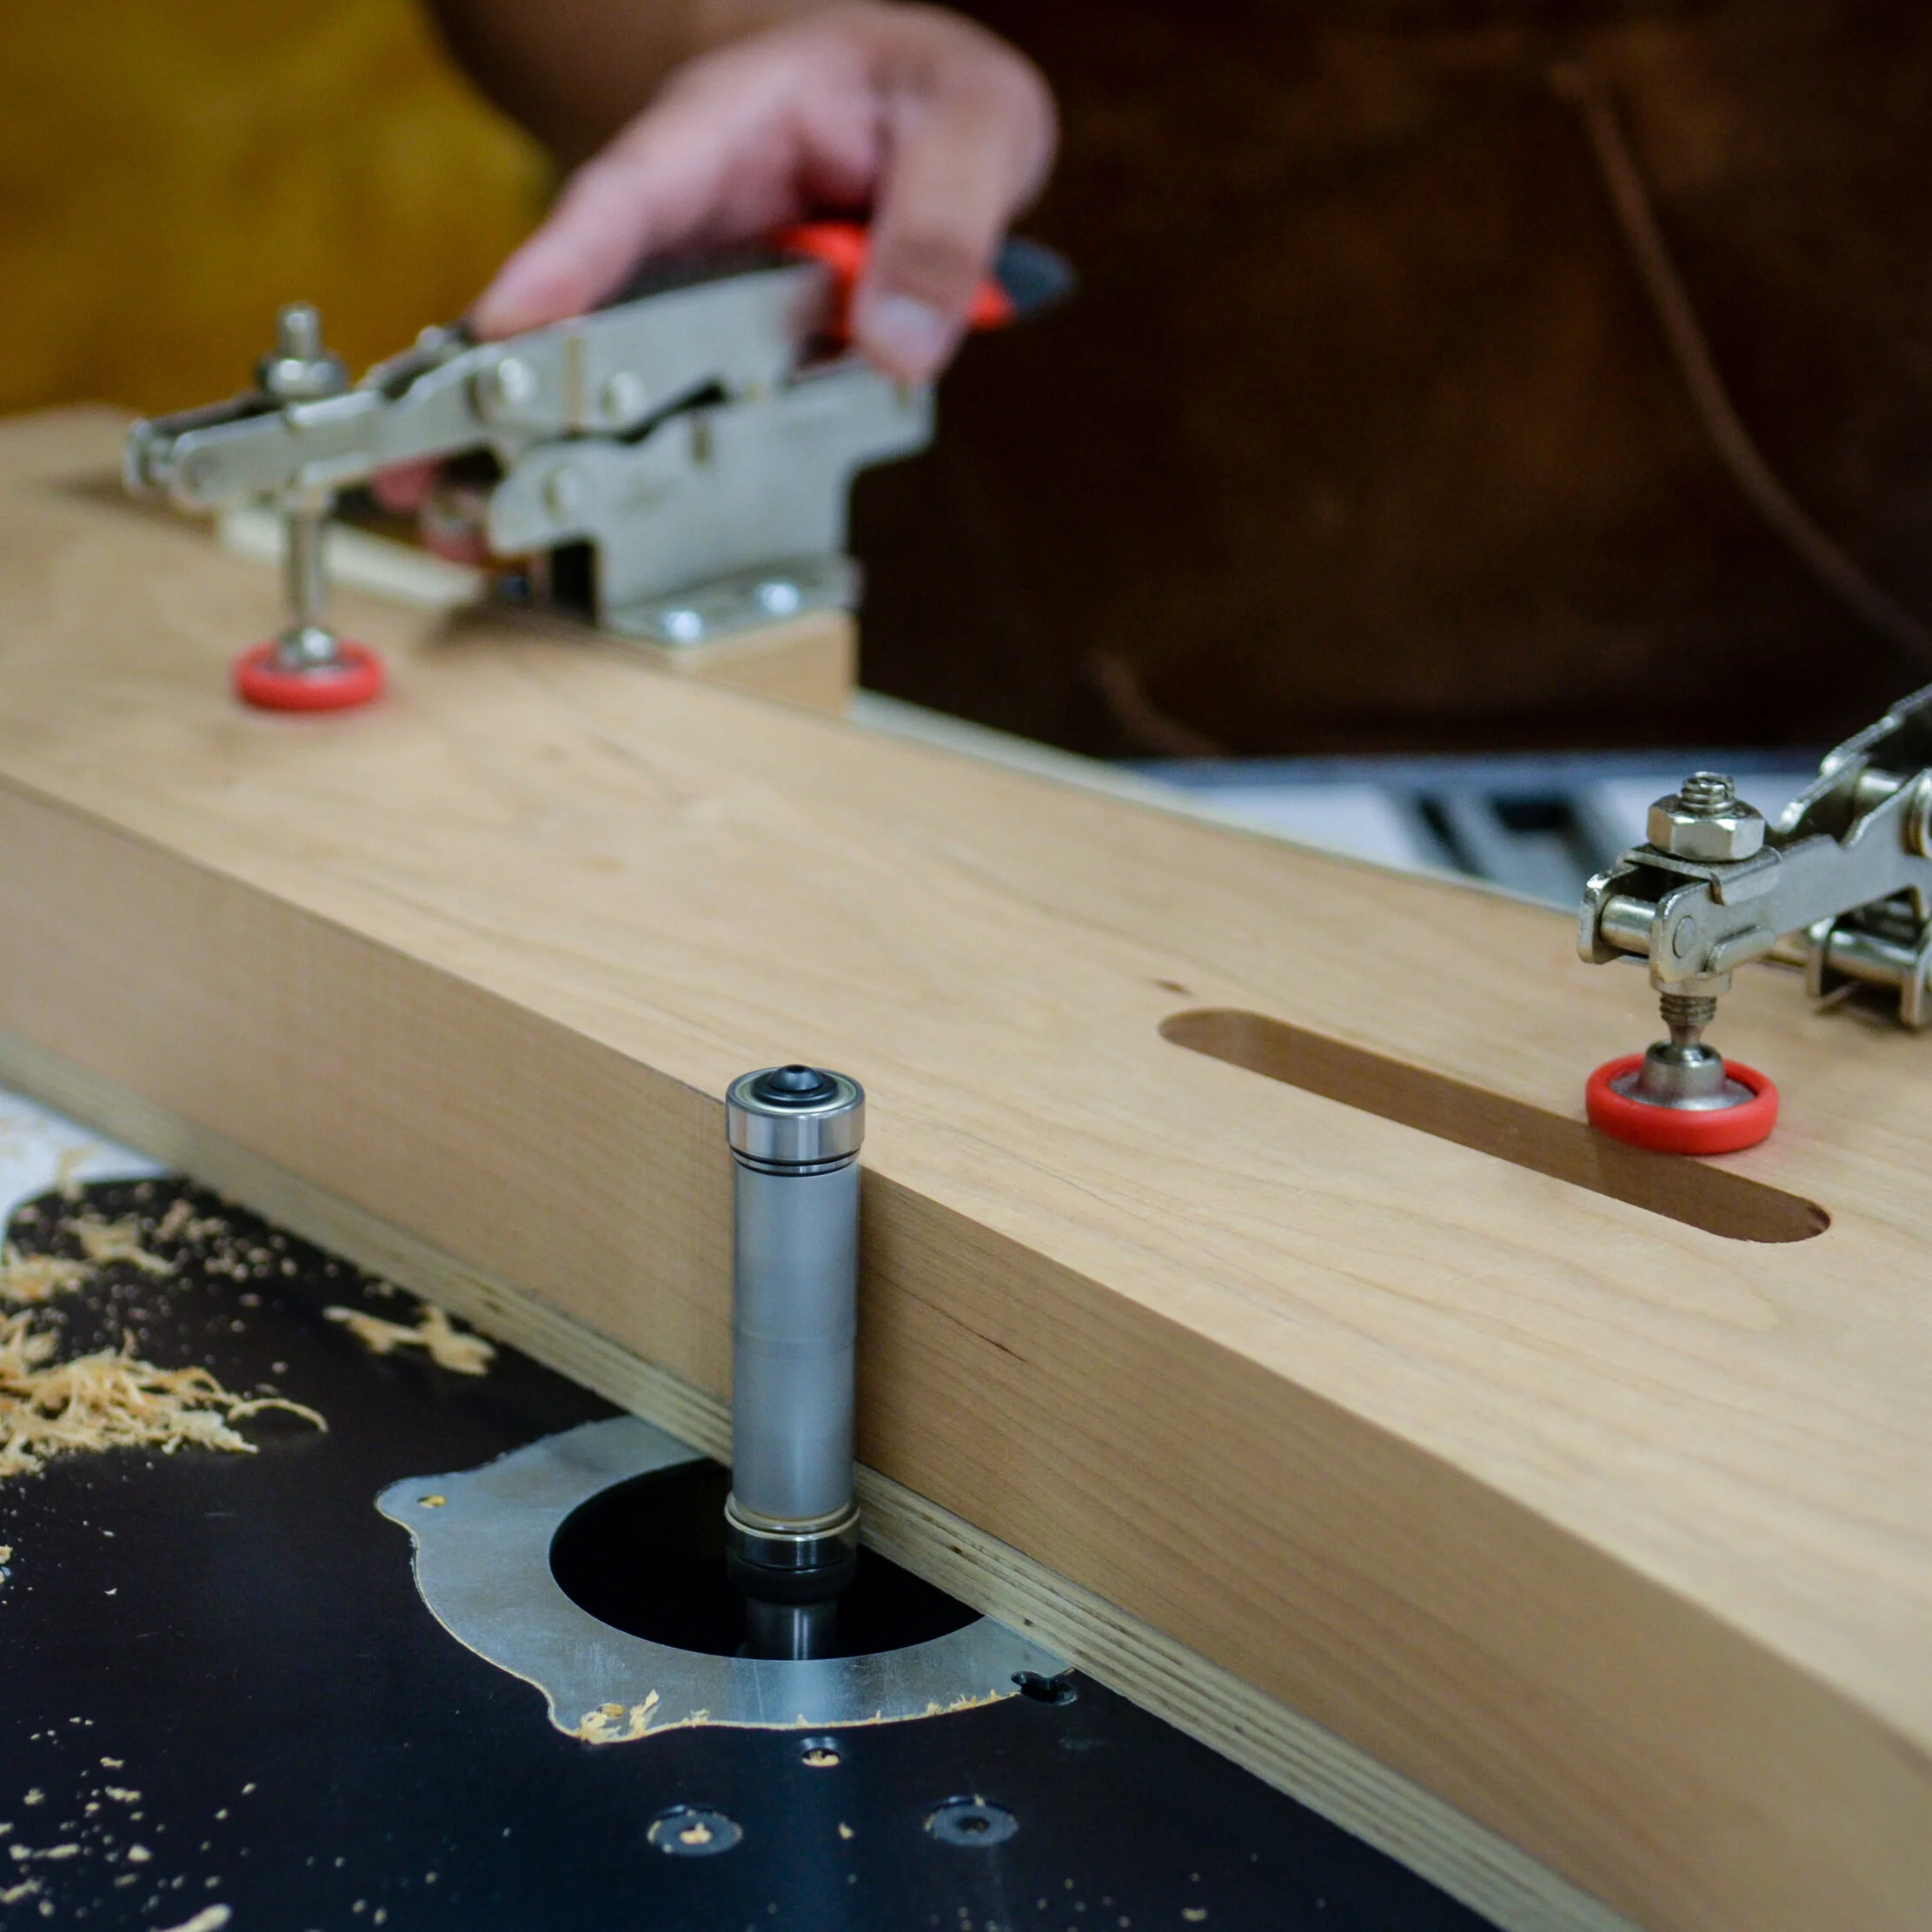
Using a pattern routing jig made from a template
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
Whenever I’m building furniture with curved pieces, I often produce a template. This helps in the layout of the work piece with respect to grain direction/selection and offers me a life size visualization of the finished piece. This also gives me the ability to reproduce that piece in the future without having to “reinvent the wheel.” Another great benefit is the ability to produce work holding jigs/fixtures that help me create exact copies on the router table. Here’s how I go about producing template out of Baltic Birch plywood and pattern routing jigs
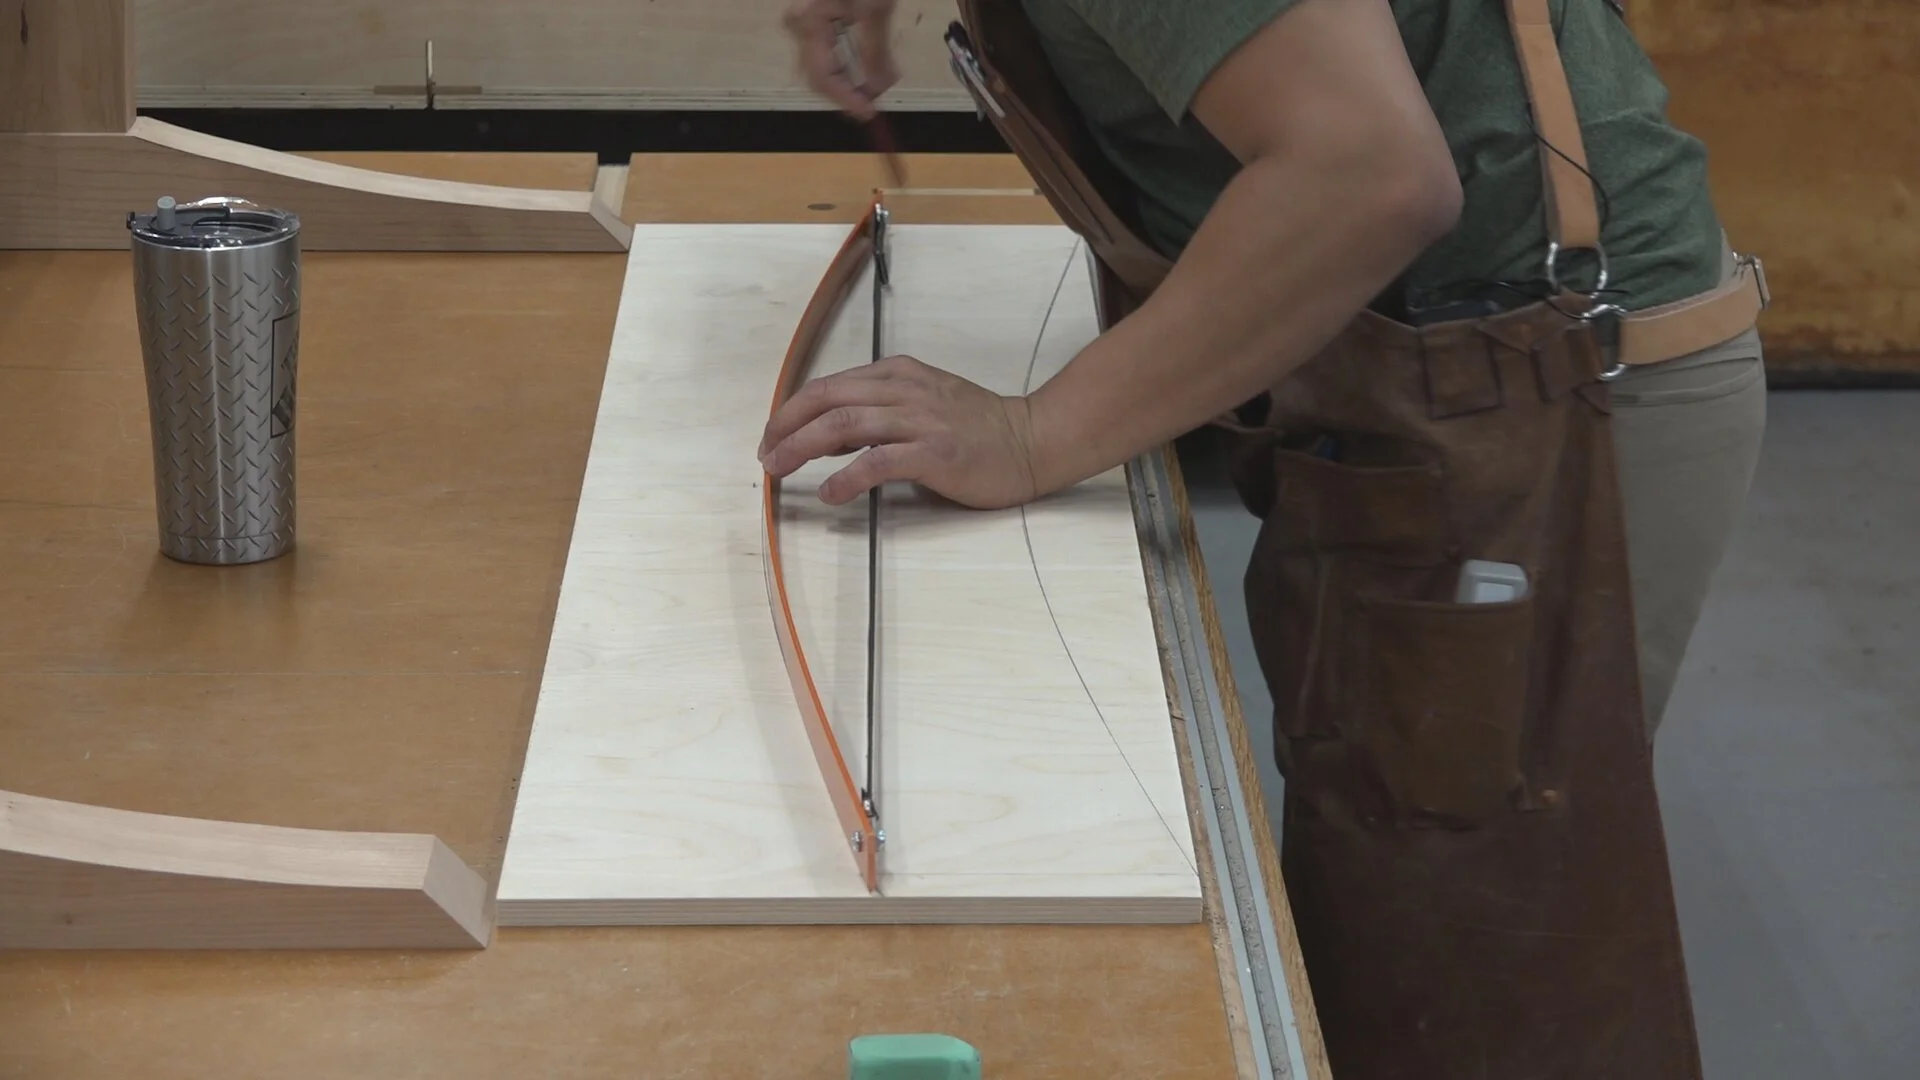
Using a drawing bow to create curves
When it comes to drawing curves, I like to use a drawing bow. A drawing bow is nothing more than a flexible piece of plastic or wood that is connected with an adjustable strap at the ends. The bow is infinitely adjustable to produce a slight curve or a drastic arc. I’ll trace out the curve from the drawing bow onto some 1/2” Baltic Birch. You can also use 1/4” MDF. I just have a lot of !/2” Baltic Birch so that’s what I use.
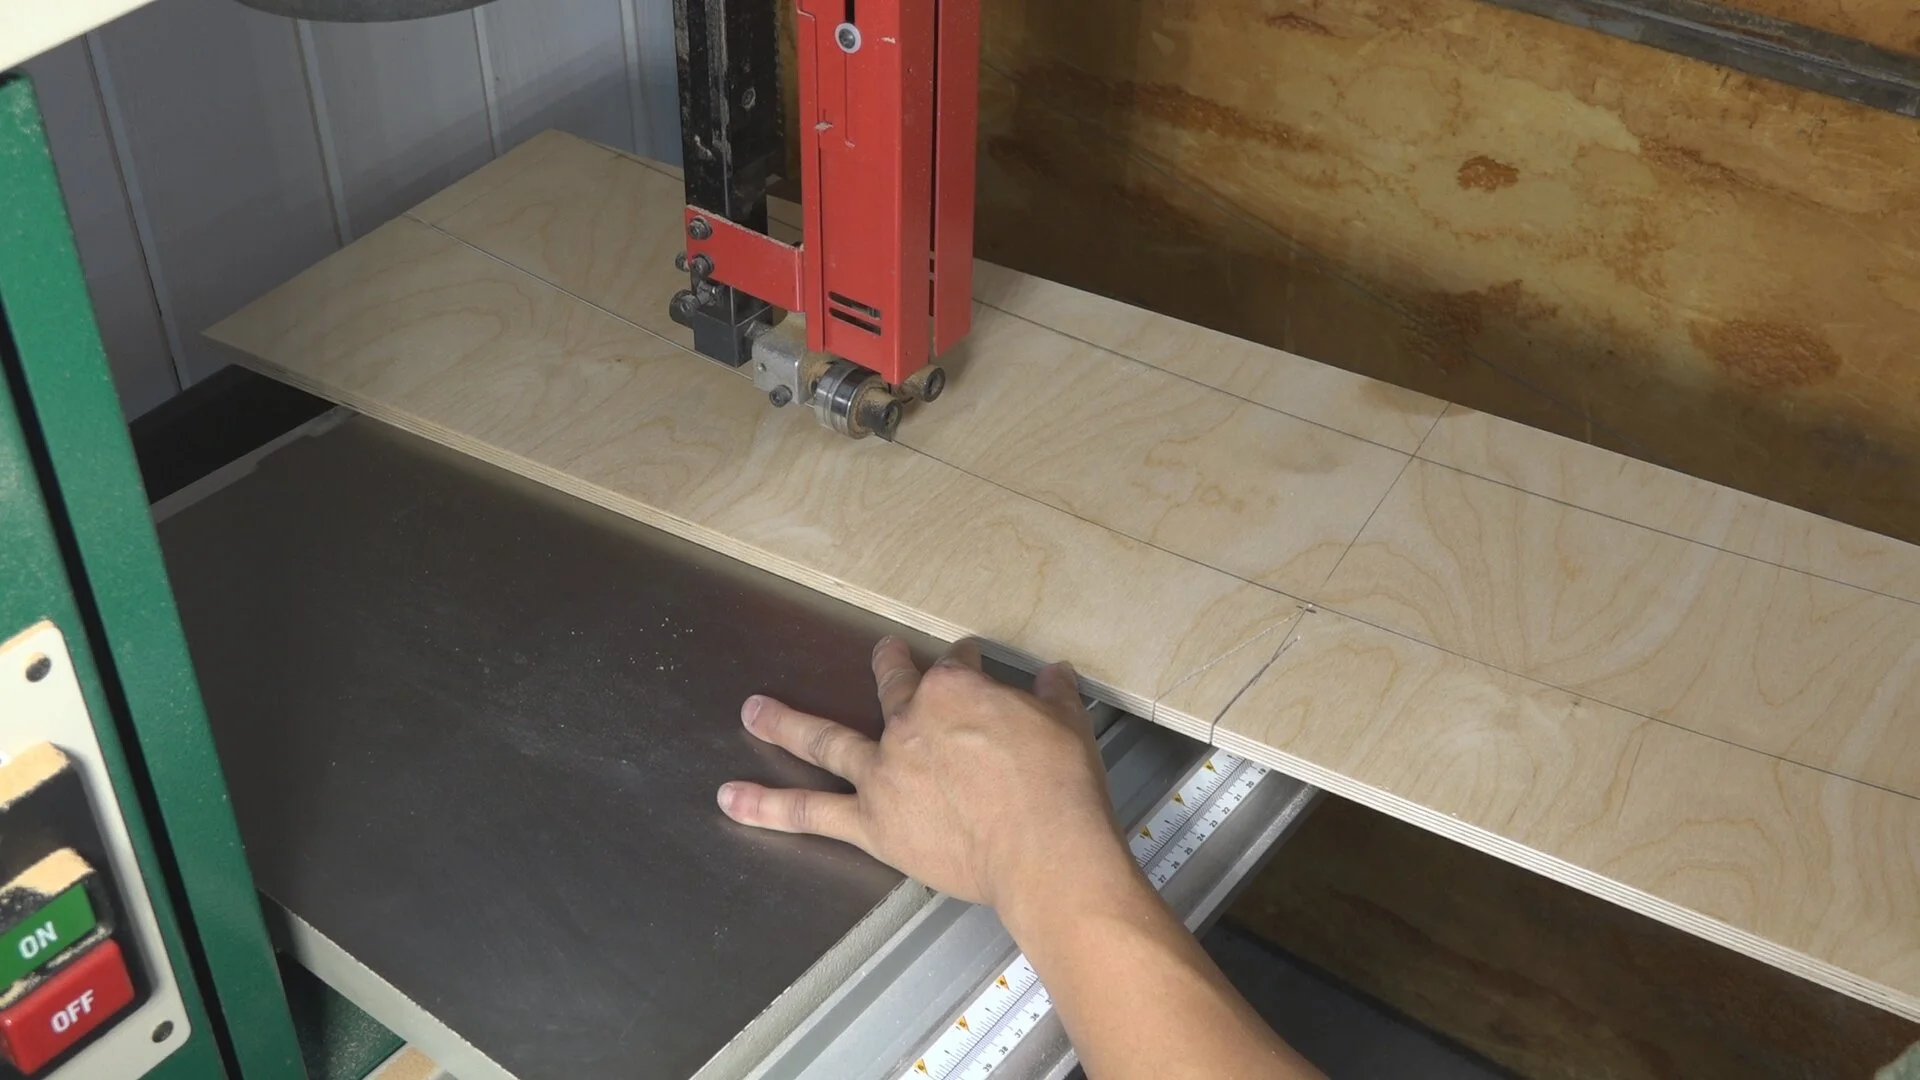
Cutting out the template on the bandsaw
I then go to the bandsaw and cut out the curve out of Baltic Birch making sure to leave about 1/8” heavy of the traced line. I like using the bandsaw but I’ve done this before with a jigsaw (also known as a saber saw). Generally, I use a jigsaw for bigger pieces since it’s easier to bring the tool to the workpiece.
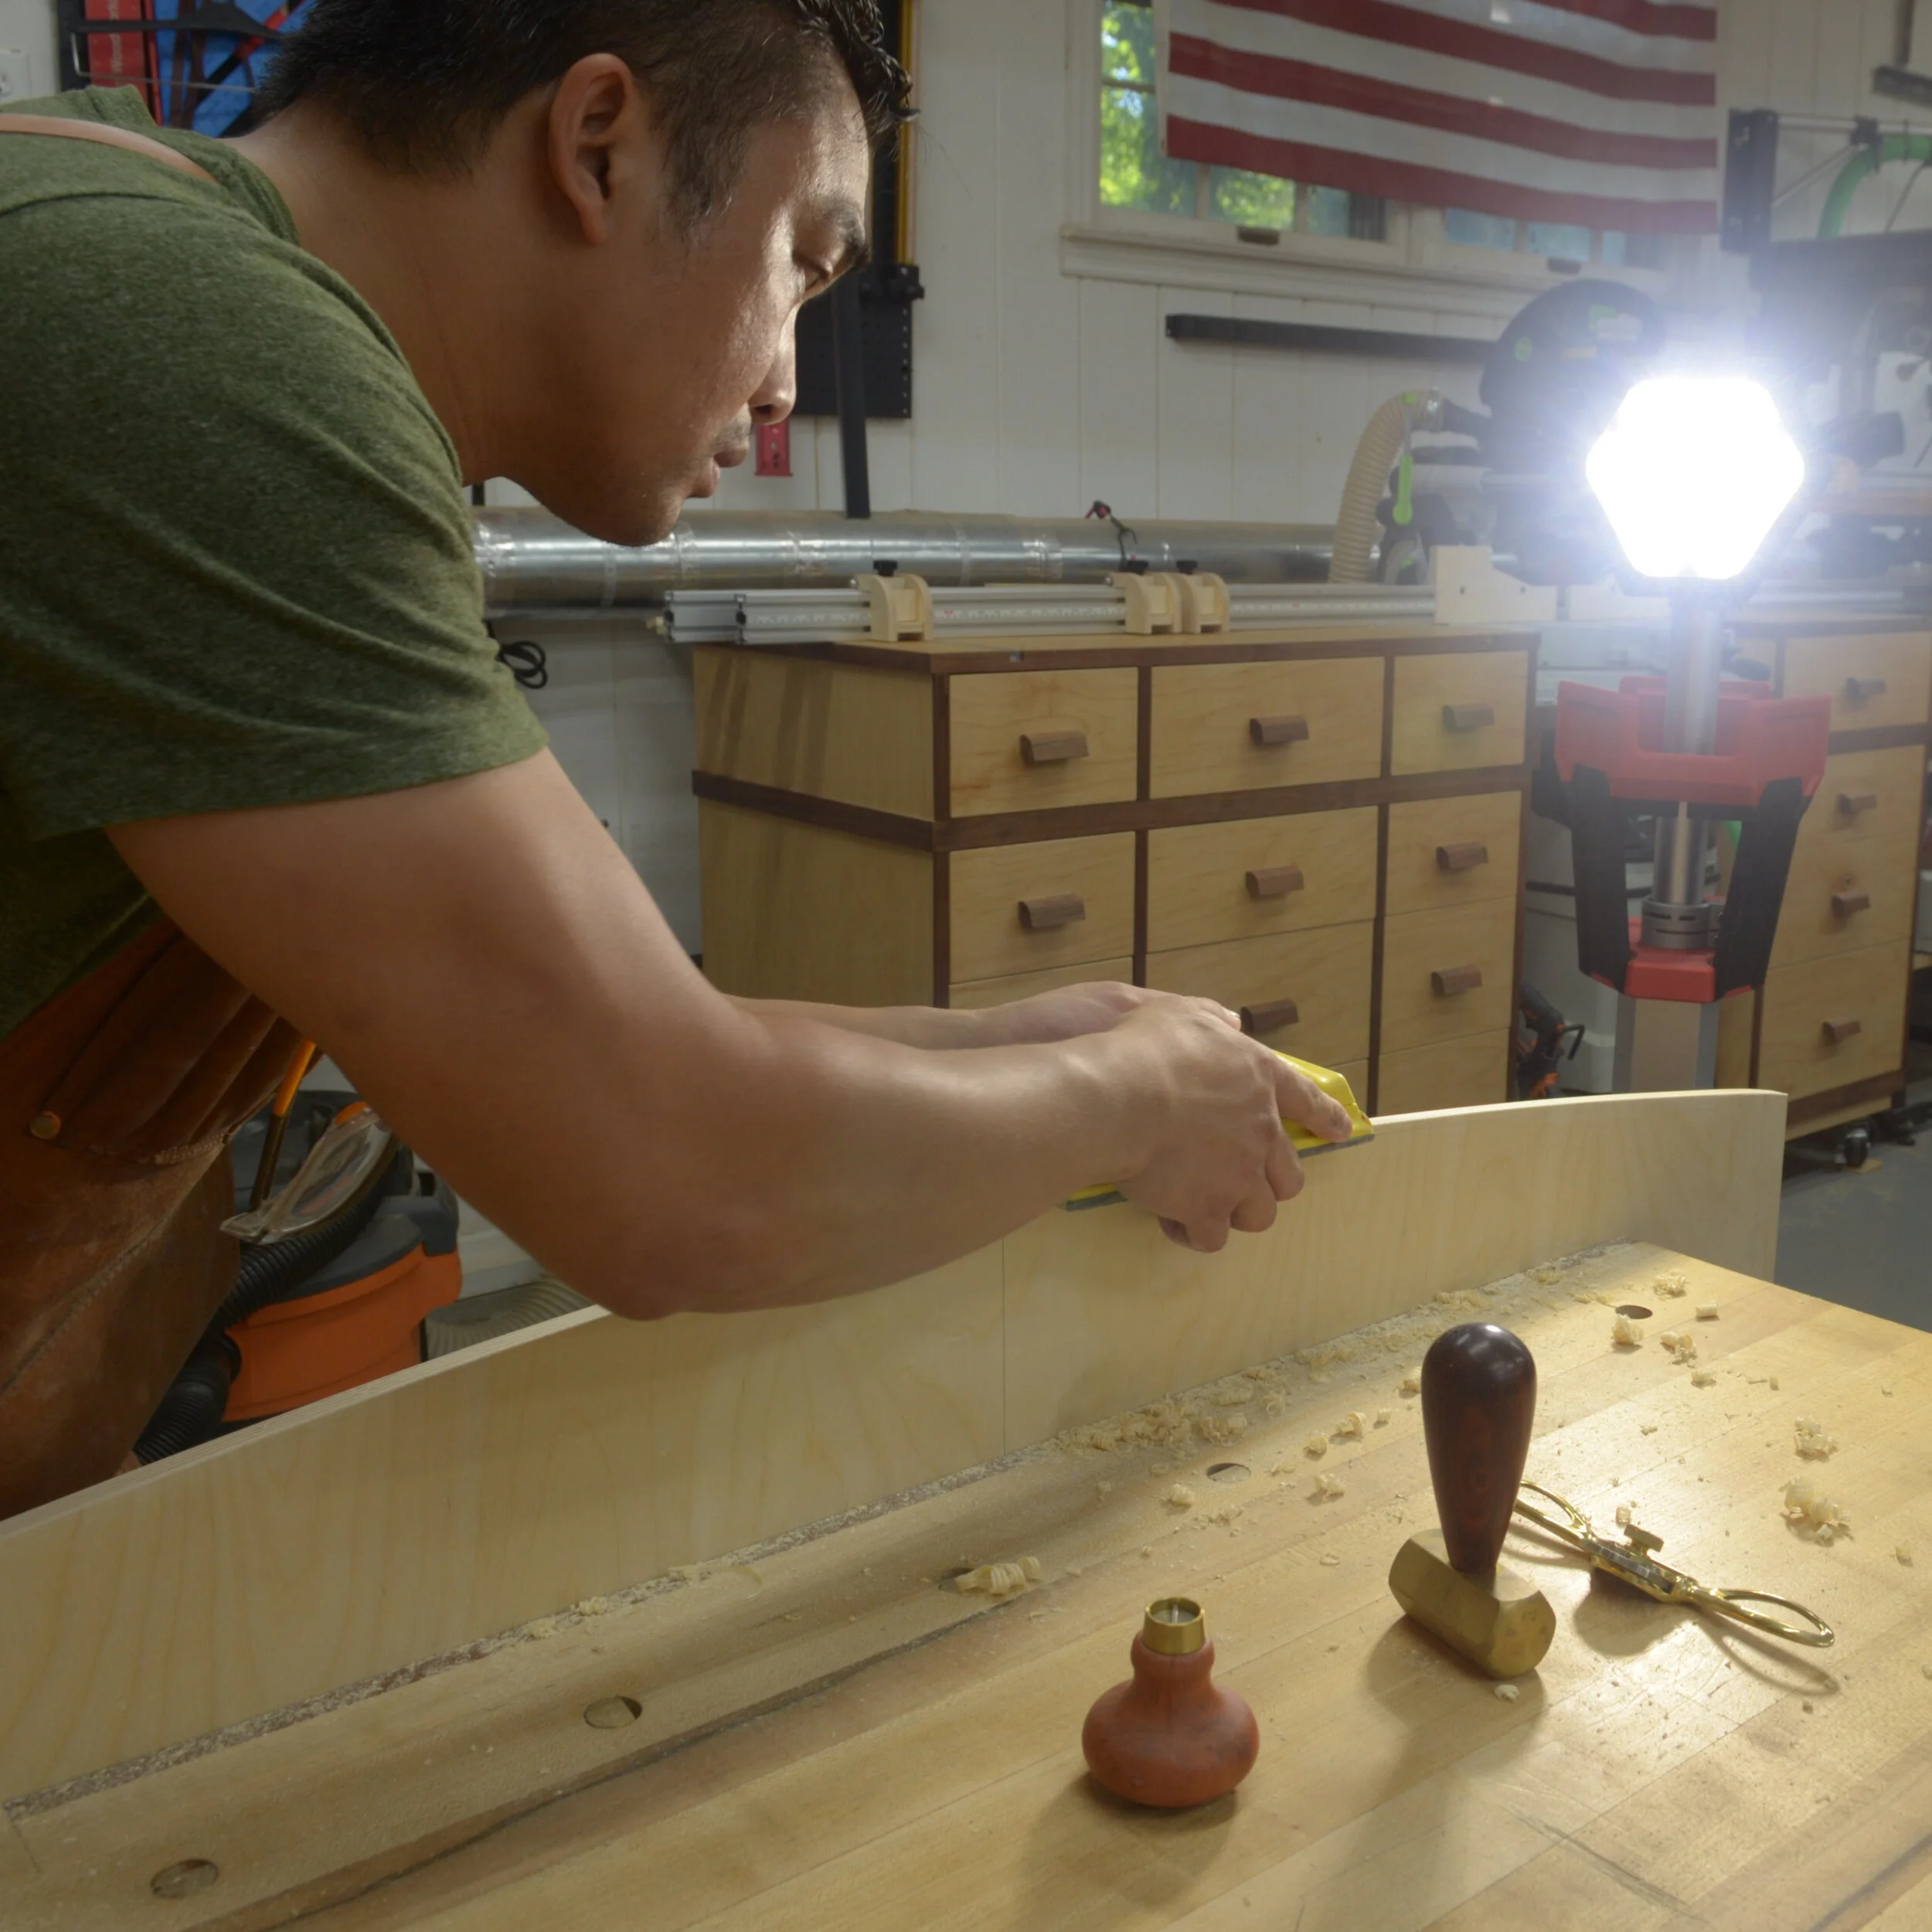
Using low raking light to smooth the curve of the template
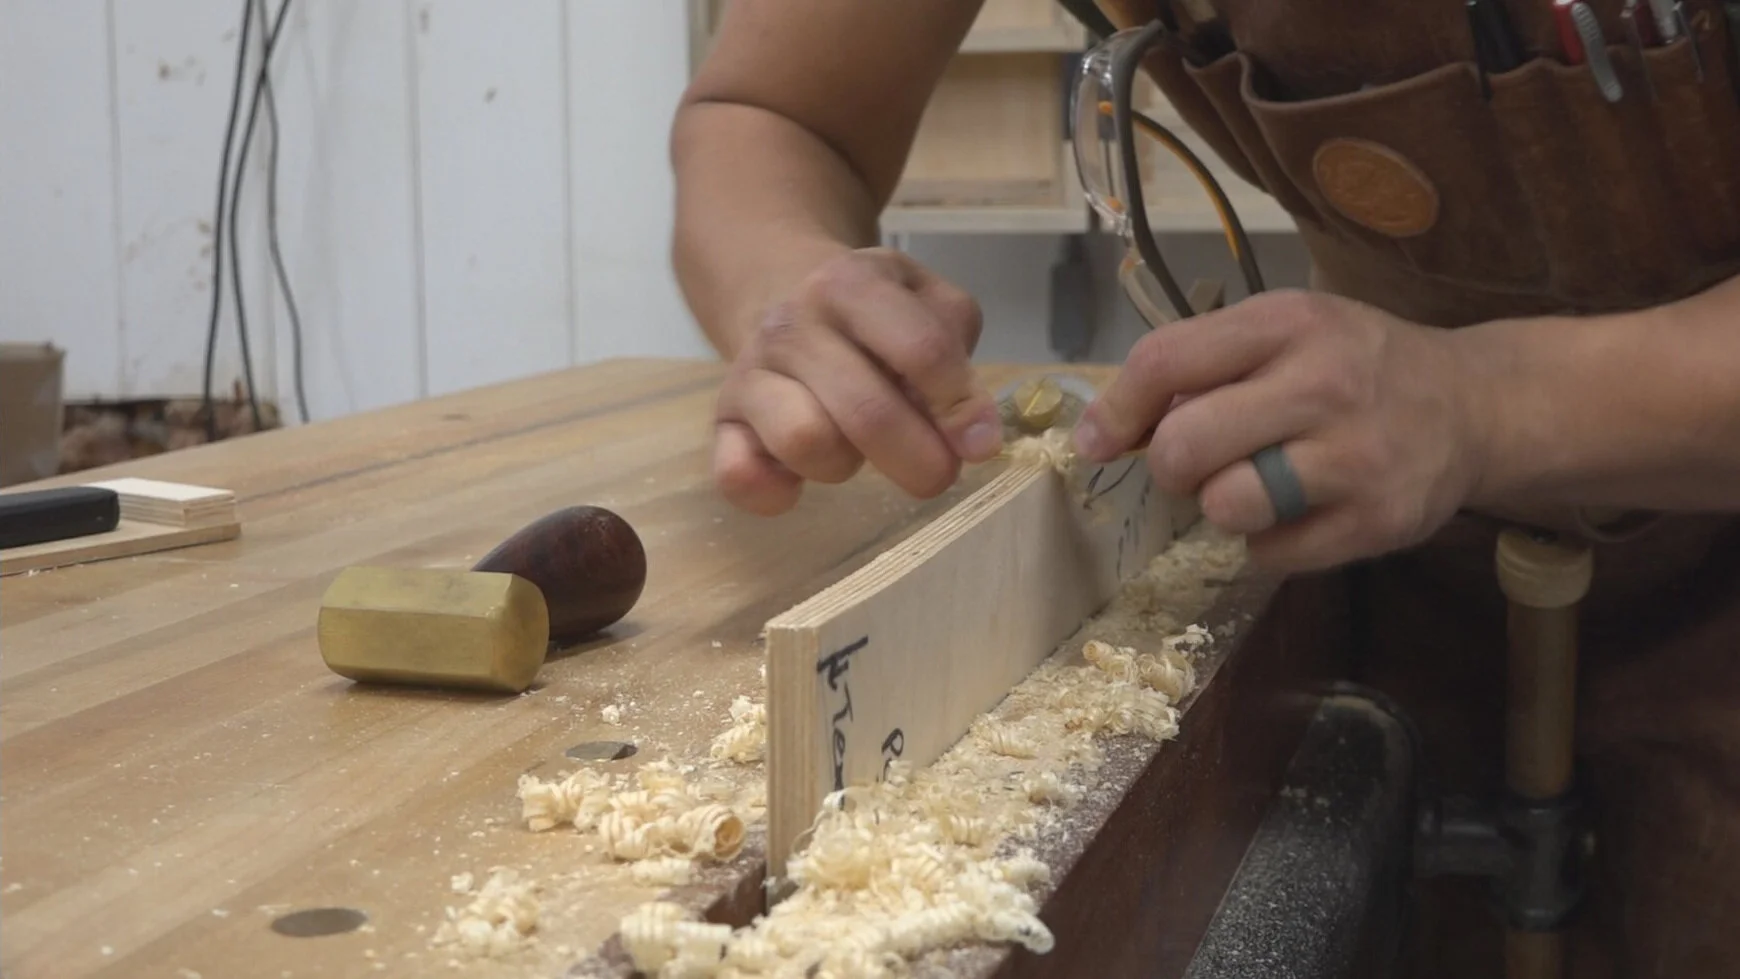
Using a spokeshave to smooth out the curve of the template
After cutting the template on the bandsaw, I go to my workbench to smooth out the curve and remove the rough material left by the bandsaw using a spokeshave and sanding block. I want to make sure I don’t have any bumpy surfaces. A good way to make sure I’ve removed enough material and to make sure I have a smooth curve is to have low raking light. I used the Milwaukee 18-Volt Lithium-Ion Cordless Rocket Dual Power Tower Light as my light source. It’s adjustable up to 7-feet and runs on either AC power or M18 batteries. This makes the light extremely versatile for all types of lighting applications.
Once I’m happy with the template, I’ll then start making the pattern routing jig. The pattern routing jig is also made of Baltic Birch but is oversized to accommodate for wooden blocks that register off of the tenons on my workpiece and also act as mounting blocks for toggle clamps. The wooden blocks are cut to the exact same thickness as the final workpiece on the Milwaukee 18-Volt Lithium-Ion Brushless Cordless 10 in. Dual Bevel Sliding Compound Miter Saw. The length and width are arbitrary for these wooden blocks but it’s important that they are big enough to mount toggle clamps. I’ll use super glue to attach the wooden blocks and then use the Milwaukee 18-Volt Lithium-Ion Brushless Cordless Gen II 18-Gauge Brad Nailer with 2-inch brad nails to secure the wooden blocks to the Baltic Birch. Once I’m happy with the location of the support/mounting blocks, I’ll then temporarily attach the template to the jig blank with double sided tape.
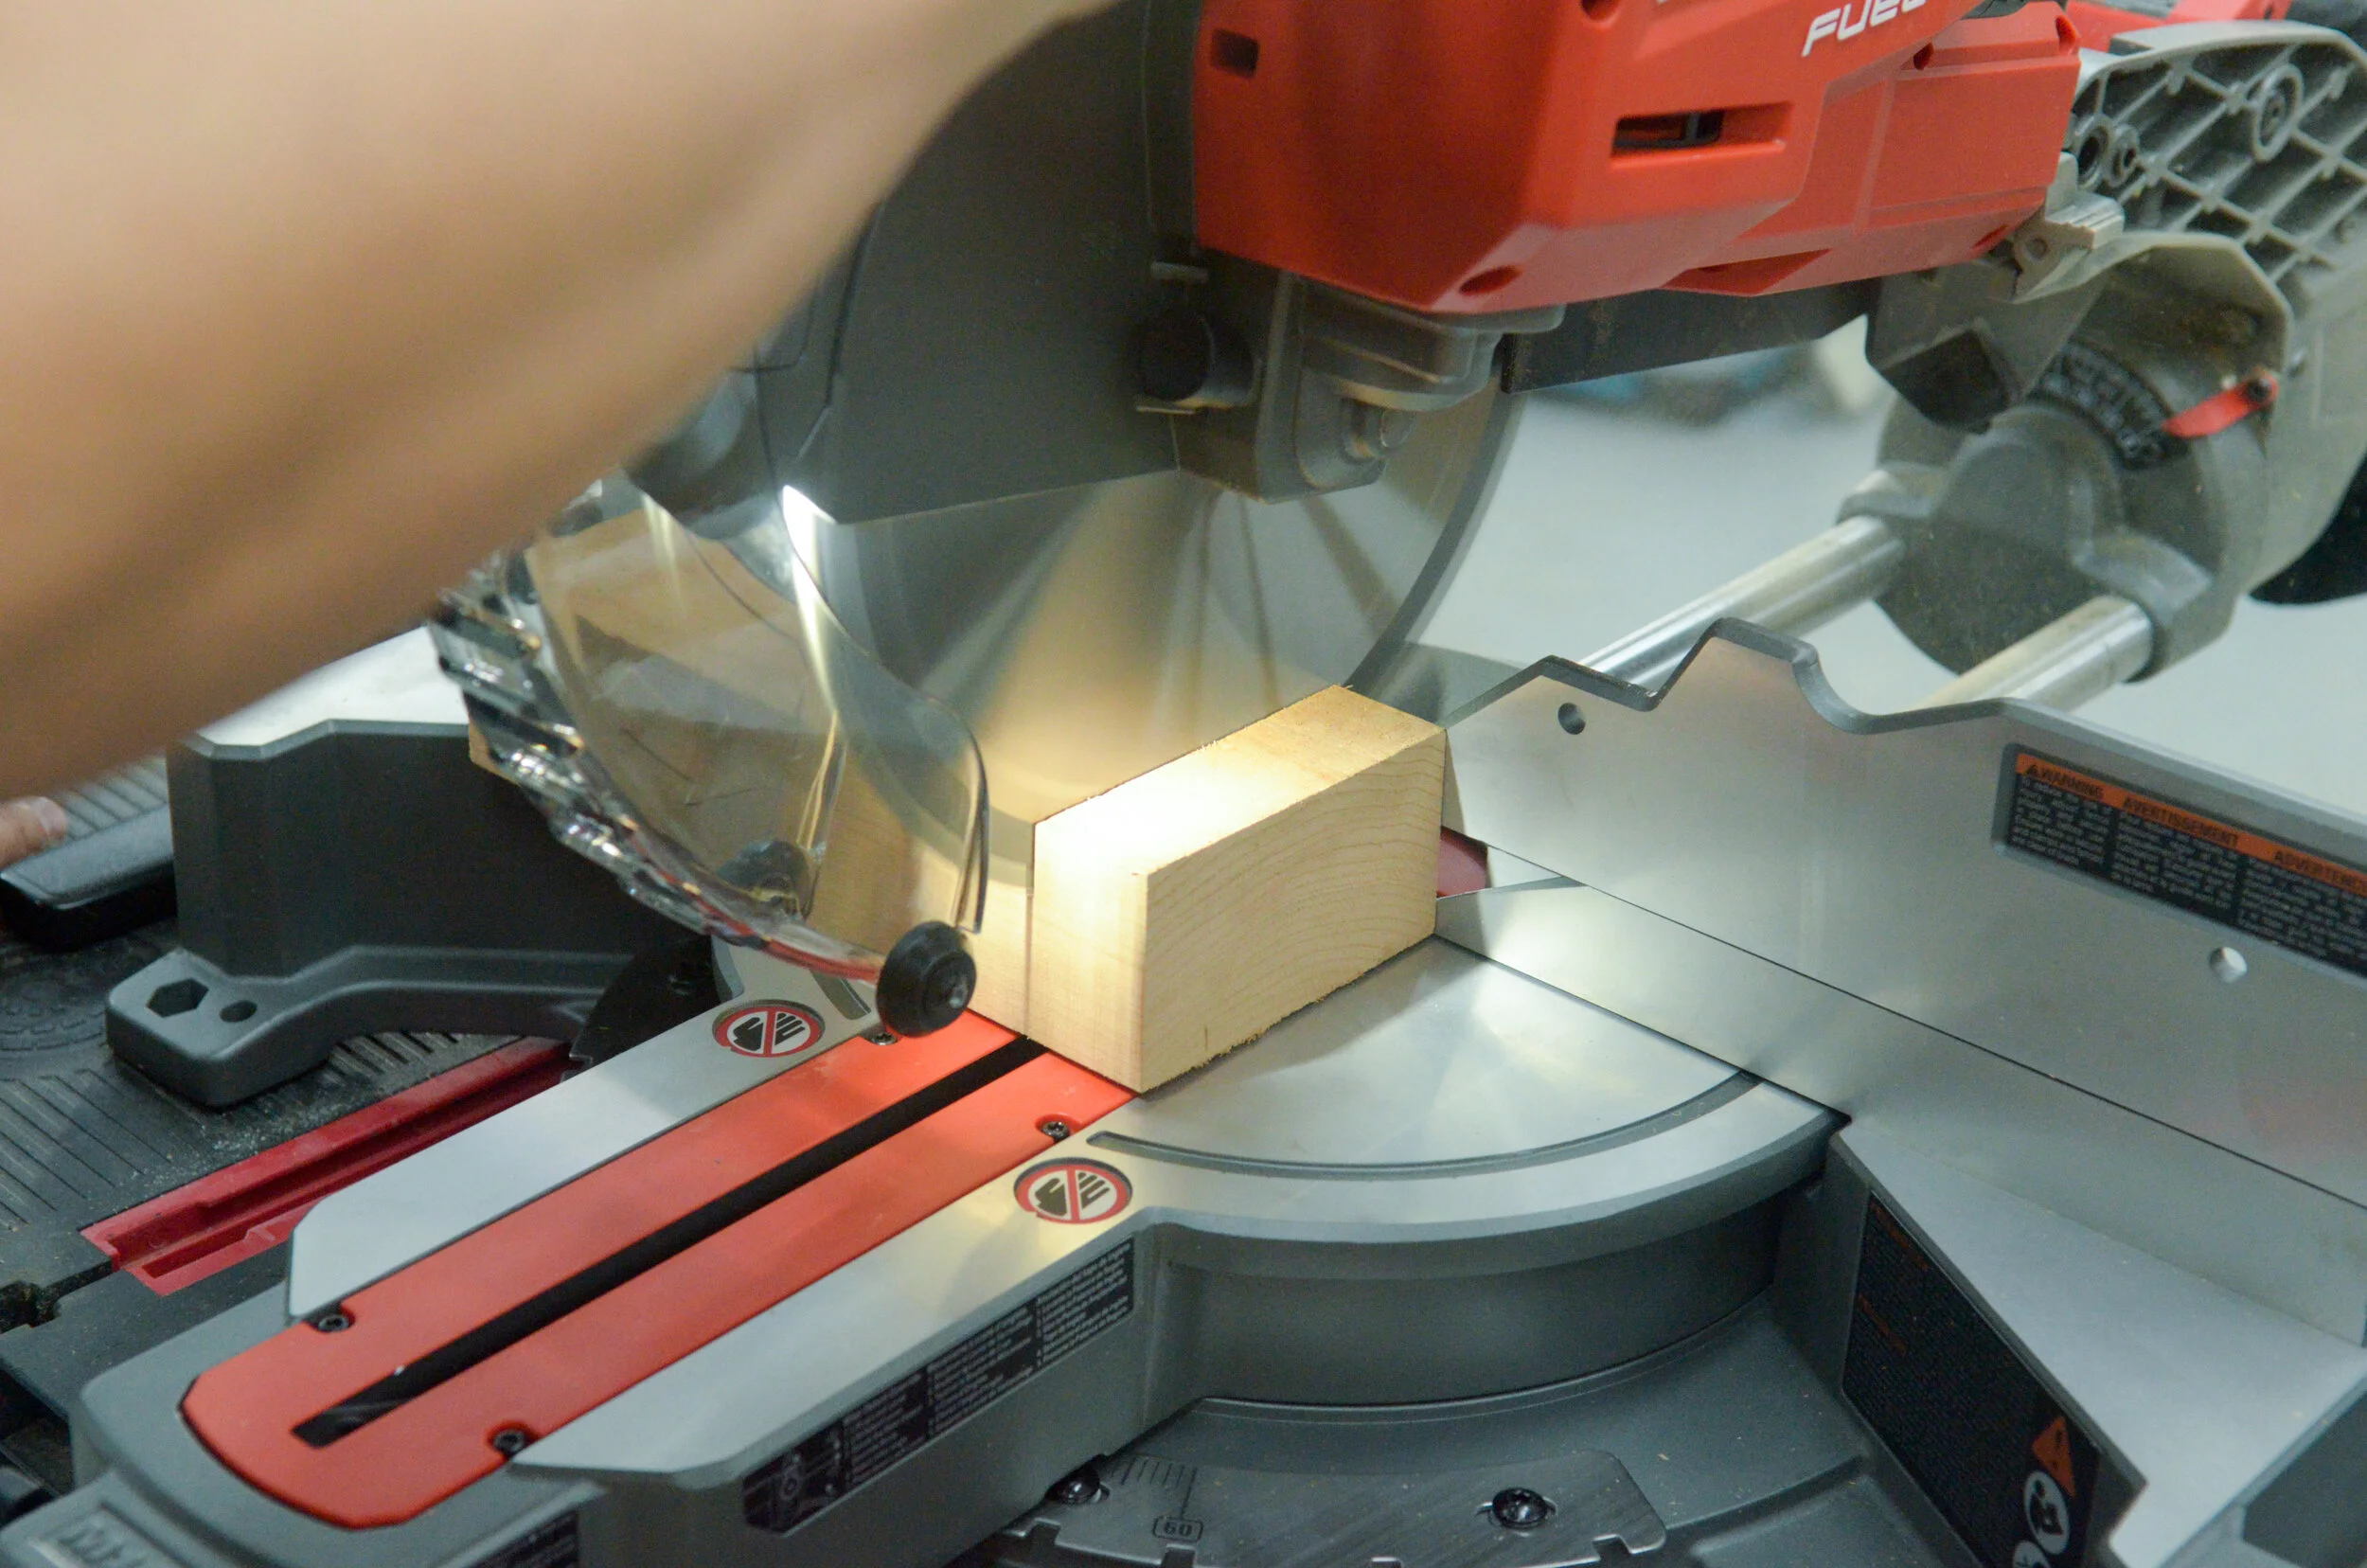
Cutting support blocks for toggle clamps on the Milwaukee 18-volt 10 in. miter saw
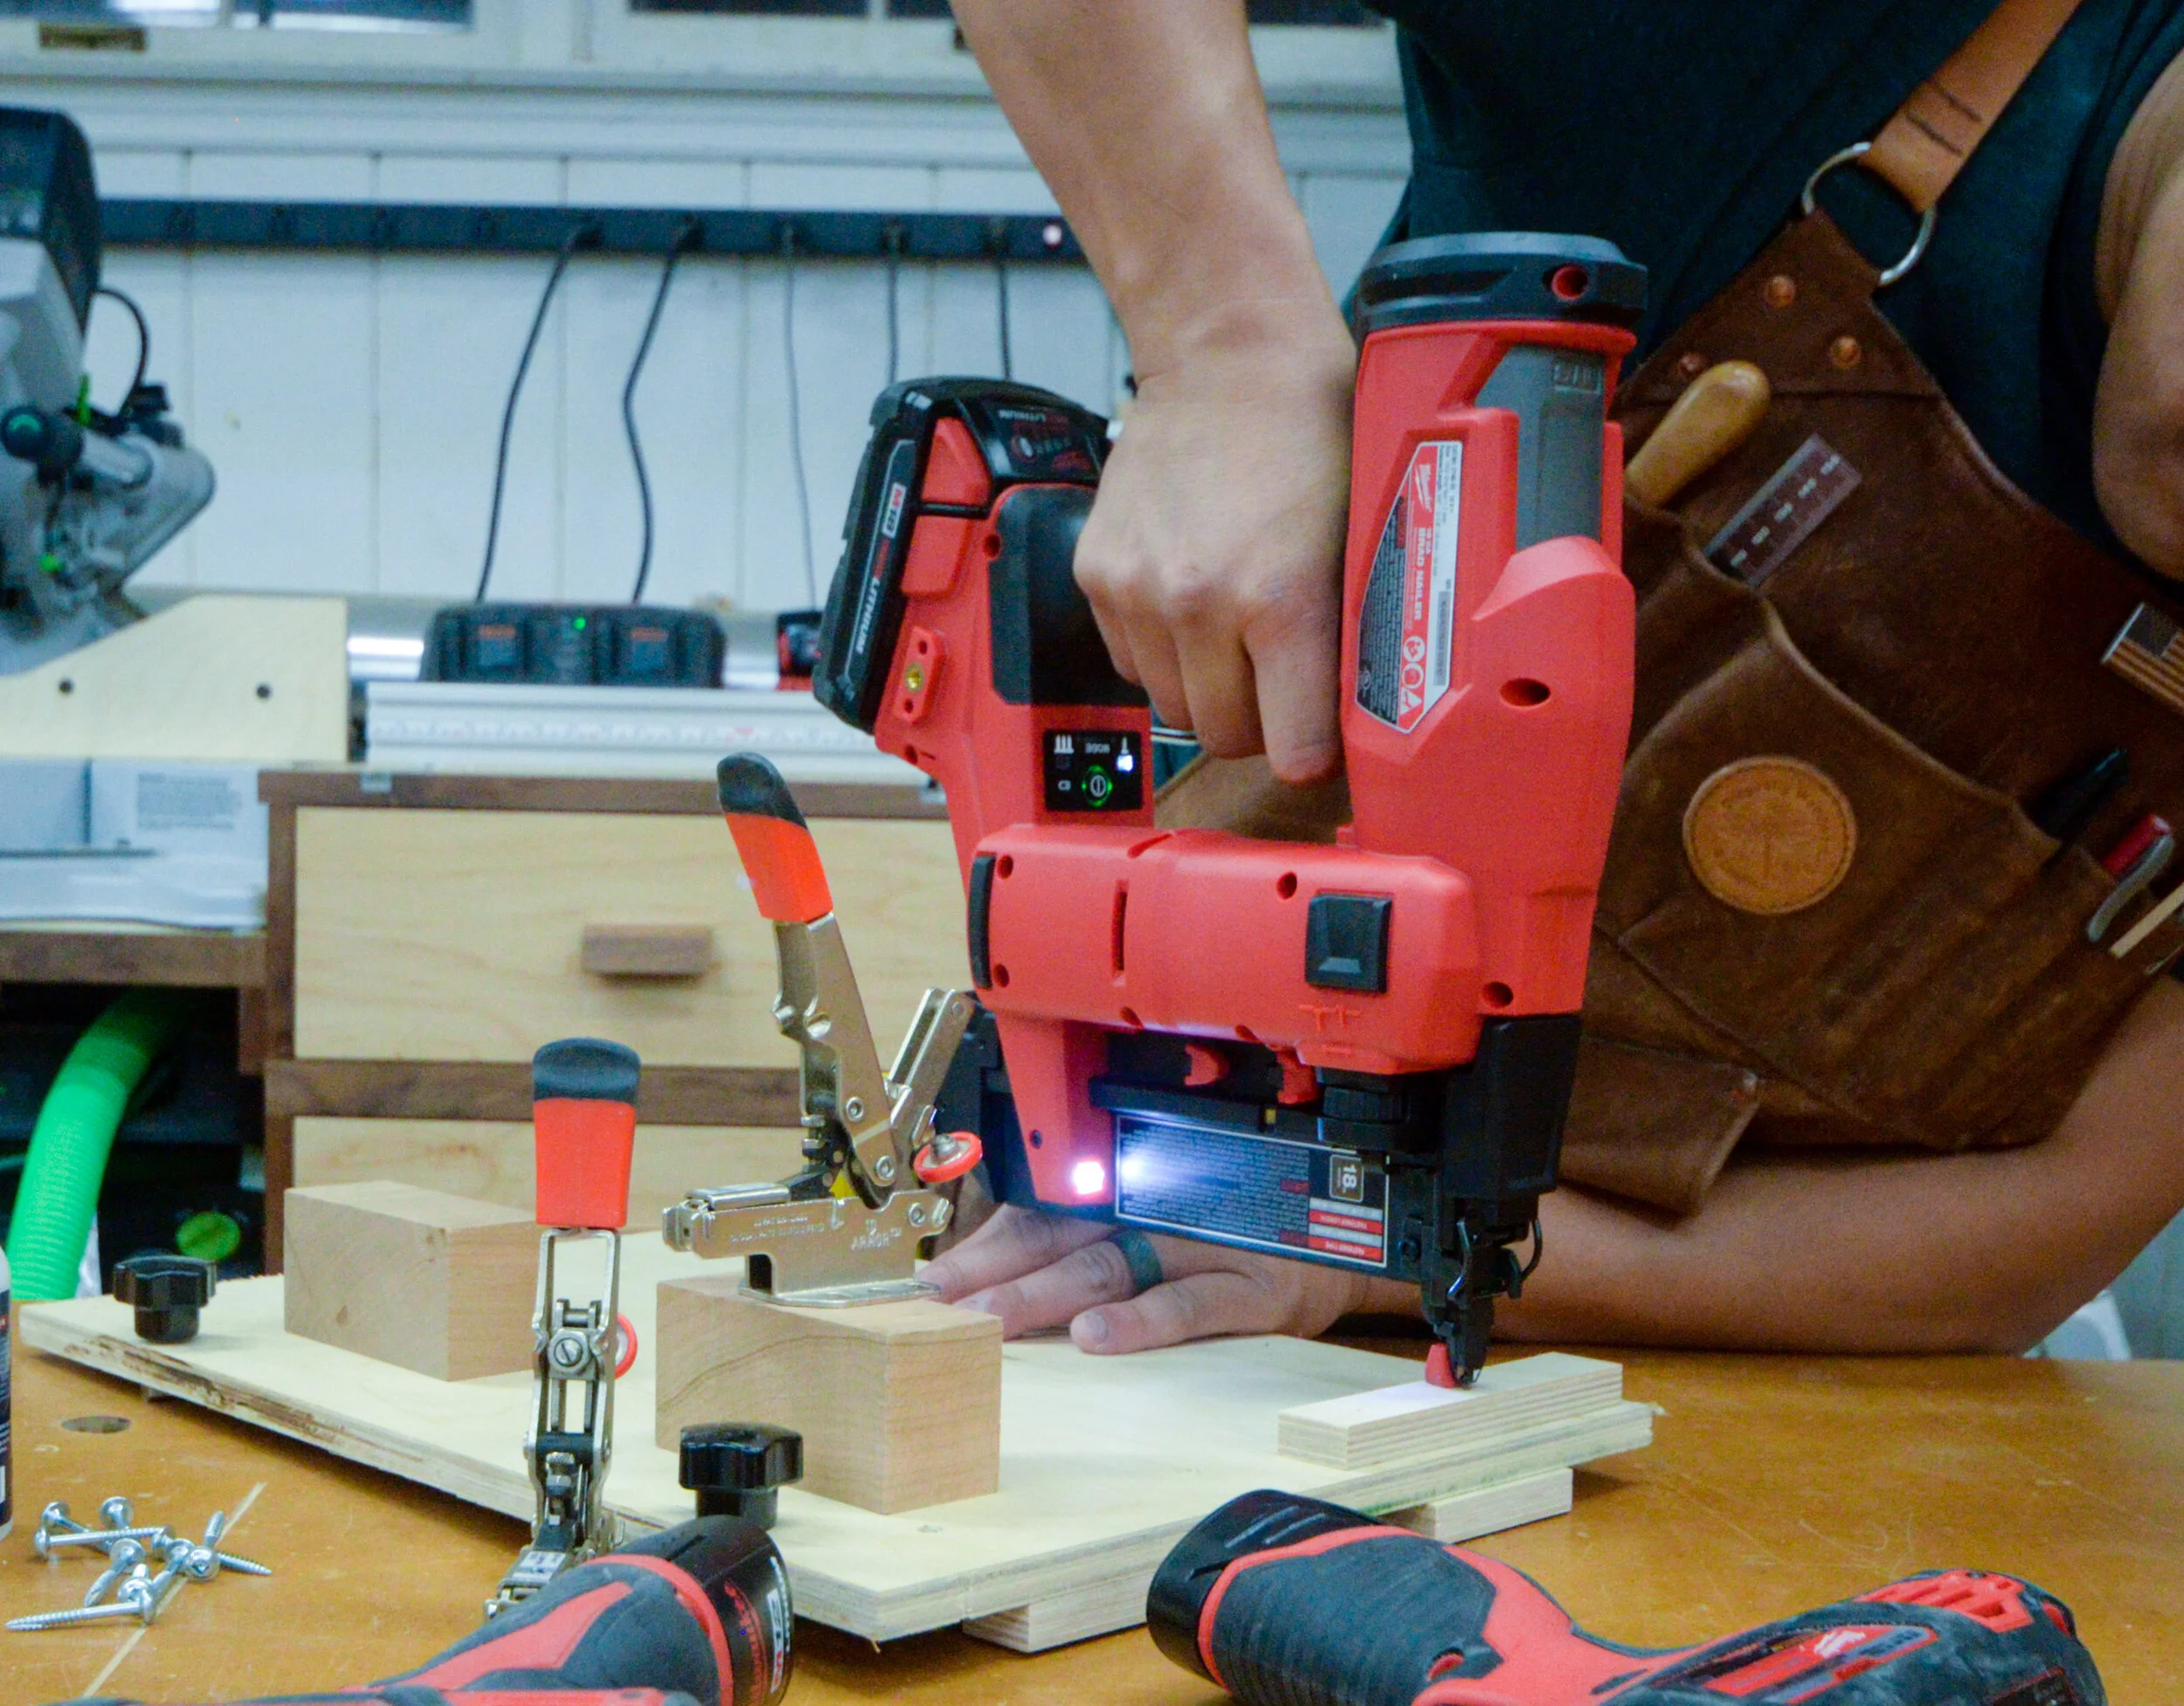
Using Milwaukee M18 brad nailer to attach stop blocks and support blocks
Now it’s back to bandsaw. With the template still attached to the pattern jig blank, I rough out the shape making sure to stay clear of the template by at least 1/8”. I then go to the router table and using a top bearing bit I pattern rout the template to the pattern jig.
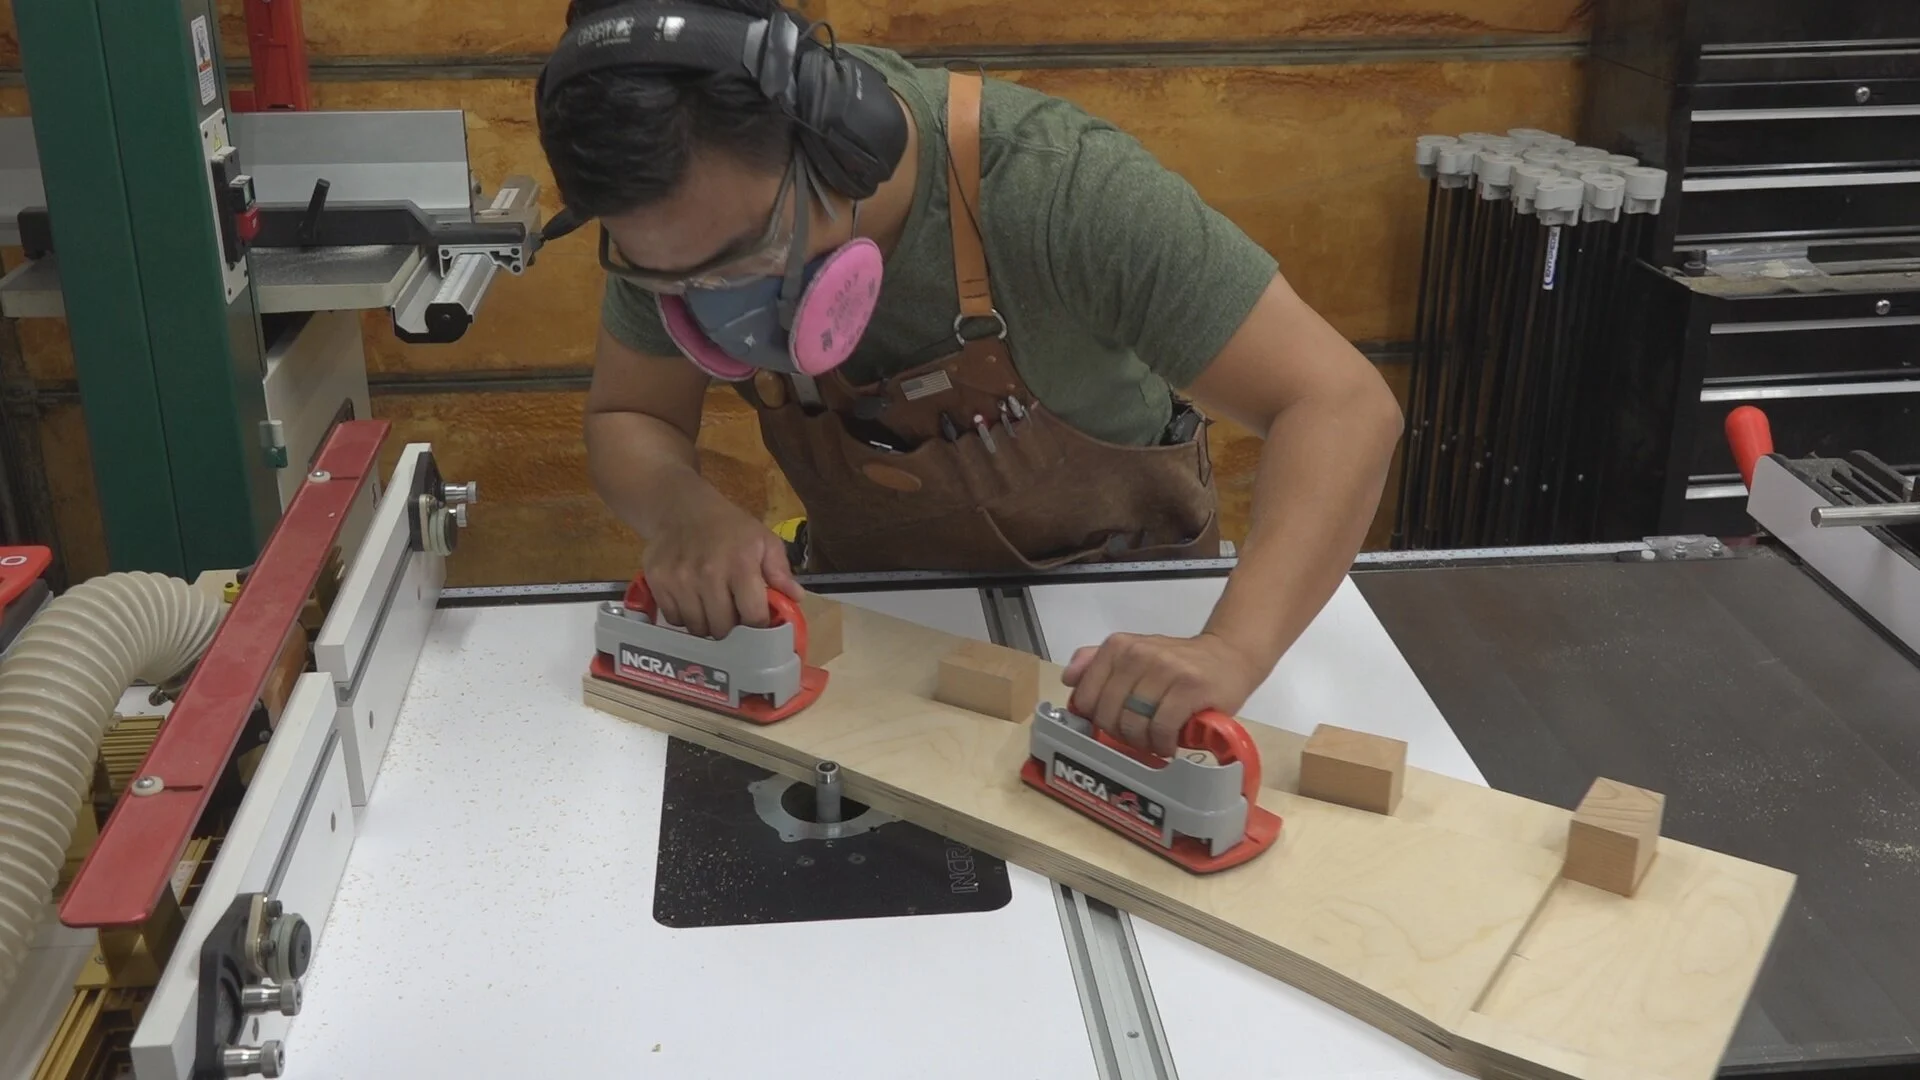
Pattern routing the template to the pattern routing jig using a top bearing bit in the router table
I'll now remove the temporarily held template from the pattern routing jig and attach toggle clamps to the work holding blocks using 1-1/2 inch screws. I want to make sure I predrill first before driving in the screws with my Milwaukee M12 FUEL SURGE 12-Volt Lithium-Ion Brushless Cordless 1/4 in. Hex Impact Driver
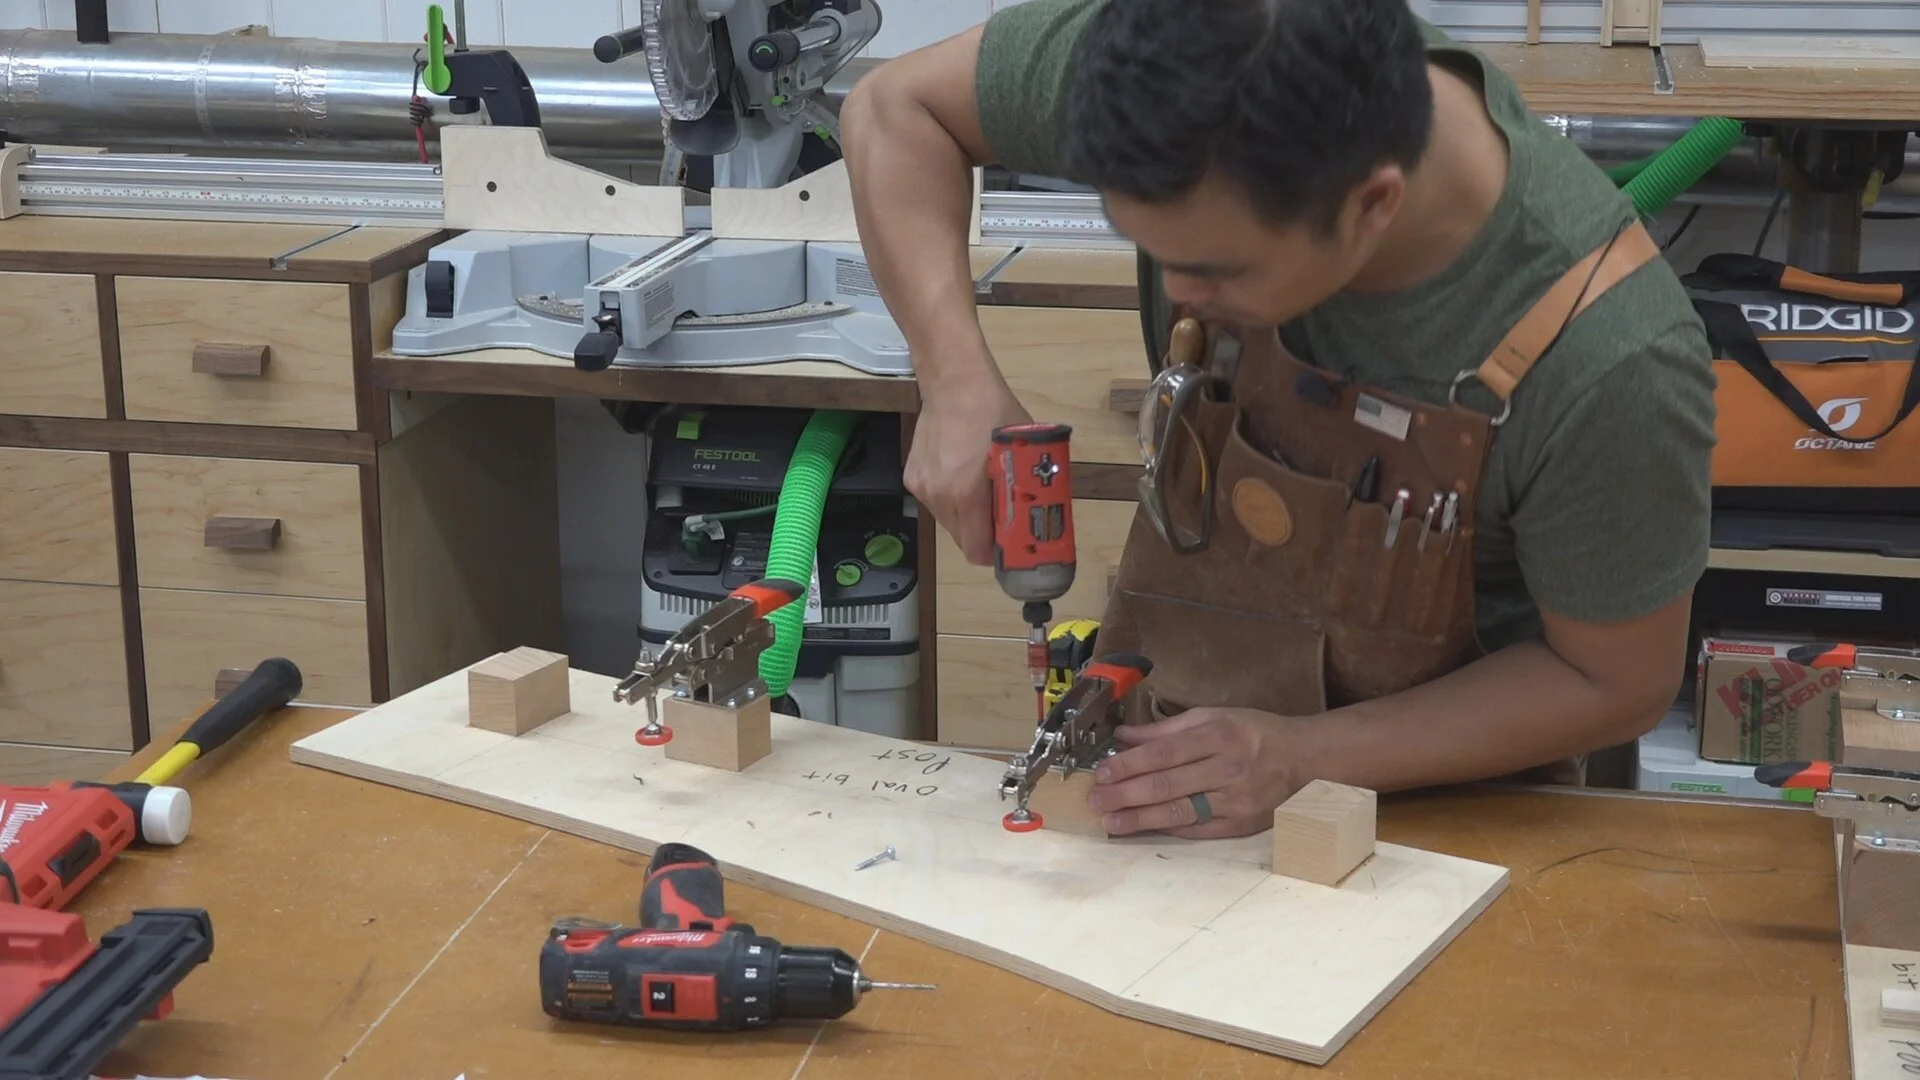
Attaching toggle clamps to the pattern routing jig by predrilling and driving 1-1/2 inch screws
Now it’s time to start shaping the actual workpiece. Not only do I have a tracing template, but I also have a pattern routing jig to make exact copies of my furniture parts.
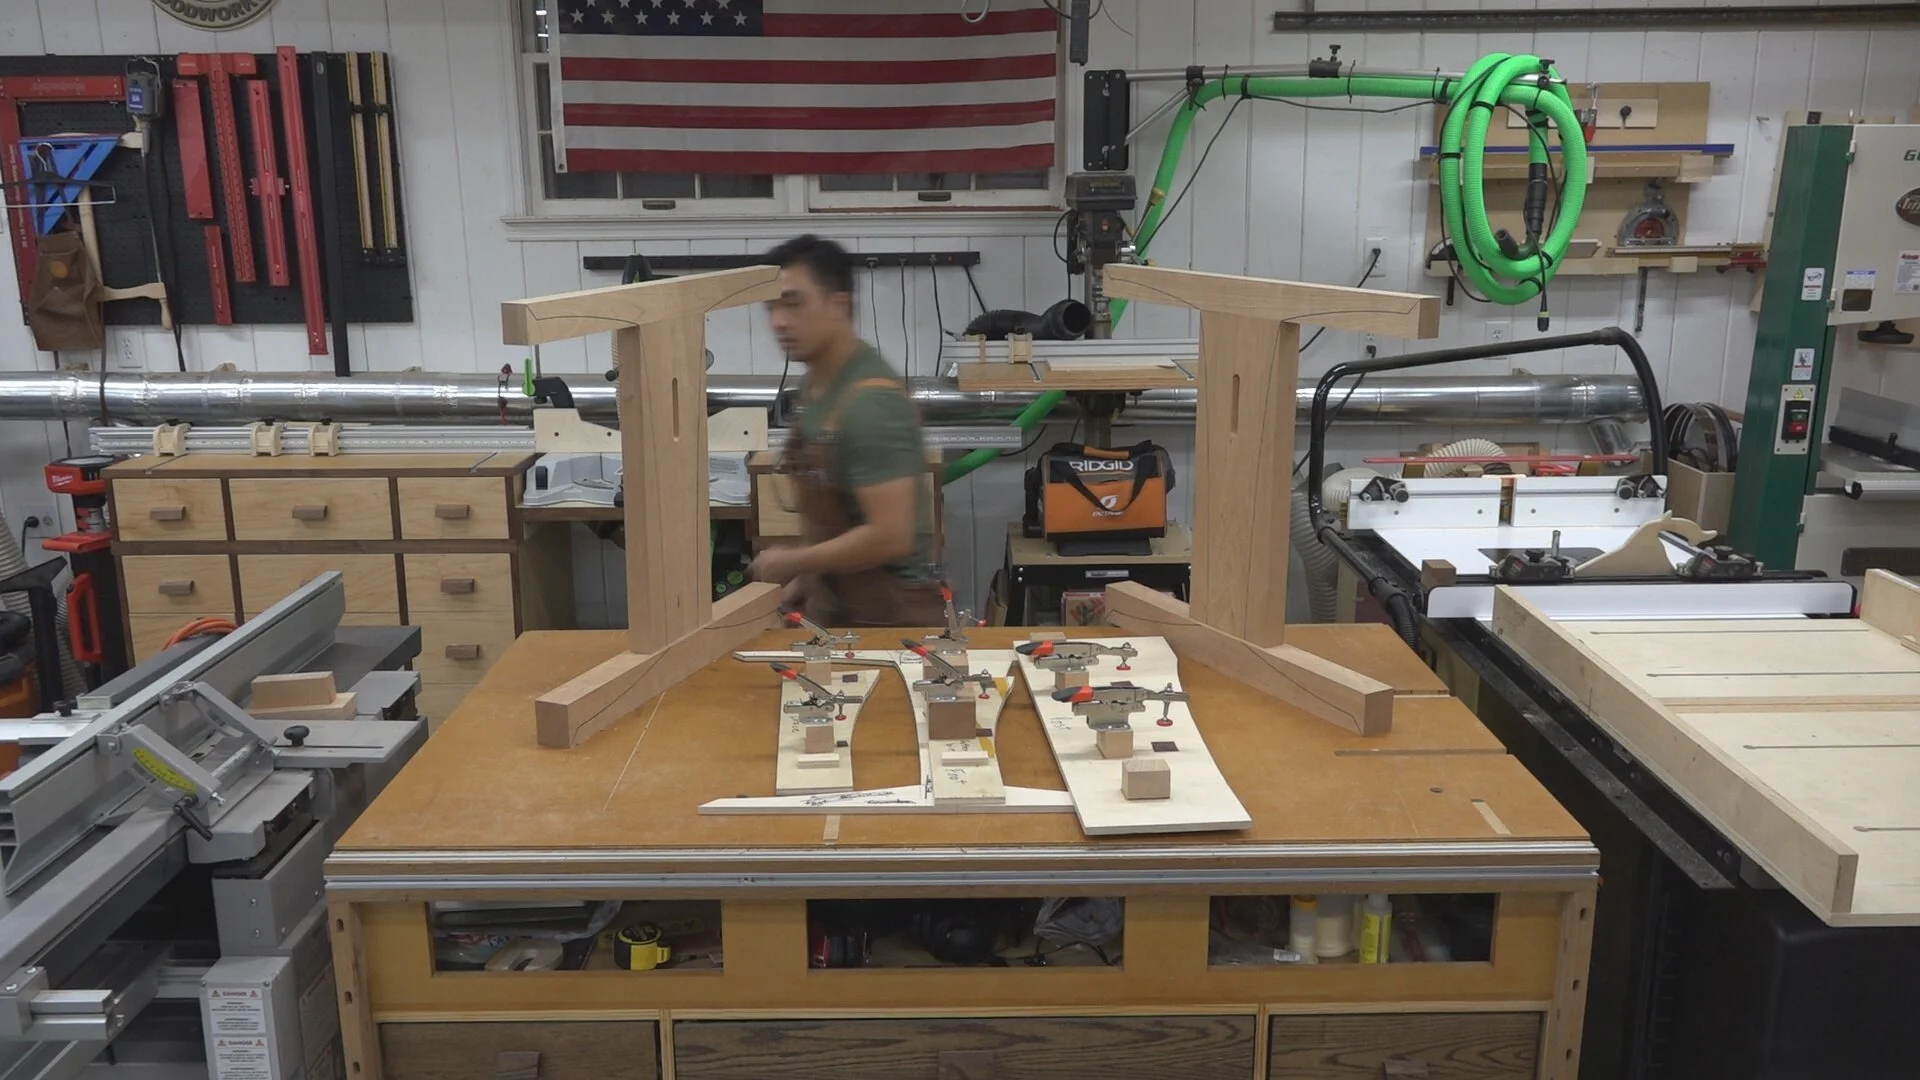
Pattern routing jigs and templates
So now I just repeat the process over again but with the actual workpiece. First I’ll trace out the template on the workpiece. Then I’ll rough out the shape on the bandsaw. Next I’ll pattern rout using the pattern routing jig and this time, a bottom bearing bit on the router table.
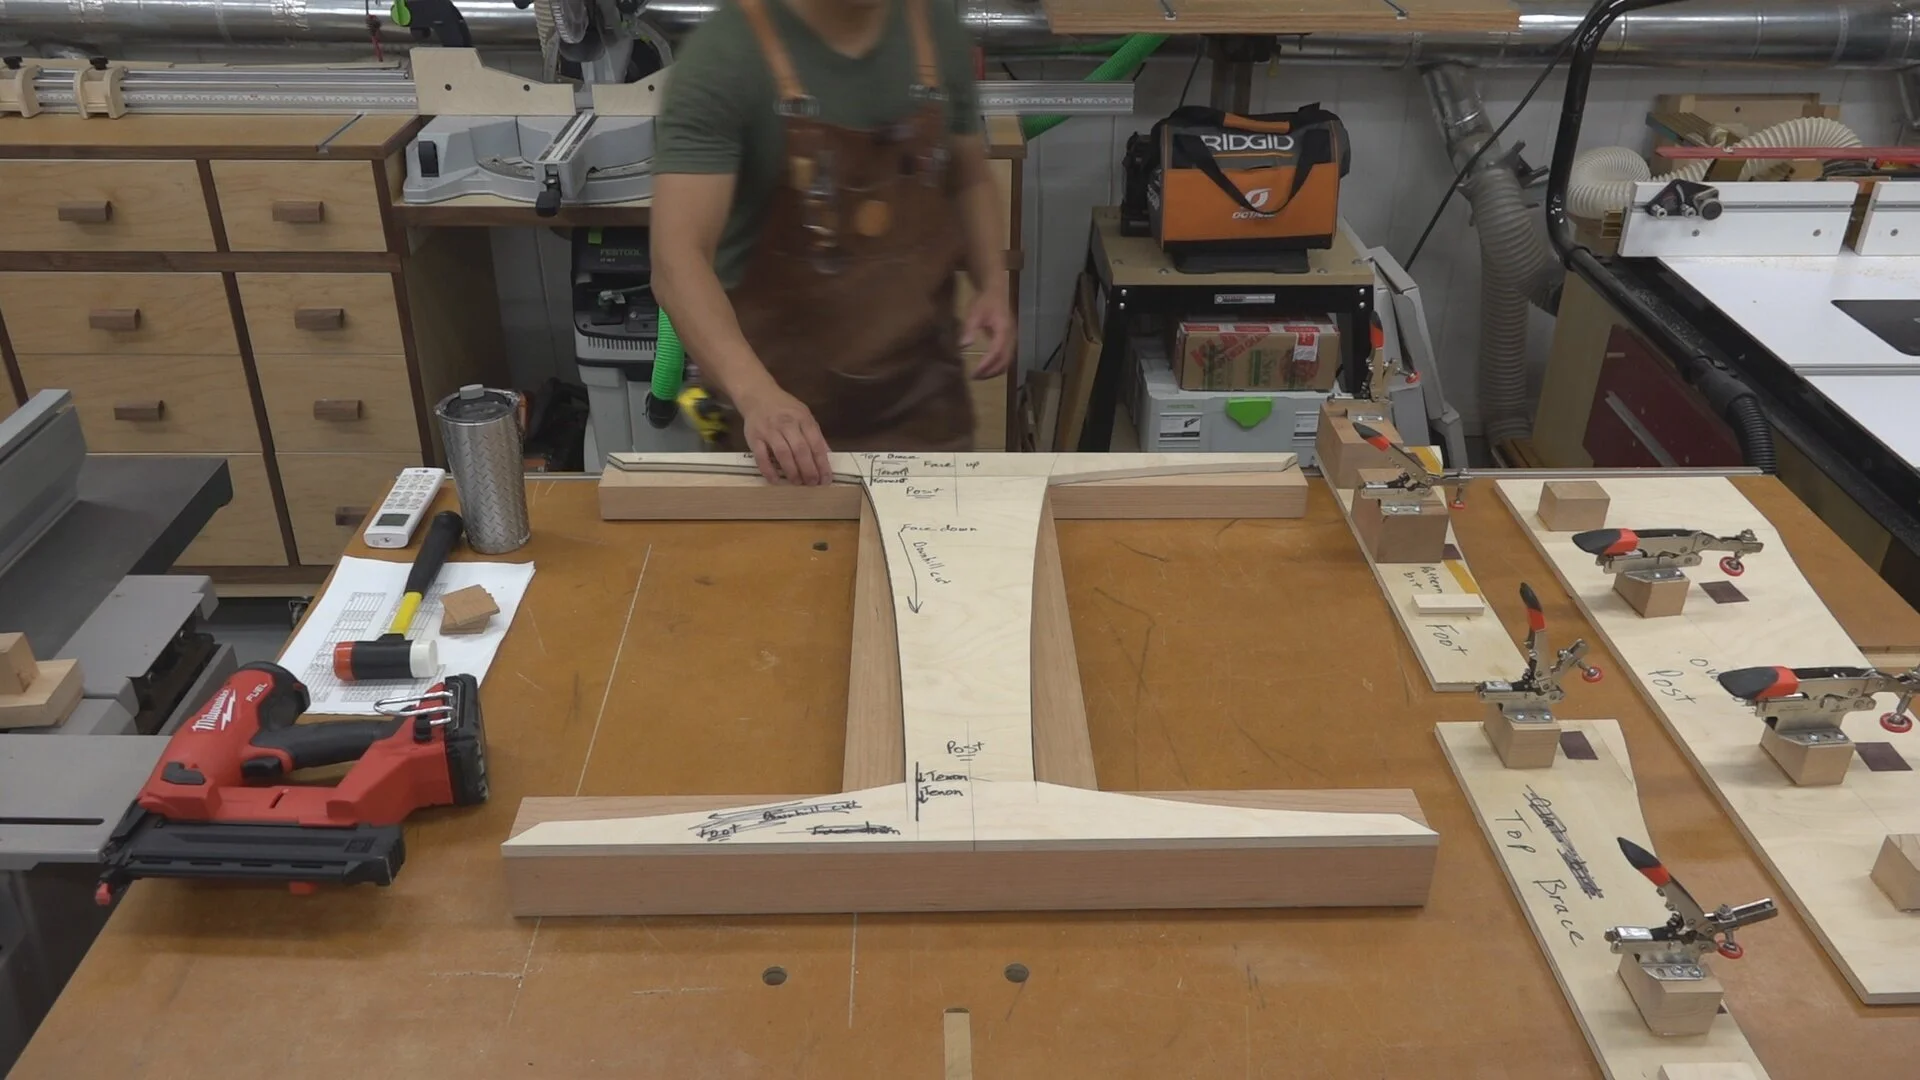
Tracing out the template
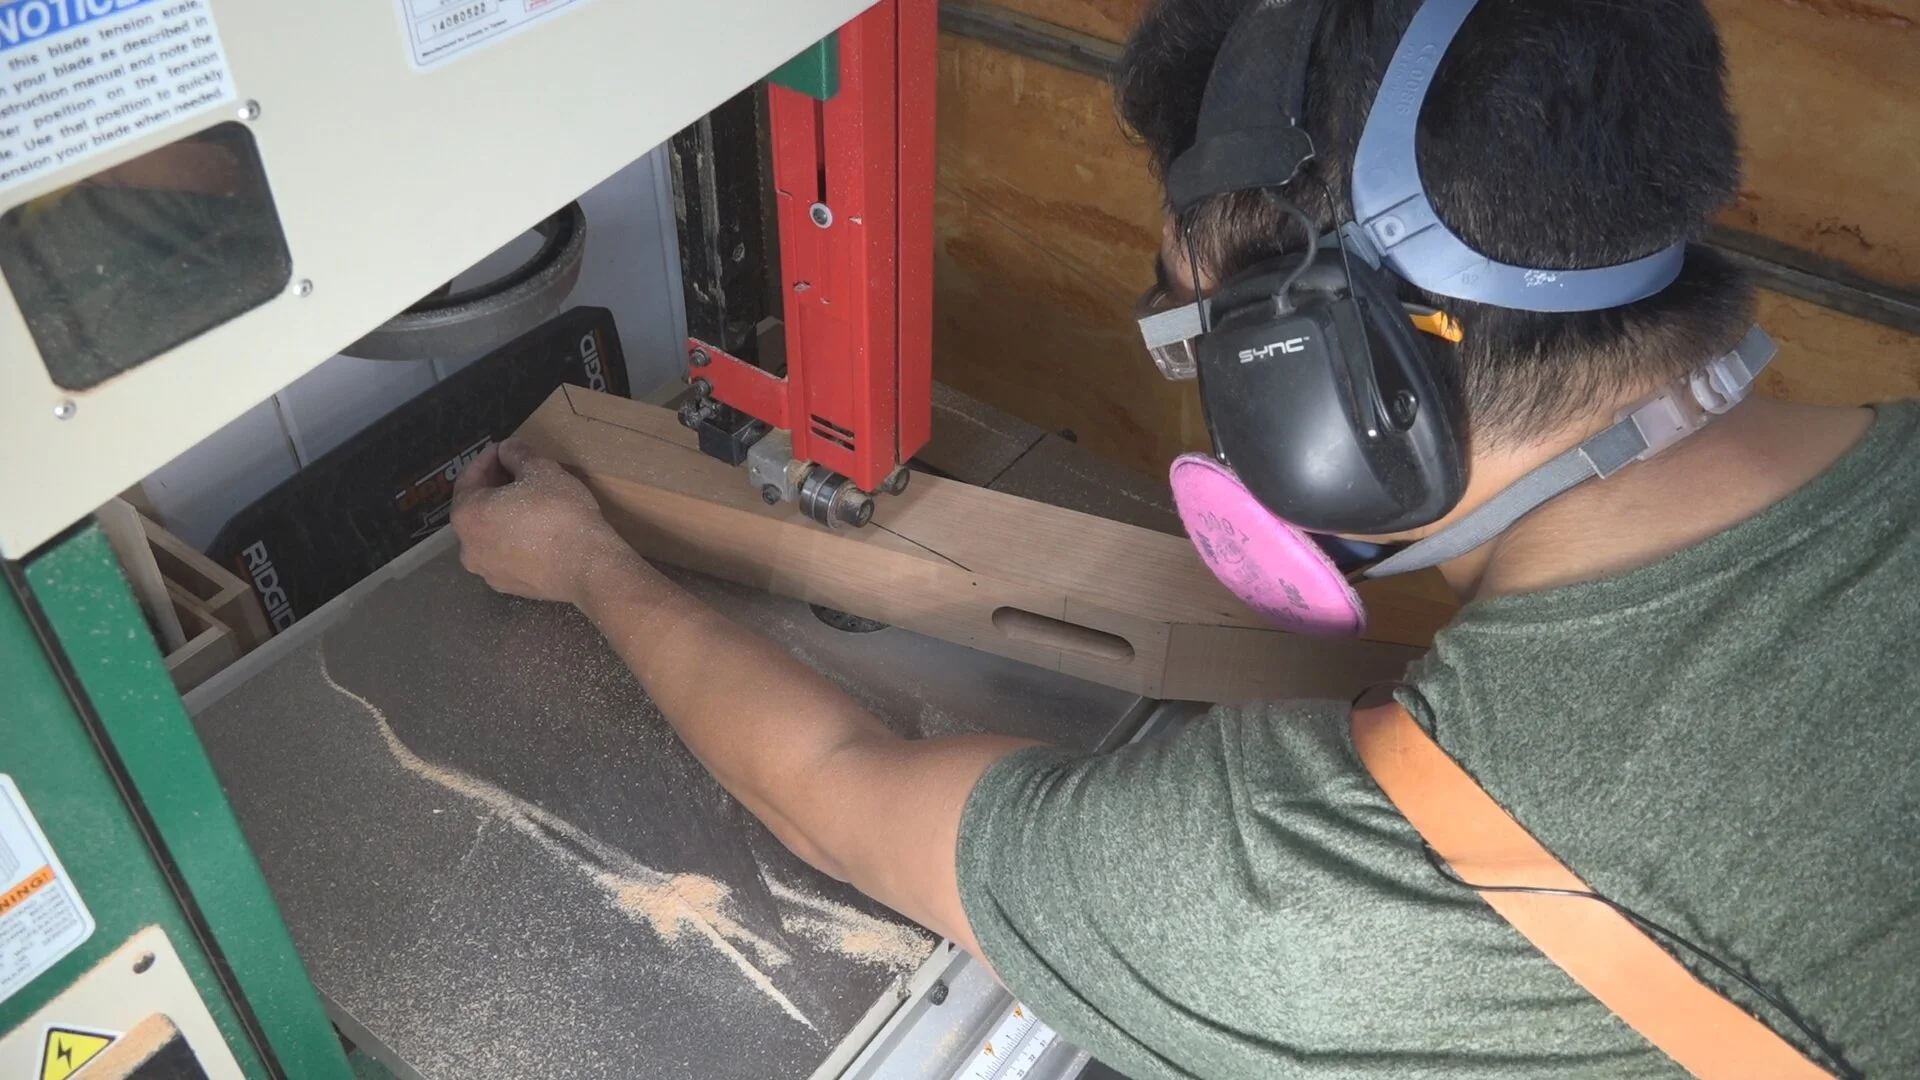
Rouging out the shape on the bandsaw
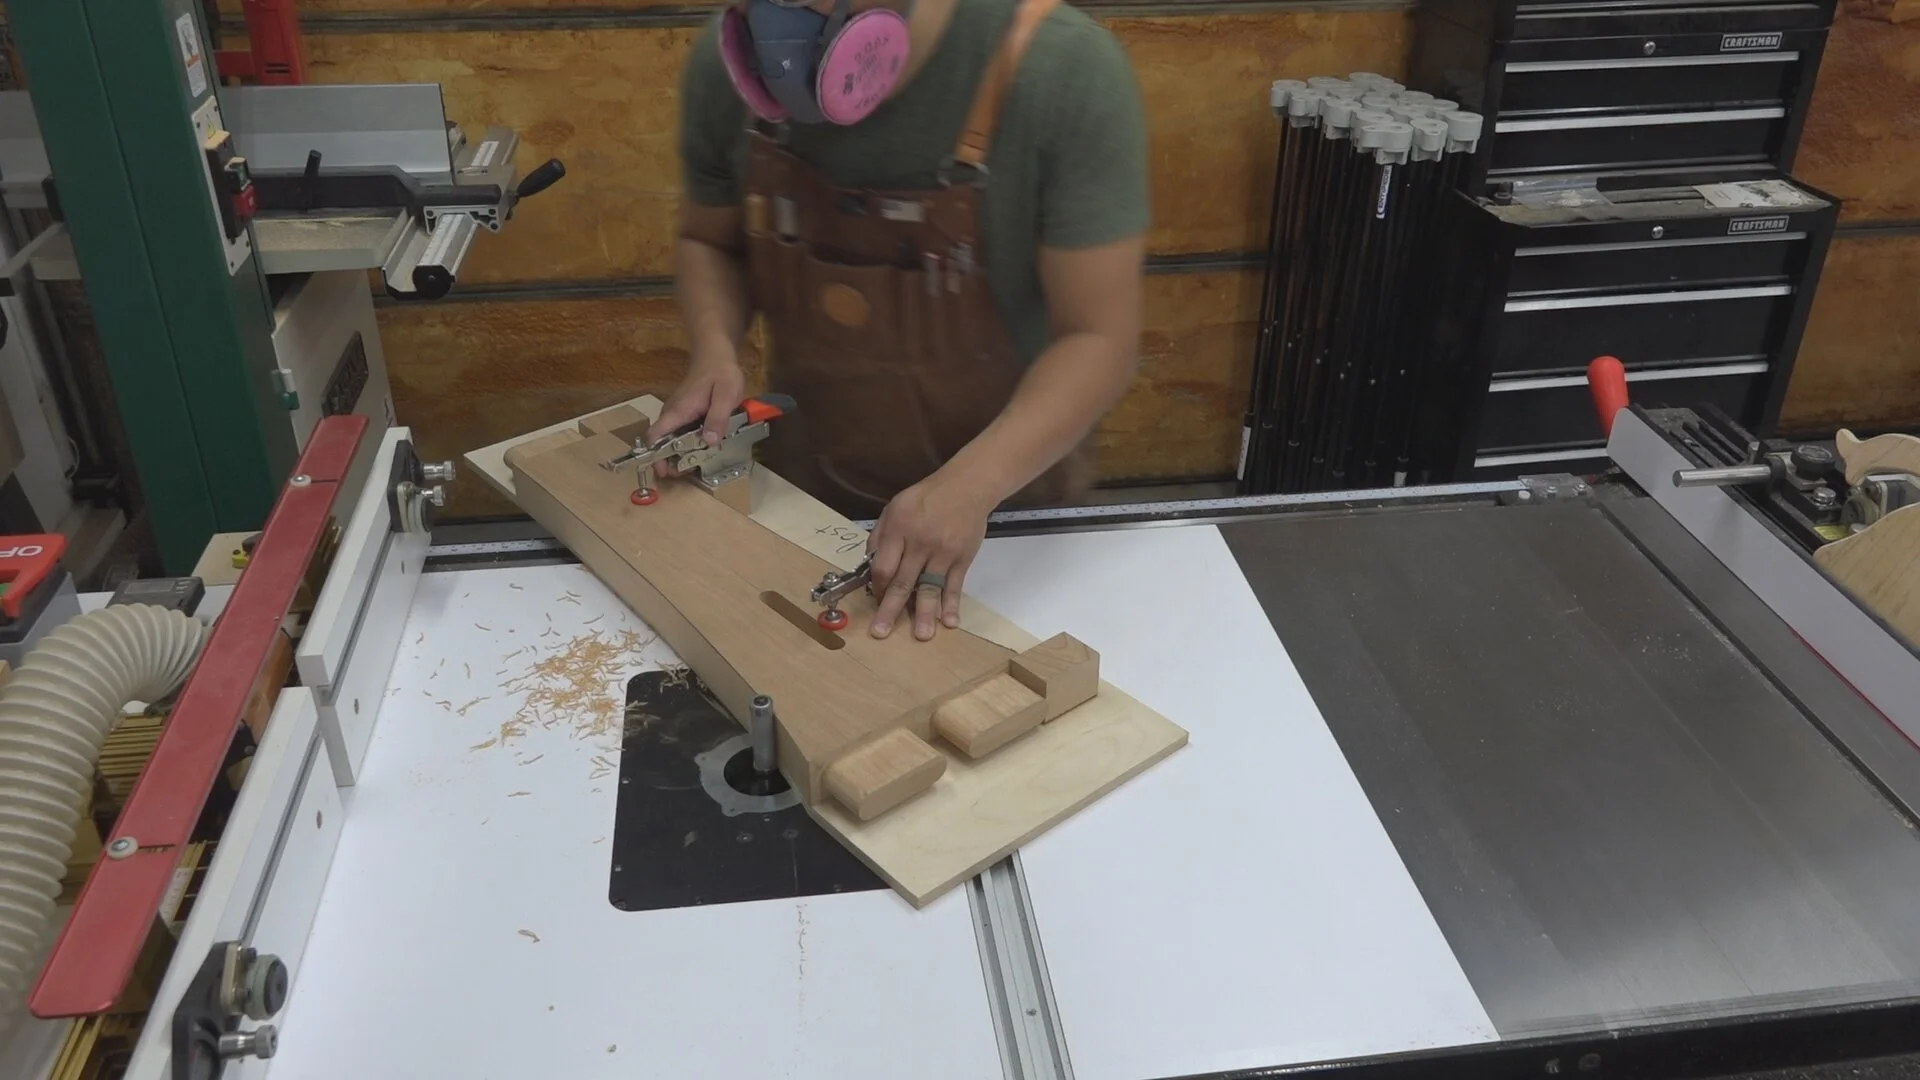
Pattern routing on the router table using a bottom bearing bit
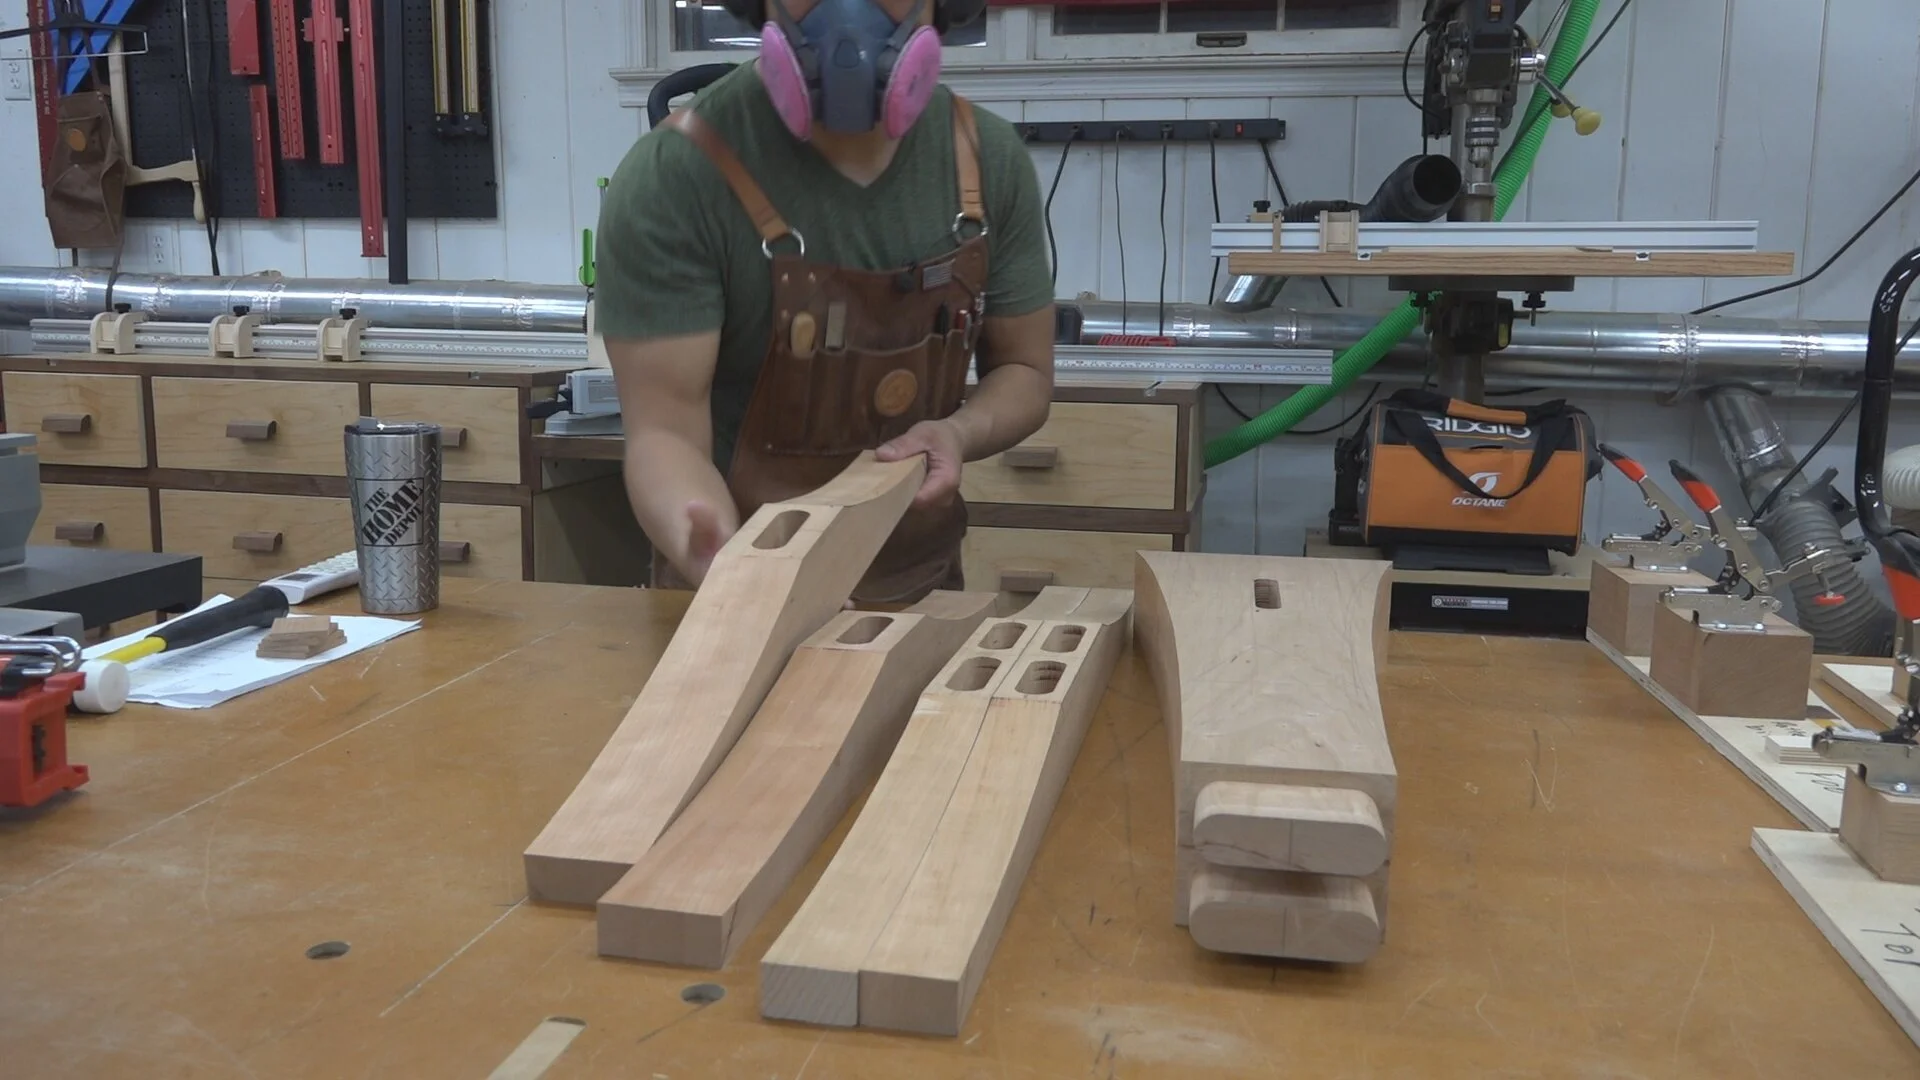
Multiple exact copies can now be produced
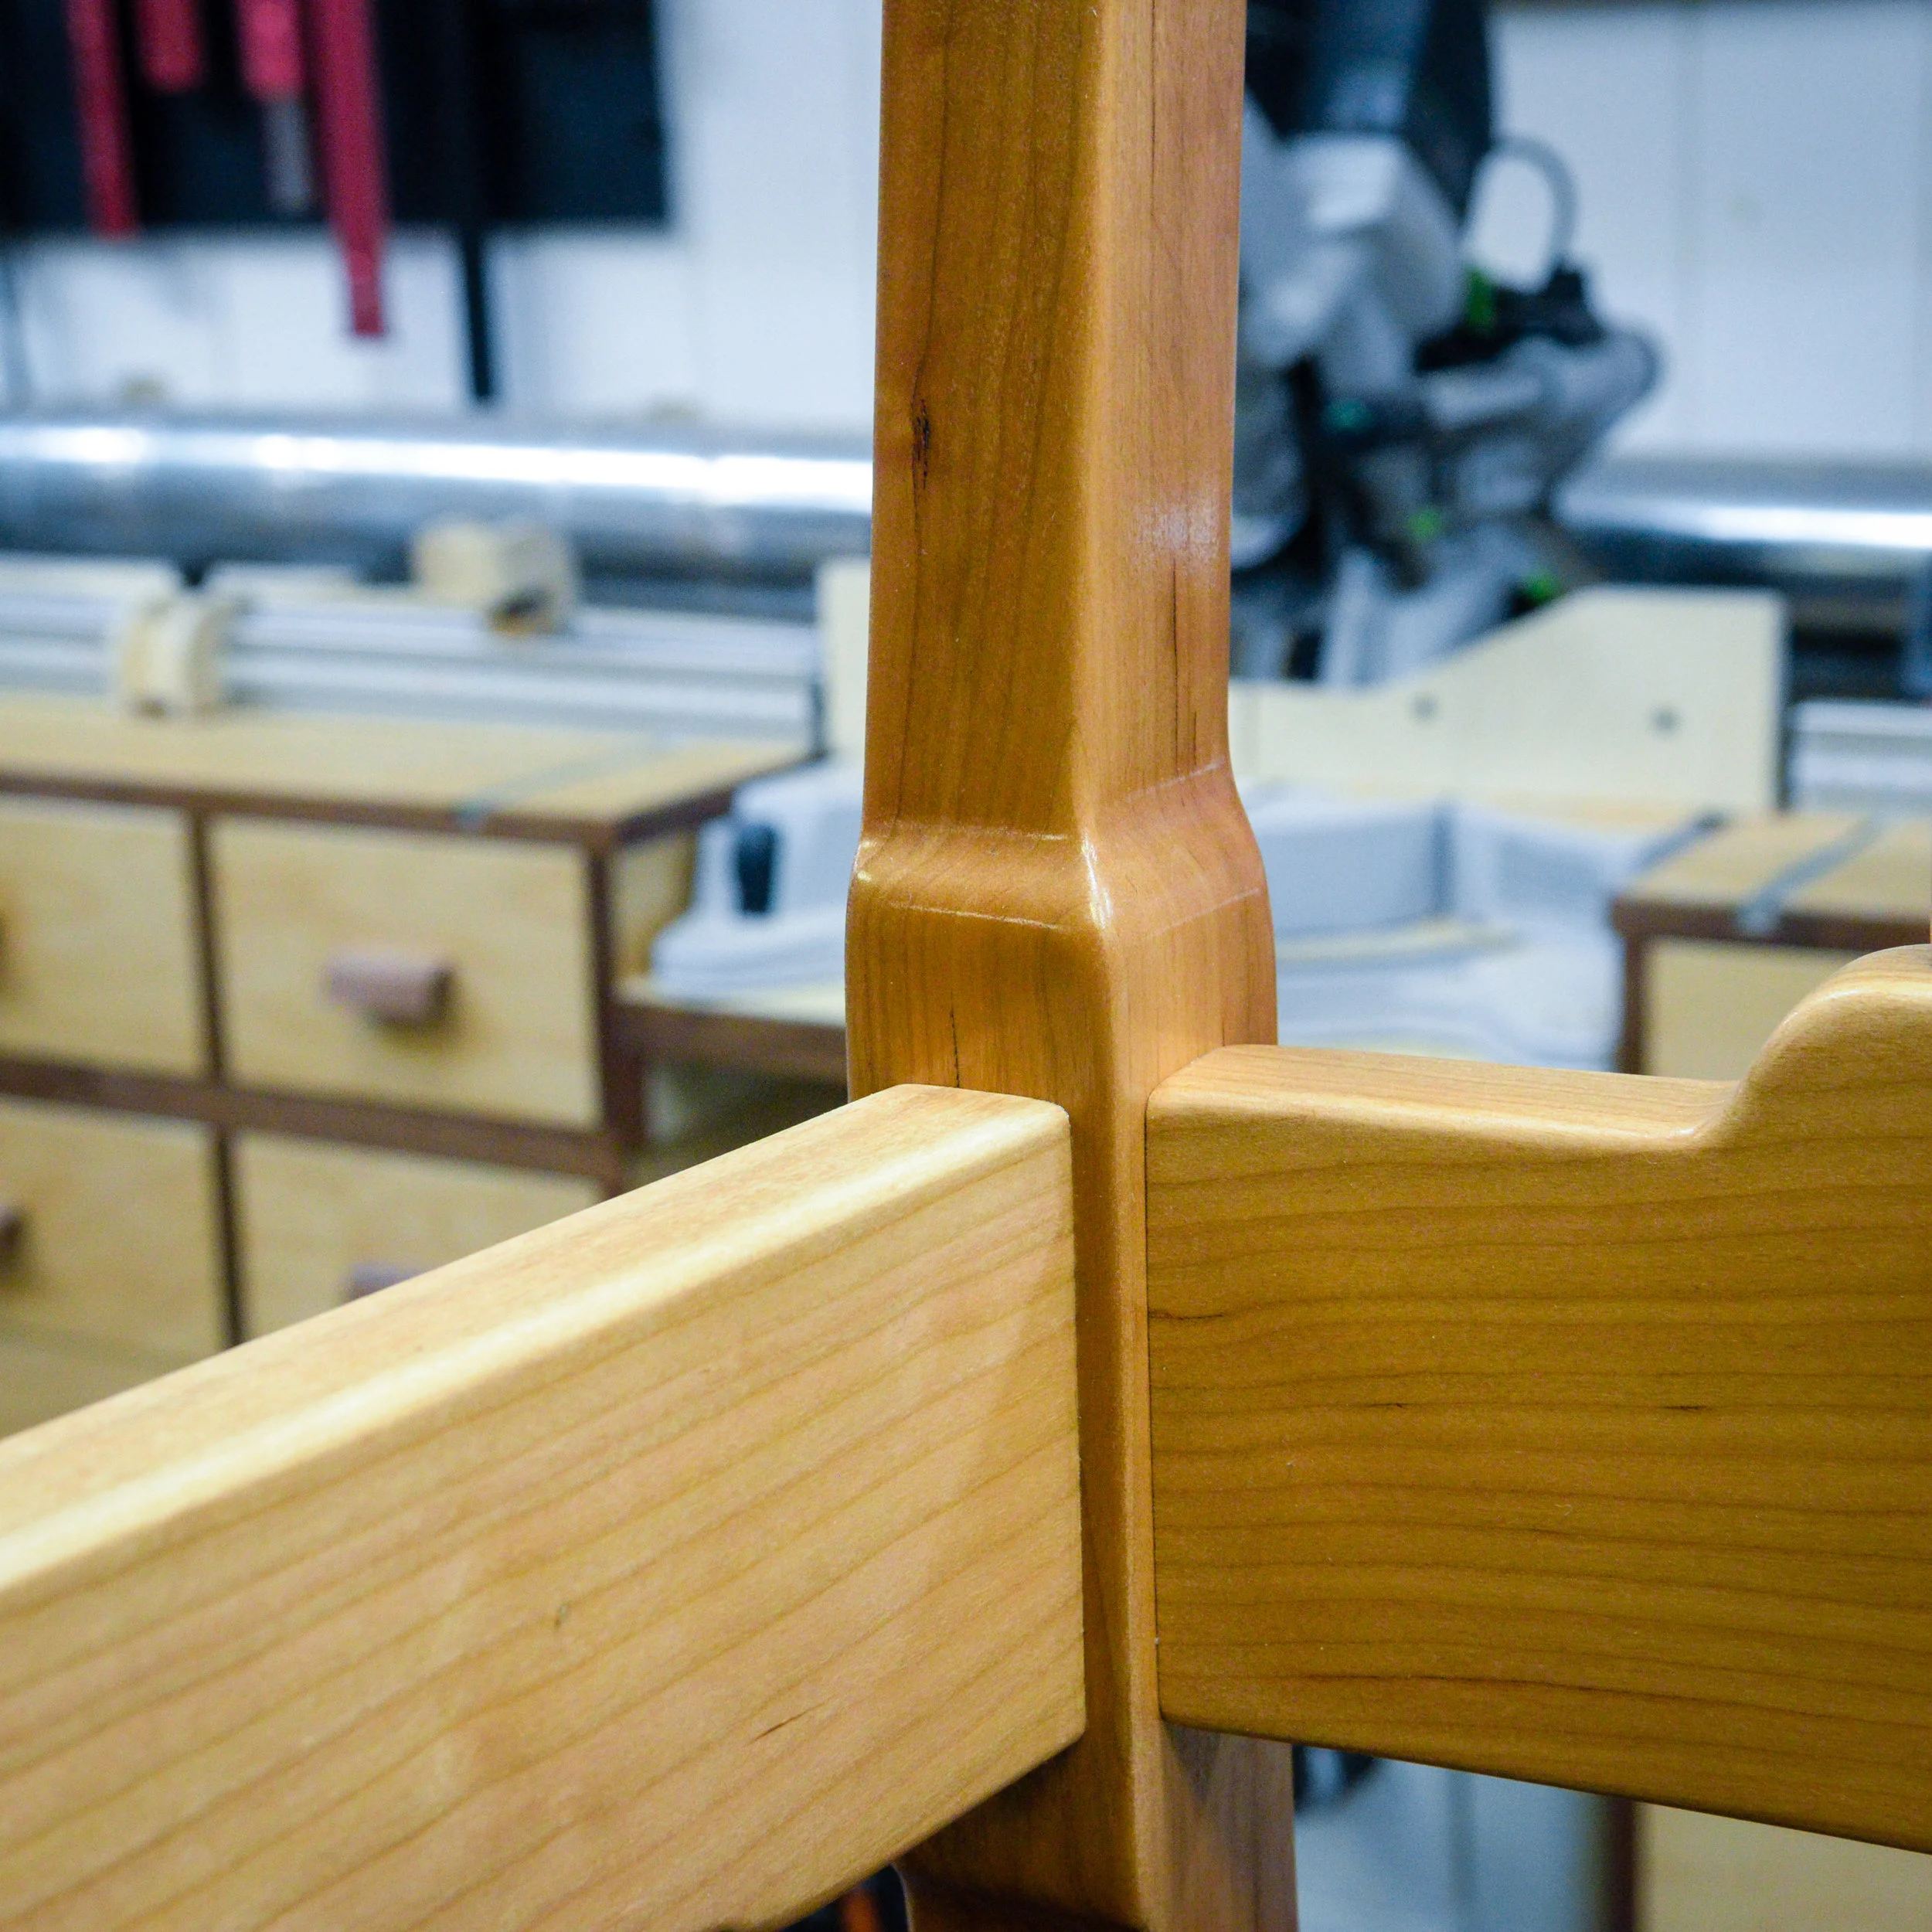
Interior Cloud Lifts on Chair Legs
The interior cloud lifts on the rear legs are shaped using both power tools and hand tools. However, after performing this operation, I realized that the use of a rotary tool may have made my work a lot easier. I’ll discuss that later. First, let me explain how I manufactured this detail.
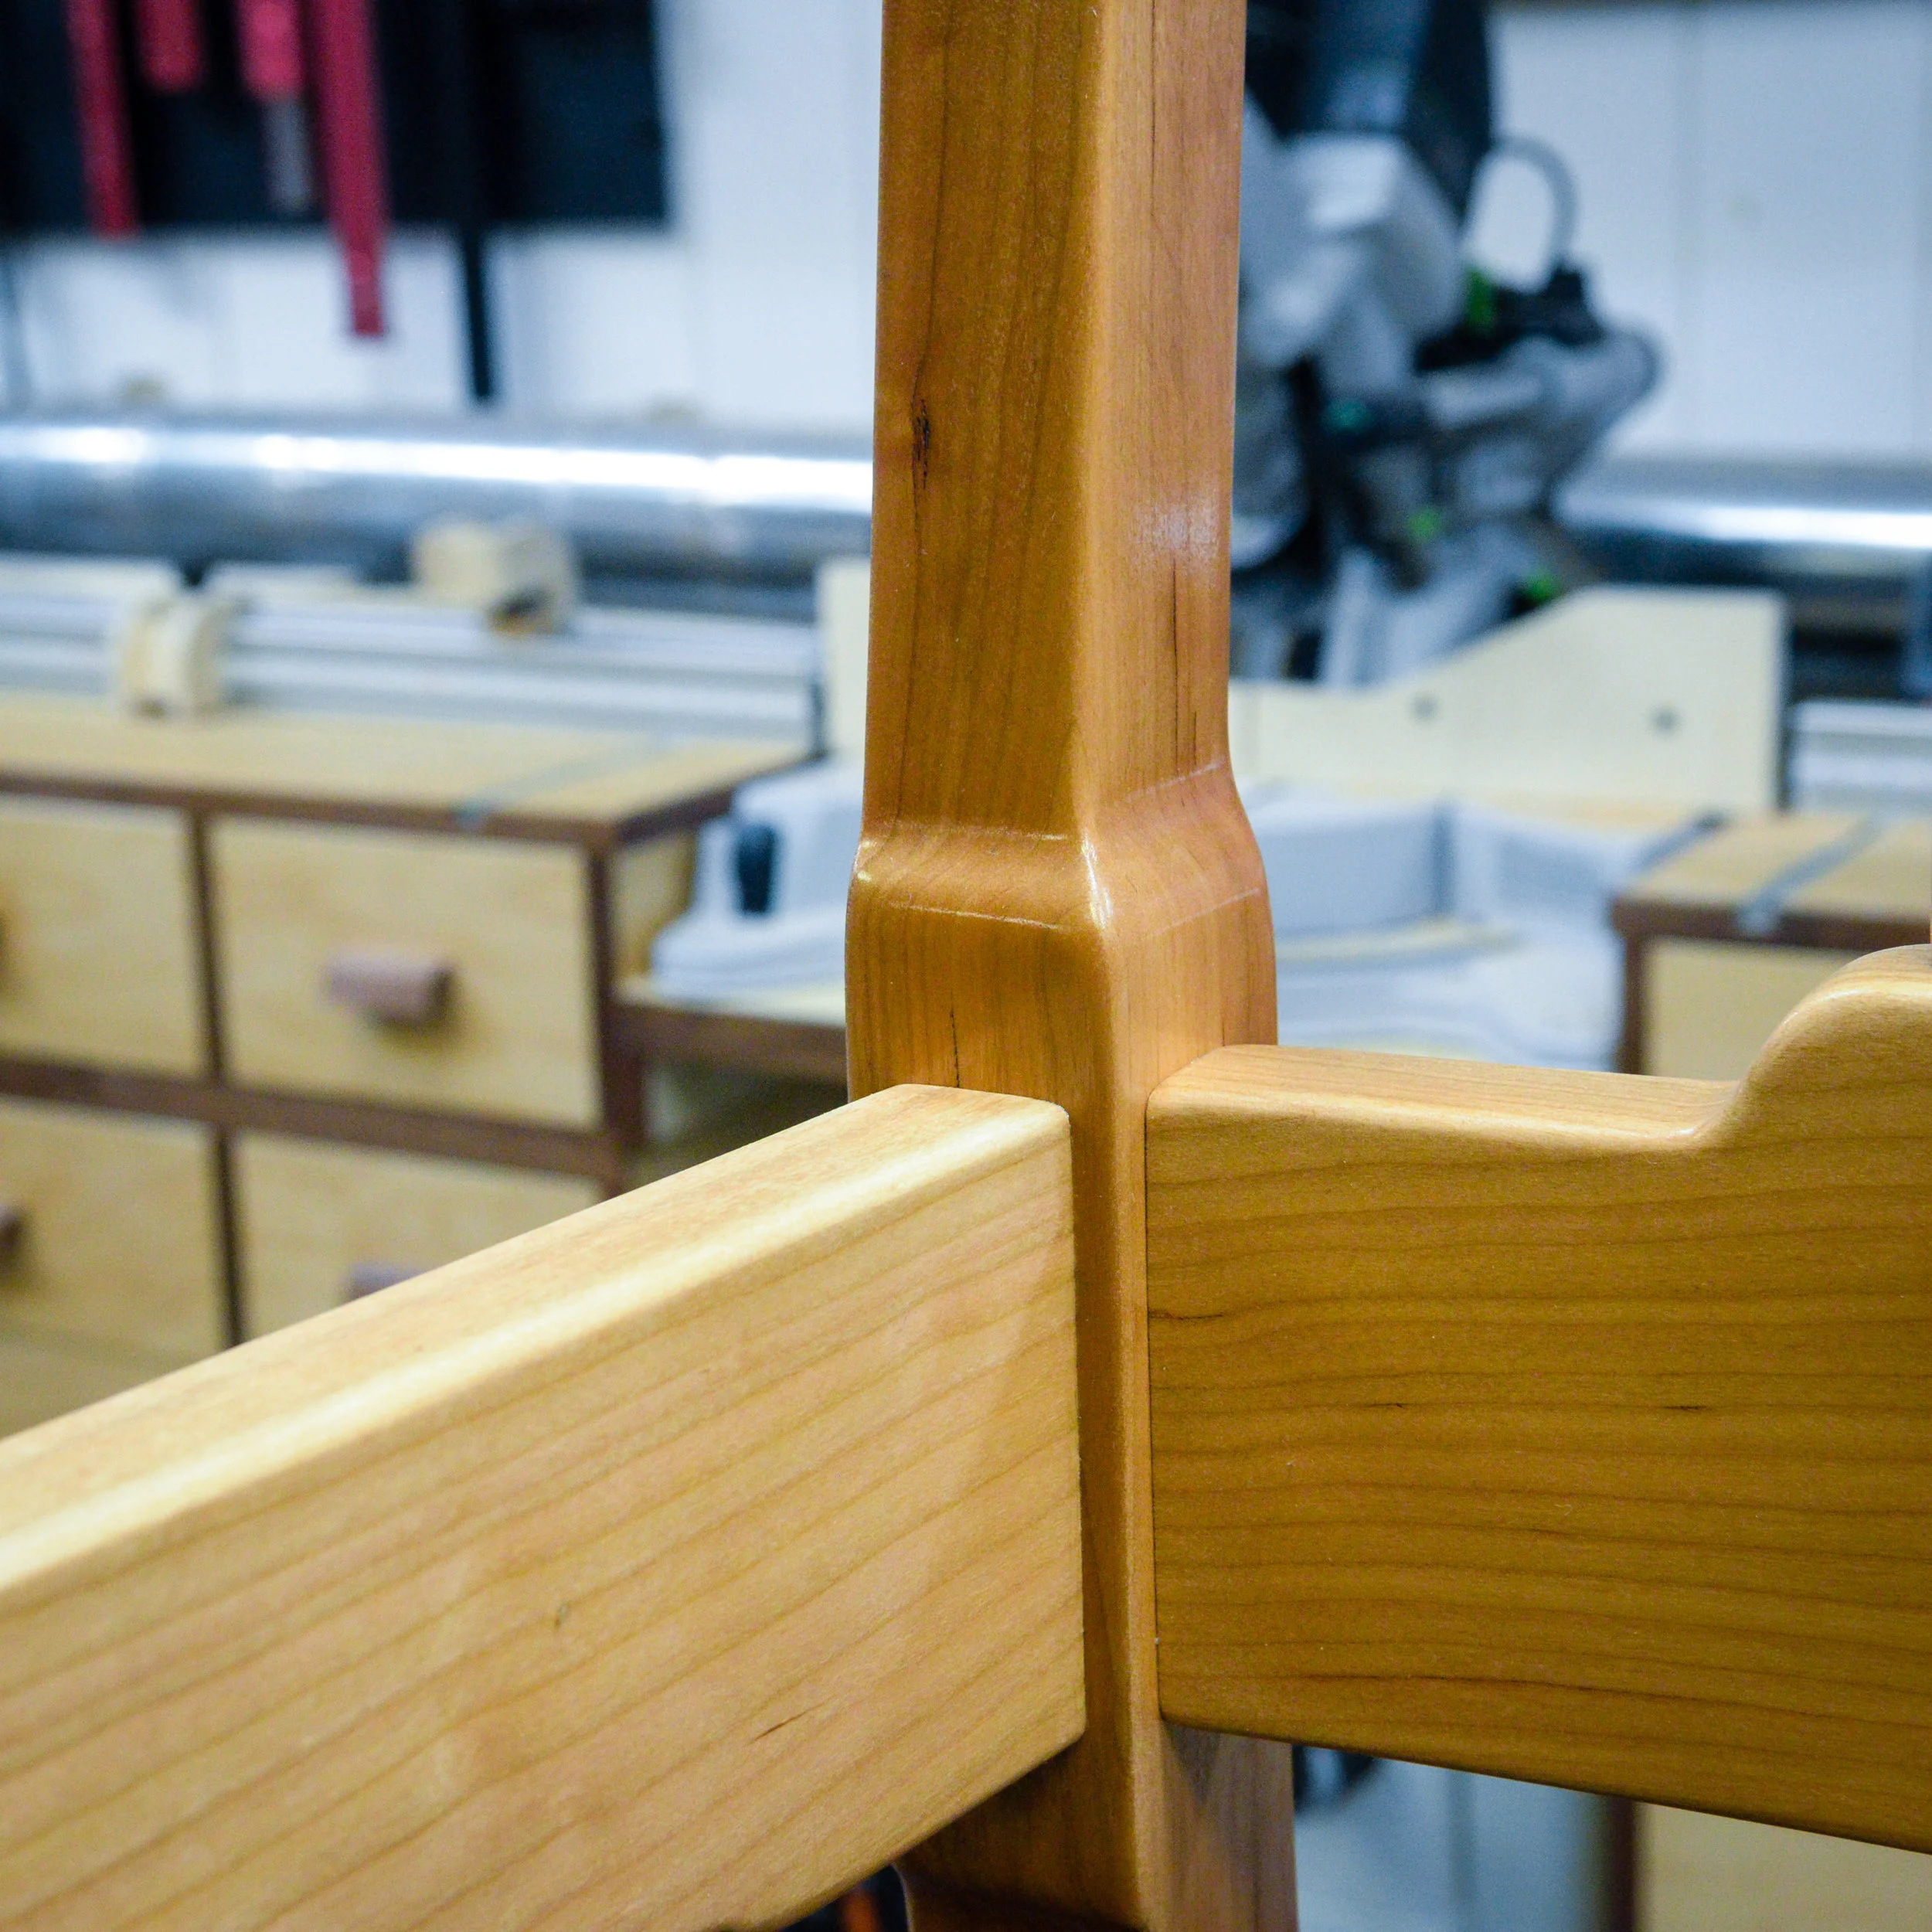
The cloud lifts seen on the rear legs of chairs I recently made
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
The interior cloud lifts on the rear legs are shaped using both power tools and hand tools. However, after performing this operation, I realized that the use of a rotary tool may have made my work a lot easier. I’ll discuss that later. First, let me explain how I manufactured this detail.
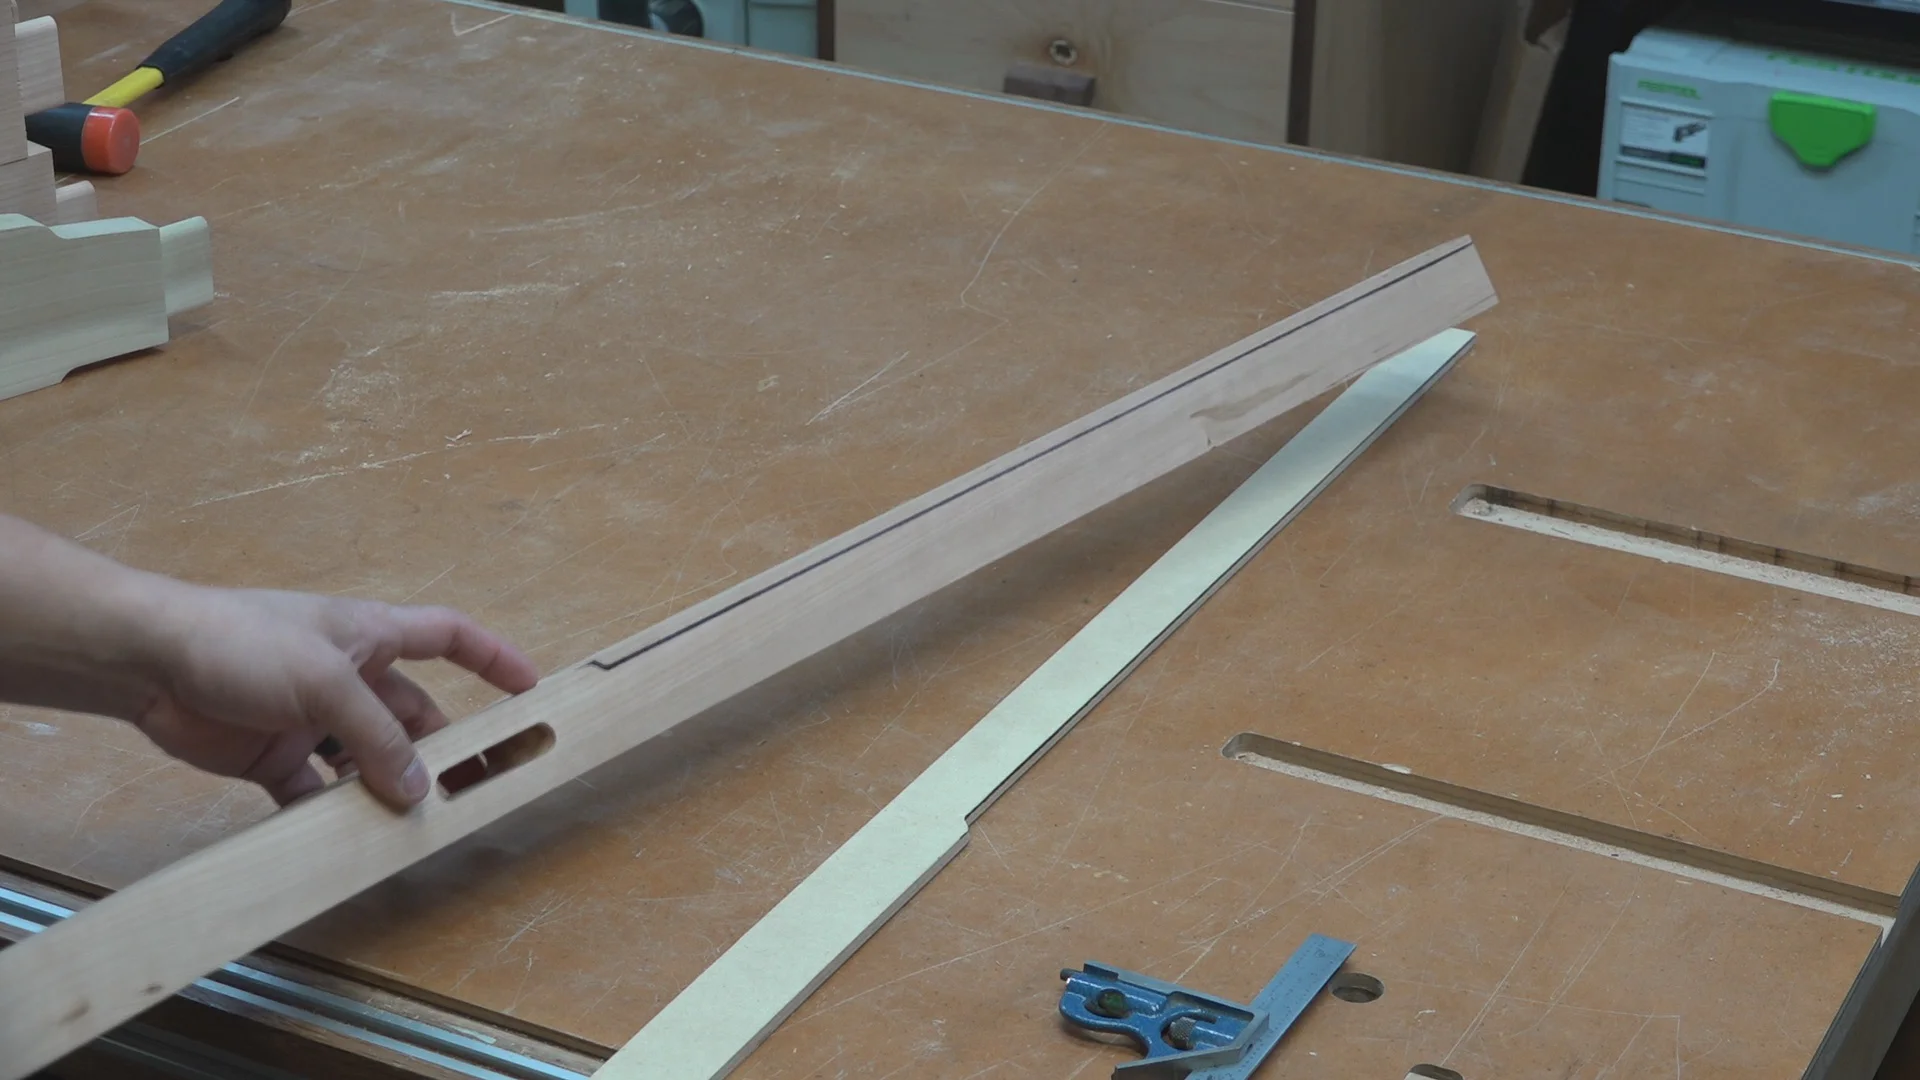
I first traced the outline of the cloud lift using a 1/4” MDF template. The 1/4” MDF is flexible making it easier to contour the template to the arc of the rear leg as I trace the outline.
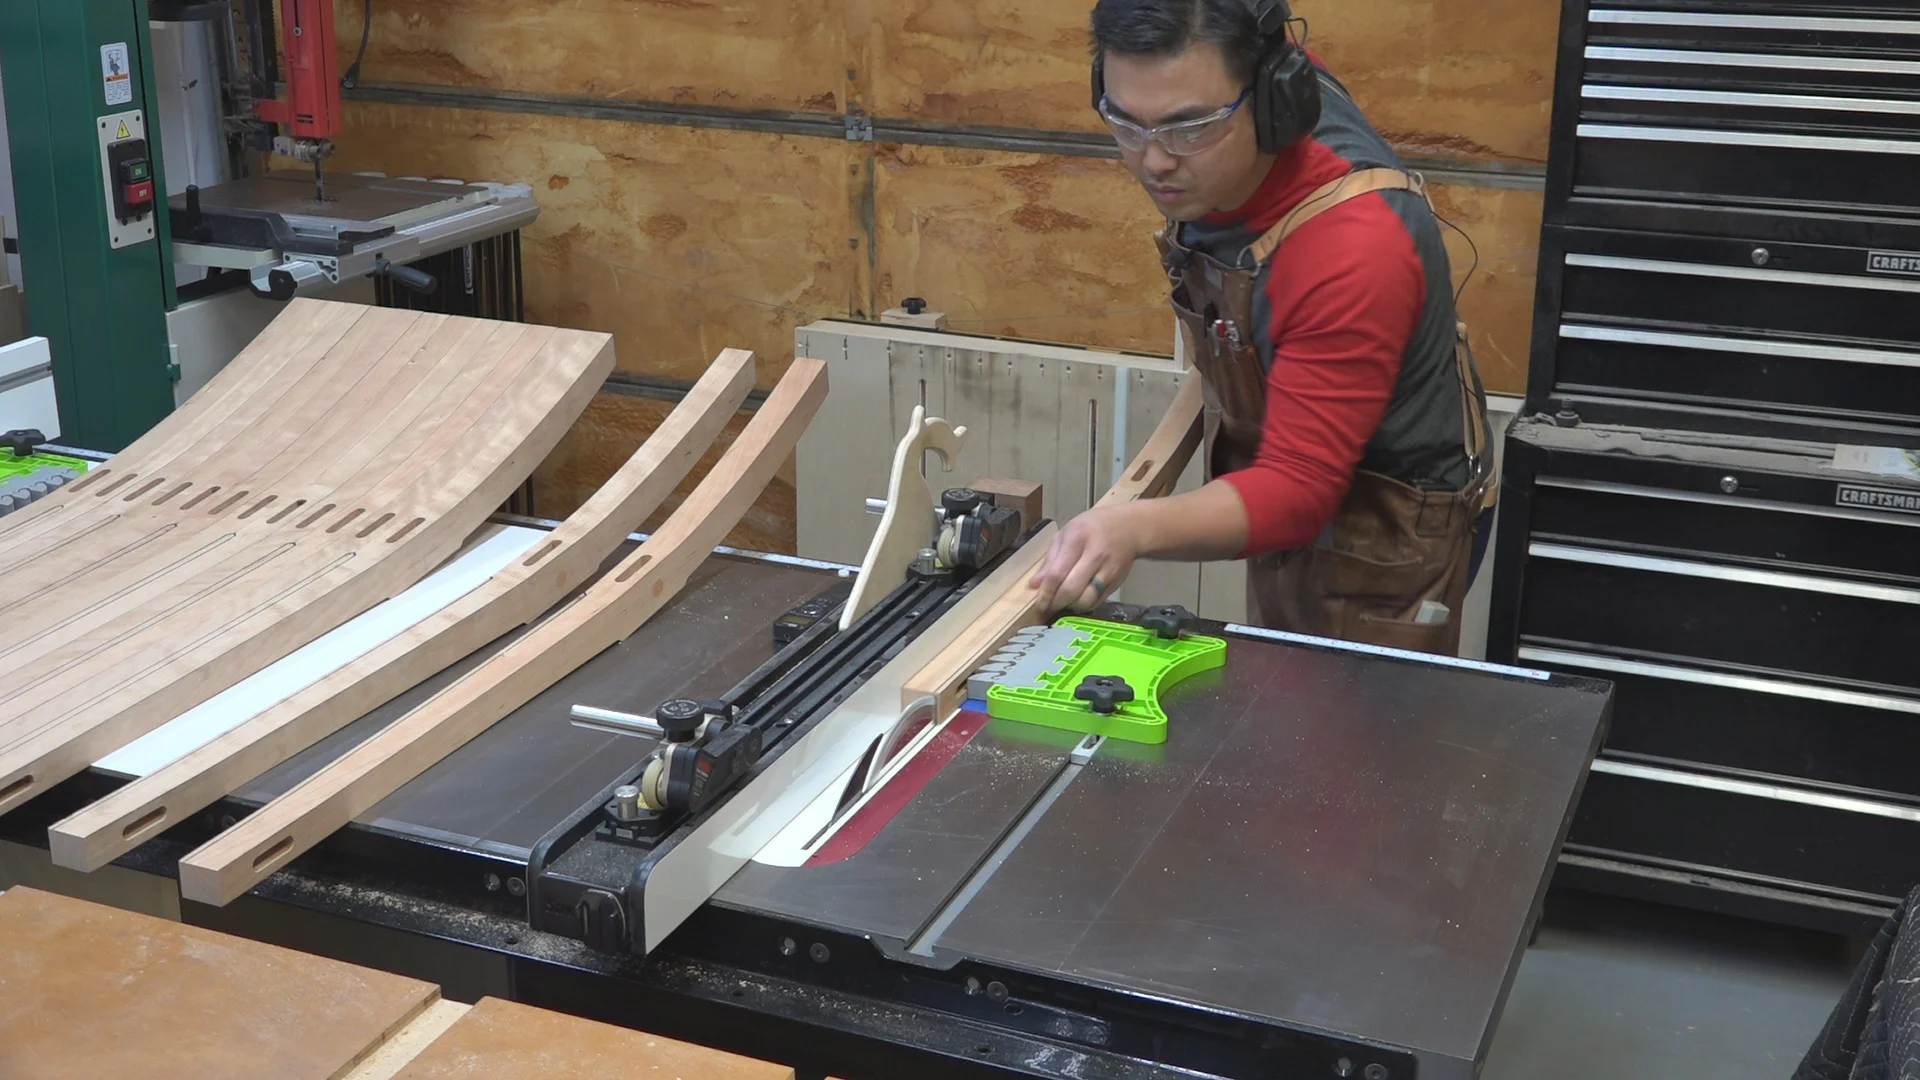
To make sure the thickness of the top of the rear leg is precise and consistent on all 16 chair legs, I made the initial cut on the table saw.
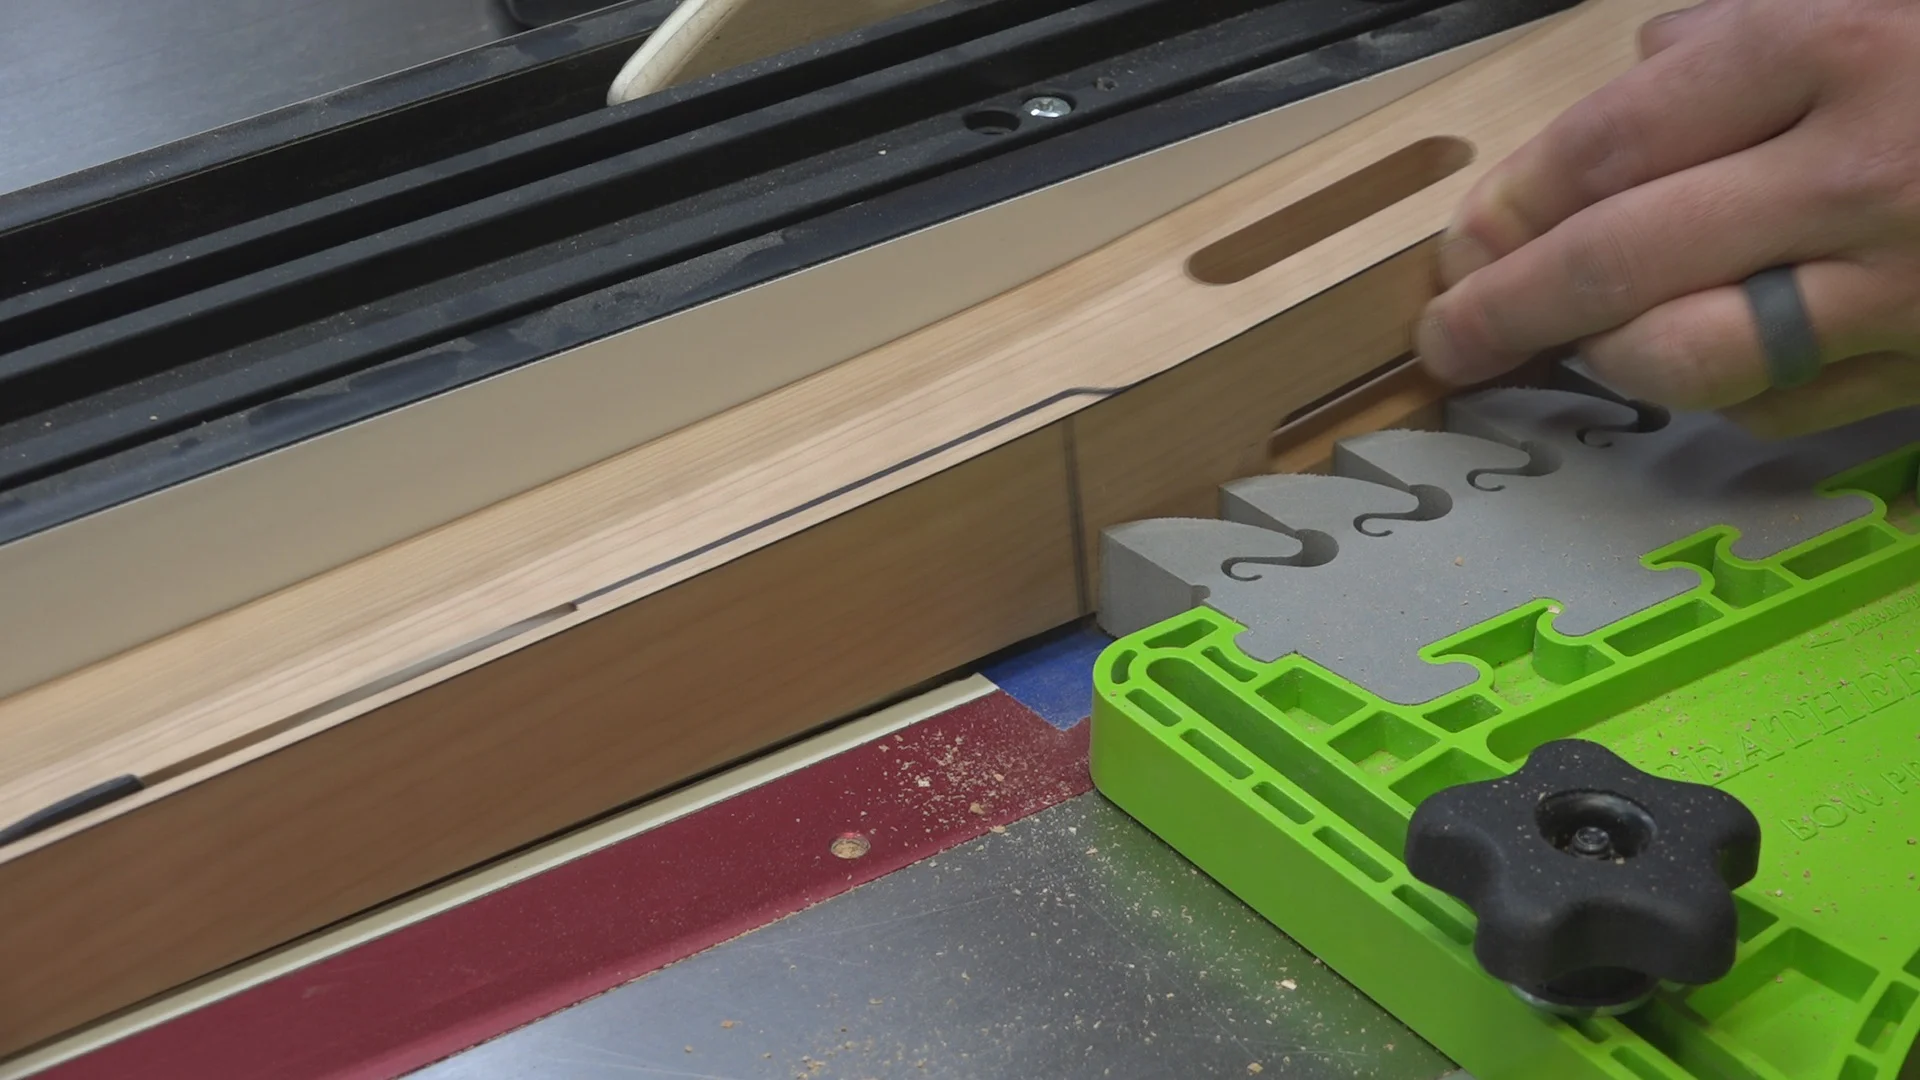
However, I had to make a “stopped cut” and avoid the blade from cutting into the curved portion of the cloud lift. I did this by placing a piece of blue painters tape just ahead of the front of the table saw blade.
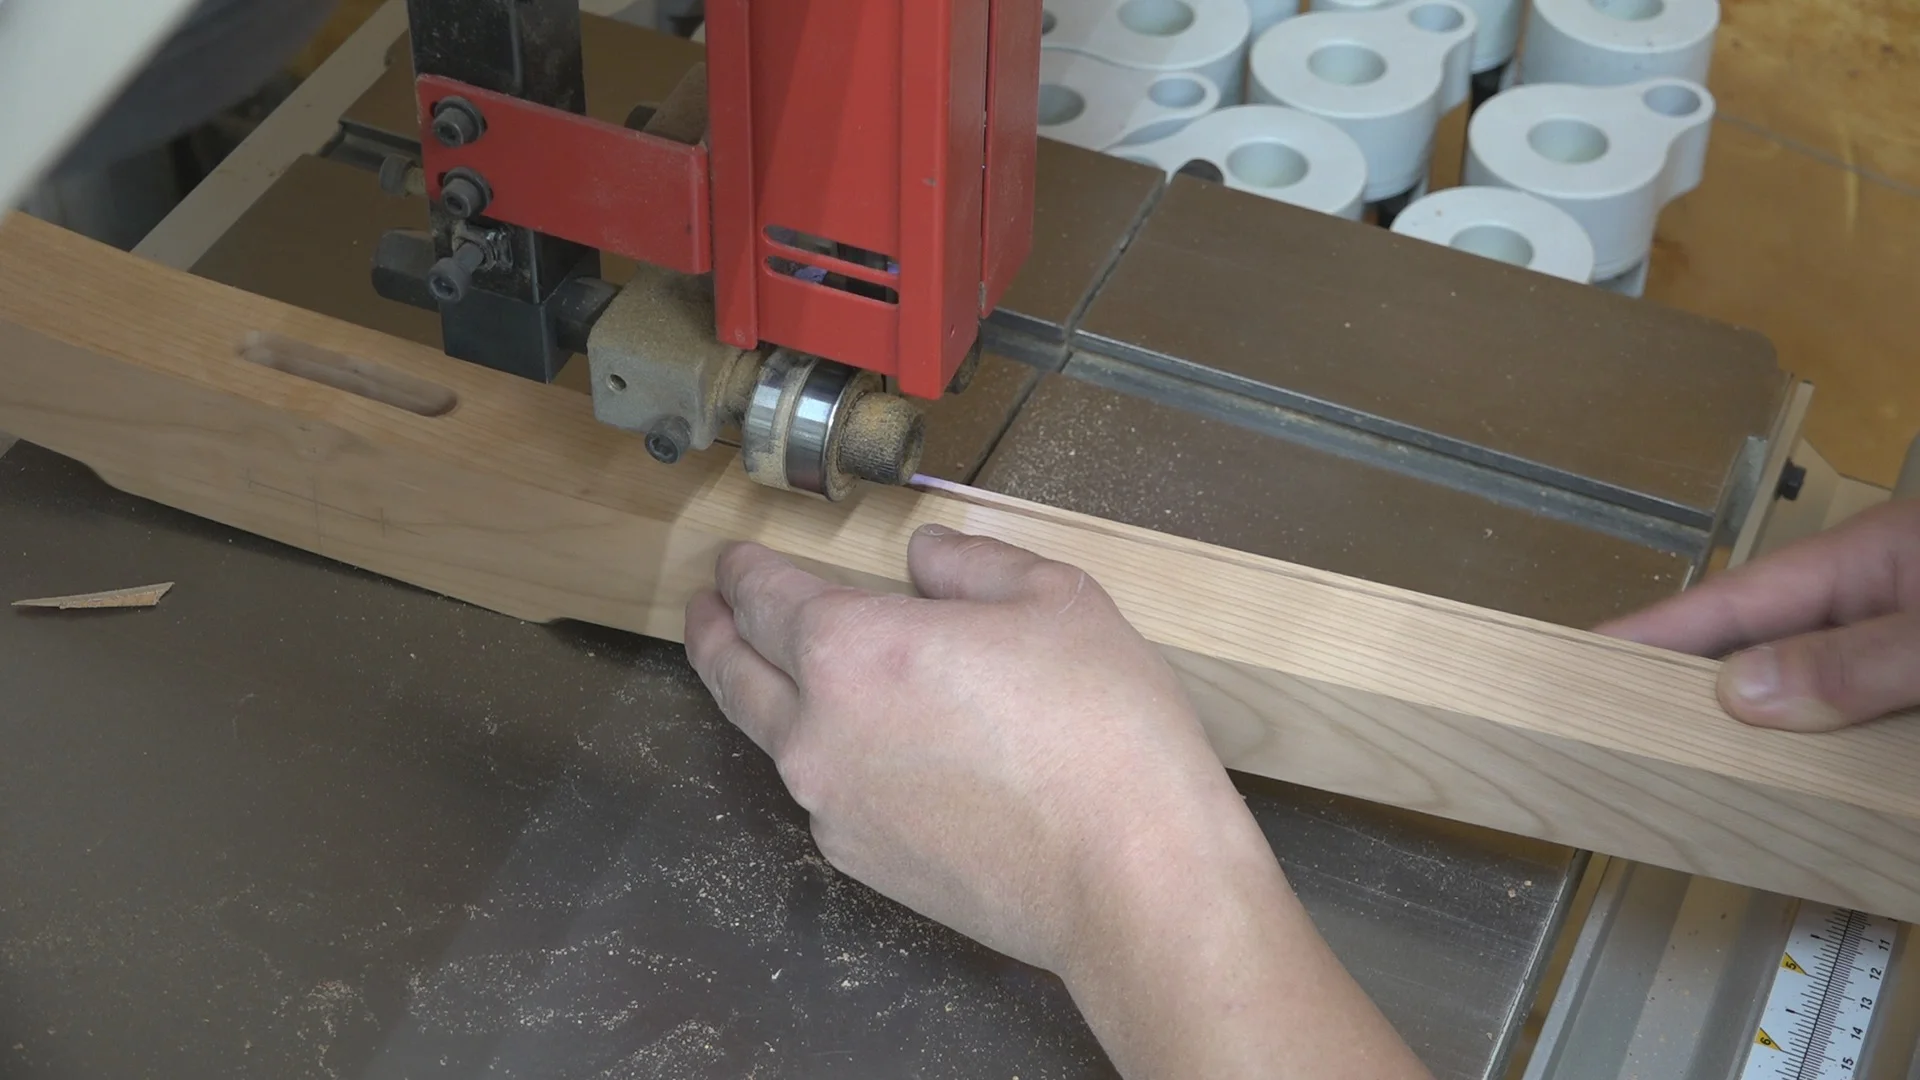
I completed this cut on the bandsaw. This was a rough cut and would be refined with a block place, rasp, and sandpaper.
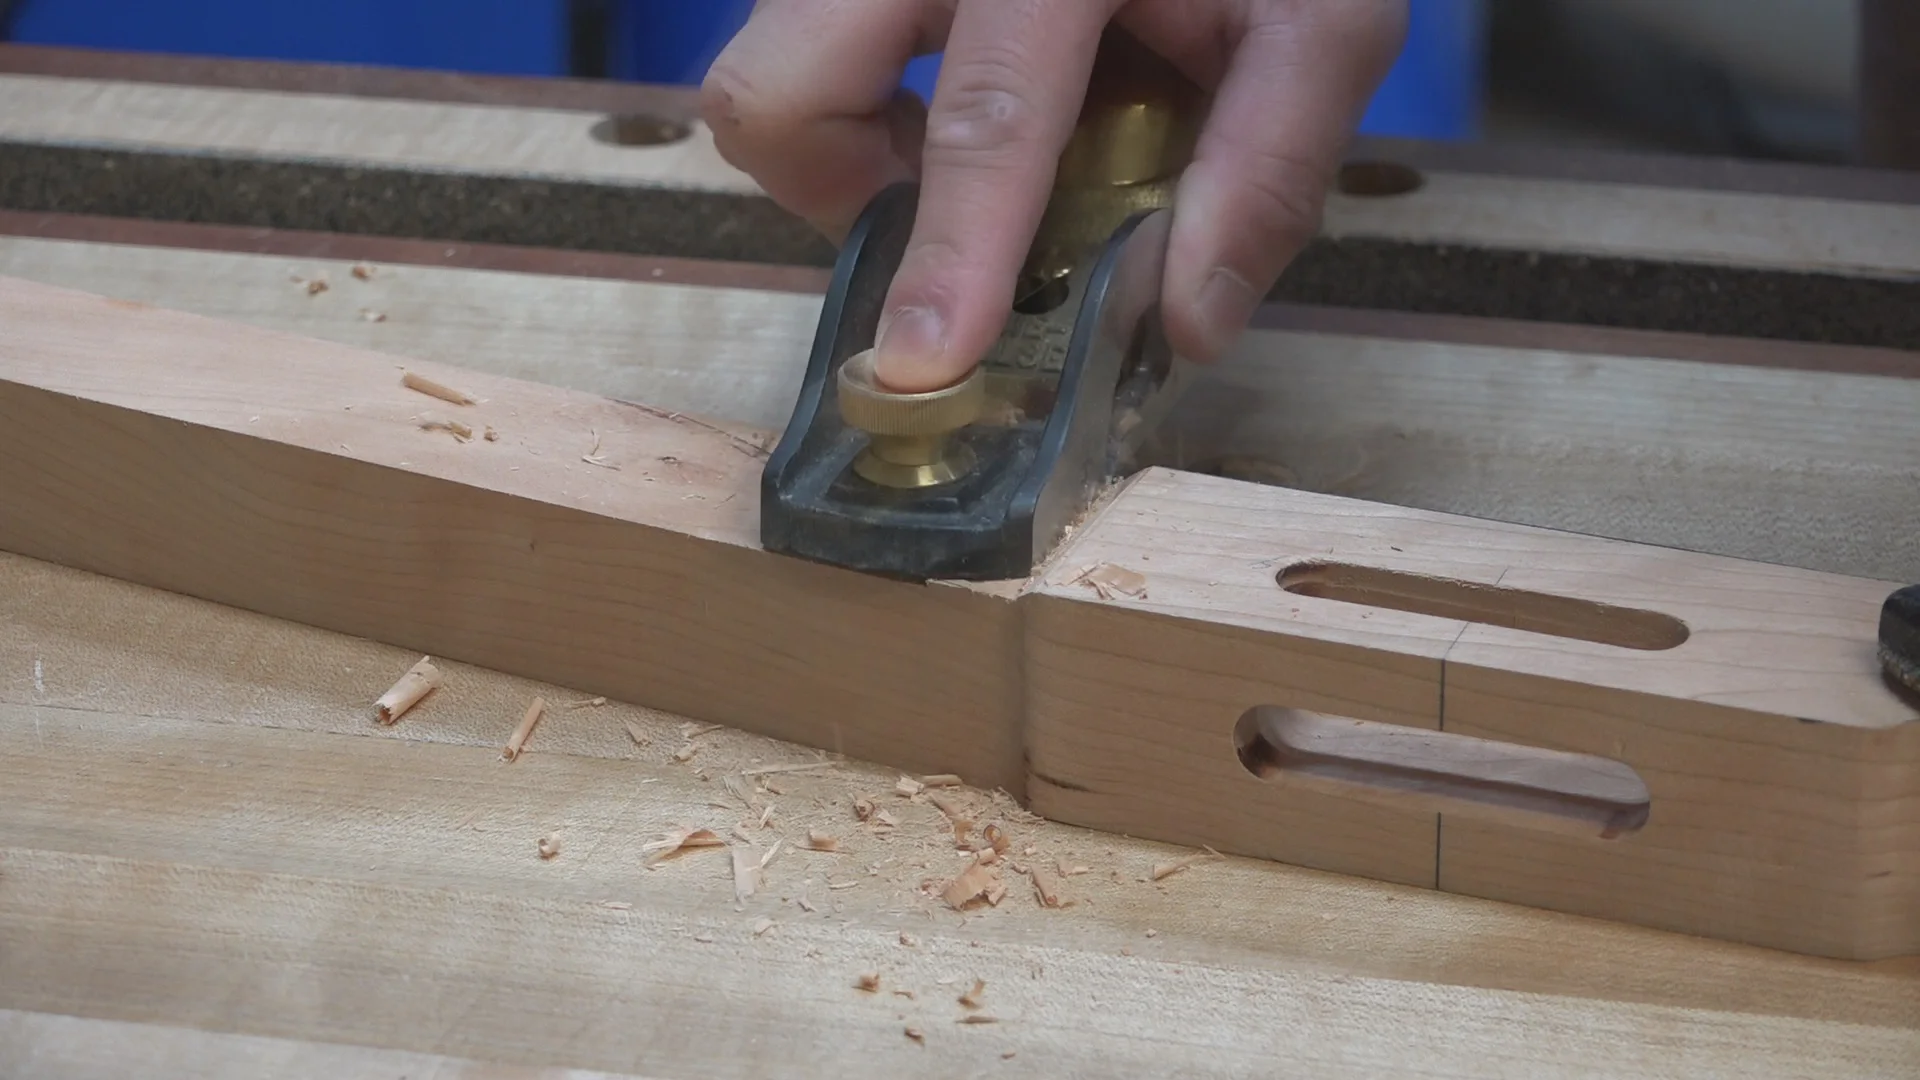
The block plane smooths the rough cut from the bandsaw to the more precise smother cut from the table saw.
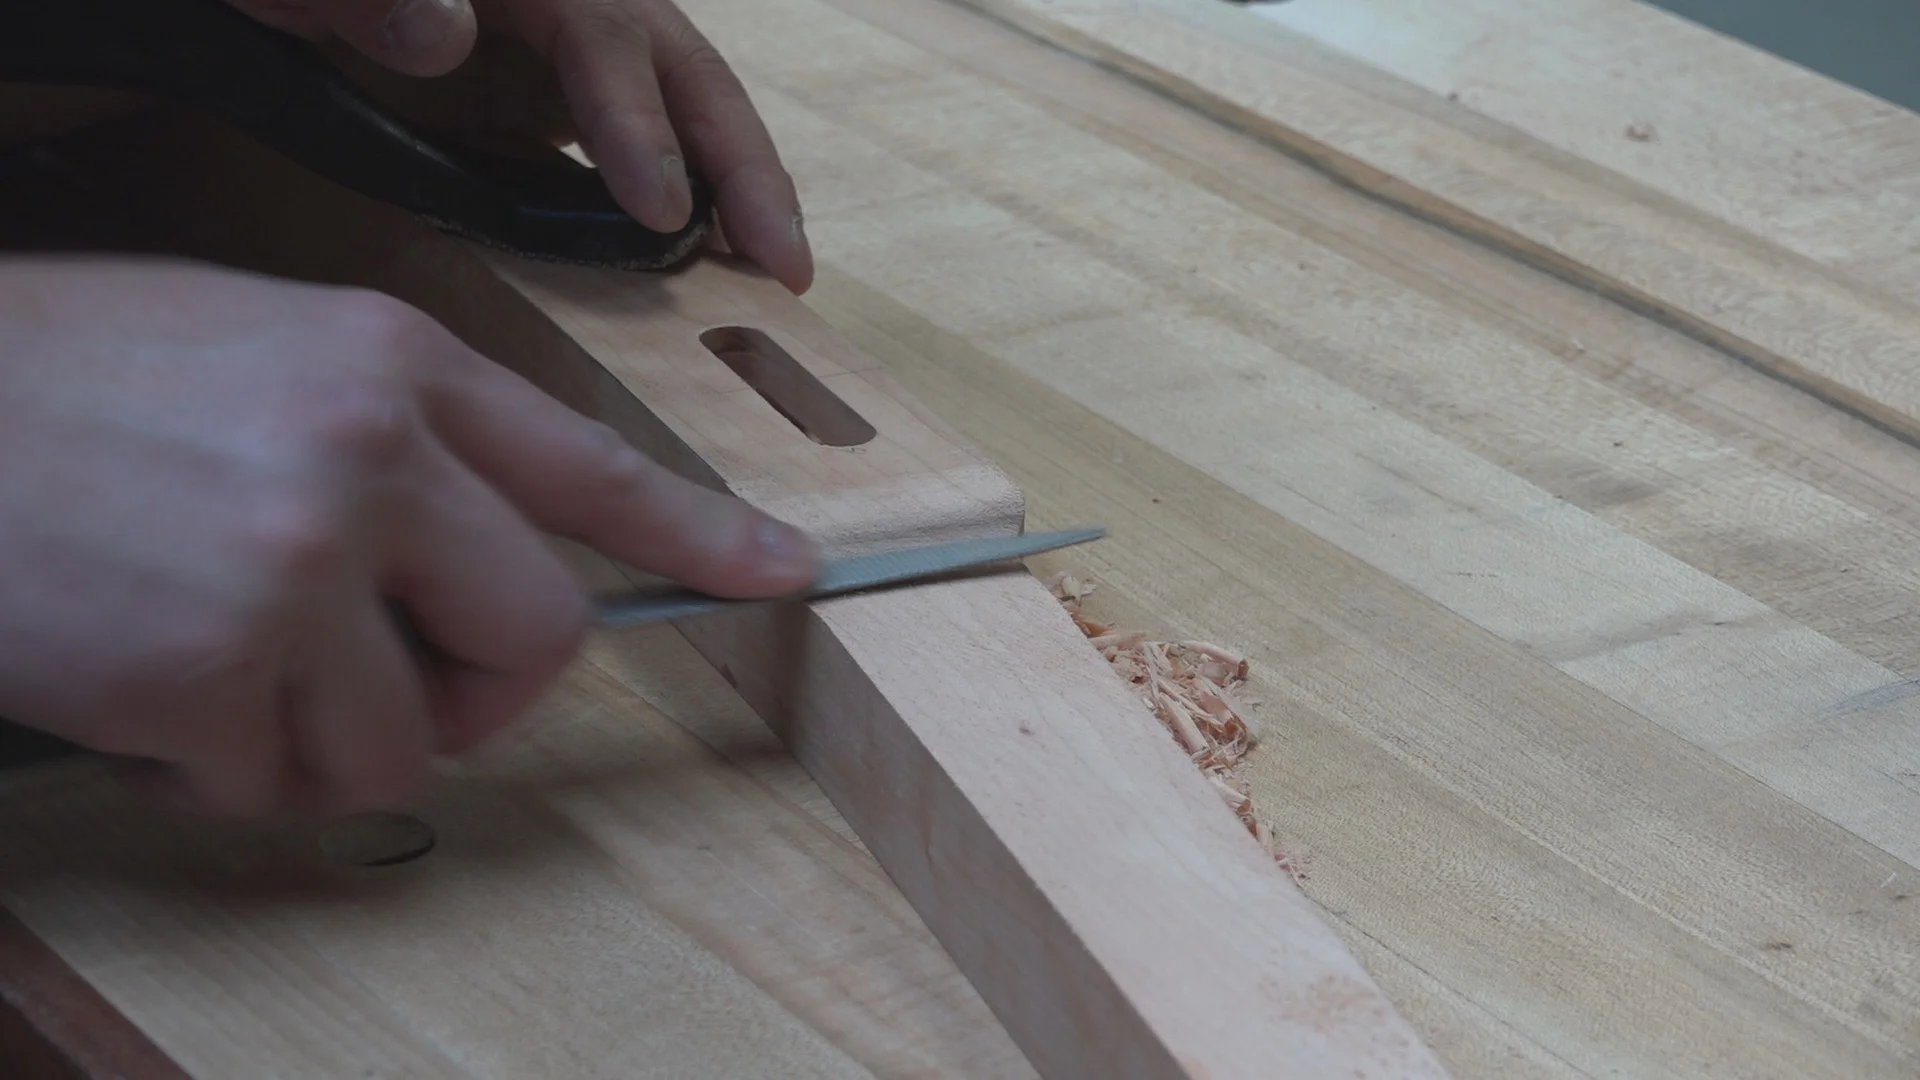
The rasp continued to smooth out the transition from the cloud lift to flat cut made by the table saw. Hand sanding finished this transition.
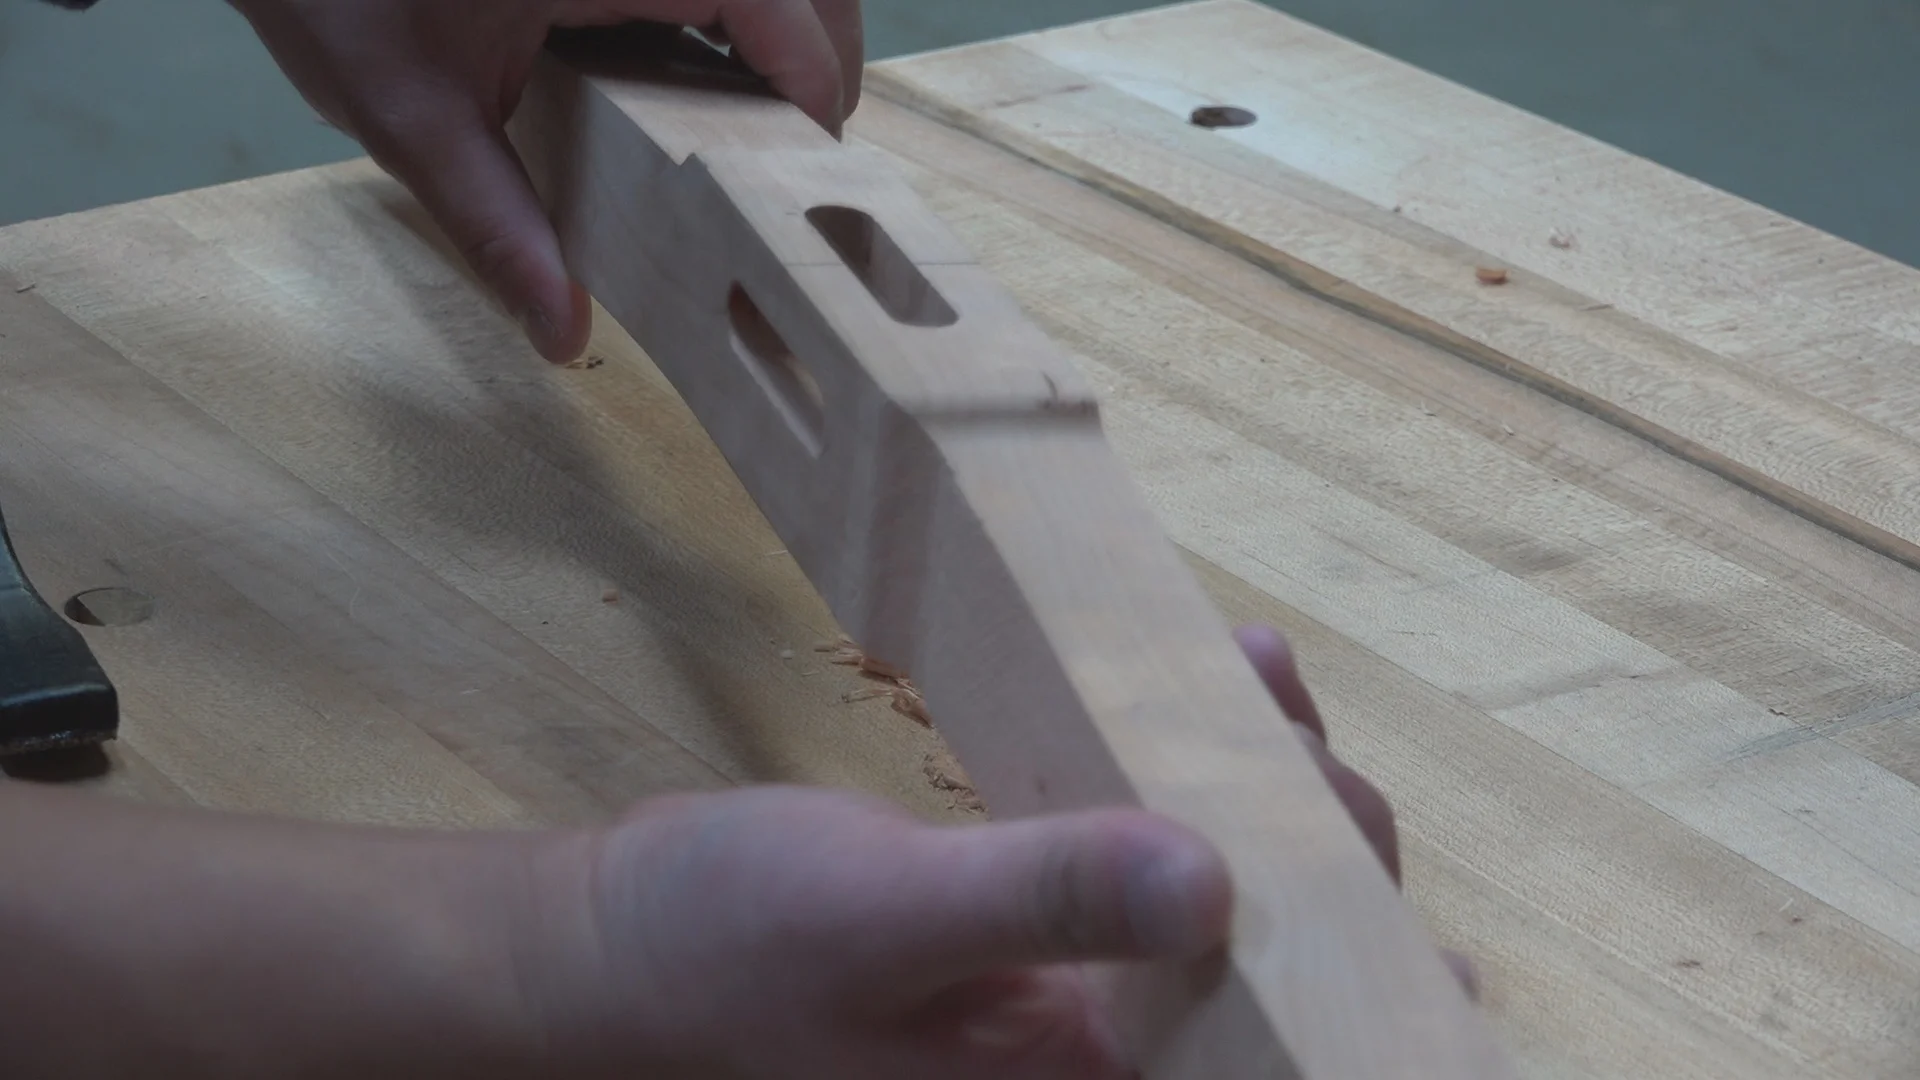
The completed interior cloud lift should match nicely with the cloud lift on the front face of the rear leg.
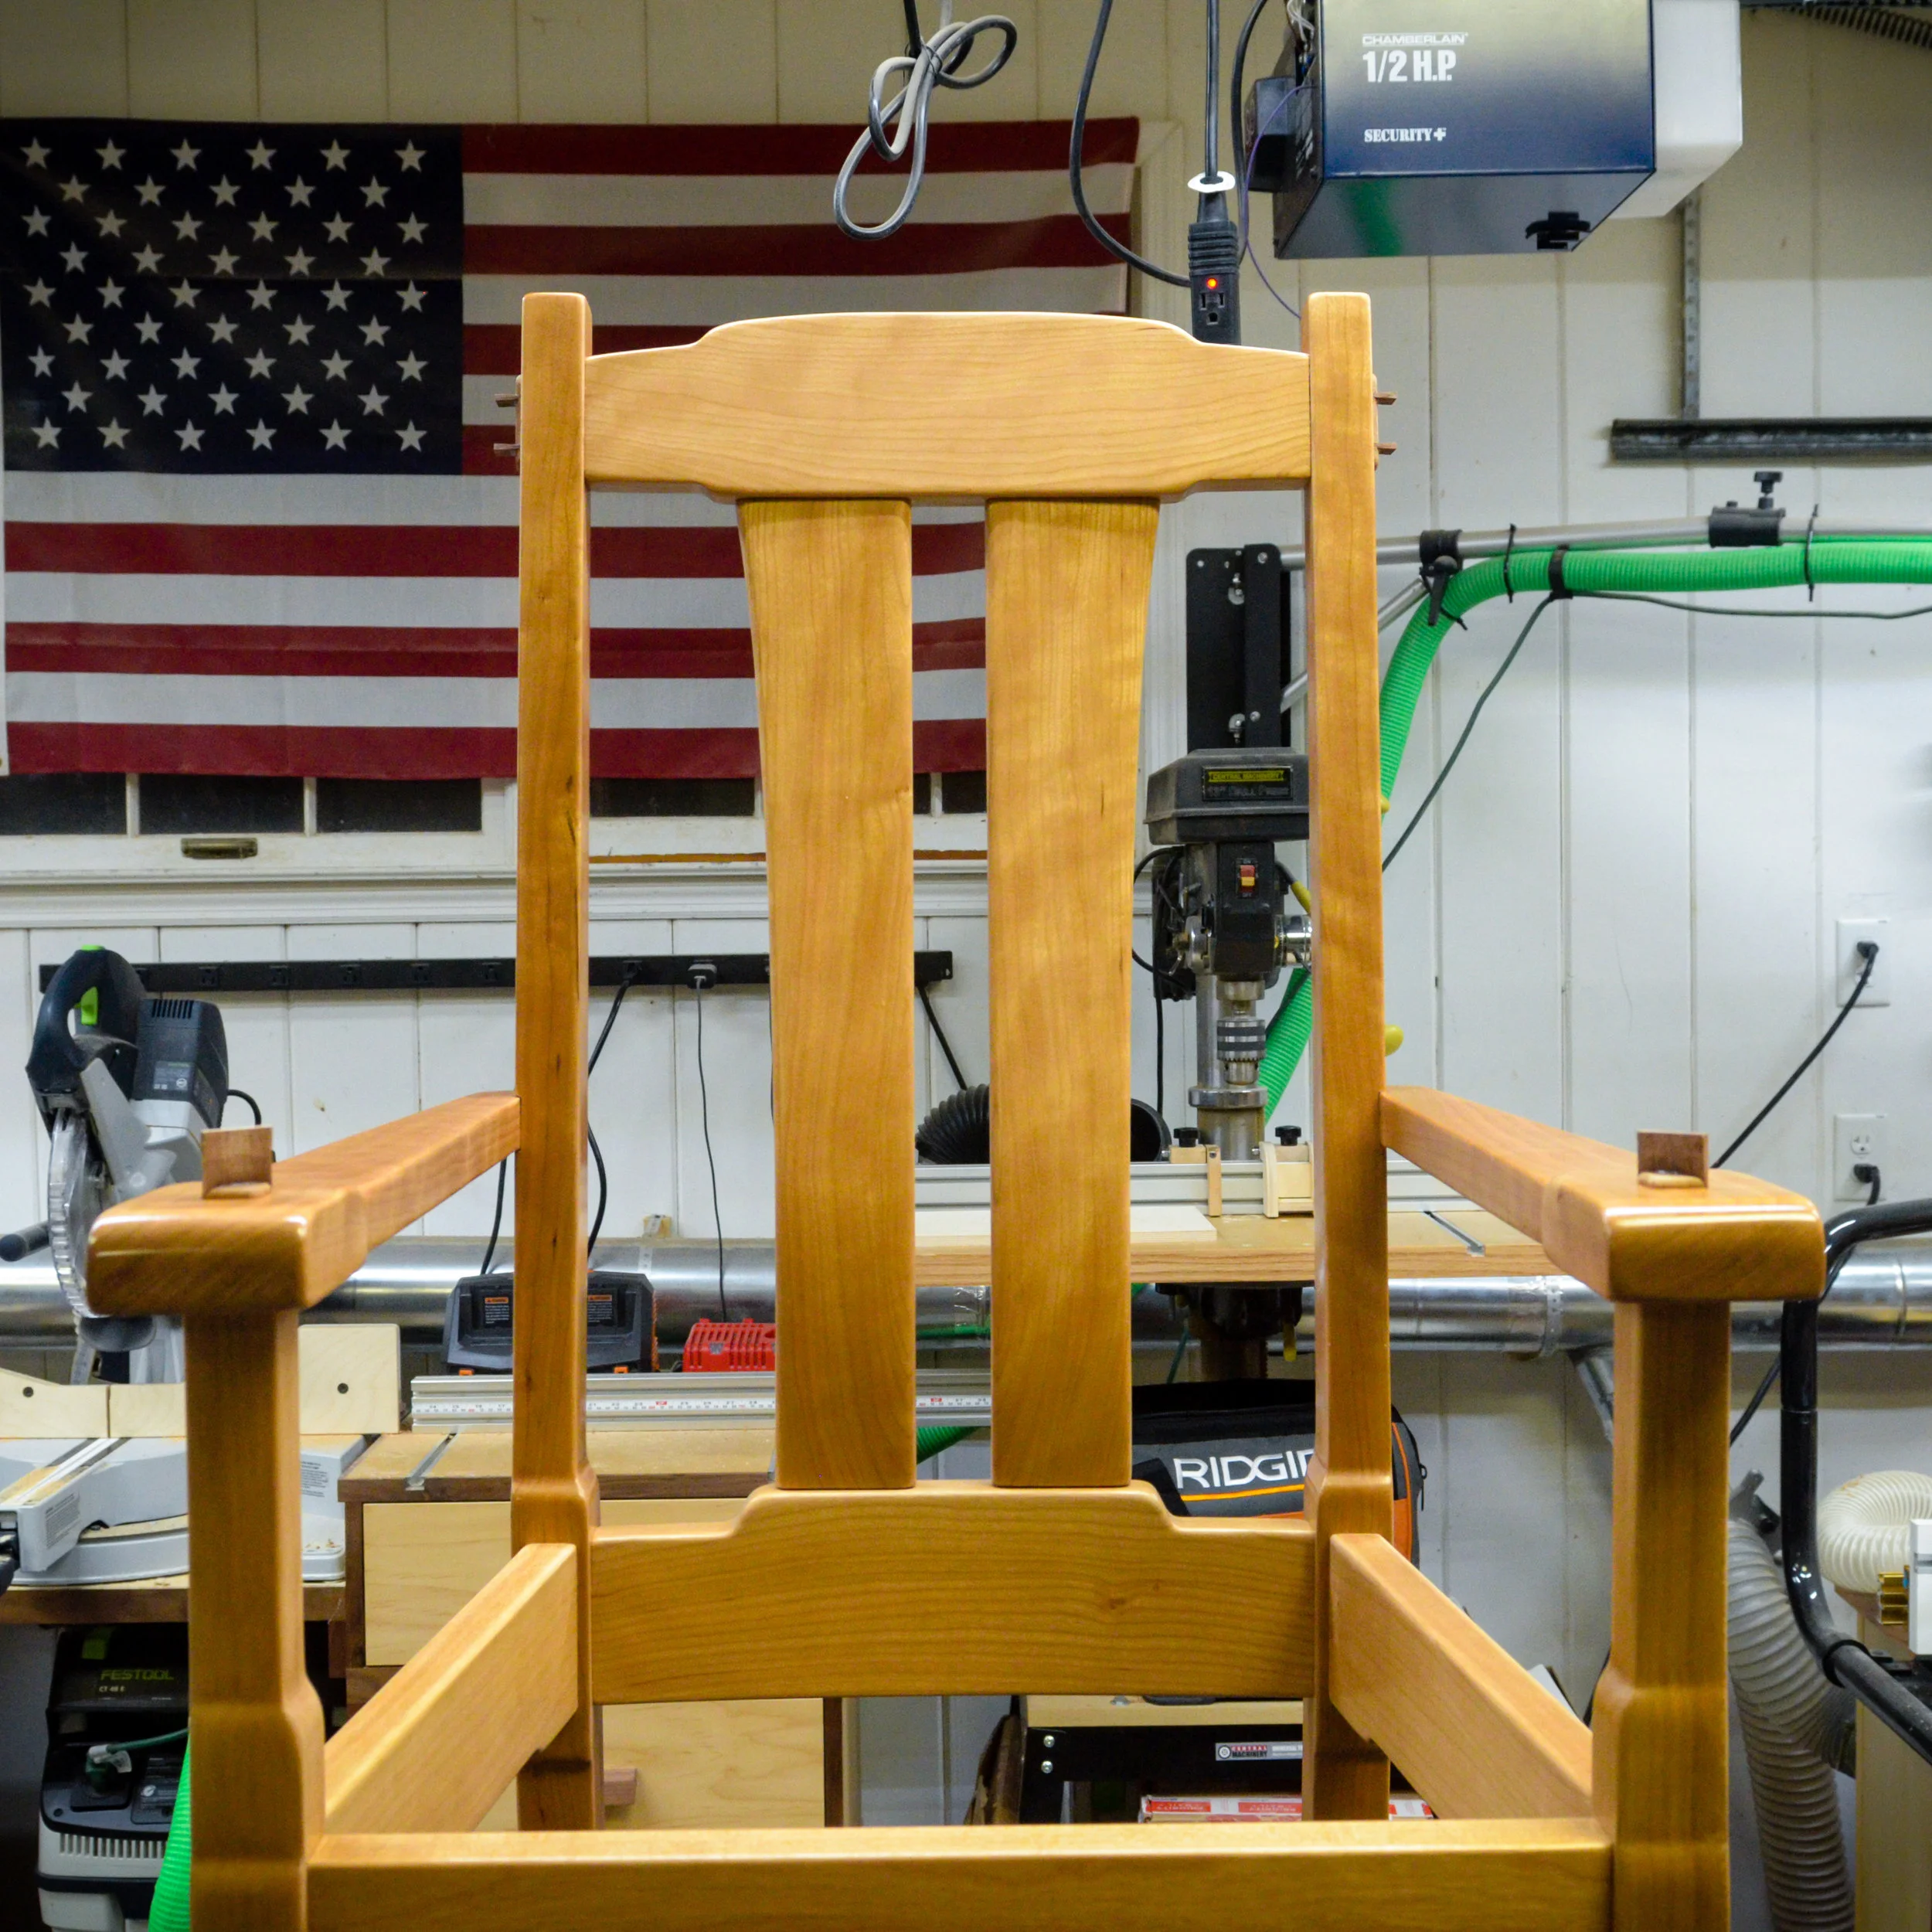
The interior cloud lift adds a beautiful detail to an Arts & Crafts style chair.
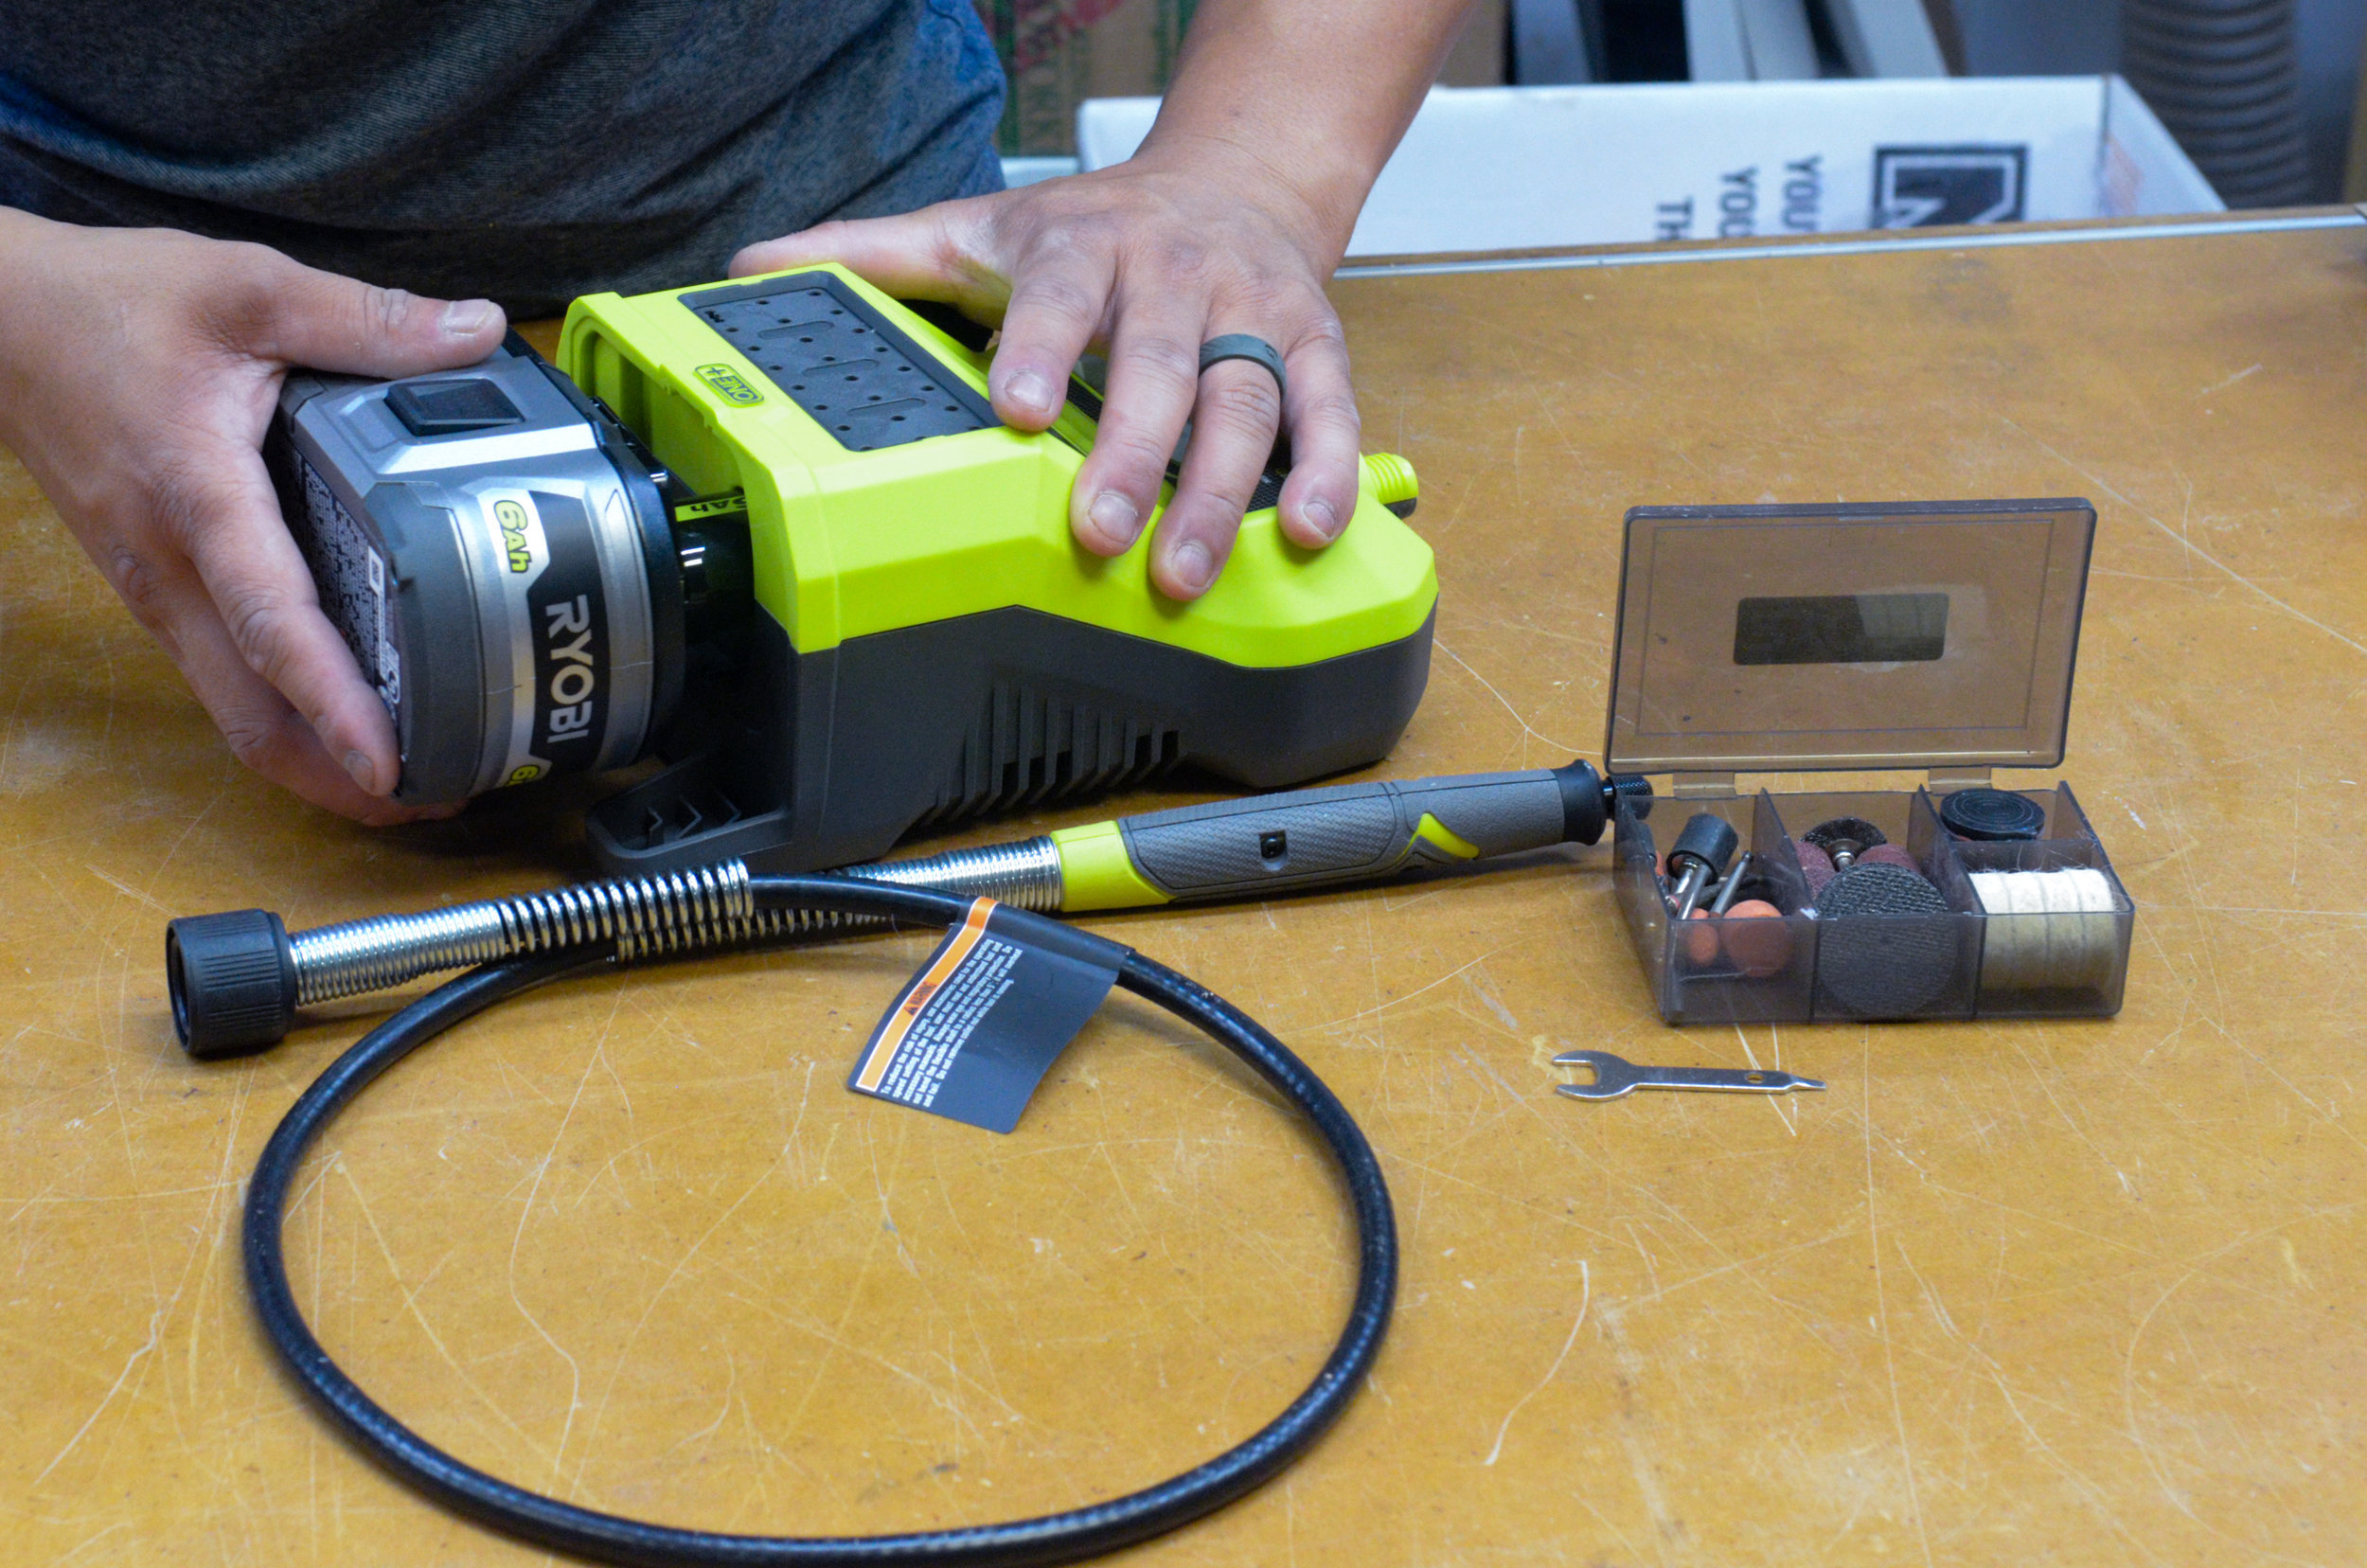
A flexible shaft rotary tool by Ryobi could have made shaping the interior cloud lift much simpler.
Using the rasps left surface of the interior cloud lift somewhat rough. Therefore, a significant amount of hand sanding had to be done to remove the marks left by the rasp. Shortly after completed all of the cloud lifts on the 16 rear chair legs, I received the Ryobi 18-Volt ONE+ Cordless Rotary Tool. This would have been the perfect tool to smooth out the transition from cloud lift to the straight portion of the rear leg.
The Ryobi cordless rotary tool uses a Ryobi One+ 18-volt battery to power the 36 in. flexible shaft tool. The rotary tool has a 1/8” collet and comes with 33 different sanding, grinding, cutting, and polishing accessories. The 3/8” sanding wheel would have been perfect to sanding away the rough marks left by the rasps. In fact, I practiced on my old prototype leg just to see what kind of a finish I would have gotten if I had gotten the tool early enough to use.
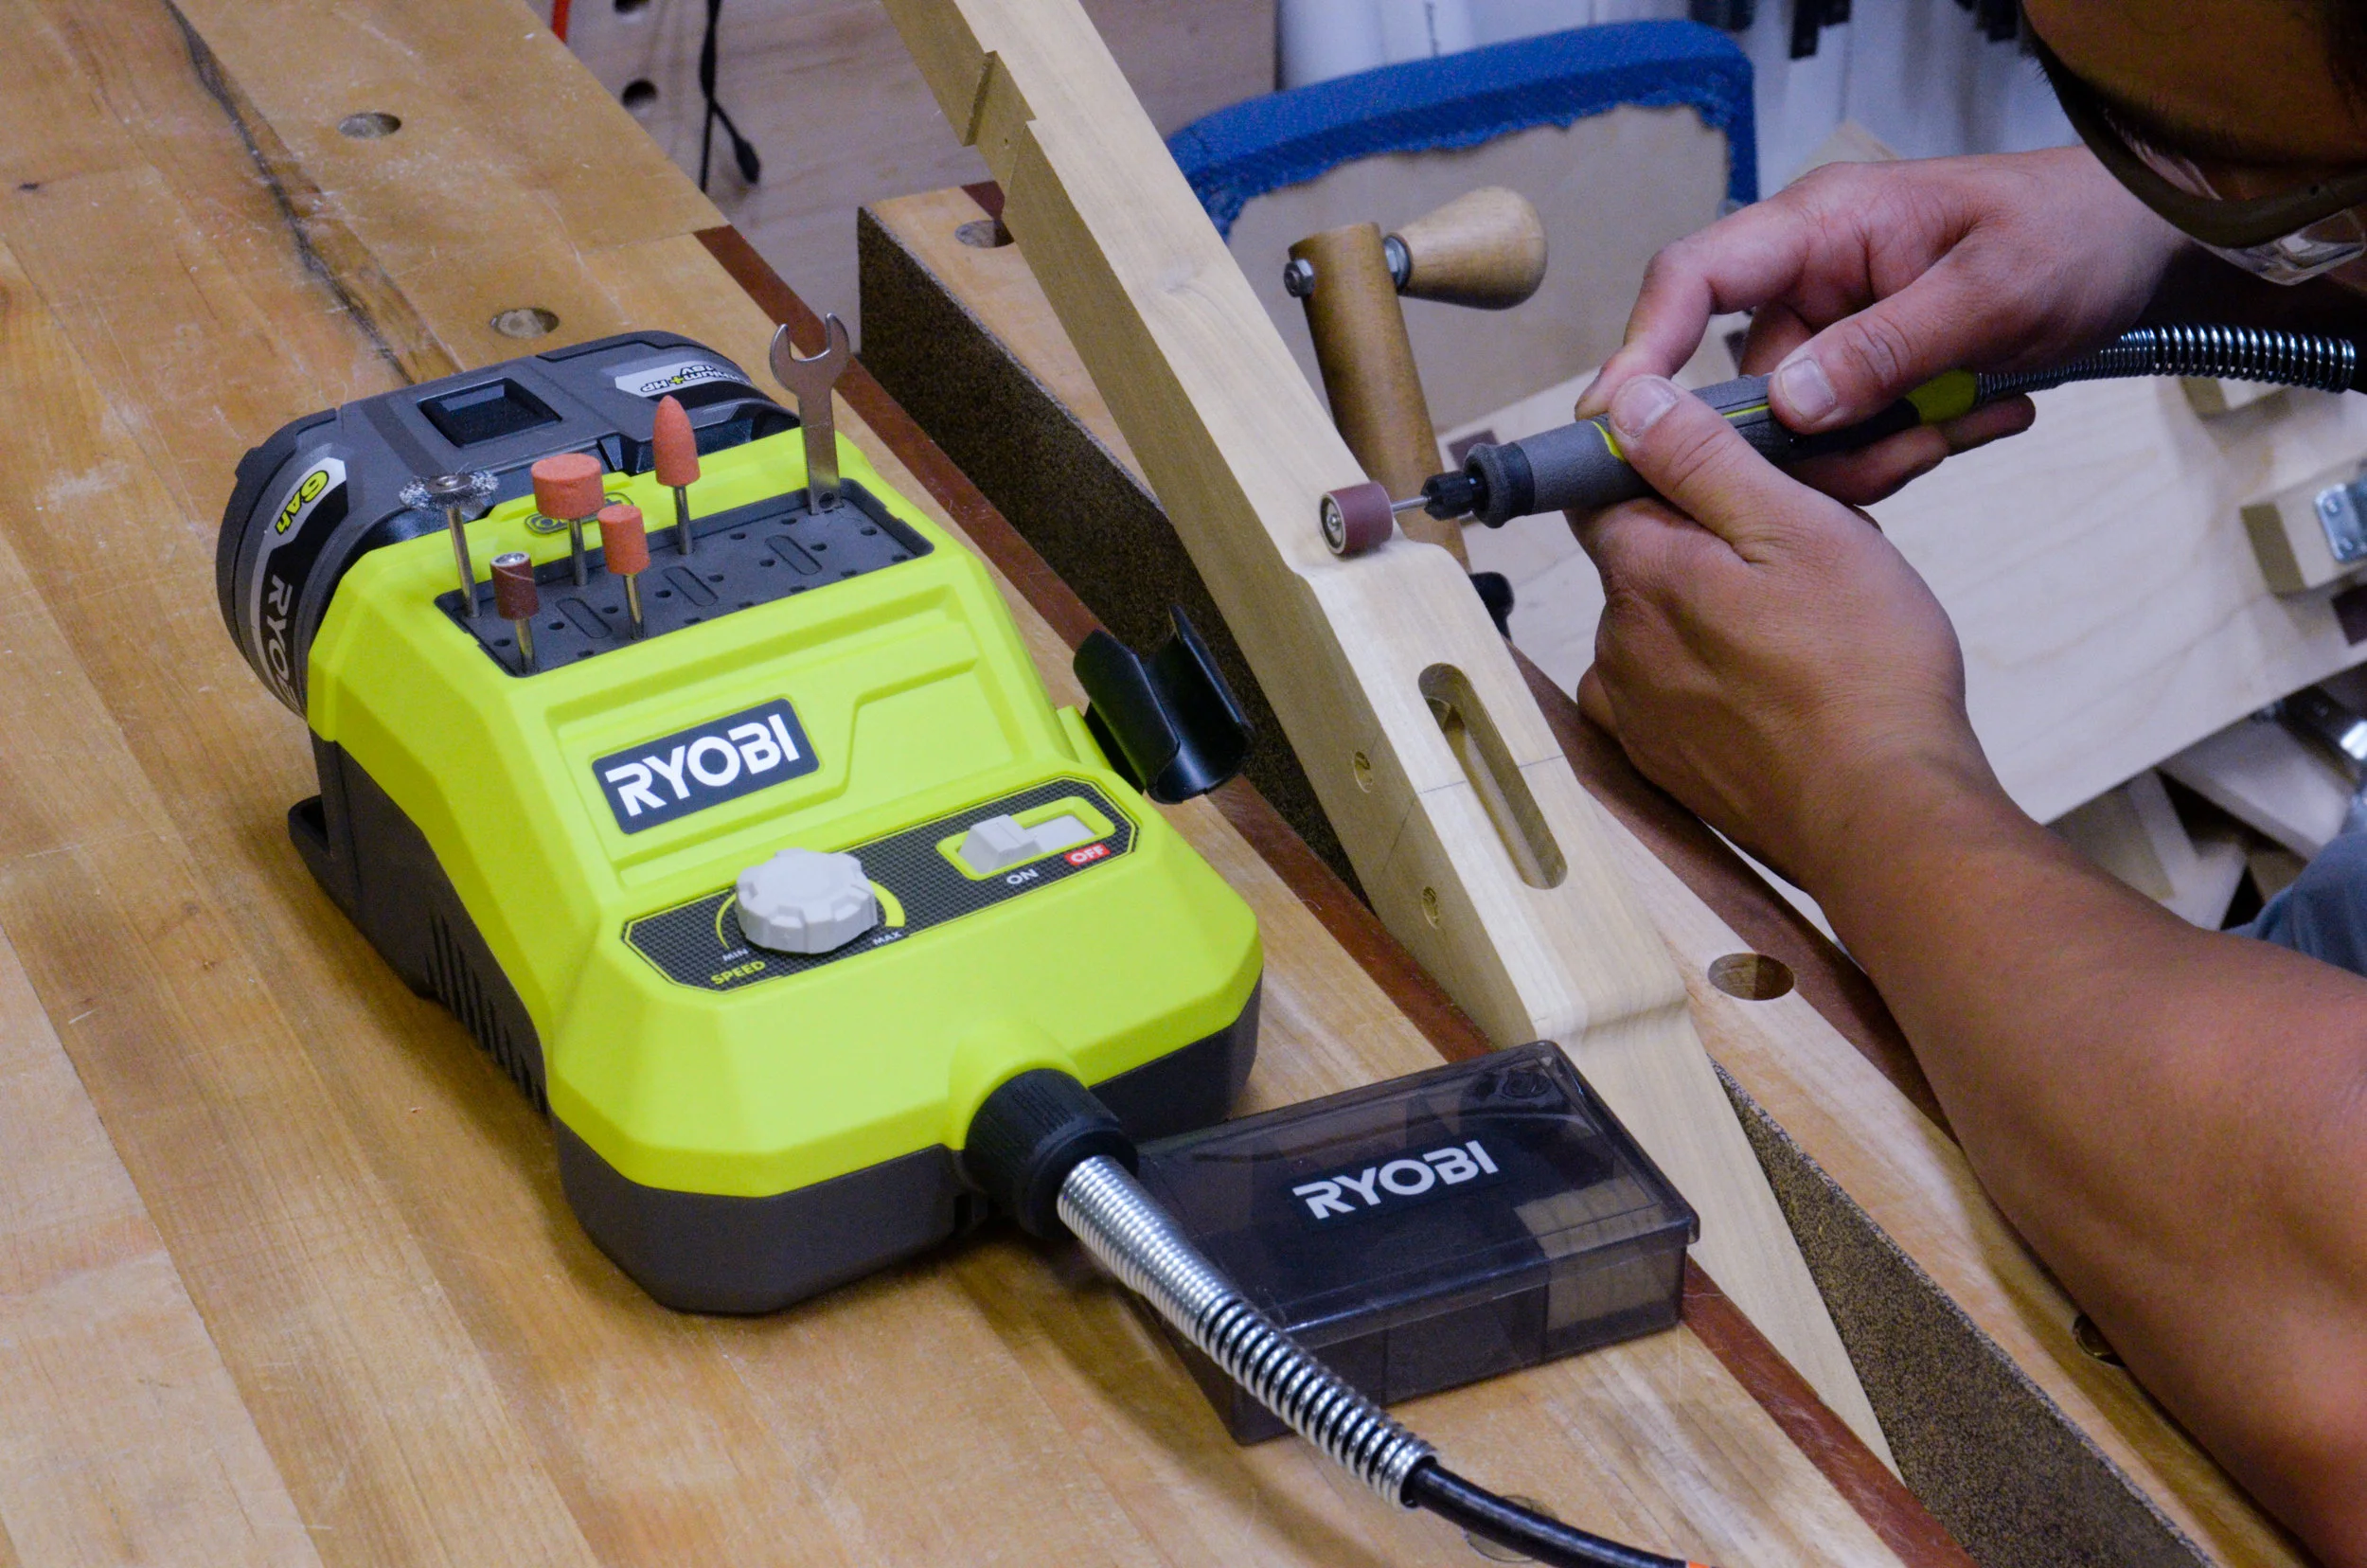
The Ryobi rotary tool would have been perfect to shape some fine detail work on the chairs.
Making a Dining Chair Seat Insert
The upholstered chair cushions for the dining chairs use a 3/4” Birch plywood insert as a platform. I cut the plywood using a circular saw and table saw. I then pattern route the chair insert and add round overs to prevent upholstery fabric from ripping and to help shape the upholstery foam.
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
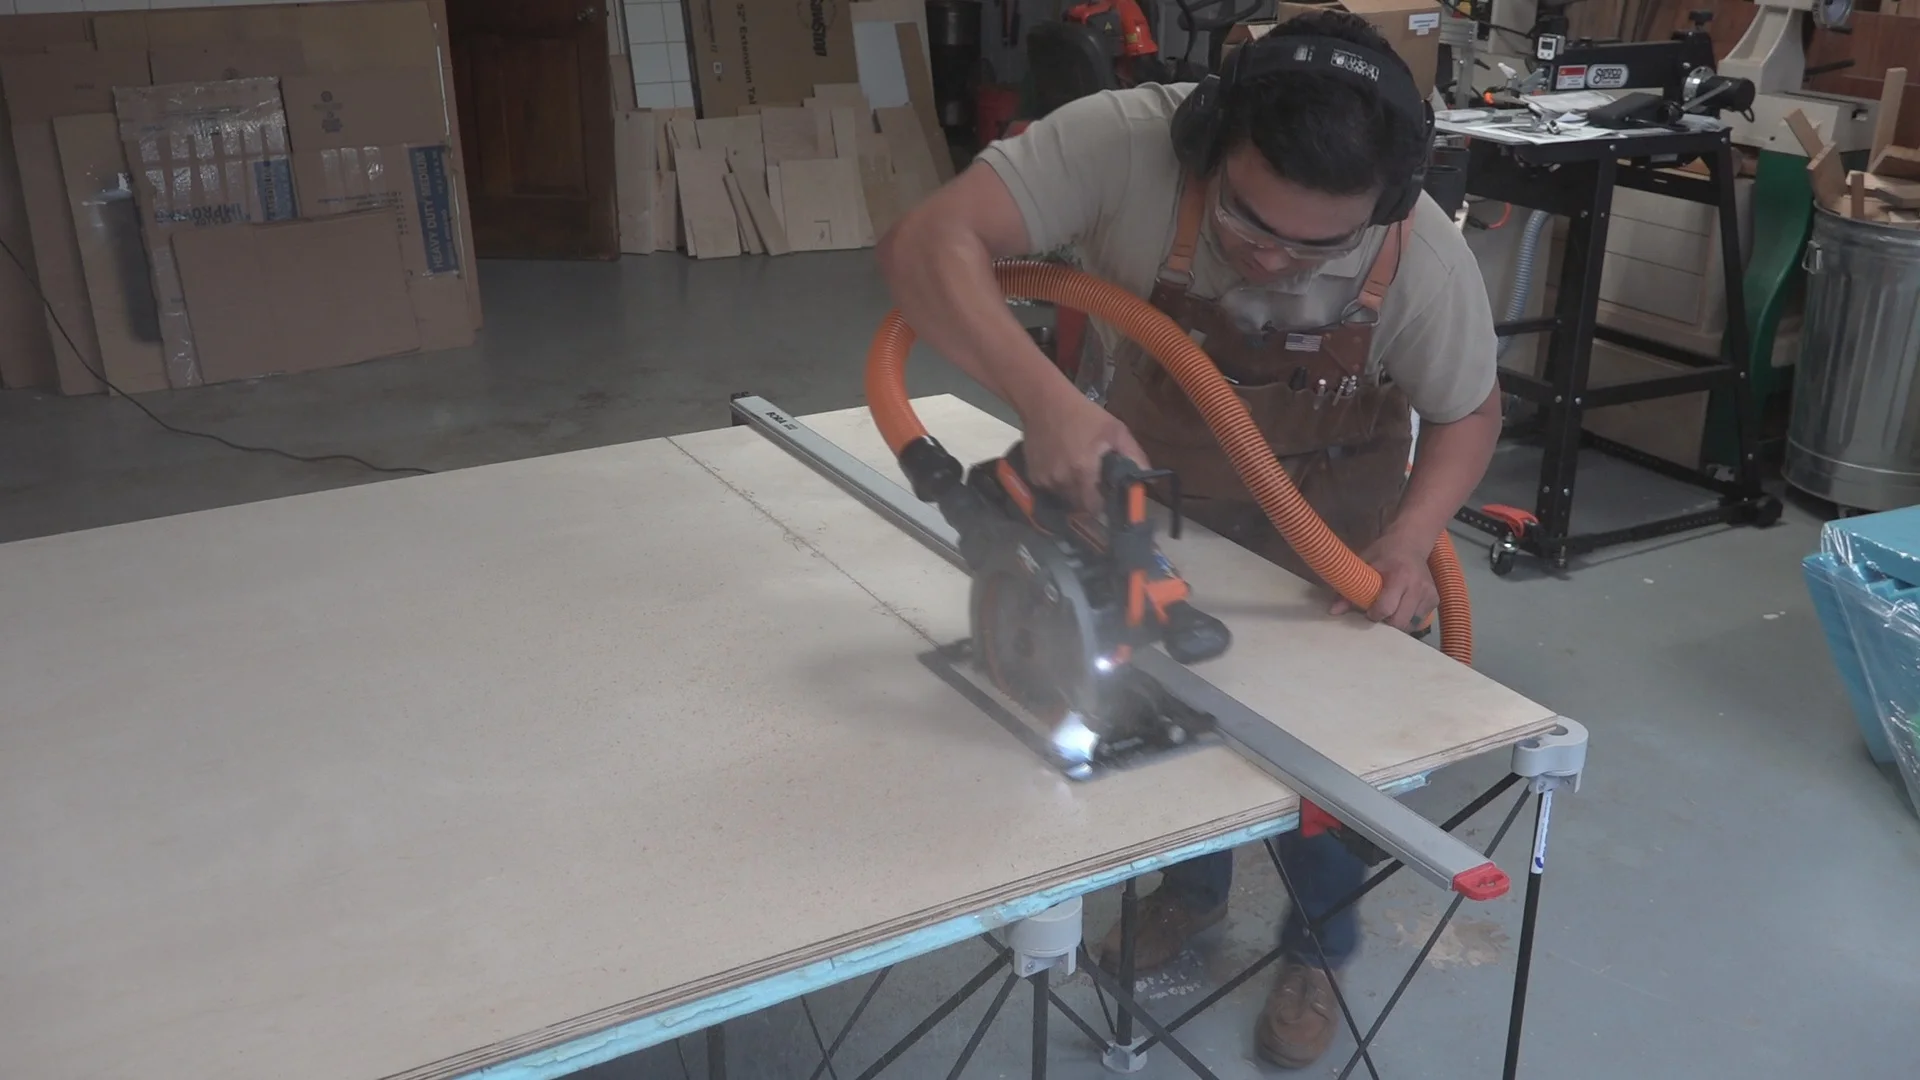
The chair inserts are made from 3/4” Birch plywood.
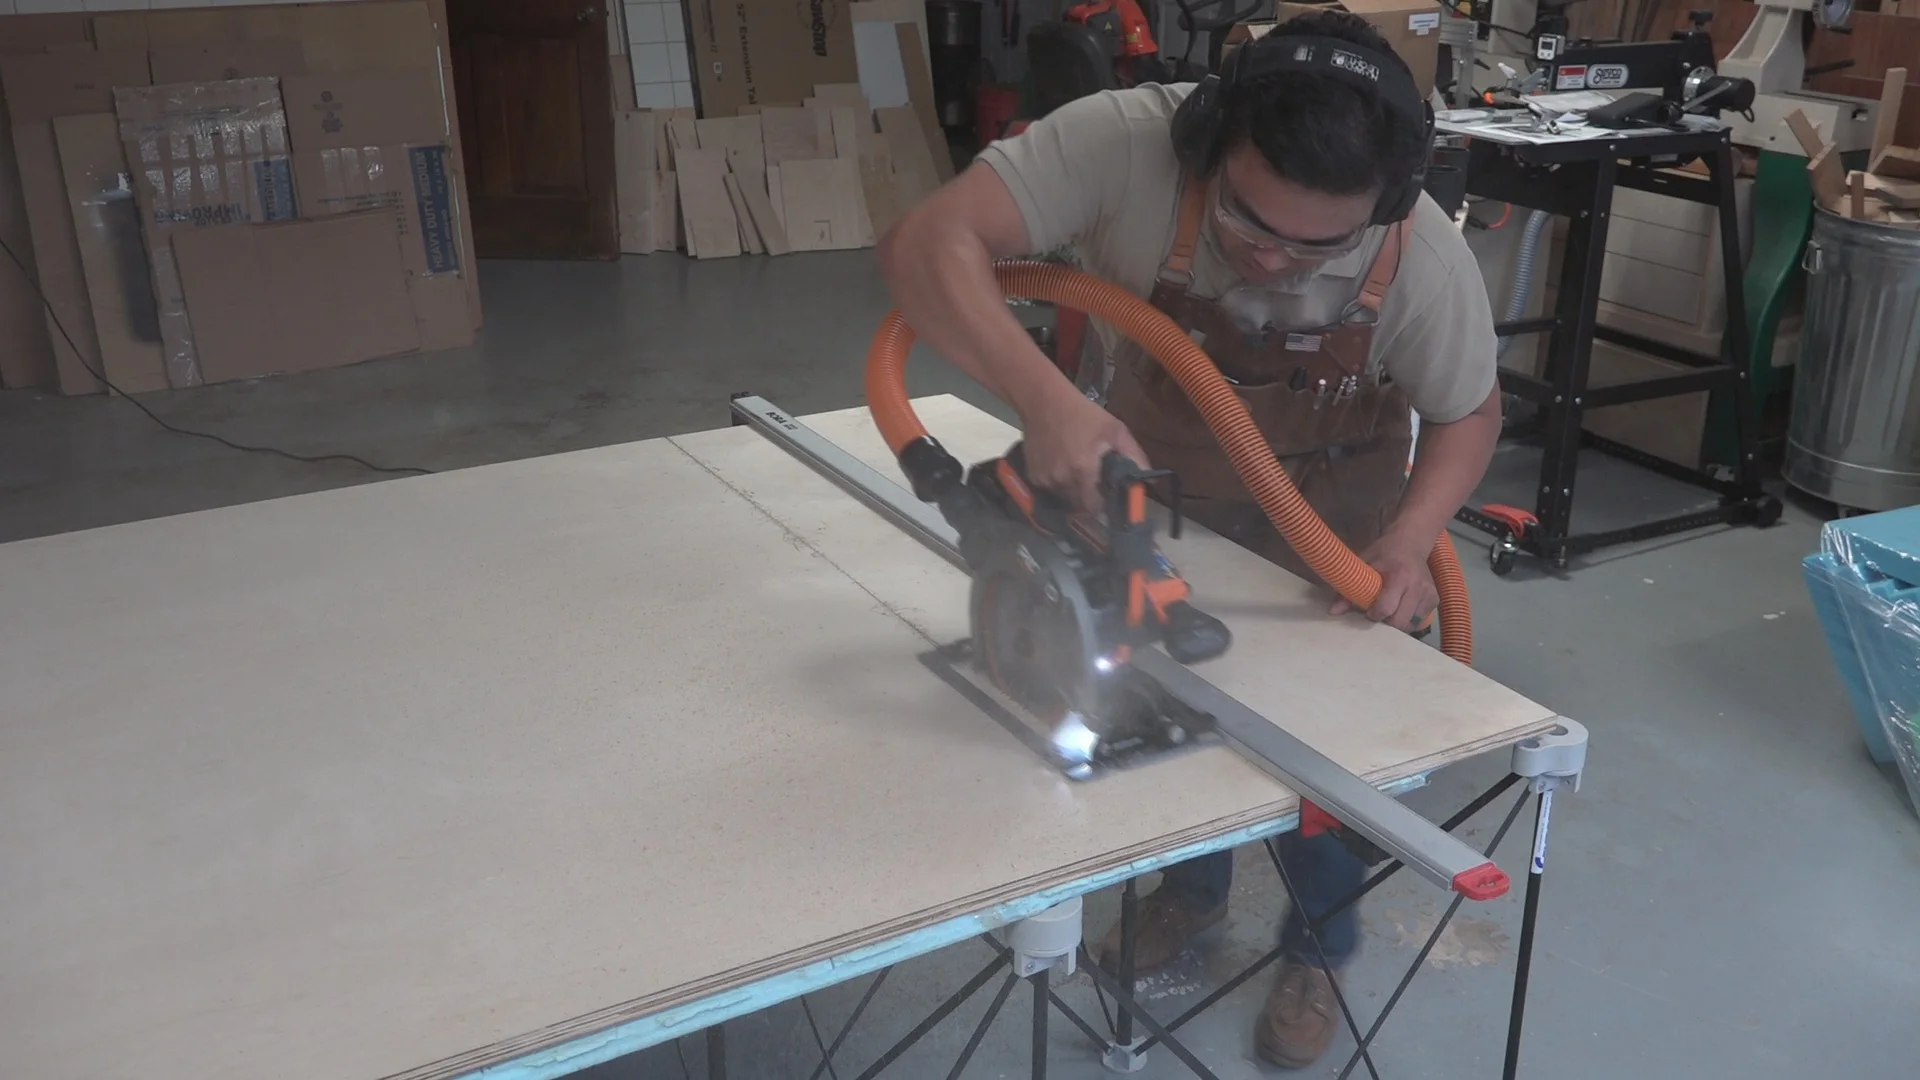
The upholstered chair cushions for the dining chairs use a 3/4” Birch plywood insert as a platform. To cut the 3/4" Birch plywood to a more manageable size, I used the Ridgid OCTANE 18V 7-1/4 in. Circular Saw. This was the first time I've ever used a battery powered circular saw. I was quite impressed by the power. The Ridgid OCTANE Circular Saw provided a dust collection port. I attached my favorite Ridgid shop vacuum but I was not impressed with the dust collection. I'm sure it collected some of the dust but I'm used to plunge saws that collect much more dust when attached to a dust extractor. However, the convenience of a battery powered circular saw greatly outweighs the lack of dust collection.
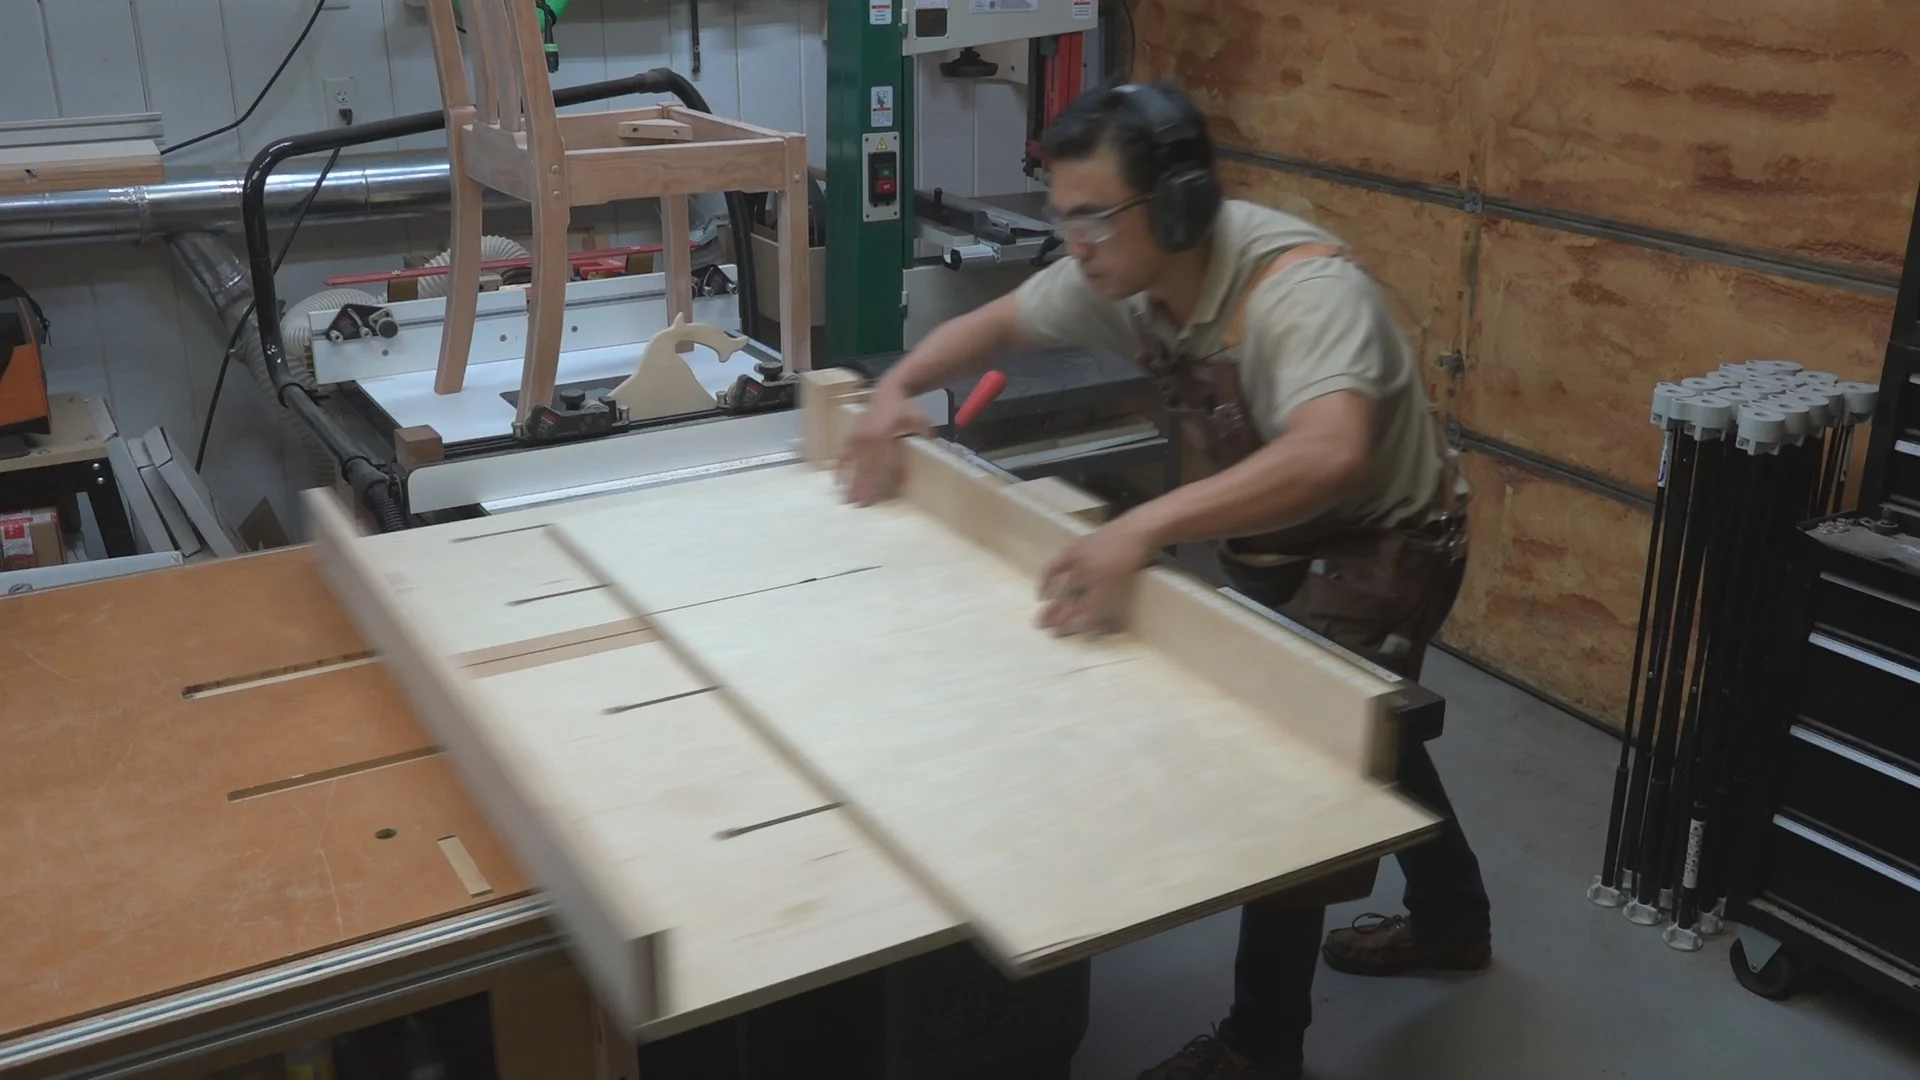
Next, I crosscut the plywood to final width on my table saw and crosscut sled.
I had already developed a template to fit within the chair rails. So I traced the outline of my template on all the chair insert blanks. I like to use a Sharpie marker because it gives me a margin of error when I’m rough cutting on the bandsaw.
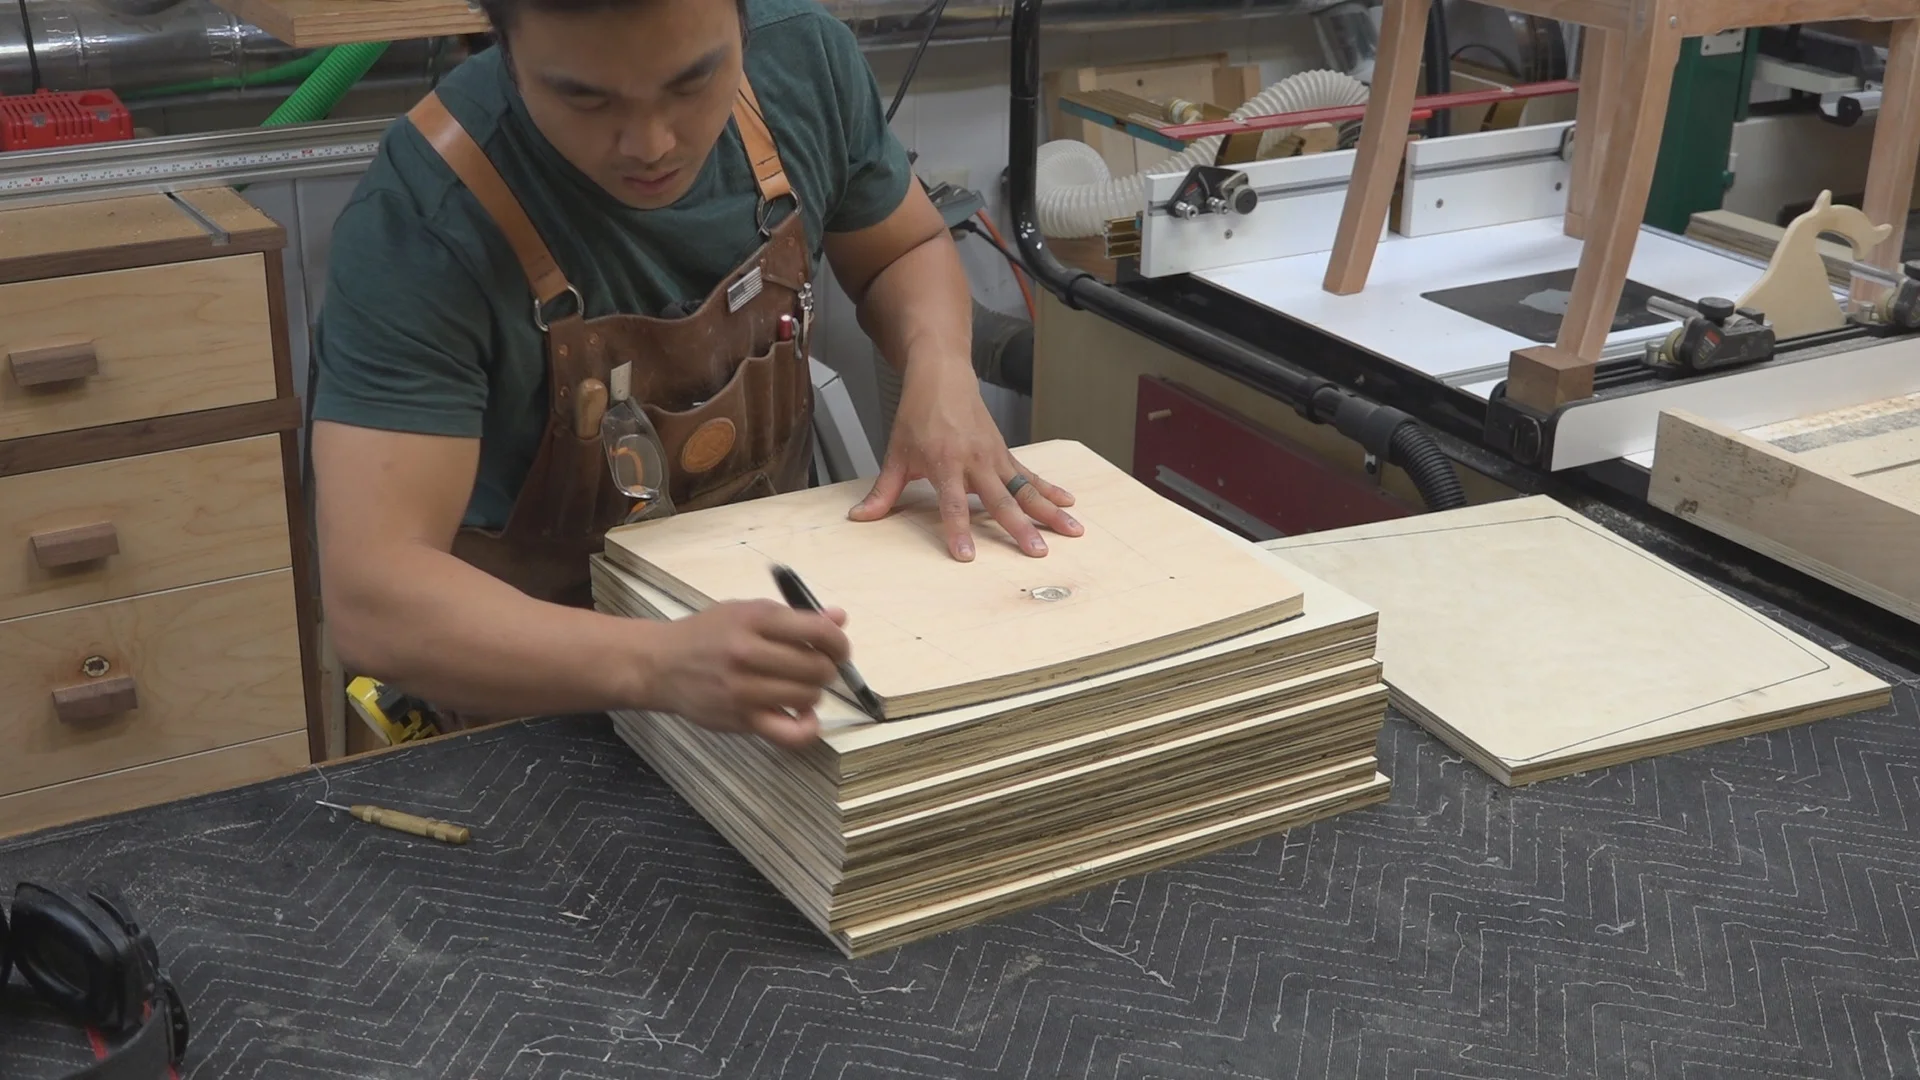
Tracing the outline of the chair insert template.
The chair inserts are rough cut on the bandsaw. I use some thin double stick tape to temporarily attach the template onto the plywood insert blanks. I used a pattern router bit on the router table to get a perfect match.
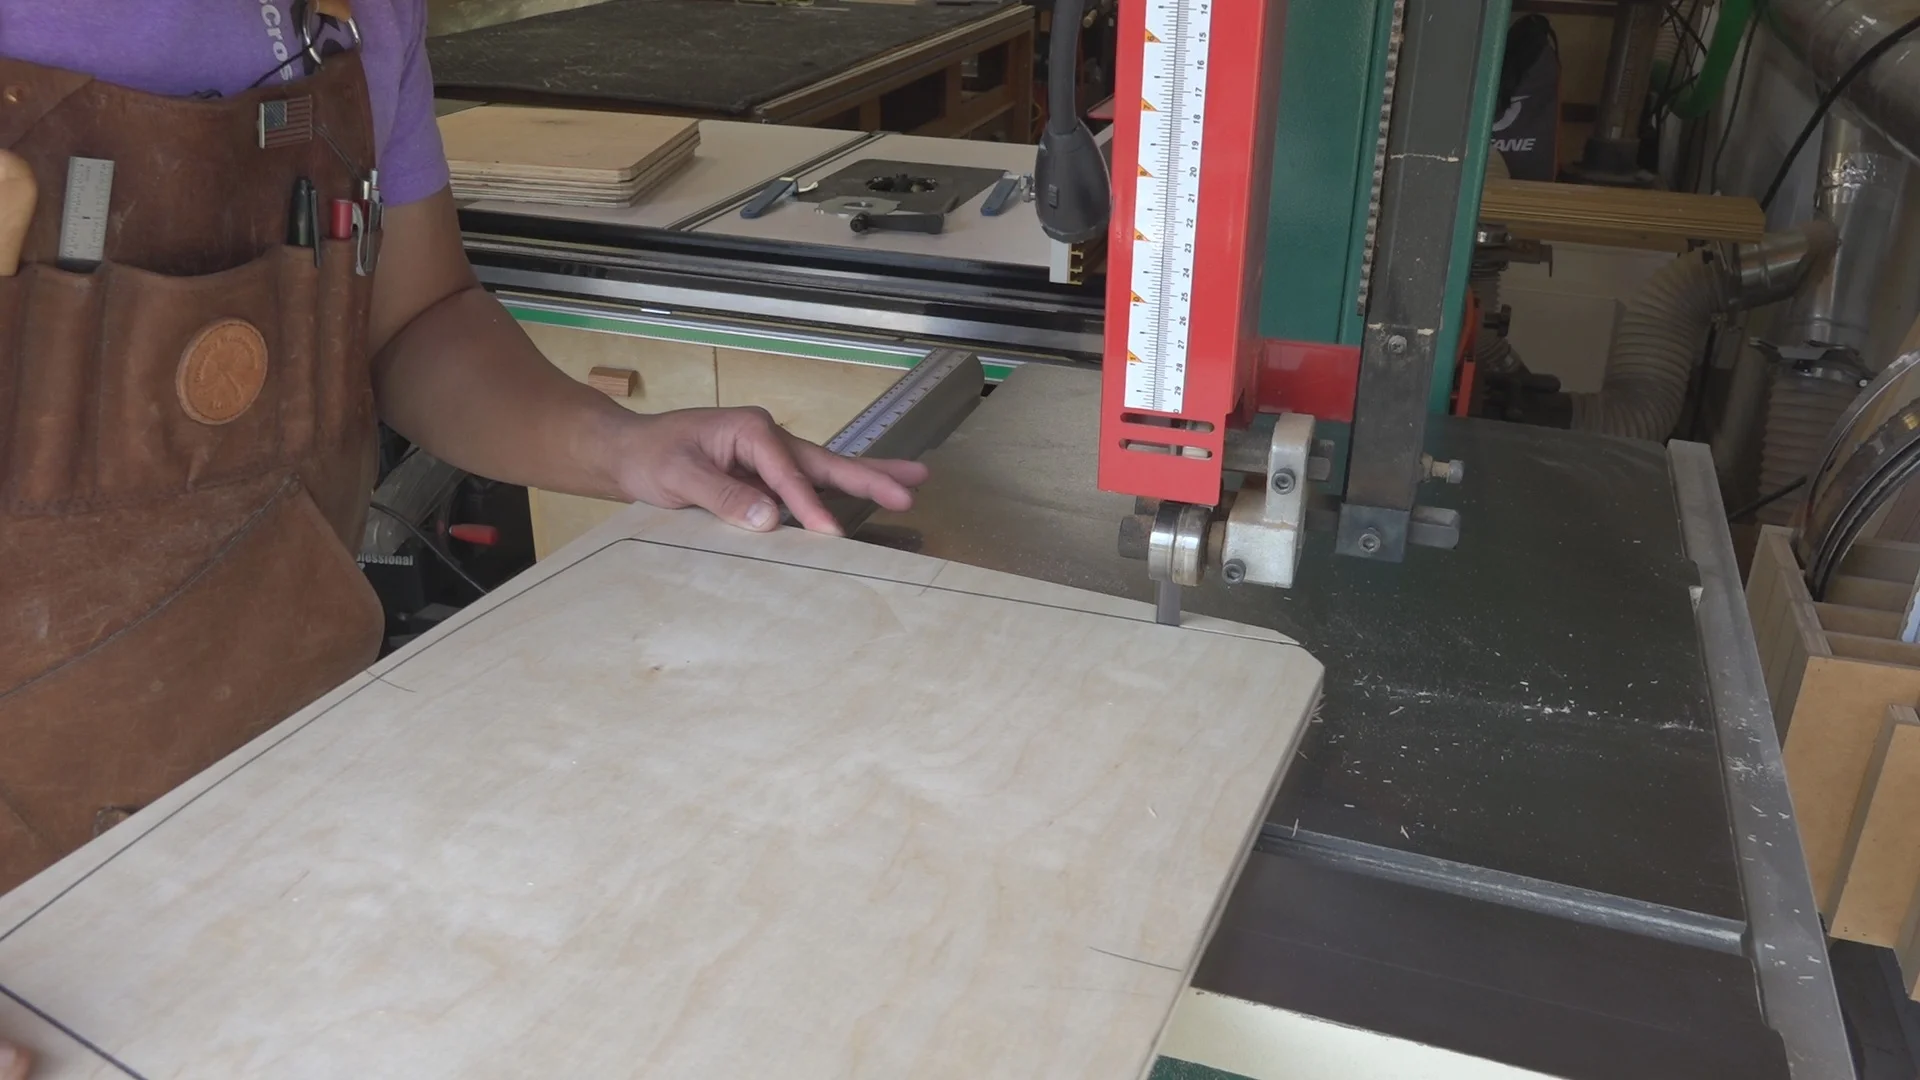
Rough cut the outline on the bandsaw.
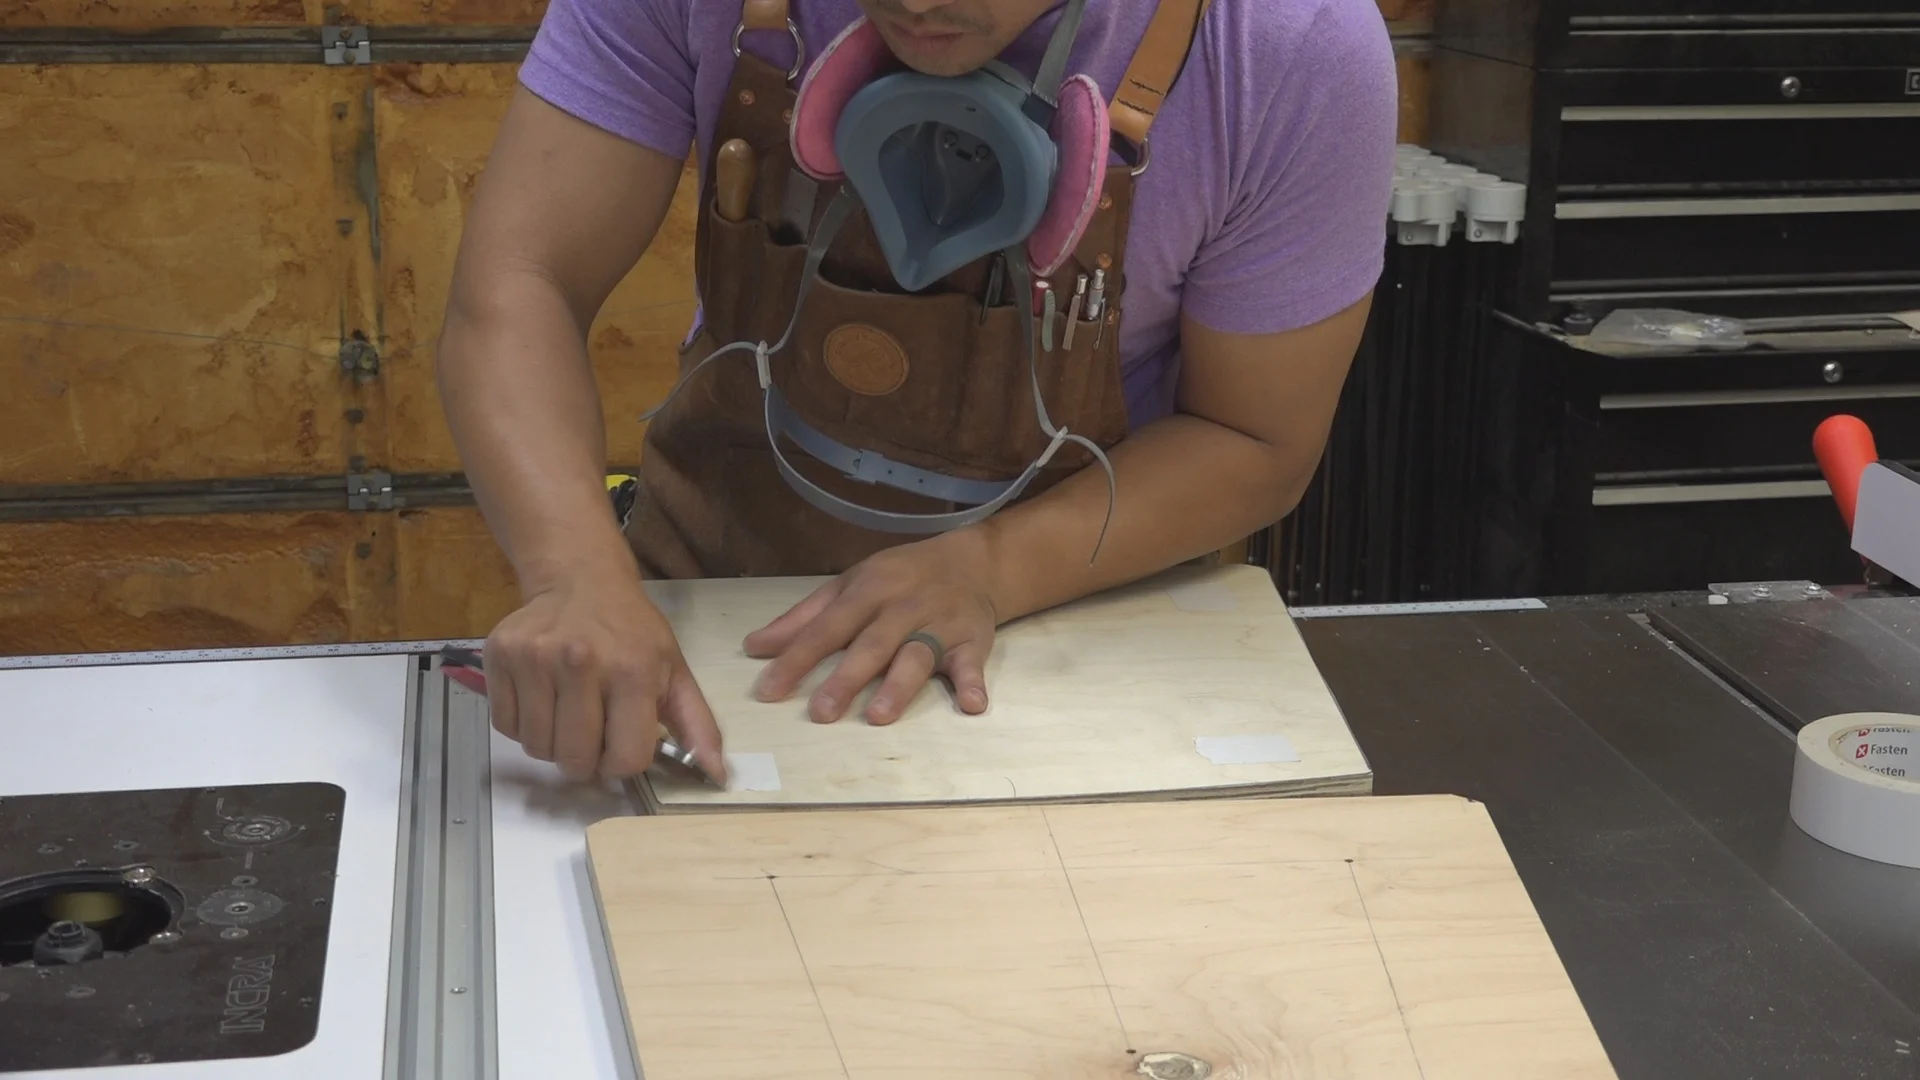
Using double stick tape to temporarily attach the template to the blank.
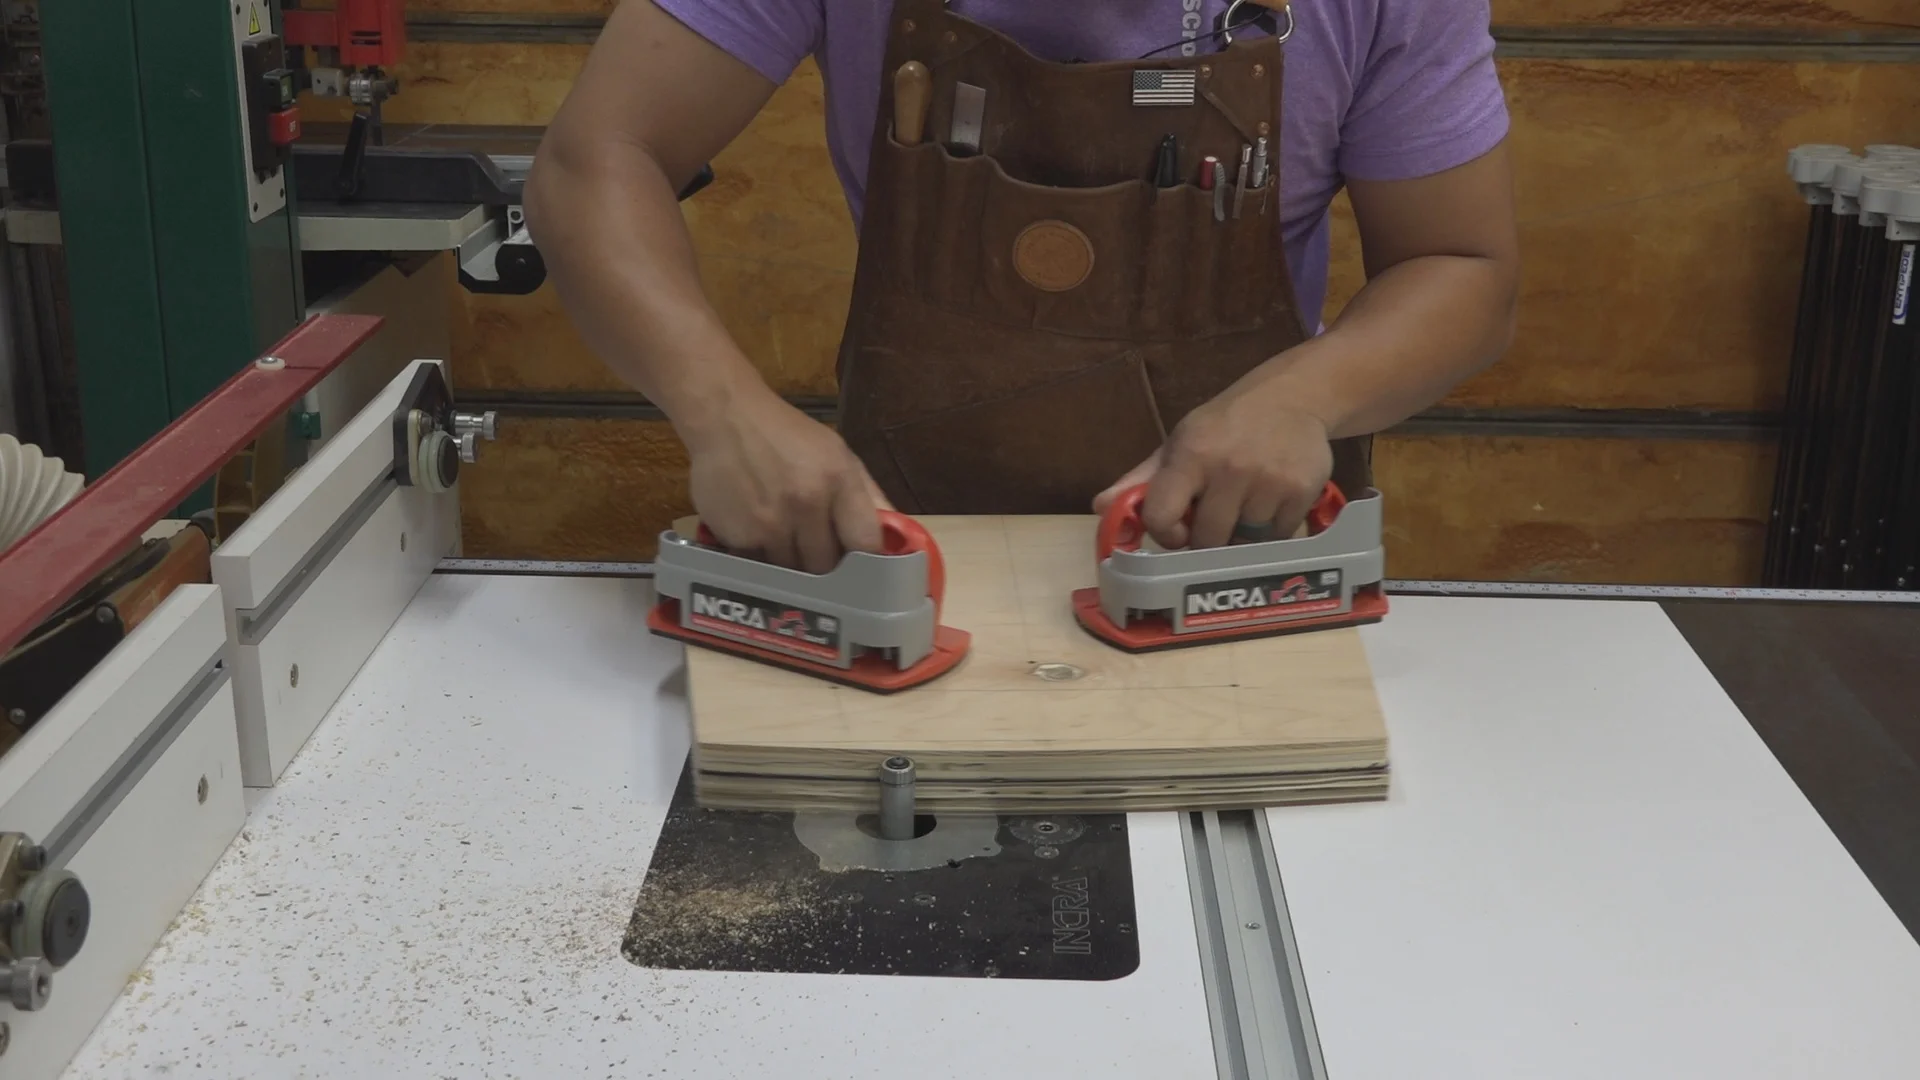
Cutting the final shape on the router table using a pattern router bit.
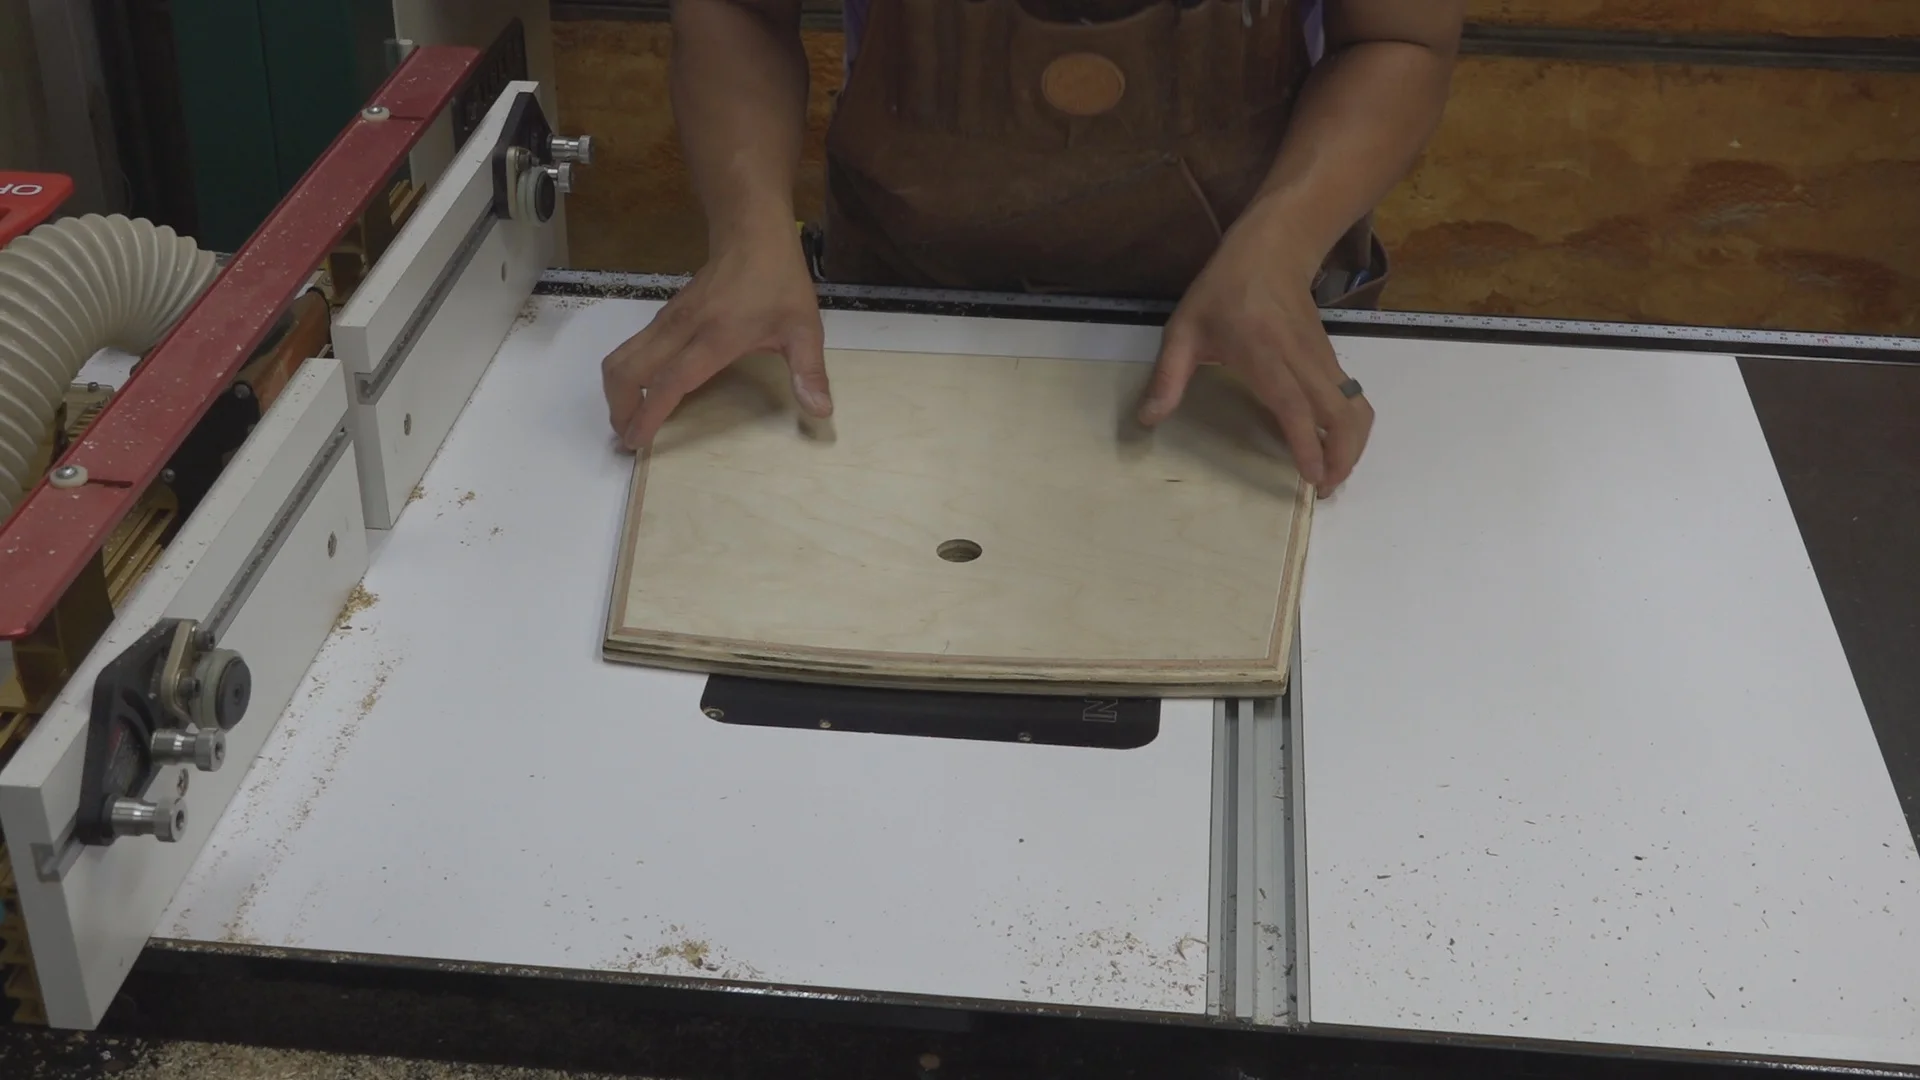
The bottom edge of the chair insert get a 1/8” round over to ensure the upholstery fabric doesn’t rip along the edge. The top edge of the chair insert get a 1/2” round over to help shape the 2” upholstery foam.
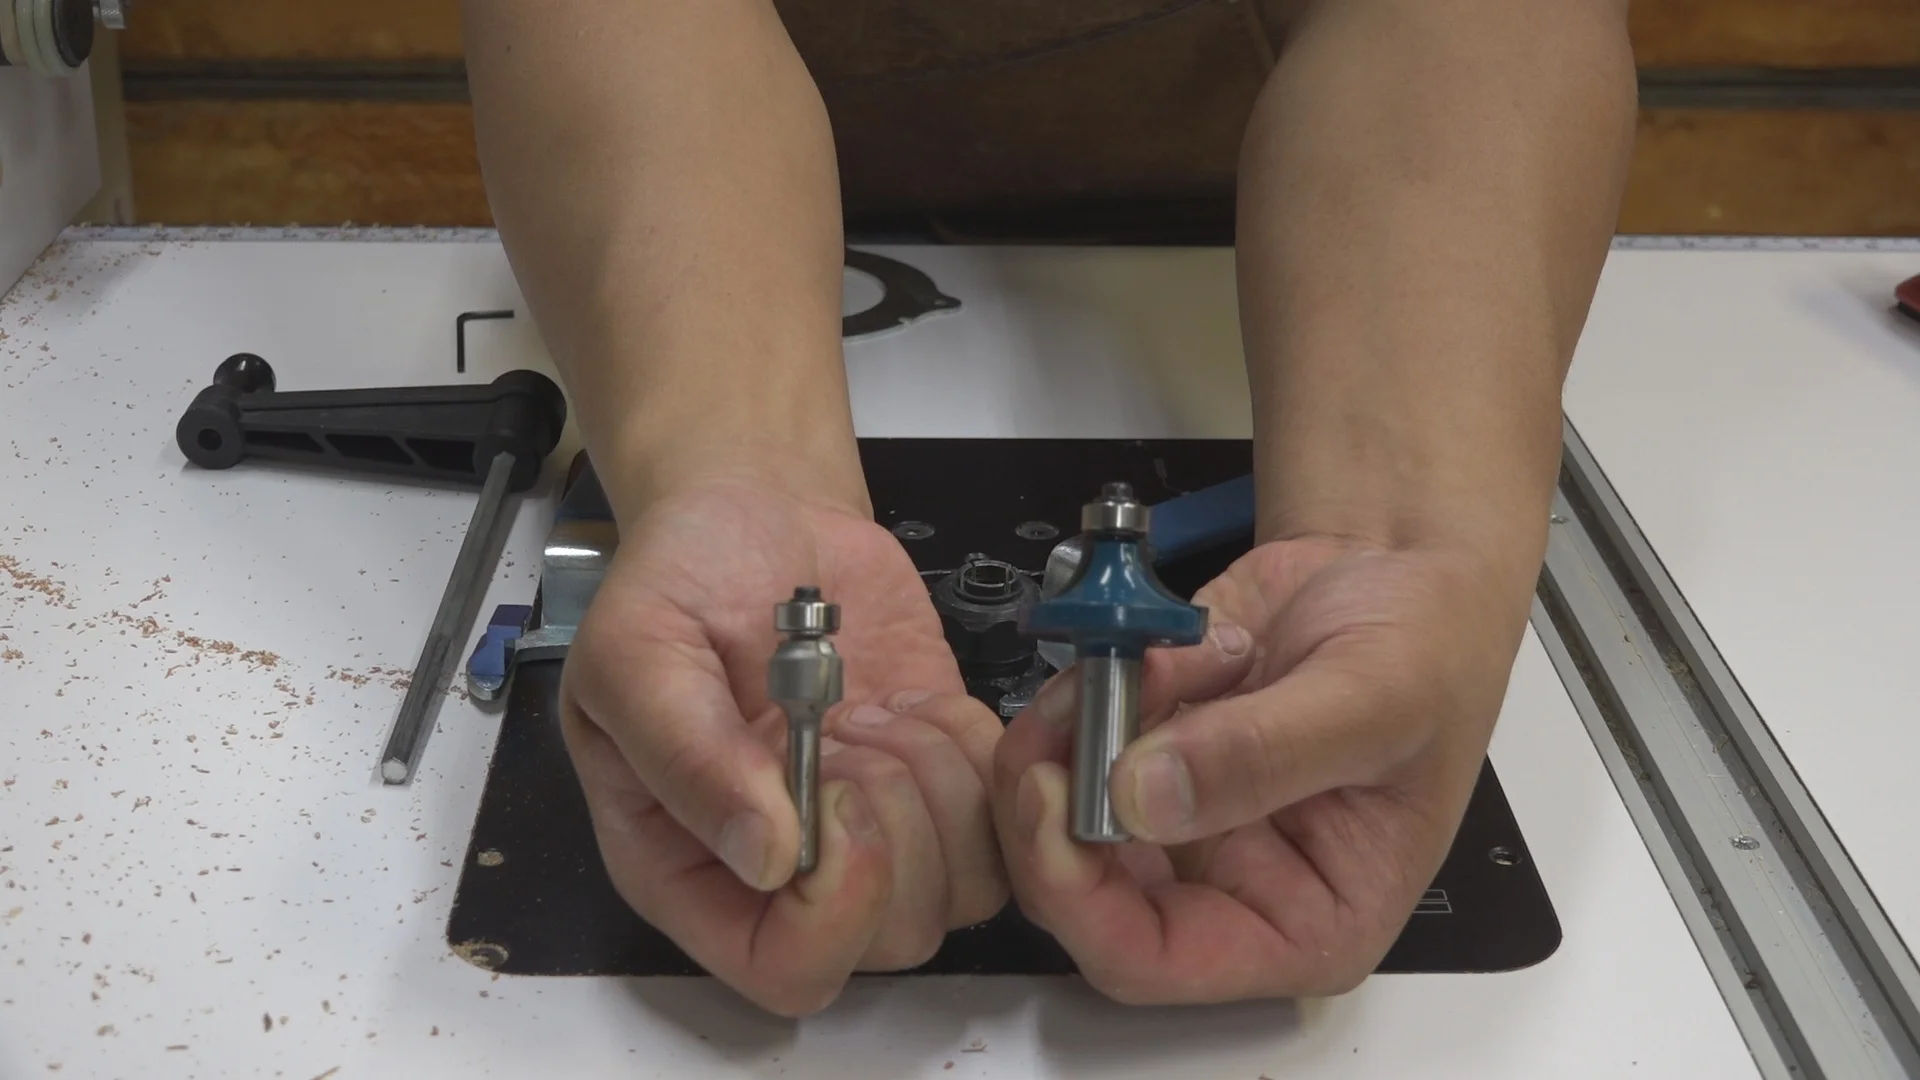
I used a 1/8” round over bit along the bottom edge of the chair insert and a 1/2” round over bit along the top edge of the chair insert.
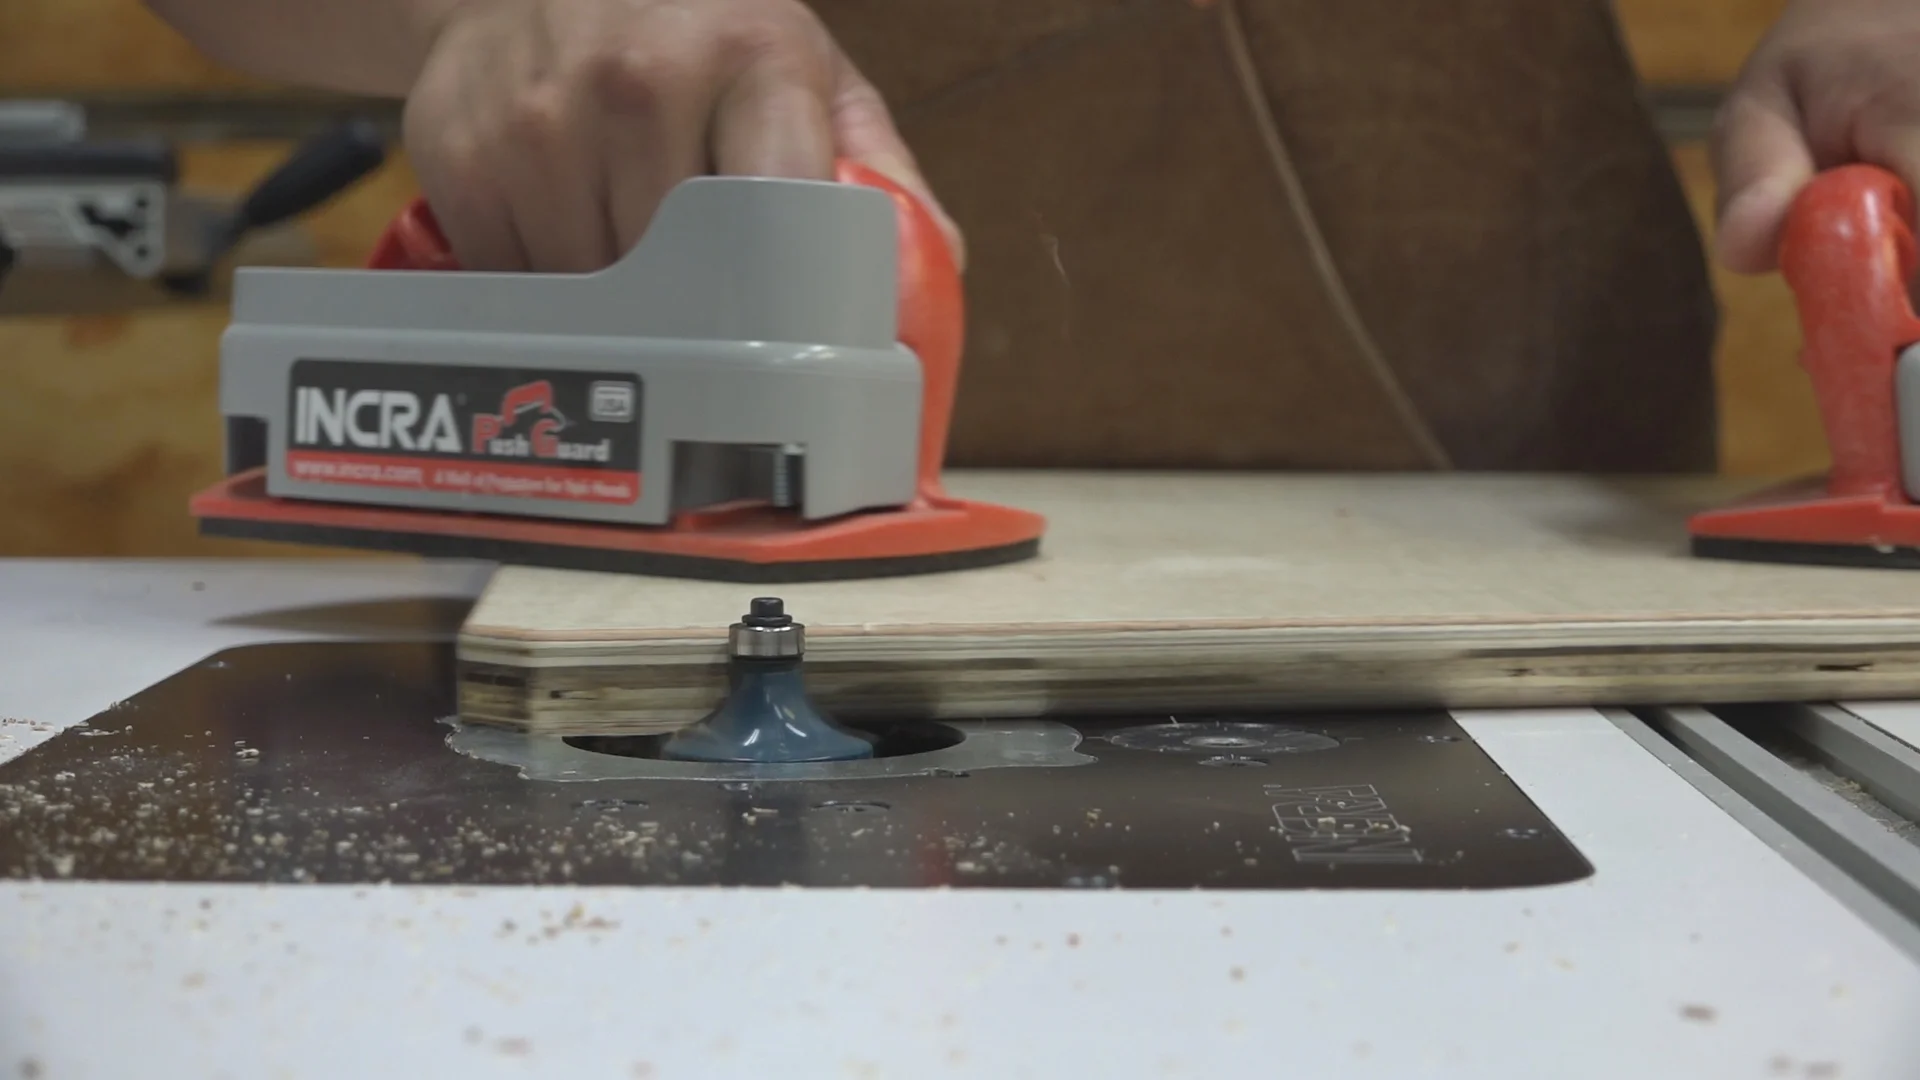
The bottom round over prevents upholstery fabric from ripping, and the top round helps shape the 2” upholstery foam.
To allow for air within the 2” upholstery foam to escape, a 1” hole was drilled towards the rear of the chair insert.
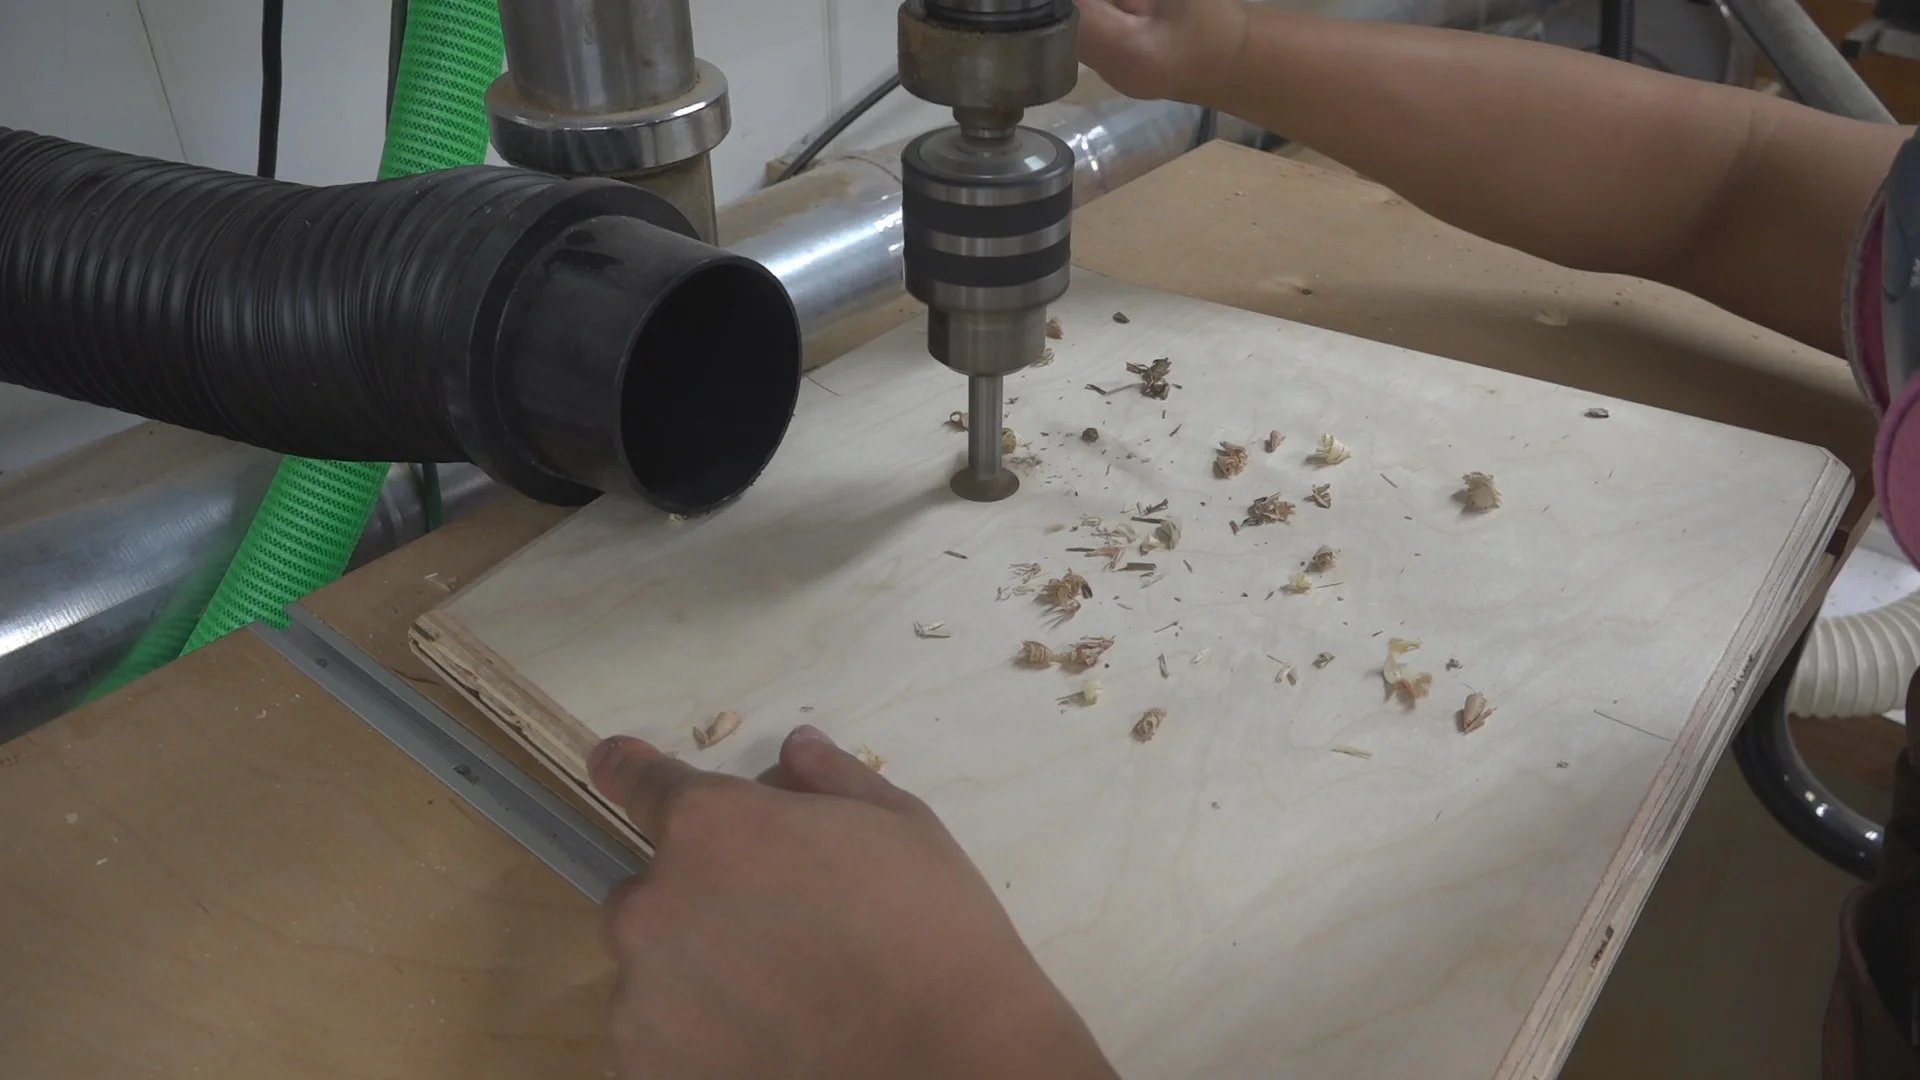
1” hole drilled towards the rear of the chair insert to allow air from the 2” upholstery foam to escape.
I ended up adding a 1/8” round over to the 1” hole to prevent the upholstery foam from getting cut along the edge.
Adding a 1/8” round over to the 1” relief hole.
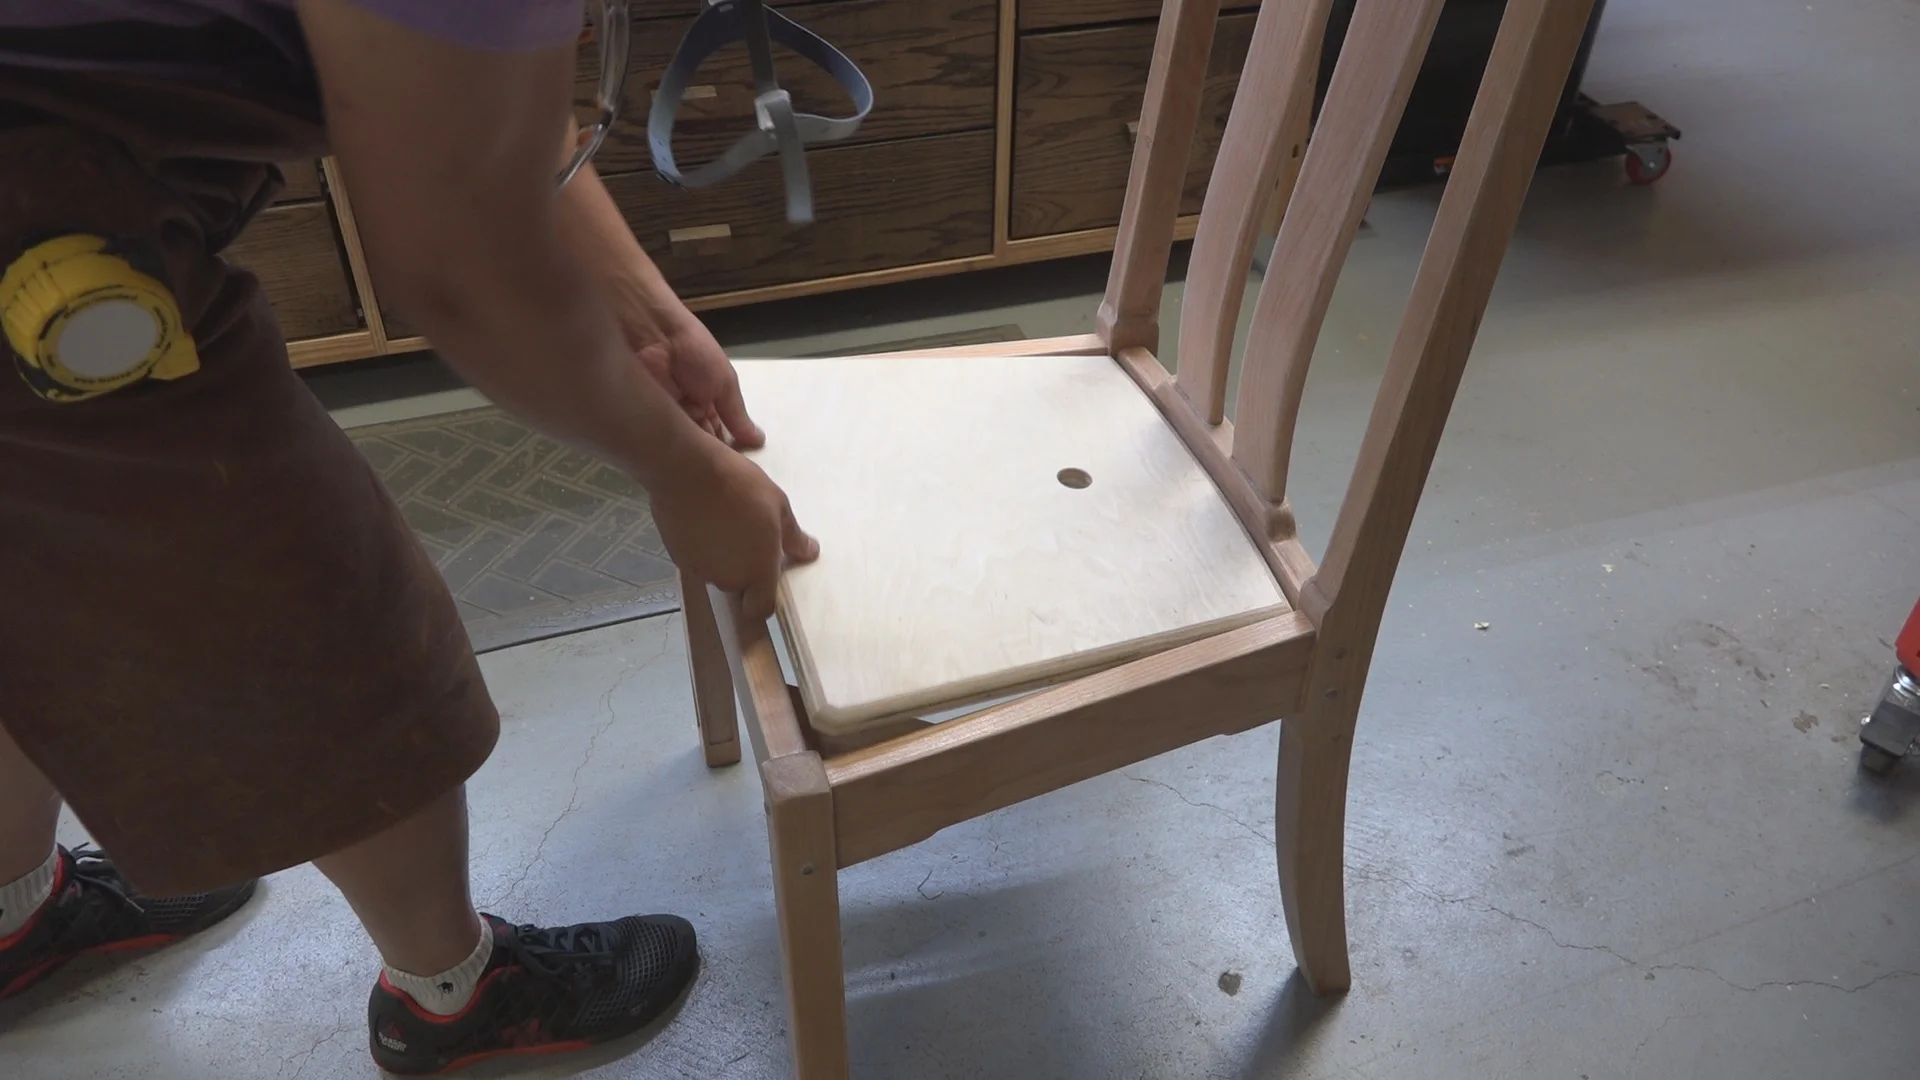
The chair inserts fit perfectly within the chair rails with about 1/4” relief on all sides to allow space for fabric.
Making and Installing Chair Corner Blocks
Corner blocks on chairs serve two purposes. The corner blocks offer rigidity to the chair rails and prevent the rails from racking. They also provide a platform for the a seat insert to sit on. Since I’m using an upholstered plywood seat insert, I decided to place the top of my corner blocks 3/4” below the top surface of the chair rails.
*This post is sponsored by The Home Depot
Links below are affiliate links, clicking on them helps me keep this site going at no extra cost to you . Thank you for supporting my site.
The corner blocks provide rigidity to the chair rails and a platform for the chair insert to sit atop.
Corner blocks on chairs serve two purposes. The corner blocks offer rigidity to the chair rails and prevent the rails from racking. They also provide a platform for the a seat insert to sit on. Since I’m using an upholstered plywood seat insert, I decided to place the top of my corner blocks 3/4” below the top surface of the chair rails.
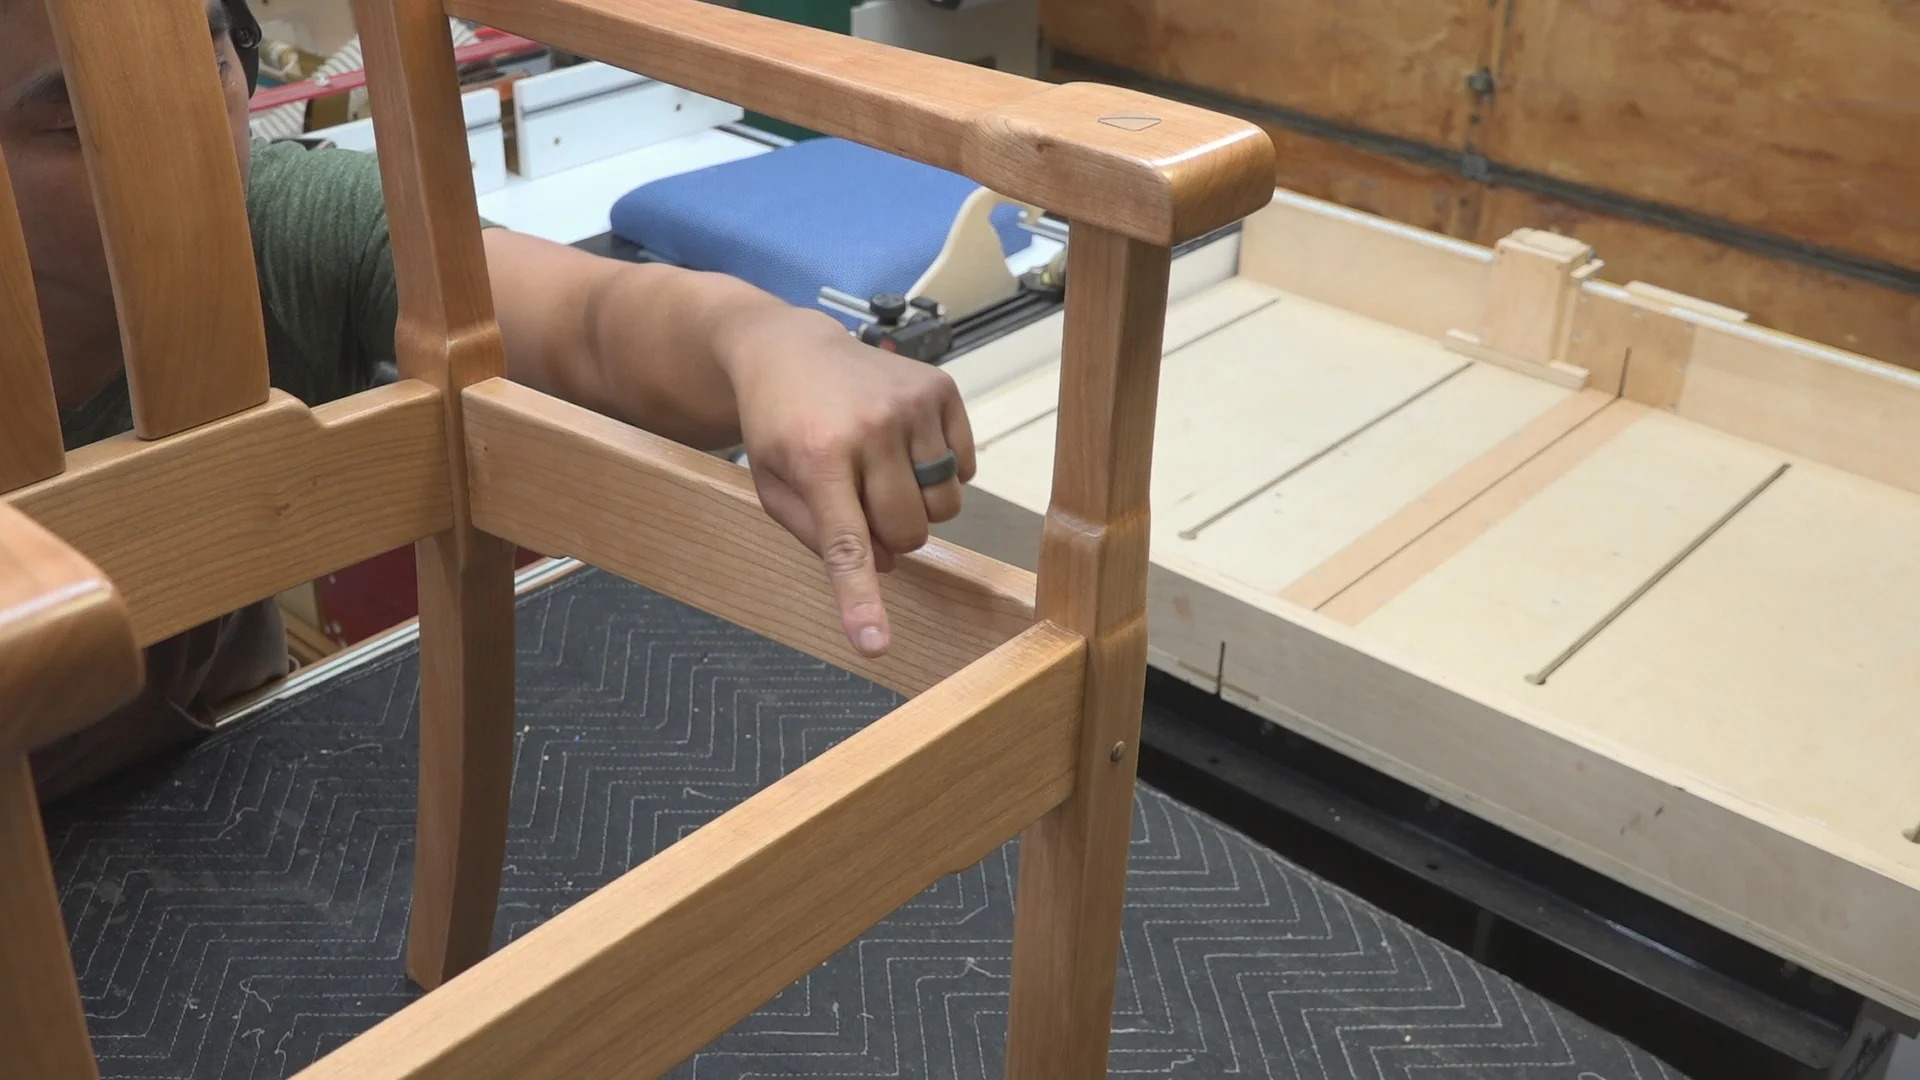
The corner blocks are placed diagonally between chair rails.
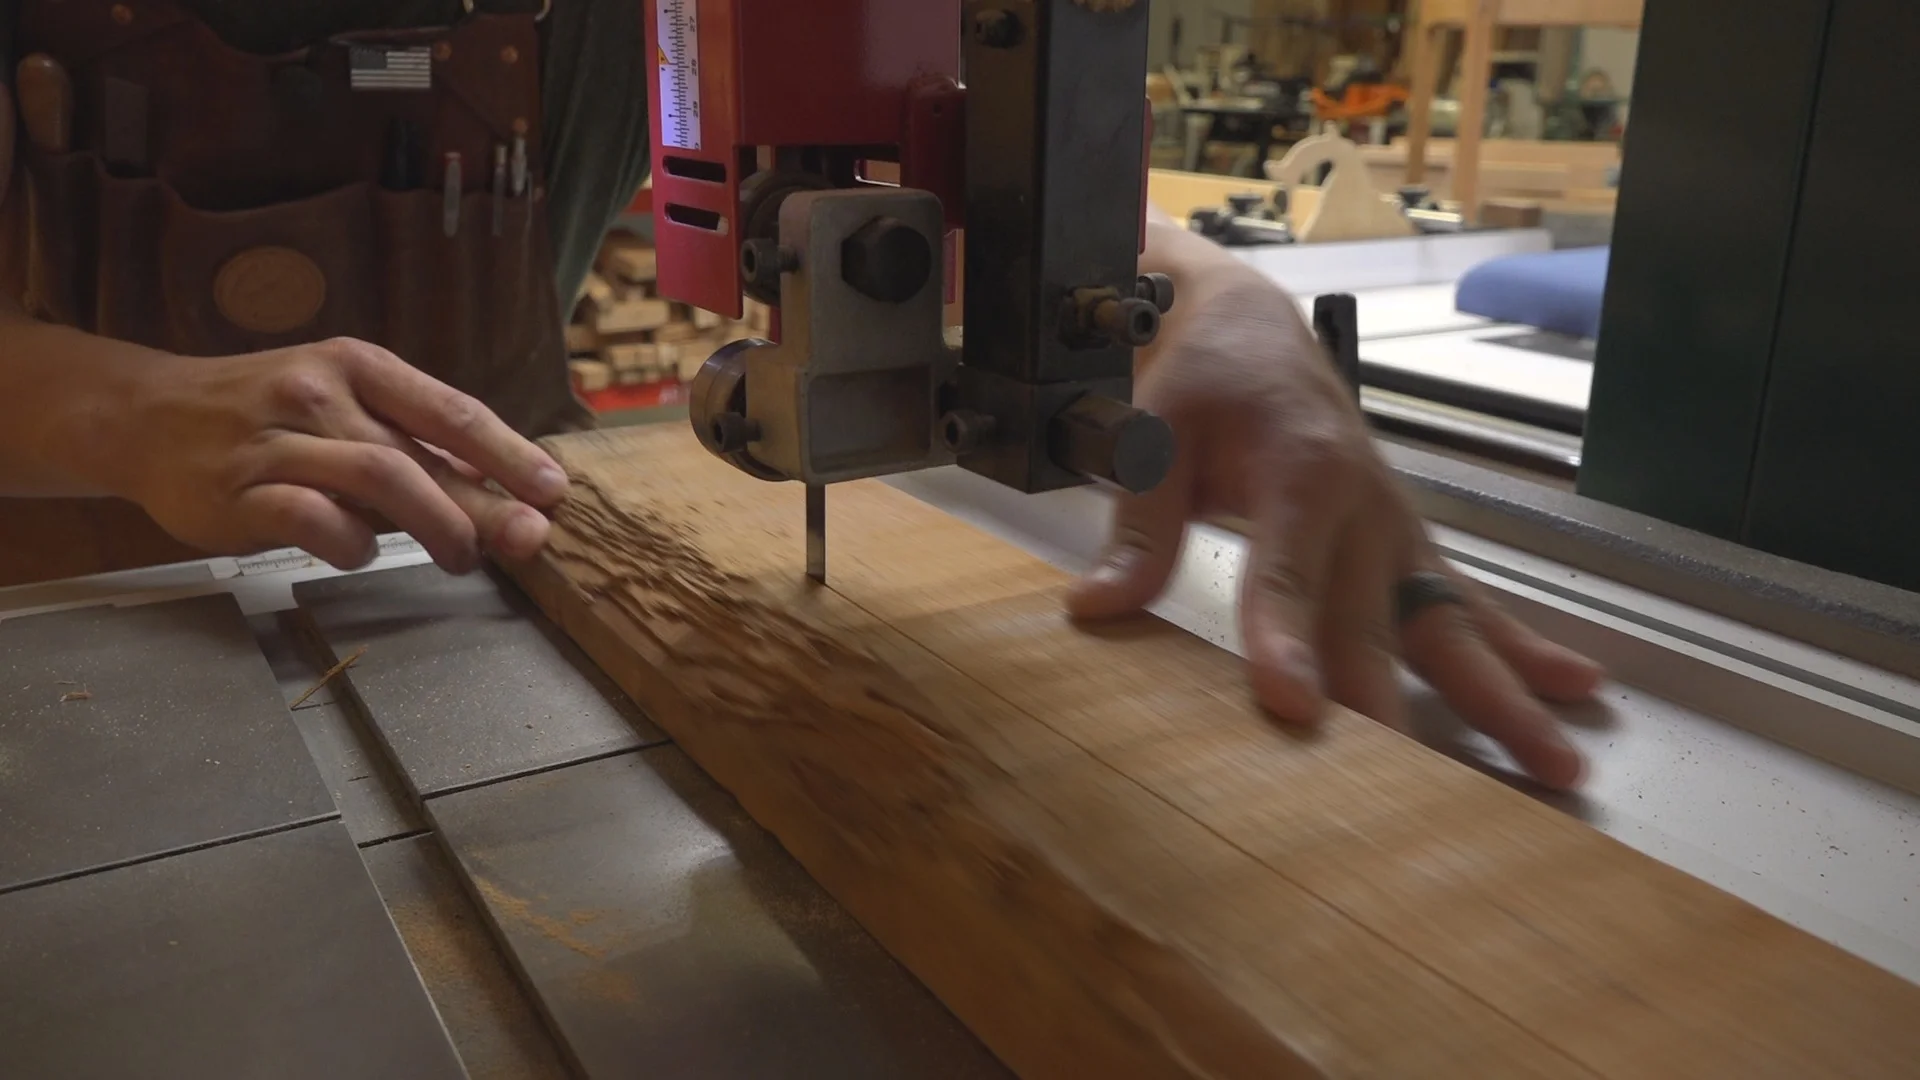
Ripping Cherry to rough width.
I first rip 5/4 Cherry stock to rough width on the bandsaw. In this case, I made the cut at 2-5/8” wide. This is the safest way to rip rough sawn lumber. I then go to the jointer to flatten material and create a 90 degree edge. I then run the material through the planer to a final thickness of 1” and final width of 2-1/2”.
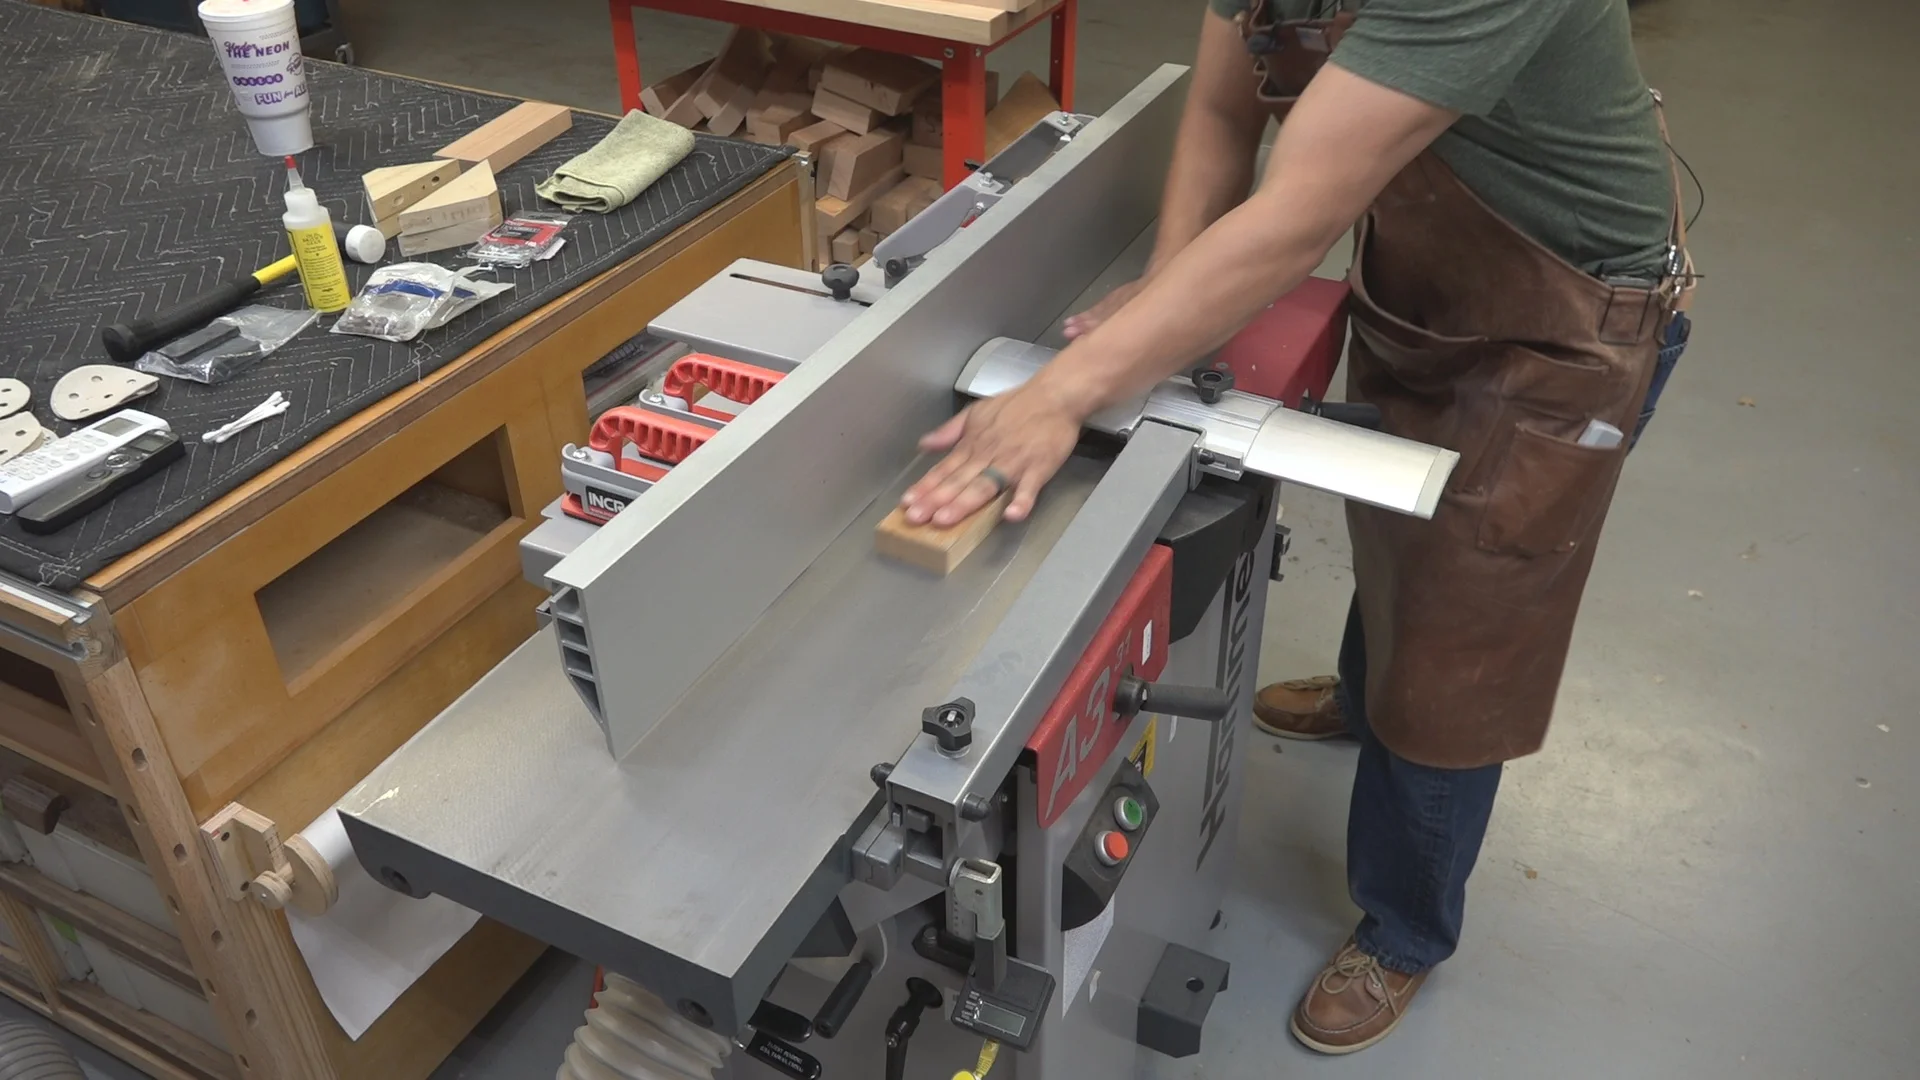
I first flatten the face.
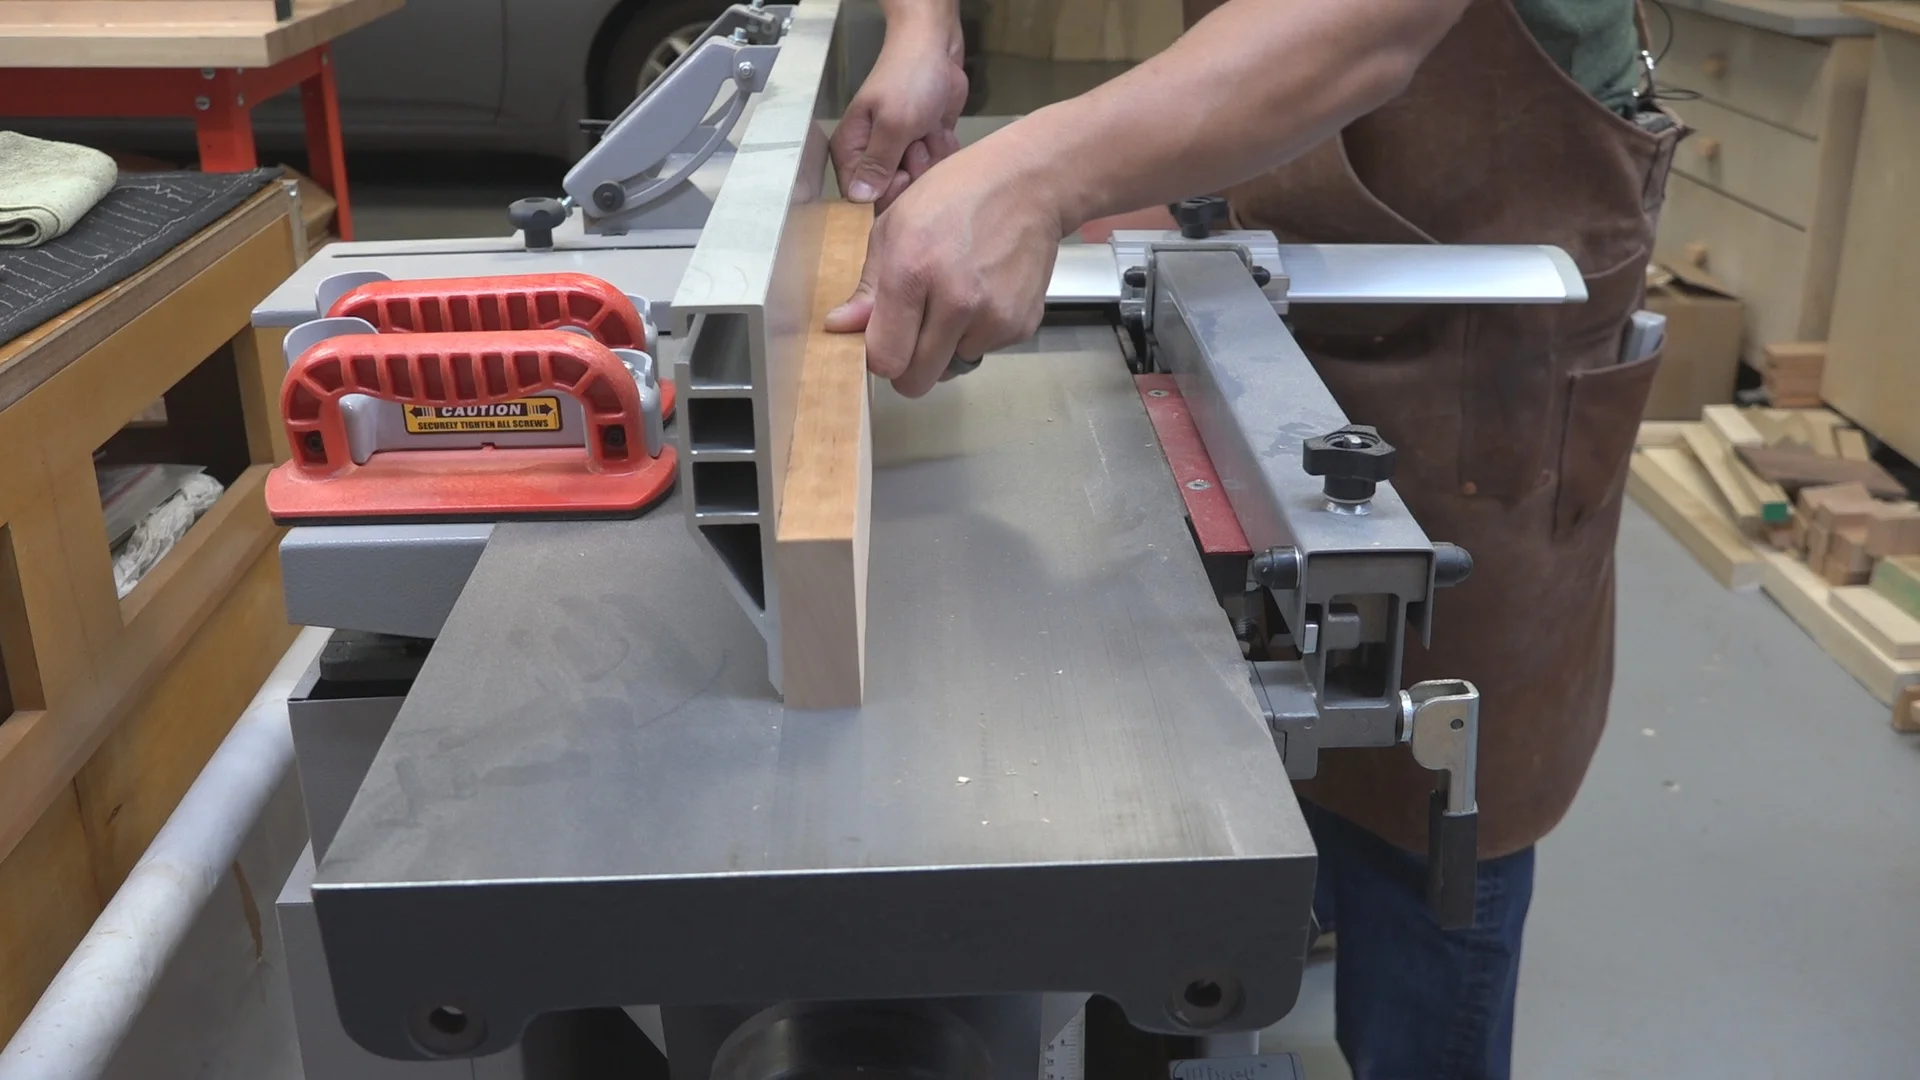
I then joint the edge perpendicular to the flattened face.
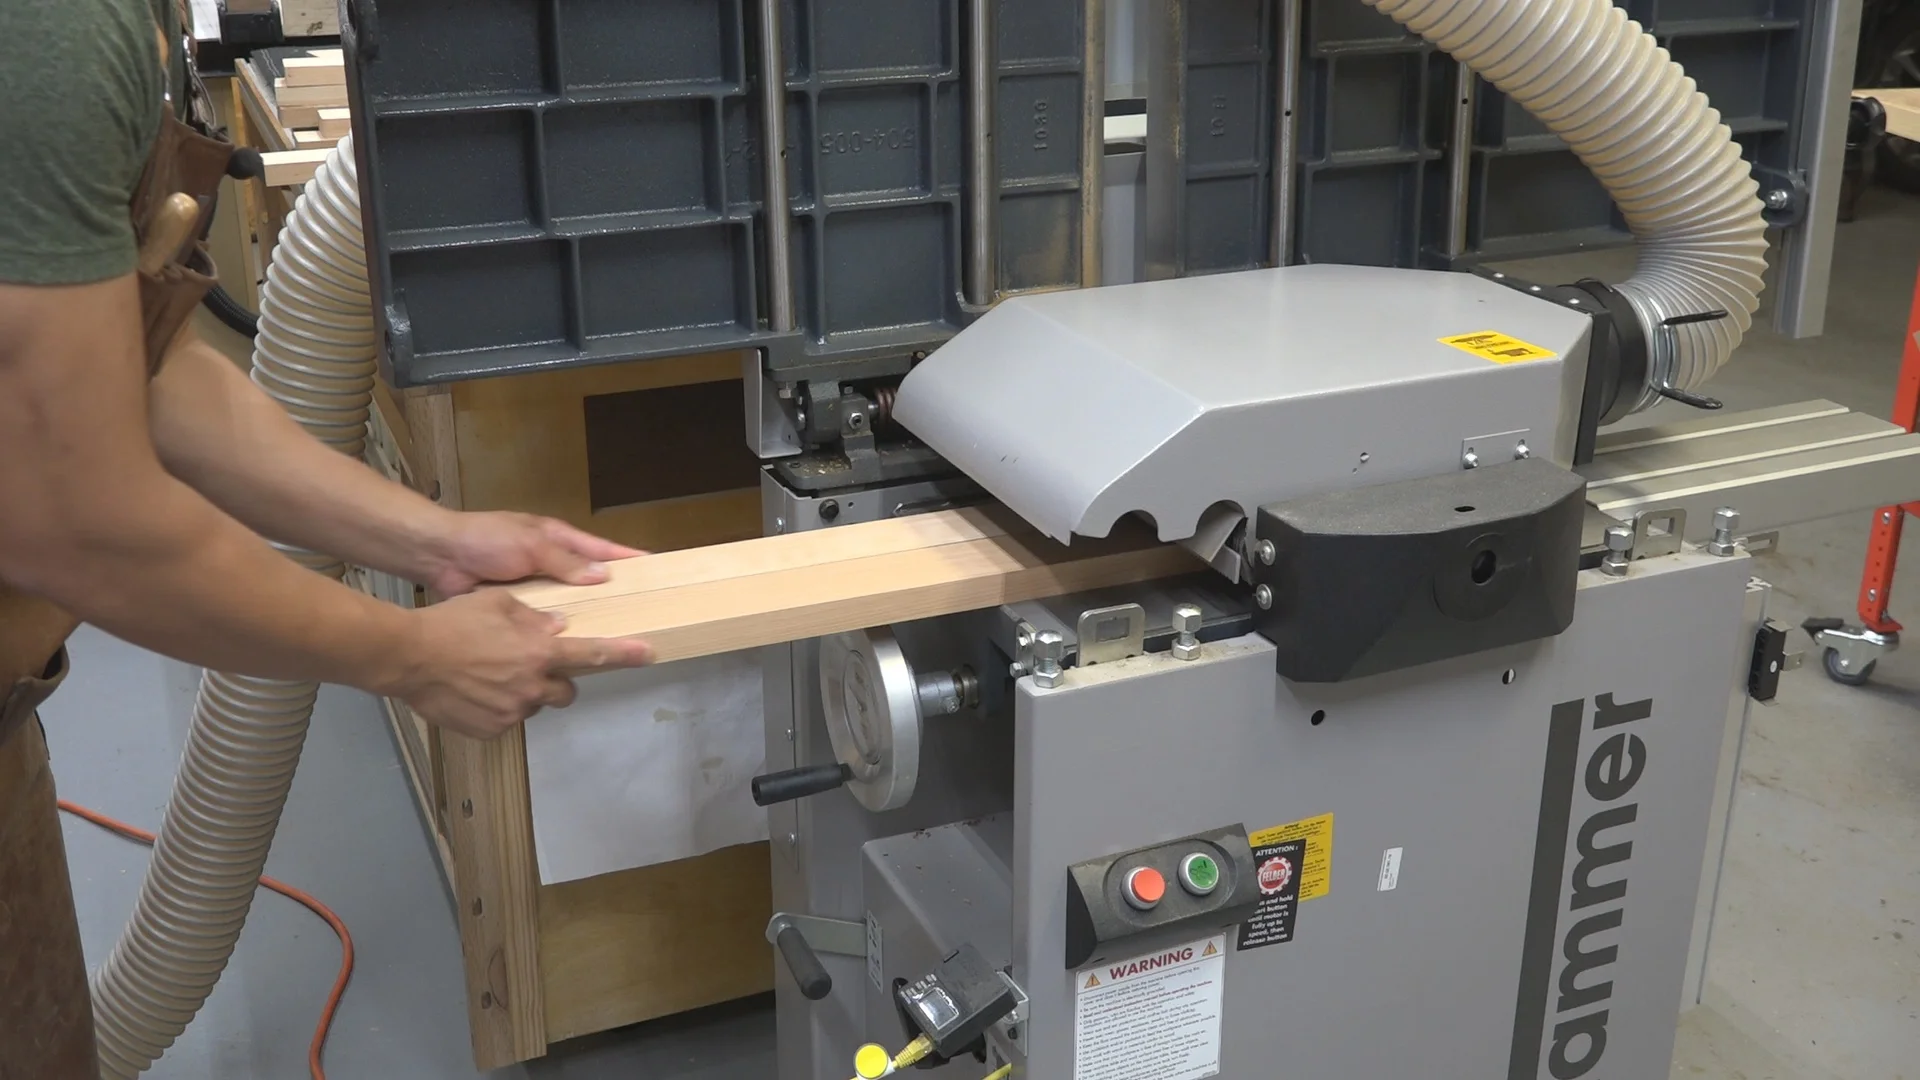
Planing to final thickness (1”) and final width (2-1/2”)
The front corner blocks are cut at 45 degrees and 53 degrees. I first cut the 45 degree miter and then the 53 degree miter on the miter saw. The length of these blocks is not that important but I made sure that the corner blocks were long enough to ensure they would clear the front chair legs.
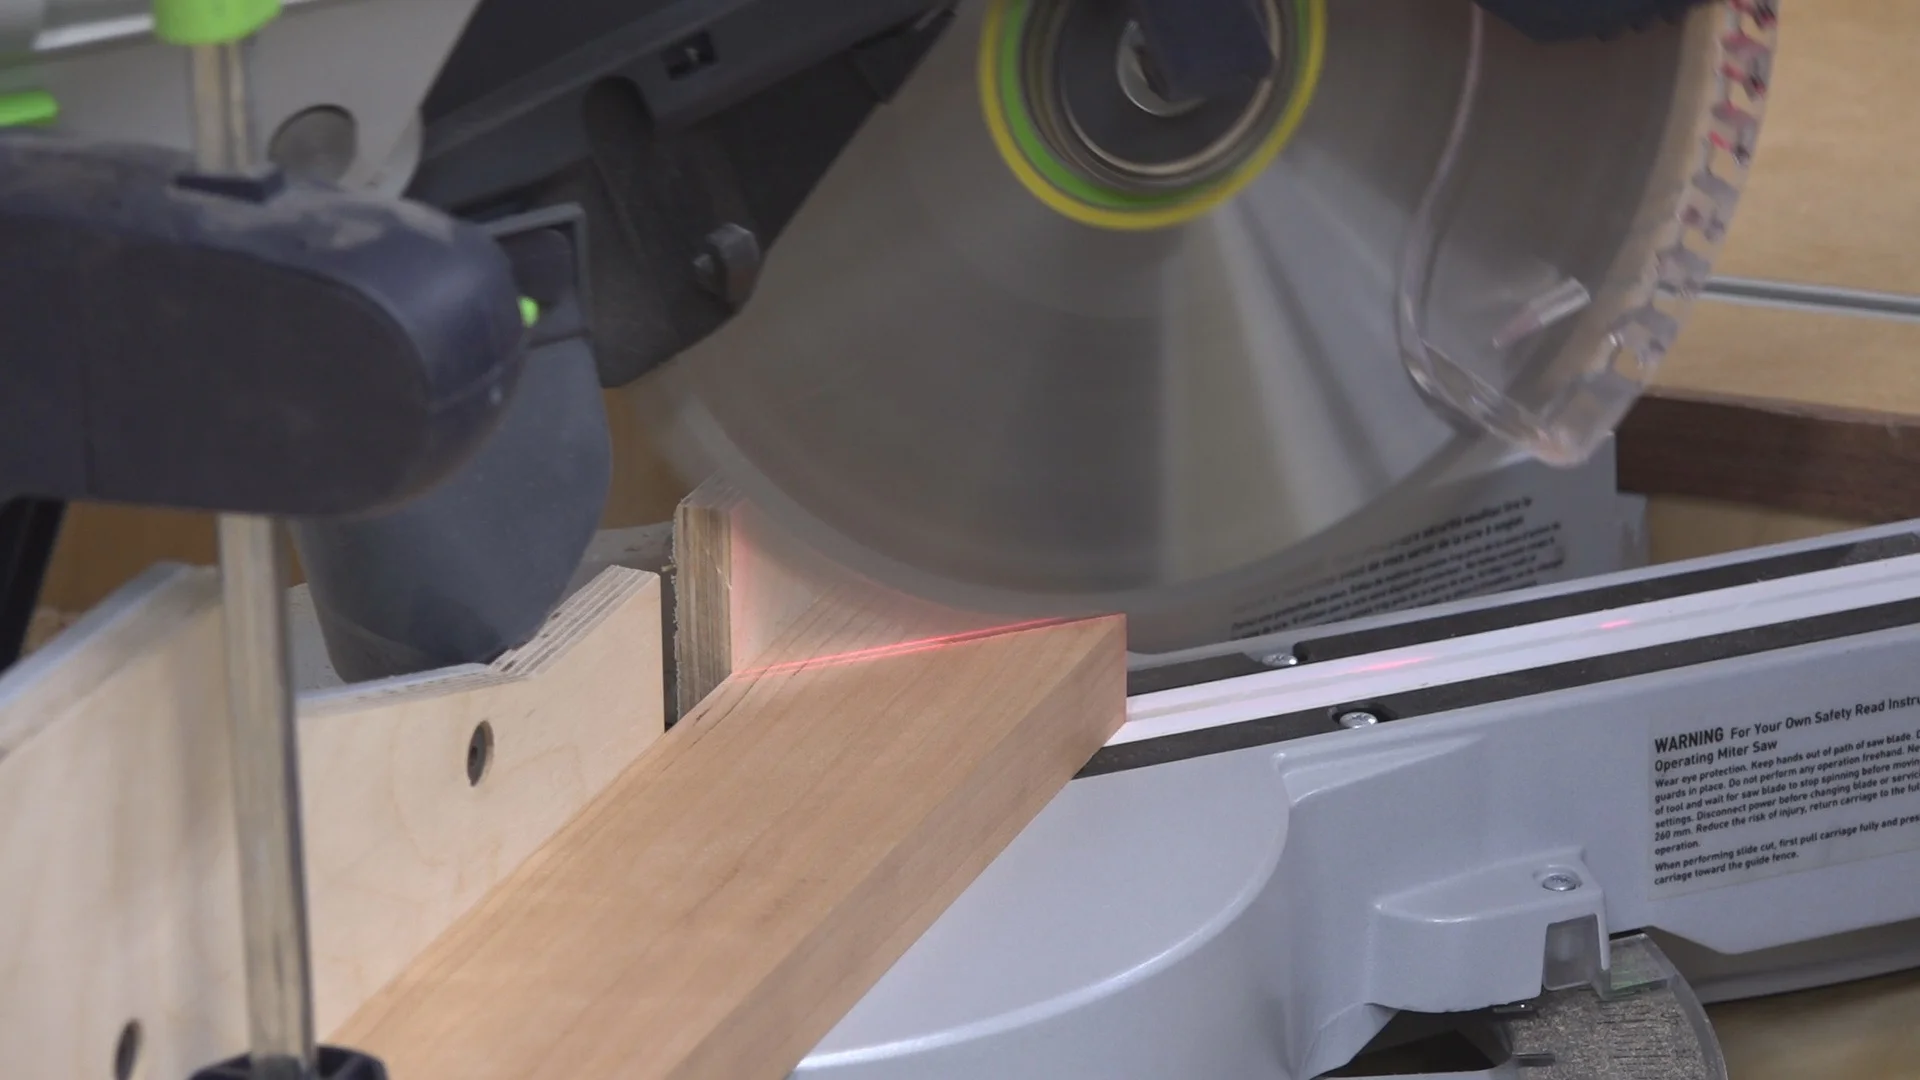
I first cut the 45 degree miter on the miter saw.
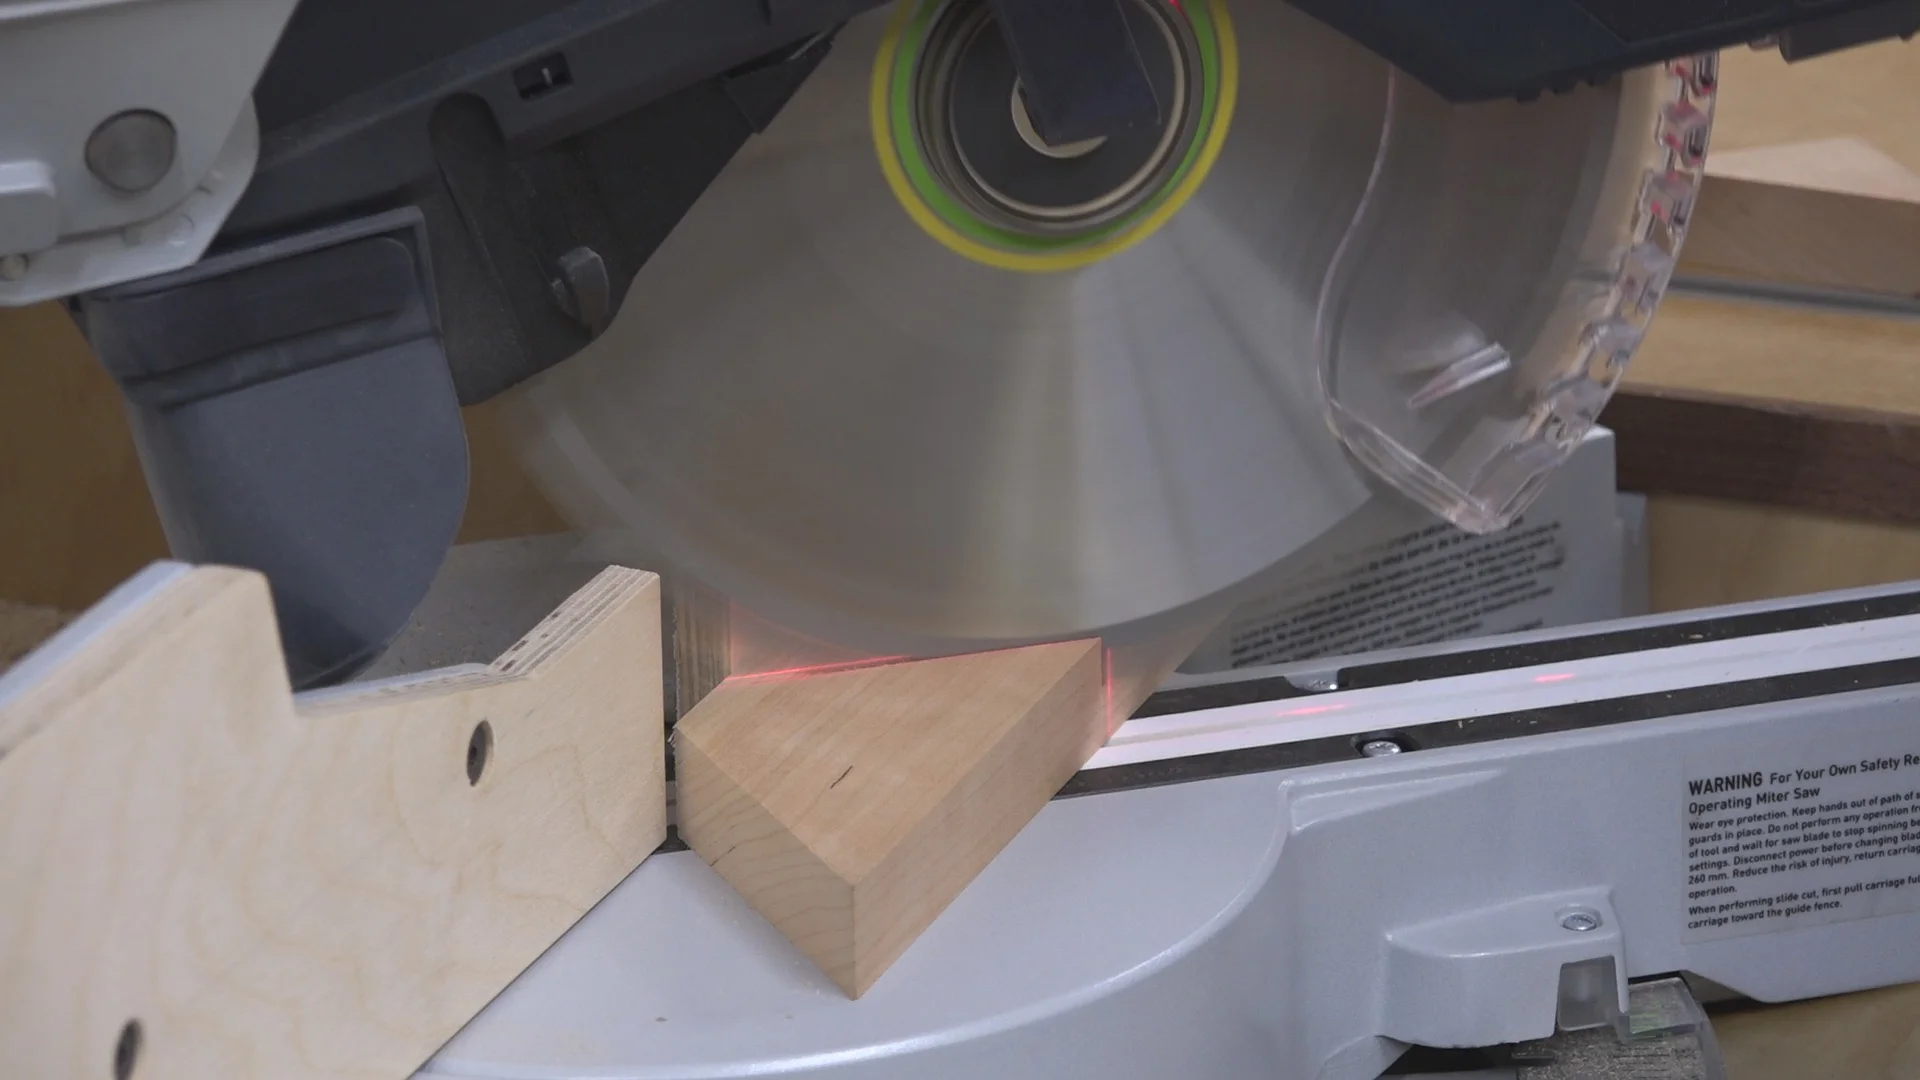
I then cut the 53 degree miter on the miter saw.
The counter bored 3/8” holes in the corner blocks were drilled on the drill press using a Forstner bit. I used a shop made drill press fence on my drill press table, a stop block, and a hand screw clamp to offer lateral support to the work piece.
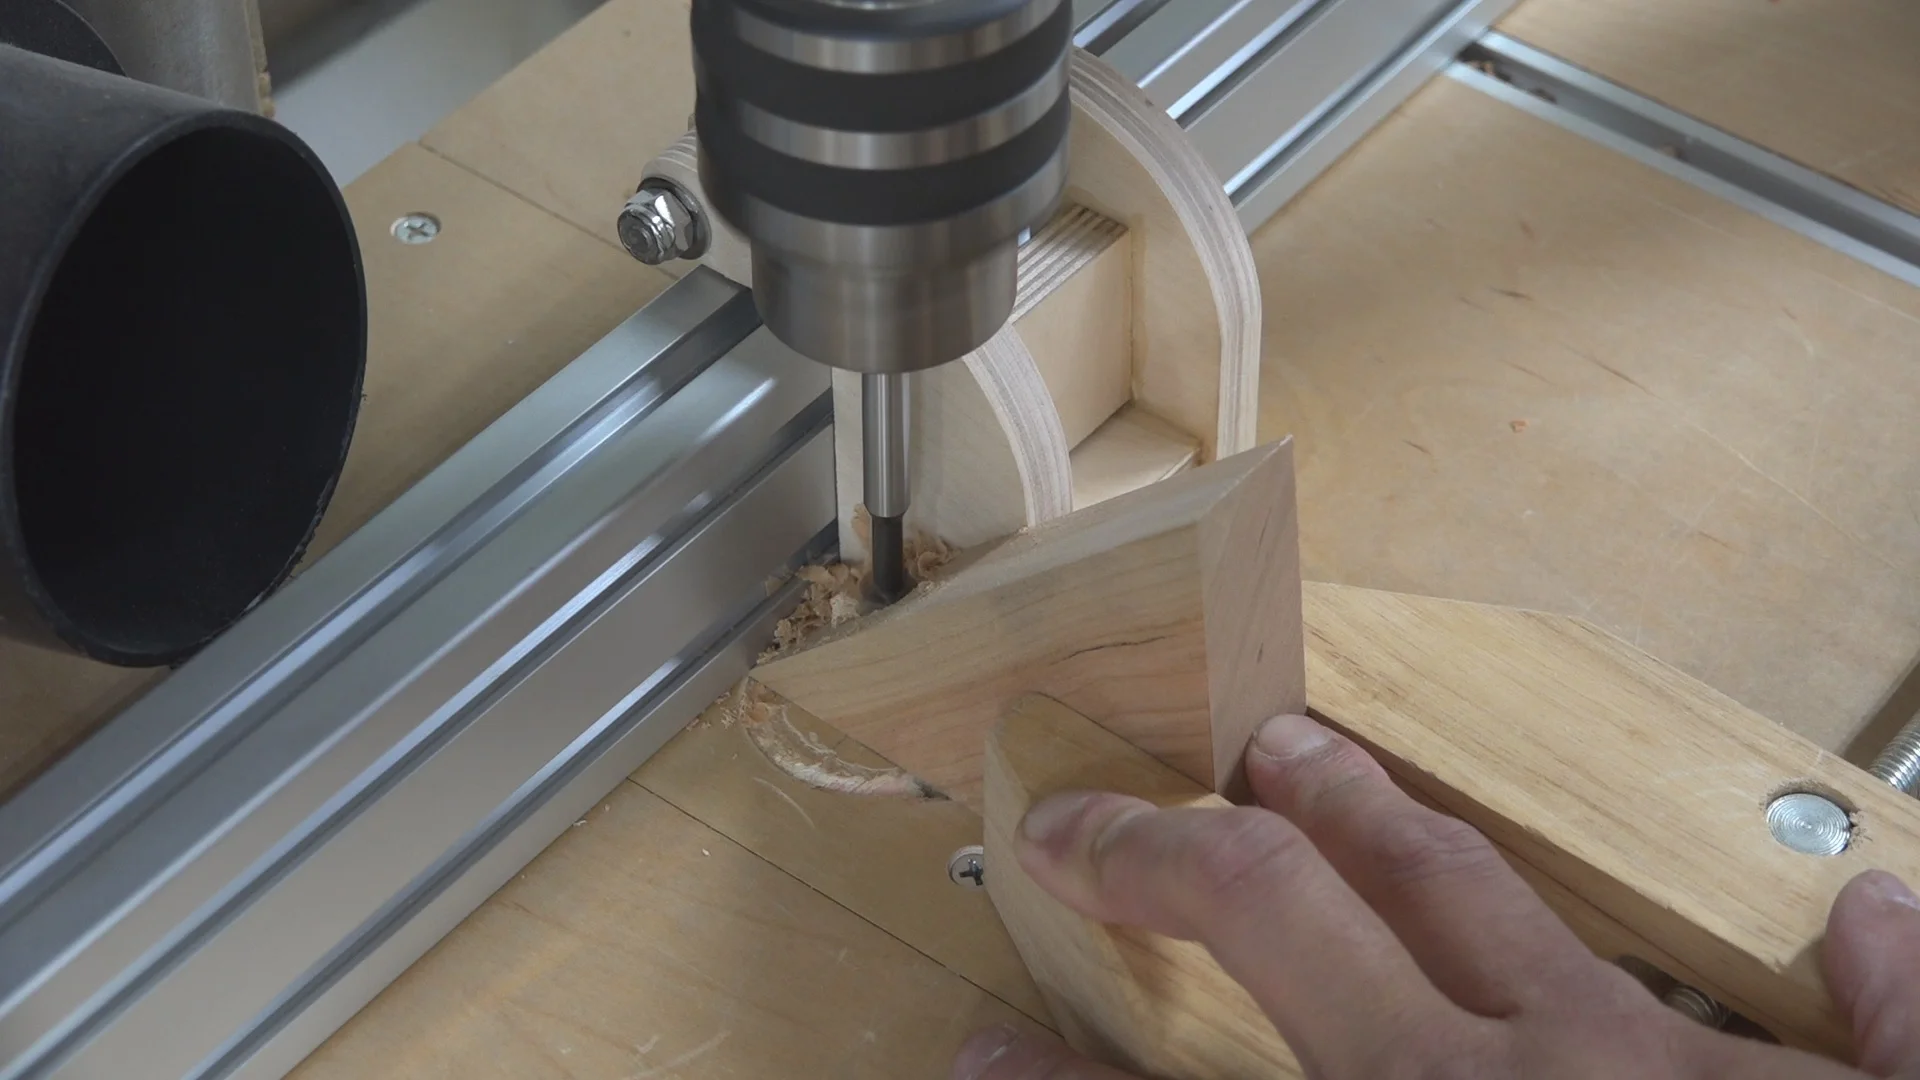
The drill press fence, stop block, and hand screw clamp helps support the work piece while drilling an angled surface.
To make sure each corner block is attached at the proper height, I used a jig and spring clamp to reference the proper height. This jig is nothing more than two pieces of the 1/2” plywood attached at a right angle.
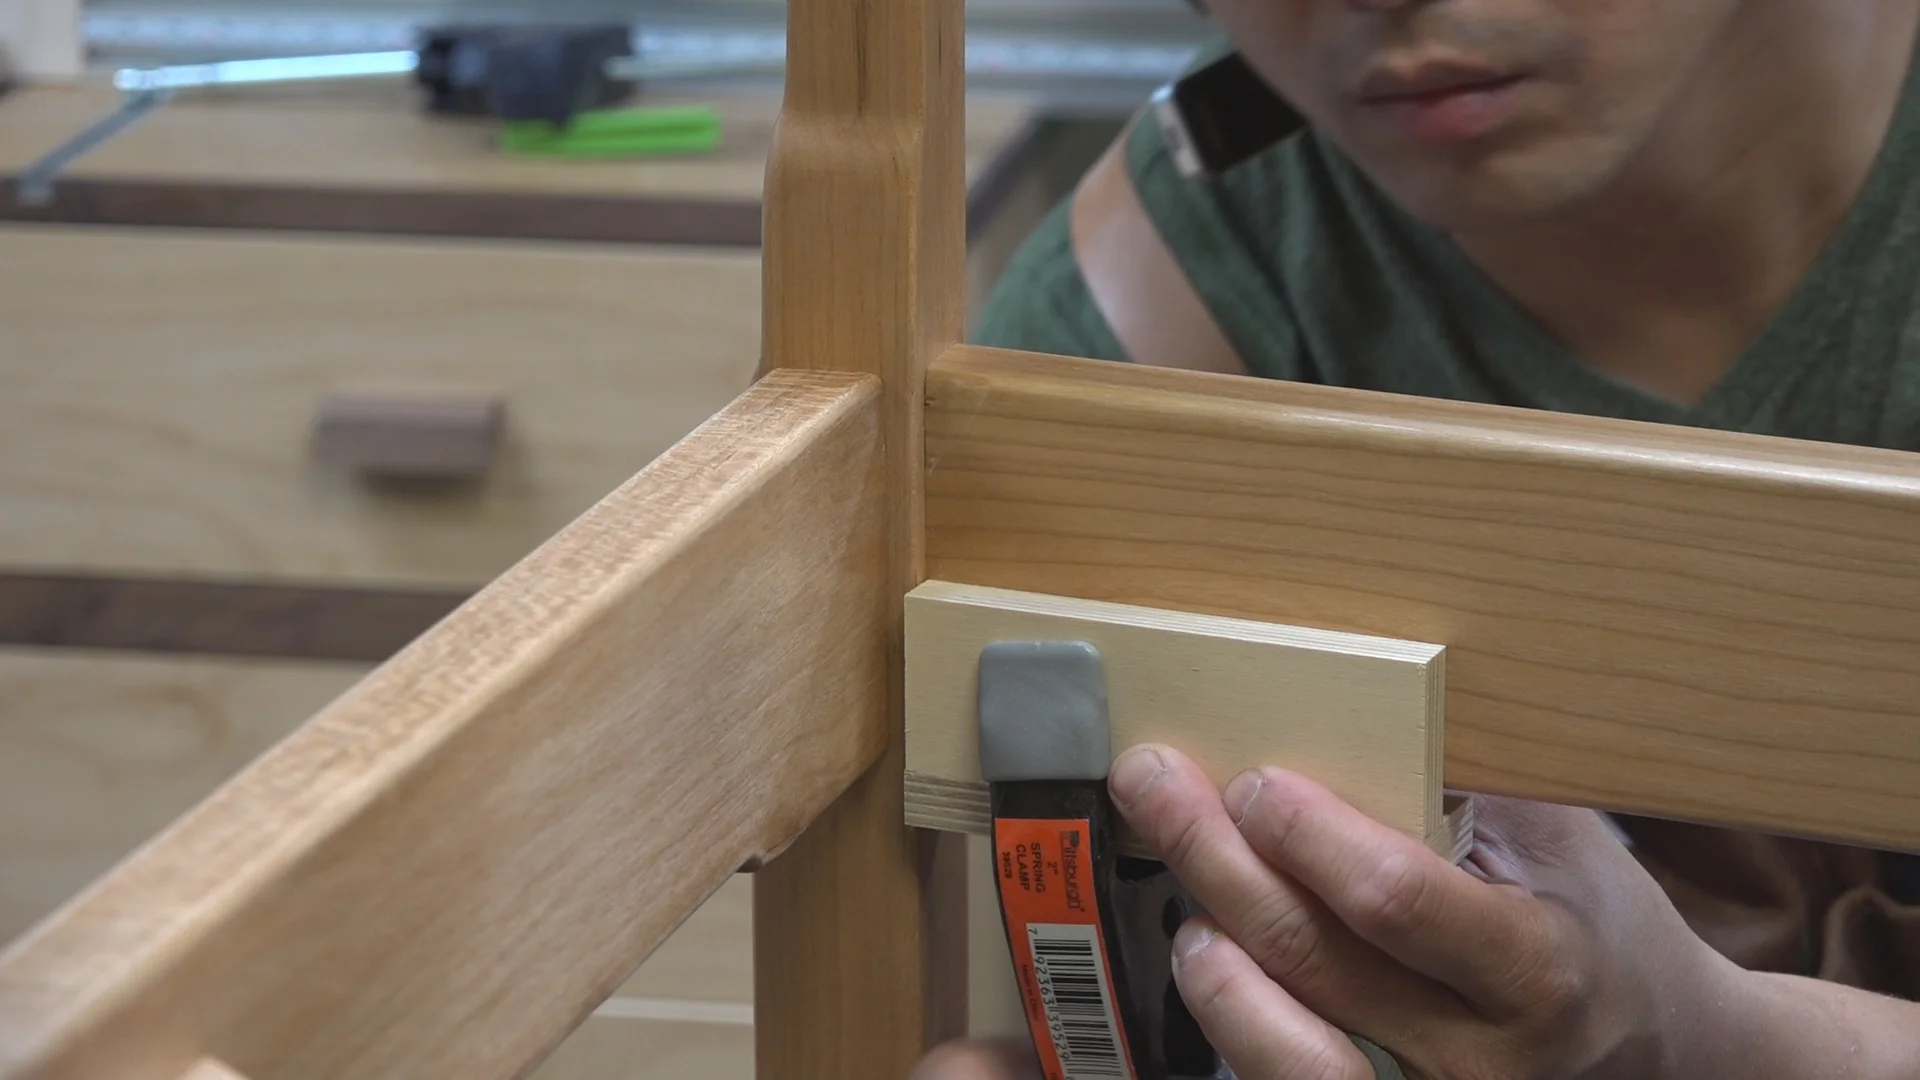
A jig and spring clamp set to the proper height to attach the corner blocks.
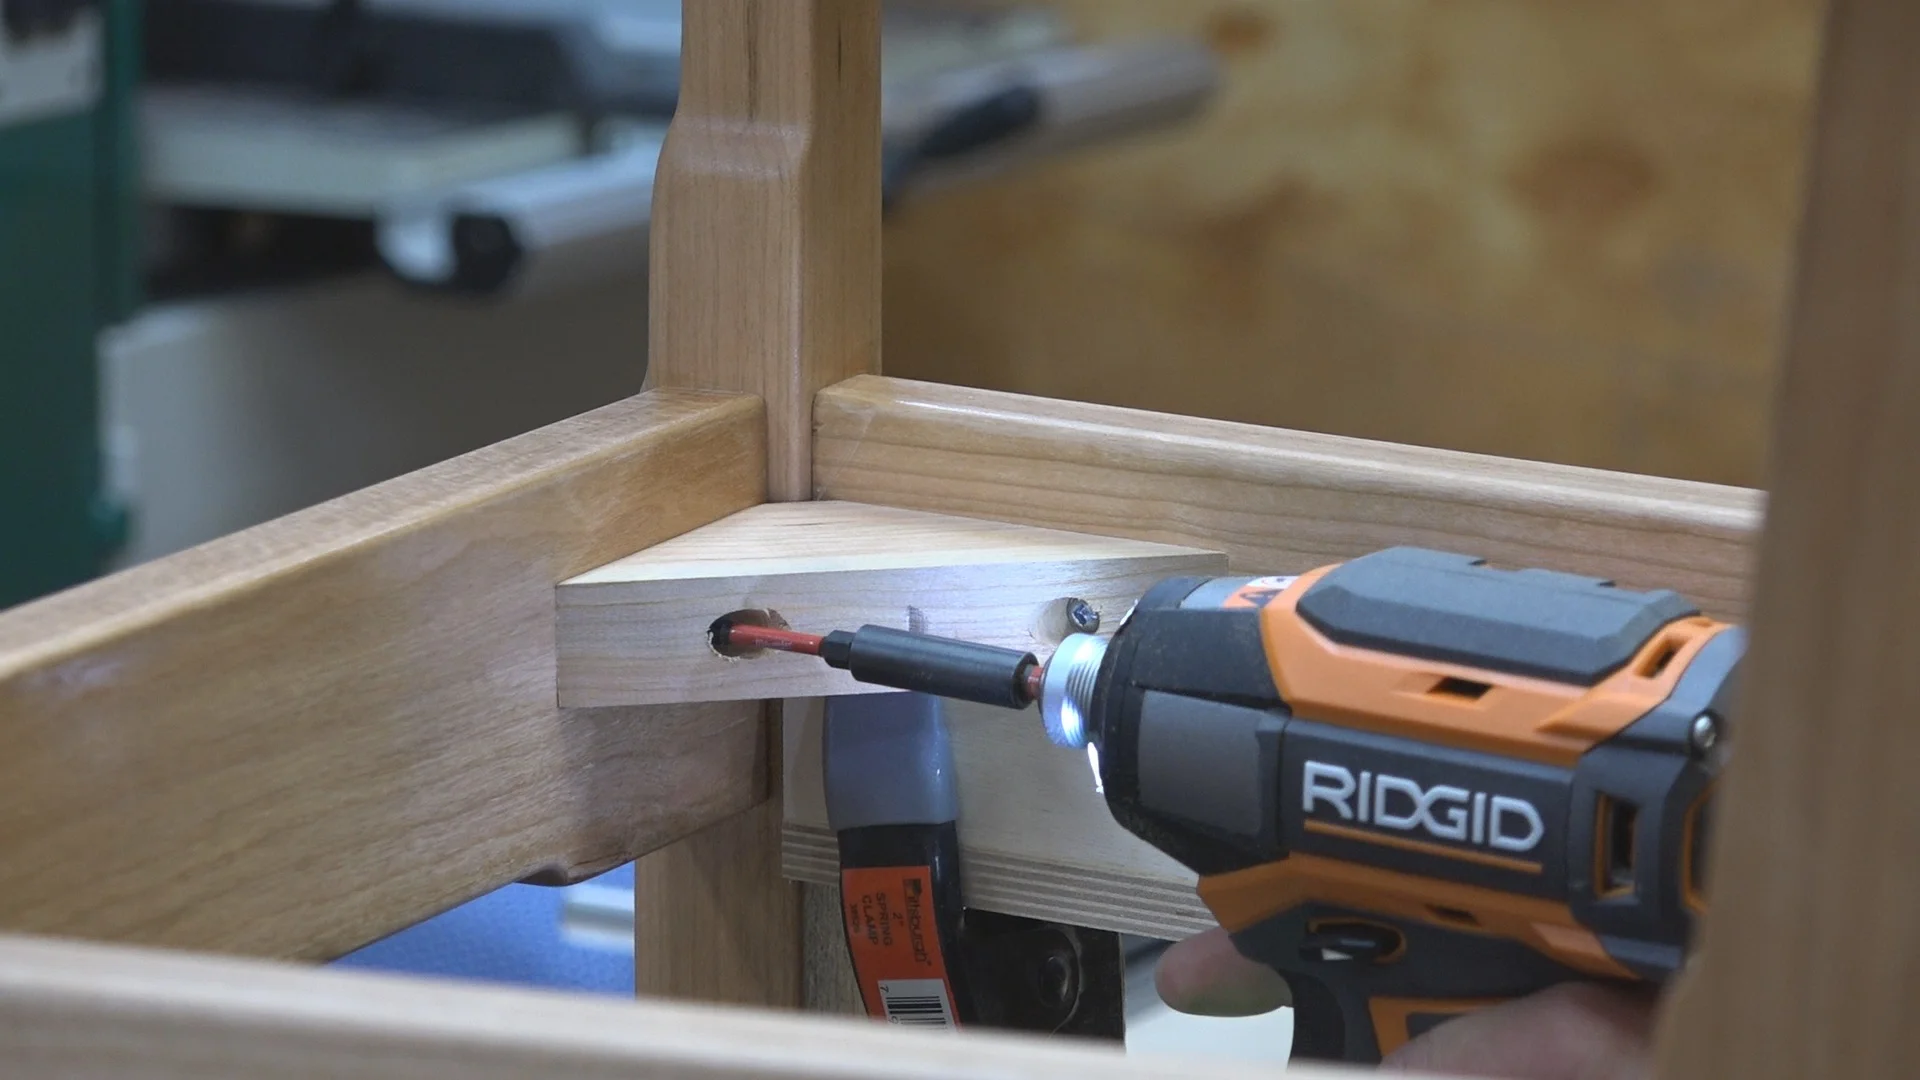
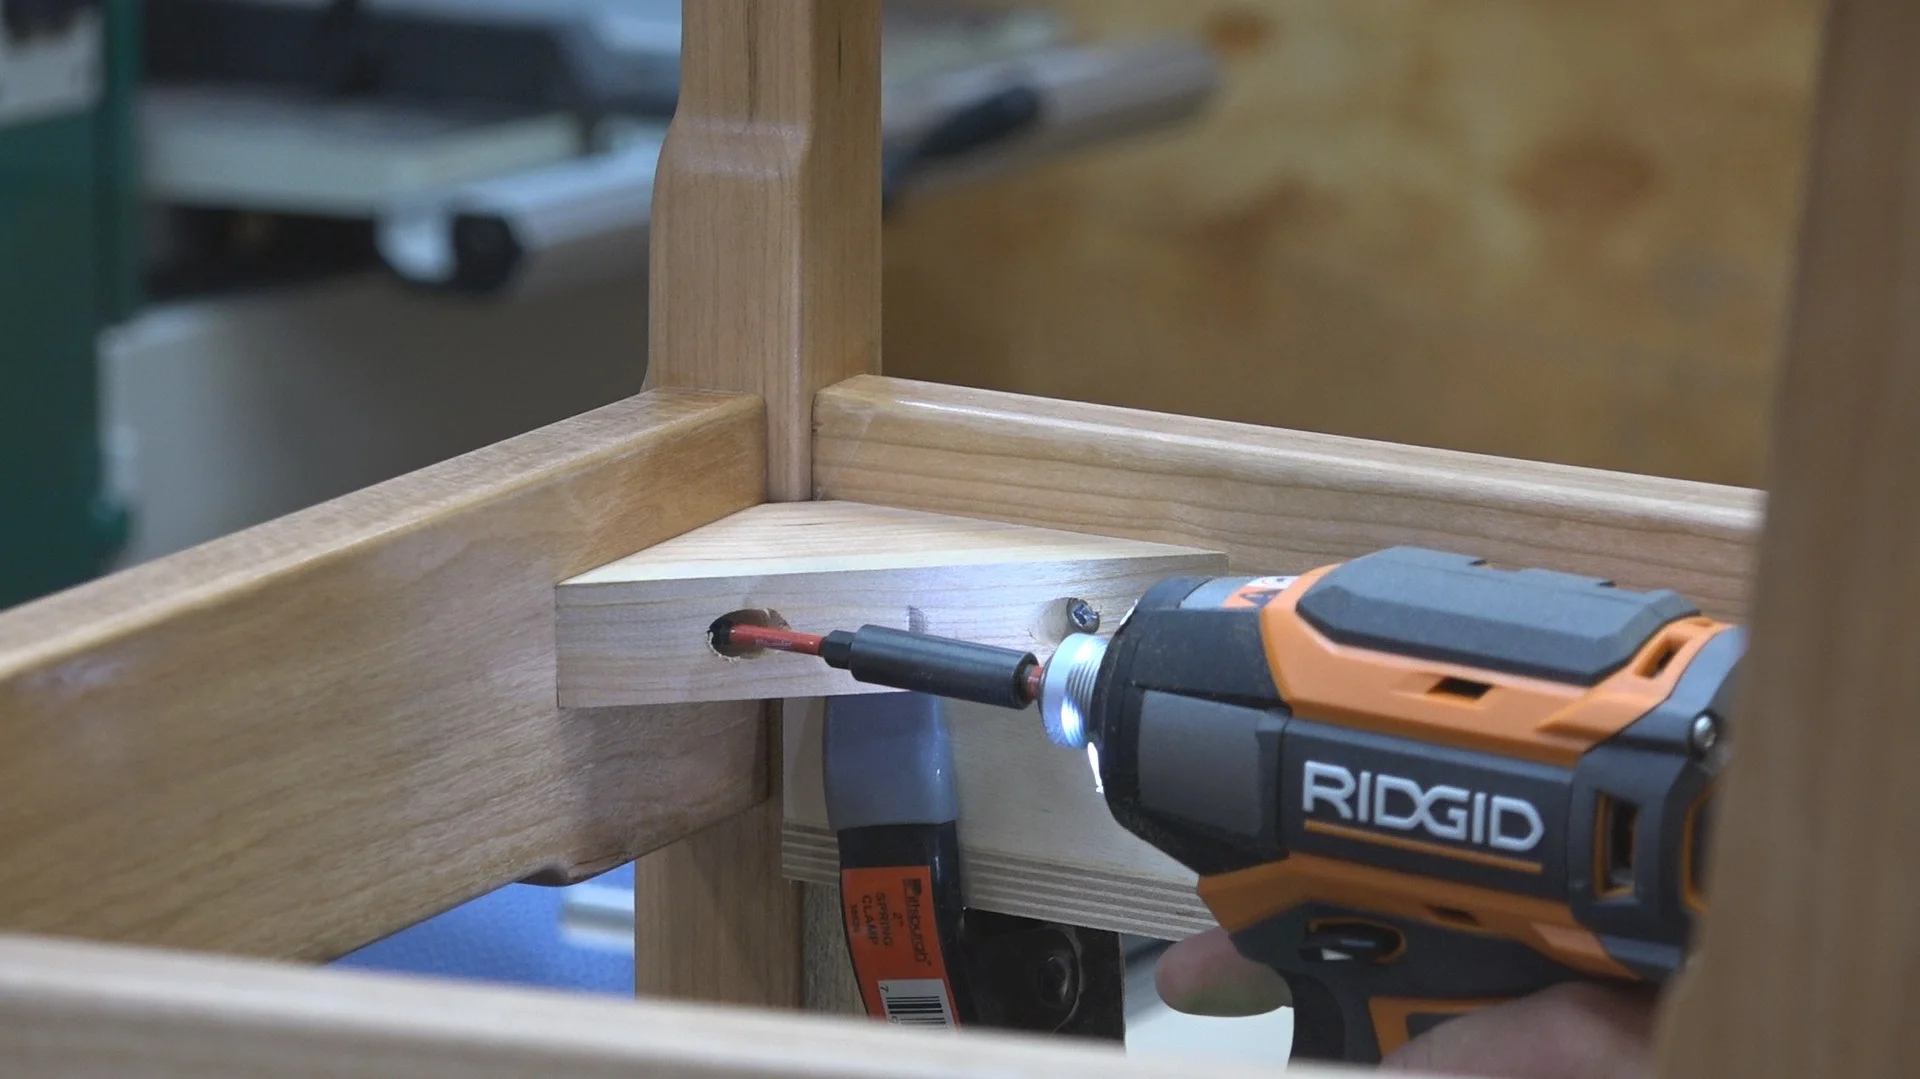
I screwed the corner blocks into place using a 1-1/2” washer head screw (Kreg brand screw). I used the Ridgid OCTANE 18V Hammer Drill/Driver and 6-Mode Impact Driver to predrill and drive the screws. The hammer drill/driver produces a whopping 1,300 in.-lbs. of torque which is way more than I need for this operation. The impact drive produces 2,400 in.-lbs. of torque which is also way more than I need to drive a 1-1/2” screw. What I really liked about the impact driver are the 6 different modes available for increased versatility (3 Speeds and 3 Specialty Modes). This ensures that the impact drive is providing the proper amount of torque so that you don’t over drive or under drive a screw. I used the Auto Stop mode which prevents the screw from being over tightened. It worked perfectly.
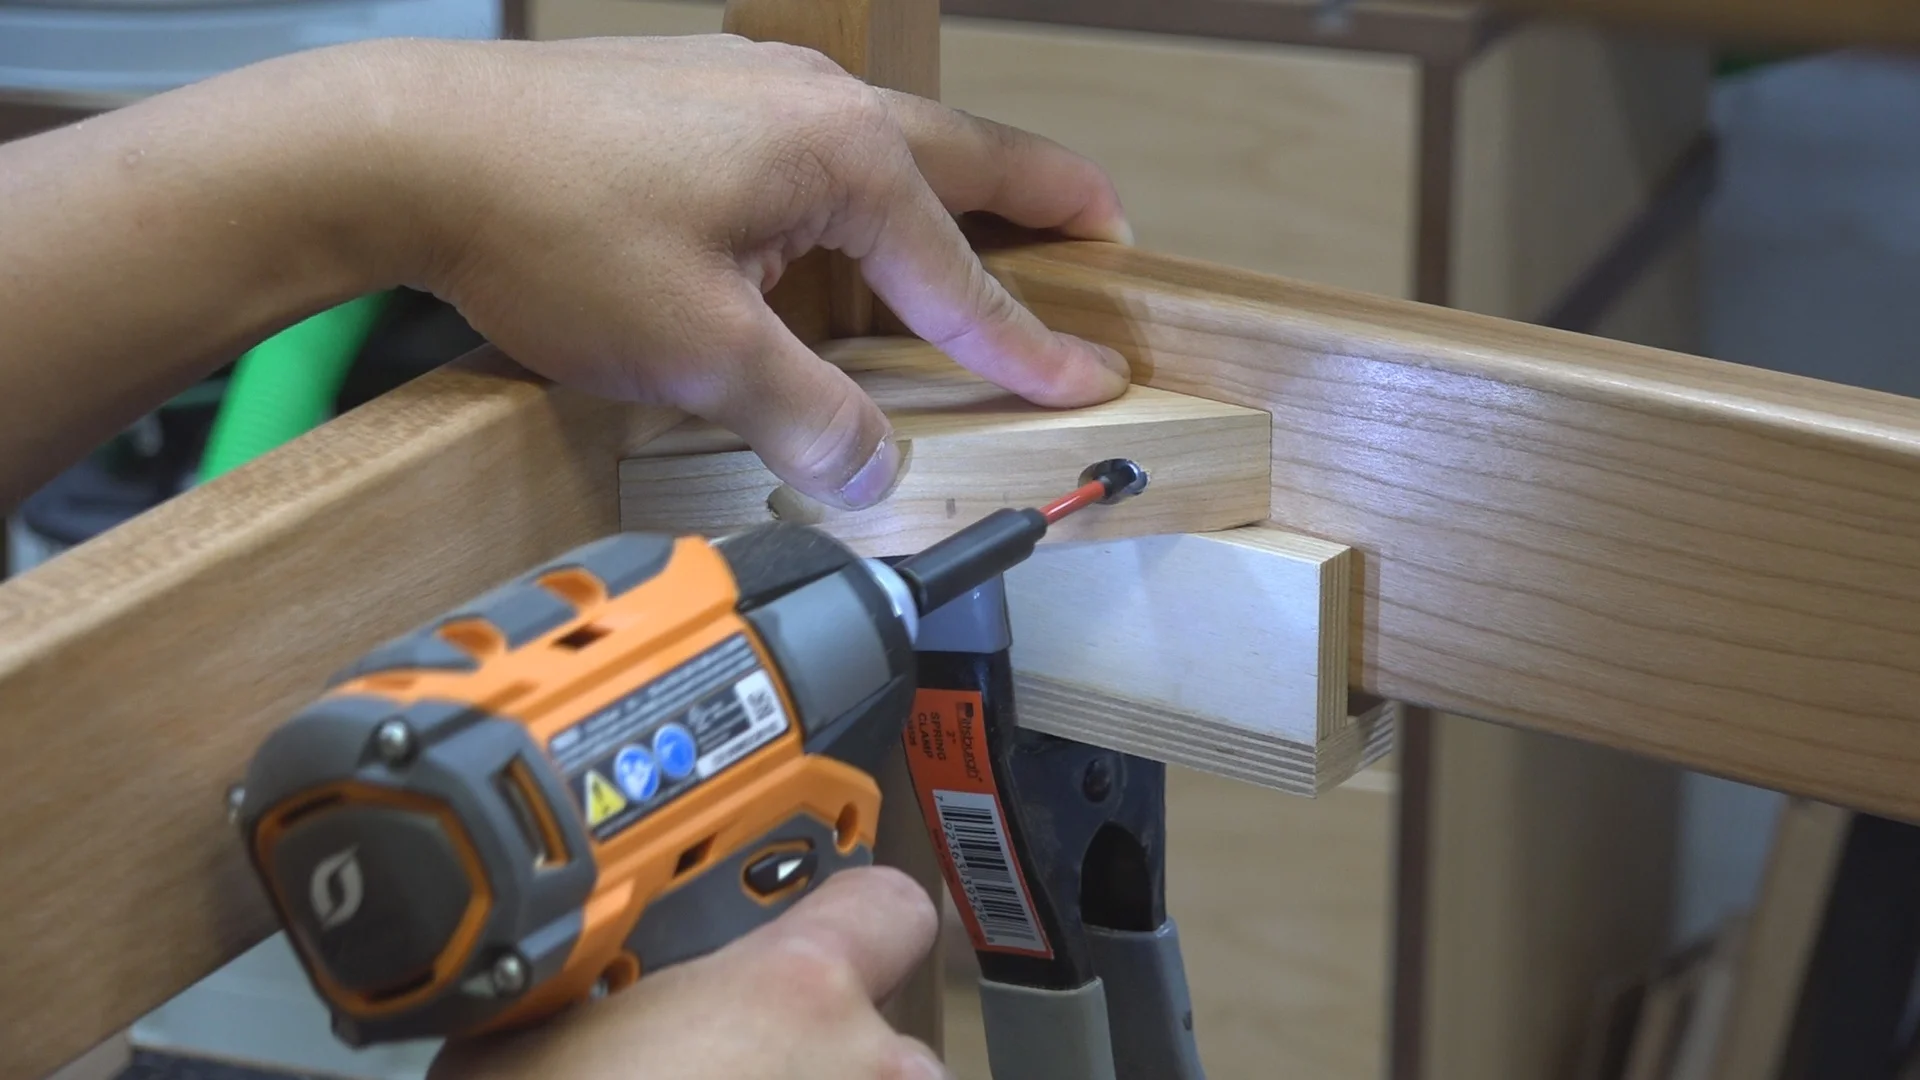
I pre-drilled and drove the screw in for the corner blocks Using the Ridgid Octane 18V Hammer Drill/Driver and 6-Mode Impact Driver.
The back corner blocks were cut at 53 degrees but also had to be cut to accommodate the curve of the back rail. I traced the inside curve of the back rail on the corner block and then cut the curve on the bandsaw. I then sanded the curve to the drawn line on the disc sander.
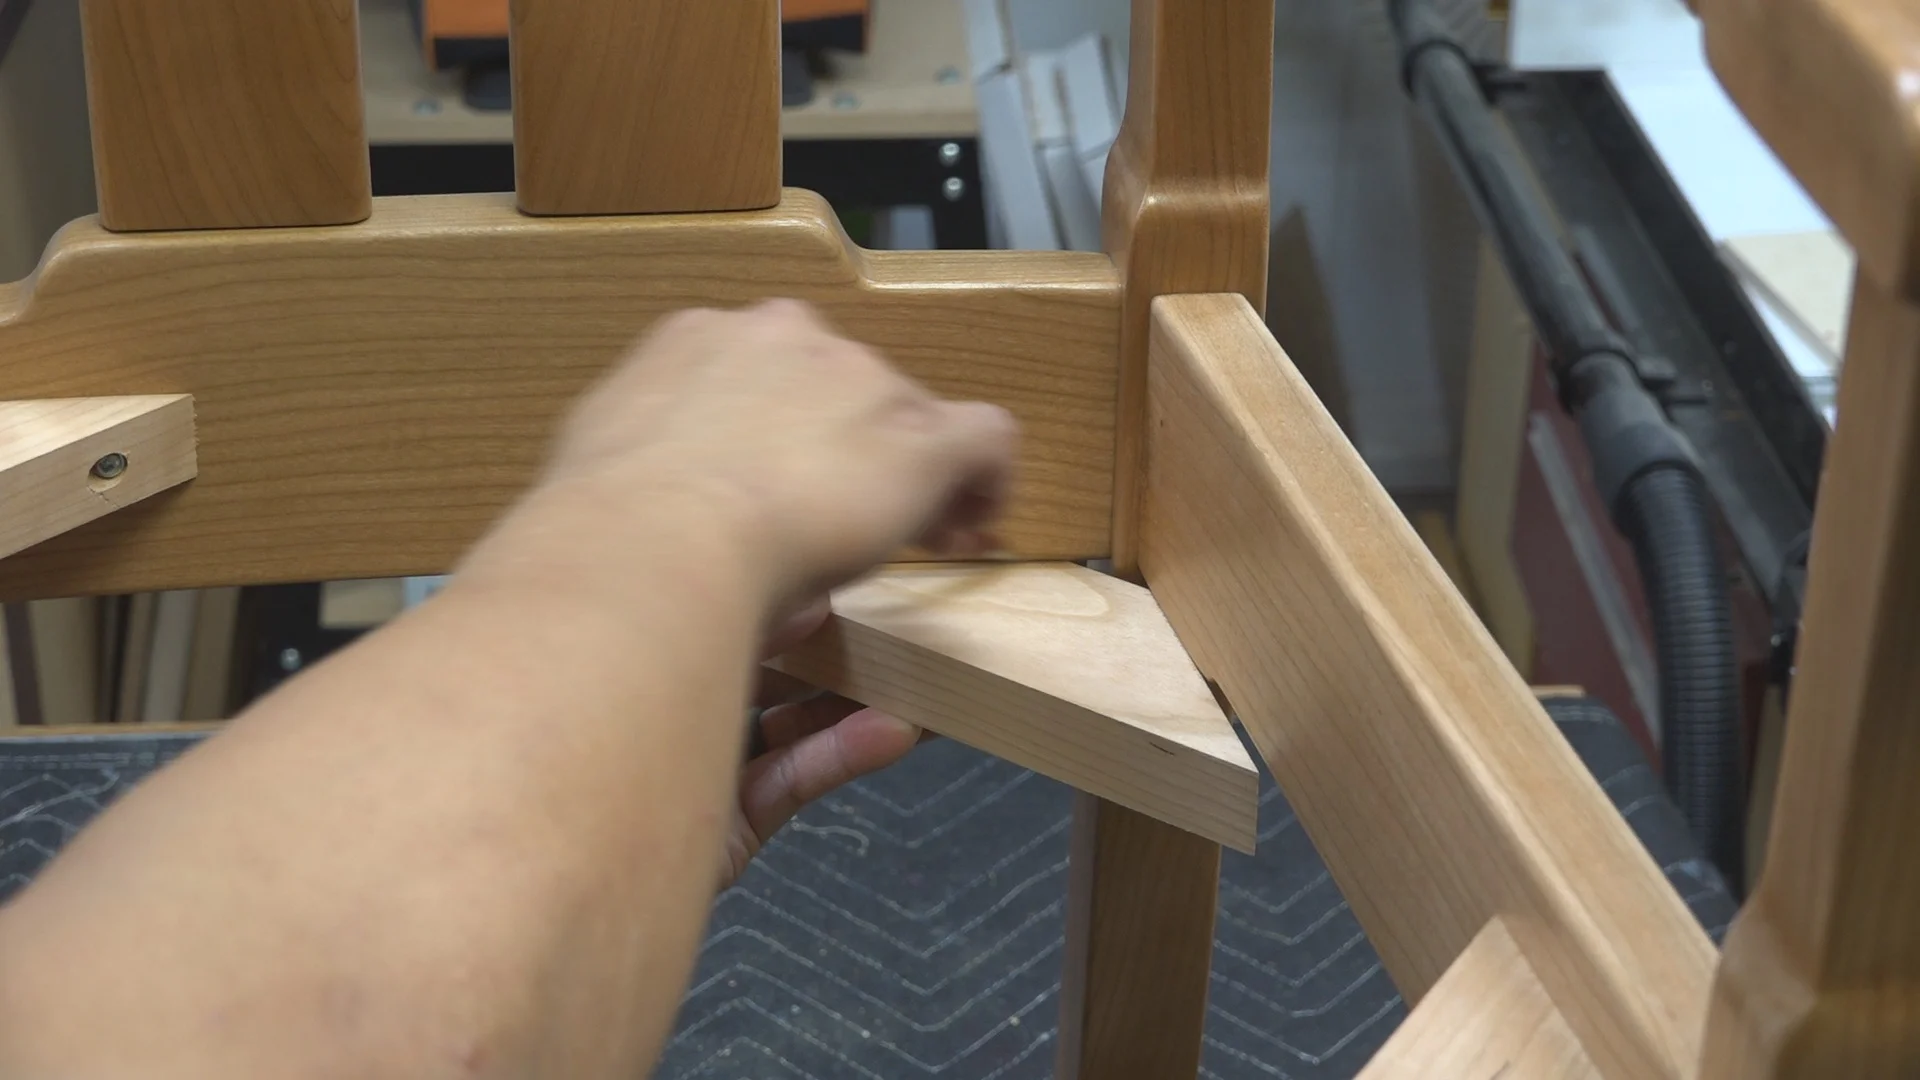
I traced the curve of the back rail.
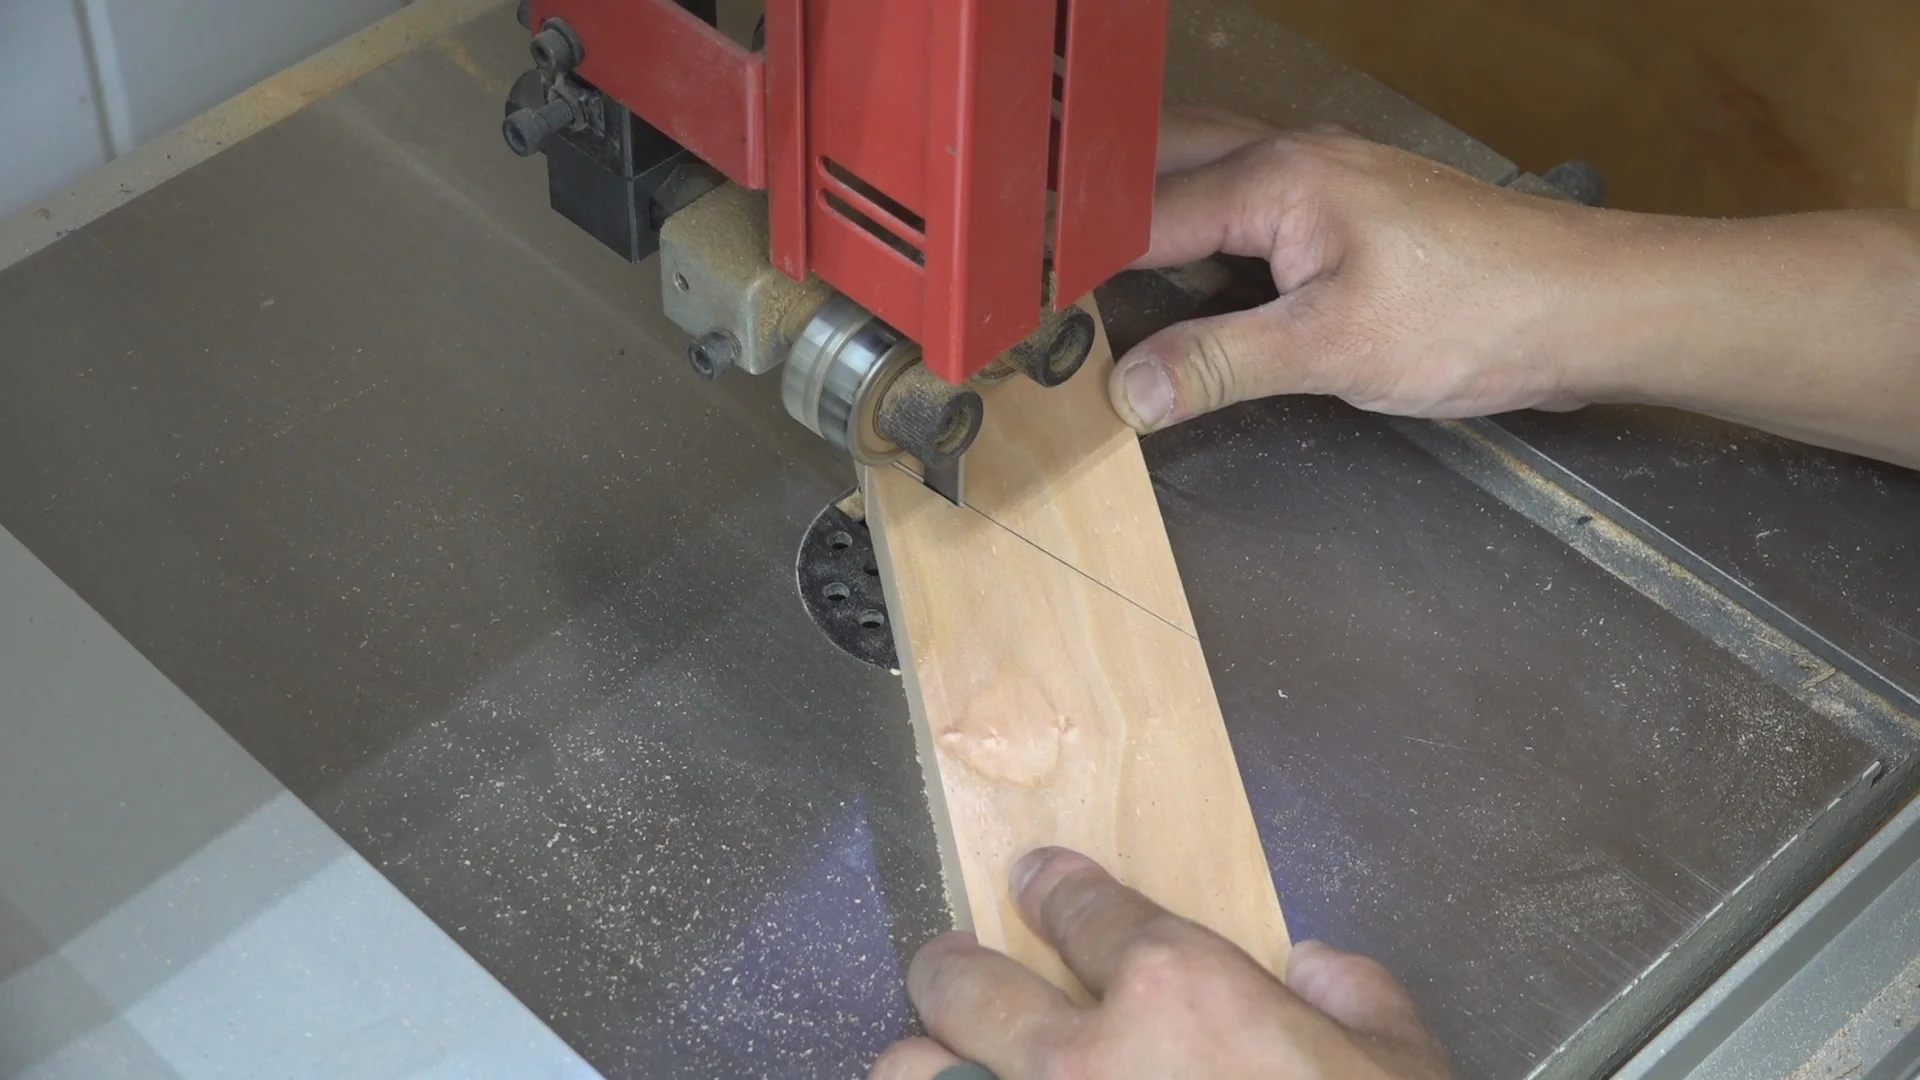
I cut the traced line on the bandsaw.
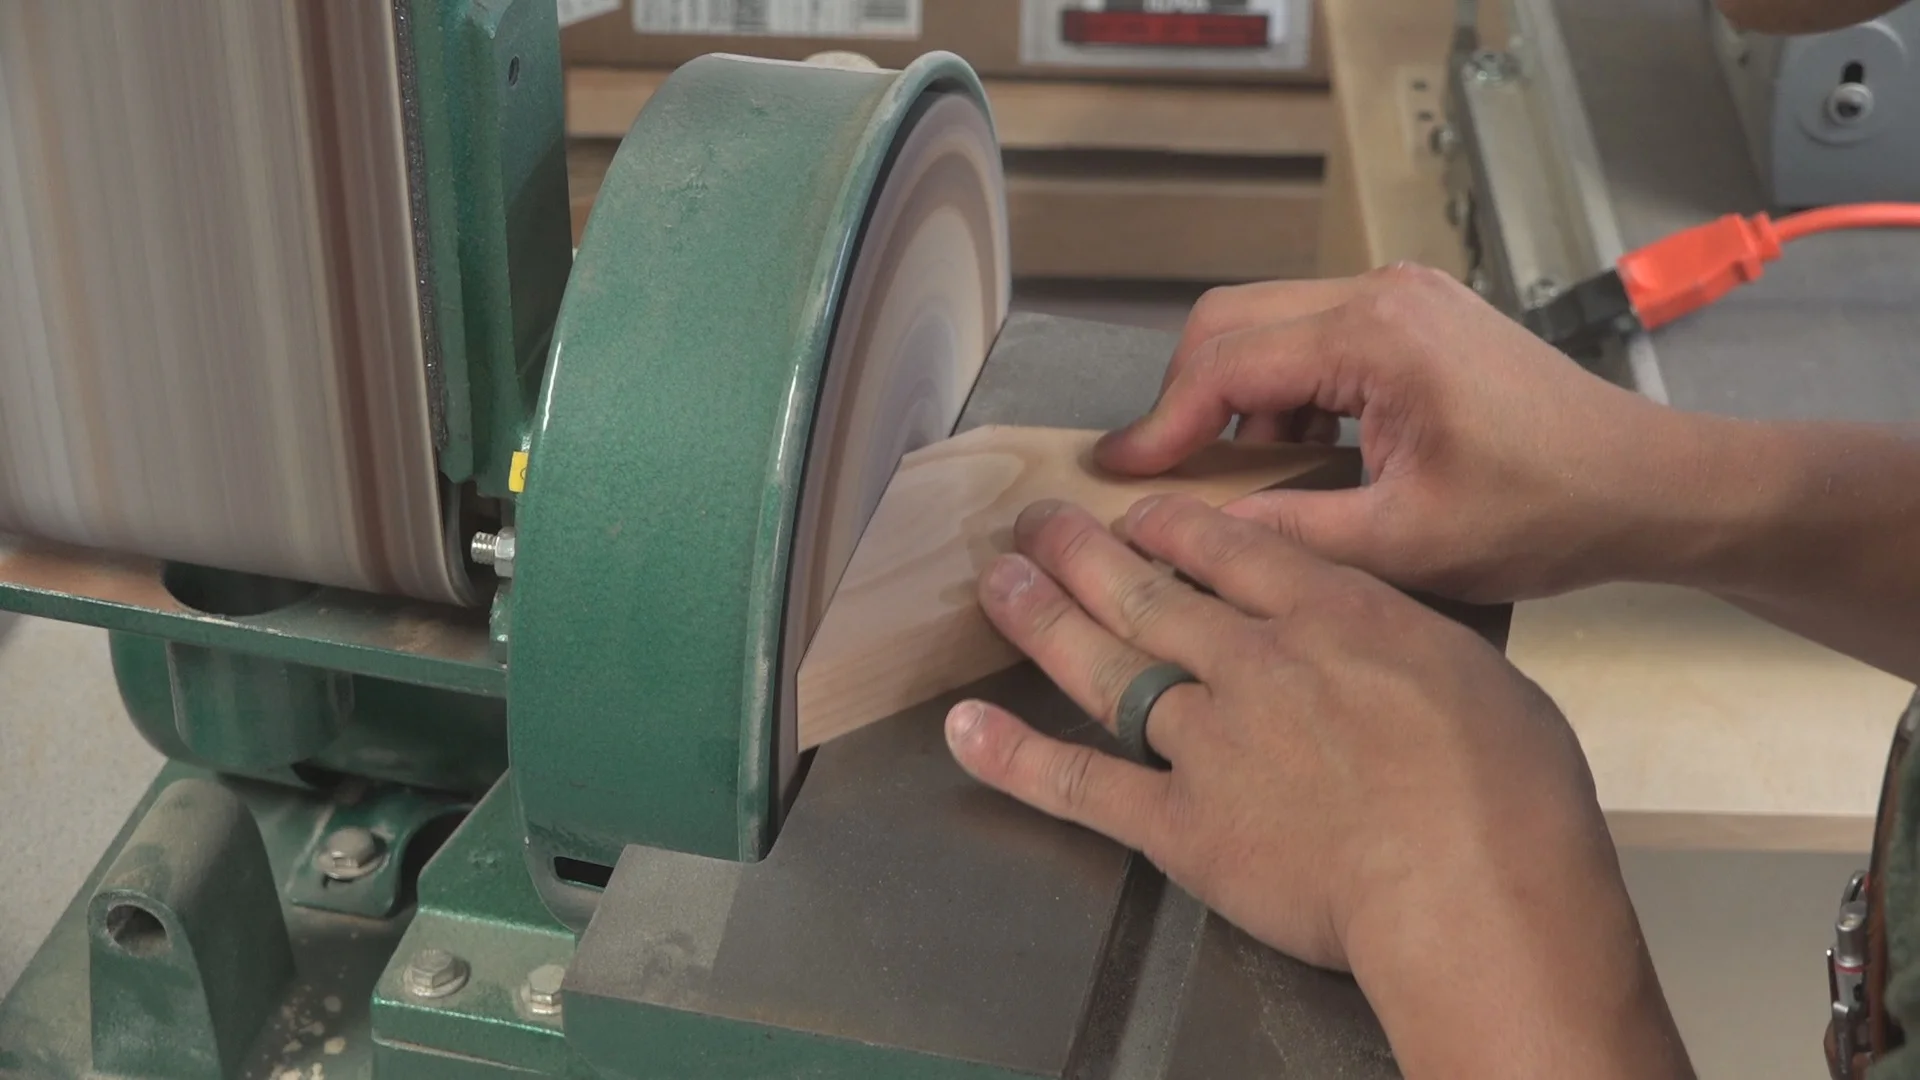
I used the disc sander clean up the bandsaw marks to get a perfect fit.
Lastly, I attached the back corner blocks in the same way as before by using the clamping jig and the Ridgid Octane Hammer Drill/Driver and Impact Driver.
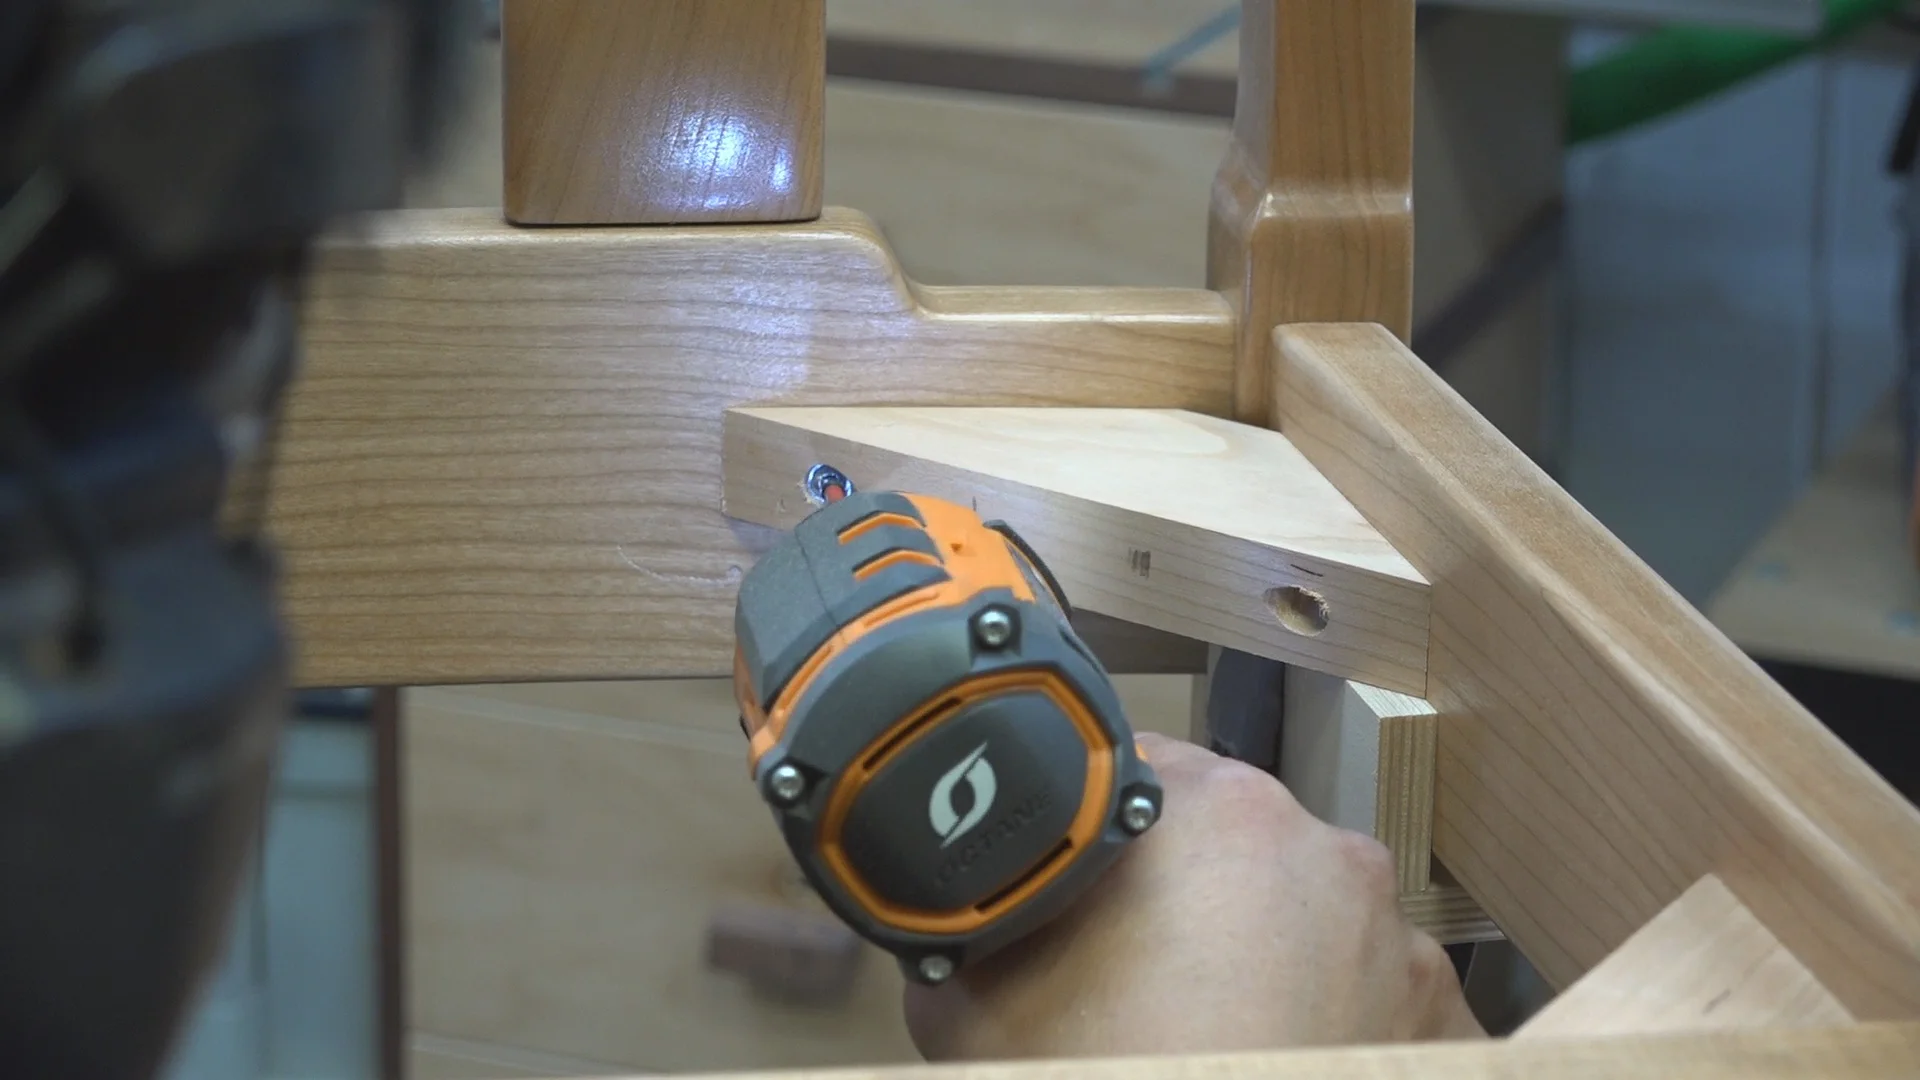
Attaching the back corner blocks. The jig and spring clamp establish the height. I used the Ridgid Octane Hammer Drill/Driver and Impact Driver to set the screws to attach the corner blocks.
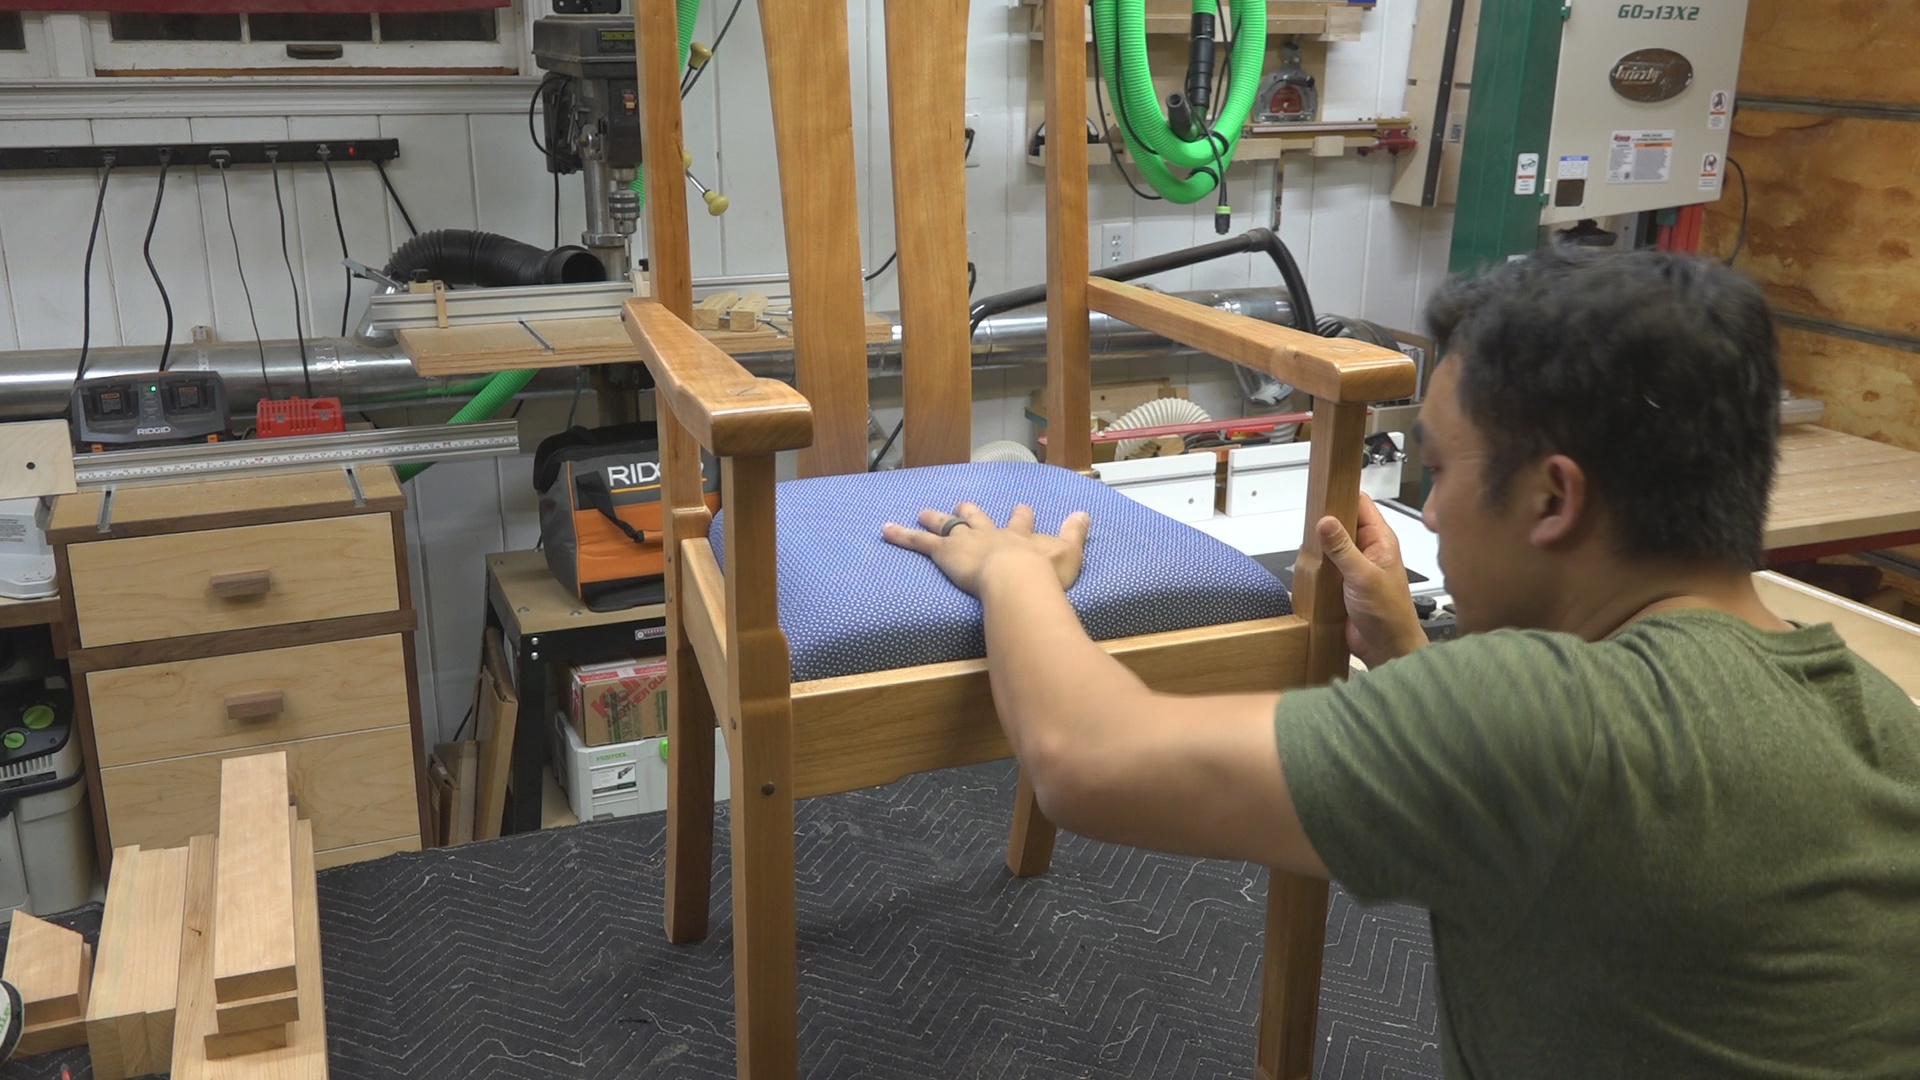
I used the prototype chair insert to test the fit of the corner blocks. I was very happy with the results.